Specifying the right aluminium profiles for automation often separates a reliable, high-speed assembly cell from a machine plagued by micro-vibrations and sensor drift. When mechanical engineers design industrial robotic positioning systems or multi-axis gantries, structural aluminium profiles for automation serve as the physical datum for every moving axis. Treating these custom aluminium extrusion linear rails as generic framing commodities invites premature bearing wear and missed cycle times.
A linear motor carriage accelerating at three gravities does not care how clean a CAD model looks on screen. It reacts to every micron of twist, thermal expansion, and elastic deflection in the underlying beam. Understanding how alloy metallurgy, cross-sectional geometry, and extrusion tolerances interact allows system integrators to build faster, stiffer, and more repeatable automated machinery.
Walk through a semiconductor packaging plant or a lithium-ion battery assembly line, and you will often encounter extruded aluminum structures on dynamic axes. Engineers choose aluminium profiles for automation because modern throughput targets demand low moving mass paired with predictable structural stiffness. However, replacing steel with aluminum requires a clear grasp of structural mechanics rather than simple part-for-part substitution.
In a multi-axis pick-and-place gantry, the X-axis and Z-axis beams represent dead weight carried by the Y-axis drive motors. According to Newton’s second law, cutting the mass of a moving bridge directly reduces the inertial torque required for a given acceleration. Reducing moving mass may help improve acceleration performance, while motor sizing, settling time, and resonance avoidance must be evaluated for the complete system including its loads, stiffness, natural frequencies, and control tuning.
Aluminum has a density of approximately 2.70 g/cm³, roughly one-third the density of carbon steel. When designed with a high-inertia hollow cross-section, an aluminum linear rail resists bending loads while keeping the moving carriage assembly light. This high strength-to-weight ratio keeps inertial forces low, preventing overshoot when an optical inspection head stops over a circuit board.
Welded steel structures look deceptively economical during initial raw material estimates, yet their hidden processing costs can accumulate rapidly on the shop floor. Welding introduces localized thermal stresses that warp long structural tubes, and depending on the material, applicable code, and dimensional requirements, a steel frame may require stress-relief annealing in an oven before machining. Afterward, a large-bed CNC gantry mill may need to skim the mounting surfaces flat, adding time to the project schedule.
By contrast, precision aluminium profiles for automation emerge from the extrusion die with integrated mounting channels, keyways, and reference flats already formed. While extreme accuracy applications still benefit from light datum skimming, many automated transfer lines bolt linear guides directly onto precision-extruded aluminum tracks. Furthermore, when a production line changes product formats, bolted aluminum assemblies can be reconfigured in hours rather than scrapped, making them well suited for reconfigurable machine structures.
Every material selection involves engineering trade-offs, and aluminum’s primary limitation is its modulus of elasticity. At roughly 69 to 70 GPa, aluminum’s Young’s modulus is about one-third that of structural steel, meaning an identical cross-section will deflect noticeably more under the same static load. Additionally, aluminum expands at roughly 23 micrometres per metre per degree Celsius, nearly twice the thermal expansion rate of steel.
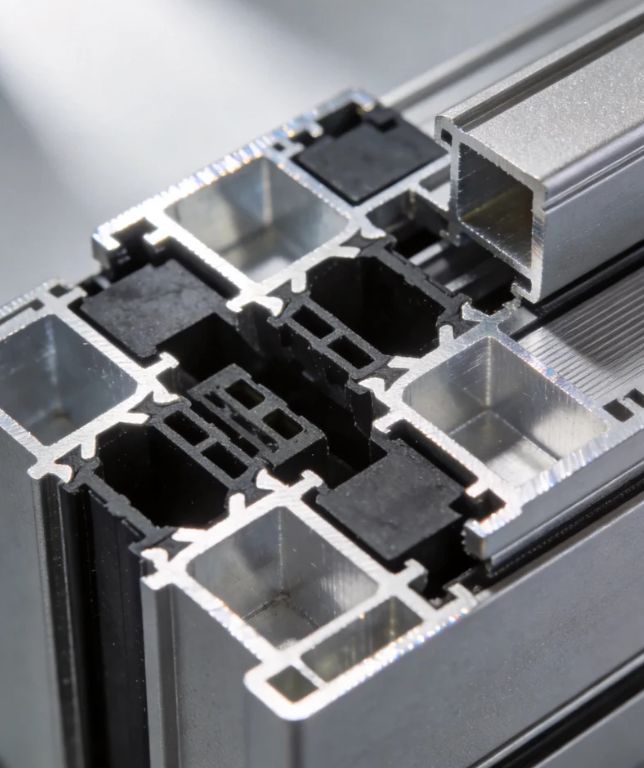
Seasoned machine builders overcome this elasticity not by wishing aluminum were steel, but by exploiting the freedom of the extrusion die. By pushing material outward from the neutral axis and increasing the profile depth, designers can raise the area moment of inertia substantially; calculate it for the actual cross-section to verify the improvement. A deeper, multi-chamber aluminum extrusion can approach the bending stiffness of a smaller steel tube while remaining considerably lighter.
Standard modular T-slot framing works admirably for machine guarding, ergonomic workbenches, and static conveyor supports. However, when a project involves high-speed linear actuators or direct-drive linear motors, standard square T-slot bars reach their mechanical limits. Purpose-built aluminium profiles for automation integrate the structural beam, guide rail seat, and motor housing into one unified profile.
In a conventional linear actuator assembly, an engineer bolts an adapter plate to a structural frame, bolts a linear motor housing to the adapter, and aligns two parallel rail tracks. Every bolted interface introduces a mechanical tolerance stack-up and a potential slip plane under vibration. Custom extrusion linear rails reduce these intermediate plates by forming the stator cavity and guide shoulders in a single extrusion pass.
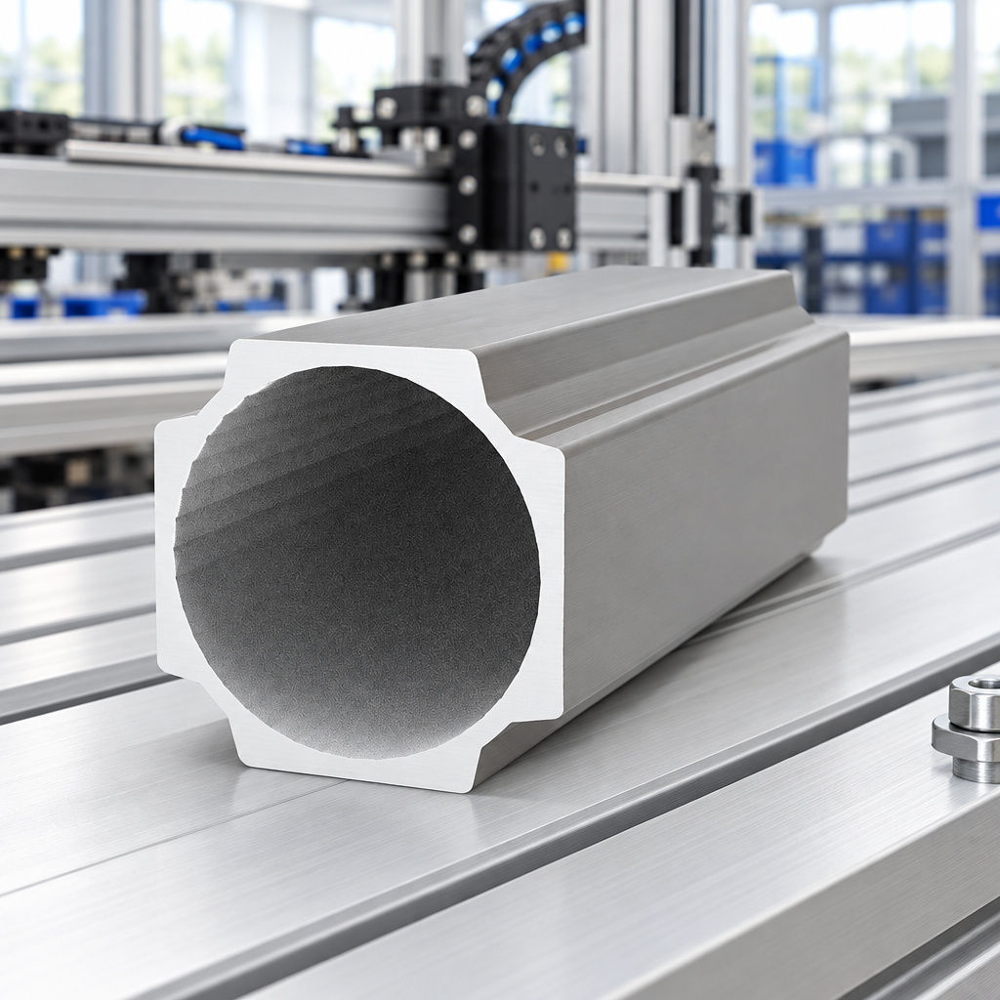
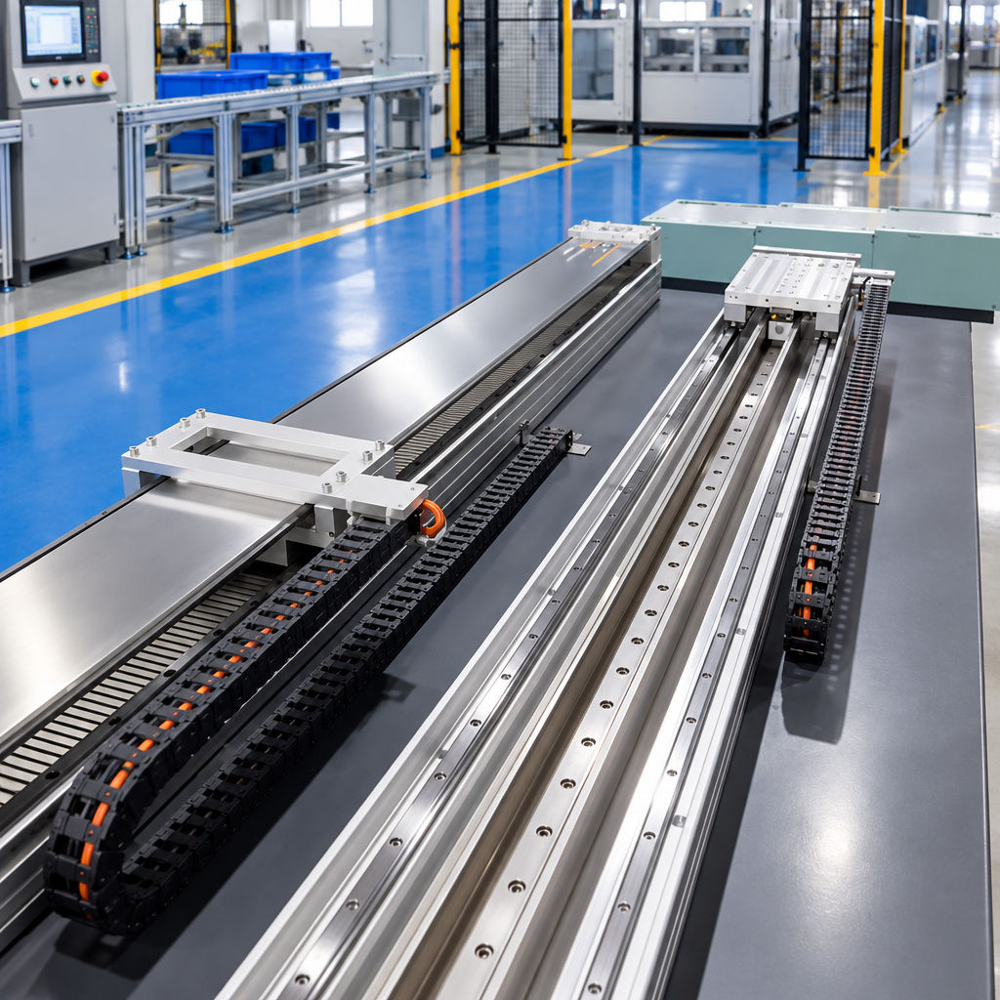
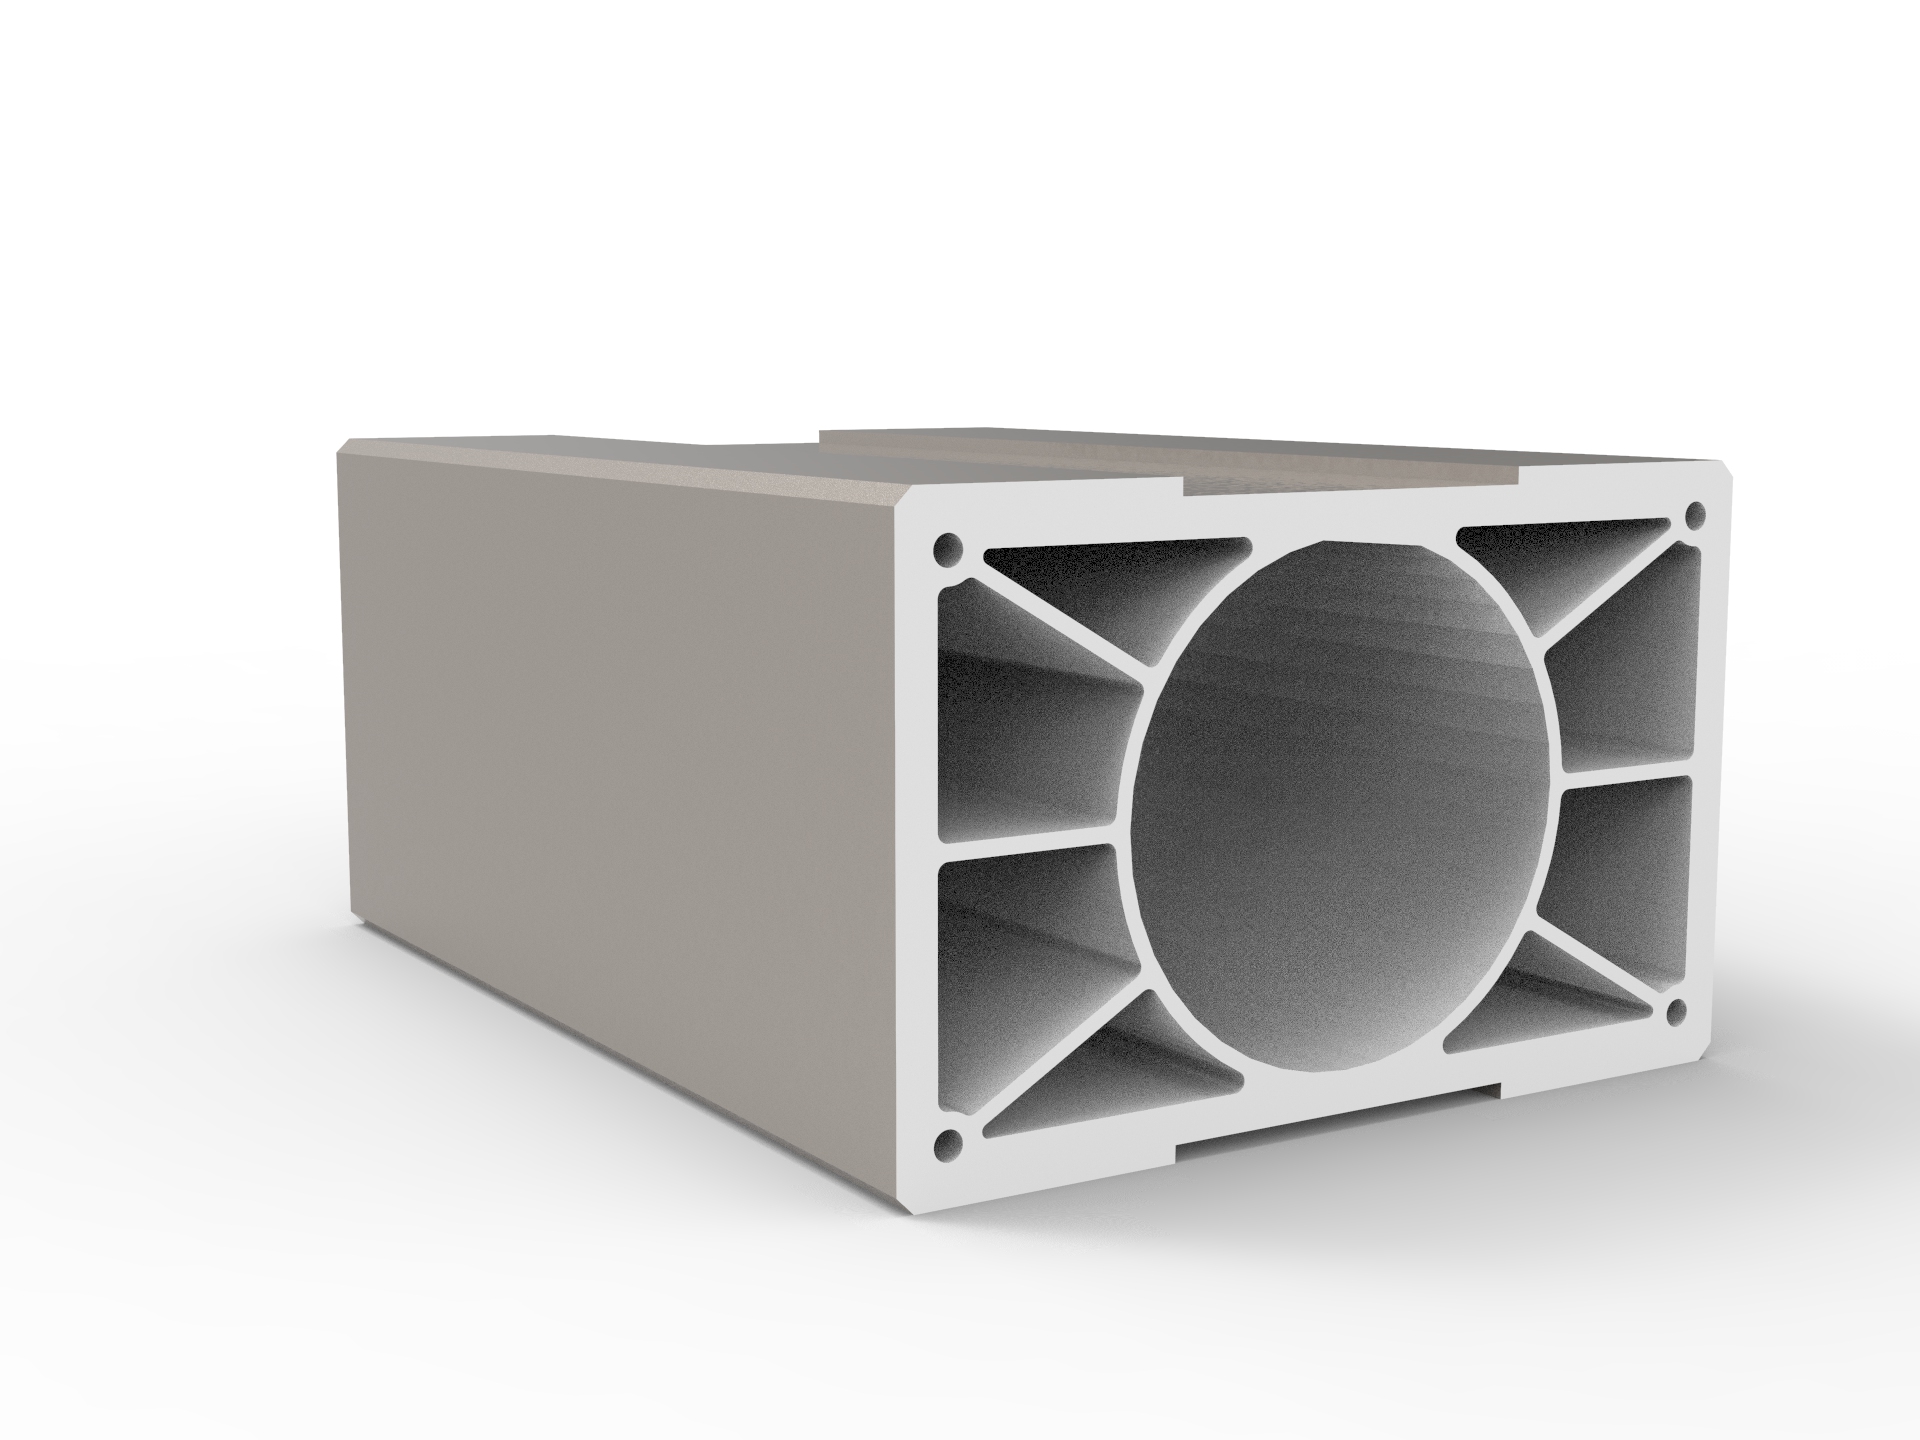
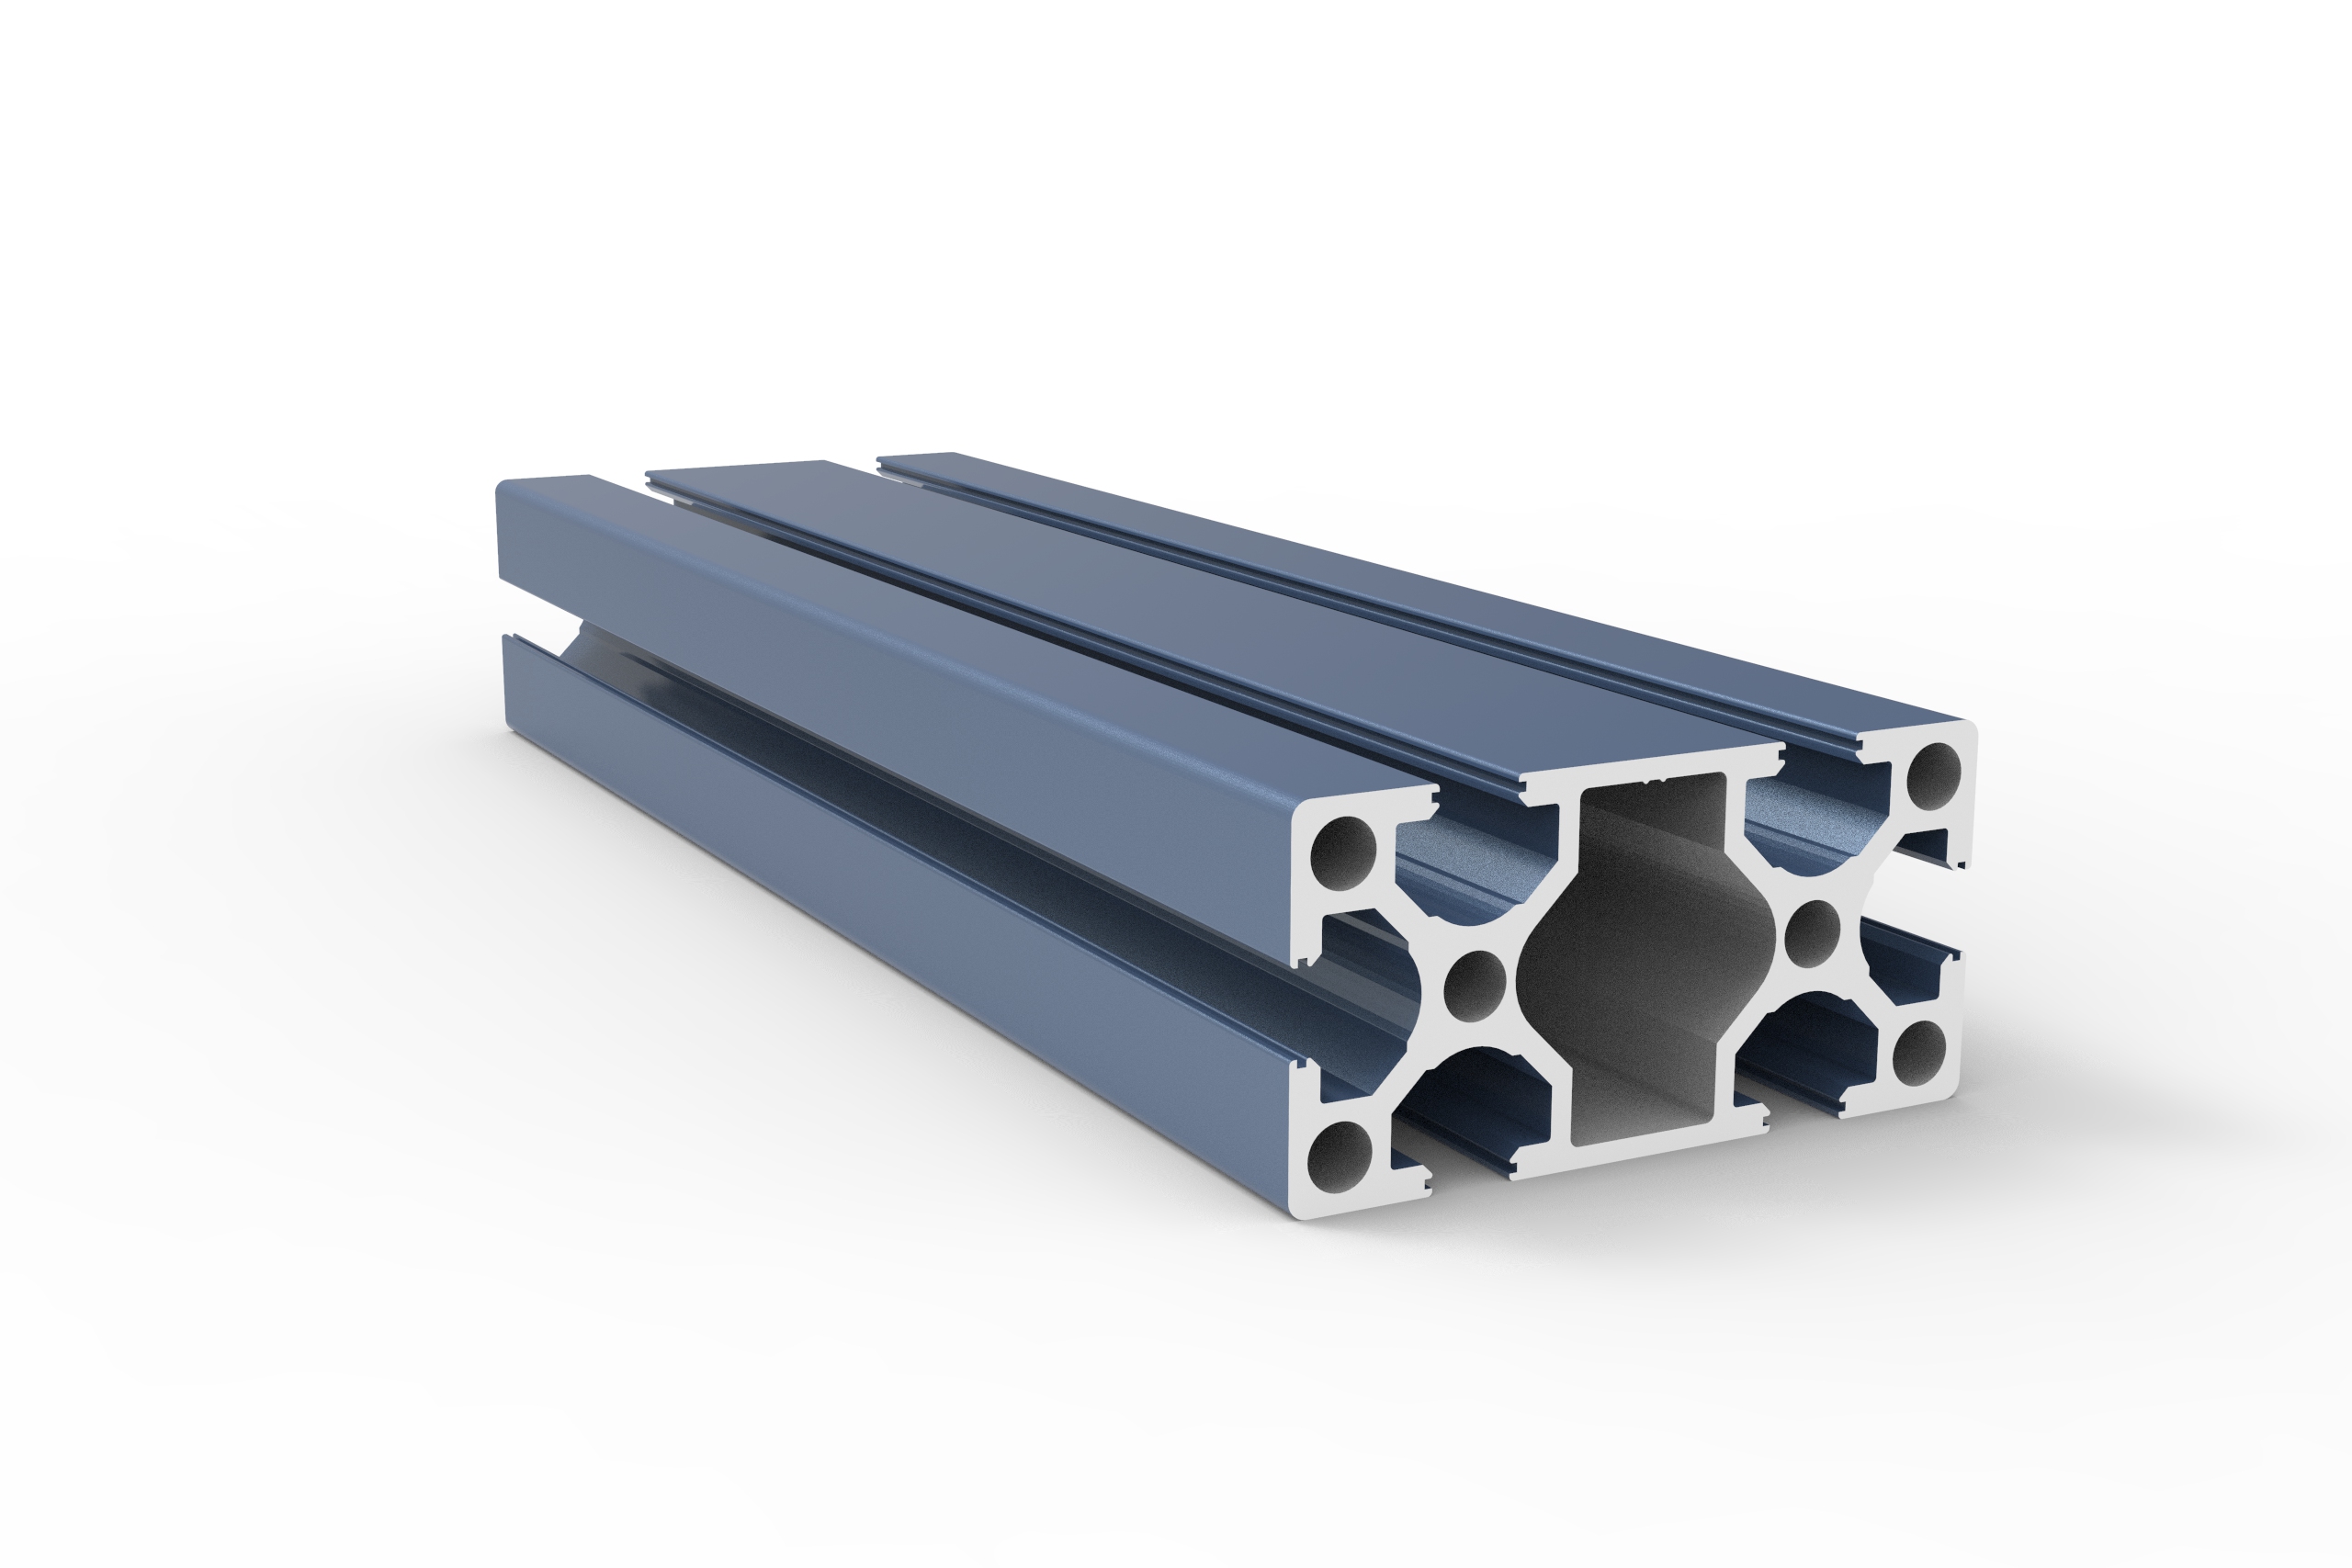
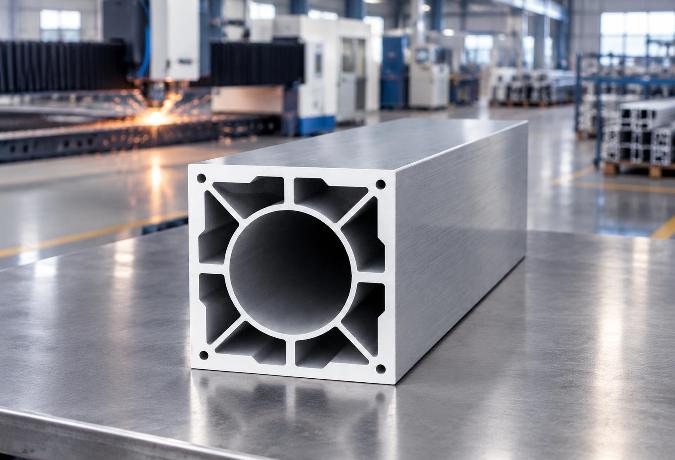
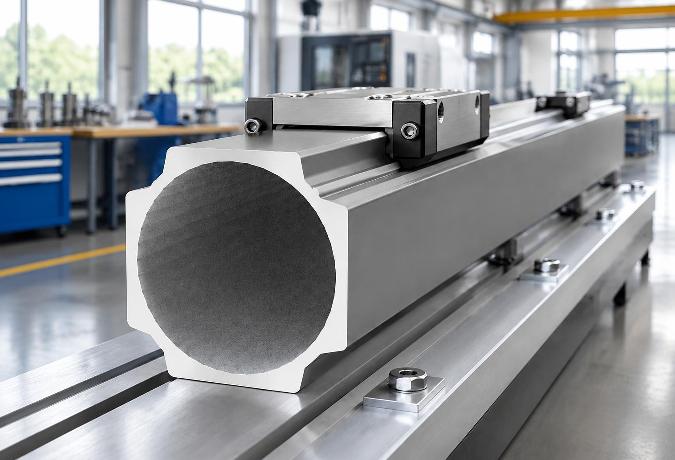
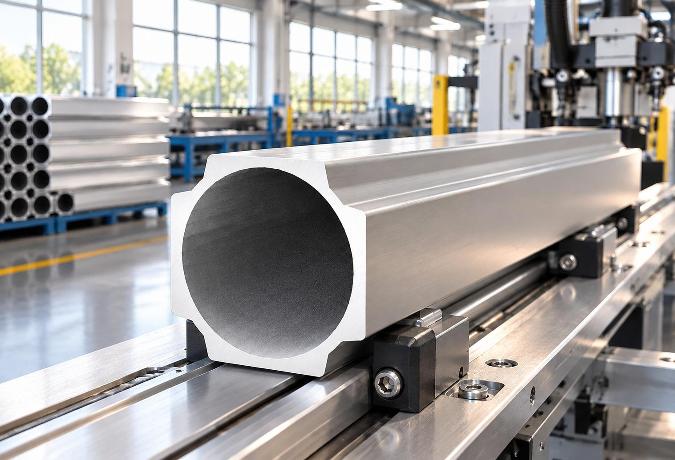
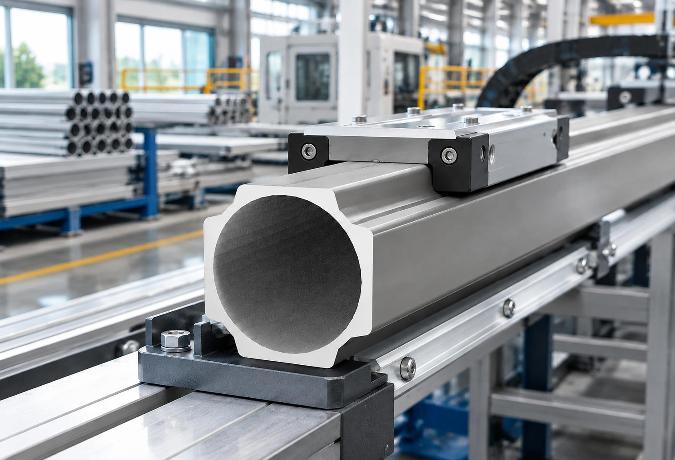
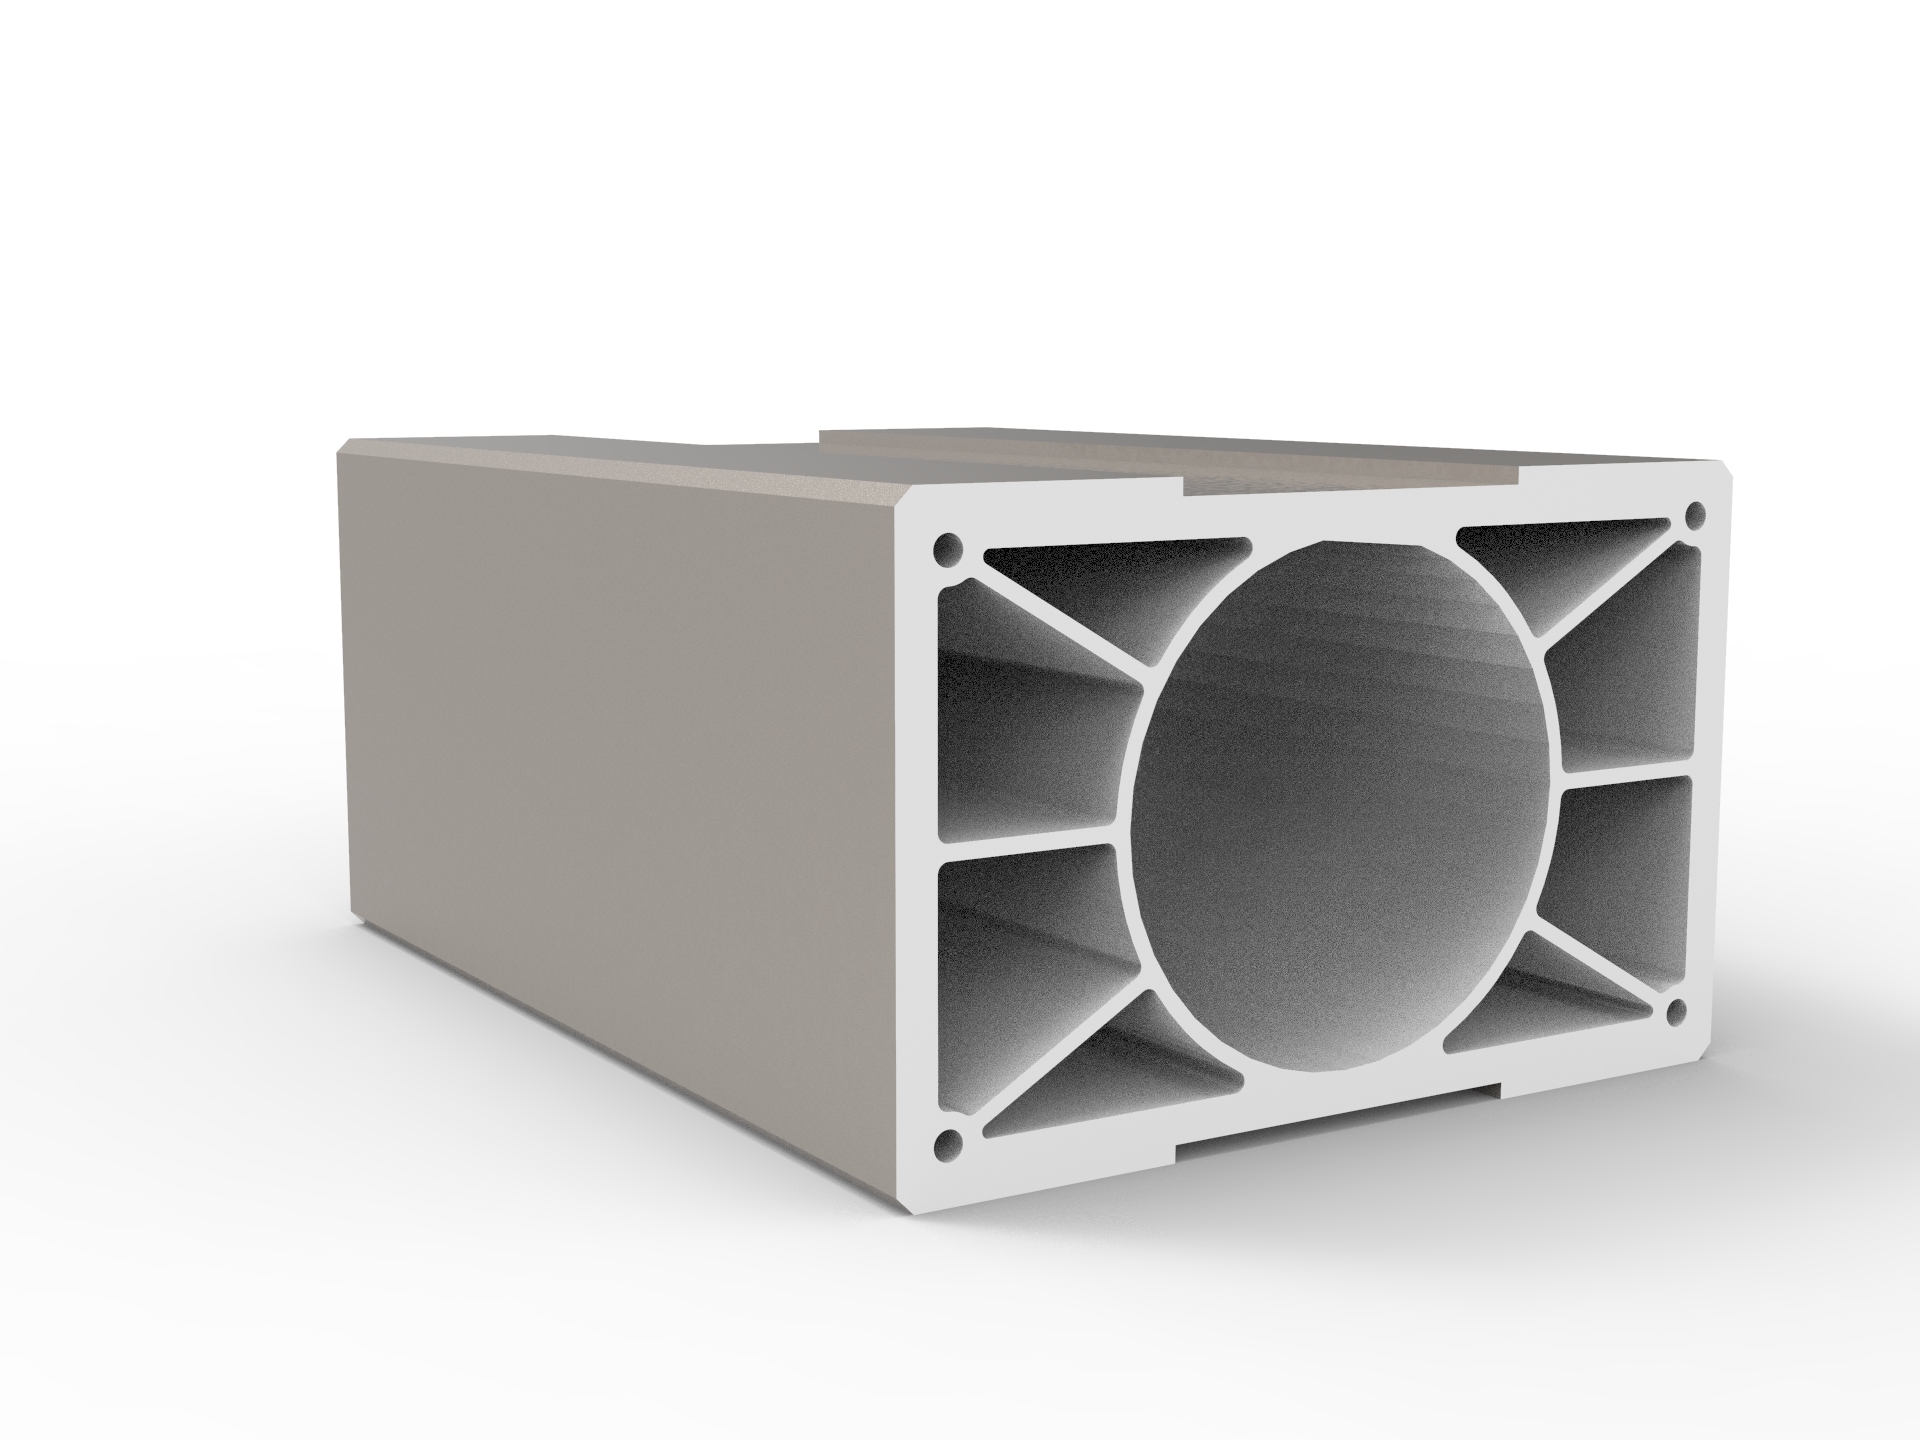
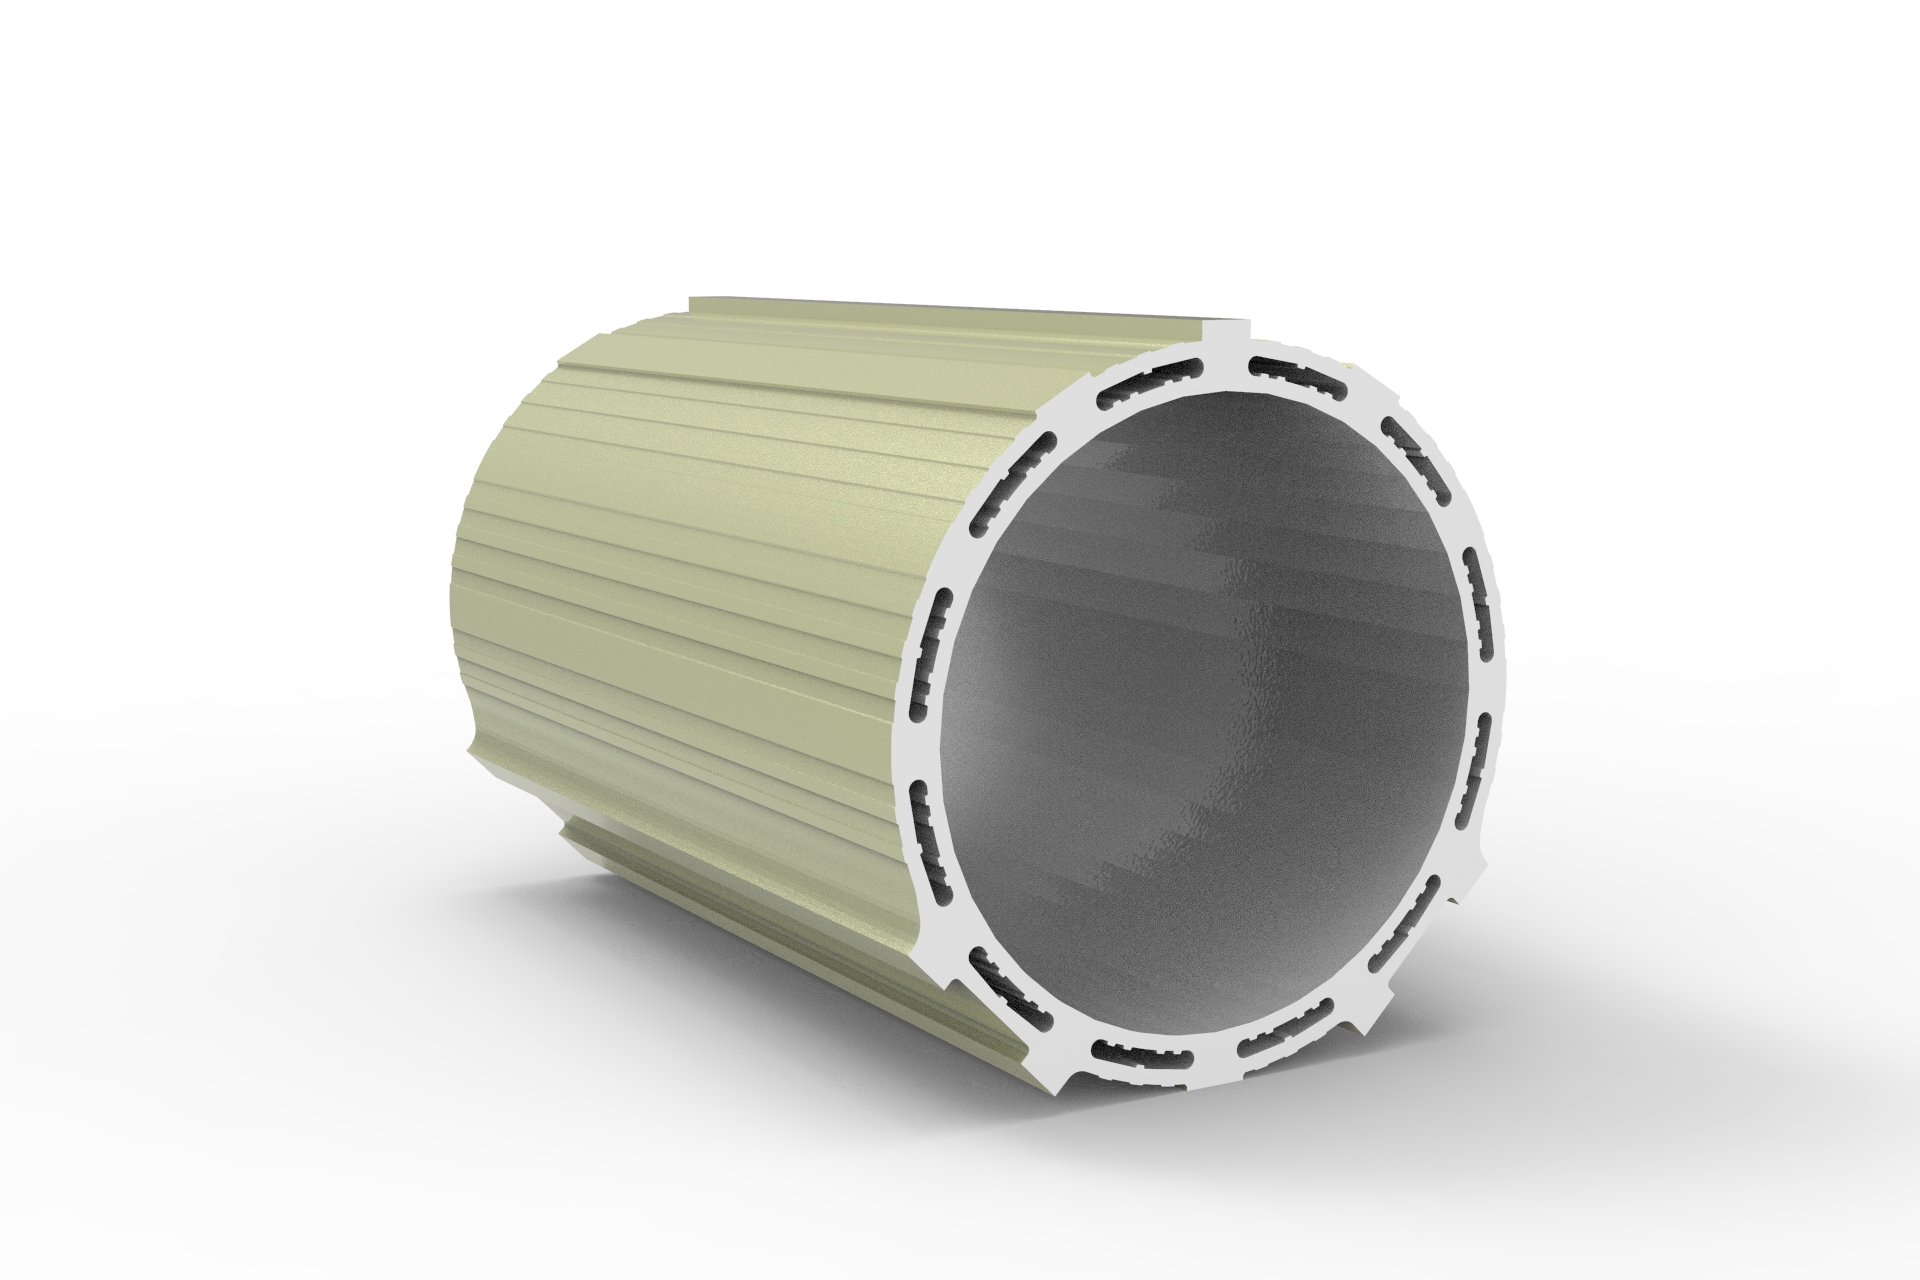
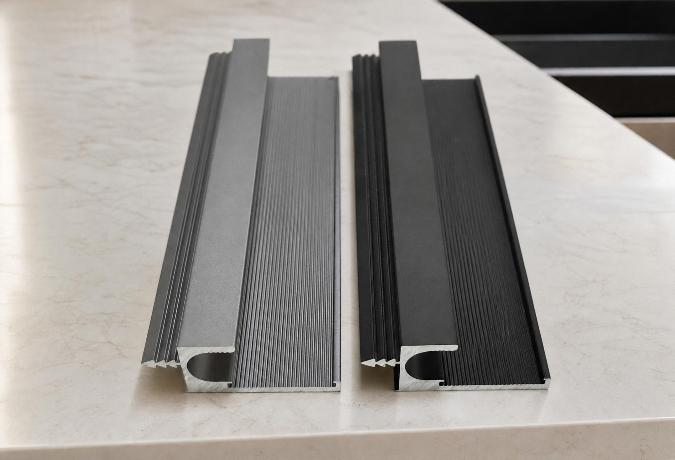
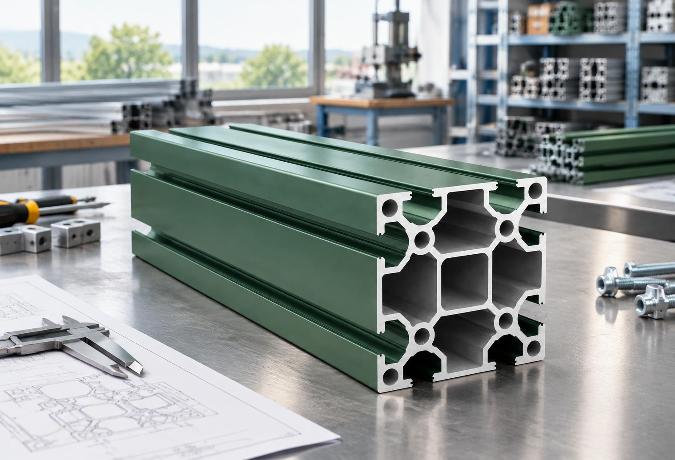
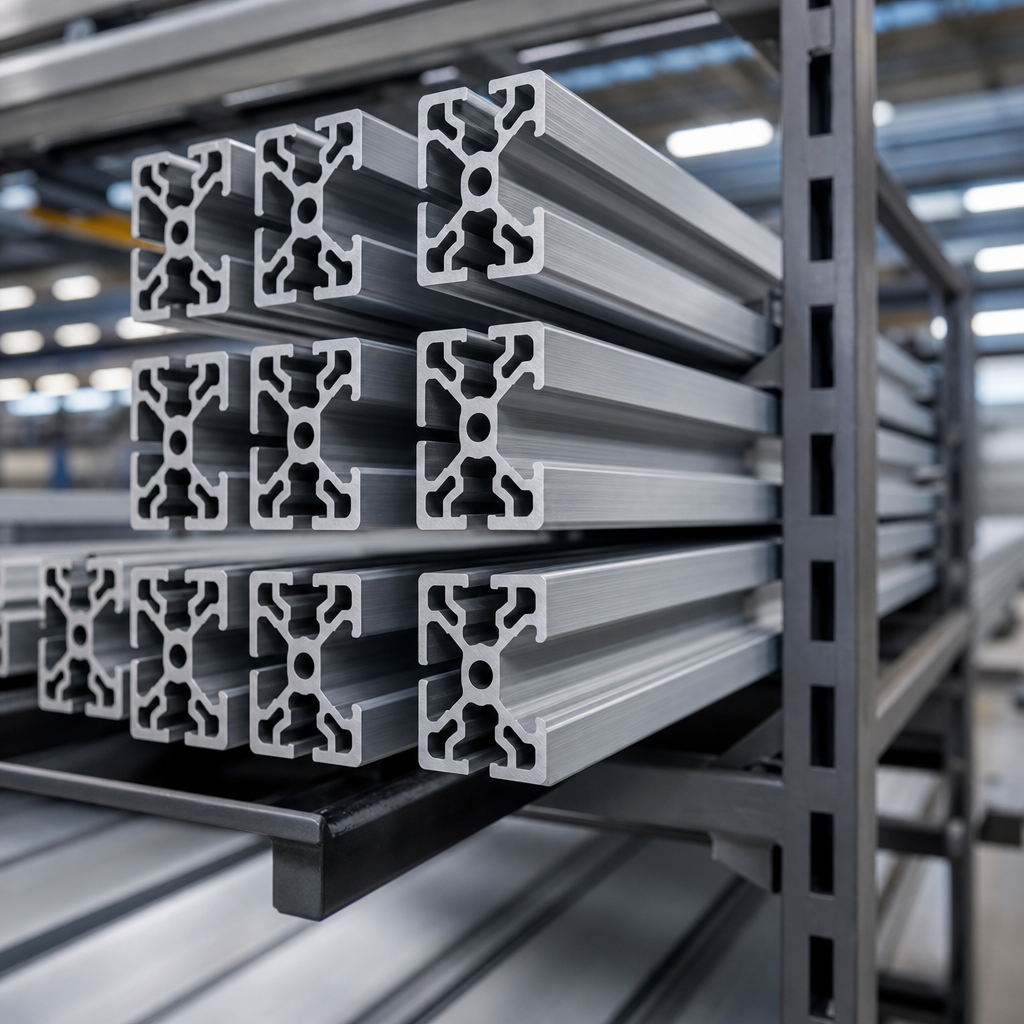
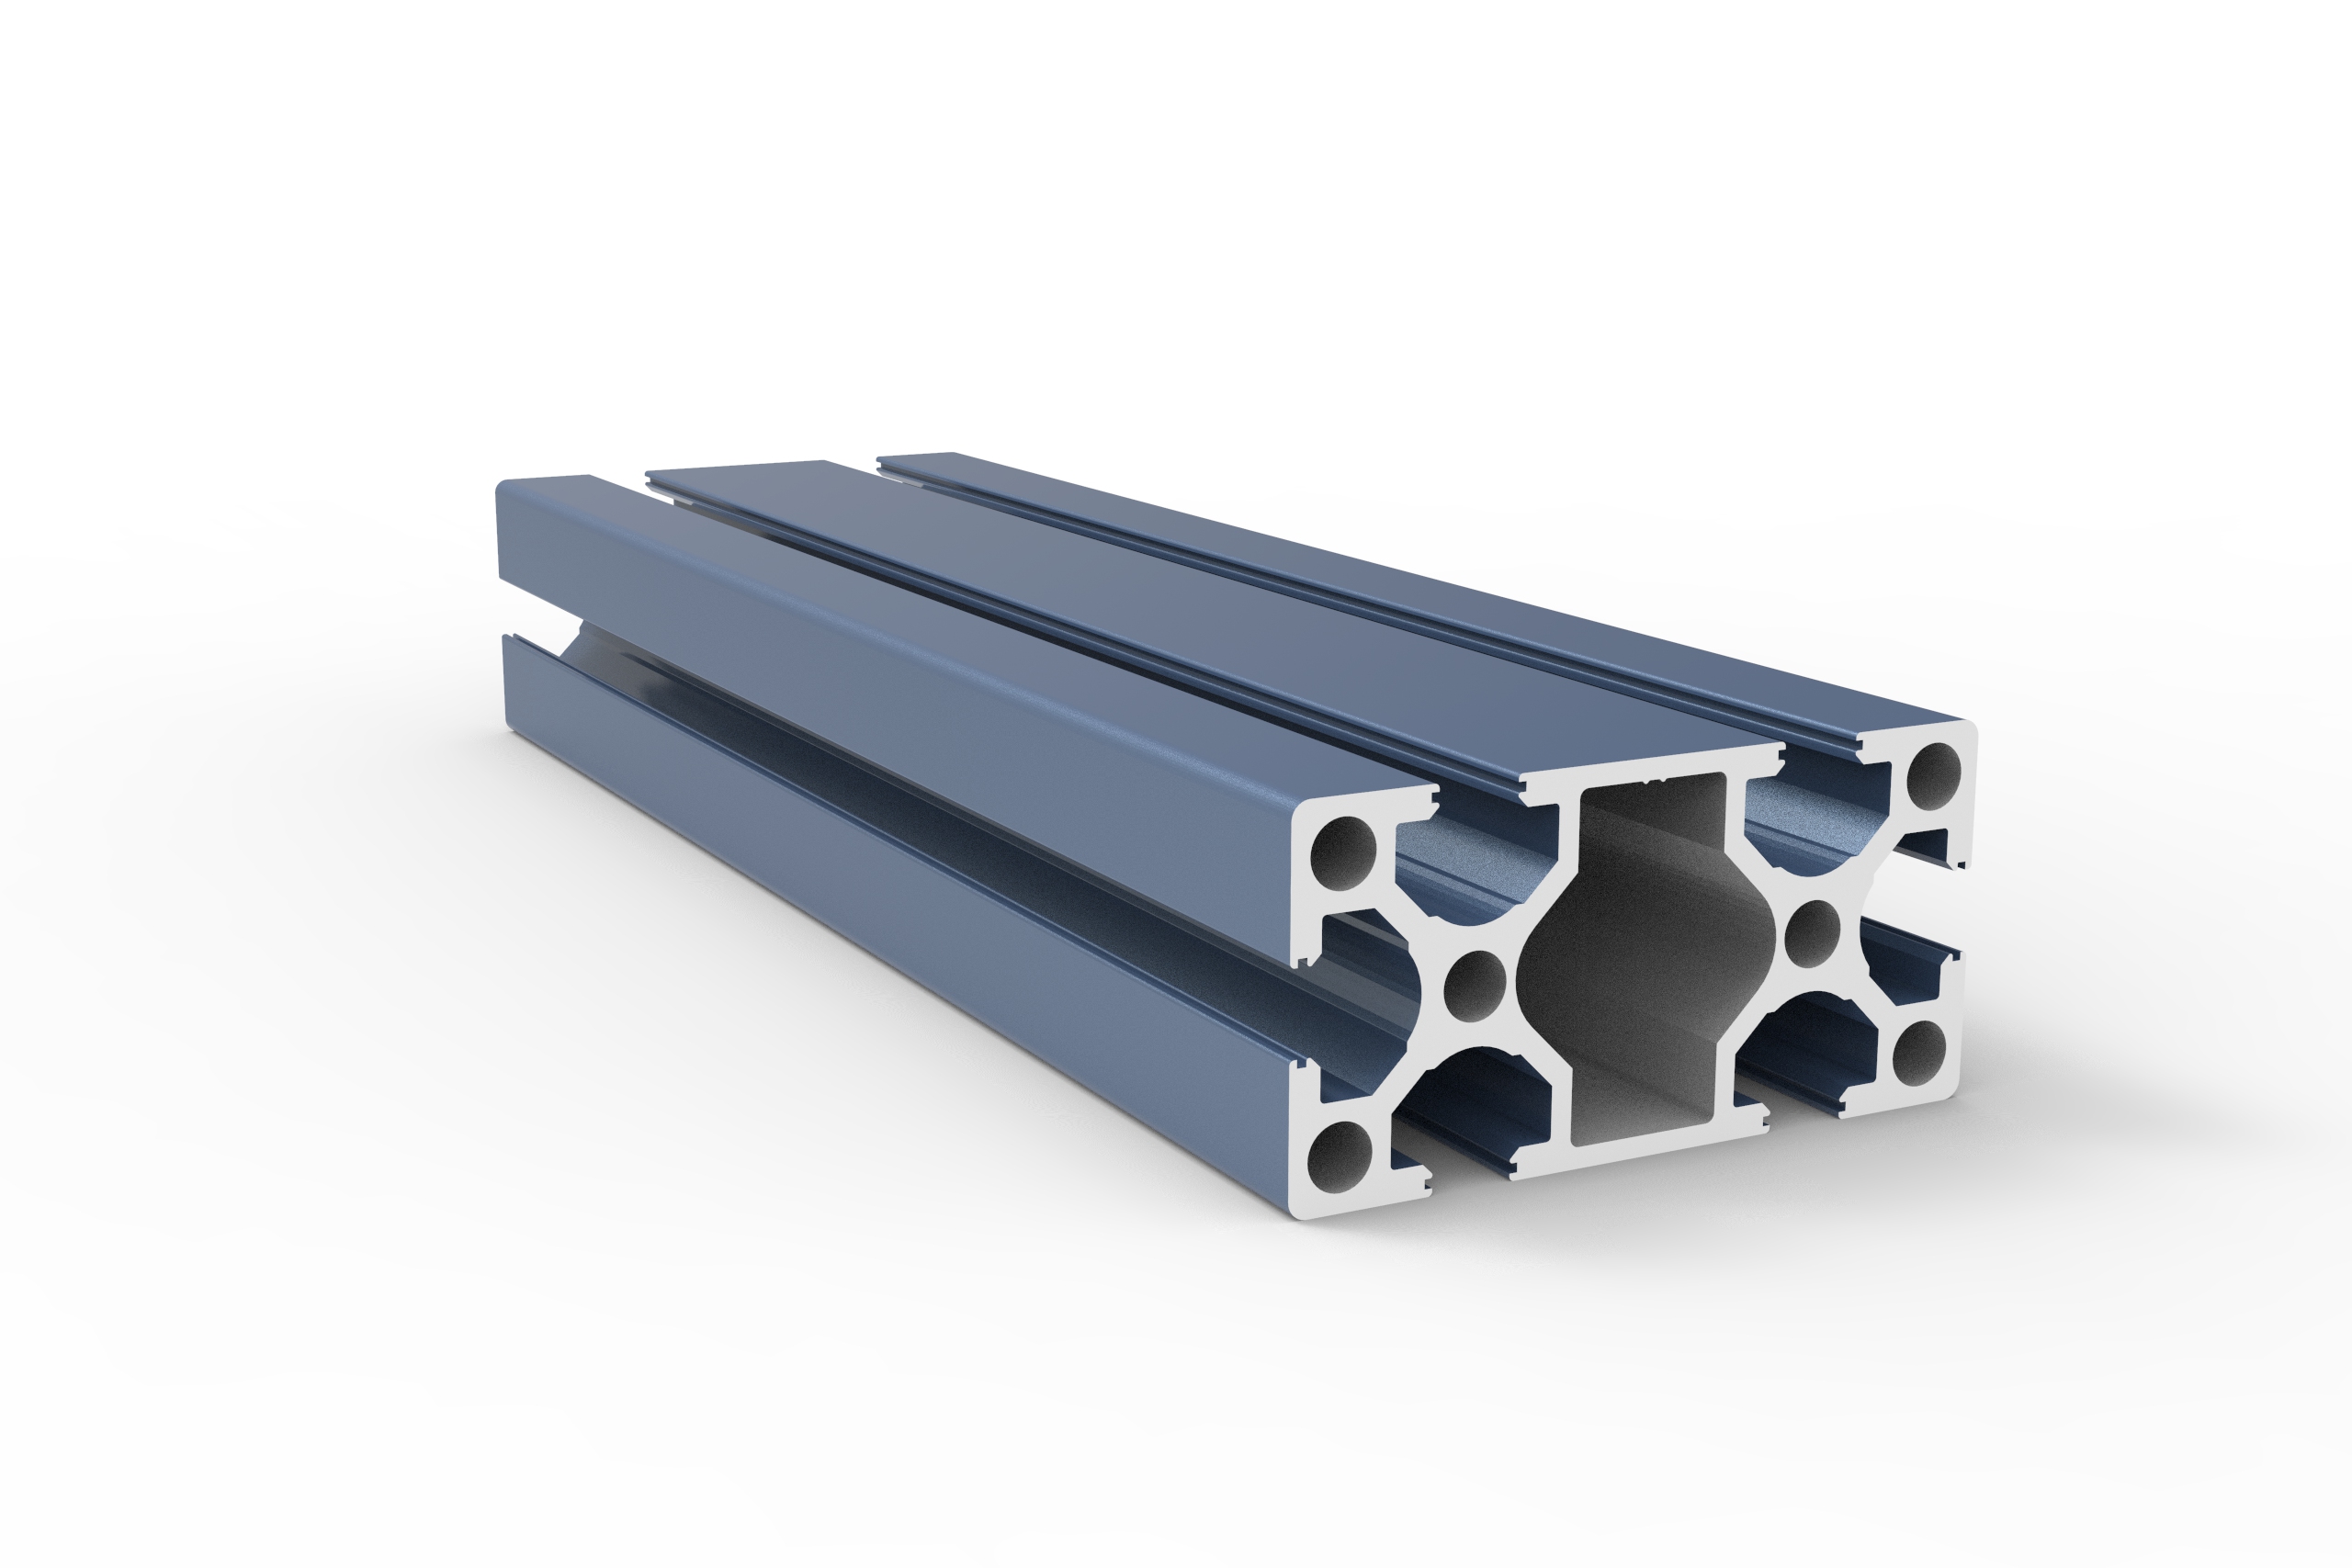
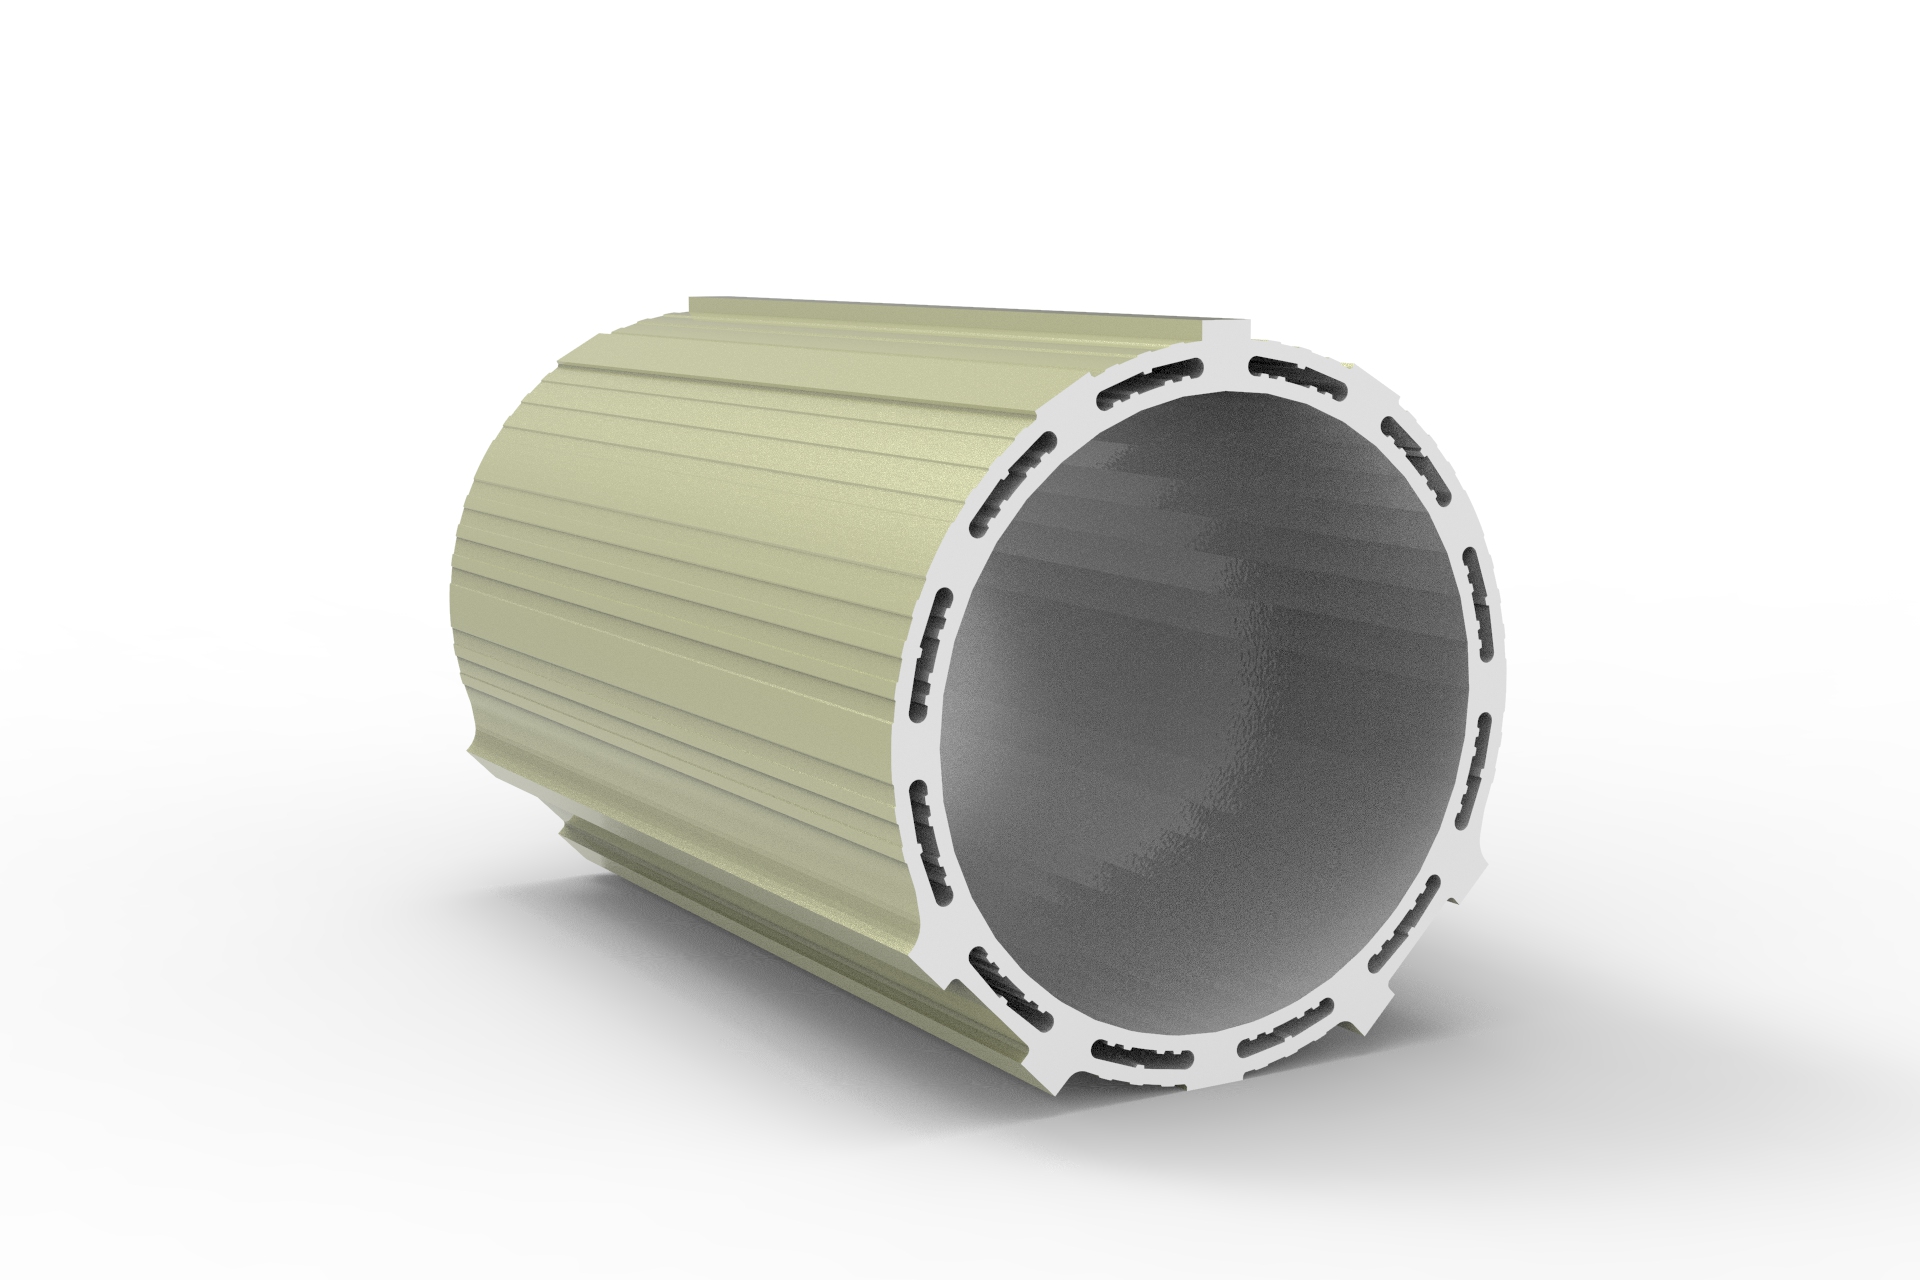
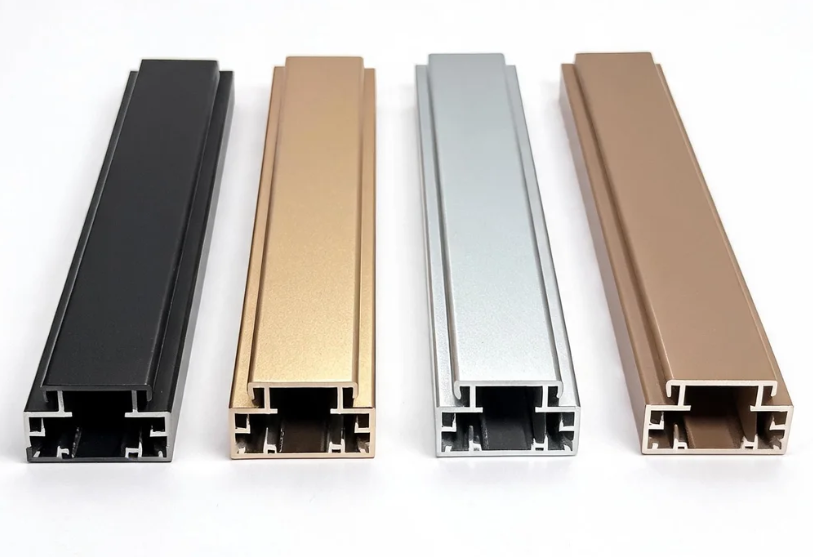
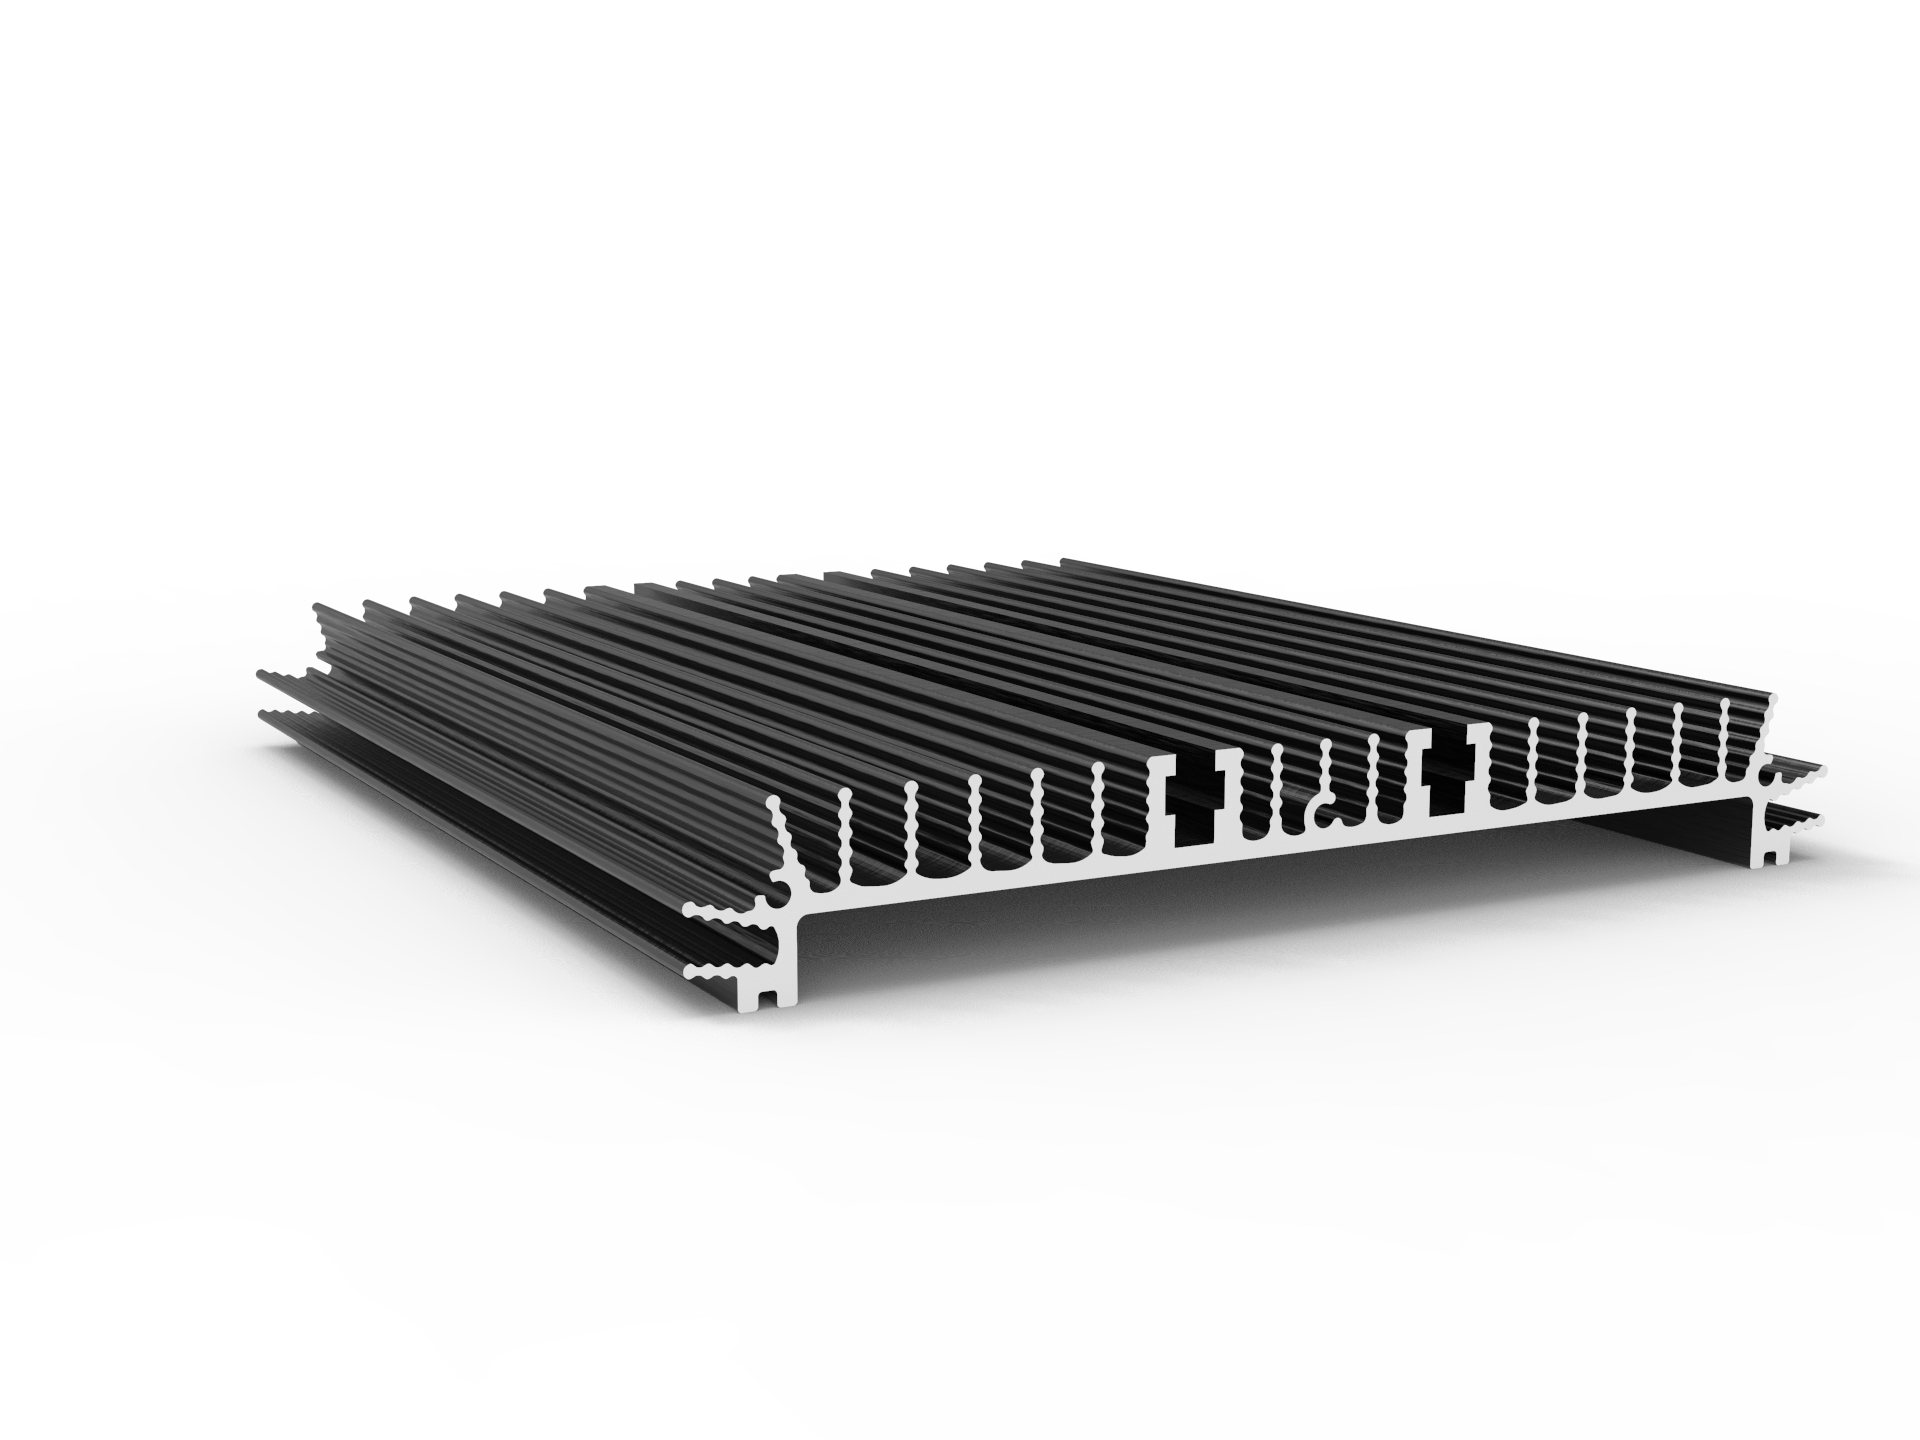
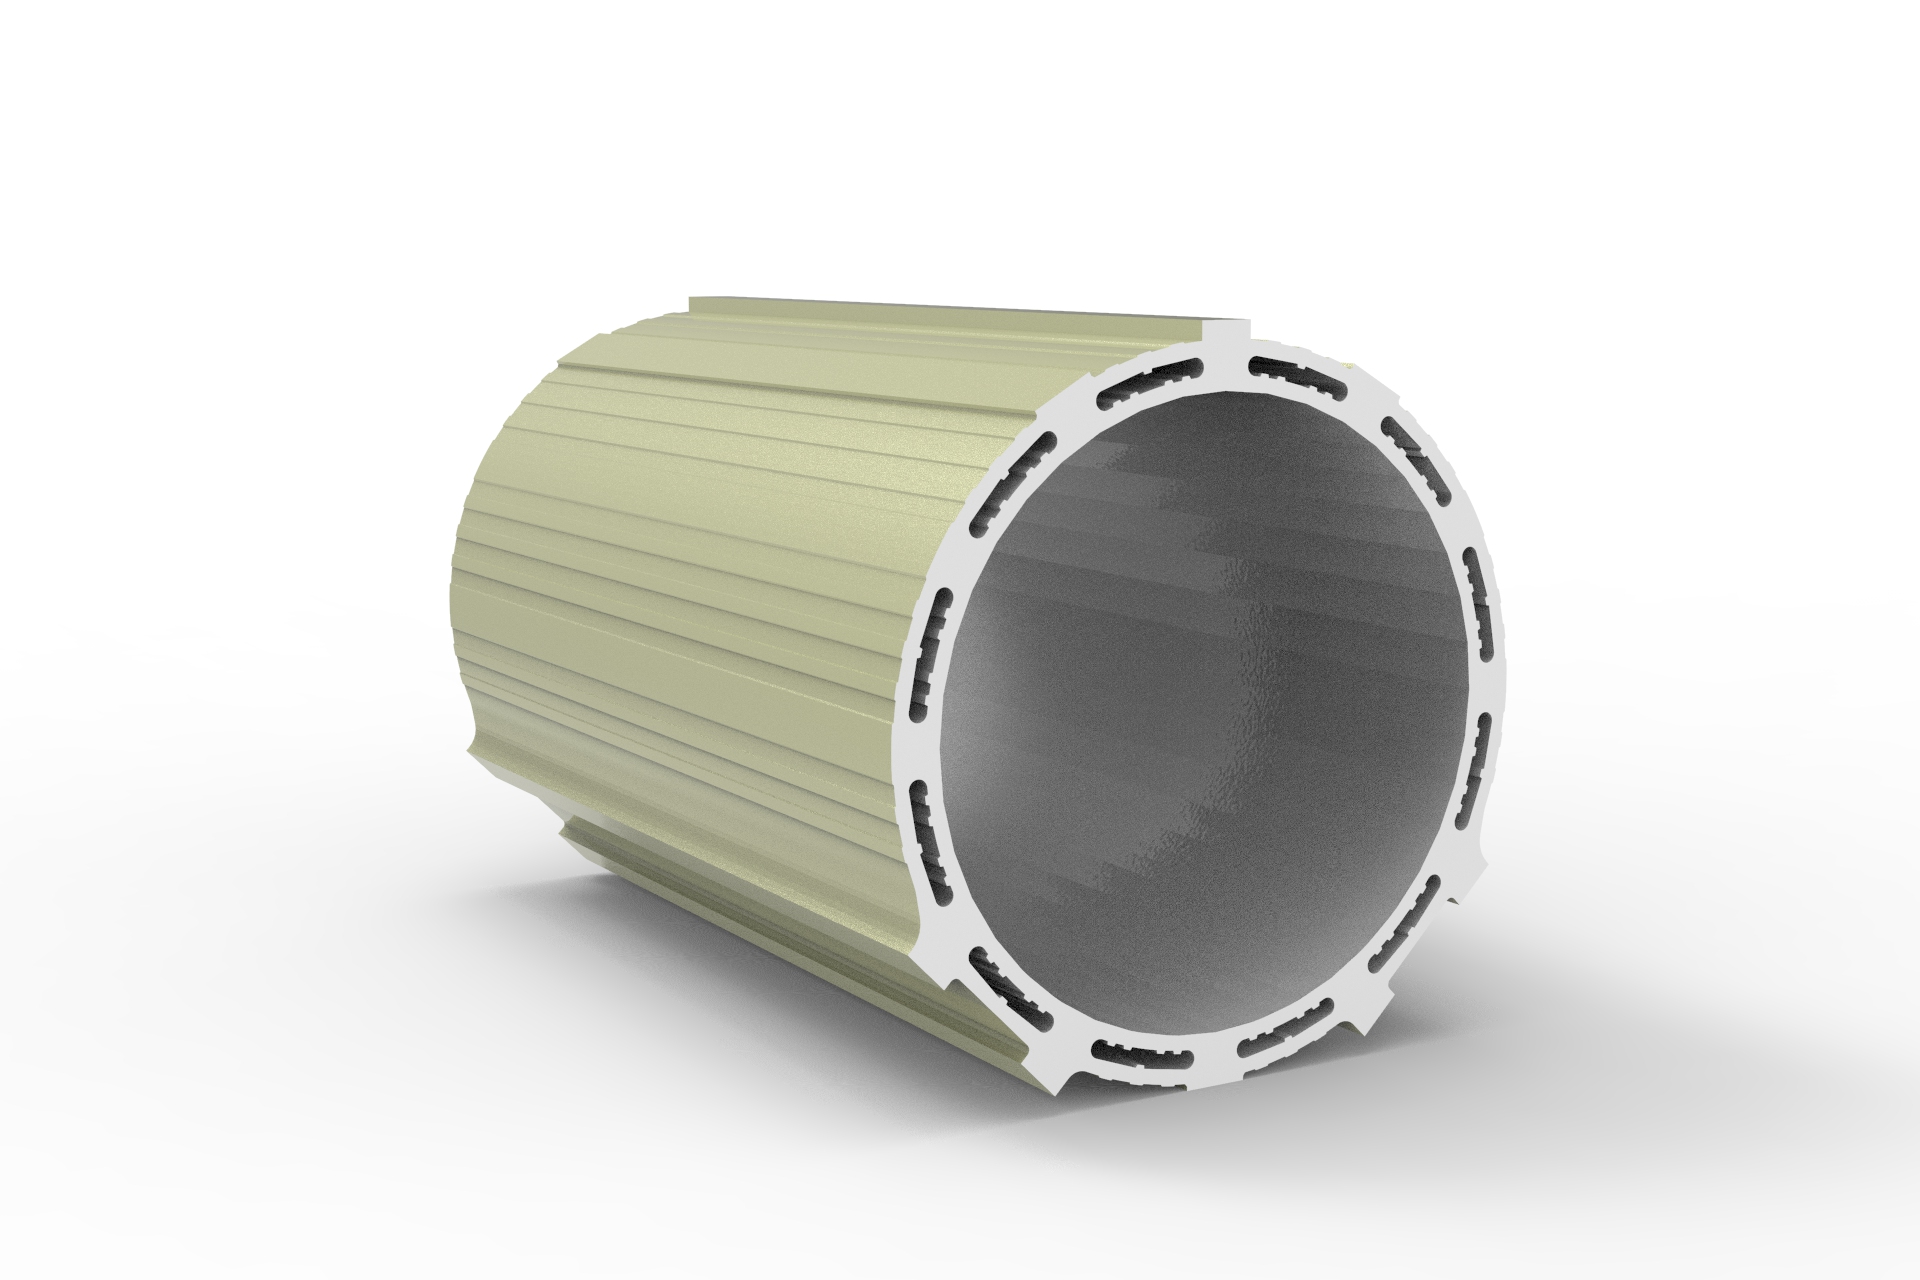
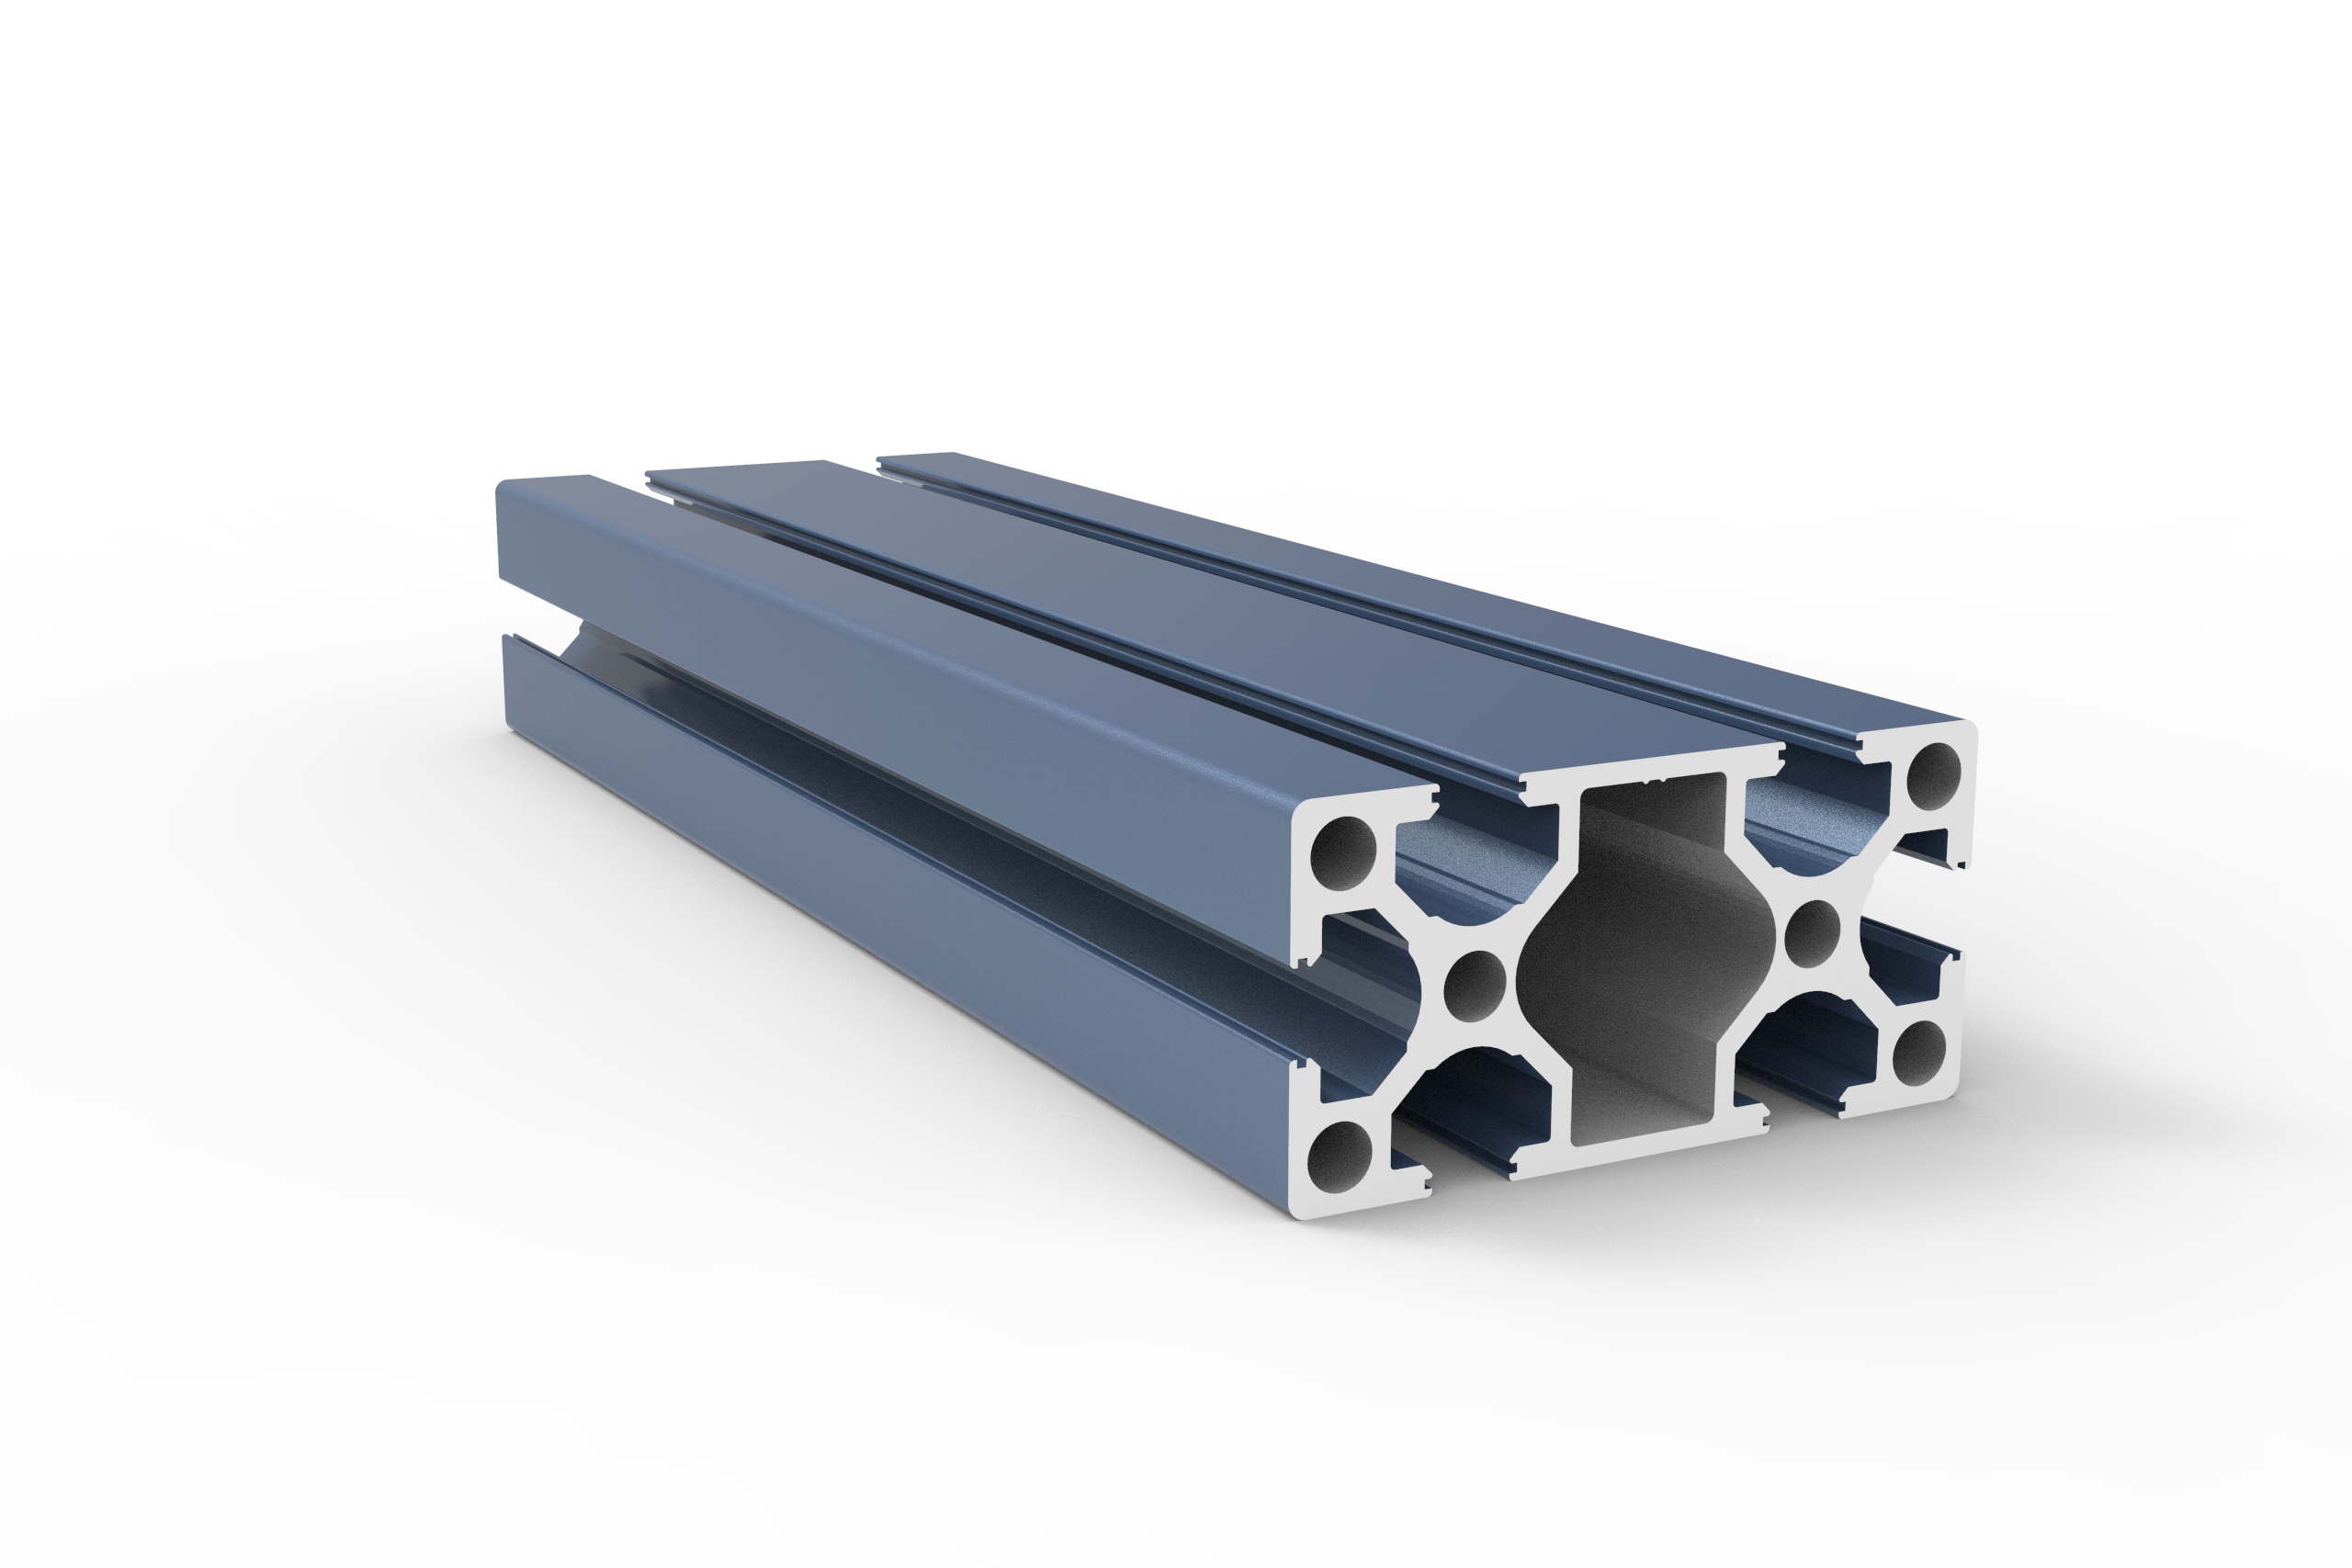
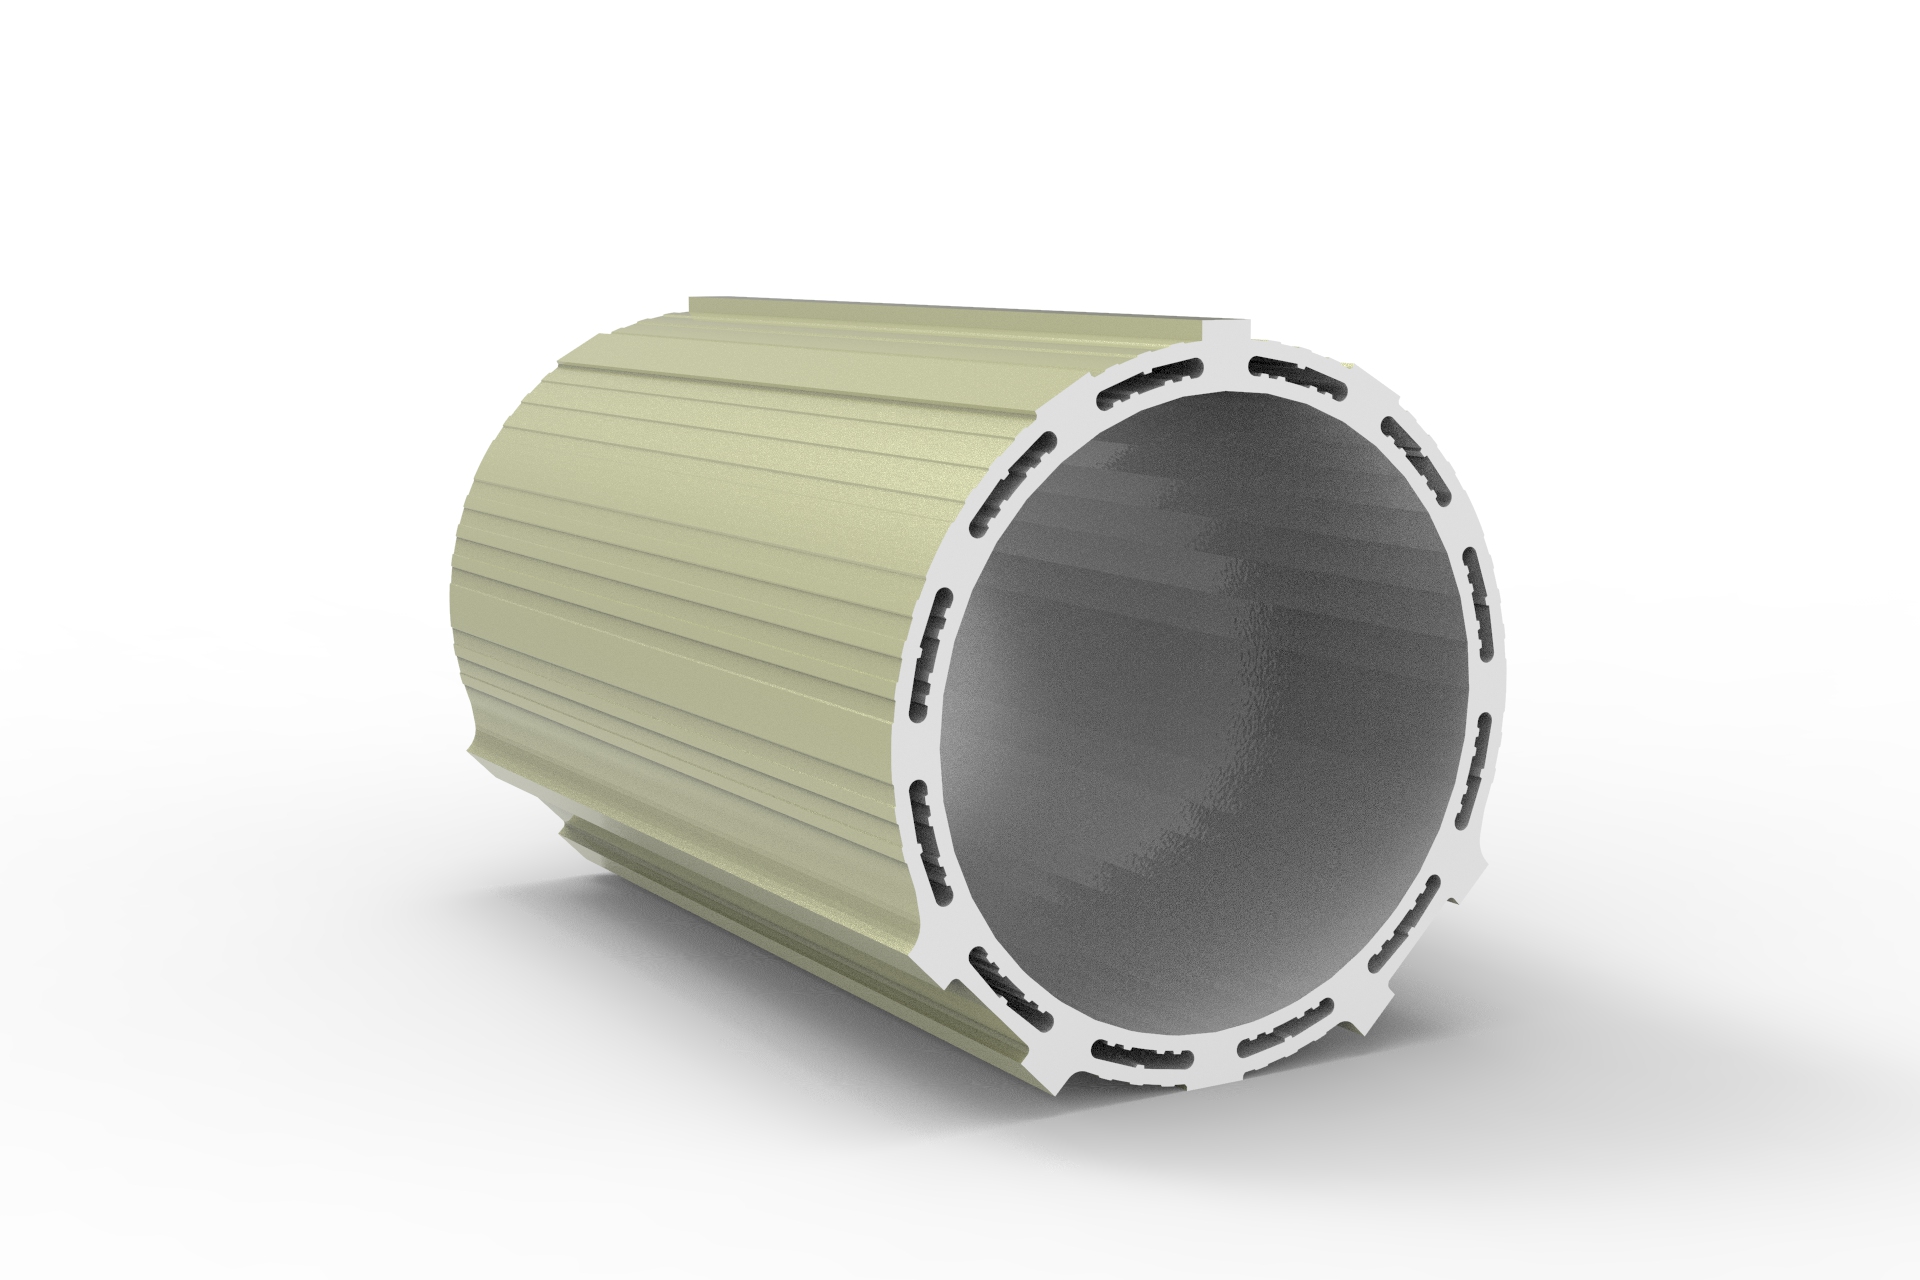
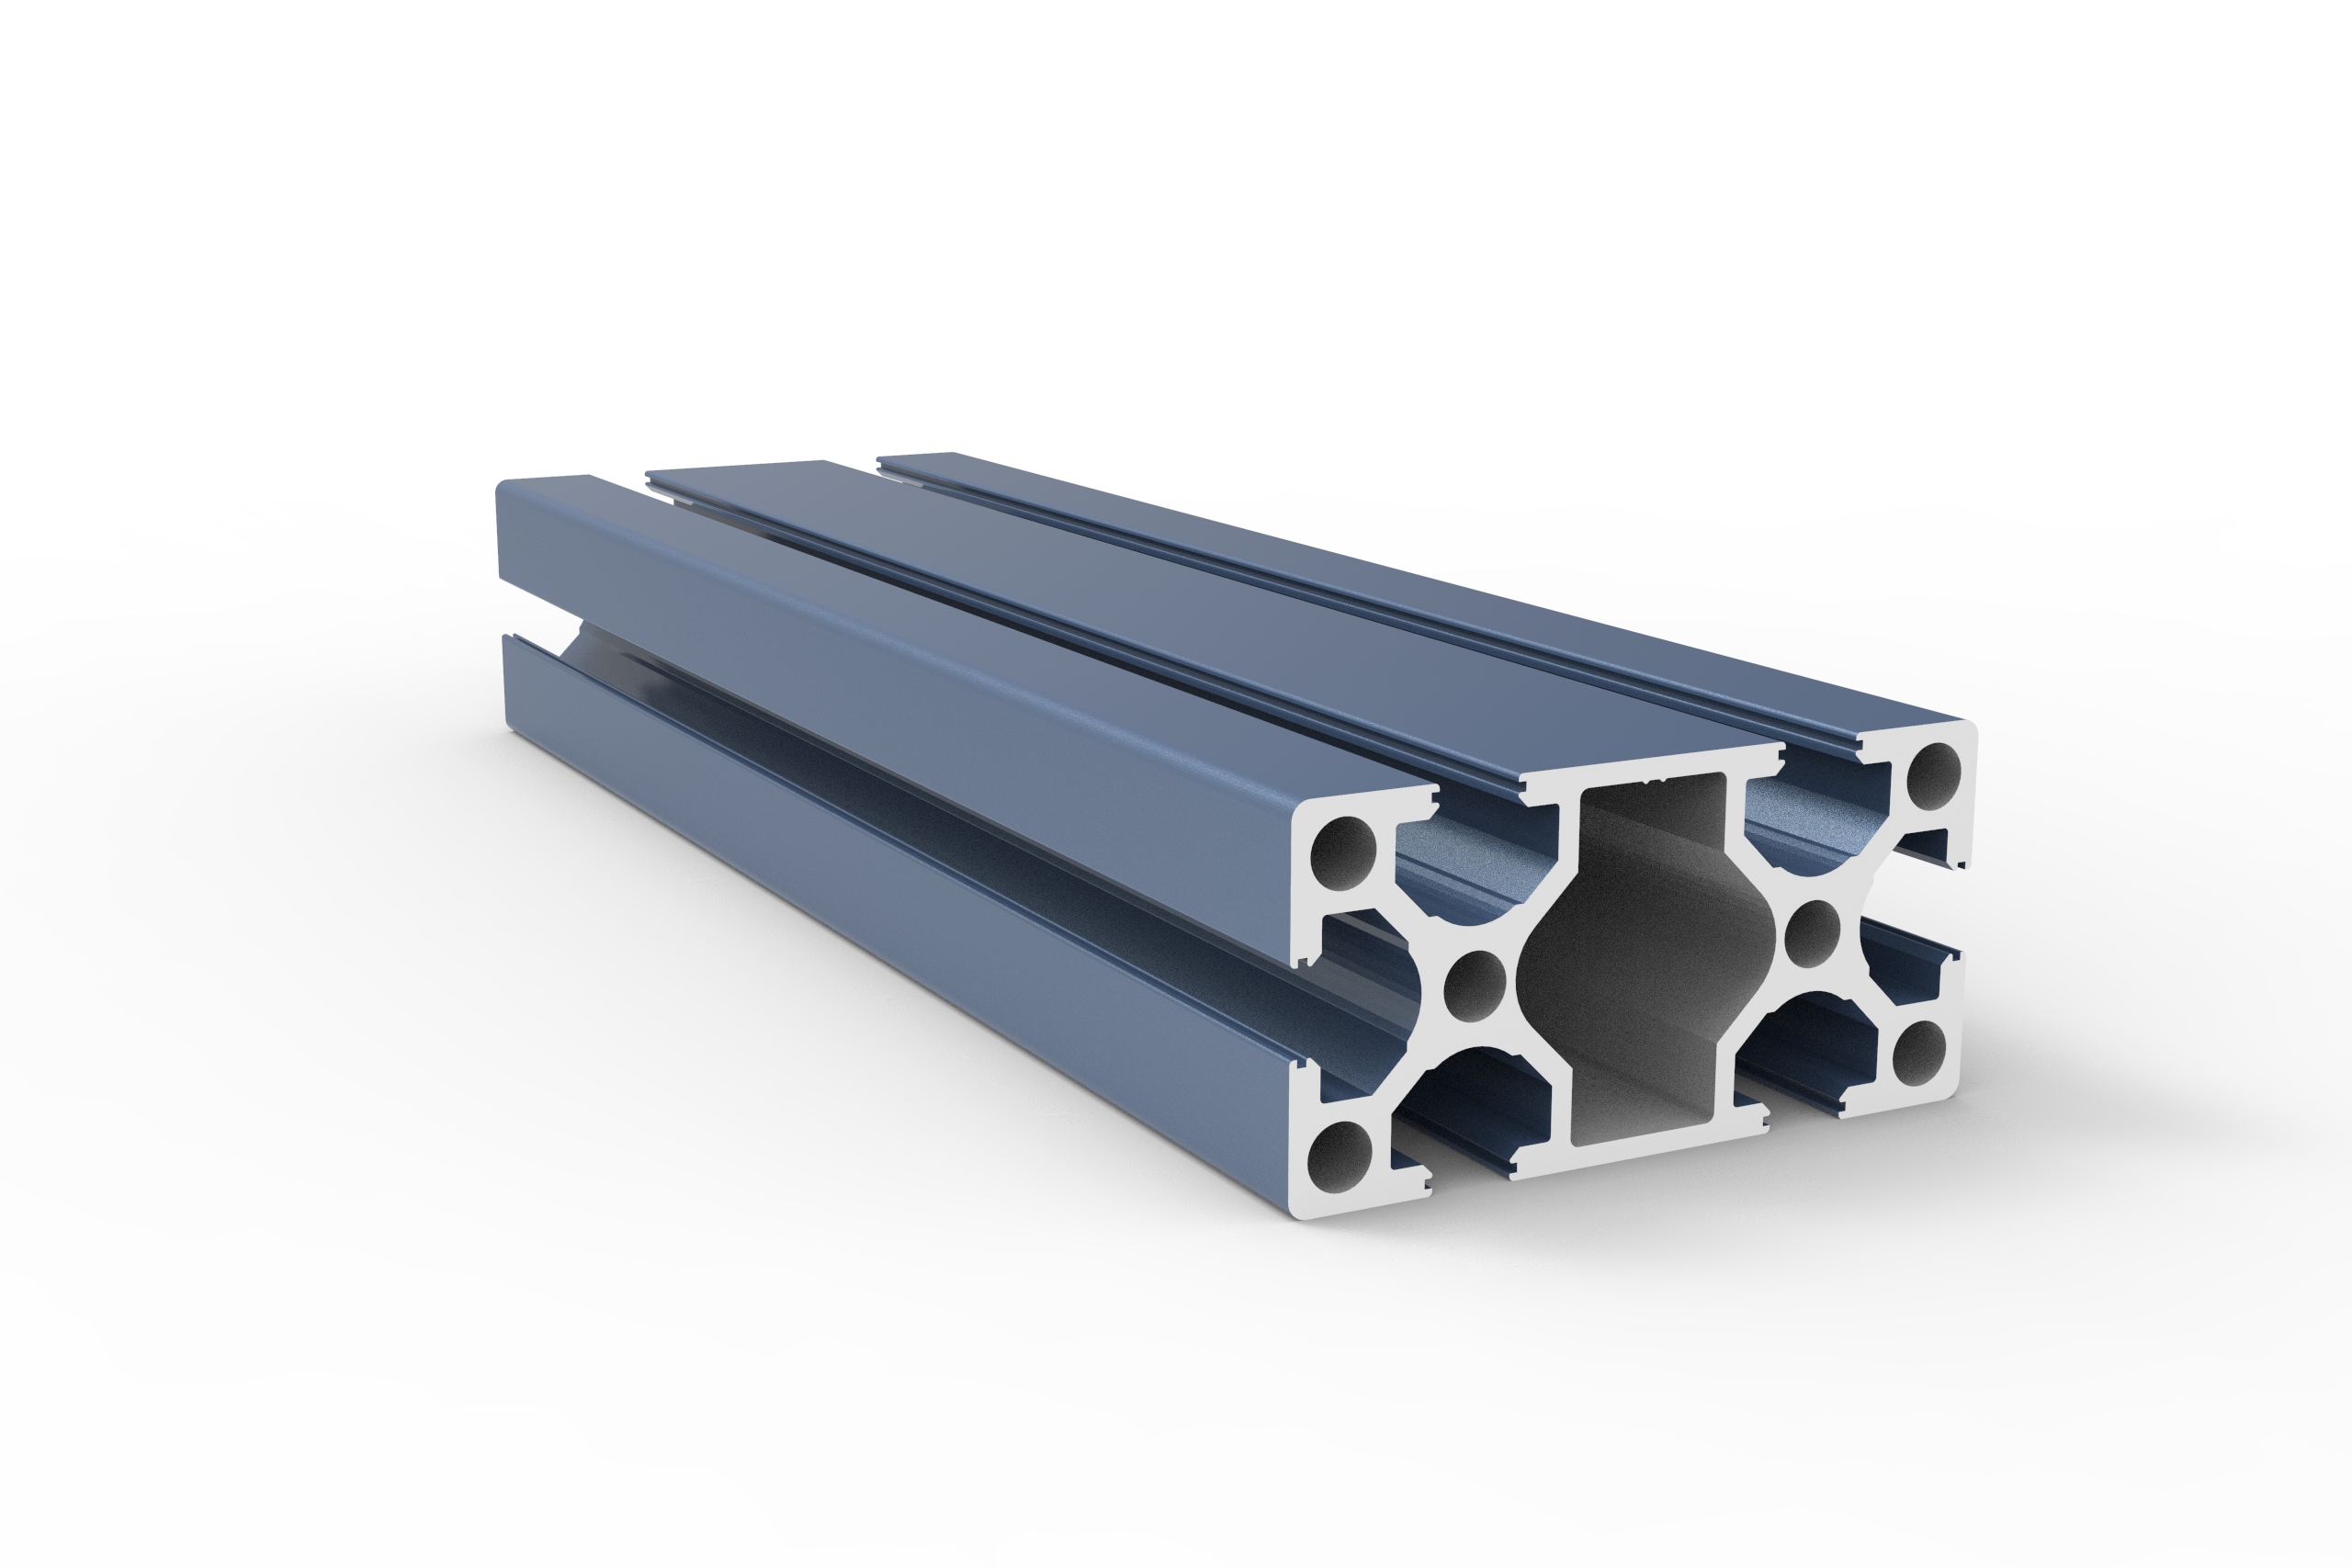
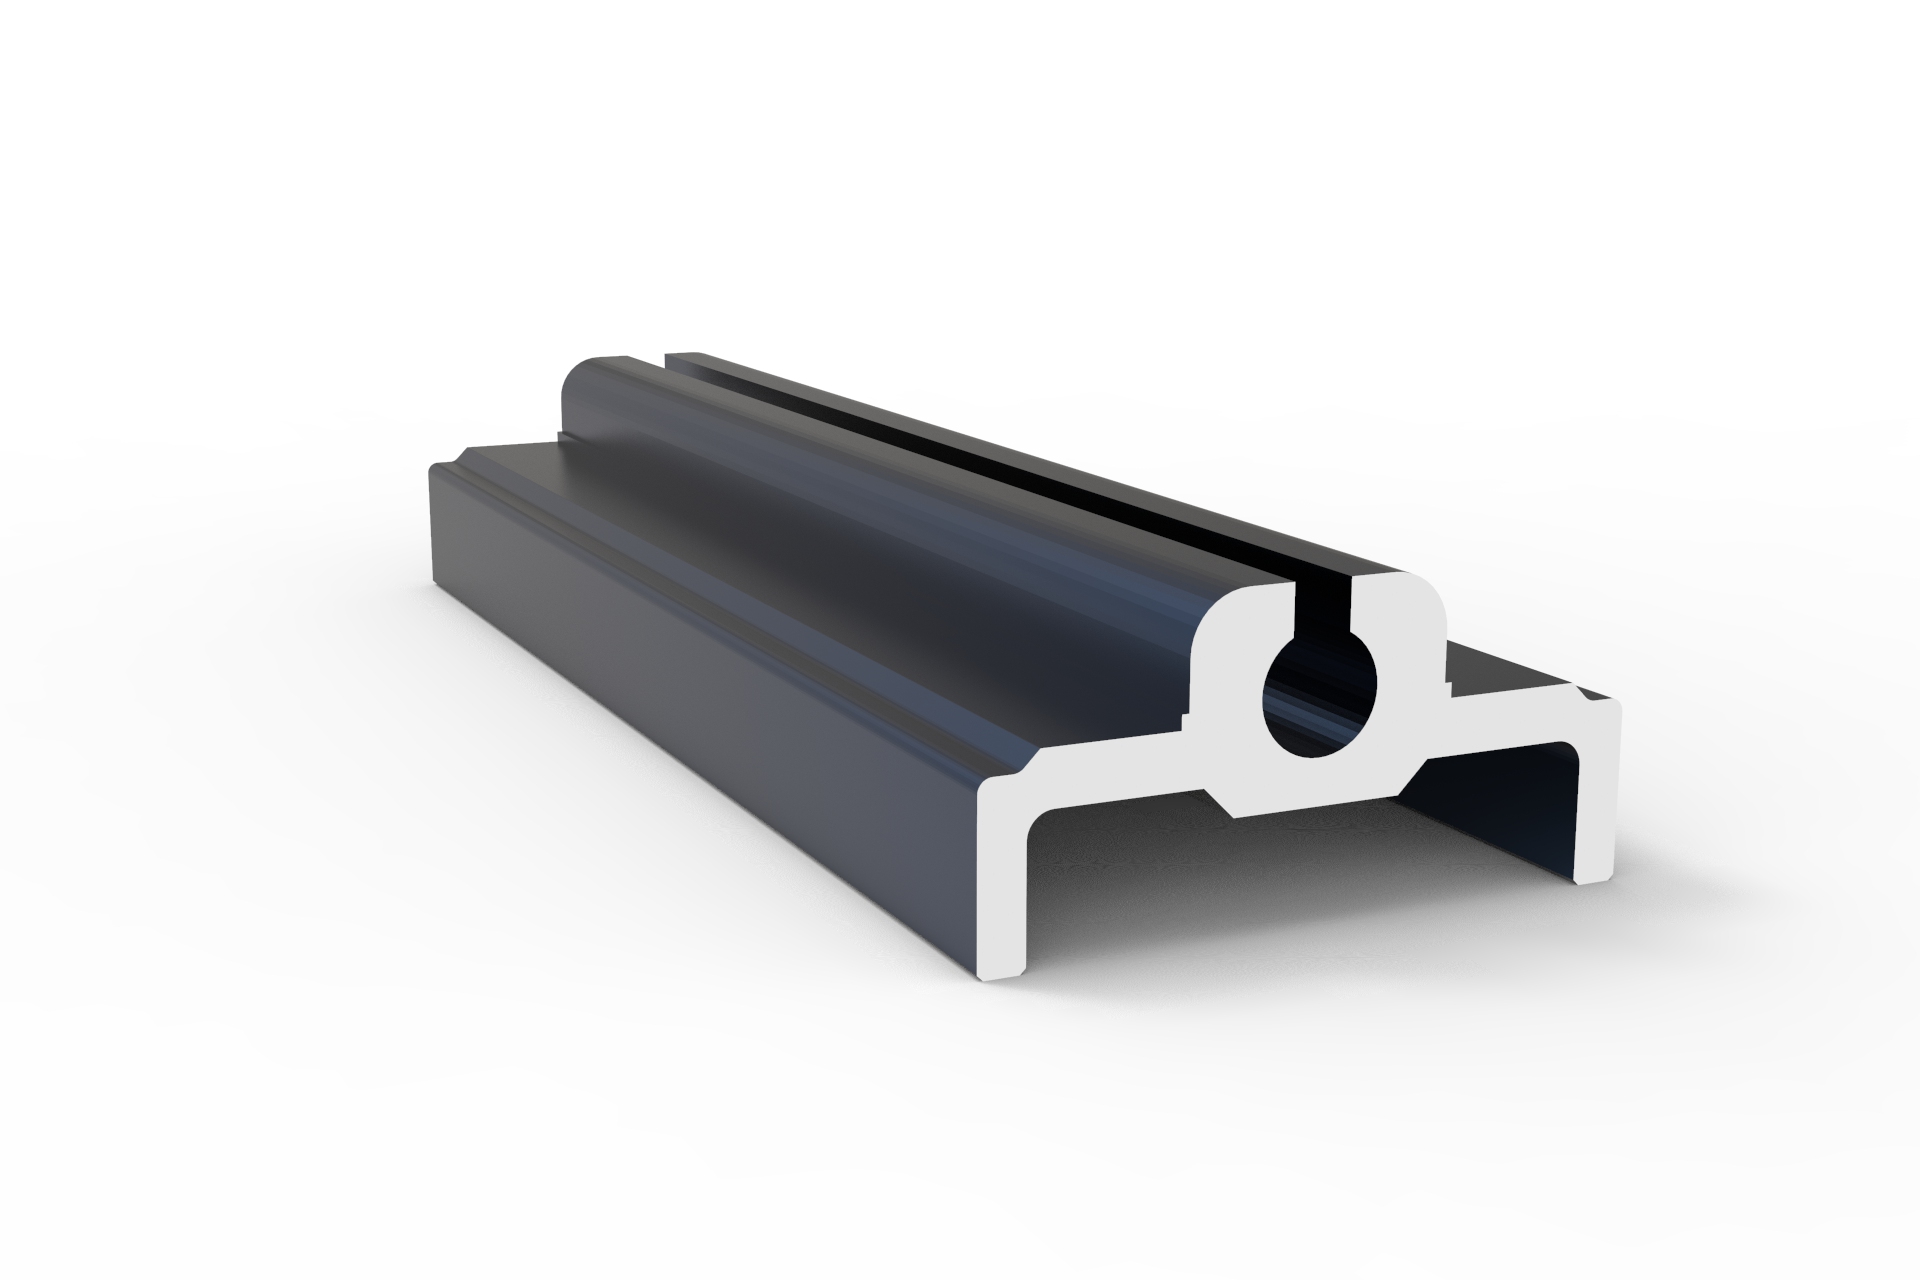
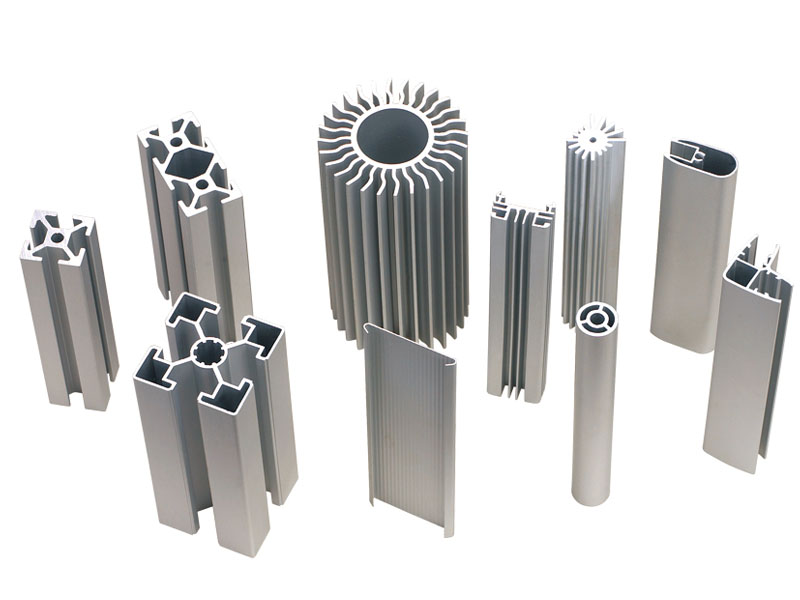
Consider a tubular linear motor design where magnetic flux symmetry around the central shaft is important for smooth thrust. By extruding a profile with a precision central circular bore surrounded by four symmetrical stepped outer ridges, the housing helps maintain concentricity along the stroke. Similarly, wide twin-track profiles can incorporate two raised trapezoidal rails flanking a recessed central flat, complete with internal cavities for optical encoders and hall-effect sensors, according to the supplied profile data.
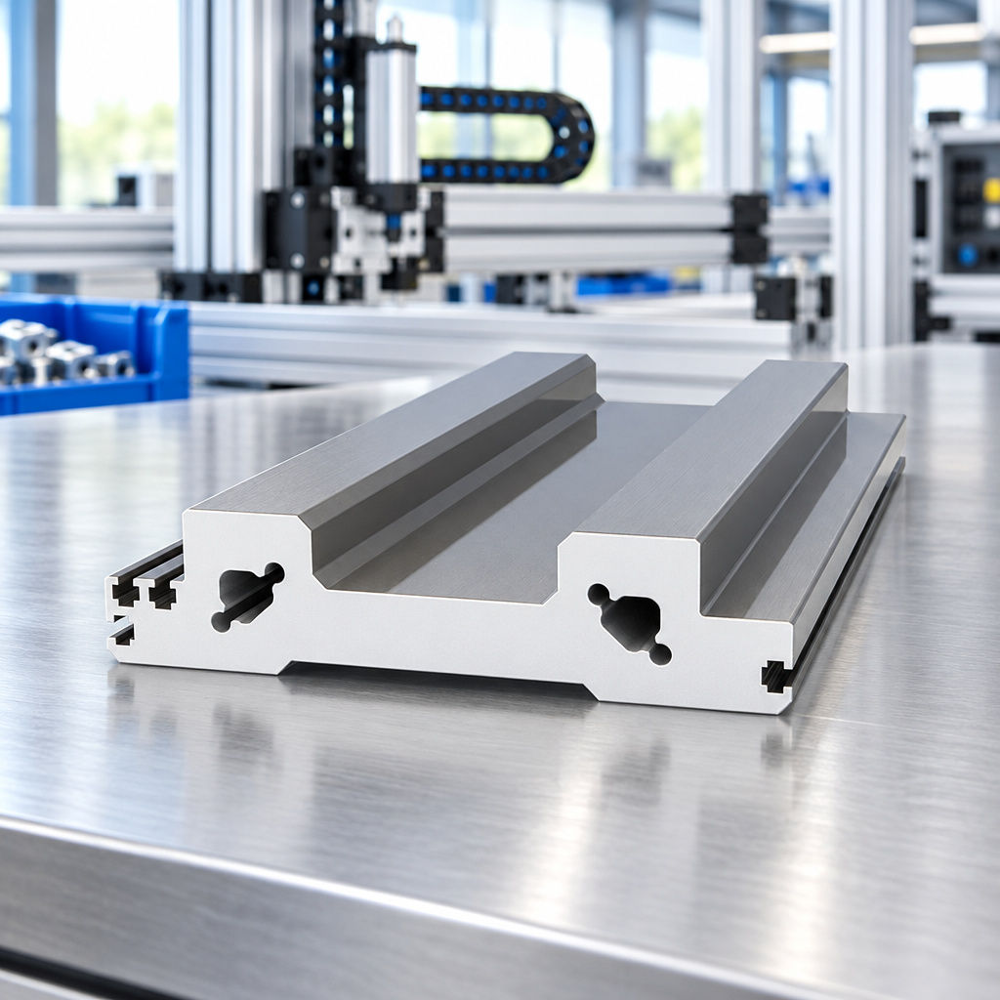
Direct-drive linear motors eliminate mechanical wear items like ball screws and timing belts, but they introduce a notable thermal challenge right inside the machine bed. In a moving-coil design, the current-carrying coil assembly rides directly over the permanent magnet track, and resistive heating transfers into the actuator base. If that heat remains trapped, thermal expansion can bow the rail and affect positioning repeatability.
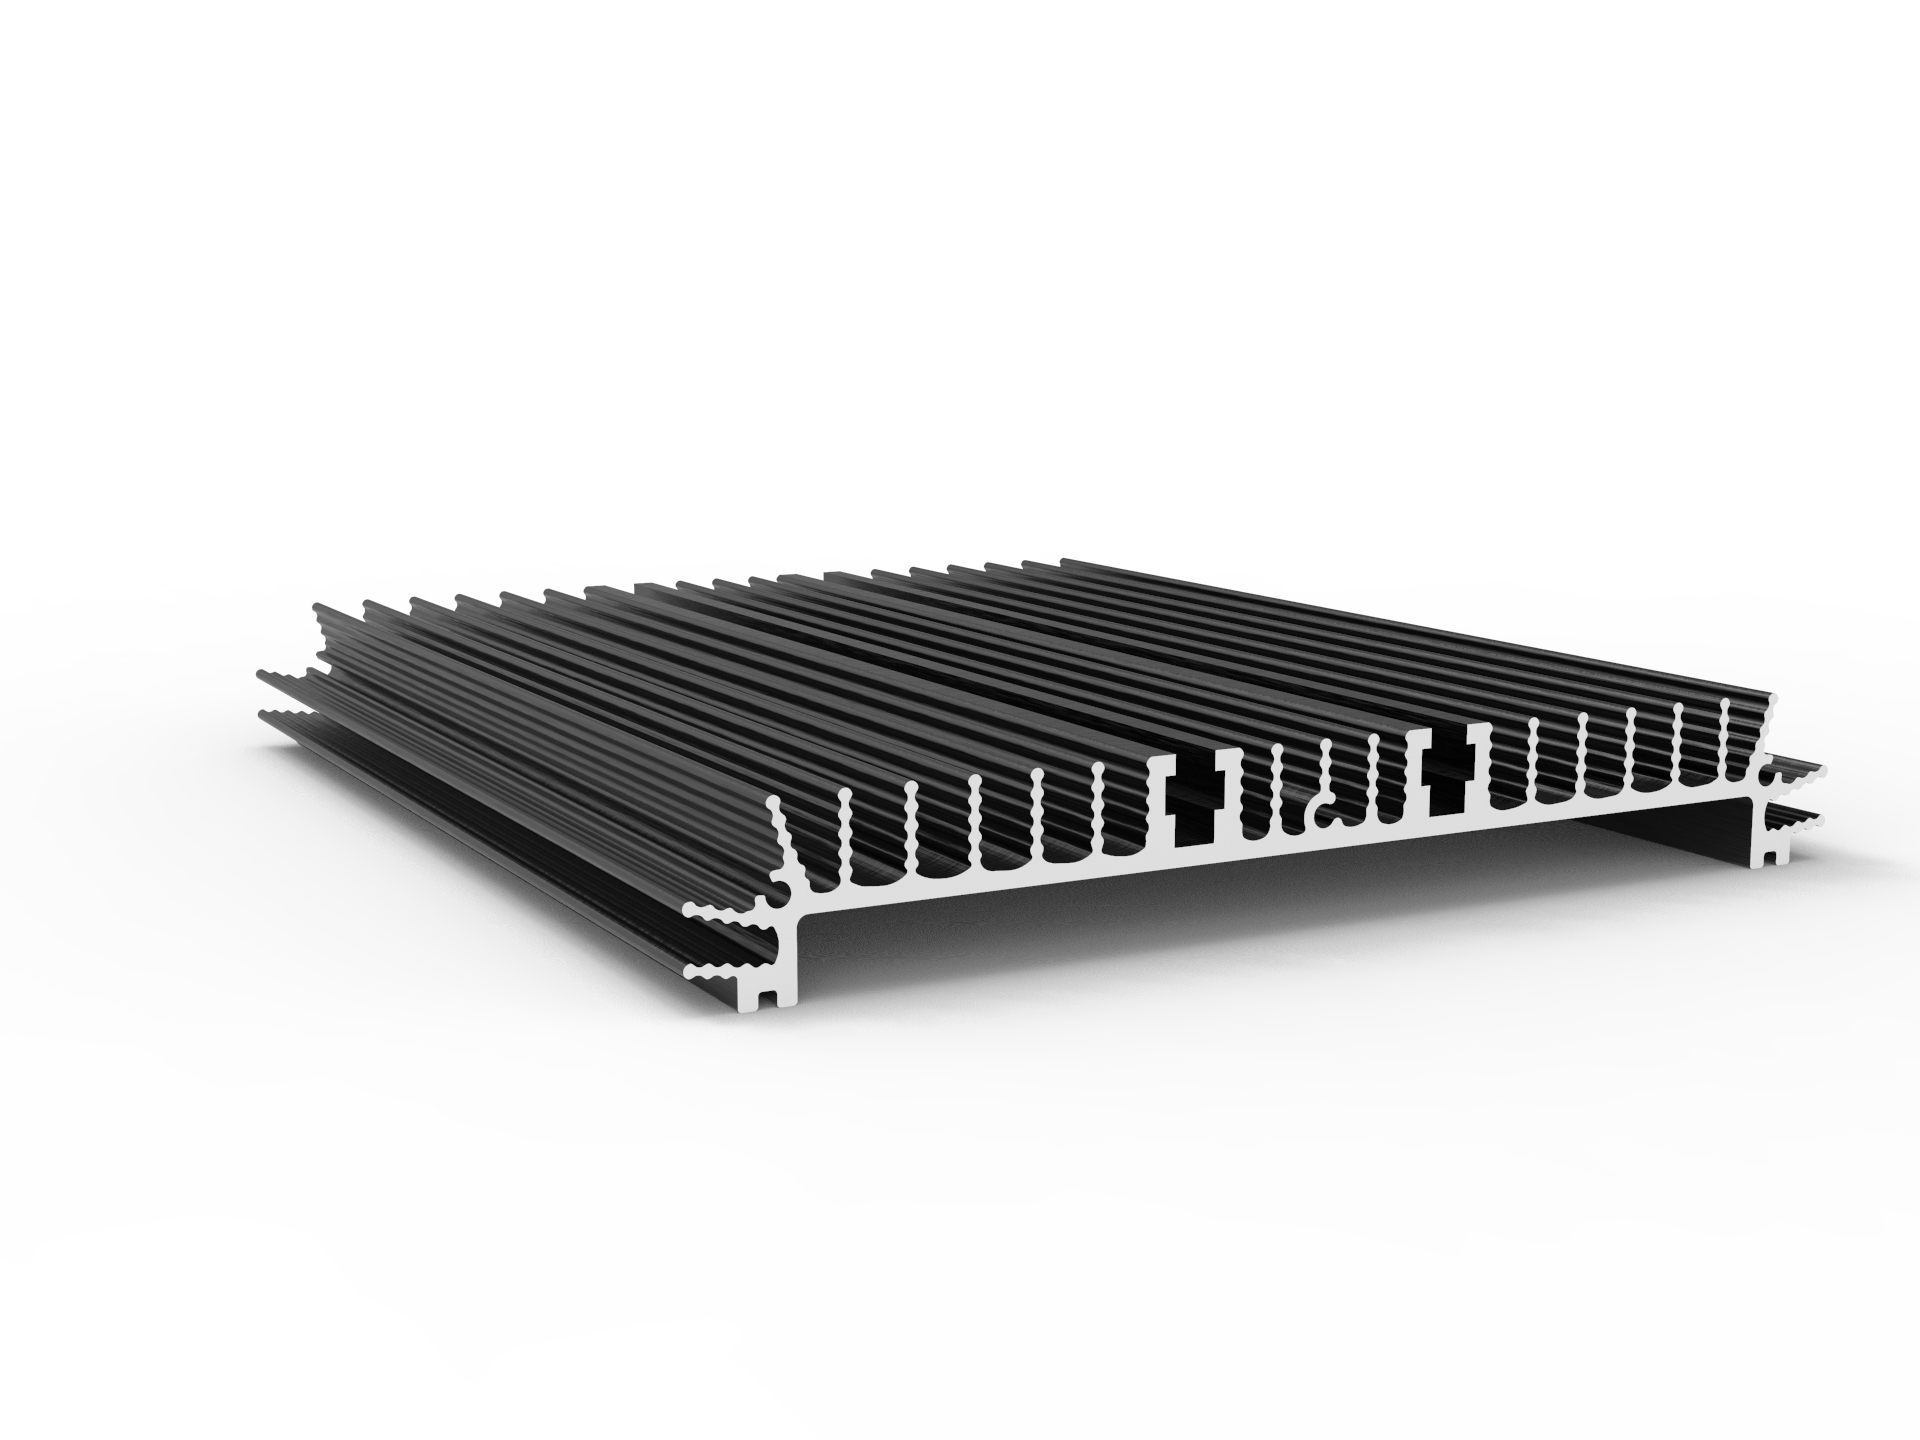
Aluminum’s relatively high thermal conductivity, typically cited in the range of 160 to 200 W/m·K across common 6xxx-series extrusion alloys, allows the structural rail to double as a passive heat exchanger. Instead of attaching separate cooling plates, engineers can specify low-profile linear rail extrusions featuring a dense array of thin vertical cooling fins down the center channel, a configuration included in this supplier’s linear rail lineup. When airflow and thermal design are adequate, air flowing across these extruded fins can aid heat dissipation before thermal gradients accumulate.
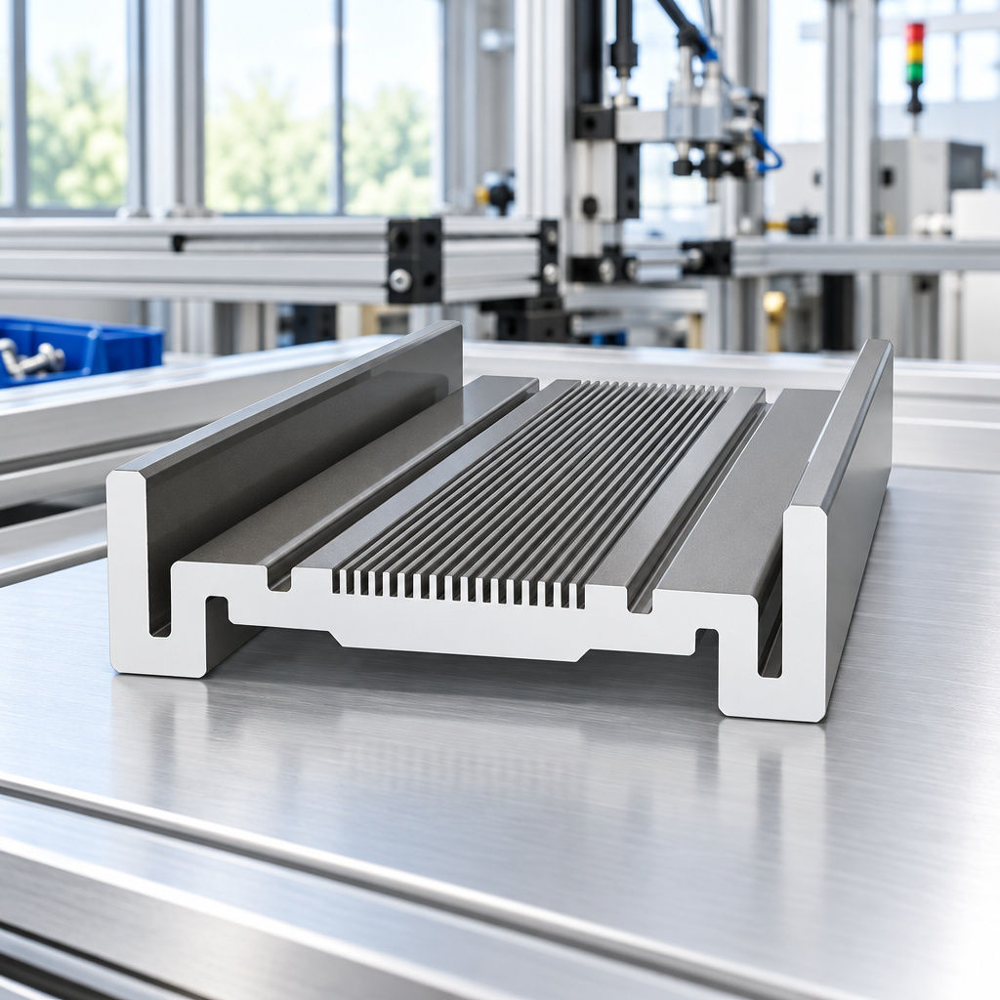
Open C-channel profiles behave poorly when subjected to eccentric loads, such as a robotic arm cantilevered off the side of a linear slide. Under off-center loading, an open channel twists like a wrung towel, causing recirculating ball carriages to bind against their steel guideways. Resisting torsional deflection requires closed hollow chambers that allow shear stress to flow continuously around the perimeter.
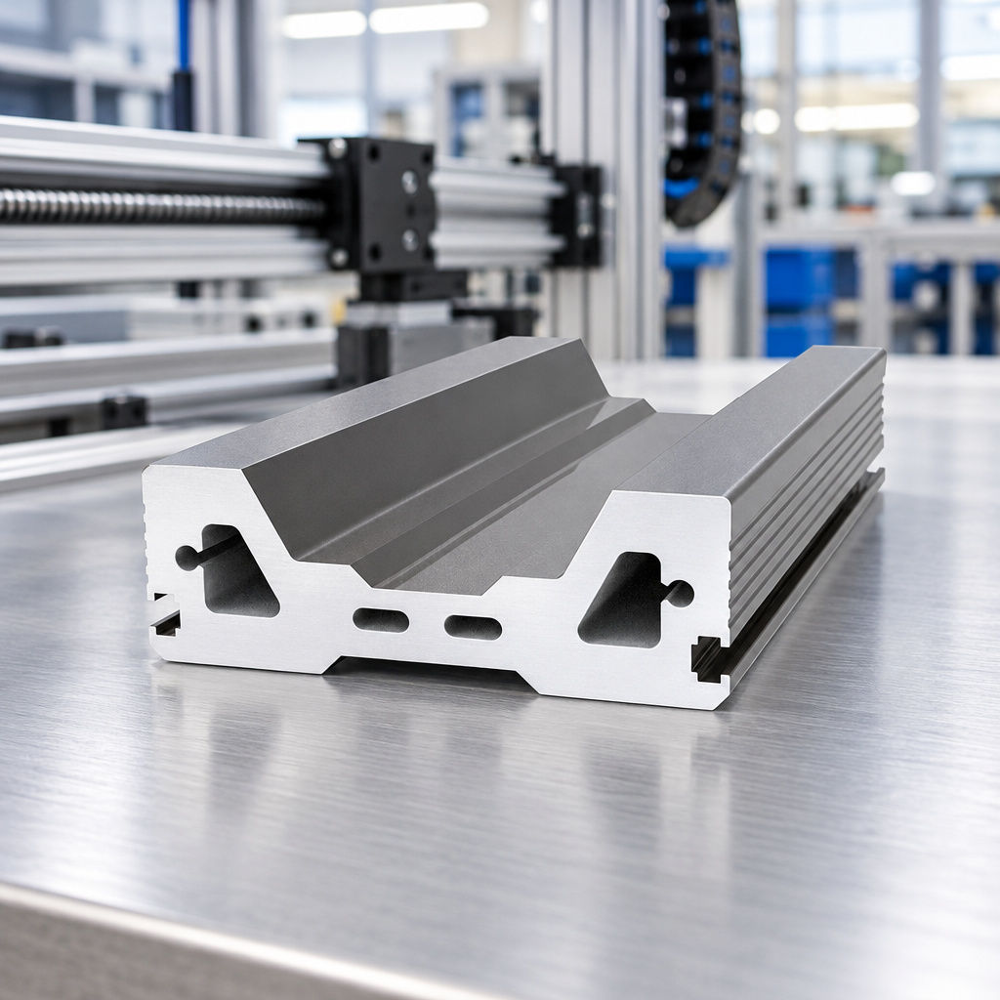
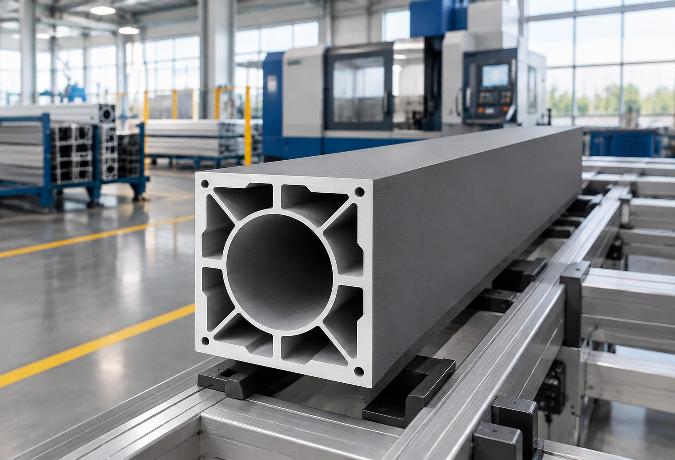
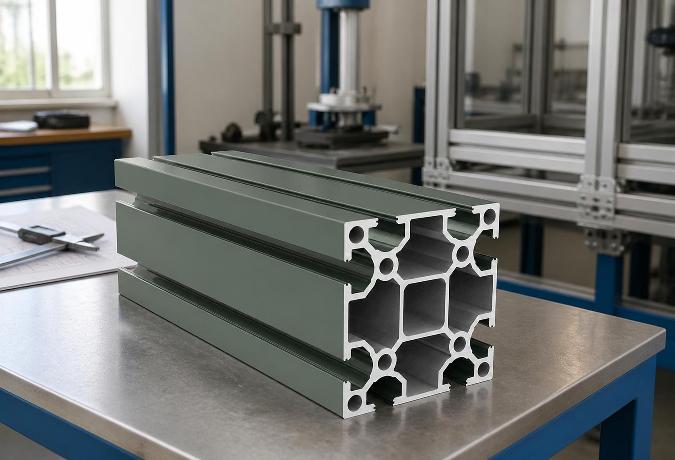
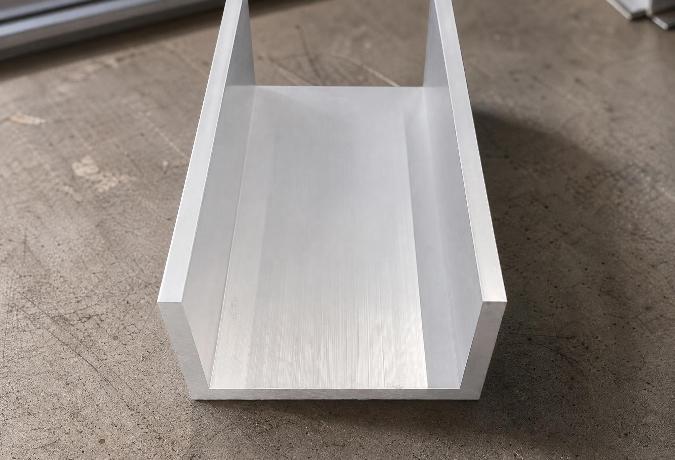
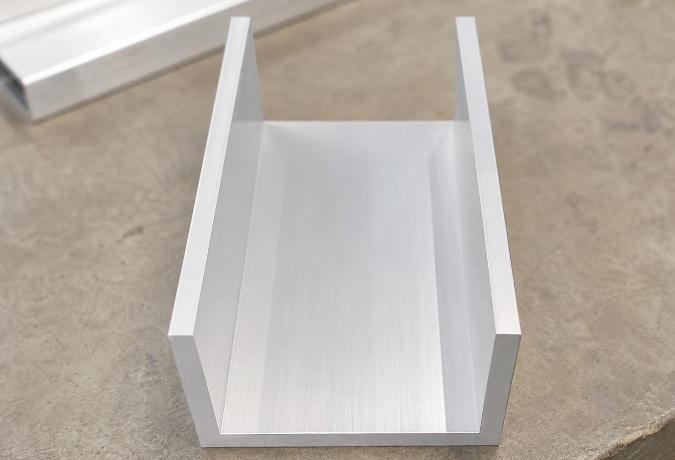
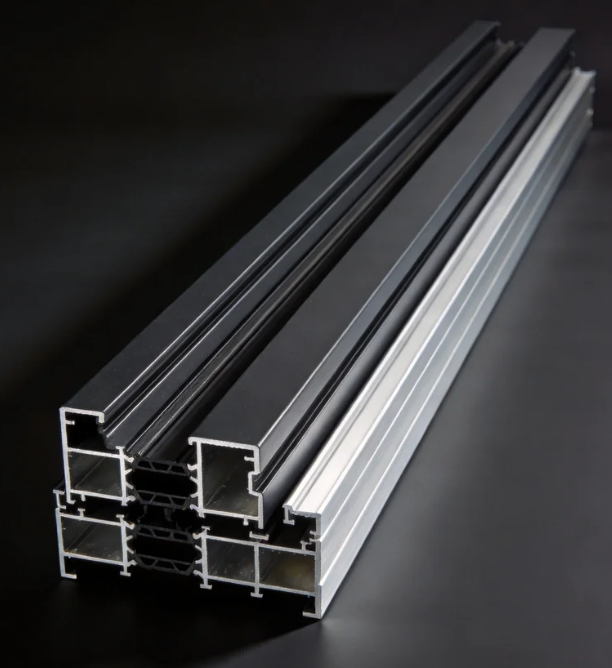
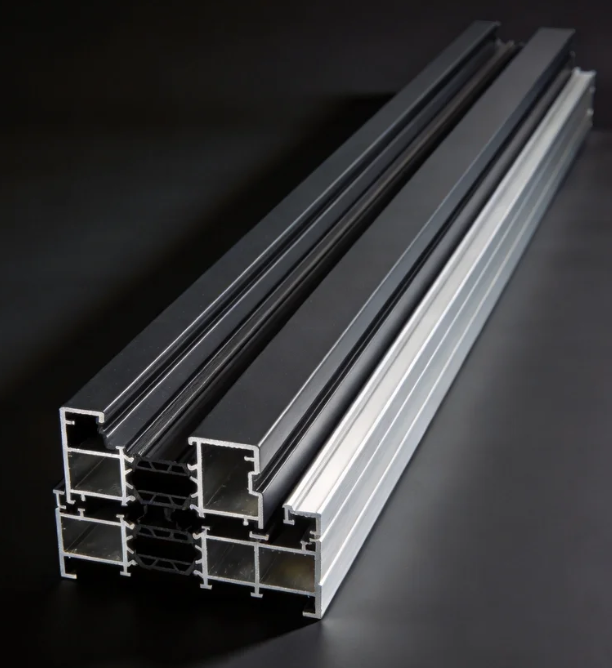
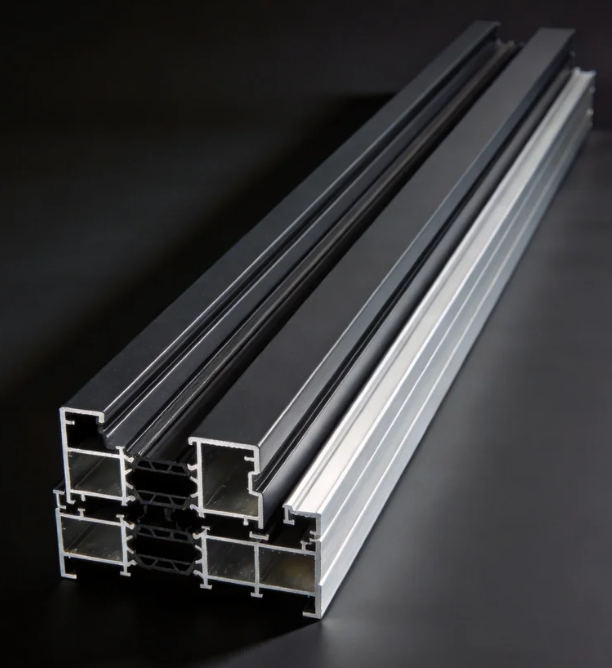
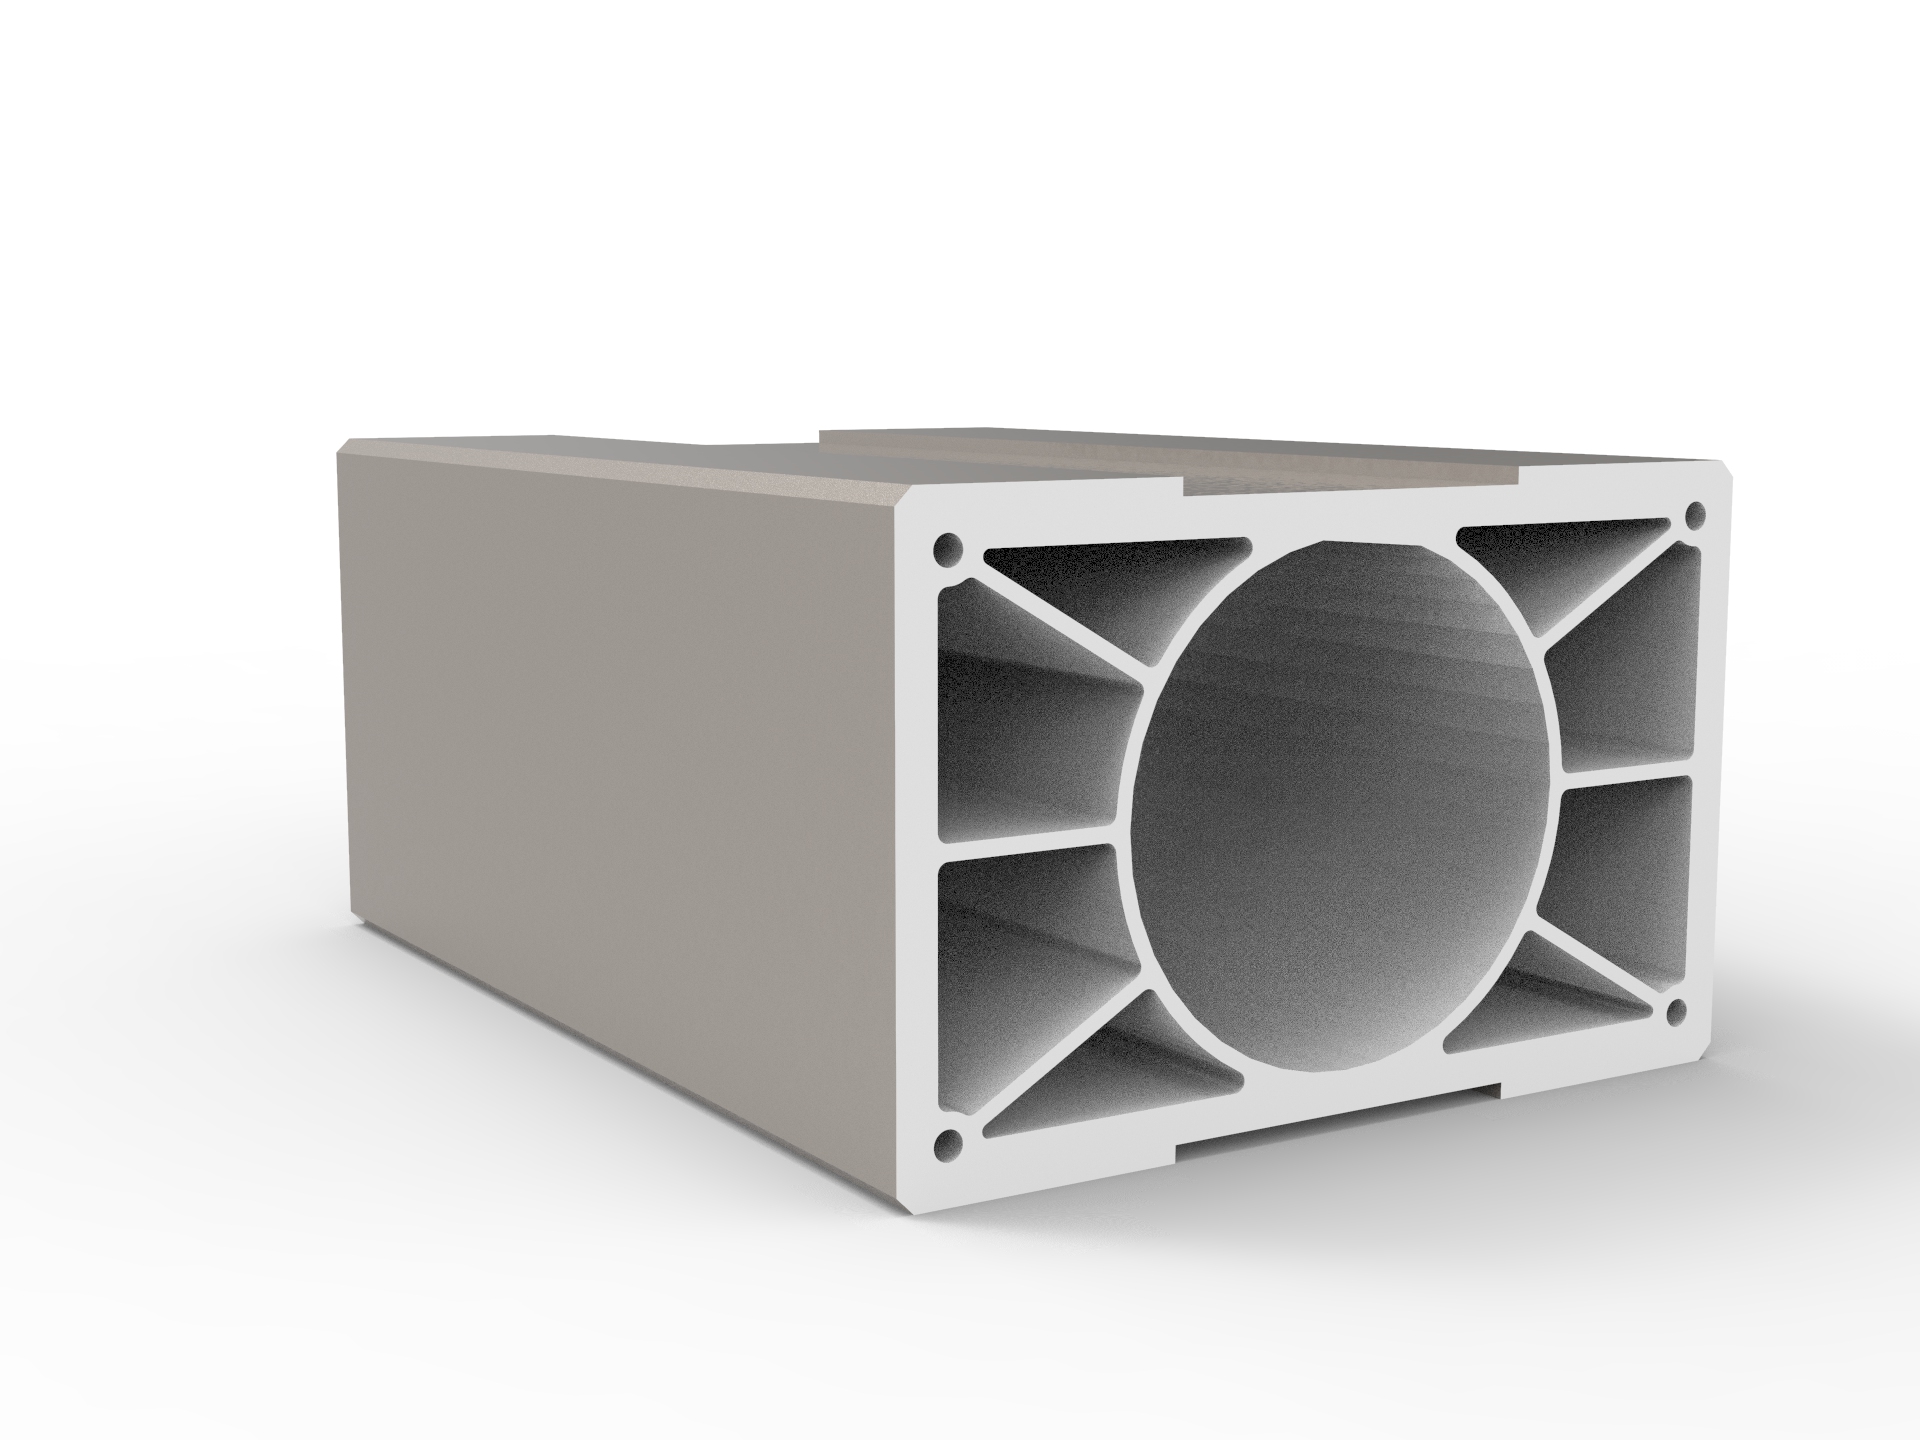
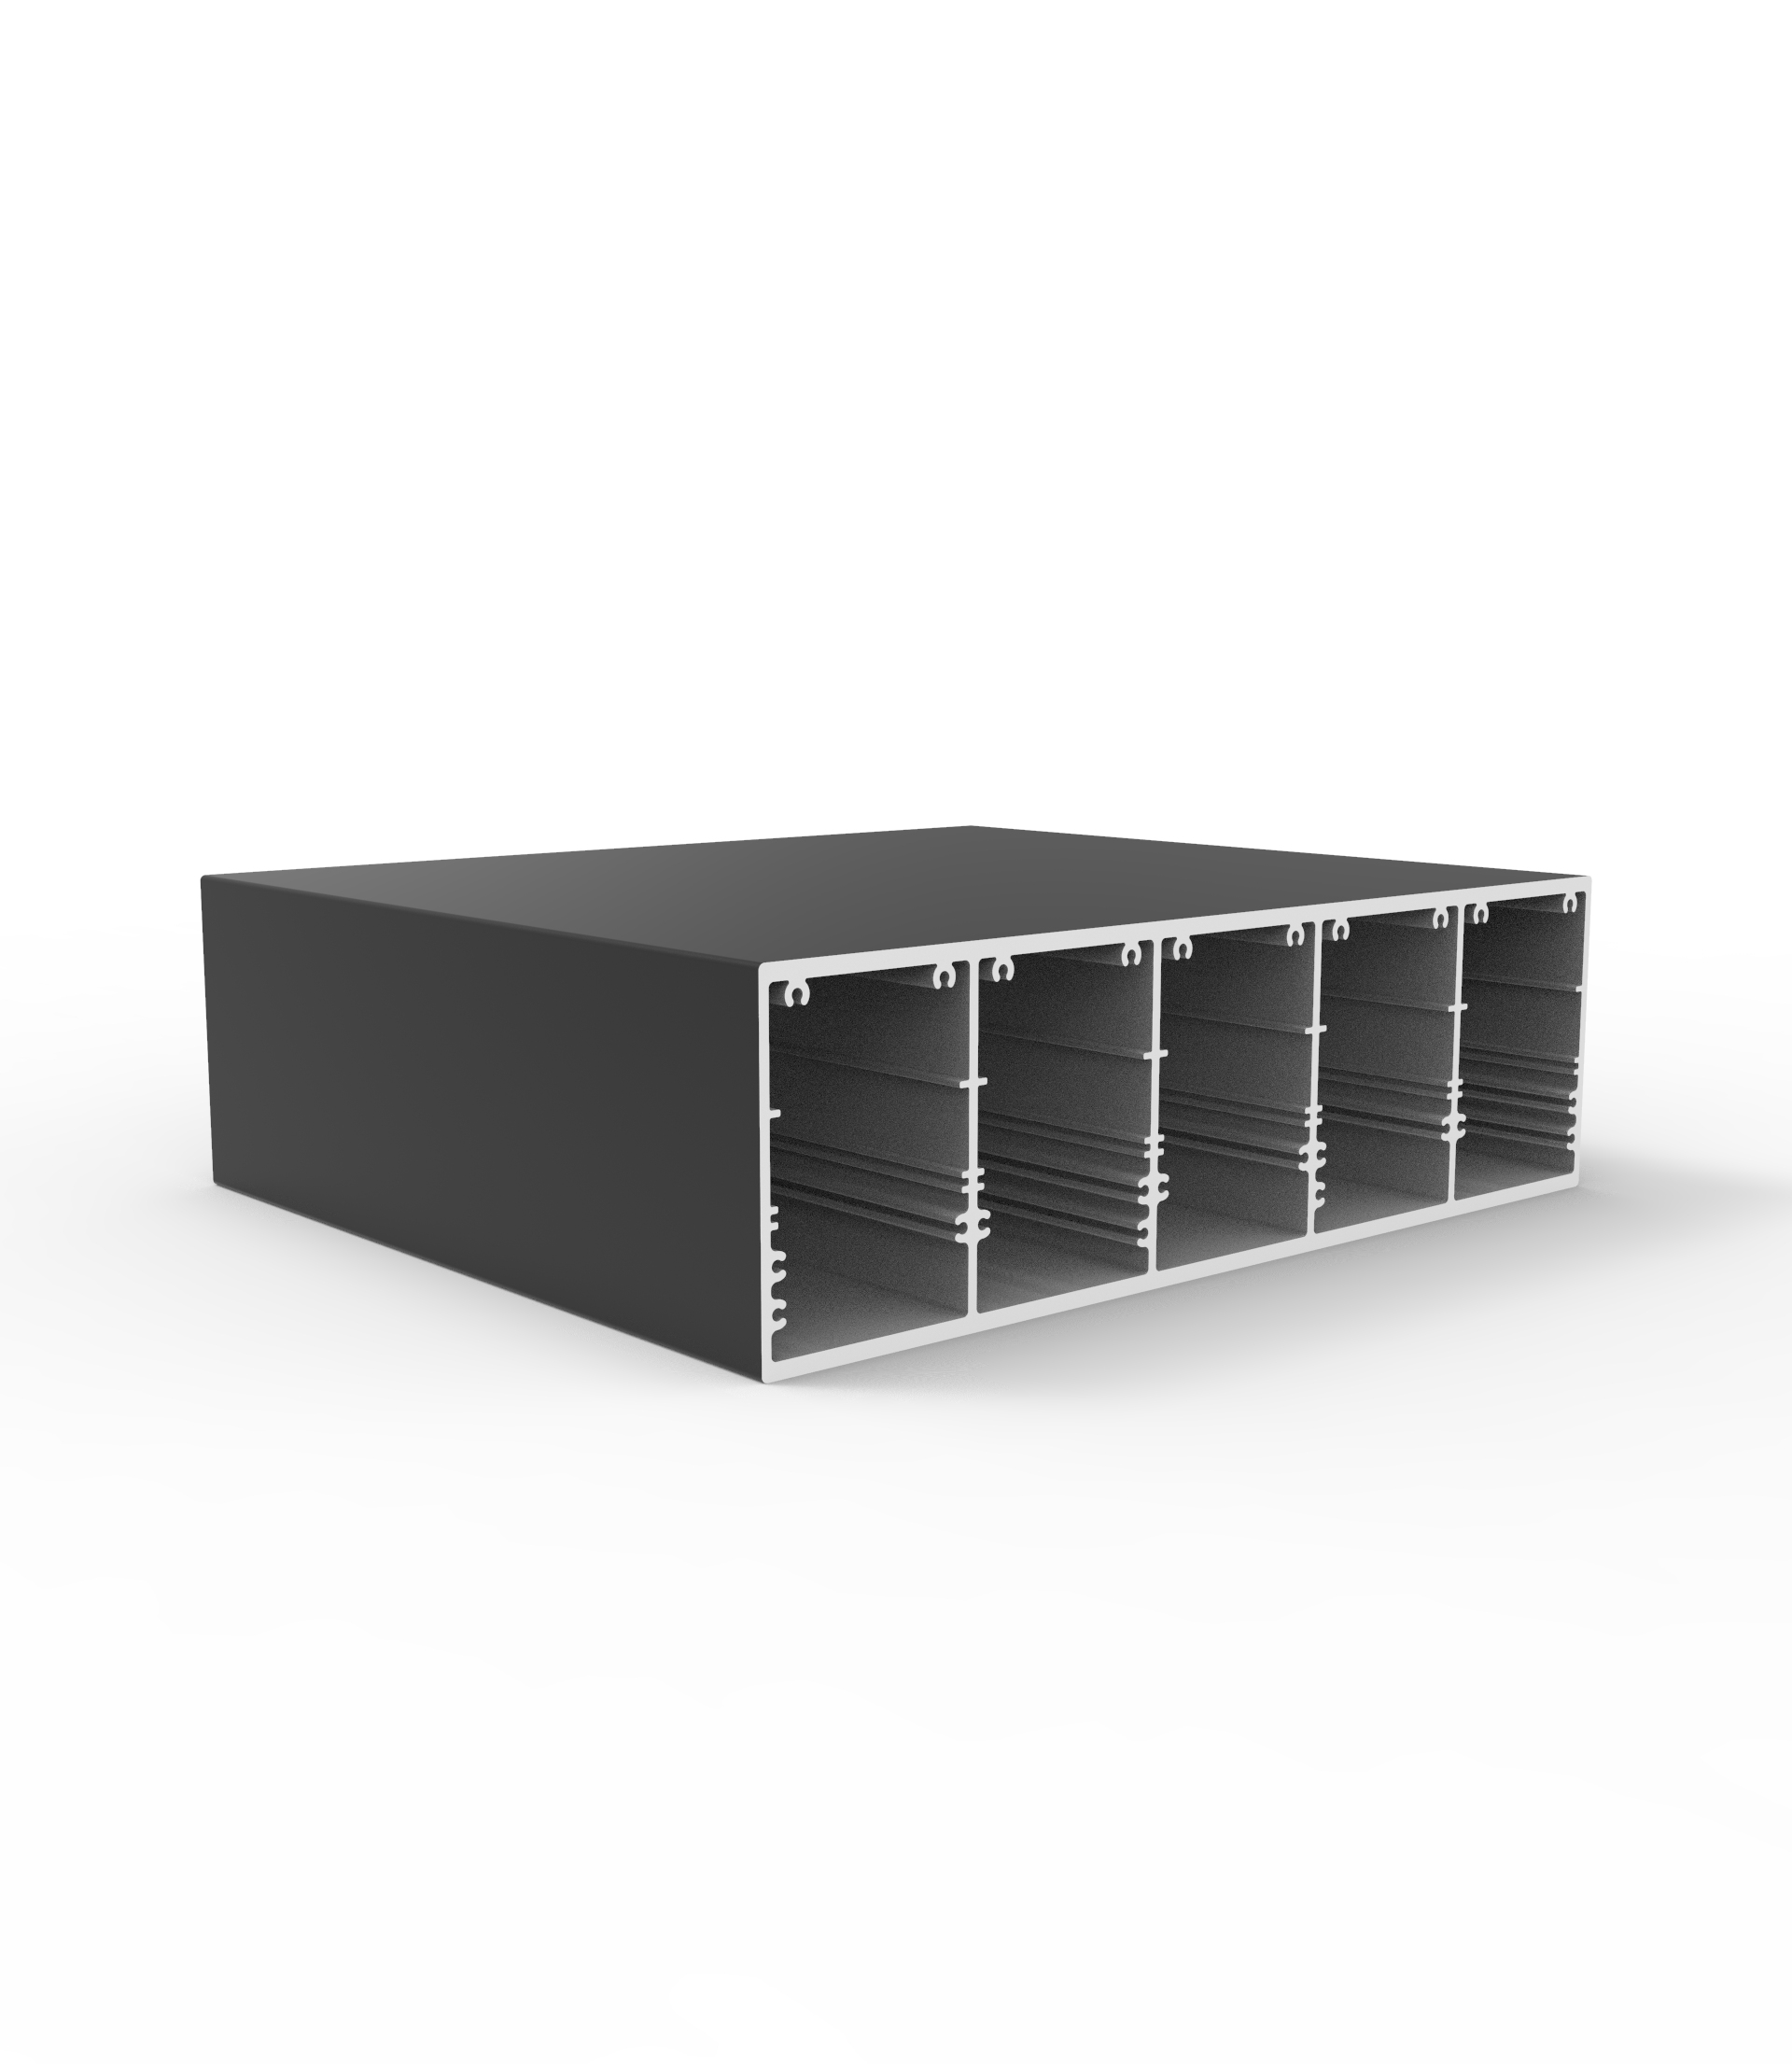
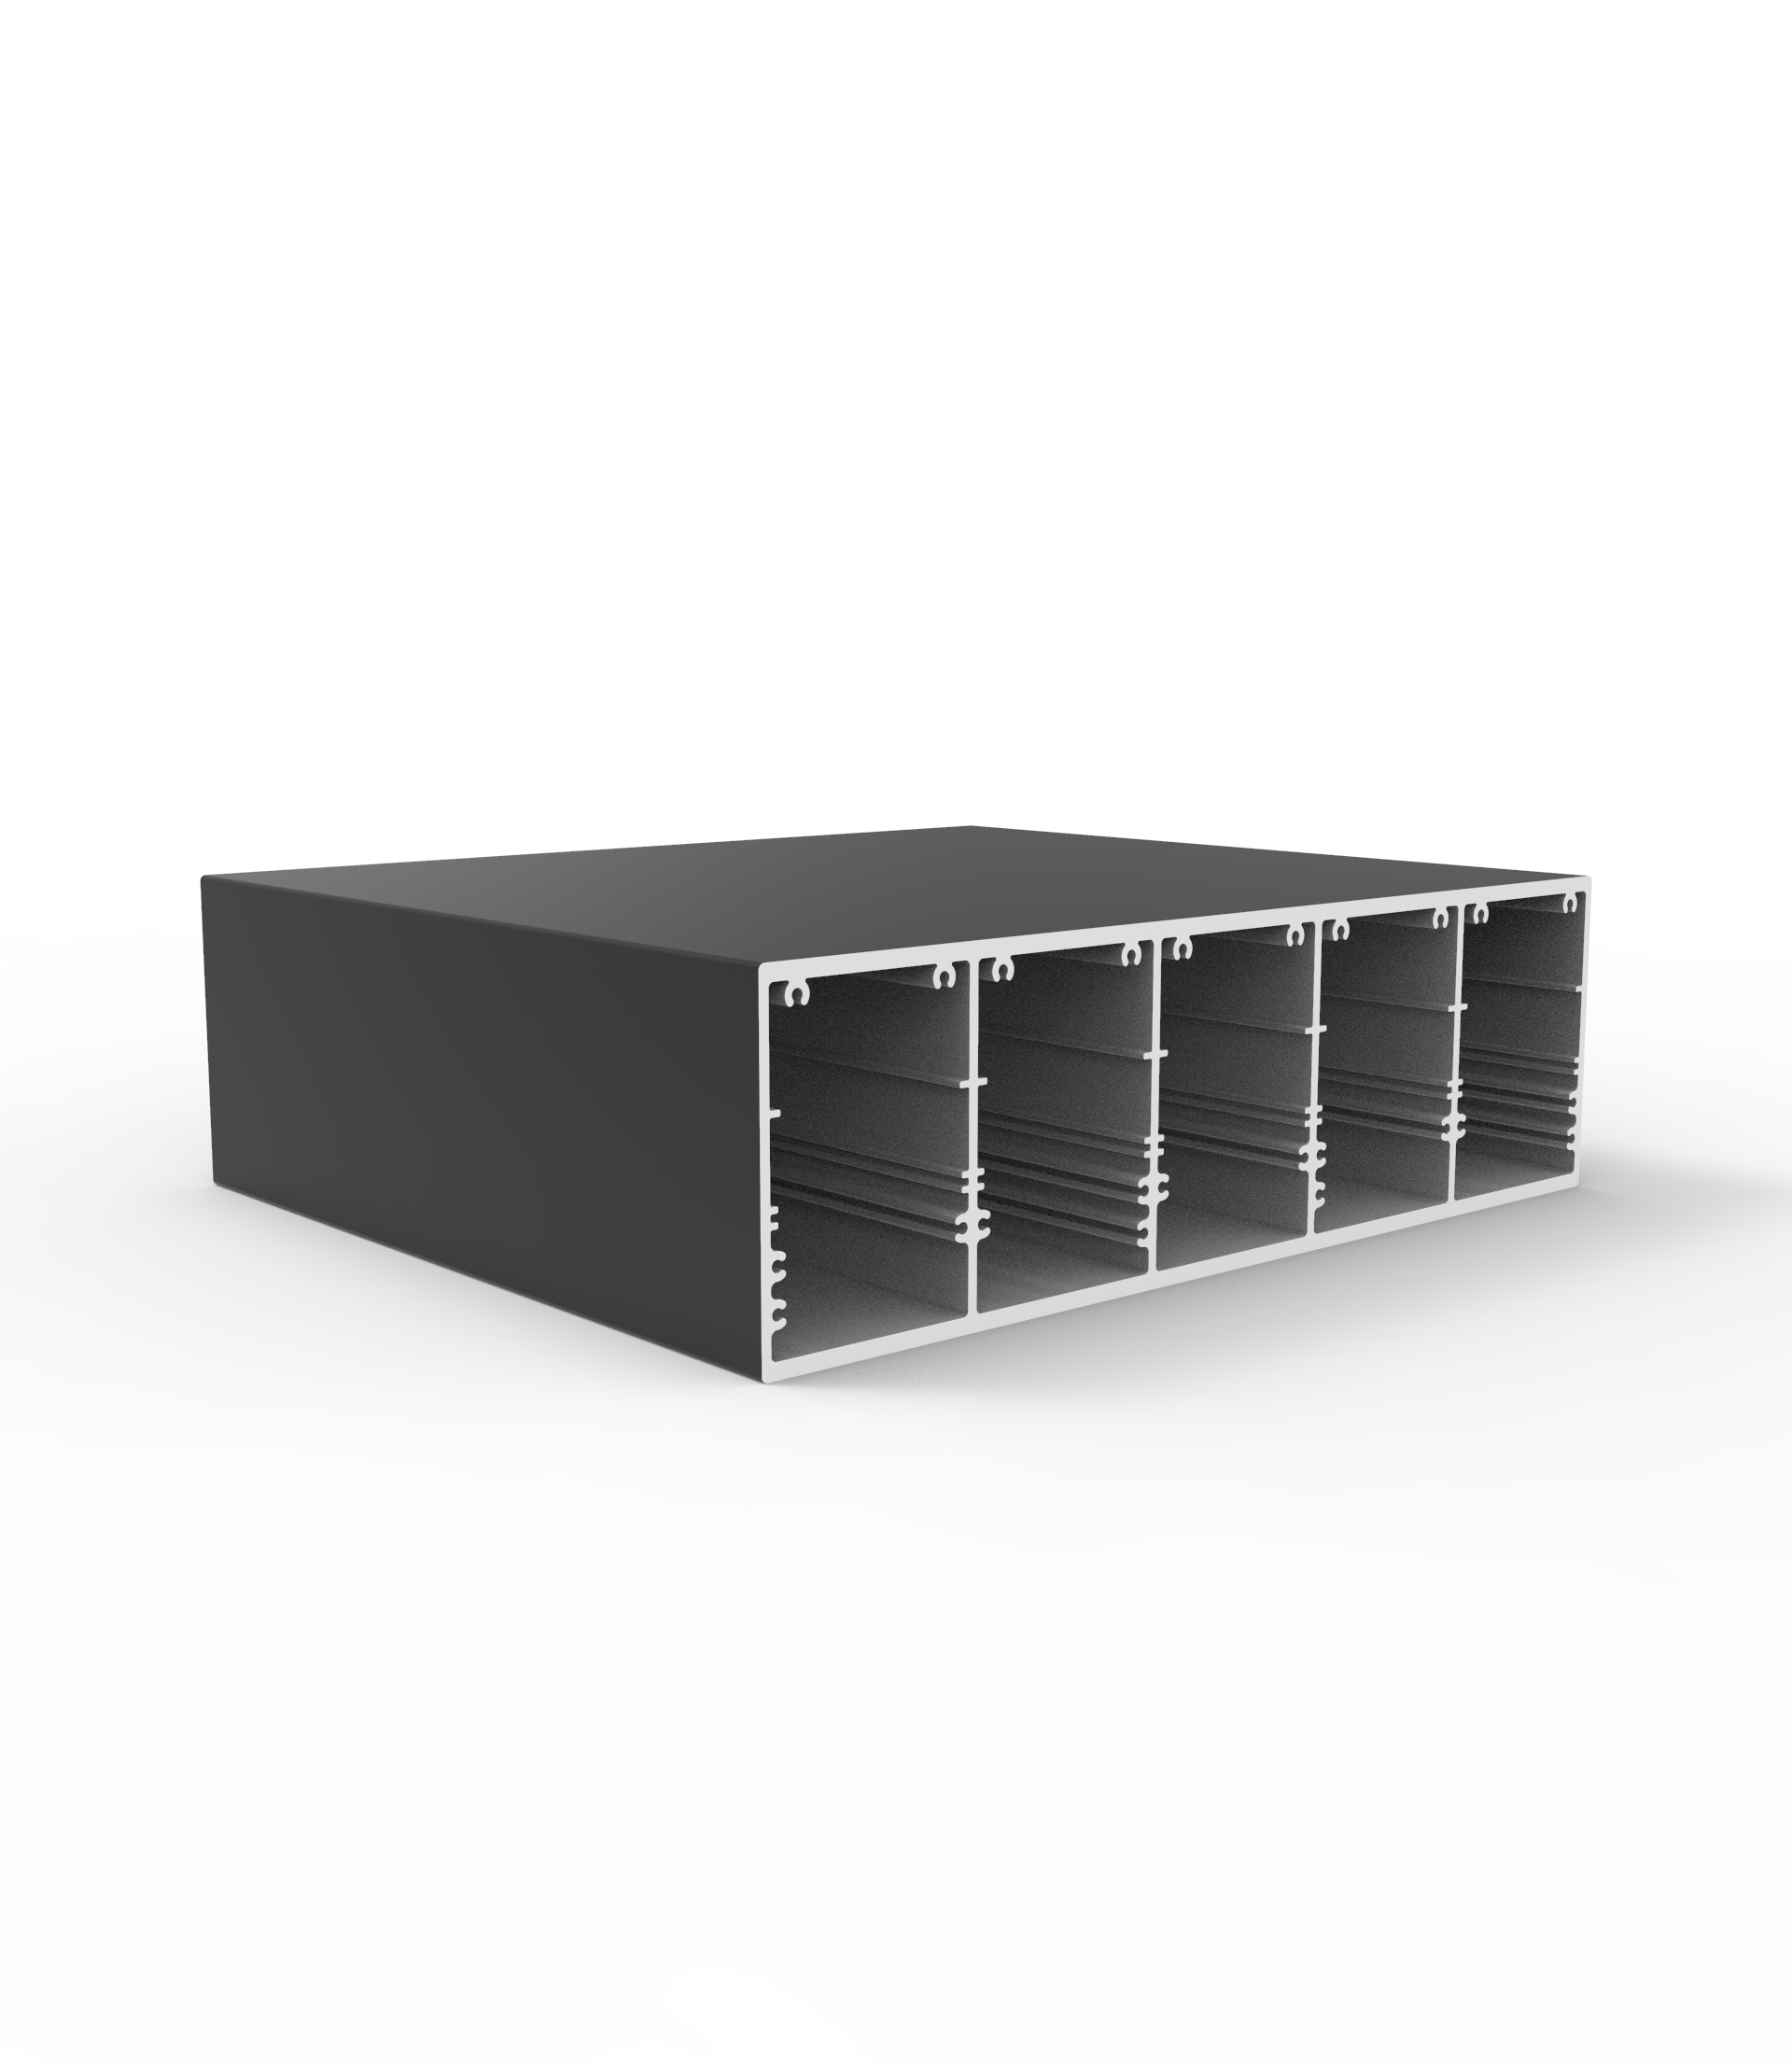
Looking closely at a heavy-duty aluminum linear actuator base reveals how internal webbing addresses this torsional problem. Raised outer shoulders house closed hollow triangular chambers reinforced with internal keyway slots, while the side walls feature horizontal heat-dissipating ridges and bottom T-slots. In deeper U-channel guide rails, complex internal triangular void channels and continuous screw-mounting bosses tie the tall side flanges to a stepped inner floor, which helps limit wall splay under lateral thrust.
Choosing the cross-sectional shape is only half the engineering battle; selecting the wrong aluminum alloy can lead to die tearing during extrusion or premature yielding in service. In industrial machinery, the 6xxx series (aluminum-magnesium-silicon alloys) is widely used because it permits precipitation hardening directly at the extrusion press or in aging ovens. For custom aluminium profiles for automation, three specific alloy and temper combinations handle the vast majority of linear motion requirements.
| Alloy & Temper | Extrudability & Geometry Complexity | Primary Automation Applications |
|---|---|---|
| 6063-T5 | Excellent; supports thin fins and smooth surfaces | Linear motor heat sink housings, intricate sensor tracks, anodized enclosures |
| 6063-T6 | Excellent; supports thin fins and smooth surfaces | Higher-load linear tracking rails, intricate sensor tracks, anodized enclosures |
| 6060-T6 | Available extrusion alloy; confirm geometry and tolerances for the specific die | Precision multi-chamber actuator bases, asymmetric guide rails |
| 6061-T6 | Moderate; requires thicker walls and simpler dies | Heavy-duty robotic gantry beams, high-load CNC linear platforms, structural plates |
When sizing a load-bearing member, use the certified mechanical properties for the specific profile and temper supplied by the manufacturer or testing laboratory, as actual strength varies with the applicable extrusion standard, profile form, and wall thickness.
When a linear rail cross-section includes delicate features, such as closely spaced cooling fins, miniature cable clip grooves, or thin retaining walls, alloy 6063 is a common choice. Because it contains a carefully balanced ratio of magnesium and silicon with minimal copper or chromium additions, 6063 flows smoothly through intricate porthole extrusion dies at moderate billet temperatures. Wall uniformity depends on the profile design, die, and extrusion conditions, and should be confirmed for the specific section.
Beyond geometric intricacy, 6063 generally responds well to electrochemical anodizing, producing a uniform oxide layer with fewer visible dark intermetallic spots than higher-alloy materials. In the T5 temper (cooled from extrusion temperature and artificially aged), it offers reliable dimensional stability for enclosures and light actuator bodies. Specifying the T6 temper (solution heat-treated and artificially aged) raises yield strength toward the upper end of its typical range for higher-load linear tracking rails.
Closely related to 6063, alloy 6060 is frequently specified under European extrusion standards and is an available alloy for this product line. Confirm with the supplier that the specific design and die can produce the required asymmetric sections and hold the required tolerances. If metal flows unevenly through the die bearing, the emerging rail can bow or twist before it reaches the cooling table.
The supplier’s product range for linear rails includes applications such as long-stroke multi-axis slide assemblies and pick-and-place linear guide platforms. Alloy selection depends on the load and the certified properties of the specific profile. When an engineer designs a complex profile with four or five asymmetric internal hollow chambers, confirm with the supplier that the specific die and profile can maintain the required tolerances and uniformity from one end of a long bar to the other. If stress relief is required, specify a stress-relieved temper such as T6511 and confirm availability with the supplier.
Sometimes sheer mechanical strength outweighs the need for thin cooling fins or mirror-smooth cosmetic anodizing. When a gantry beam must support a heavy multi-axis robot or withstand high cutting forces in CNC equipment, engineers often step up to alloy 6061-T6. Thanks to higher alloying additions, including roughly 0.25 percent copper, some 6061-T6 extrusion strength values can overlap those of selected structural steel grades; compare certified properties for the specific materials.
However, 6061 resists deformation inside the extrusion press more than 6063 or 6060. Extruding 6061-T6 typically requires slightly thicker minimum wall sections, larger corner radii, and more conservative hollow chamber geometries to avoid tearing or die mandrel breakage. It also machines cleanly with short, manageable chips, making it well suited to heavy linear rail bases that undergo extensive secondary CNC drilling, tapping, and pocket milling.
Even a strong alloy will underperform in a linear motion assembly if the profile surface waves like a washboard or corrodes in a humid factory. Unlike architectural window frames where visual appearance rules, aluminium profiles for automation depend heavily on geometric form tolerances and surface durability. Understanding what an extrusion press can naturally hold, and how surface finishes interact with those dimensions, helps prevent costly assembly issues.
When mounting two steel linear guide rails in parallel along an aluminum actuator base, three geometric tolerances govern success: flatness across the width, longitudinal straightness, and axial twist. Industry extrusion tolerance standards define permissible deviations in millimetres per metre of length for general and precision profiles. If axial twist exceeds the compliance of the linear bearings, carriage preload can spike, generating heat and accelerating wear on the bearing raceways.
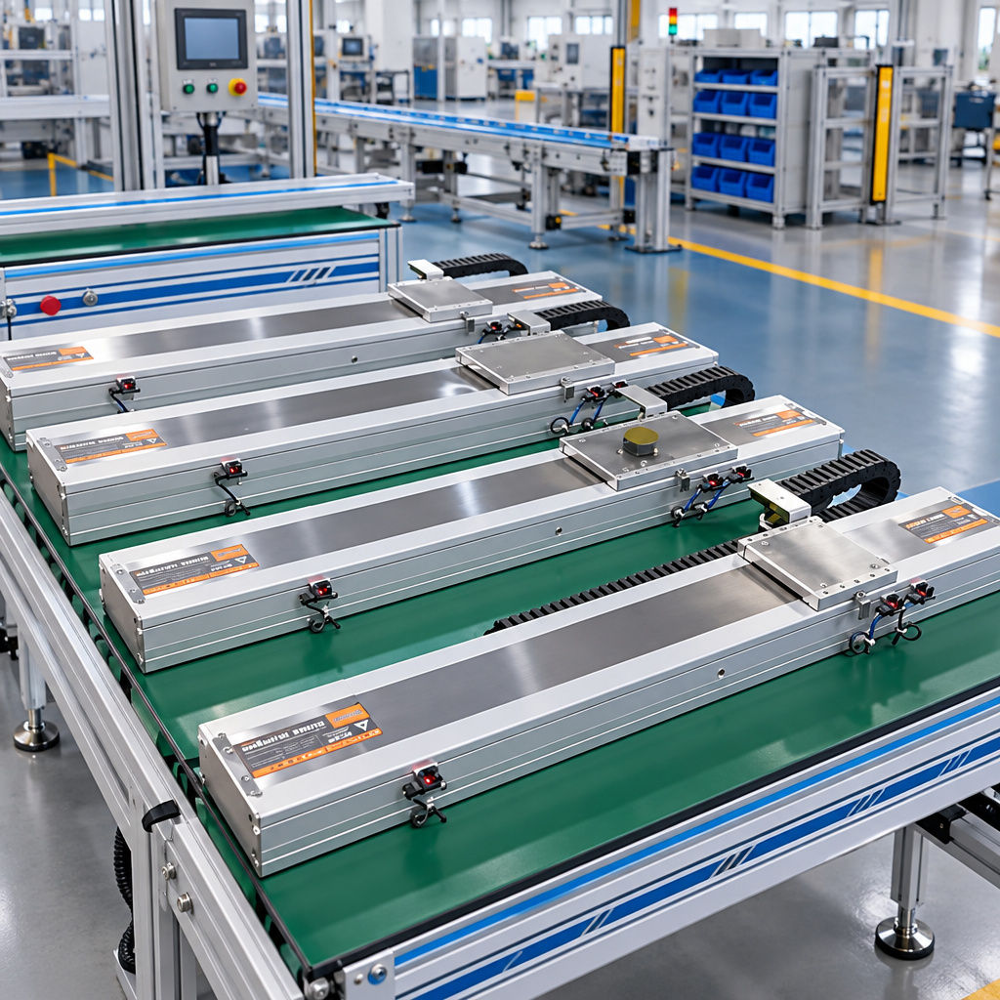
In practical factory builds, precision extrusion can deliver consistent profile geometry for direct assembly in many pick-and-place modules, per the manufacturing approach described for this product line. Direct mounting is conditional on measured or certified profile tolerances meeting the guide manufacturer’s requirements. As seen in assembled linear motor units equipped with stainless steel dust cover strips and polymer cable drag chains, consistent profile geometry supports smooth carriage travel over long strokes. For ultra-precision optical or semiconductor stages requiring very tight flatness, engineers often add a small machining allowance on the rail mounting pads for a final skim pass.
Raw aluminum forms a thin natural oxide skin almost instantly in air, yet industrial environments subject linear rails to coolants, abrasive dust, and sliding friction. Selecting the appropriate surface treatment protects the base metal and matches the operational demands of the automated cell:
Transitioning from a conceptual motion sketch to a production-ready extrusion drawing requires systematic coordination between mechanical design and extrusion tooling engineering. Rushing a profile cross-section into steel die cutting without reviewing wall thickness transitions or secondary machining steps frequently triggers revision delays. Following a structured specification workflow keeps custom linear rail projects on schedule and within budget.
Before finalizing outer profile dimensions, quantify both static payload weight and dynamic inertial forces during peak acceleration:
A well-designed extrusion die shifts labor out of the CNC machine shop and builds assembly features directly into the raw bar:
Once the technical drawing is frozen, engineering specs must align with realistic manufacturing logistics and supply chain capacity. Tooling and unit economics depend on the design and volume; compare supplier quotations for the specific profile and alternative manufacturing processes. For custom aluminium extrusion linear rail sections, standard minimum order quantities typically range from 250 to 500 kg per section, with production delivery times running between 10 and 20 days depending on surface treatment and CNC fabrication complexity, based on figures supplied for this product line.
Partnering with an experienced extruder helps complex multi-chamber linear rails move smoothly from CAD to the assembly bench. Established in 1998, Xinhe Aluminium brings more than 25 years of manufacturing experience across R&D, extrusion, and fabrication, supplying customers in over 50 countries and regions. For us, supporting industrial automation projects means backing custom profile development, spanning length cutting, precision drilling, and multiple surface treatment options, with a library of over 5,000 profile products and an annual capacity of 200,000 tons.
Direct mounting is conditional on the measured or specified profile tolerances meeting the guide manufacturer’s requirements. When produced using precision extrusion dies in alloys like 6060-T6 or 6063-T6, flatness and straightness tolerances may be adequate for standard preload ball guide requirements in many general automation, packaging, and material handling applications. Machine the mounting datum when the as-extruded tolerances do not meet the guide’s accuracy requirements. For ultra-precision CNC machinery or sub-micron semiconductor stages using heavy-preload roller guides, skim-milling the mounting datum after extrusion is advisable.
In dry, climate-controlled indoor factories, bolting austenitic stainless steel (such as A2/304 or A4/316) fasteners into anodized aluminum profiles rarely causes significant galvanic corrosion, since the large aluminum profile acts as an expansive anode relative to the small fastener cathode, and the anodized oxide layer adds electrical insulation. In high-humidity or washdown environments, engineers can reduce thread seizure and localized pitting by using a compatible isolation method for all metal contact surfaces. A nylon washer under the bolt head alone does not isolate the threaded joint. Use only a joint compound or coating system whose manufacturer confirms suitability for the materials and environment, and consider coated helical thread inserts where appropriate.
Tooling and production lead times vary with die complexity and part requirements. For custom linear rail and actuator profiles, the typical minimum order quantity cited for this product range is 250 to 500 kilograms per cross-sectional profile. Once the profile drawing is approved, extrusion, heat treatment, surface finishing, and delivery typically take 10 to 20 days according to the supplied specifications.
Clear or hard-coat anodizing and electrophoresis (e-coating) are options to evaluate for cleanroom, medical, and high-humidity electronics assembly lines. Unlike liquid paint or thick powder coatings that can chip under mechanical impact and shed particulate contamination, anodizing converts the aluminum surface itself into an integral oxide layer. Electrophoresis can add a smooth, sealed film over a specified pretreatment, potentially improving wipe-down characteristics. Verify particle-shedding performance and compatibility with isopropyl alcohol, mild alkaline disinfectants, or other cleaners with the coating supplier for the intended process, as suitability depends on the specified finish and operating conditions.
Designing high-throughput automated machinery requires looking at structural framing and linear actuator bases as active mechanical components rather than passive supports. By leveraging custom cross-sectional geometry, such as closed triangular torsion chambers, integrated cooling fins, and integral guide shoulders, engineers can offset aluminum’s lower elastic modulus while shedding considerable moving gantry weight. Pairing the right geometry with purpose-selected alloys like 6063-T5/T6, 6060-T6, or 6061-T6 helps each axis accelerate cleanly with reduced thermal drift or torsional binding.
When evaluating suppliers for your next generation of machinery, align your CAD tolerances early with an extrusion partner capable of holding tight flatness specs and delivering finished, ready-to-assemble rails. Whether your project requires standard modular framing or custom aluminium profiles for automation such as integrated linear motor housings and precision aluminium extrusion linear rails, specifying the right alloy, temper, and surface finish upfront supports long-term positioning accuracy on the factory floor.
Aluminium Profiles for Kitchen Cabinets: A Practical Guide to Types, Alloys and Finishes
What is the usual MOQ when ordering custom size sliding windows?
What is the typical lead time for shipping floding door orders?
Aluminium Railing Profiles: An Engineering Guide to Alloys, Structural Loads, and Custom Extrusions
LED Aluminium Profile Guide: Thermal Engineering, Extrusion Alloys, and Architectural Integration
Which Awing window specifications matter most for heavy rain protection?
What sustainable Architecture profile options can reduce embodied carbon?
Aluminium Extrusion for Electric Vehicles: Engineering Lighter, Safer NEV Architectures
Aluminium Door Profiles: An Engineering and Sourcing Guide for Modern Architectural Framing
What evidence is needed to claim Awing window seal failure under warranty?
How do I confirm Awing window drawings before production begins?
Can a Shutter prototype confirm both light control and ventilation performance?
Aluminium Extrusion Profiles for Solar Panels: Engineering and Sourcing Guide
The Definitive Guide to Aluminium Extrusion Profiles: Engineering Principles, Modular Systems, and P
Could smart Casement windows become a practical alternative to standard models?
Is it practical to develop a private-label Sliding window for my brand?
What spare parts should I stock for Floding door after-sales support?
Architectural and Industrial Aluminium Angle Profile Guide: Structural Sizing, Alloy Selection, and
How can I prevent my Casement window color formula from being reused?
What coating compliance evidence should I request for Decorative profile?
What information helps a factory understand my Sliding door customization needs?
Are new Shutter materials improving durability while reducing total project cost?
What extra charges should I ask about when buying Casement doors?
What files do I need to provide for a custom Decorative profile?
Should I hold the final Shutter payment until an independent inspection passes?
Are Decorative profile tooling fees normally refundable after reaching volume targets?
What defective-rate threshold should trigger compensation for Casement windows?
How can I tell whether an Architecture profile seller owns a real factory?
Can Shutter slat shapes be customized without creating long tooling delays?
Can a remote audit reliably confirm Sliding window quality controls?
How do I confirm an Architecture profile meets the required wall loads?
Can missing Casement window test reports delay customs clearance or installation?
How should I send CAD details for a custom Casement door design?
Choosing Industrial Aluminium Profiles for Laser Cutting Machines: A Technical Guide
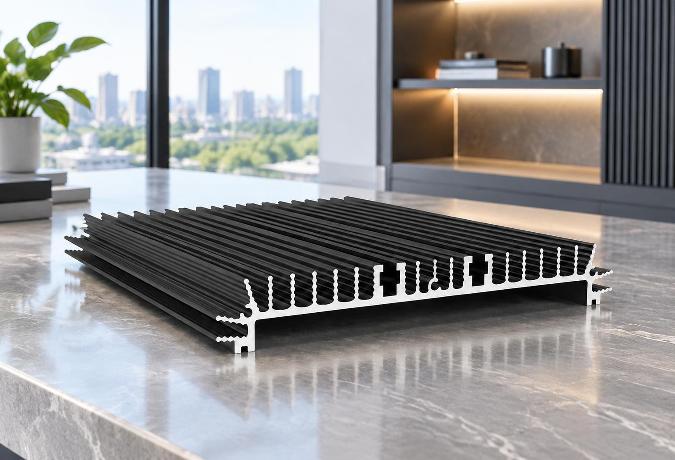
How LED Aluminium Profile Heatsinks Manage Thermal Challenges in High-Performance Lighting
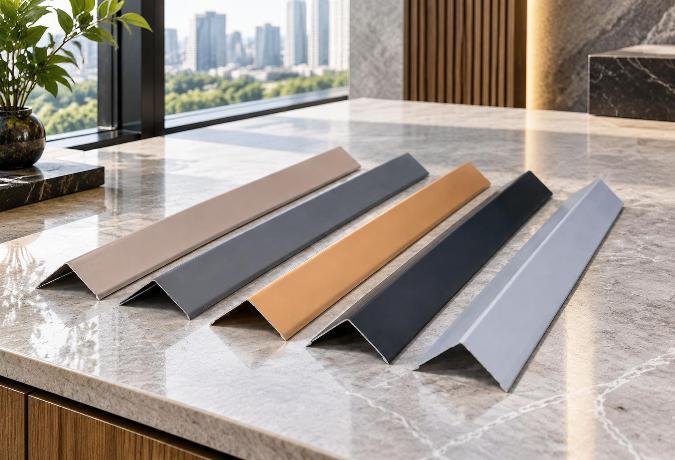
Architectural Aluminium Profiles: Choosing the Right Angle Design for Framing and Trim
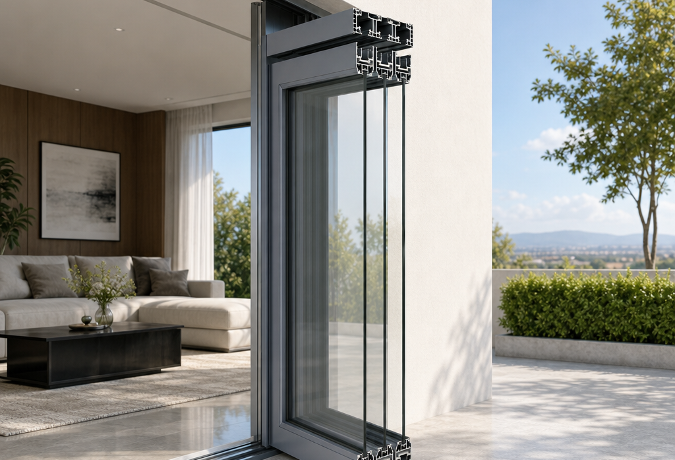
Choosing the Right Aluminium Door Profiles for Narrow-Frame Sliding Systems
Aluminium Window Profiles: Engineering Durable Facades for Modern Buildings
Aluminium Wardrobe Profiles: A Practical Guide to Frames, Tracks, and Finishes
Choosing the Right Aluminium Linear Rail Profile for Motion Systems
Anodized Aluminium Profiles: Material Selection and Practical Applications in Modern Design
Aluminium Decorative Profiles: Design, Installation, and Interior Applications
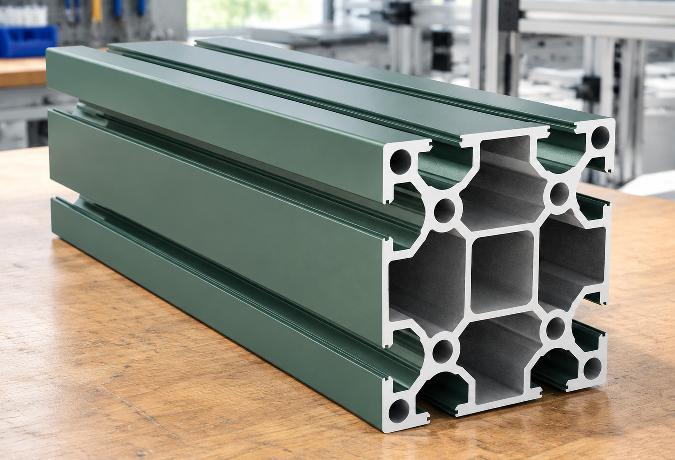
Aluminium Profiles for Automation: A Practical Guide to Modular Frame Design
Aluminium Extrusion for Furniture: Structural Logic Behind Lightweight Precision
Aluminium Thermal Break Profiles: Design Principles and Practical Applications
How do suppliers normally handle Sliding door installation problems overseas?
Choosing the Right Aluminium Balustrade Profiles for Your Project
Aluminium Louver Profiles: Light Control and Ventilation in Modern Architecture
Aluminium Curtain Wall Profiles: Structural Design and Performance in Modern Architecture
Aluminium Trim Profiles: Bridging Aesthetics and Performance in Modern Interior Design
How do I verify Casement window production capacity before signing a contract?
Powder Coated Aluminium Profiles: Durability and Design in Modern Applications
How Aluminium Heatsink Profiles Keep Electronics From Cooking Themselves
How do FOB and CIF change my risks when importing Sliding doors?
What support should I receive if Architecture profile dimensions are wrong?
Inside an Aluminium Profile Factory: How Angle Profiles Are Made and Chosen
What is a realistic MOQ for a first Sliding window trial order?
Which factory records should I review before buying Industrial profile?
Aluminium Extrusion for Machinery: Choosing the Right Profile for Industrial Equipment
Aluminium Extrusion for LED Lighting: Choosing the Right Heatsink Profile
Can a Floding door supplier protect my private design from competitors?
Which Industrial profile tolerances affect assembly accuracy and finished quality?
Can trade credit insurance cover my Architecture profile purchase risk?
Custom Aluminium Extrusion Profiles: Engineering Precision into Industrial Motion Systems
T-Slot Aluminium Extrusion: Structural Framework Design Without Welding
Which recycled-content records are credible for Sliding window procurement?
Aluminium Sliding Door Profiles: A Practical Guide to Frame Design and Performance
How Aluminium Extrusion Manufacturers in China Support Linear Motion Systems
What contract clauses protect my money if Casement door quality is unacceptable?
How do I confirm Sliding door testing equipment is calibrated and current?
Should I visit an Architecture profile plant before placing a large order?
Which compliance tests should a Floding door pass before international shipment?
How do I compare Decorative profile color samples under different lighting?
What payment and price terms make sense for a small Casement window order?
What lead time should I allow for a seasonal Floding door order?
How can I compare Floding door alternatives when supply costs suddenly rise?
Which new Sliding door technologies can lower maintenance costs over time?
How are recycled materials changing the future cost of Floding doors?
How long should a custom Casement door sample normally take to prepare?
What gap between a Sliding window sample and bulk order is acceptable?
Which Decorative profile finishes are becoming more sustainable and cost-effective?
What logistics fees should be listed separately in a Sliding window quote?
How might volatile aluminum prices affect future Sliding window sourcing?
Which audit questions reveal labor risks at a Casement door factory?
Can Decorative profile suppliers provide fast remote guidance for finish defects?
What should a Shutter sample include so I can assess production quality?
Do Sliding door materials need traceability records for customs clearance?
What environmental declarations are useful when importing Architecture profile?
Why Blade Geometry Determines Whether Aluminium Louvers Actually Work
Engineering an Aluminium Angle Profile: Structural Mechanics and Application Realities
What usually drives Architecture profile costs more, alloy or surface treatment?
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
Why the Thermal Break Cavity Matters More Than Frame Thickness in Aluminium Framed Windows and Doors
The T-Slot Groove Geometry That Makes Aluminium Framing Weld-Free
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
Structural Dynamics of Industrial Aluminium Profiles in Laser Cutting Gantries
The Engineering Mechanics Behind High-Performance Aluminium Shutters
What factory documents should I request for a Floding door supplier review?
Which delivery term gives me better control over Decorative profile freight costs?
What low-carbon Awing window materials are gaining wider market acceptance?
Why Sliding Door Track Geometry Determines Wardrobe Longevity
Engineering Mechanics and Surface Dynamics of Aluminium Channel Profiles
Understanding Aluminium Round Tube Specifications for Structural Engineering
Why the 90-Degree Angle in Standard Aluminium Profiles Determines Structural Reliability
How can I ensure a Floding door sample matches the planned mass production?
Why Mullion Thickness Determines How Much Glass an Aluminium Curtain Wall Can Actually Hold
Engineering Dimensional Stability in Aluminium Extrusions for Channel Profiles
Engineering the Structural Framework: The Mechanics of Aluminium Profiles for Kitchen Cabinets
Choosing an Aluminium Profile Supplier: What Actually Separates the Reliable Ones from the Rest
Can Awing window orders ship in batches to avoid project delays?
What response time should I expect for Awing window warranty claims?
Navigating the Supply Chain: Evaluating an Aluminium Profile Manufacturer for B2B Procurement
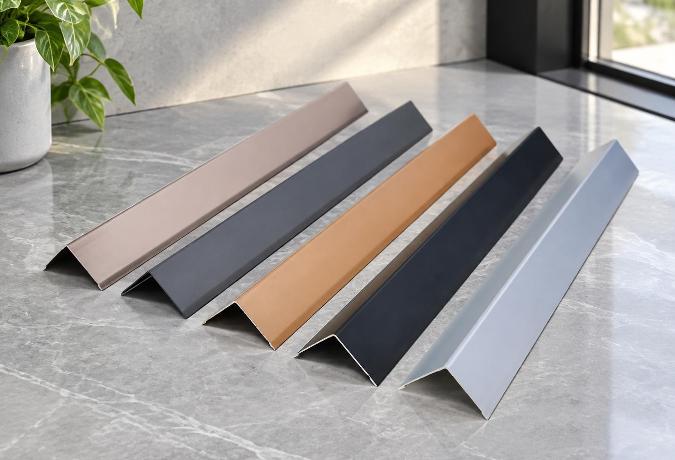
Engineering Structural Integrity Through Precision L-Shaped Aluminium Profiles
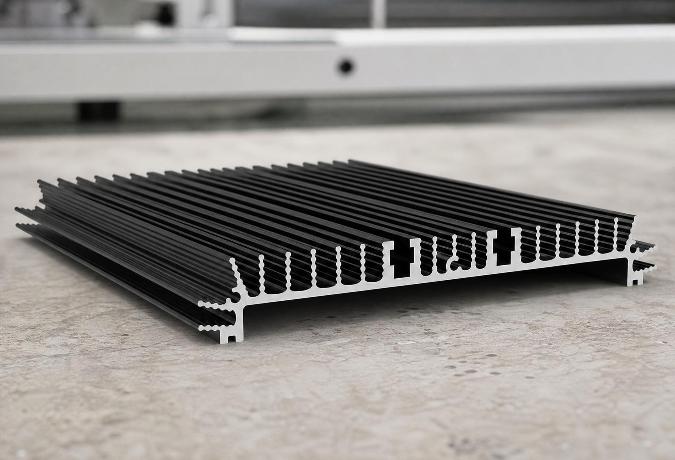
Thermal Dynamics in High-Power Electronics: Engineering Aluminium Heatsink Profiles
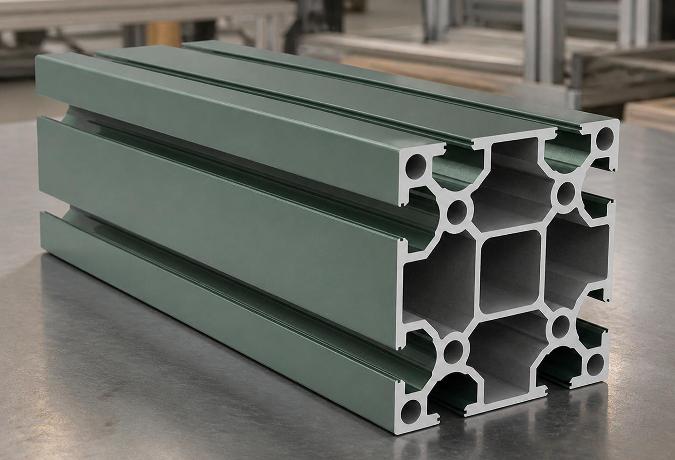
Why the T-Slot Design Determines the Real Strength of Structural Aluminium Extrusions
How long should replacement Sliding window parts remain available after purchase?
Should I expect volume discounts when reordering the same Sliding window model?
The Multi-Strip Sealing Structure Inside Aluminium Windows and Doors
Engineering Lightweight Rail Structures Through Extruded Aluminium Profiles
Why the Frame Width on an Aluminium Sliding Door Determines Your Room’s Light
The Engineering Behind Decorative Aluminium Profiles: Alloys, Surface Treatments, and Edge Protectio
What alternative materials could make Casement doors more resilient and recyclable?
How can I compare Awing window quotes without missing hidden packing costs?
Decoding Structural Tolerances in Aluminium Extrusion Profiles for Channel Applications
Engineering an Aluminium Square Tube for Modern Structural Integrity
Engineering Tolerances and Alloy Mechanics in Extruded Aluminium Construction Profiles
The Engineering Mechanics Behind Aluminium Angle Profiles in Modern Construction
Can an Industrial profile be modified for my assembly without weakening it?
What warning signs suggest a Sliding door seller may disappear after payment?
What energy-efficient alternatives to Casement doors are worth comparing now?
Can a Casement window handle temperature changes without seal failure?
Who pays for unloading and destination handling under Casement door CIF terms?
Custom Aluminium Extrusion Profiles: The Engineering Mechanics of T-Slot Frameworks
Material Transitions and Geometric Stability in Decorative Aluminium Profiles
Can I negotiate a lower Sliding door MOQ for a showroom launch?
Key Advantages of Using Structural Aluminium Extrusion Profiles in Construction
What evidence shows an Awing window factory manages coating waste properly?
How can I protect my deposit when ordering custom Decorative profile?
How do I spot unusually low Industrial profile prices before committing funds?
How can I check that a Shutter supplier is not using unapproved subcontractors?
What contract terms protect my Casement door drawings and branding?
How can I compare Casement door insulation ratings before placing an order?
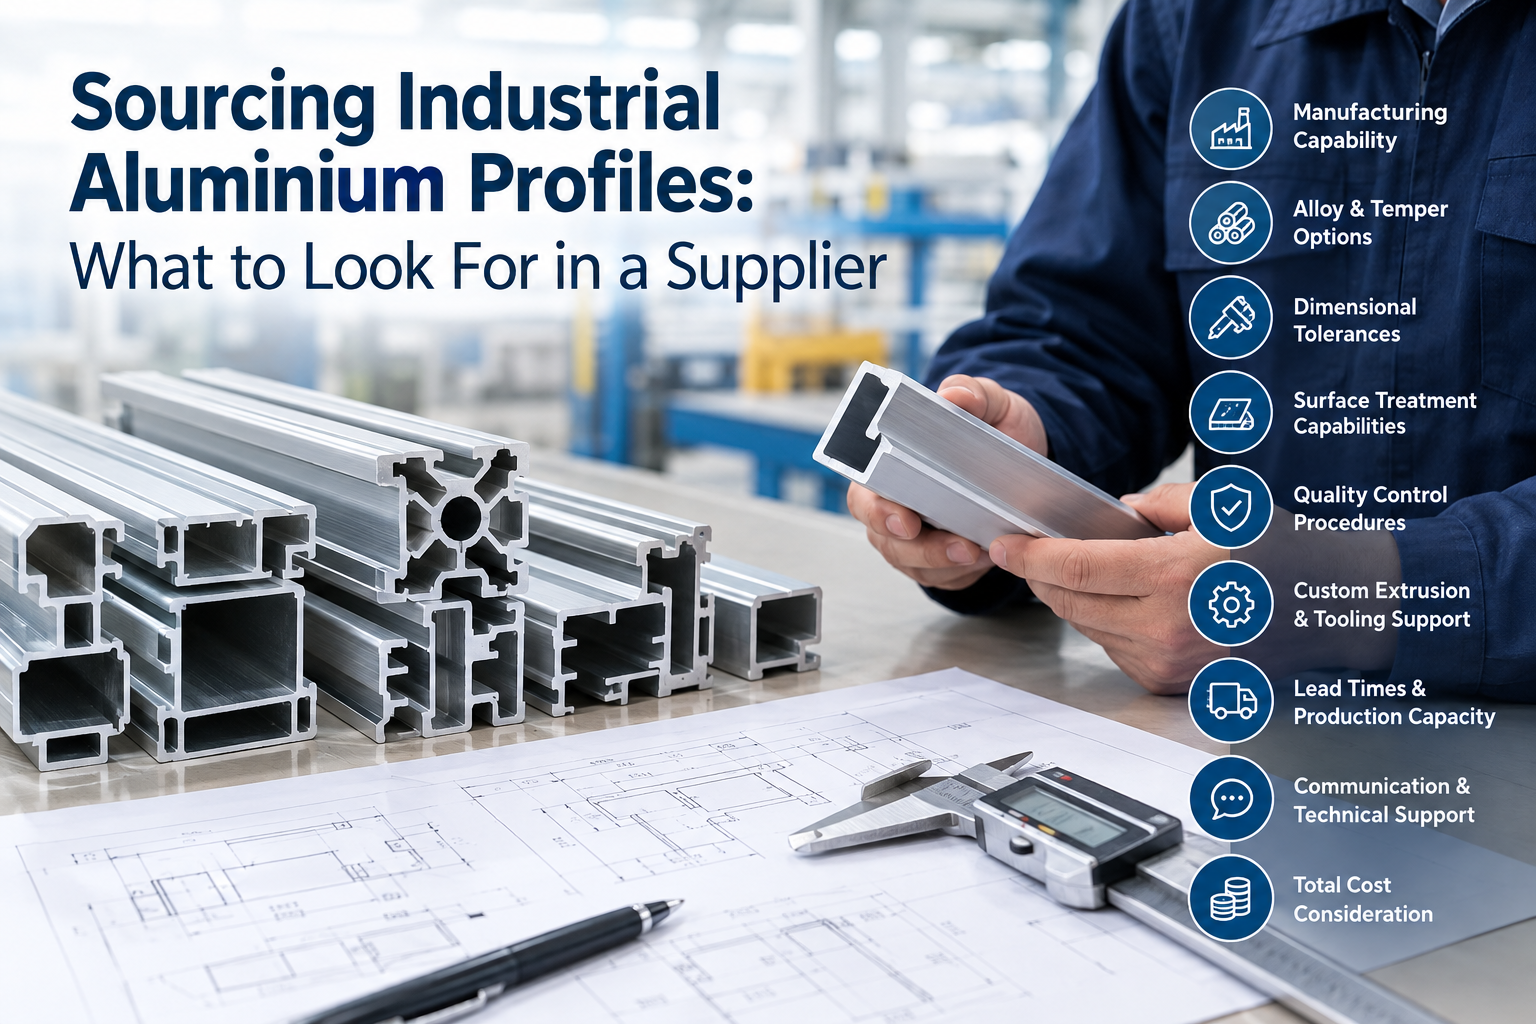
Sourcing Industrial Aluminium Profiles: What to Look For in a Supplier
How do I keep ownership of a custom Architecture profile extrusion die?
The Energy Efficiency Benefits of an Aluminium Frame Sliding Glass Window
How do I check Industrial profile alloy grades against the shipping documents?
What Casement window warranty period is reasonable for an overseas buyer?
How are defective Sliding window units usually replaced internationally?
How can I reduce breakage risks when shipping Casement windows overseas?
The Structural Mechanics Behind Decorative Aluminium Profiles
How Do Engineers Select Industrial Aluminium Profiles for High-Load Frameworks?
What payment structure reduces my risk on a first Industrial profile order?
Should I approve a Casement window sample before checking its hardware strength?
Structural Mechanics of Channel Extrusions in Architectural Aluminium Profiles
Engineering Mechanics of Aluminium Extrusion Profiles in Channel Systems
What functional tests should I perform on a Sliding door prototype?
What payment terms are fair when Decorative profile colors remain unconfirmed?
Is a letter of credit practical for a large Casement window shipment?
How should Industrial profile bundles be packed to prevent transit damage?
Which safety documents should I request for Awing window imports?
What shipping delays commonly affect Architecture profile orders during peak season?
How to Specify Extruded Aluminium Profiles: Costs, Alloys, and Tolerances
Is a Floding door suitable for a wide opening exposed to strong winds?
Structural Integrity in Modular Design: Engineering T-Slot Aluminium Extrusion Profiles
Resolving Corner Stress: The Engineering Mechanics Behind Aluminium Profiles in Architectural Framin
How do Floding door prices change with glass, hardware, and finish choices?
How can I prove Shutter defects remotely without returning every unit?
How can I shorten Awing window sampling without losing critical tests?
Does ordering mixed Shutter sizes usually change the unit price or MOQ?
How should Industrial profile warranty responsibility be shared after assembly?
How should I plan Shutter inventory when ocean freight schedules change?
How do escrow arrangements reduce risk for a new Floding door supplier?
What frame materials make a Sliding window last in harsh coastal weather?
How can I verify that a Shutter certificate matches the actual product?
Can automated Shutters replace manual systems without raising lifecycle costs?
How do I choose the right Casement window size for a windy building?
What should an ethical audit cover at a Decorative profile factory?
How should I document Industrial profile defects before disputing the final payment?
Are lightweight Industrial profile alloys reliable enough for demanding machinery?
Are thermal-break casement windows becoming a better long-term choice than standard frames?
What is a realistic MOQ for custom sliding windows without pushing up unit cost?
What casement window specs should I compare for windy and rainy project sites?
Are there better material options for sliding windows if aluminum prices rise?
How do I ensure aluminum casement windows can handle extreme coastal winds?
What is the typical minimum order quantity for commercial sliding windows?
Are there energy-saving alternatives to sliding windows that reduce material and maintenance costs?
Are energy-efficient Awing windows a practical alternative for reducing long-term building costs?
What alternatives to traditional sliding doors can lower costs without sacrificing durability?
What alternatives to industrial profiles can reduce material costs without hurting strength?
Extruded Aluminium Profiles: Flexible Manufacturing for Diverse Customer Needs
Why Aluminium Curtain Walls Are Popular in Modern Architecture
How do I choose a decorative profile that stays stable in humid or harsh environments?
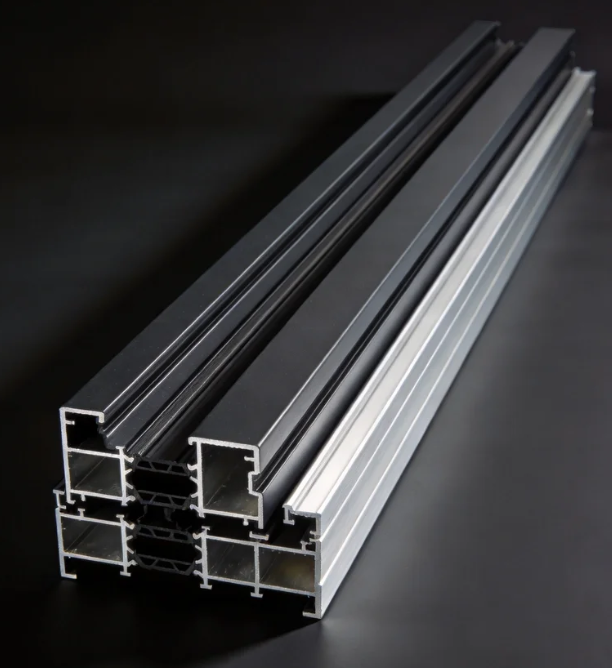
How do I choose an architecture profile that stays stable in harsh outdoor conditions?
How can I compare Awing window specs to avoid poor performance in harsh weather?
How can I compare Sliding door sizes and hardware ratings for harsh commercial environments?
How do I choose the right shutter specifications for harsh climates without overpaying?
What eco-friendly alternatives to folding doors can cut costs without hurting durability?
How do I choose the right shutter specifications for harsh weather without overpaying?
What eco-friendly casement door materials can lower costs without hurting durability?
What newer materials can replace industrial profiles without raising costs or supply risks?
How do I choose a decorative profile that stays stable in humid, high-traffic spaces?
What sustainable material alternatives can replace aluminum architecture profiles?
What should I check in Awing window specs to ensure reliable performance in harsh weather?
How can I compare Sliding door sizes and thermal ratings for harsh climates before buying?
What newer materials can replace aluminum in awning windows without raising our costs?
How do I choose the right Sliding door specs for smooth operation in harsh environments?
How do I choose a folding door that stays stable in harsh weather and heavy daily use?
How can I choose the right shutter specifications for harsh weather and long-term use?
How do I compare casement door U-values, hardware, and weather sealing before buying?
How do I choose the right industrial profile size for strength and load needs?
How do I choose the right shutter specifications for harsh weather and long-term commercial use?
How do I choose the right Casement door size and hardware for harsh weather?
What greener alternatives to decorative profile can cut costs without hurting durability?
What lower-cost, eco-friendly materials can replace decorative profiles?
What lower-carbon alternatives to aluminum architecture profiles are practical for our project?
How can I compare sliding door systems for insulation, security, and long-term use?
What is the standard production lead time for bulk orders of folding doors?
How do I choose the right Awing window size and glass specification for harsh weather?
How can I test shutter samples so the final bulk order matches their quality and finish?
Can suppliers make custom double glass casement doors from my CAD drawings?
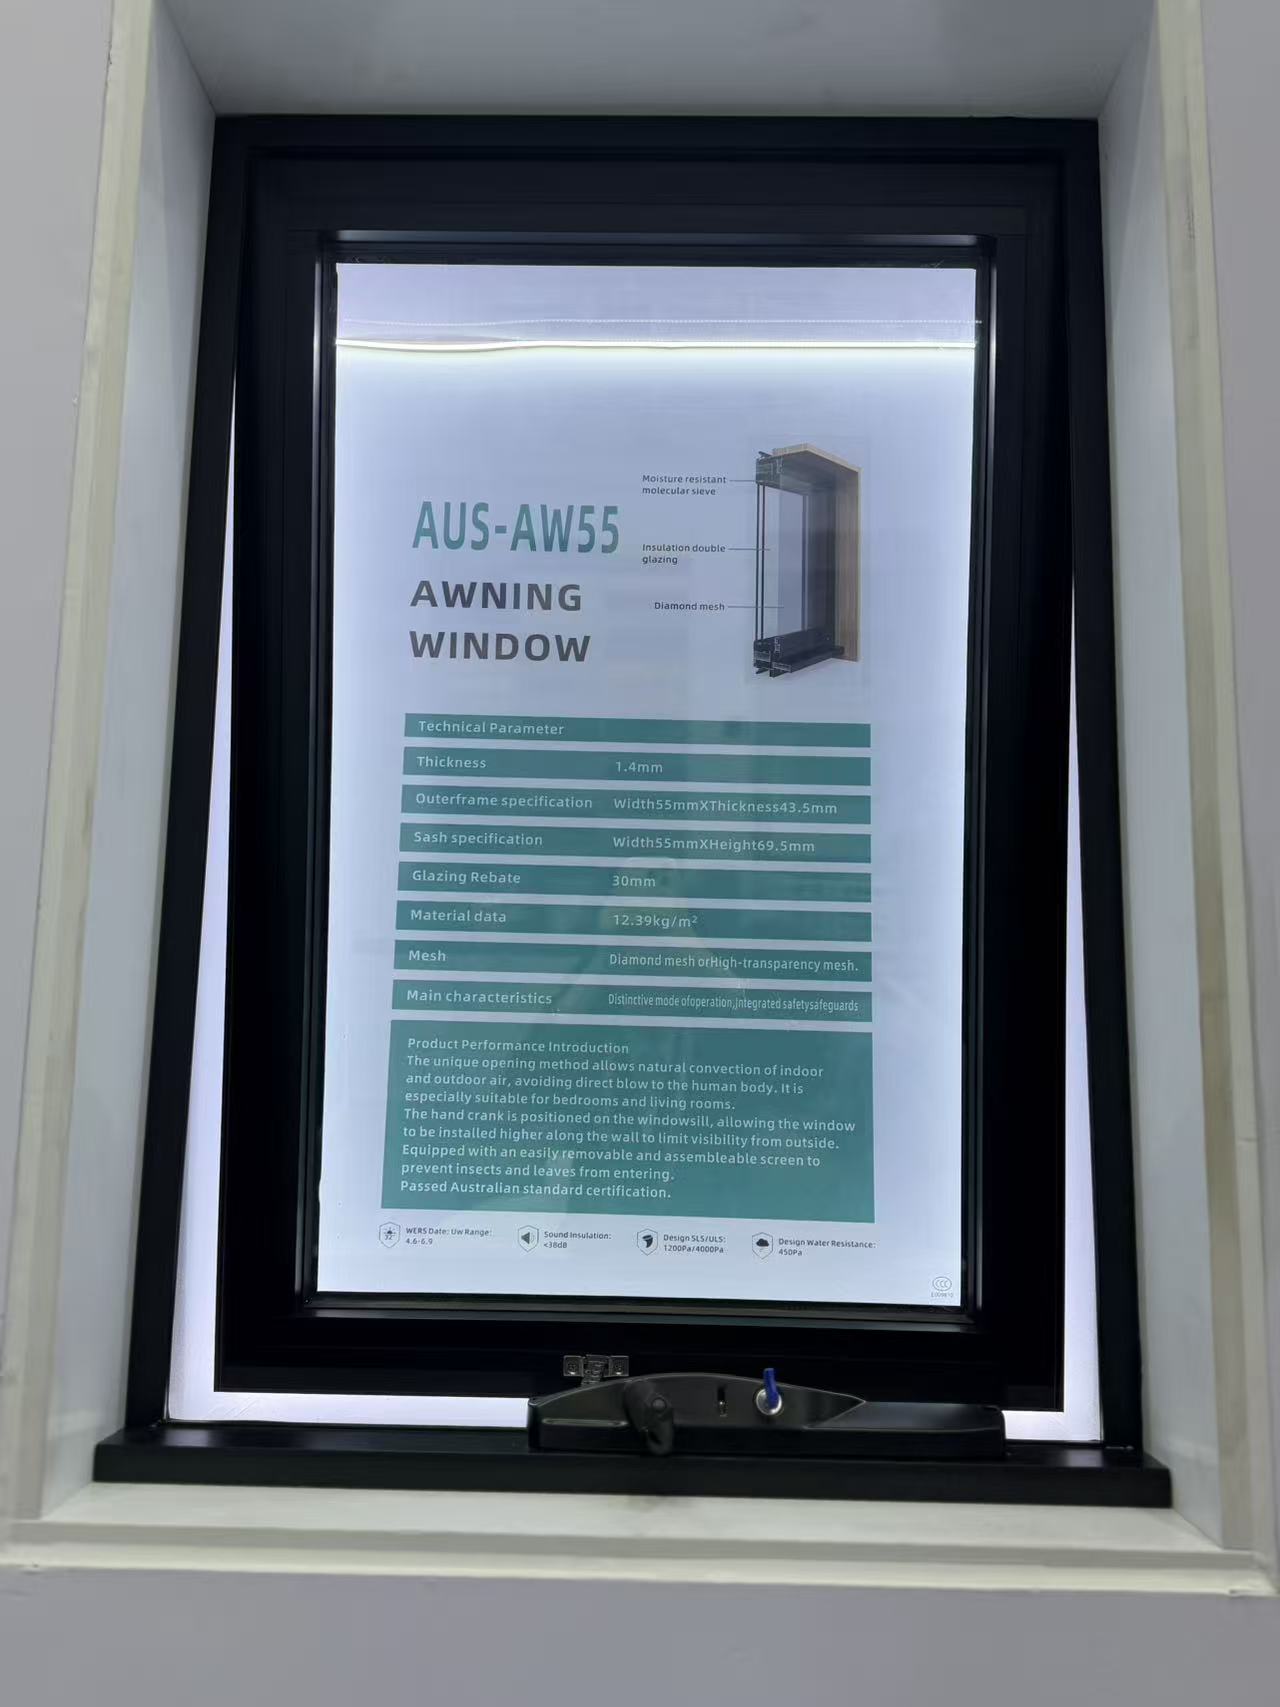
What safety certifications should I request when importing awning windows?
How long does it usually take a factory to make custom shutter samples?
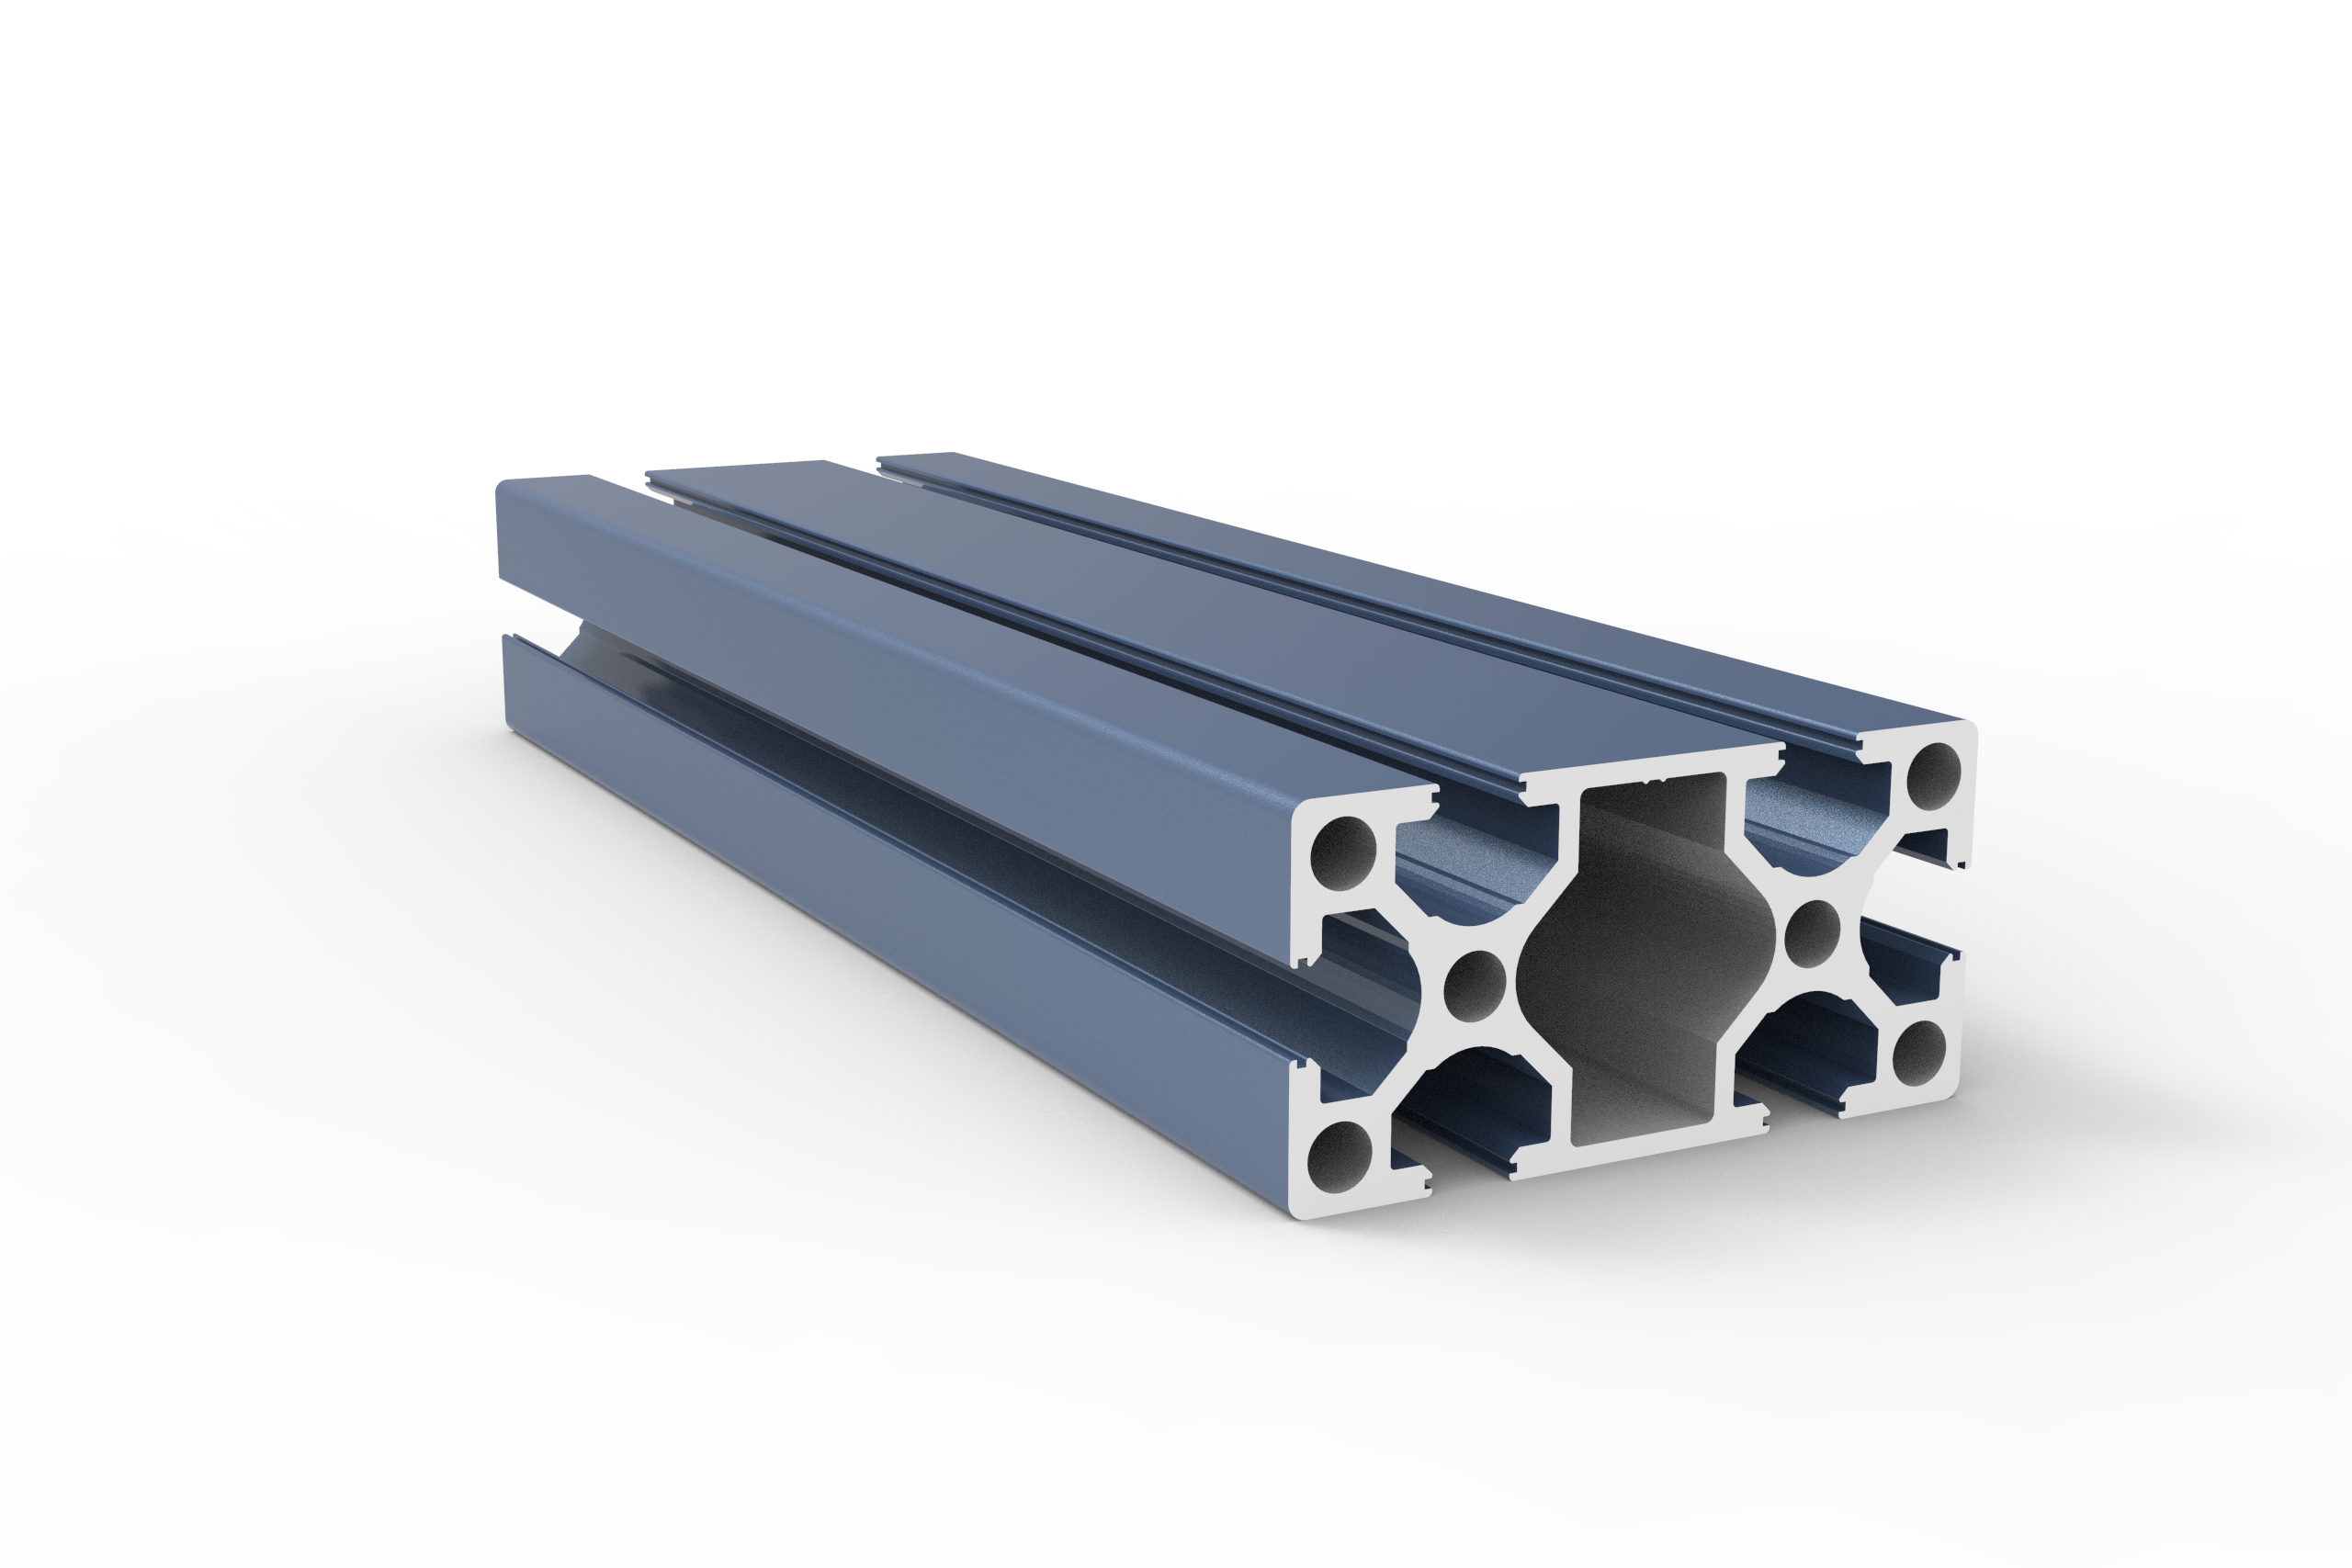
What T-slot industrial profile size is best for a heavy duty machine frame?
How do I choose the right stainless steel decorative profile for high humidity areas?
How do I choose the right aluminum architecture profile for coastal buildings?
How do I choose the right stainless steel decorative profile for high humidity areas?
What wind load specs should I check for aluminum casement windows in coastal high-rises?
How do I know which aluminum industrial profile alloy is best for heavy machinery frames?
How do I choose the right alloy grade for aluminum architecture profiles?
How do I select the right heavy-duty hardware for exterior commercial floding doors?
How do I select the right glass thickness for bulk awing window orders?
What frame thickness is recommended for commercial aluminum casement doors?
What frame thickness is best for high-rise commercial sliding windows?
How to choose weather resistant aluminum floding door specs for commercial use?
How do I choose the best water tightness rating for commercial awing windows?
How do I choose the right frame material for commercial casement doors?
How do I choose the right wind load rating for sliding windows in coastal areas?
What is the best material for outdoor decorative profiles to prevent rust and fading?
How do I choose the right track thickness for high-traffic commercial sliding doors?
How do I choose between PVC and basswood shutters for high-humidity areas?
How do I choose between double and triple glazing for casement windows in cold climates?
How do I choose the right industrial profile thickness for heavy-duty cnc machine frames?
How do I choose the right alloy for outdoor architecture profiles to prevent corrosion?
Can you design a slim frame profile for modern minimalist look?
How do I choose the right wind-resistant floding door for a coastal commercial building?
What key specs ensure a casement window can withstand heavy rain and high winds?
How do I choose the right aluminum alloy grade for heavy-duty industrial profiles?
Which alloy grade of architecture profile is best for coastal areas to resist rust?
How do you pack windows to prevent glass breakage in transit?
Are slim-frame thermal break systems replacing traditional ones?
Does the price include the matching frame and installation kit?
How do you protect our proprietary design drawings from leaks?
How do I choose the right decorative profile for high-traffic hotel lobbies?
Is your factory the actual manufacturer or a trading partner?
Is it possible to 3D print a prototype before cutting steel?
Do you outsource any part of the painting process to others?
How do you handle replacement parts for damaged track rollers?
Do you accept escrow payments through third-party platforms?
Do you have ISO 9001 certification for your production line?
Are there extra fees if we pay via bank telegraphic transfer?
What is the price difference between powder coat and anodized?
What is the warranty period for the lock and hinge hardware?
What is your policy for dimensional deviations in the batch?
What happens if the shipment is delayed due to factory error?
Do you offer online technical support if color fading occurs?
Is it possible to engrave our brand logo on the tension screw?
Do you offer credit terms for long-term purchasing partners?
Can you palletize the shipments for easy forklift unloading?
What are the latest eco-friendly finish trends for decorative profiles in modern interior design?
What are the tooling cost and design limitations for customizing heavy-duty industrial profiles?
Has your architecture profile manufacturing facility passed ISO 9001 certification?
Can we use Alibaba Trade Assurance for our initial sliding door order to mitigate risk?
Do you provide free corner samples of the casement window frame for color verification?
Is it possible to custom-match a specific RAL color for a decorative profile order?
Can I request a 3D-printed sample before ordering a custom industrial profile mold?
Can you extrude an architecture profile based on our proprietary CAD drawings?
What thermal performance certifications does a sliding door need for the UK market?
How are heavy floding door panels crated to ensure safe unloading at the job site?
Can we arrange our own freight forwarder to pick up the casement door shipment FOB?
What is the estimated ocean freight transit time for a shutter shipment from China to Europe?
How can we source replacement seals for your awing window models in the future?
How are sliding windows typically packaged to prevent glass breakage during ocean transit?
What is the average lead time for a 40ft container of standard aluminum casement windows?
Are there any extra tooling fees if my decorative profile order doesn’t meet the MOQ?
Can I get 3D printed prototypes of custom architecture profiles before committing to mold tooling?
How is smart glass technology being integrated into modern residential sliding door units?
What options do you have for customizing the threshold height of an aluminum floding door?
What thermal break technology should I look for in a heavy-duty aluminum casement door?
What quality control processes do you perform on shutter hardware before final assembly?
Do you offer DDP shipping terms for awing window orders delivered to our warehouse?
Is it possible to order a fully functional sliding window sample for mock-up testing?
Do you provide replacement hardware if the casement window hinges fail within 5 years?
How do you handle claims for decorative profile items damaged during transit?
What is the standard MOQ for custom-extruded aluminum industrial profile orders?
How does the order volume affect the per-ton price of custom architecture profile designs?
What is the warranty period for the rollers and tracks on your heavy-duty sliding doors?
How can we secure our deposit when purchasing high-value custom floding doors from a new supplier?
Can your factory match custom anodized colors for decorative profiles based on physical samples?
Is there a lighter alternative to aluminum industrial profile structures for robotics?
What payment security measures do you have for custom architecture profile tooling fees?
Can I order a sliding door with custom grid patterns between the glass panes?
How do you protect buyers against financial loss if the floding door shipment is delayed?
Are slim-frame aluminum casement door designs becoming more popular in modern offices?
What is your policy for replacing shutter components that arrive with color mismatch?
What kind of remote technical support do you offer for sliding window installation?
What is the maximum safe size for a top-hung awing window in commercial projects?
What environmental management standards does your decorative profile plant follow?
What is the standard lead time for producing a 40ft container of casement window orders?
What is the warranty period for the anodized finish on your industrial profile?
What are the latest eco-friendly trends in architecture profile manufacturing?
What is the average wholesale price per square meter for double-glazed sliding door systems?
How do I calculate the structural load requirement for a 5-panel exterior floding door?
Do your exterior shutter systems comply with Florida building codes for hurricane protection?
Do you offer Letter of Credit (L/C) payment options for casement door bulk orders?
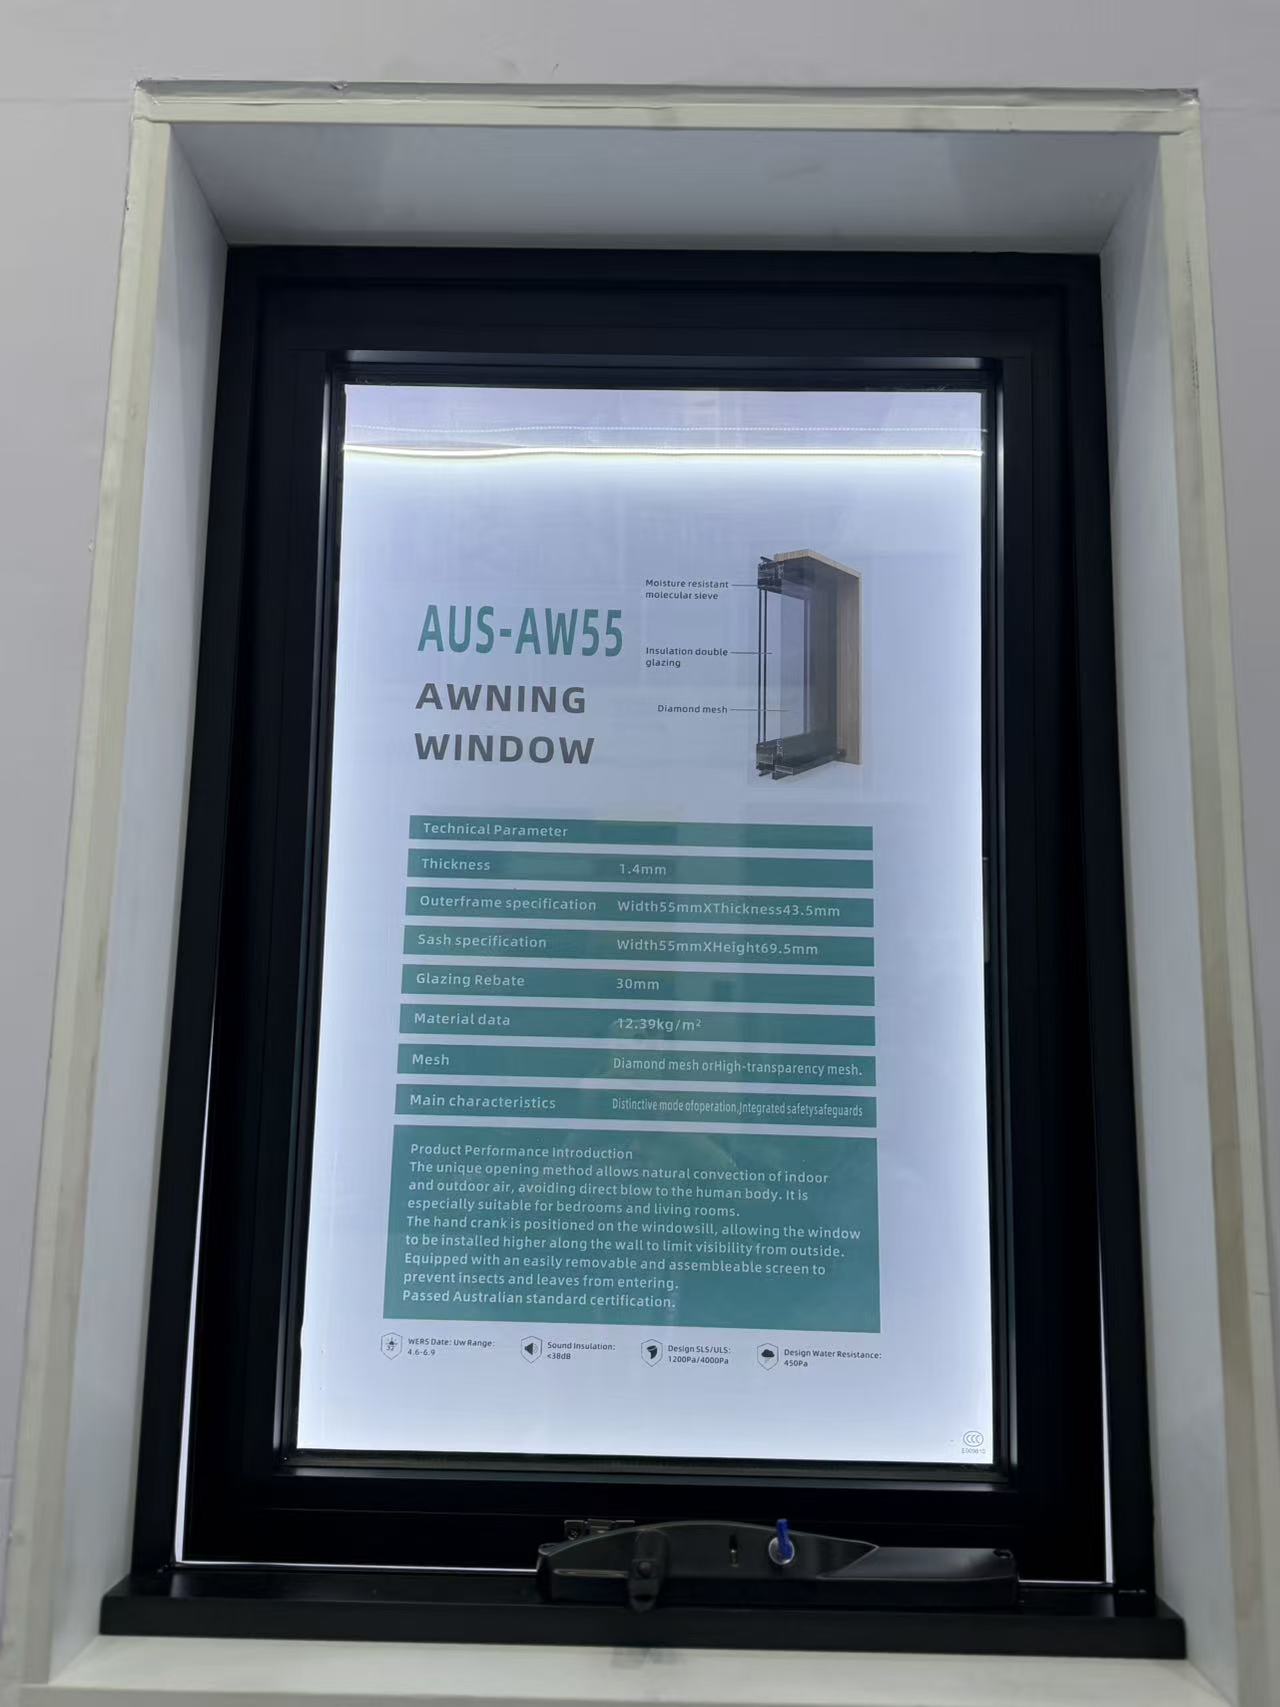
Which water tightness certifications are required for importing an awing window to Europe?
Do you allow virtual factory tours to inspect the sliding window assembly line?
What is the typical MOQ for ordering standard-sized aluminum casement window units?
How long does it take to receive a physical sample of a gold-anodized decorative profile?
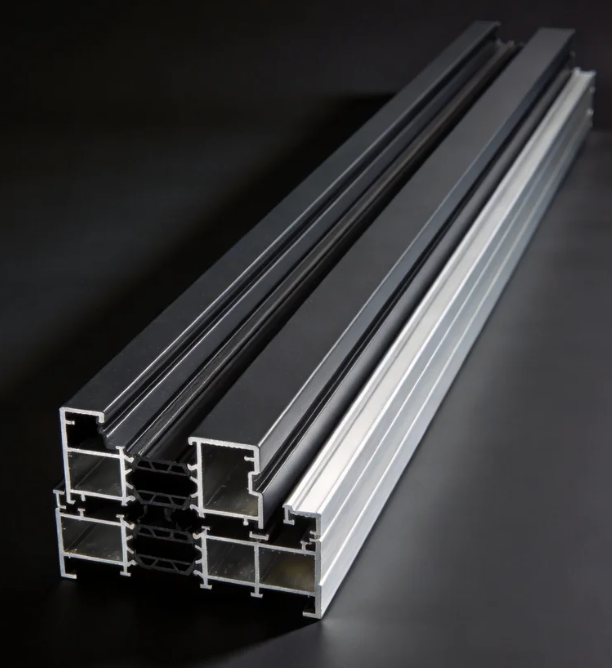
How do I choose the right alloy grade for architecture profiles in high-rise coastal buildings?
How do I choose the right track and roller specs for heavy-duty commercial sliding doors?
The core advantages of using aluminium profiles for the canopy
International demand: Dual drive by new energy and infrastructure
The advantages of using aluminium profiles to manufacture robot arms
The advantages of using aluminum profiles for door and window frames
The impact of the conflict between the United States and Iran on the price of aluminum
The advantages of using aluminium alloy for the main structure of high-speed train carriages
Methods for distinguishing Indoor and Outdoor Aluminium Doors
Maintenance methods and tips for aluminium doors and windows
Characteristic of outward-opening and hung aluminium windows
Xinhe Aluminium Research: 7.14-7.18 Analysis of Aluminium Prices
Seven Benefits Of Using Aluminium Profiles In Curtain Wall Systems
The Application of Aluminium Profiles in New Energy Vehicles
The Composition and Application of Series 6 Aluminium Alloys
Top 5 Benefits of Using LED Aluminium Profiles in Modern Lighting
A Complete Guide to Aluminium Frame Profiles for Modern Structures
Exploring the Strength and Versatility of Aluminium Extrusion Profiles
How to Choose the Right Aluminium Profile Supplier for Your Project
COMPANY