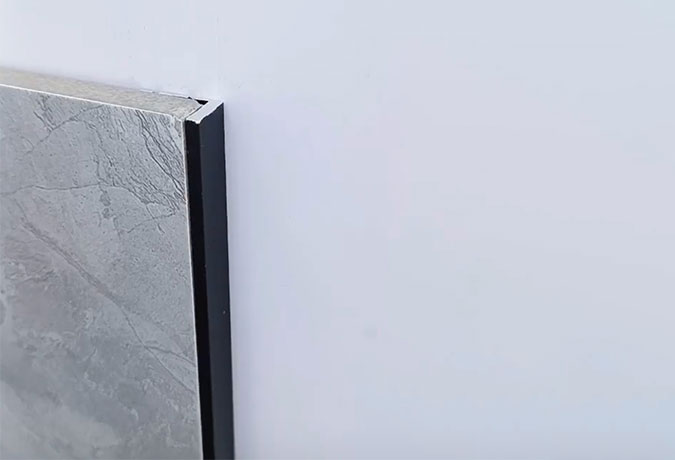
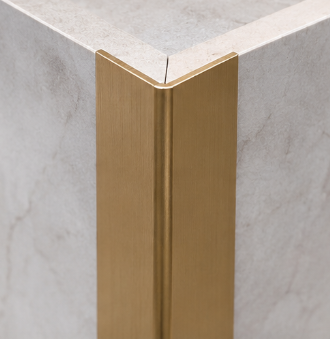
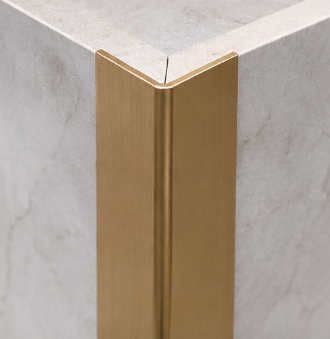
Architectural edges are historically vulnerable. Drywall corners crumble under moderate impact. Wood trims warp when exposed to fluctuating humidity. Integrating decorative aluminium profiles fundamentally alters this dynamic. These extruded metal components shift edge protection from a purely aesthetic afterthought to a calculated structural barrier.
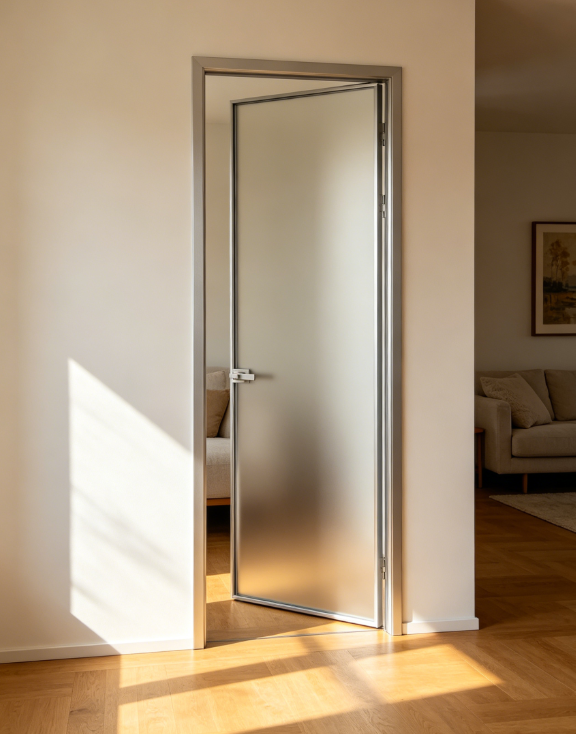
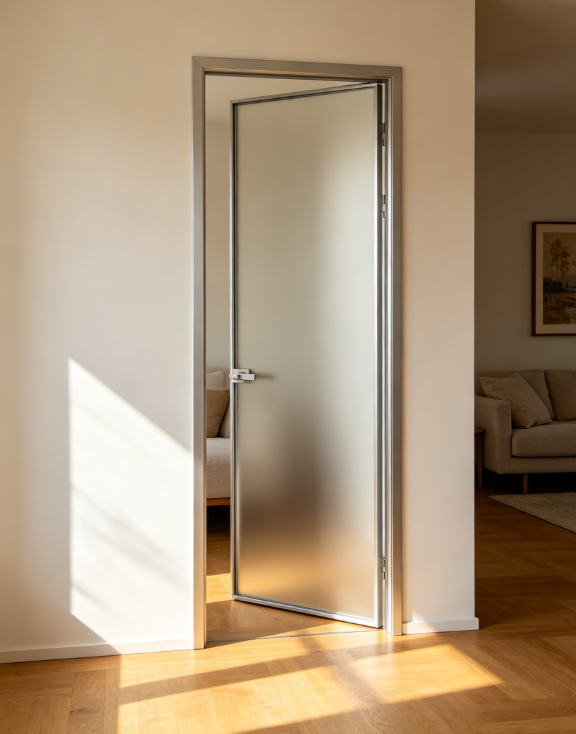
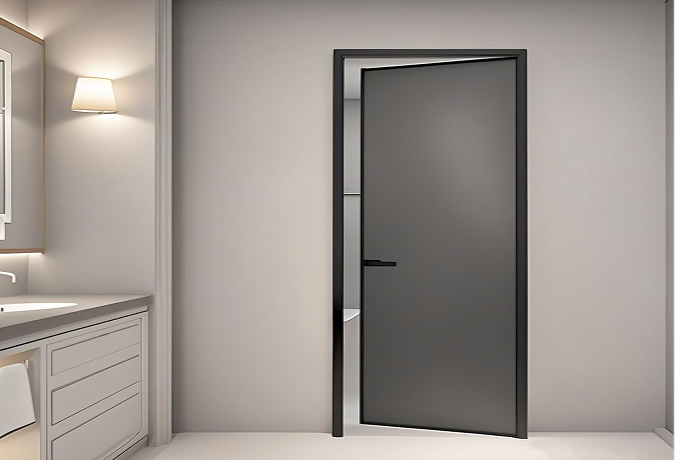
Designers often treat trim merely as a visual framing device. This perspective ignores the sheer physical stress concentrated at material transitions. A minimalist hallway doorway, for example, absorbs continuous micro-impacts over its lifespan. The trim must absorb and distribute these kinetic loads before they reach the fragile gypsum or plaster beneath.
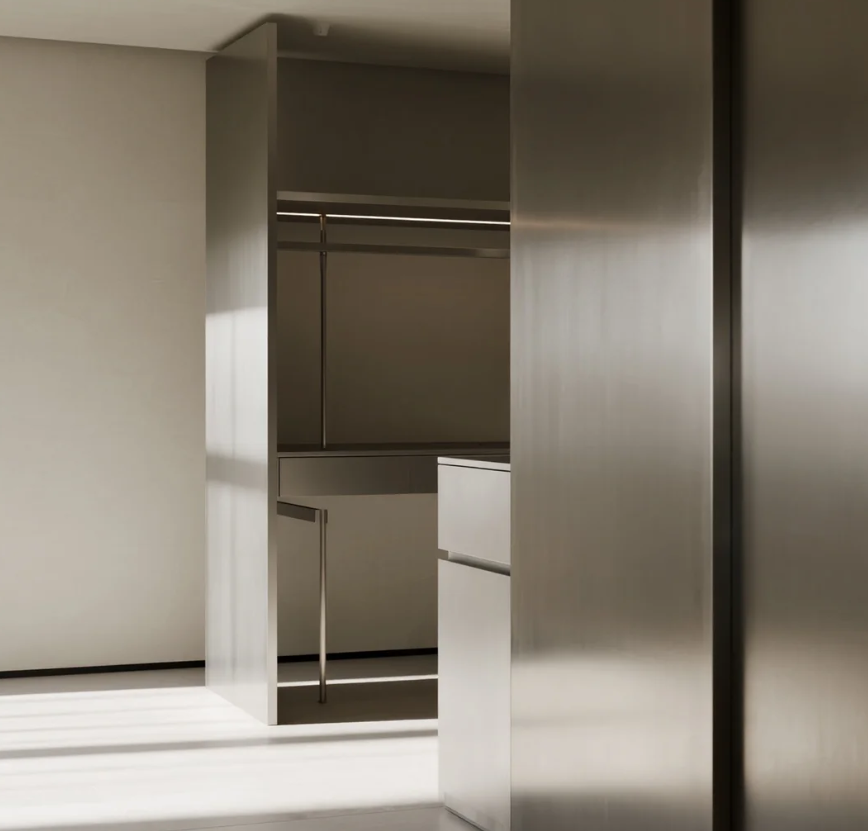
Metallic casings provide this essential load distribution while maintaining sharp architectural lines.
The integration of such metal framing creates a deliberate buffer zone. Energy dissipates through the rigid alloy structure rather than cracking the adjacent wall finish.
Material science dictates the performance ceiling of any metal extrusion. Most standard trim profiles rely heavily on the 6063 and 6463 alloy series. Magnesium and silicon are the primary alloying elements here. They form magnesium silicide, which provides the necessary strengthening precipitate during the heat treatment process.
Raw alloy composition alone is insufficient for architectural demands. The tempering process, specifically T5 and T6 designations, dictates the final yield strength. T5 involves cooling directly from an elevated temperature shaping process, followed by artificial aging. This yields a stable internal grain structure suitable for complex, thin-walled geometries without internal fracturing.
Clients often ask why aerospace-grade alloys are not utilized for interior trim. High-strength 7000-series aluminum is notoriously difficult to extrude into intricate shapes. The friction generated during extrusion ruins the precise surface finish required for aesthetic applications. The 6000-series strikes the exact mathematical balance between extrudability, surface smoothness, and mechanical rigidity.
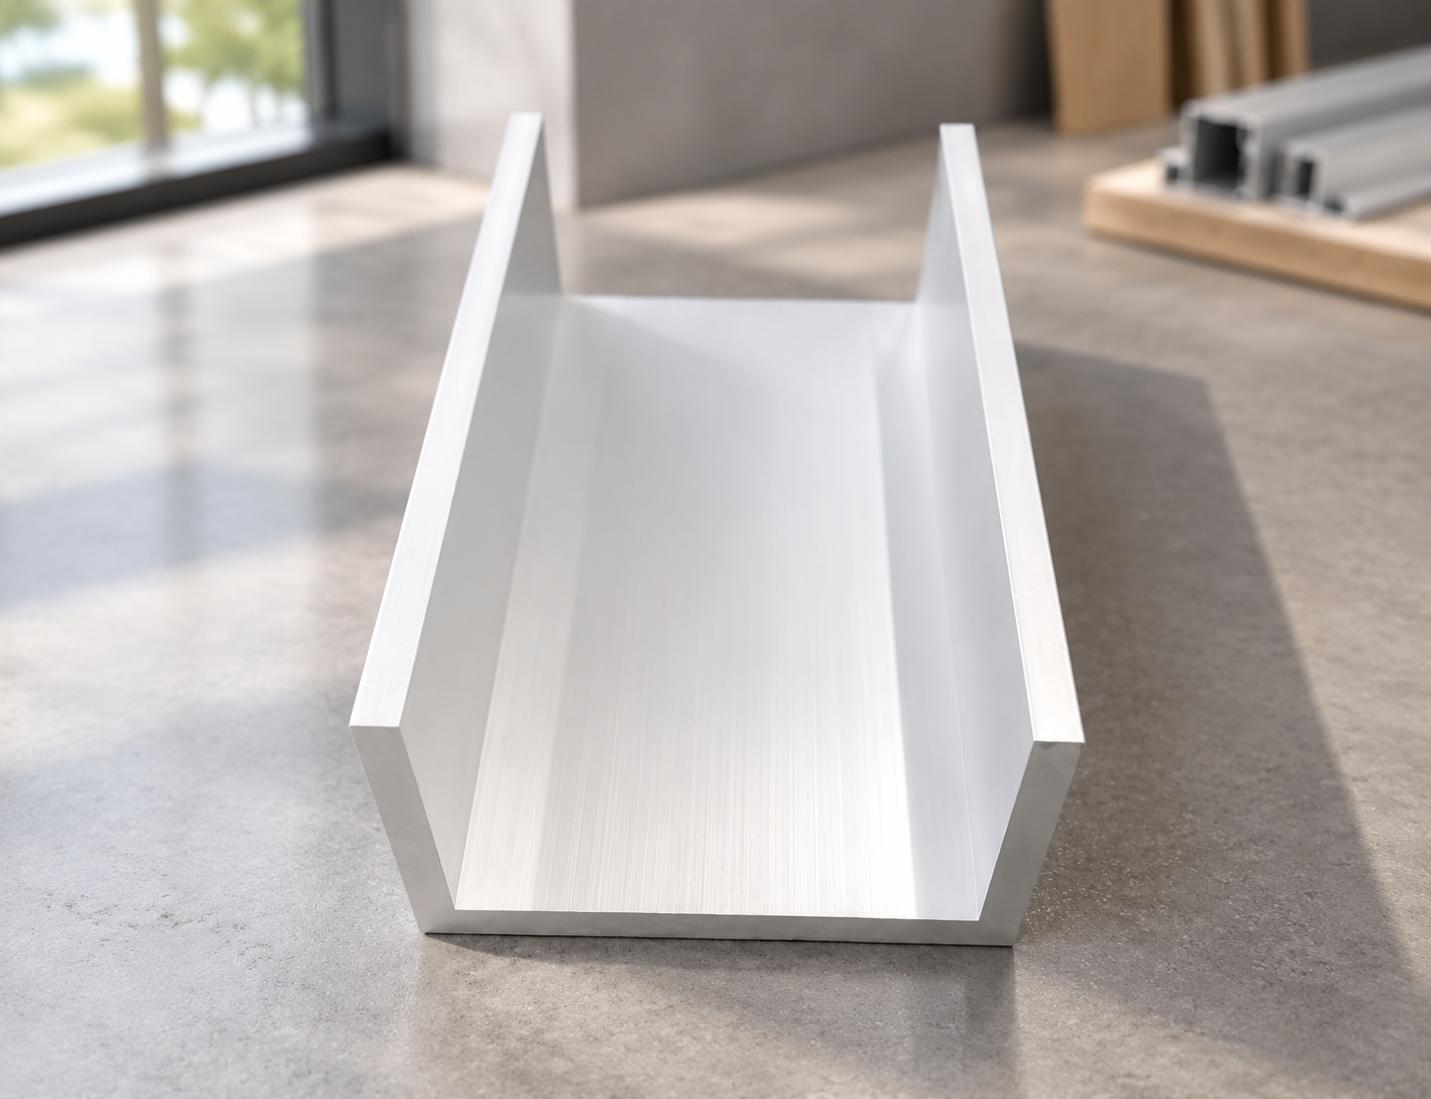
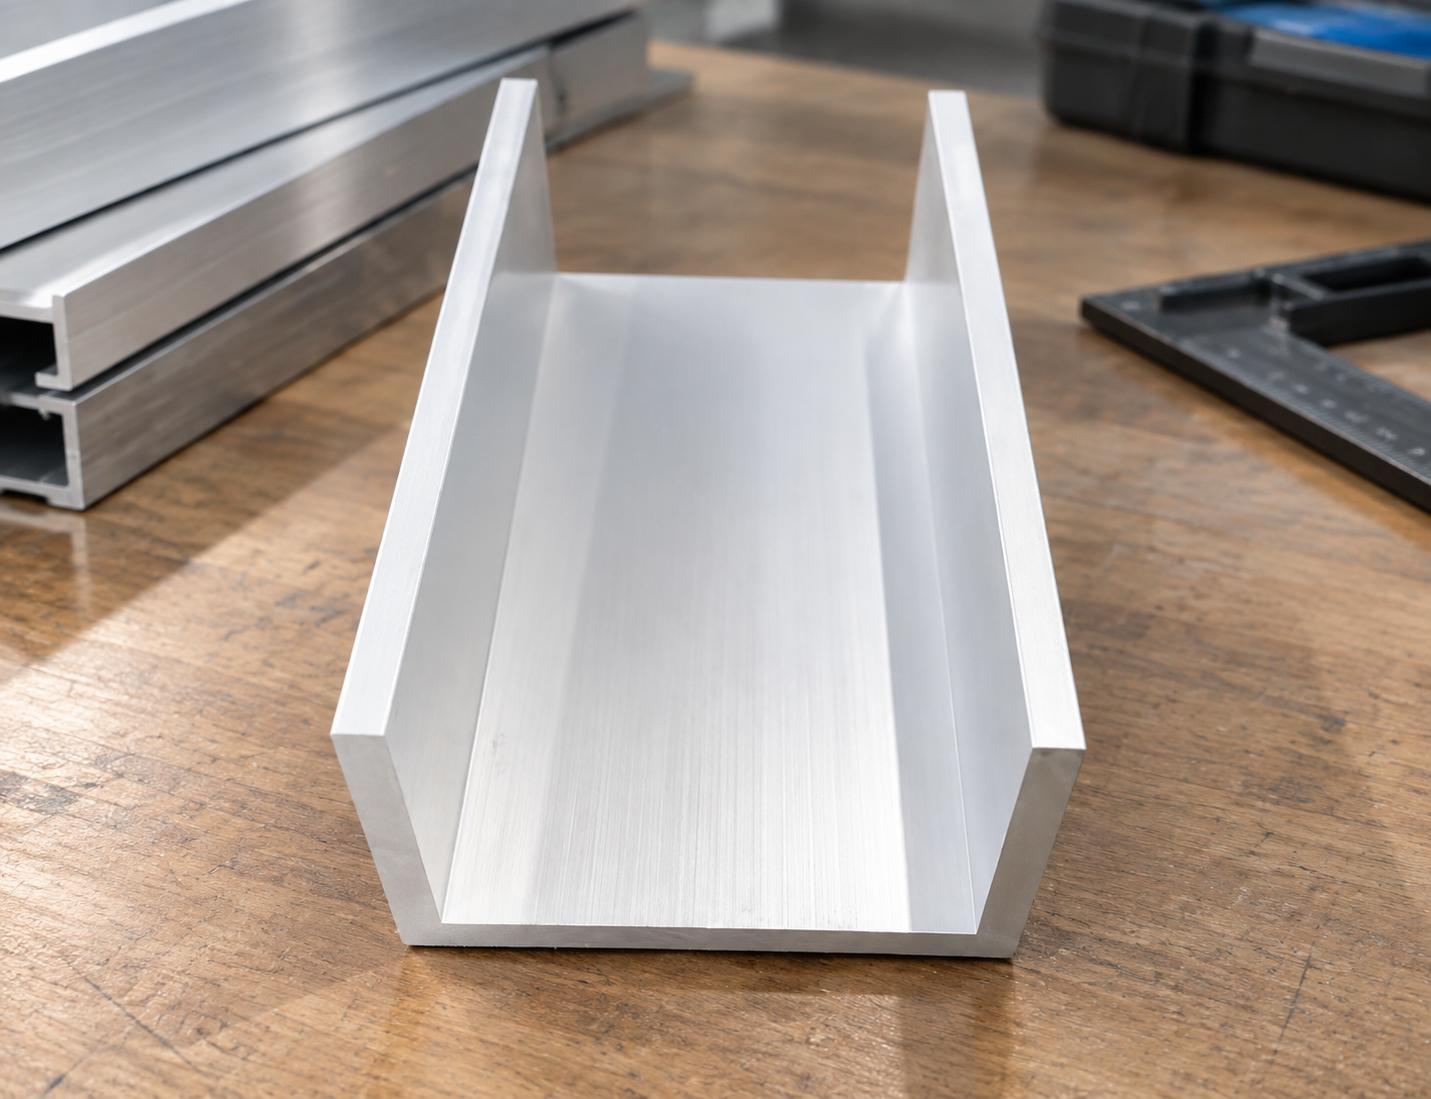
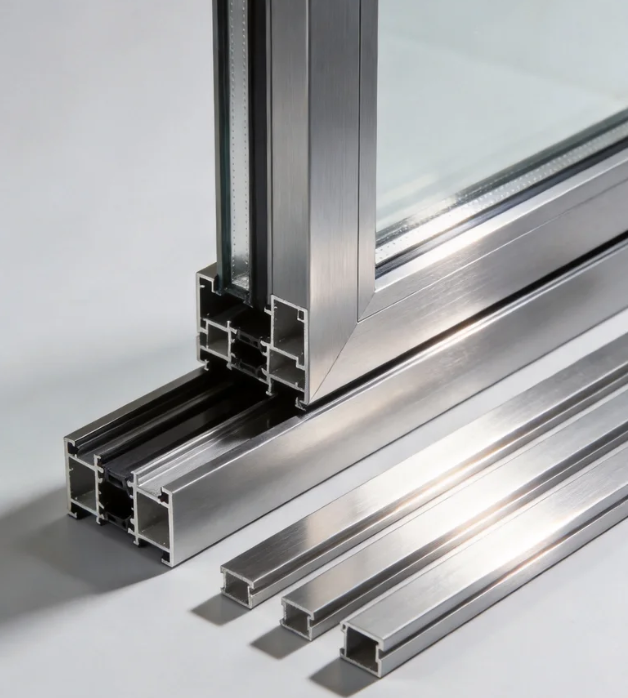
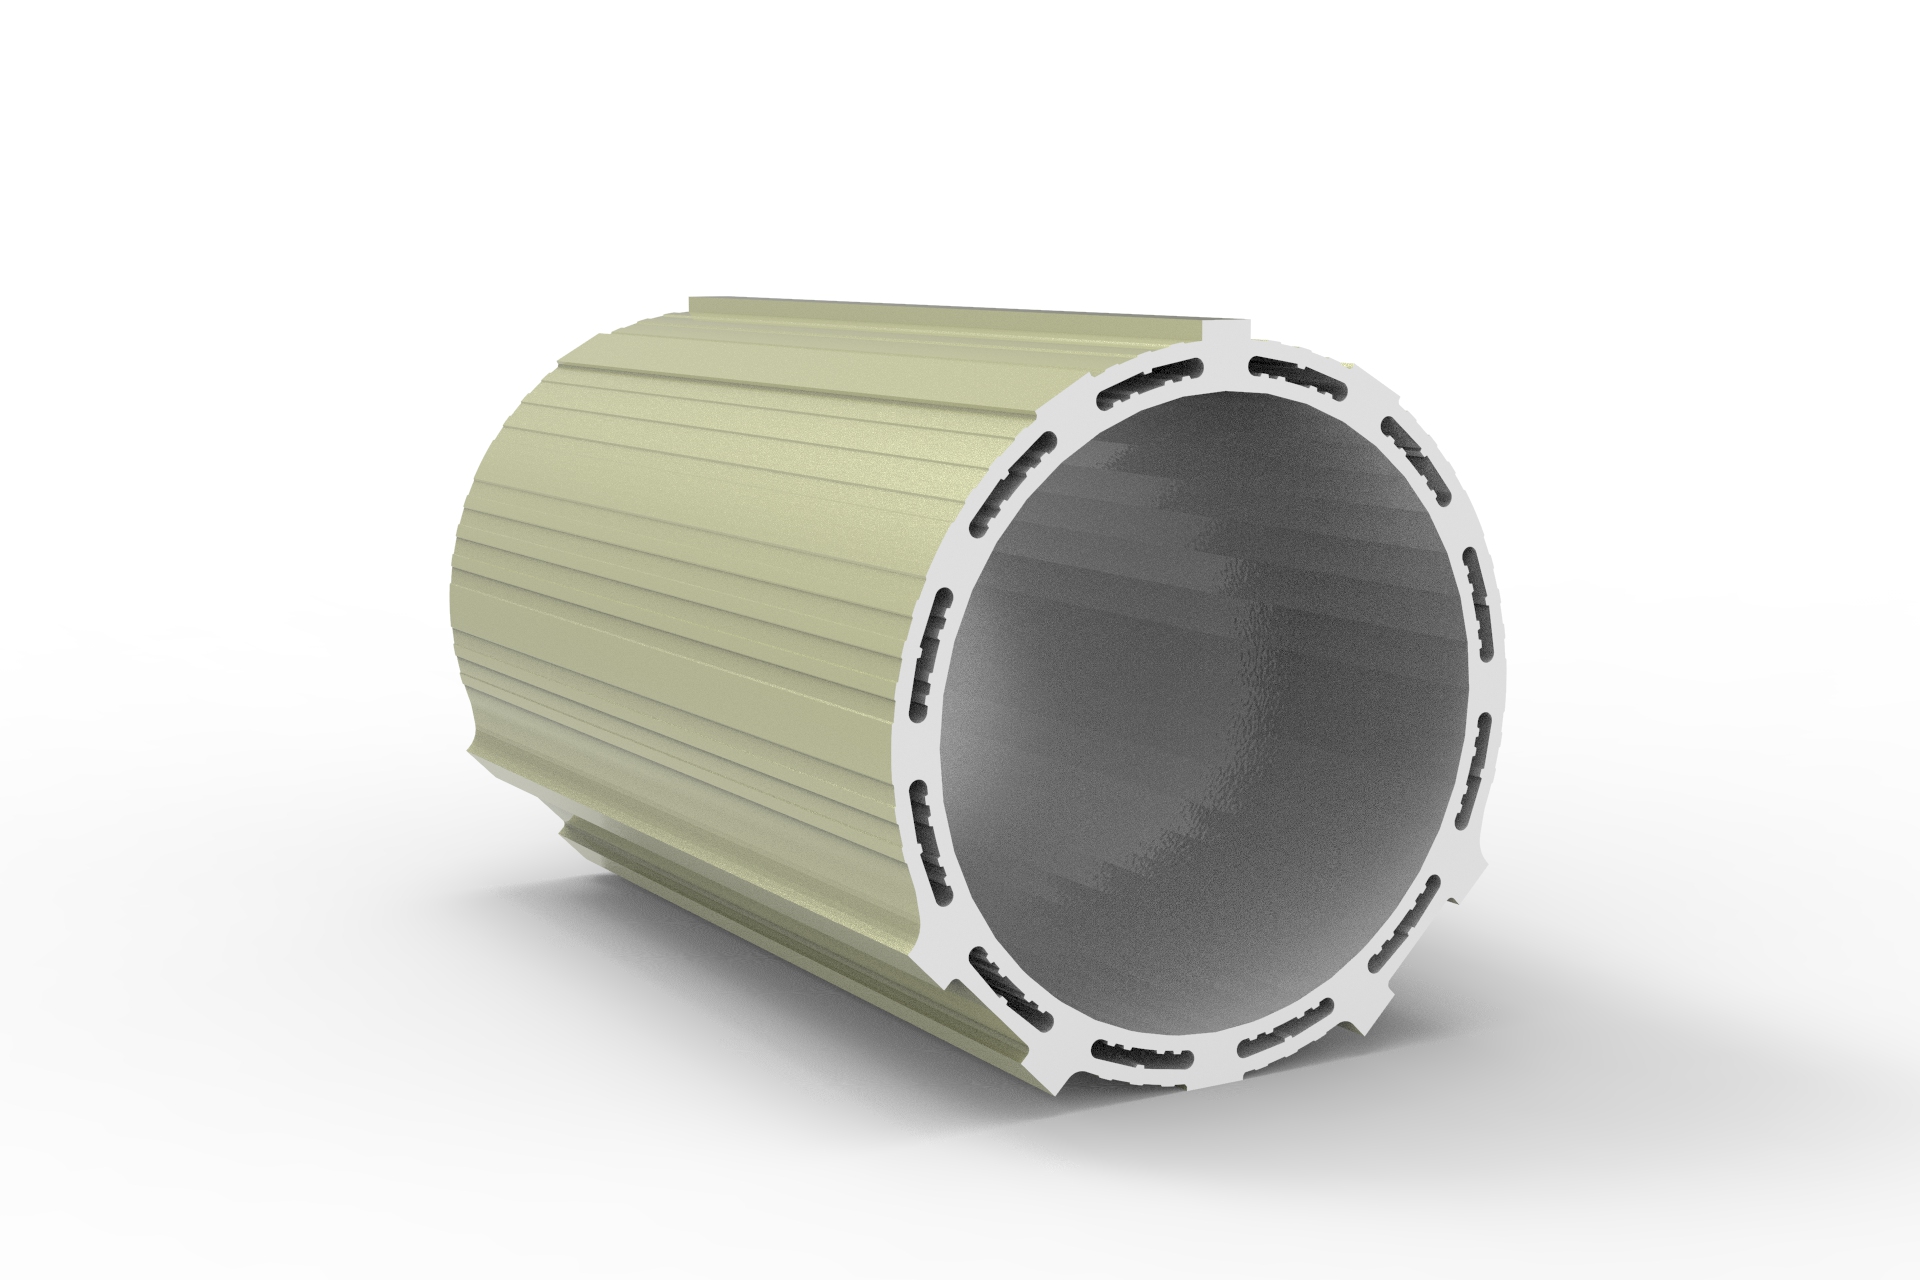
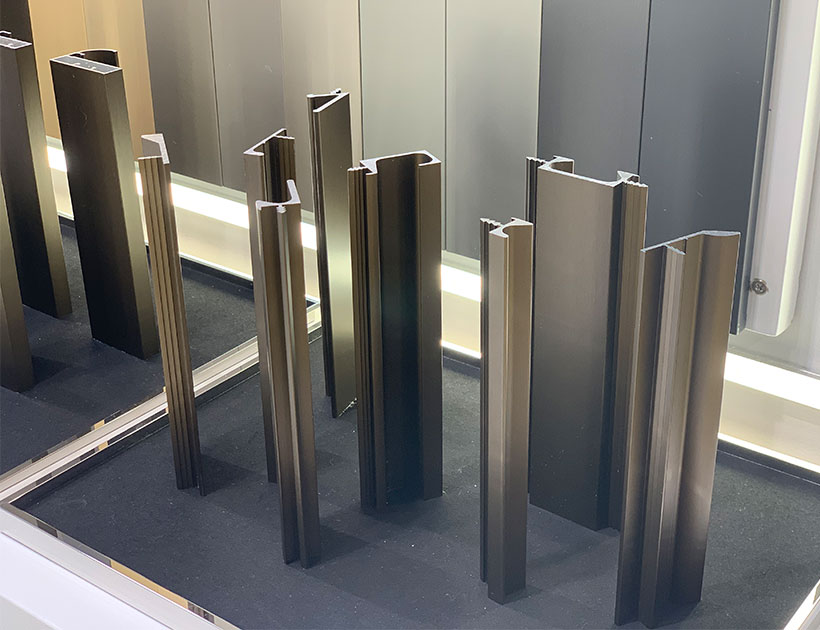
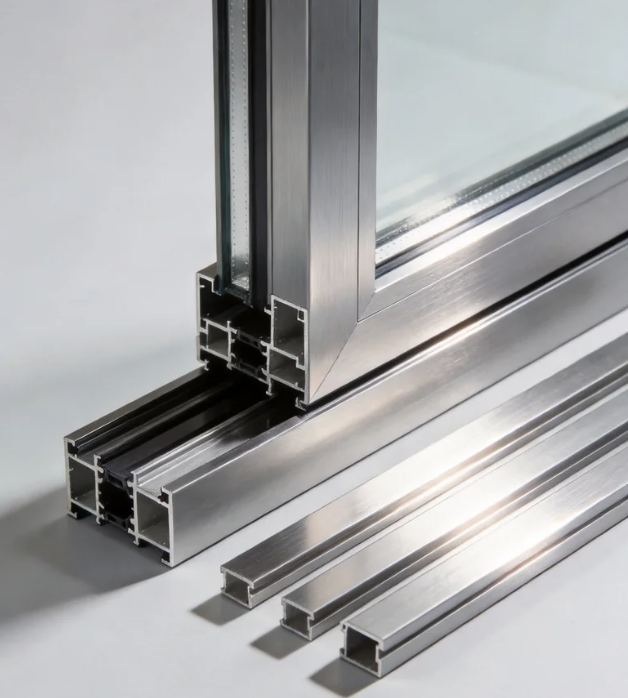
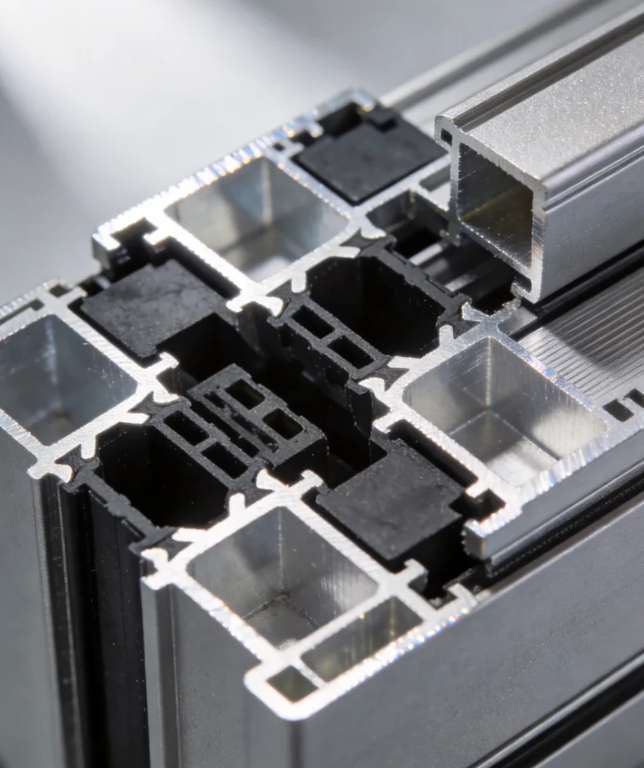
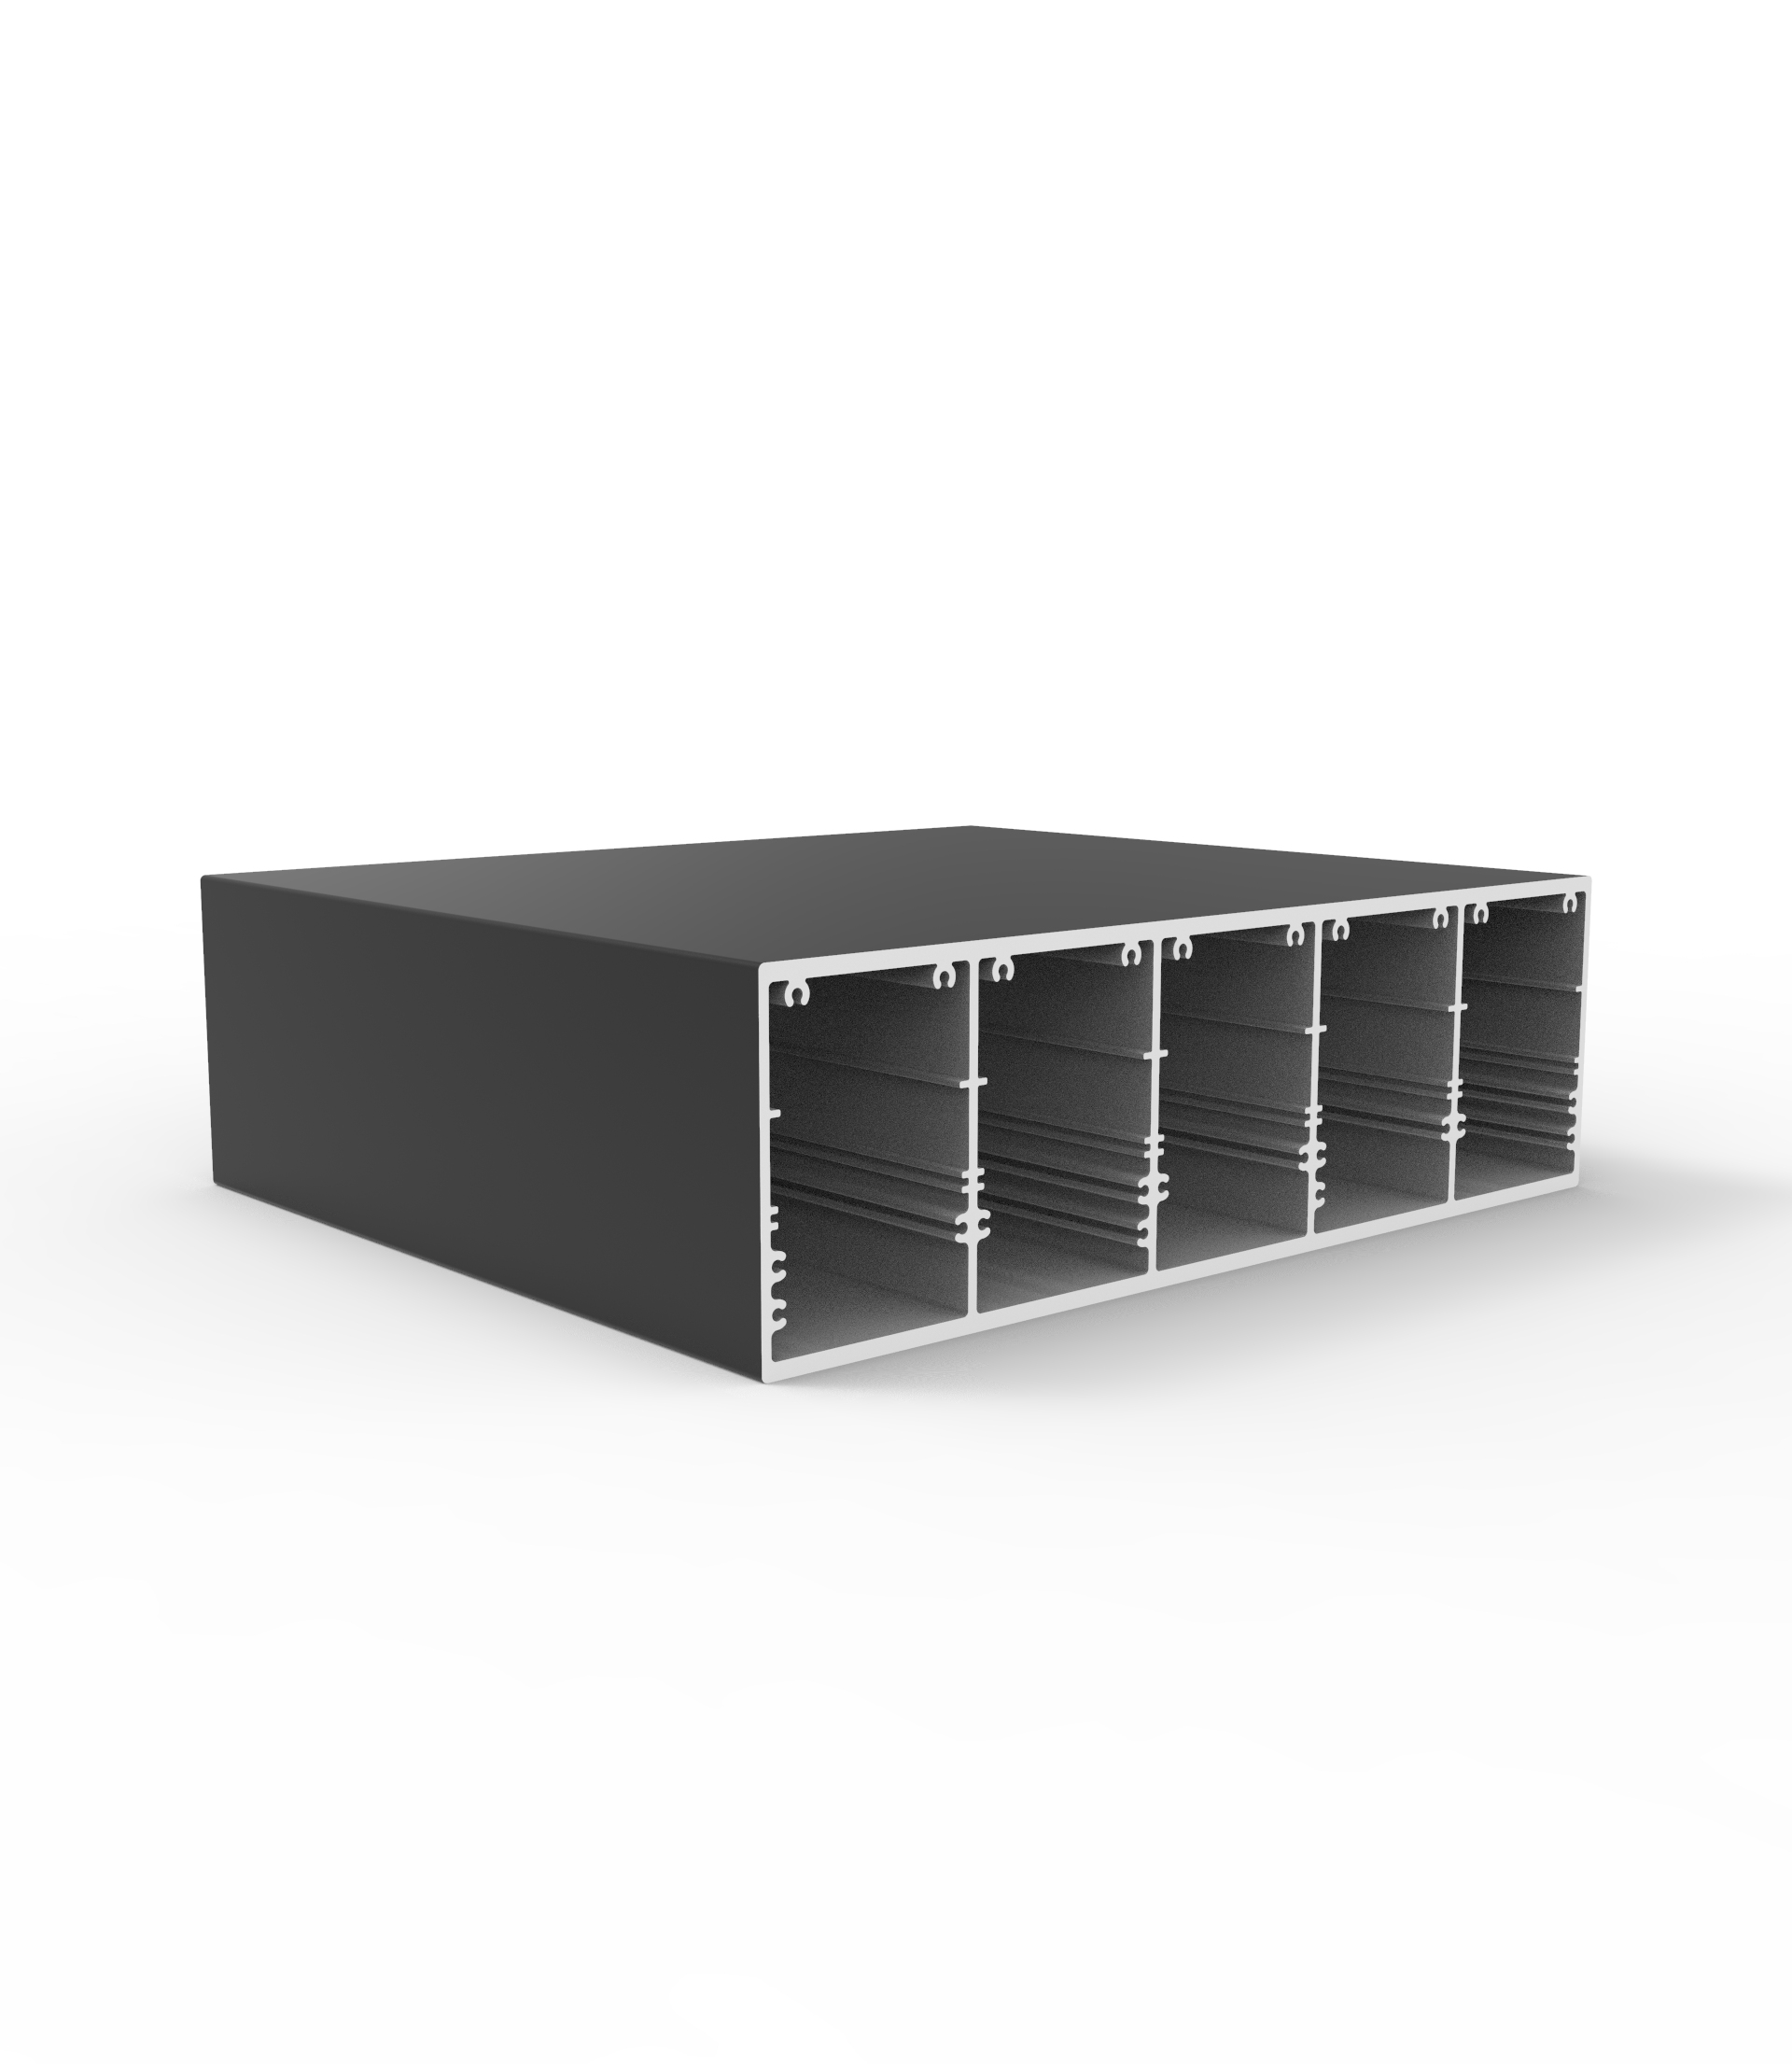
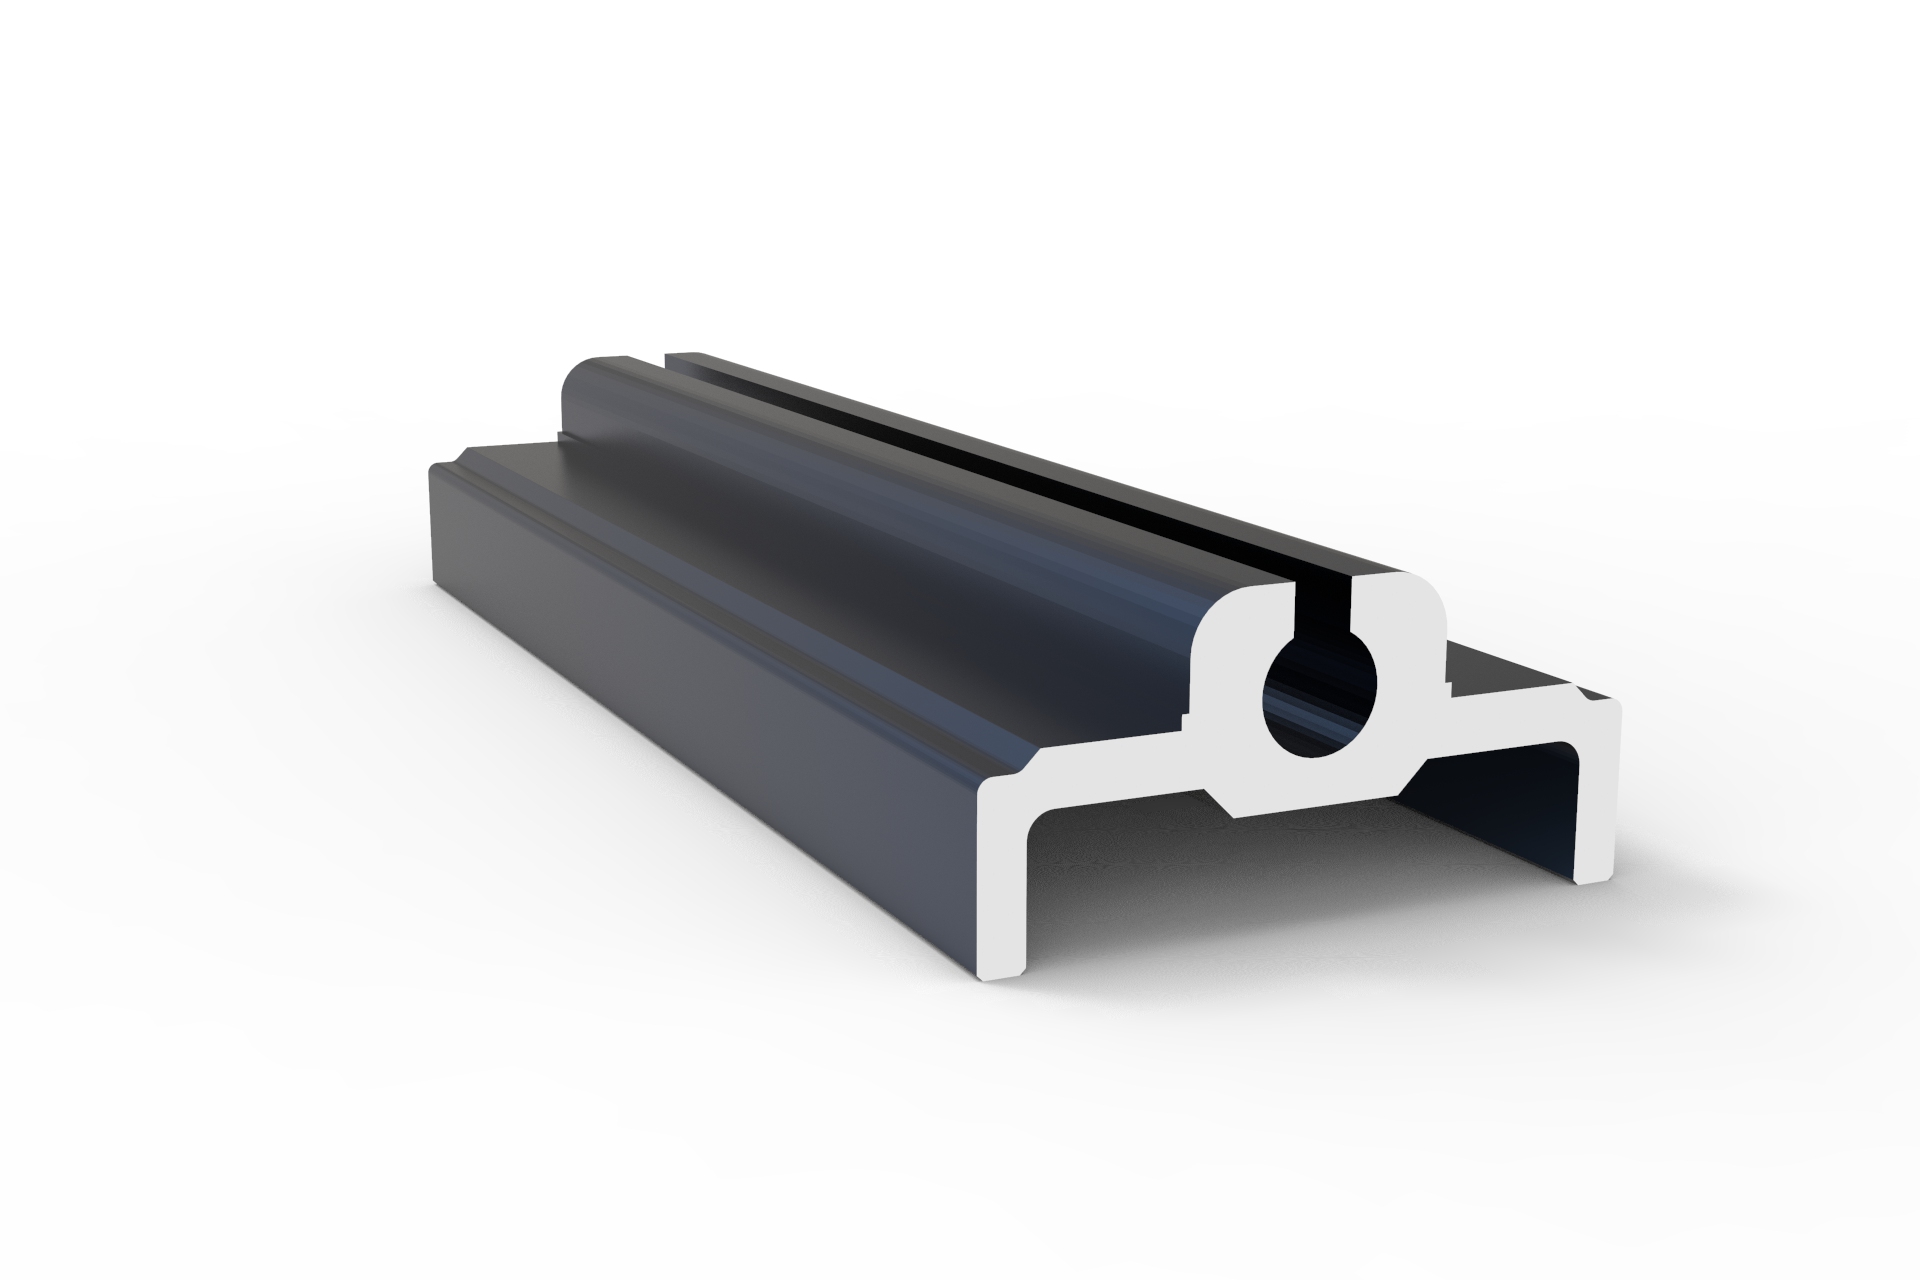
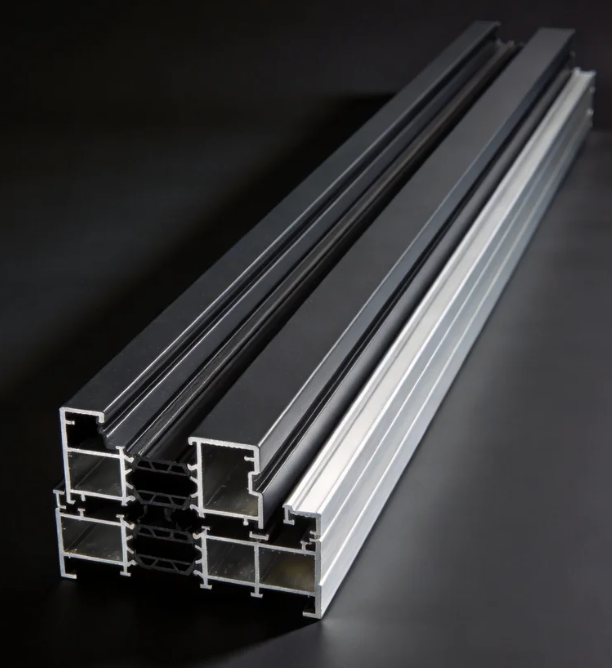
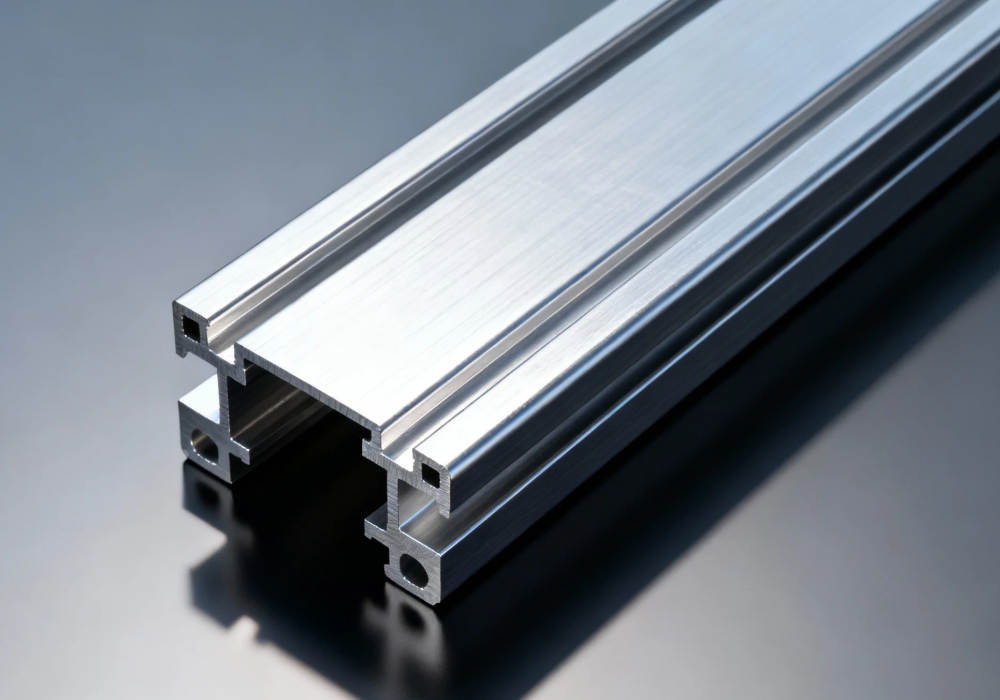
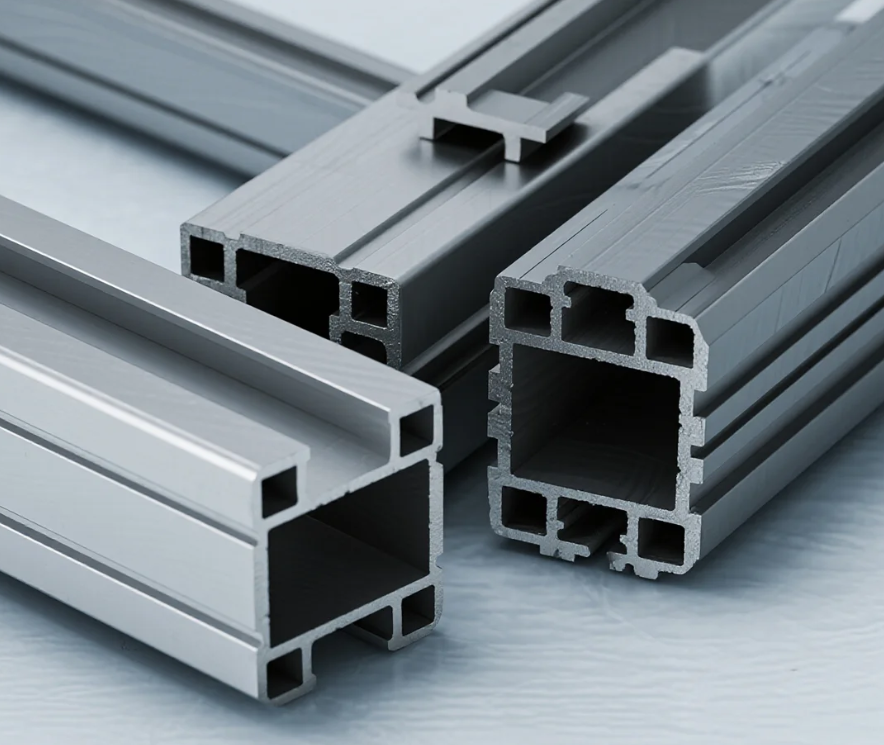
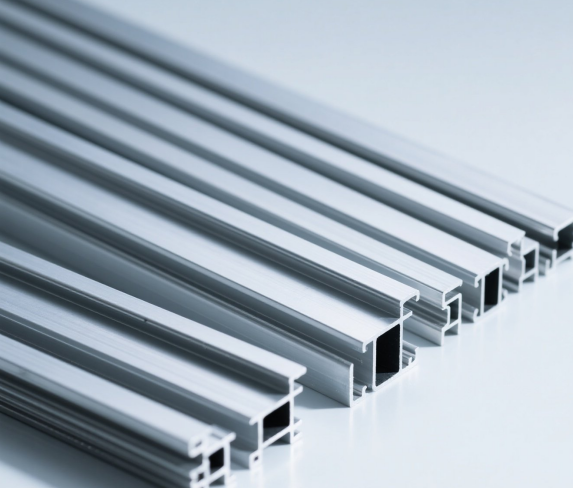
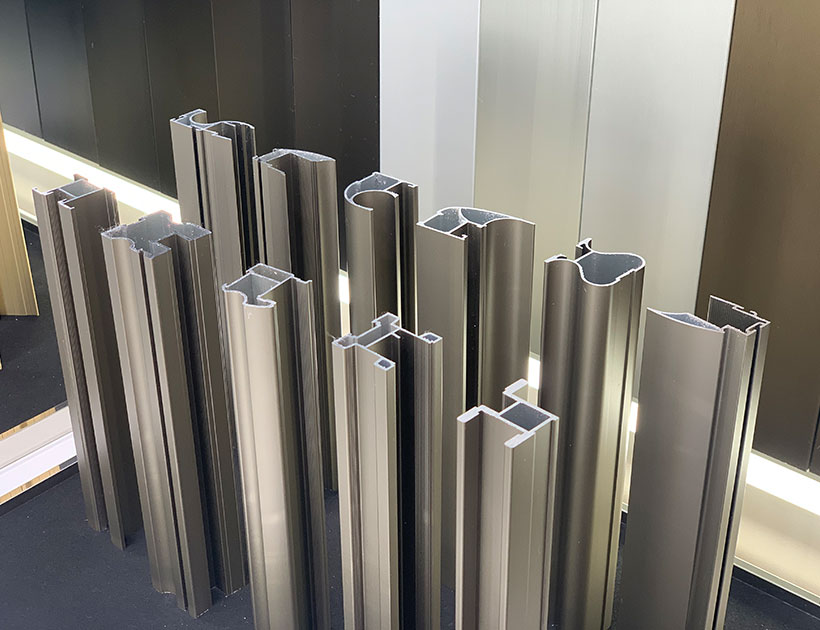
Cross-sectional geometry matters far more than mere wall thickness. A flat, solid piece of metal bends under localized pressure. Extruding the metal into complex U-channel or J-channel configurations drastically increases the moment of inertia. This geometric stiffness prevents the trim from bowing or deflecting across long spans.
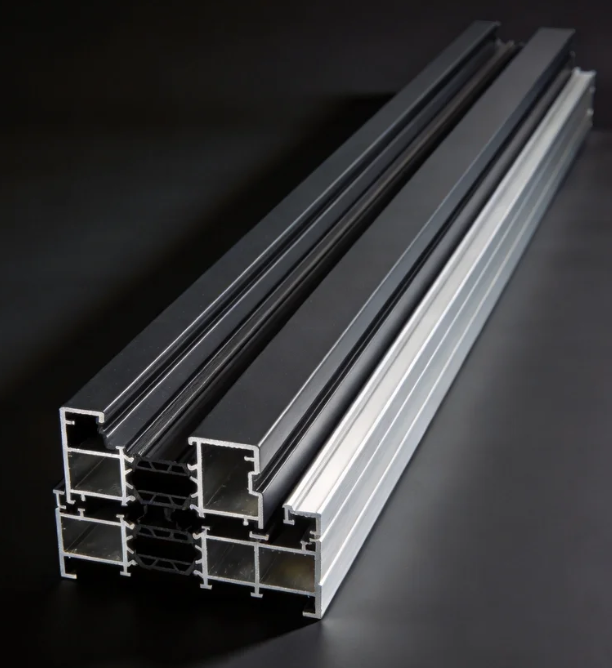
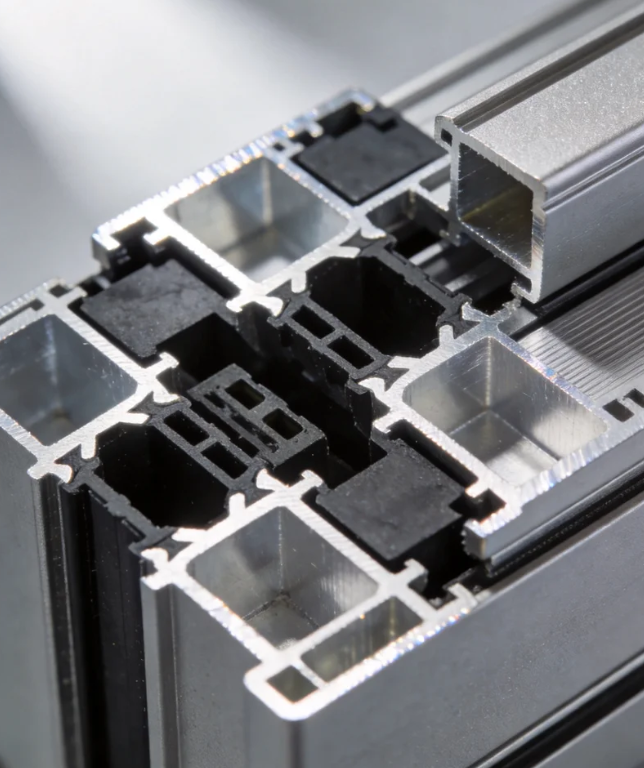
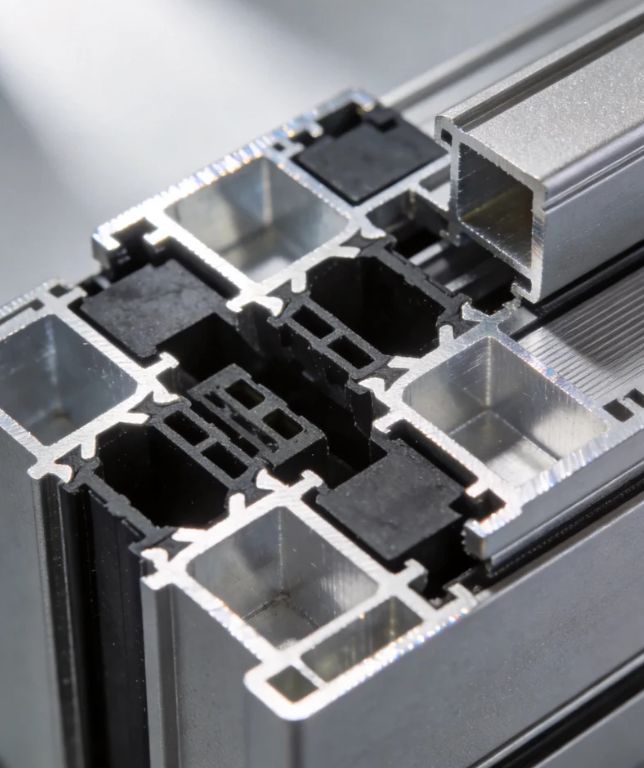
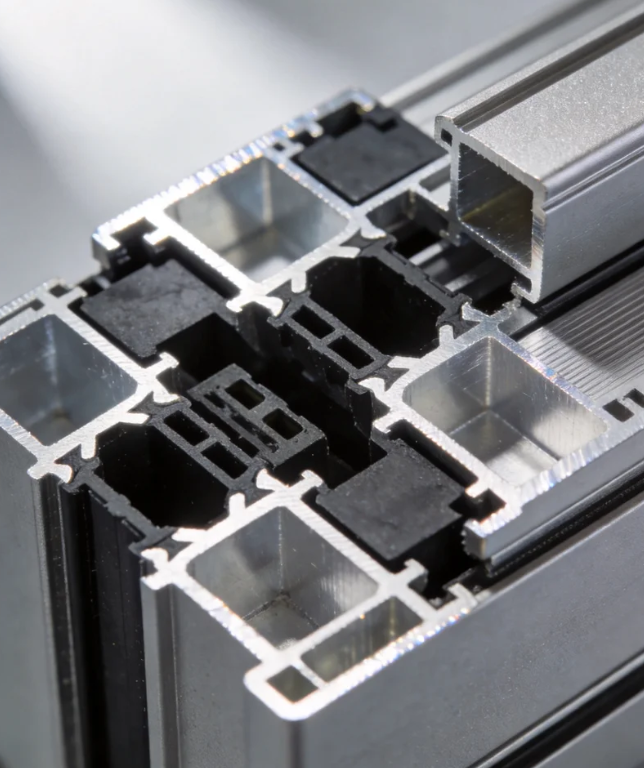
Modern extrusions feature integrated mounting tracks hidden from the visible surface. These internal structural stiffener ribs serve a dual purpose. They provide rigid anchoring points for concealed fasteners, while simultaneously acting as internal reinforcement struts. This one-piece molding approach eliminates the weak points inherent in multi-piece welded or bonded assemblies.
Precise geometric tolerances directly impact environmental sealing. When a profile clamps over a raw wall panel edge, the gap must be microscopic. Extruded decorative aluminium profiles can hold tolerances tight enough to prevent moisture migration. This mechanical barrier blocks humidity from seeping into MDF or drywall cores.
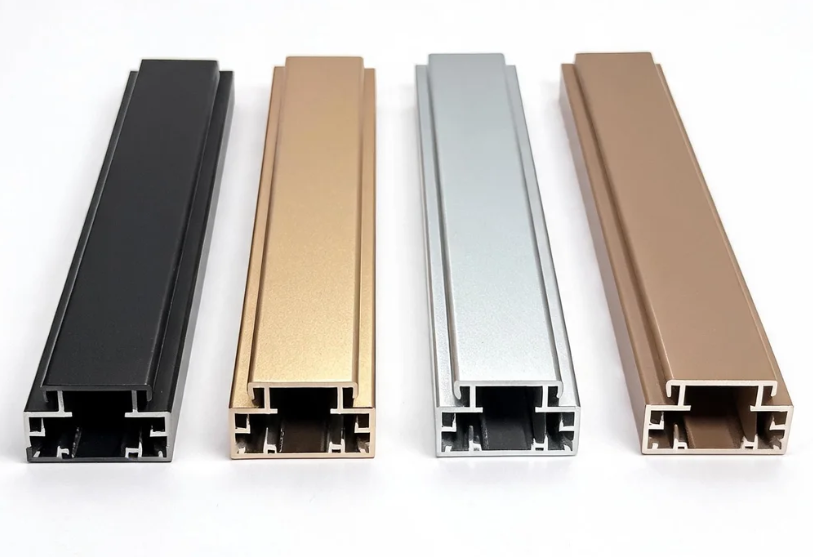
Raw aluminum instantly oxidizes when exposed to air. Anodizing harnesses this natural decay mechanism and weaponizes it into a protective shell. By submerging the profile in an acid electrolyte bath and passing a direct current through it, the natural oxide layer thickens artificially. This anodic film is quite literally grown from the base metal.
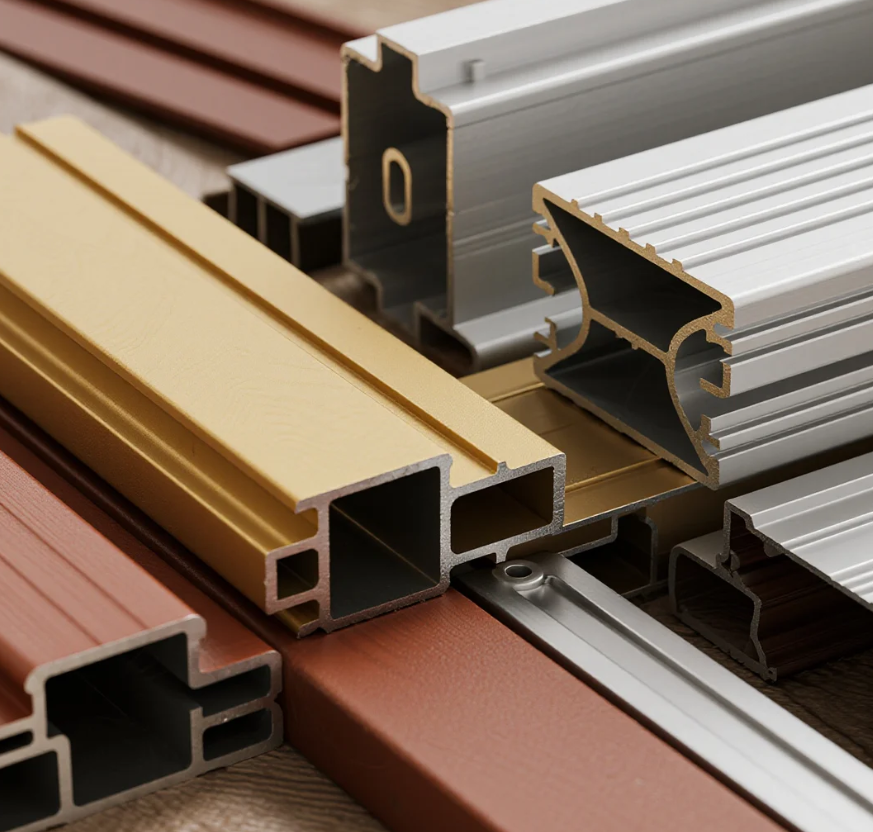
Unlike paint, an anodic layer cannot peel or flake off. It is fully integrated into the crystalline structure of the metal itself. For applications requiring specific color matching, alternative surface treatments are deployed. These include:
Electrophoresis applies a clear acrylic resin over the anodized layer using an electrical field. This seals the microscopic pores left behind by the anodizing process. The resulting surface is remarkably smooth and highly resistant to chemical cleaners. Fingerprints, smudges, and environmental pollutants simply wipe away without degrading the underlying metal.
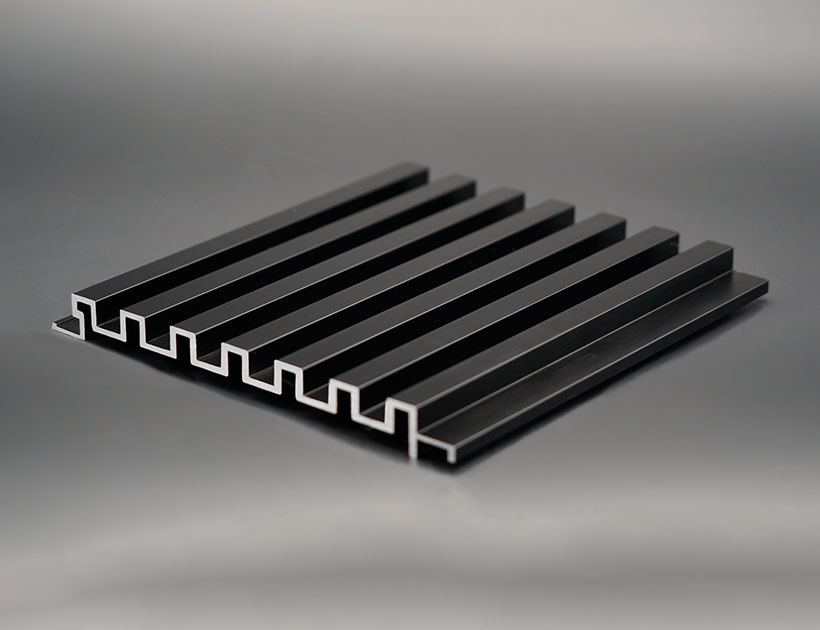
Understanding the exact operational parameters helps in specifying the correct hardware for commercial spaces. Engineering data removes the ambiguity from material selection. The table below outlines the baseline mechanical and logistical constraints for standard extruded trim solutions.
| Parameter | Engineering Specification |
|---|---|
| Alloy Grades | 6063, 6463 |
| Temper States | T5, T6 |
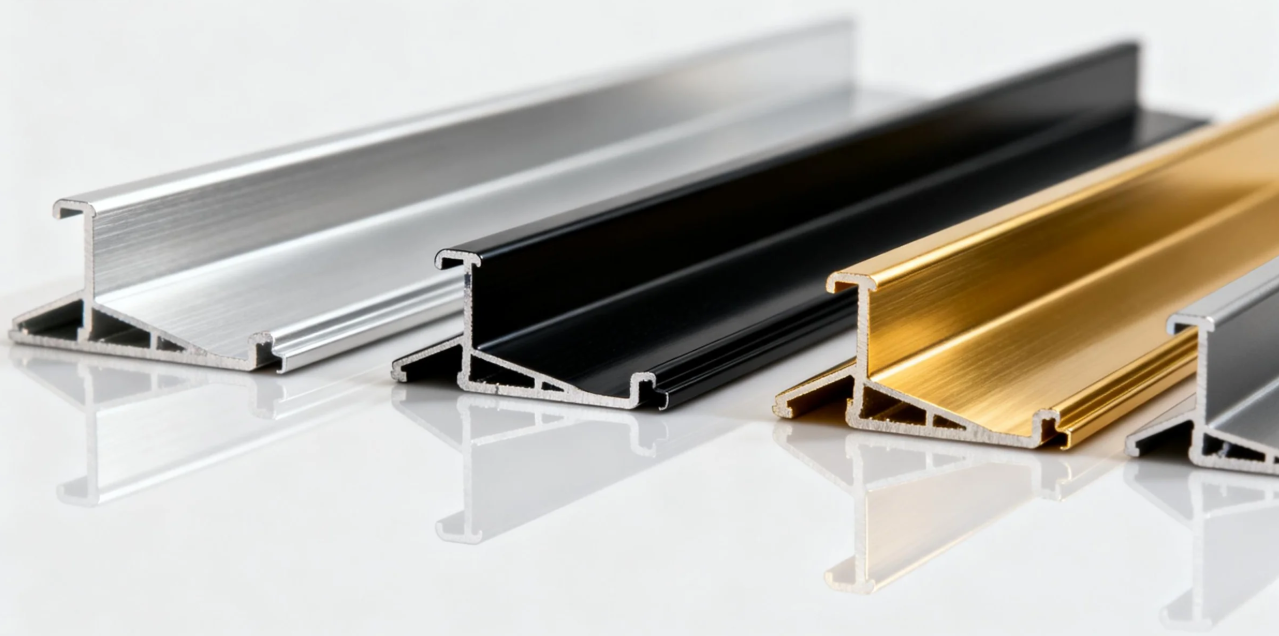
| Surface Finishes | Anodized, Electrophoresis, Powder Coated, Wood Grain |
| Standard MOQ | 200 to 500 kilograms per section |
| Production Cycle | 10 to 20 days |
These specifications represent standard manufacturing baseline limits. Pushing an extrusion wall thickness below standard minimums risks thermal distortion during the artificial aging process. Over-specifying a T6 temper on a highly complex, thin-walled shape can lead to brittle failure during installation clipping.
Misaligned expectations regarding installation tolerances often lead to project delays. Contractors sometimes treat precision metal trims with the same blunt force applied to timber. We must clarify the mechanical realities of these extrusions to ensure long-term structural integrity.
Q: Can we bend standard extruded trim profiles on-site to fit curved architectural walls?
A: Rigid extrusions tempered to T5 or T6 cannot be cold-formed on-site without structural failure. The metal will buckle, and the anodized surface layer will craze or crack. Curved walls require factory-rolled profiles processed before the final artificial aging and surface treatment stages.
Q: Do integrated mounting channels eliminate the need for construction adhesives?
A: Mechanical fasteners secure the profile, but they do not dampen vibration. Adhesives act as a necessary acoustic decoupling layer between the rigid metal and the wall substrate. Relying solely on mechanical clips often results in a hollow, metallic rattle when adjacent doors are shut.
Consistent quality across large-scale commercial deployments requires significant infrastructure. A single high-rise project might demand hundreds of distinct architectural edge configurations. Operating with over 25 years of industry experience, for us, fulfilling massive scale orders means utilizing an annual production capacity of 200,000 tons. This volume allows for tight control over the entire metallurgical lifecycle, from raw billet casting to final surface curing.
Custom tooling dictates the final precision of any profile. The steel dies used for extrusion undergo immense thermal and mechanical stress. Micro-abrasions on the die translate directly to visible striations on the finished aluminum surface. Frequent die maintenance and replacement are non-negotiable engineering requirements for producing premium architectural hardware.
Architects continuously push for thinner sightlines in interior detailing. They want the structural strength of steel with the visual weight of paper. Extruded channels manage this contradiction through clever internal geometry. A profile that appears to be a mere millimeter thick externally often hides deep anchoring ribs within the wall cavity.
Material transitions define the subconscious quality of a space. A poorly resolved corner or a warping baseboard immediately shatters the illusion of architectural permanence. By anchoring vulnerable edges with highly engineered decorative aluminium profiles, designers solve a critical mechanical flaw. The resulting interior spaces remain sharp, durable, and structurally sound long after the initial installation.
How Do Engineers Select Industrial Aluminium Profiles for High-Load Frameworks?
What payment structure reduces my risk on a first Industrial profile order?
Should I approve a Casement window sample before checking its hardware strength?
Structural Mechanics of Channel Extrusions in Architectural Aluminium Profiles
Engineering Mechanics of Aluminium Extrusion Profiles in Channel Systems
What functional tests should I perform on a Sliding door prototype?
What payment terms are fair when Decorative profile colors remain unconfirmed?
Is a letter of credit practical for a large Casement window shipment?
How should Industrial profile bundles be packed to prevent transit damage?
Which safety documents should I request for Awing window imports?
What shipping delays commonly affect Architecture profile orders during peak season?
How to Specify Extruded Aluminium Profiles: Costs, Alloys, and Tolerances
Is a Floding door suitable for a wide opening exposed to strong winds?
Structural Integrity in Modular Design: Engineering T-Slot Aluminium Extrusion Profiles
Resolving Corner Stress: The Engineering Mechanics Behind Aluminium Profiles in Architectural Framin
How do Floding door prices change with glass, hardware, and finish choices?
How can I prove Shutter defects remotely without returning every unit?
How can I shorten Awing window sampling without losing critical tests?
Does ordering mixed Shutter sizes usually change the unit price or MOQ?
How should Industrial profile warranty responsibility be shared after assembly?
How should I plan Shutter inventory when ocean freight schedules change?
How do escrow arrangements reduce risk for a new Floding door supplier?
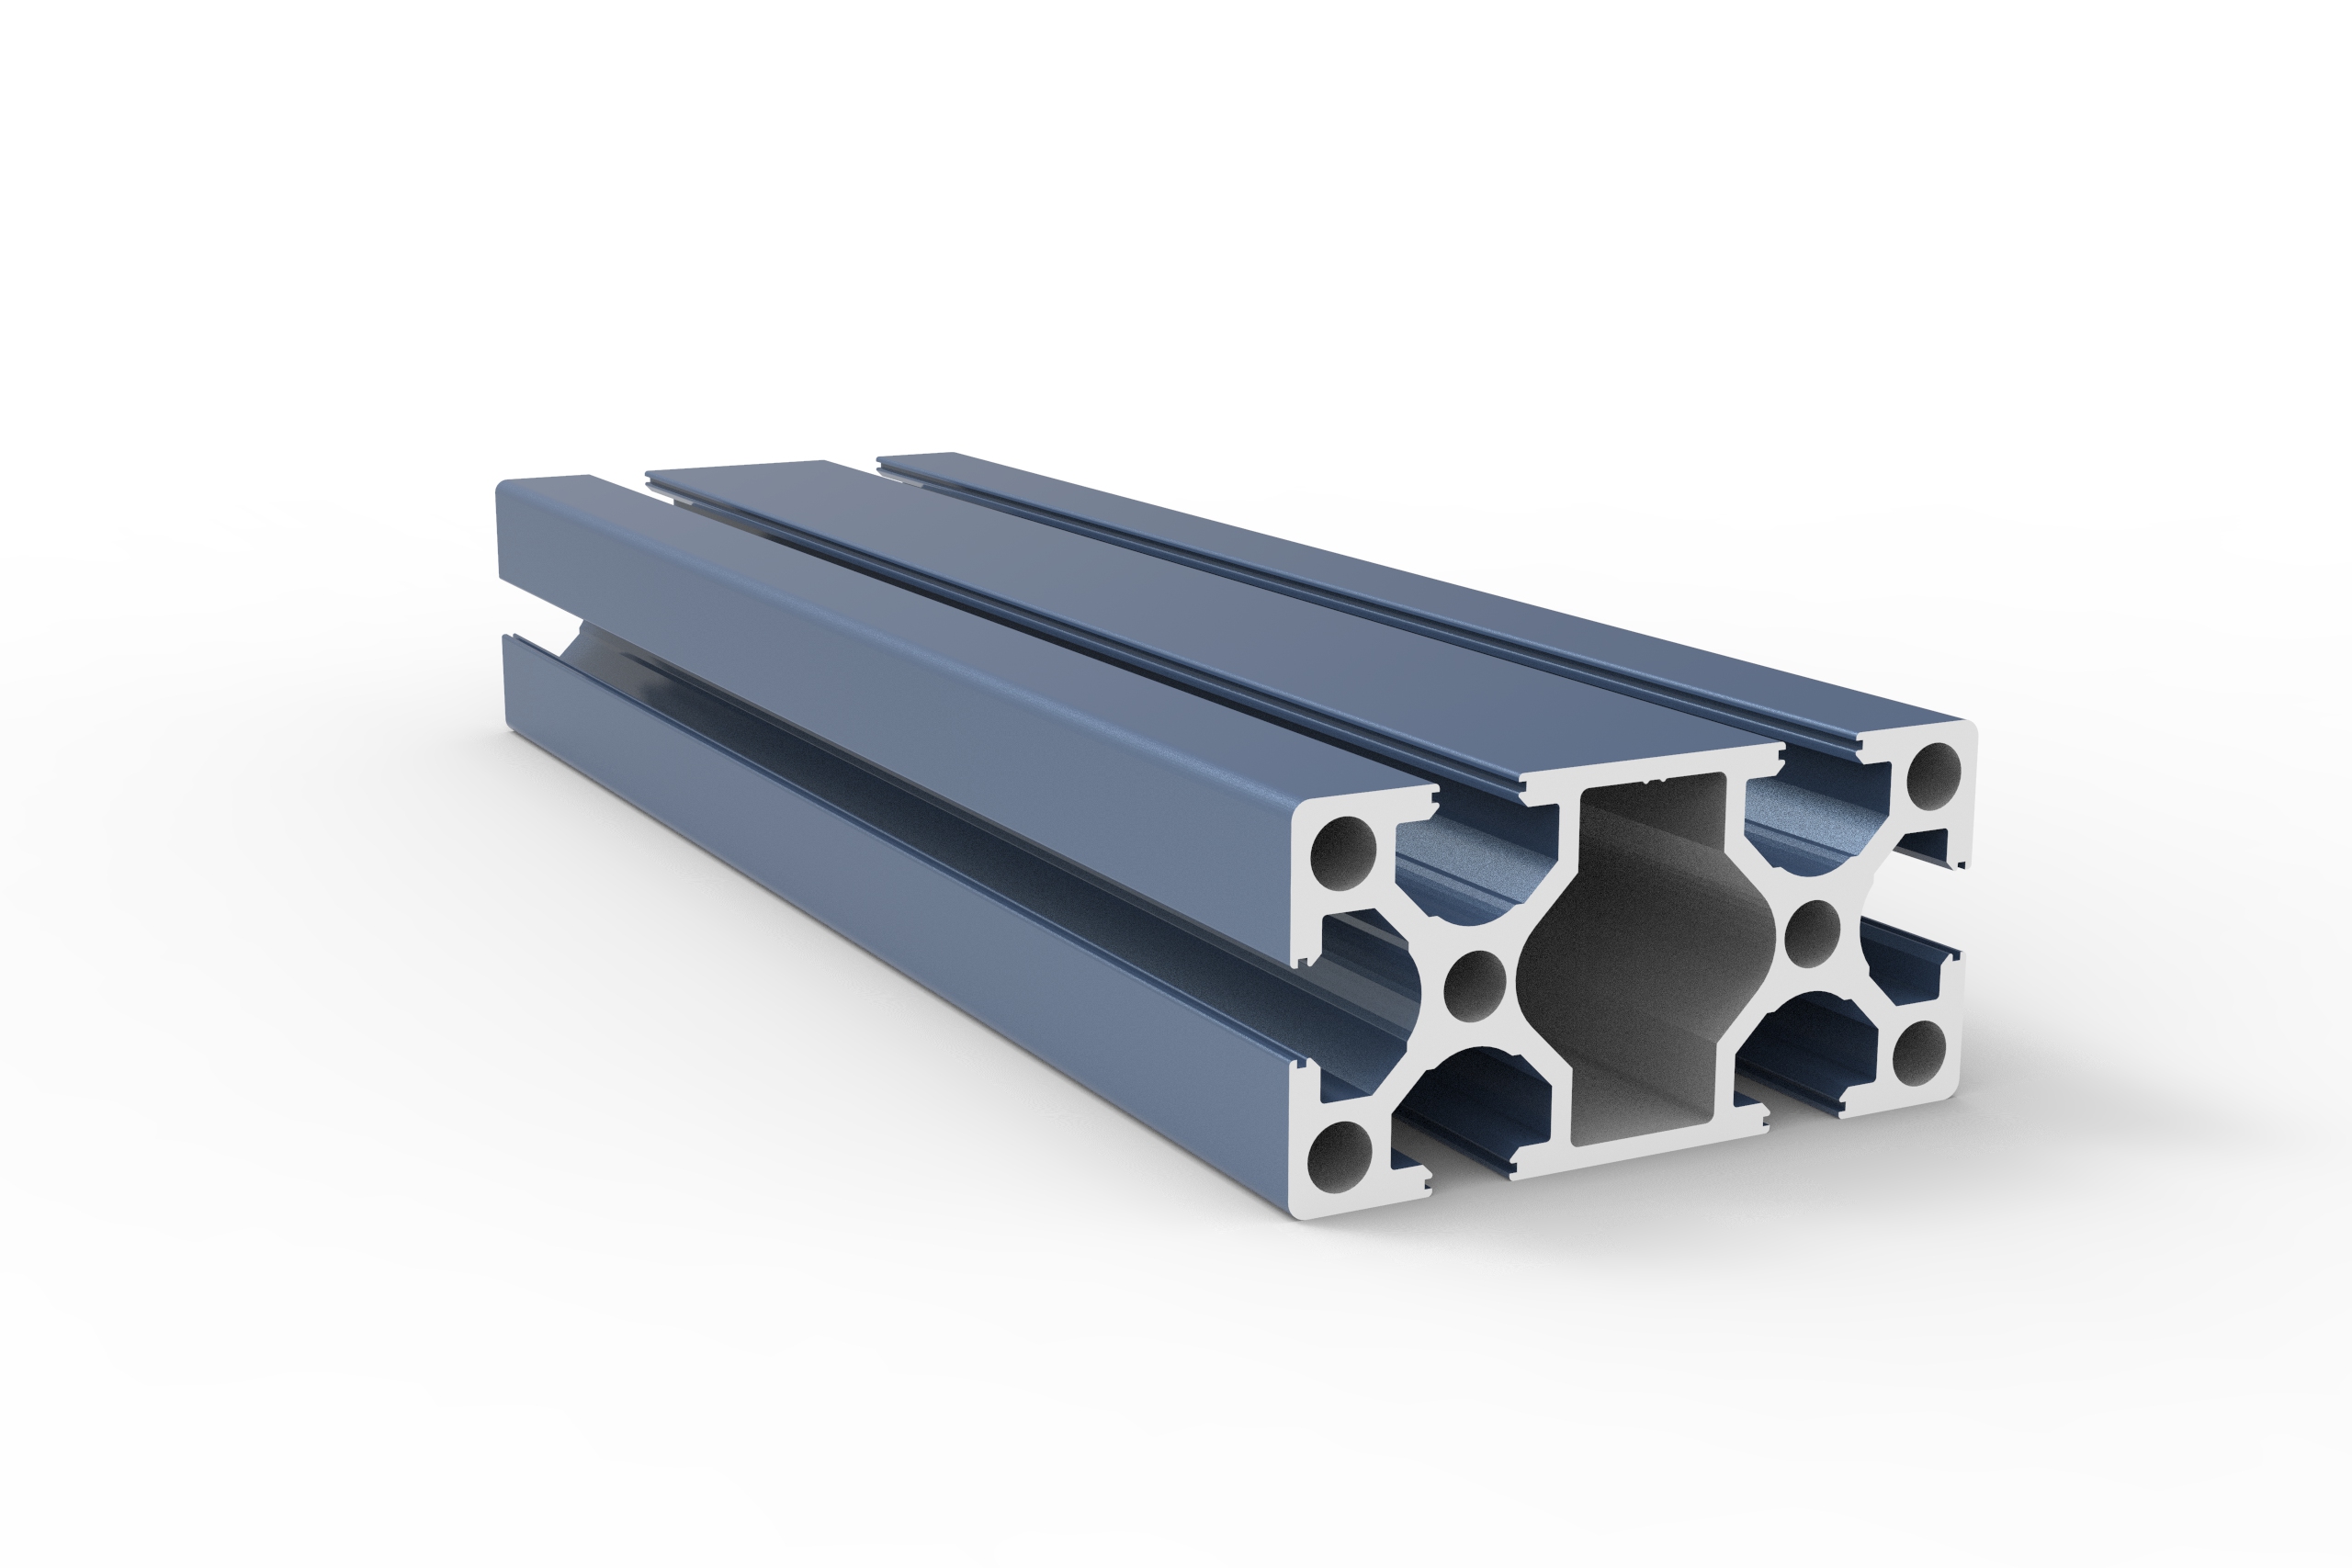
What frame materials make a Sliding window last in harsh coastal weather?
How can I verify that a Shutter certificate matches the actual product?
Can automated Shutters replace manual systems without raising lifecycle costs?
How do I choose the right Casement window size for a windy building?
What should an ethical audit cover at a Decorative profile factory?
How should I document Industrial profile defects before disputing the final payment?
Are lightweight Industrial profile alloys reliable enough for demanding machinery?
Are thermal-break casement windows becoming a better long-term choice than standard frames?
What is a realistic MOQ for custom sliding windows without pushing up unit cost?
What casement window specs should I compare for windy and rainy project sites?
Are there better material options for sliding windows if aluminum prices rise?
How do I ensure aluminum casement windows can handle extreme coastal winds?
What is the typical minimum order quantity for commercial sliding windows?
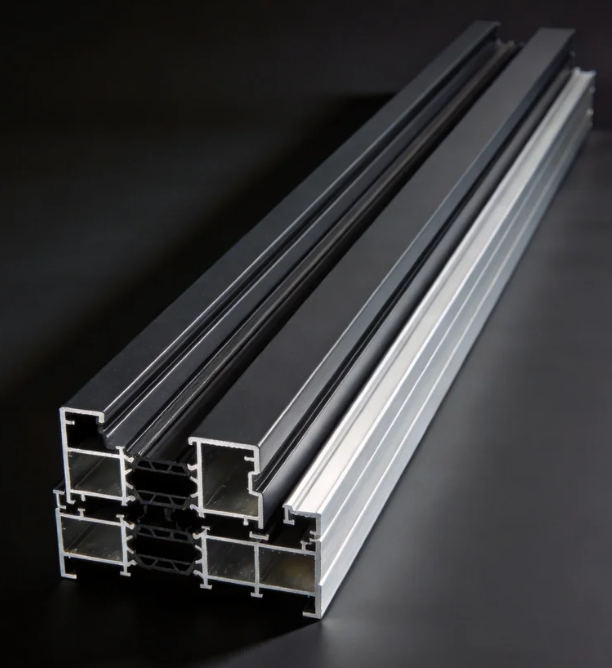
Are there energy-saving alternatives to sliding windows that reduce material and maintenance costs?
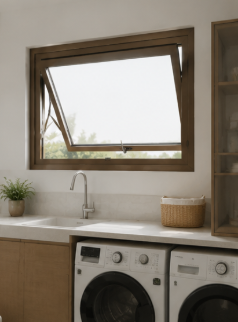
Are energy-efficient Awing windows a practical alternative for reducing long-term building costs?
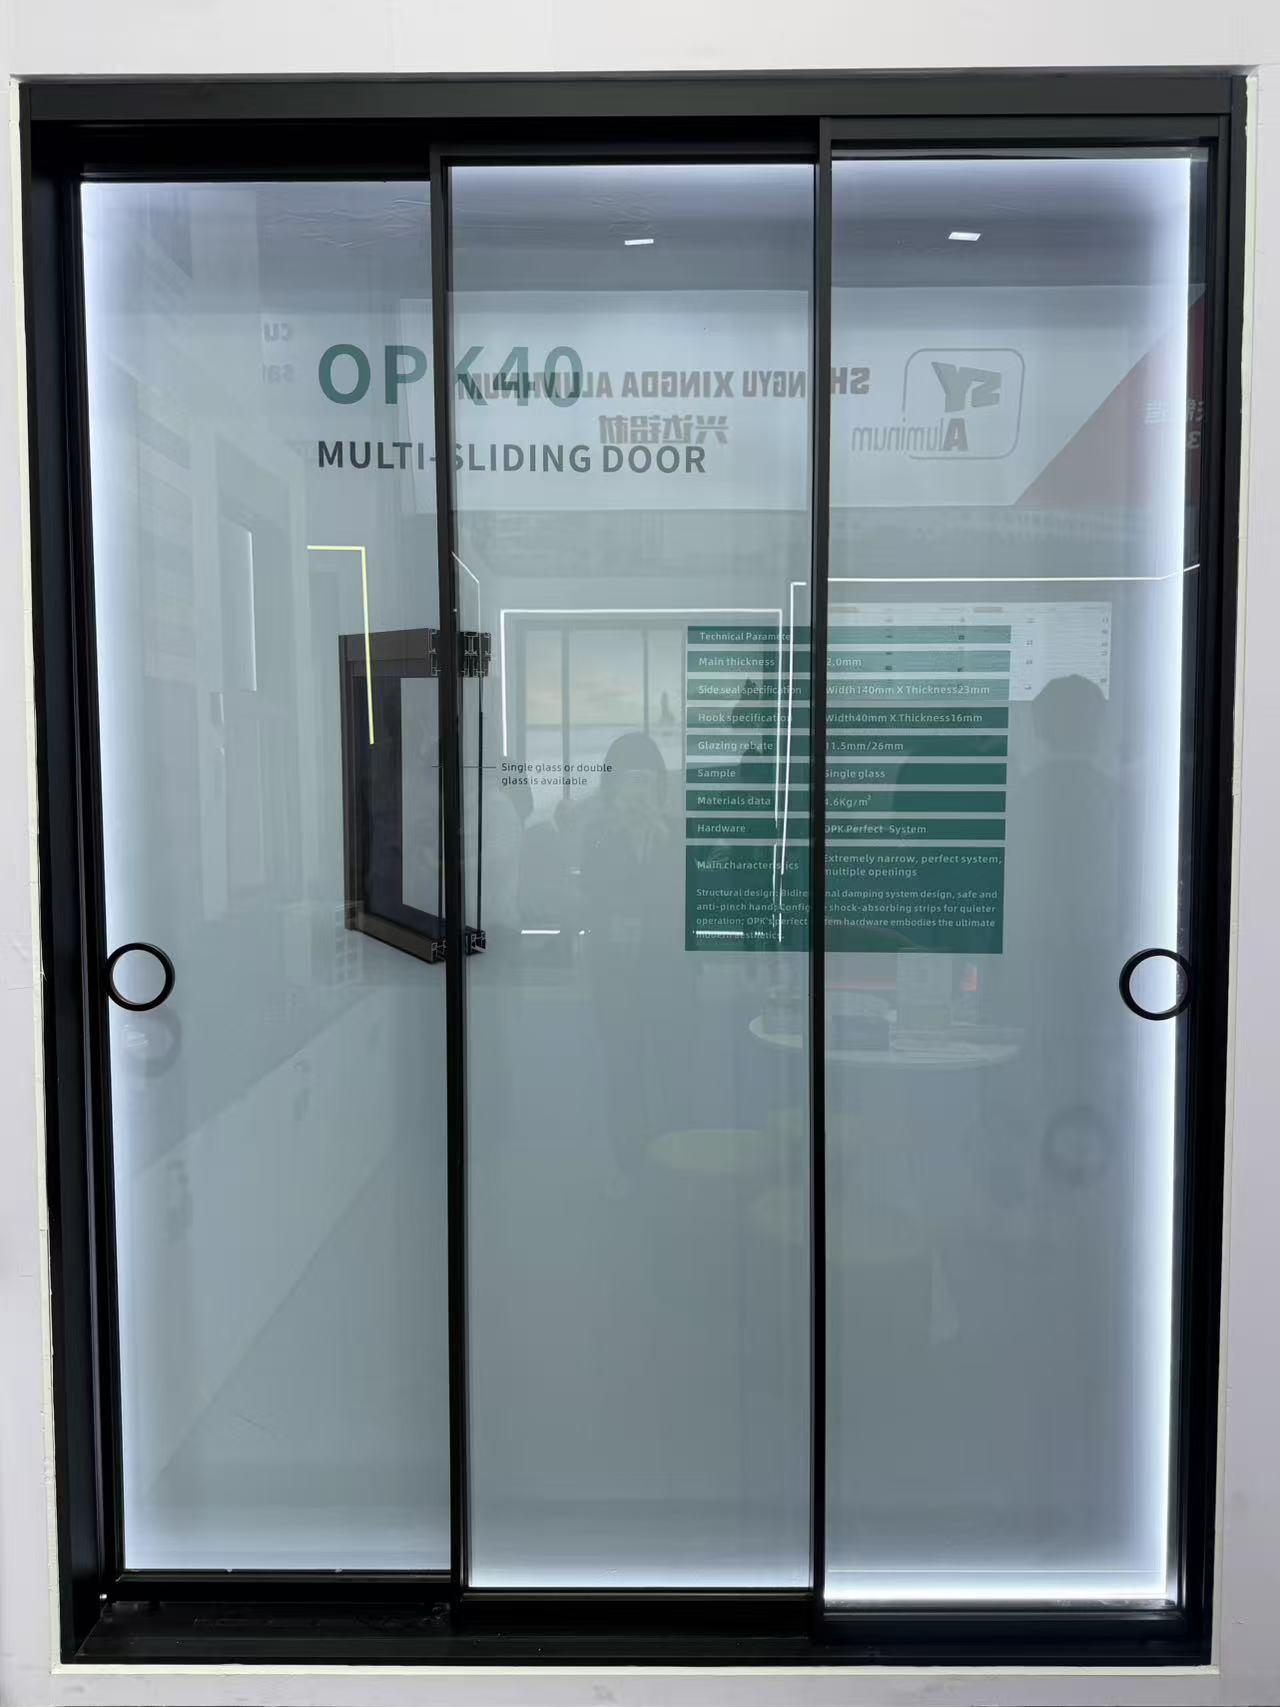
What alternatives to traditional sliding doors can lower costs without sacrificing durability?
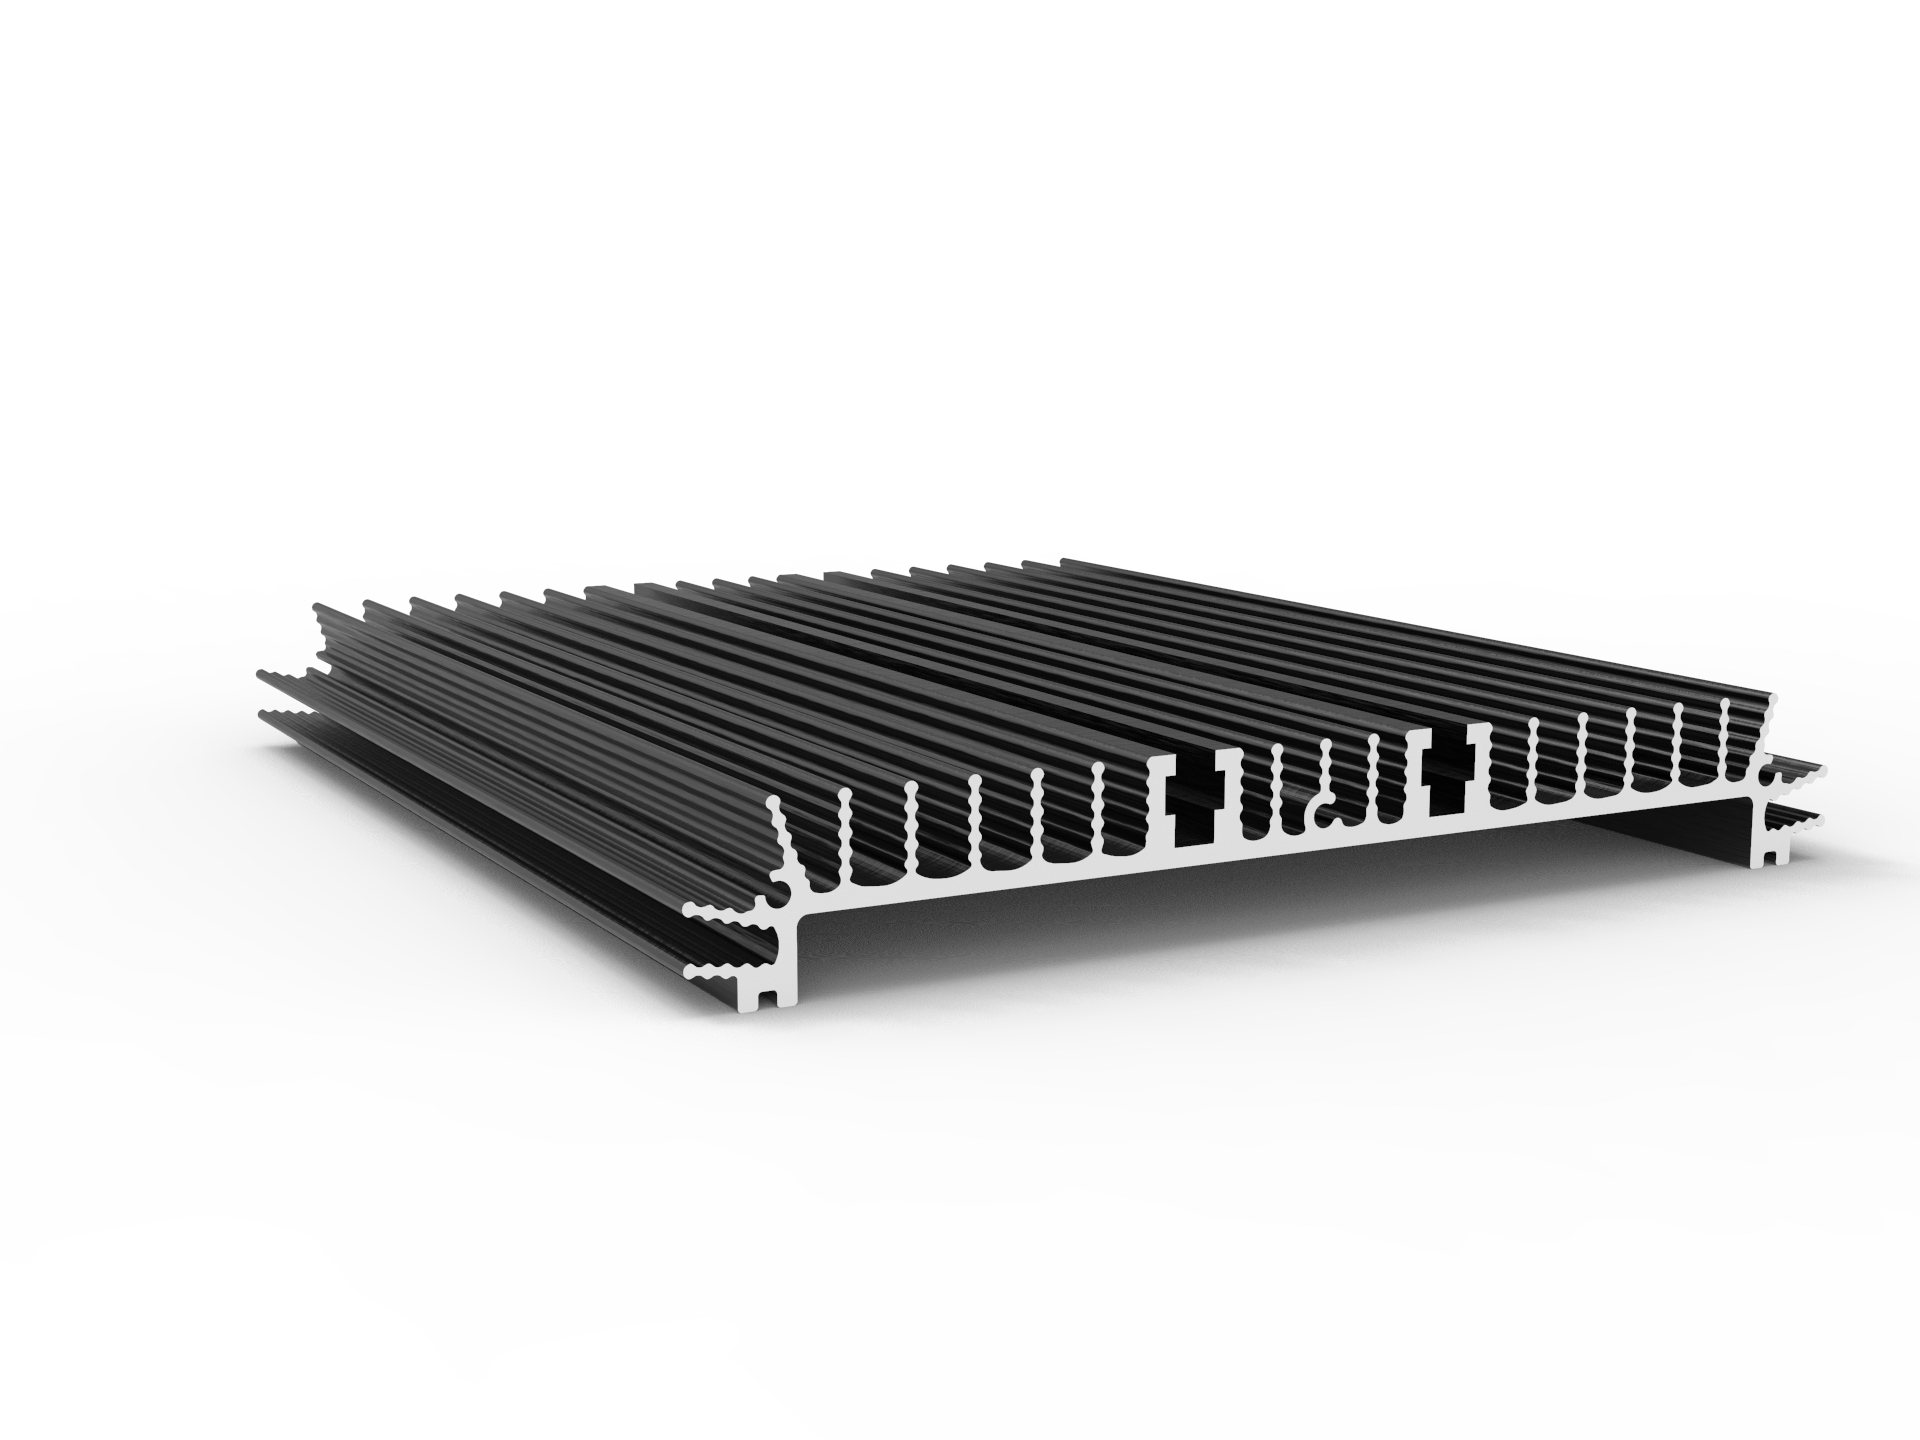
What alternatives to industrial profiles can reduce material costs without hurting strength?
Extruded Aluminium Profiles: Flexible Manufacturing for Diverse Customer Needs
Why Aluminium Curtain Walls Are Popular in Modern Architecture
How do I choose a decorative profile that stays stable in humid or harsh environments?
How do I choose an architecture profile that stays stable in harsh outdoor conditions?
How can I compare Awing window specs to avoid poor performance in harsh weather?
How can I compare Sliding door sizes and hardware ratings for harsh commercial environments?
How do I choose the right shutter specifications for harsh climates without overpaying?
What eco-friendly alternatives to folding doors can cut costs without hurting durability?
How do I choose the right shutter specifications for harsh weather without overpaying?
What eco-friendly casement door materials can lower costs without hurting durability?
What newer materials can replace industrial profiles without raising costs or supply risks?
How do I choose a decorative profile that stays stable in humid, high-traffic spaces?
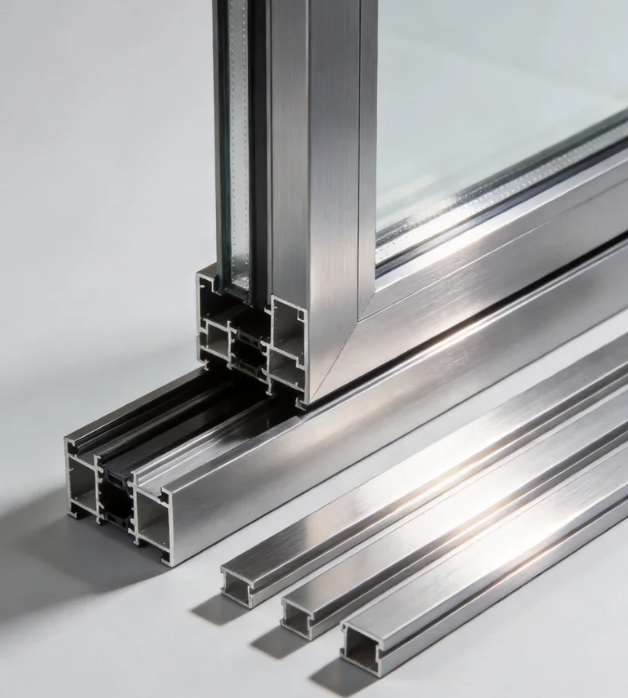
What sustainable material alternatives can replace aluminum architecture profiles?
What should I check in Awing window specs to ensure reliable performance in harsh weather?
How can I compare Sliding door sizes and thermal ratings for harsh climates before buying?
What newer materials can replace aluminum in awning windows without raising our costs?
How do I choose the right Sliding door specs for smooth operation in harsh environments?
How do I choose a folding door that stays stable in harsh weather and heavy daily use?
How can I choose the right shutter specifications for harsh weather and long-term use?
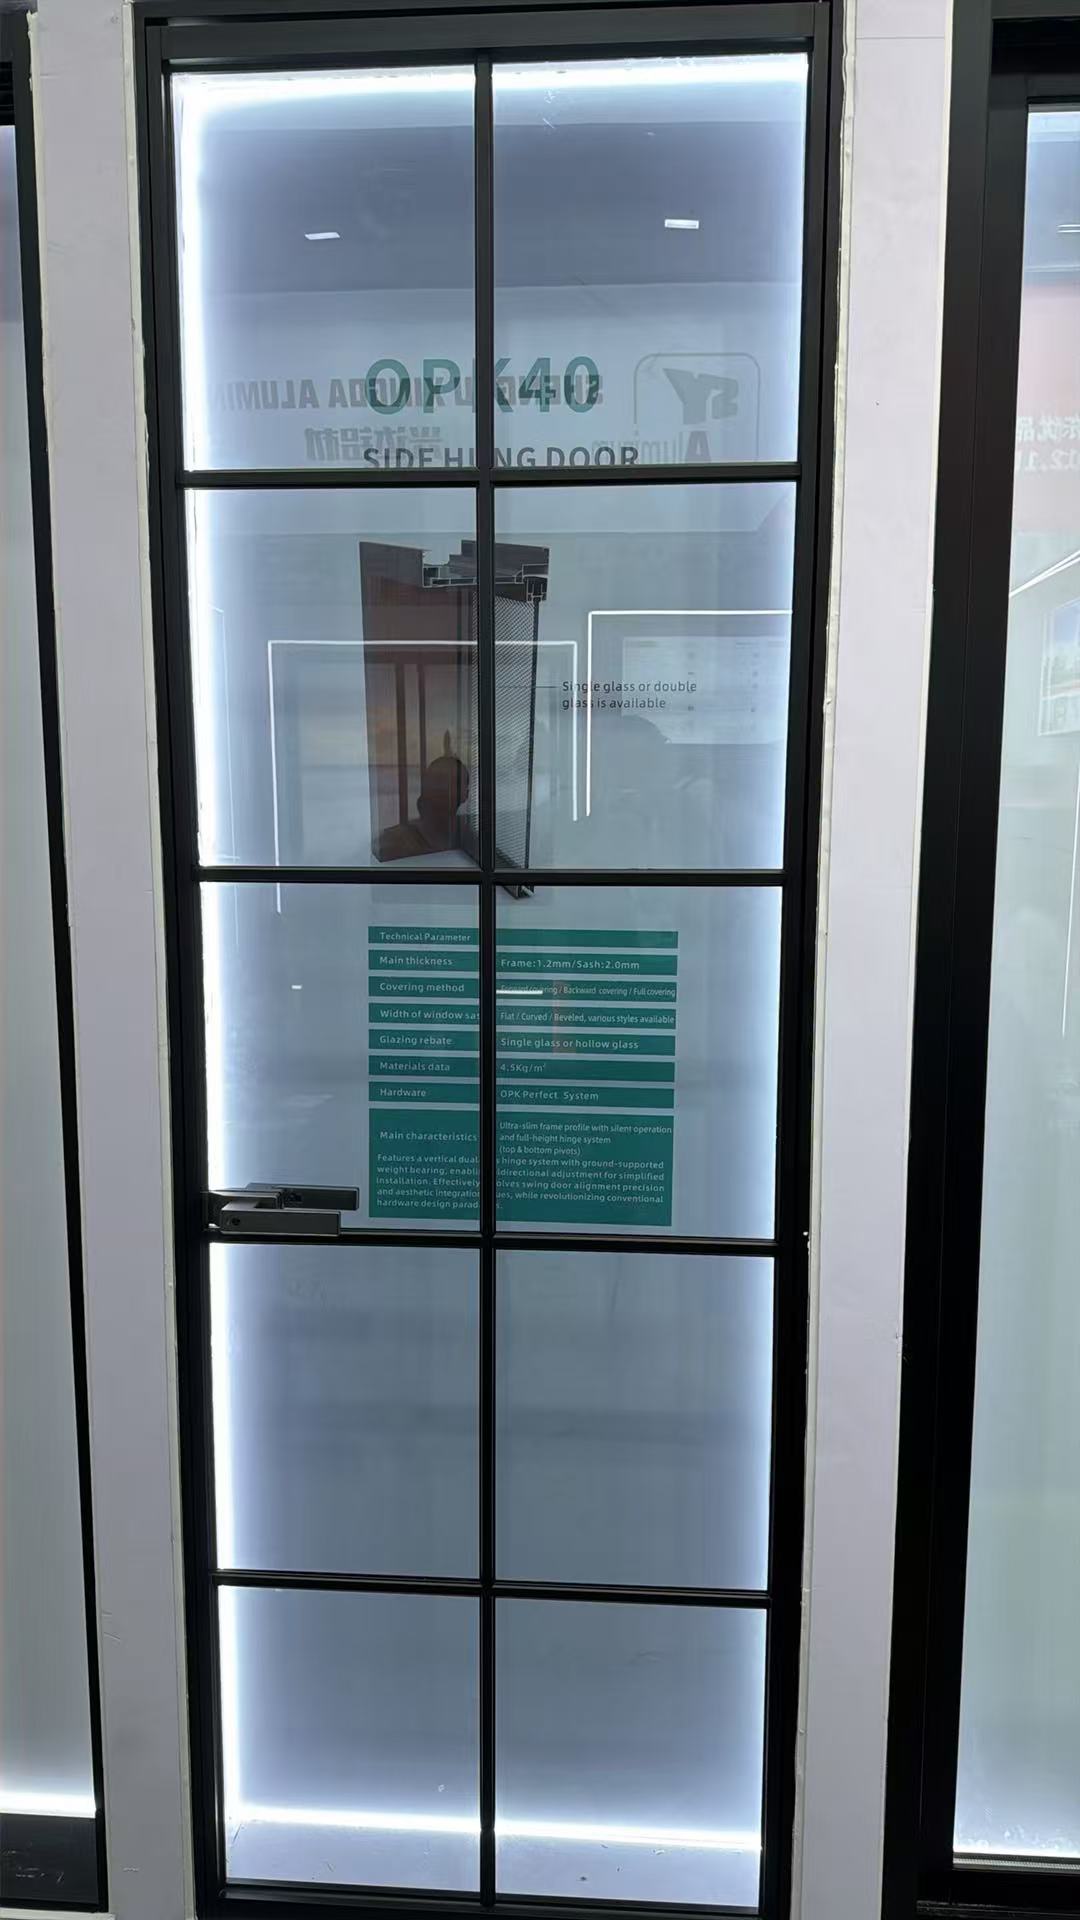
How do I compare casement door U-values, hardware, and weather sealing before buying?
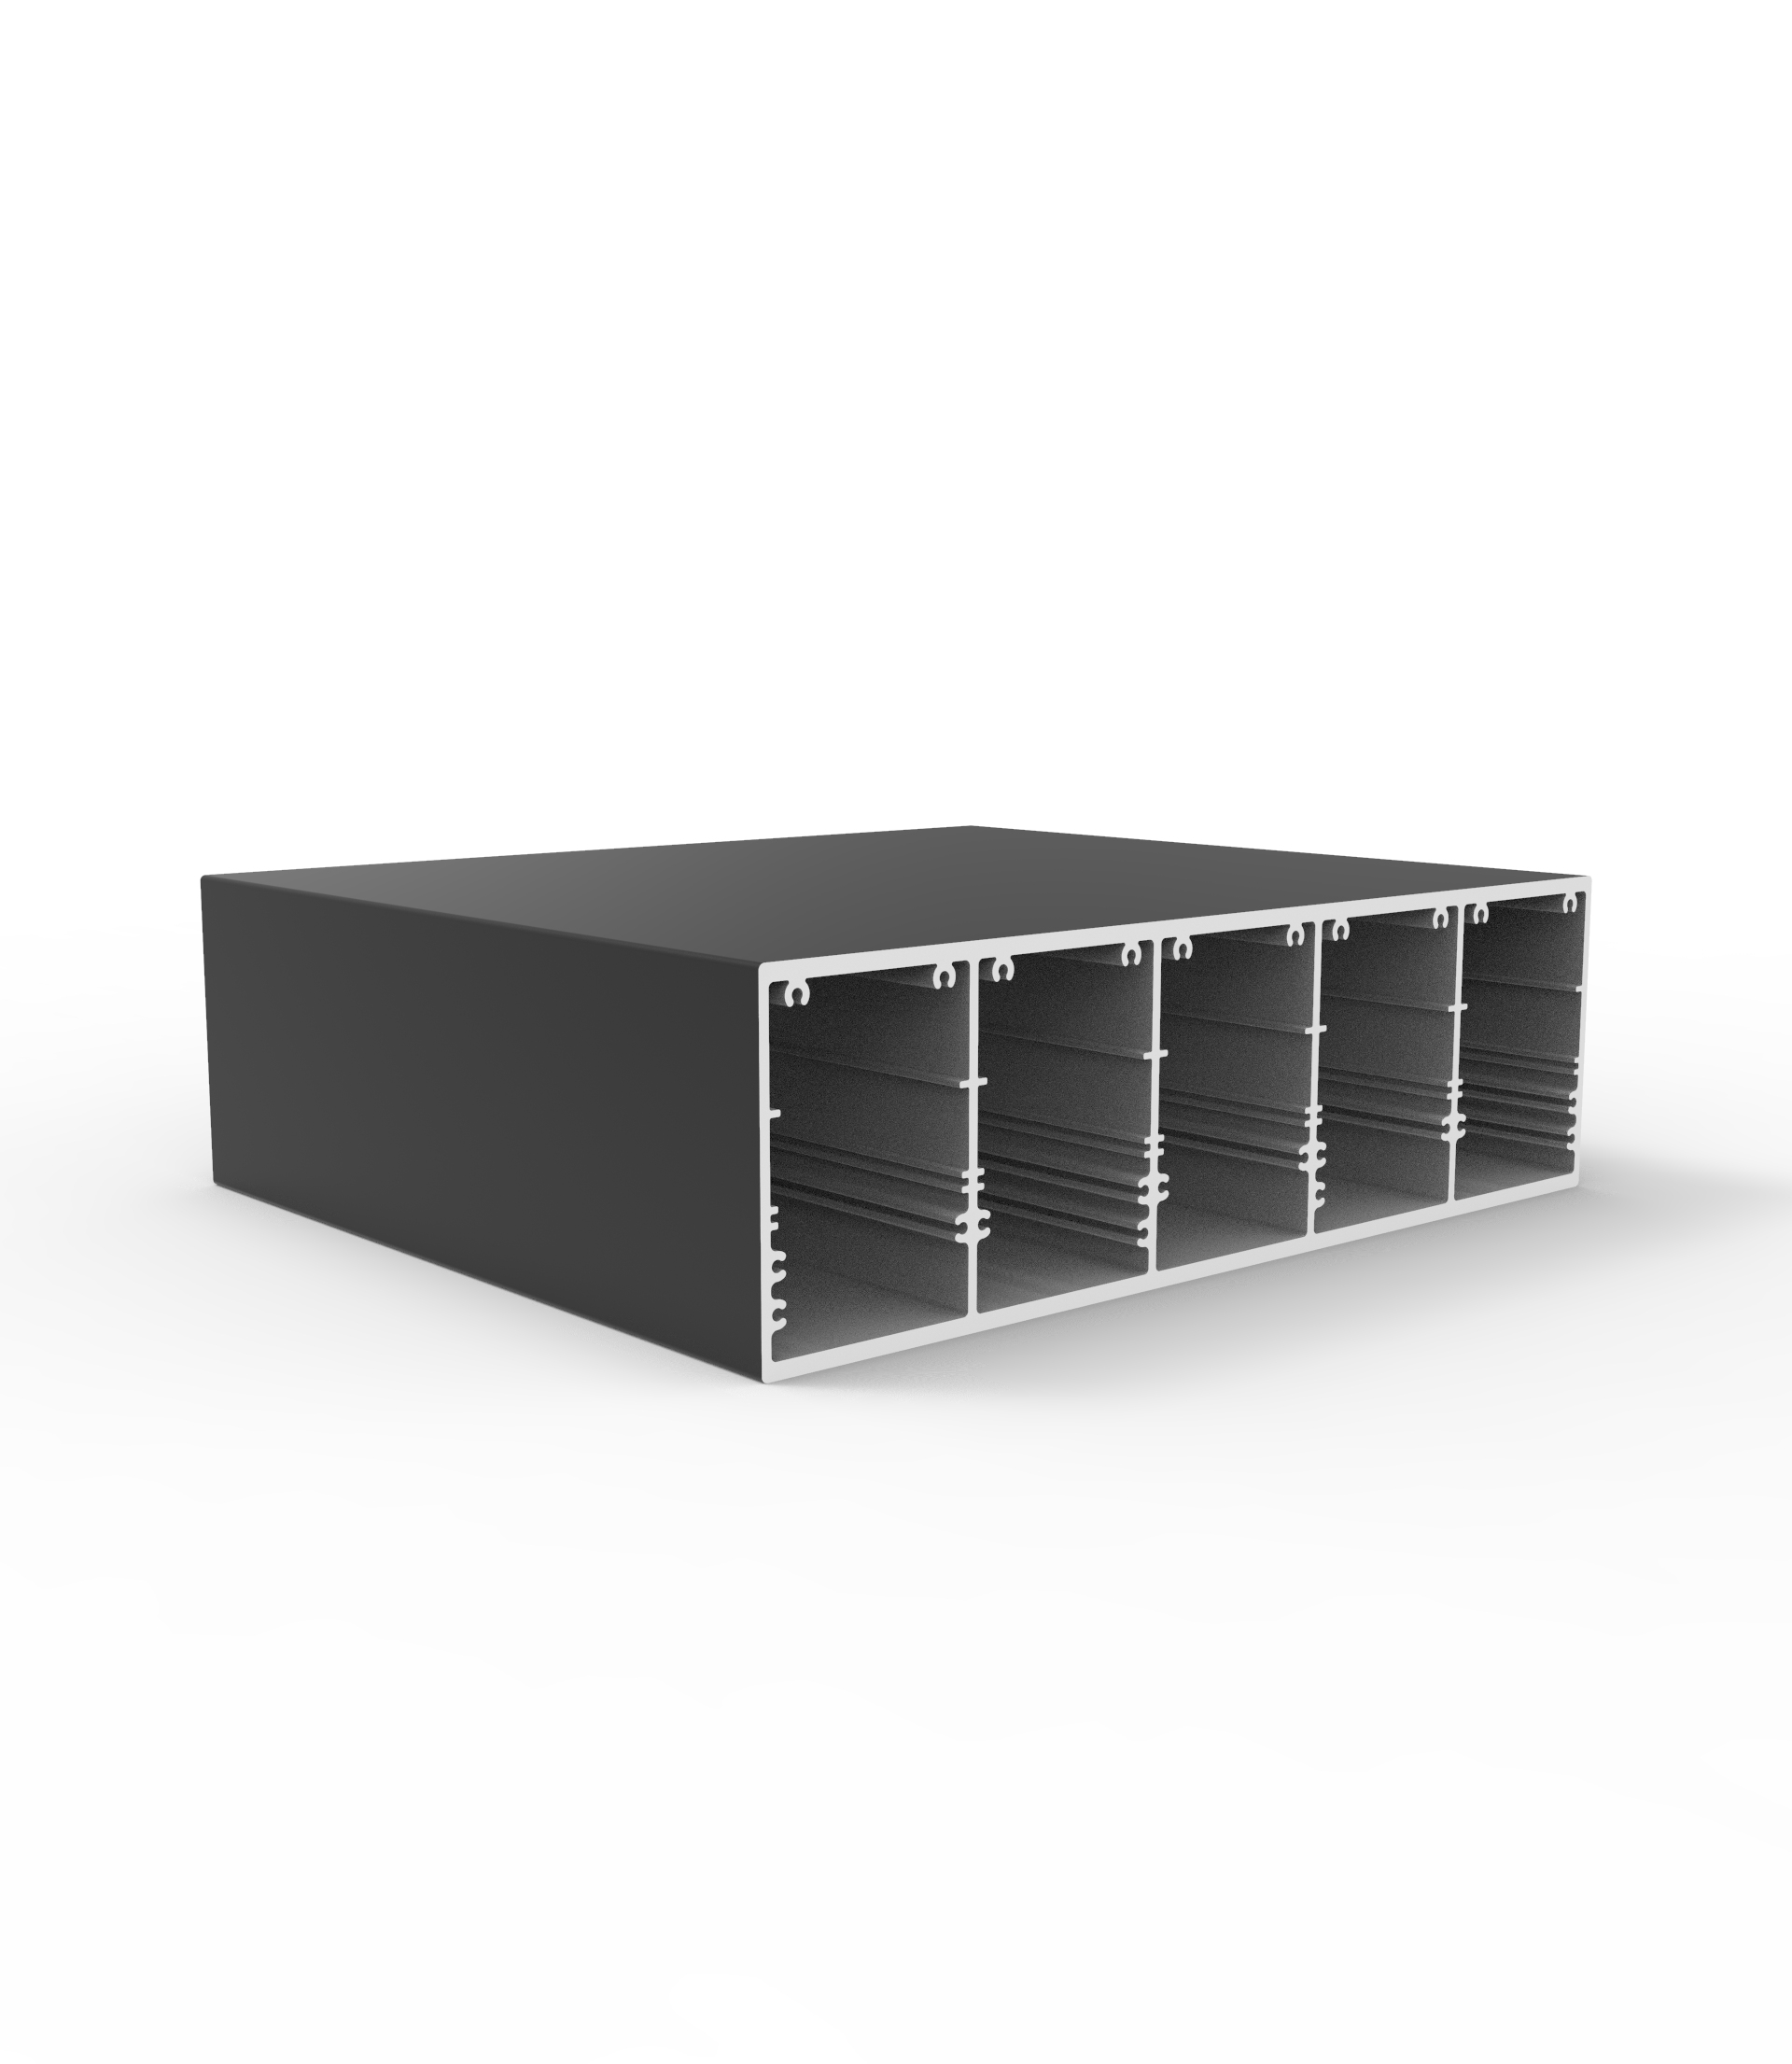
How do I choose the right industrial profile size for strength and load needs?
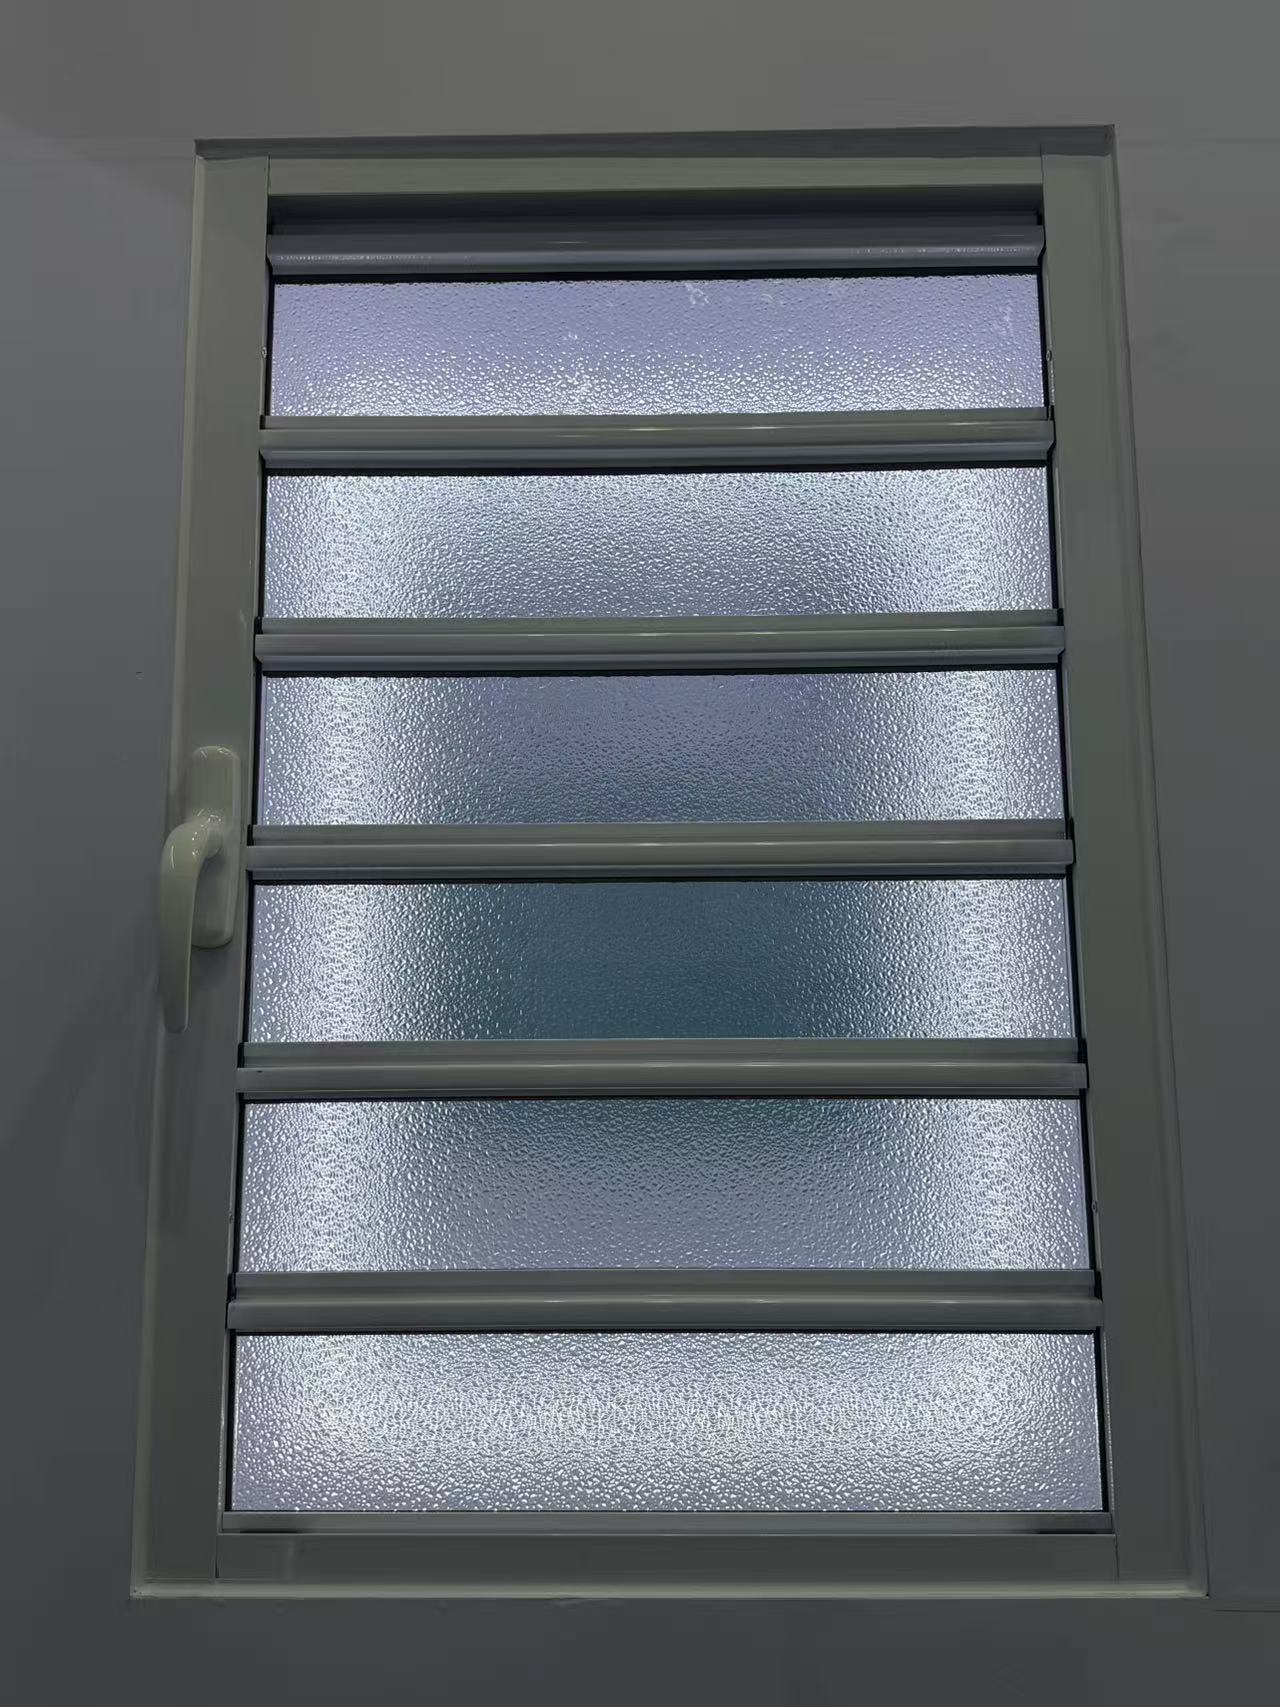
How do I choose the right shutter specifications for harsh weather and long-term commercial use?
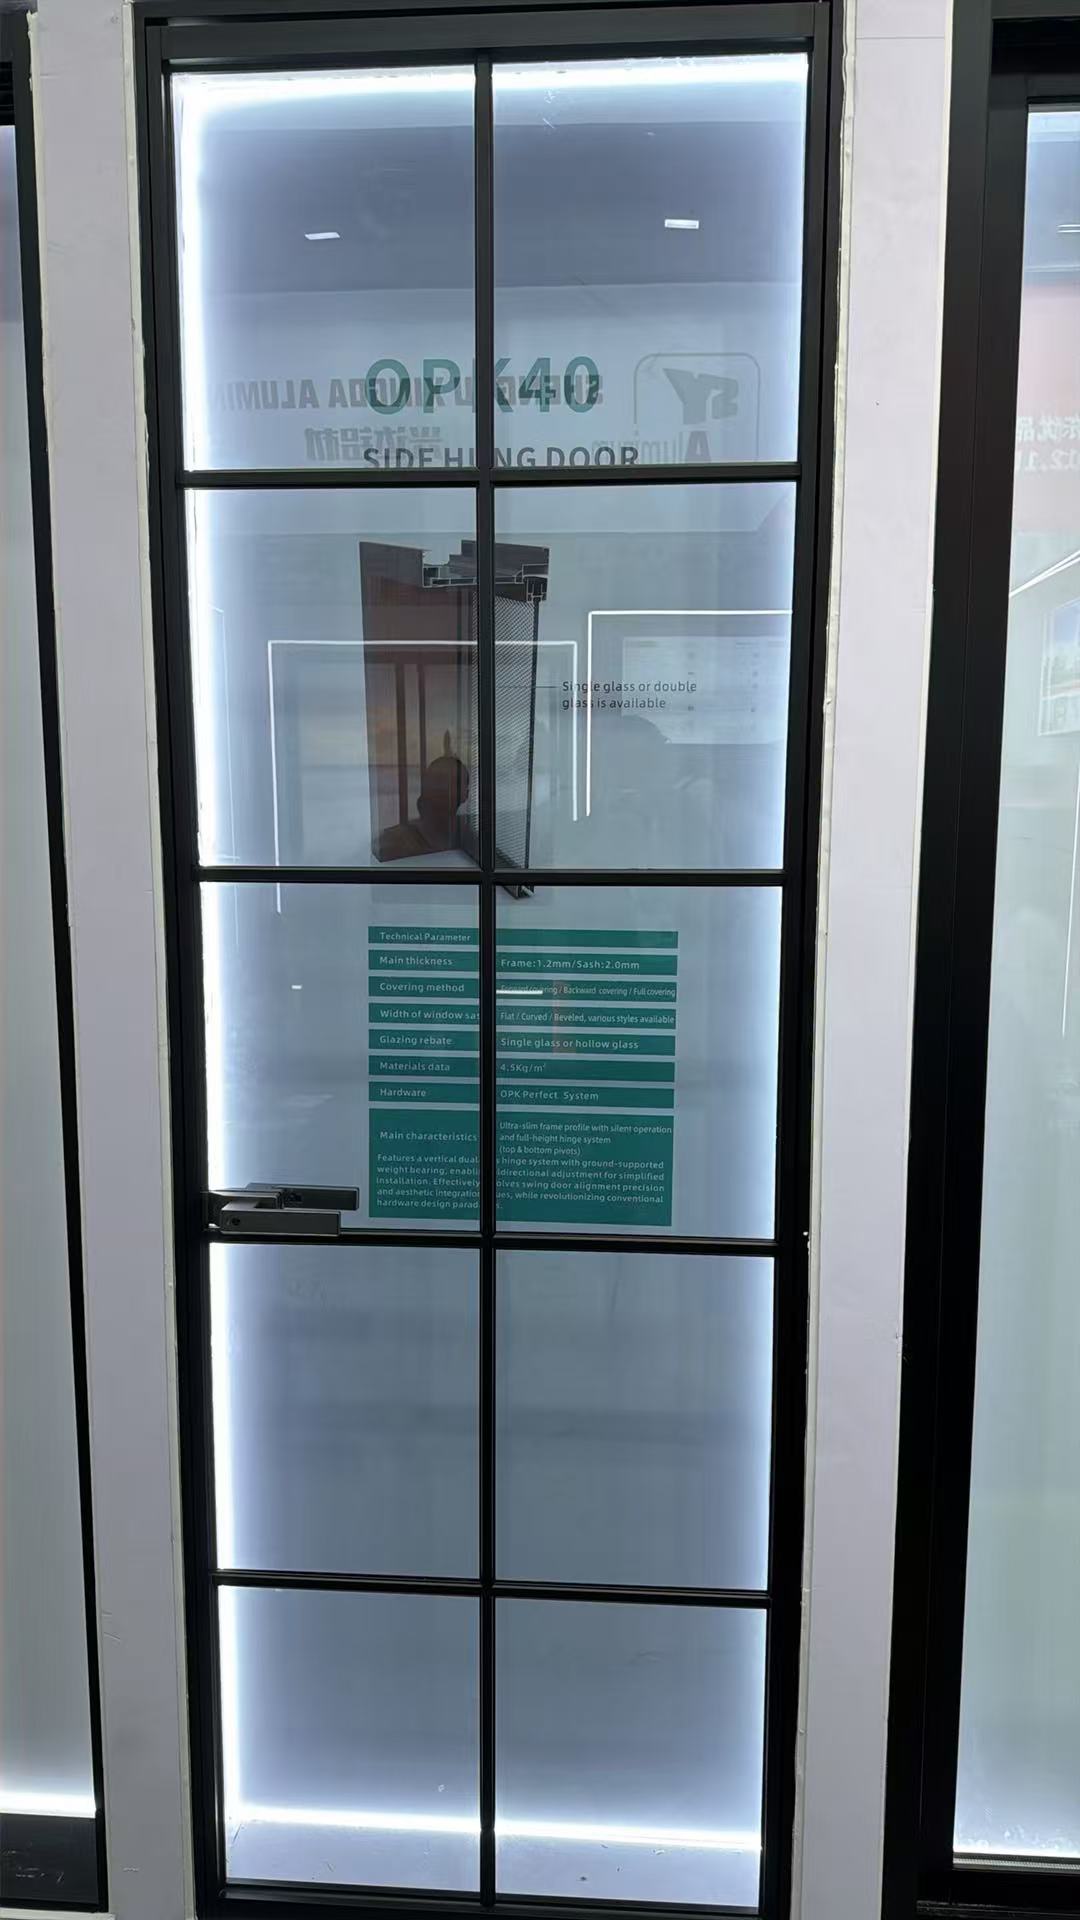
How do I choose the right Casement door size and hardware for harsh weather?
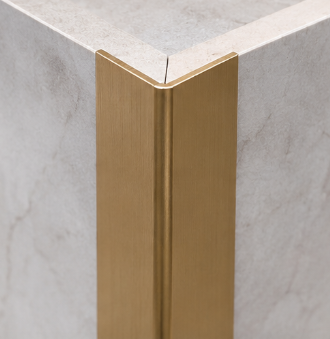
What greener alternatives to decorative profile can cut costs without hurting durability?
What lower-cost, eco-friendly materials can replace decorative profiles?
What lower-carbon alternatives to aluminum architecture profiles are practical for our project?
How can I compare sliding door systems for insulation, security, and long-term use?
What is the standard production lead time for bulk orders of folding doors?
How do I choose the right Awing window size and glass specification for harsh weather?
How can I test shutter samples so the final bulk order matches their quality and finish?
Can suppliers make custom double glass casement doors from my CAD drawings?
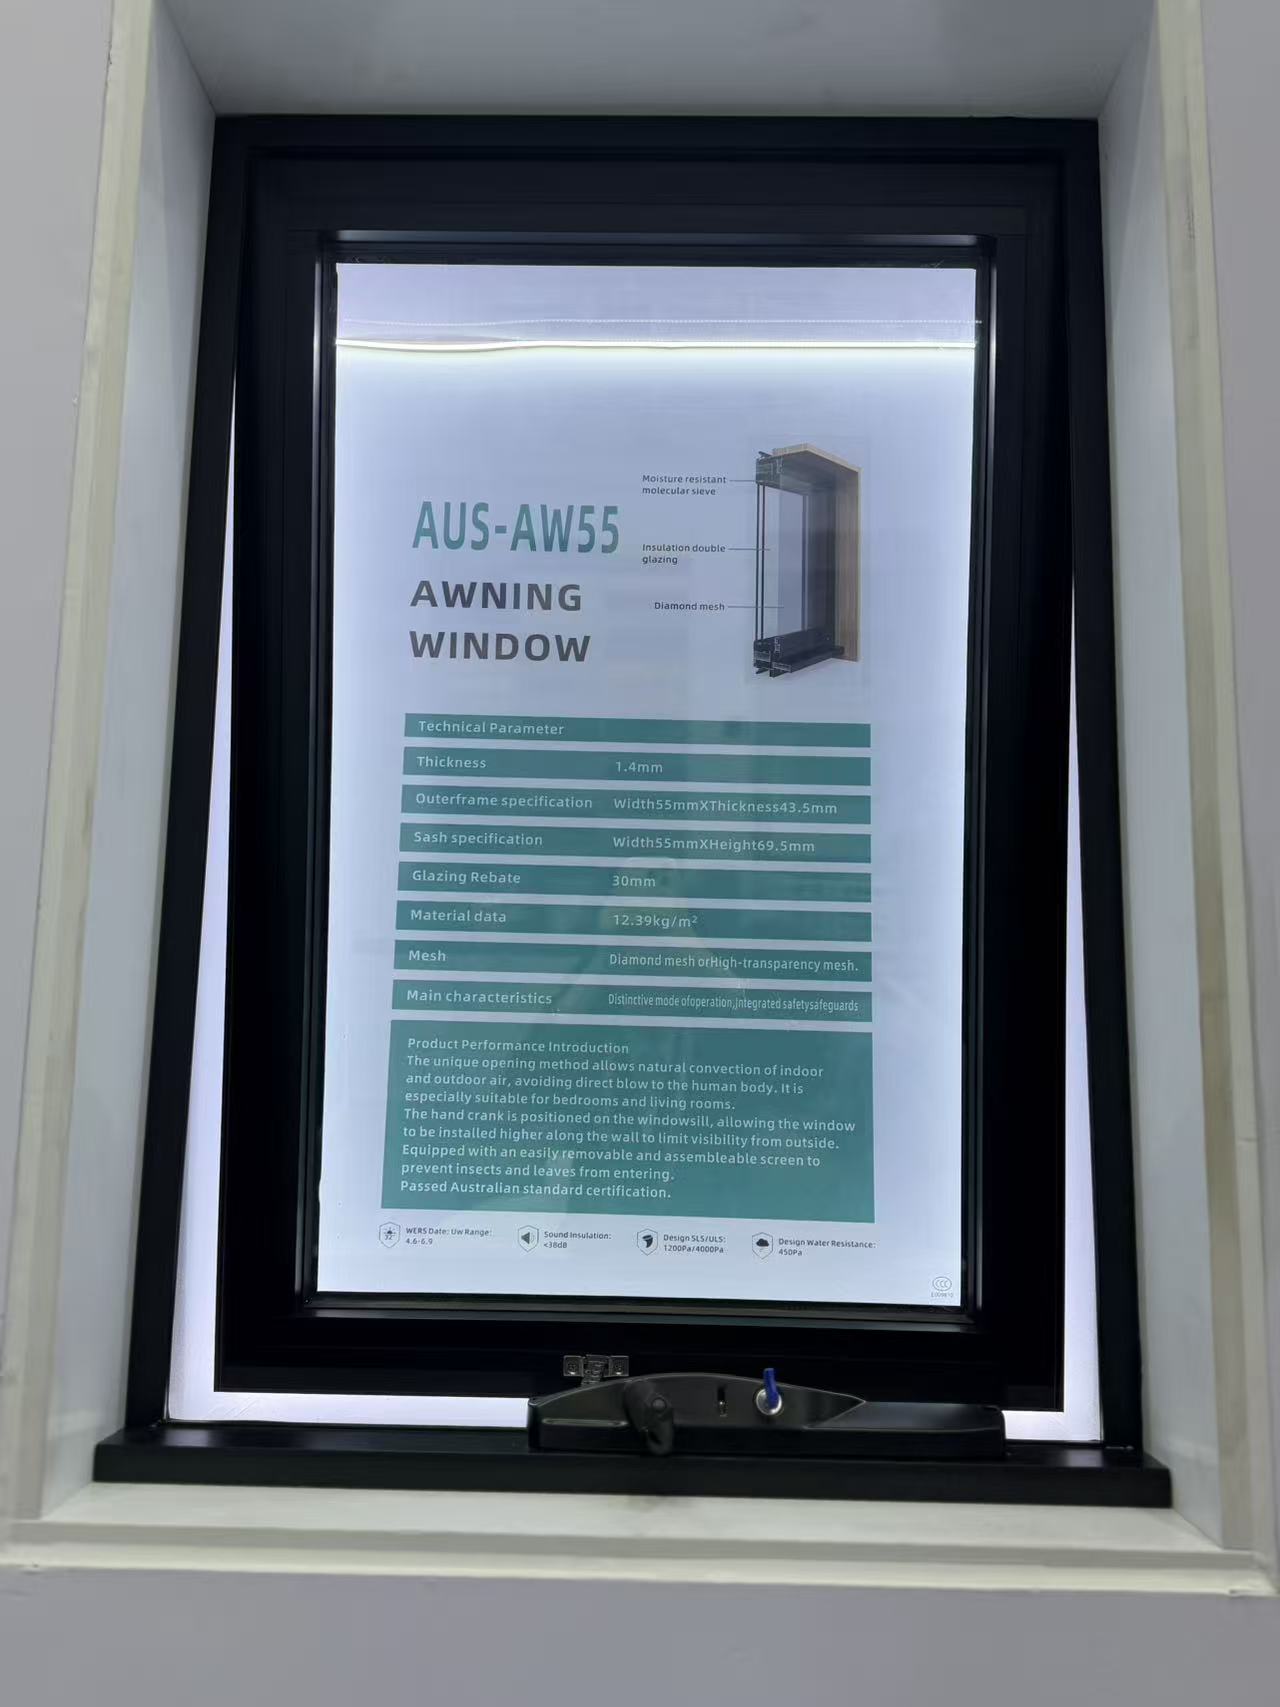
What safety certifications should I request when importing awning windows?
How long does it usually take a factory to make custom shutter samples?
What T-slot industrial profile size is best for a heavy duty machine frame?
How do I choose the right stainless steel decorative profile for high humidity areas?
How do I choose the right aluminum architecture profile for coastal buildings?
How do I choose the right stainless steel decorative profile for high humidity areas?
What wind load specs should I check for aluminum casement windows in coastal high-rises?
How do I know which aluminum industrial profile alloy is best for heavy machinery frames?
How do I choose the right alloy grade for aluminum architecture profiles?
How do I select the right heavy-duty hardware for exterior commercial floding doors?
How do I select the right glass thickness for bulk awing window orders?
What frame thickness is recommended for commercial aluminum casement doors?
What frame thickness is best for high-rise commercial sliding windows?
How to choose weather resistant aluminum floding door specs for commercial use?
How do I choose the best water tightness rating for commercial awing windows?
How do I choose the right frame material for commercial casement doors?
How do I choose the right wind load rating for sliding windows in coastal areas?
What is the best material for outdoor decorative profiles to prevent rust and fading?
How do I choose the right track thickness for high-traffic commercial sliding doors?
How do I choose between PVC and basswood shutters for high-humidity areas?
How do I choose between double and triple glazing for casement windows in cold climates?
How do I choose the right industrial profile thickness for heavy-duty cnc machine frames?
How do I choose the right alloy for outdoor architecture profiles to prevent corrosion?
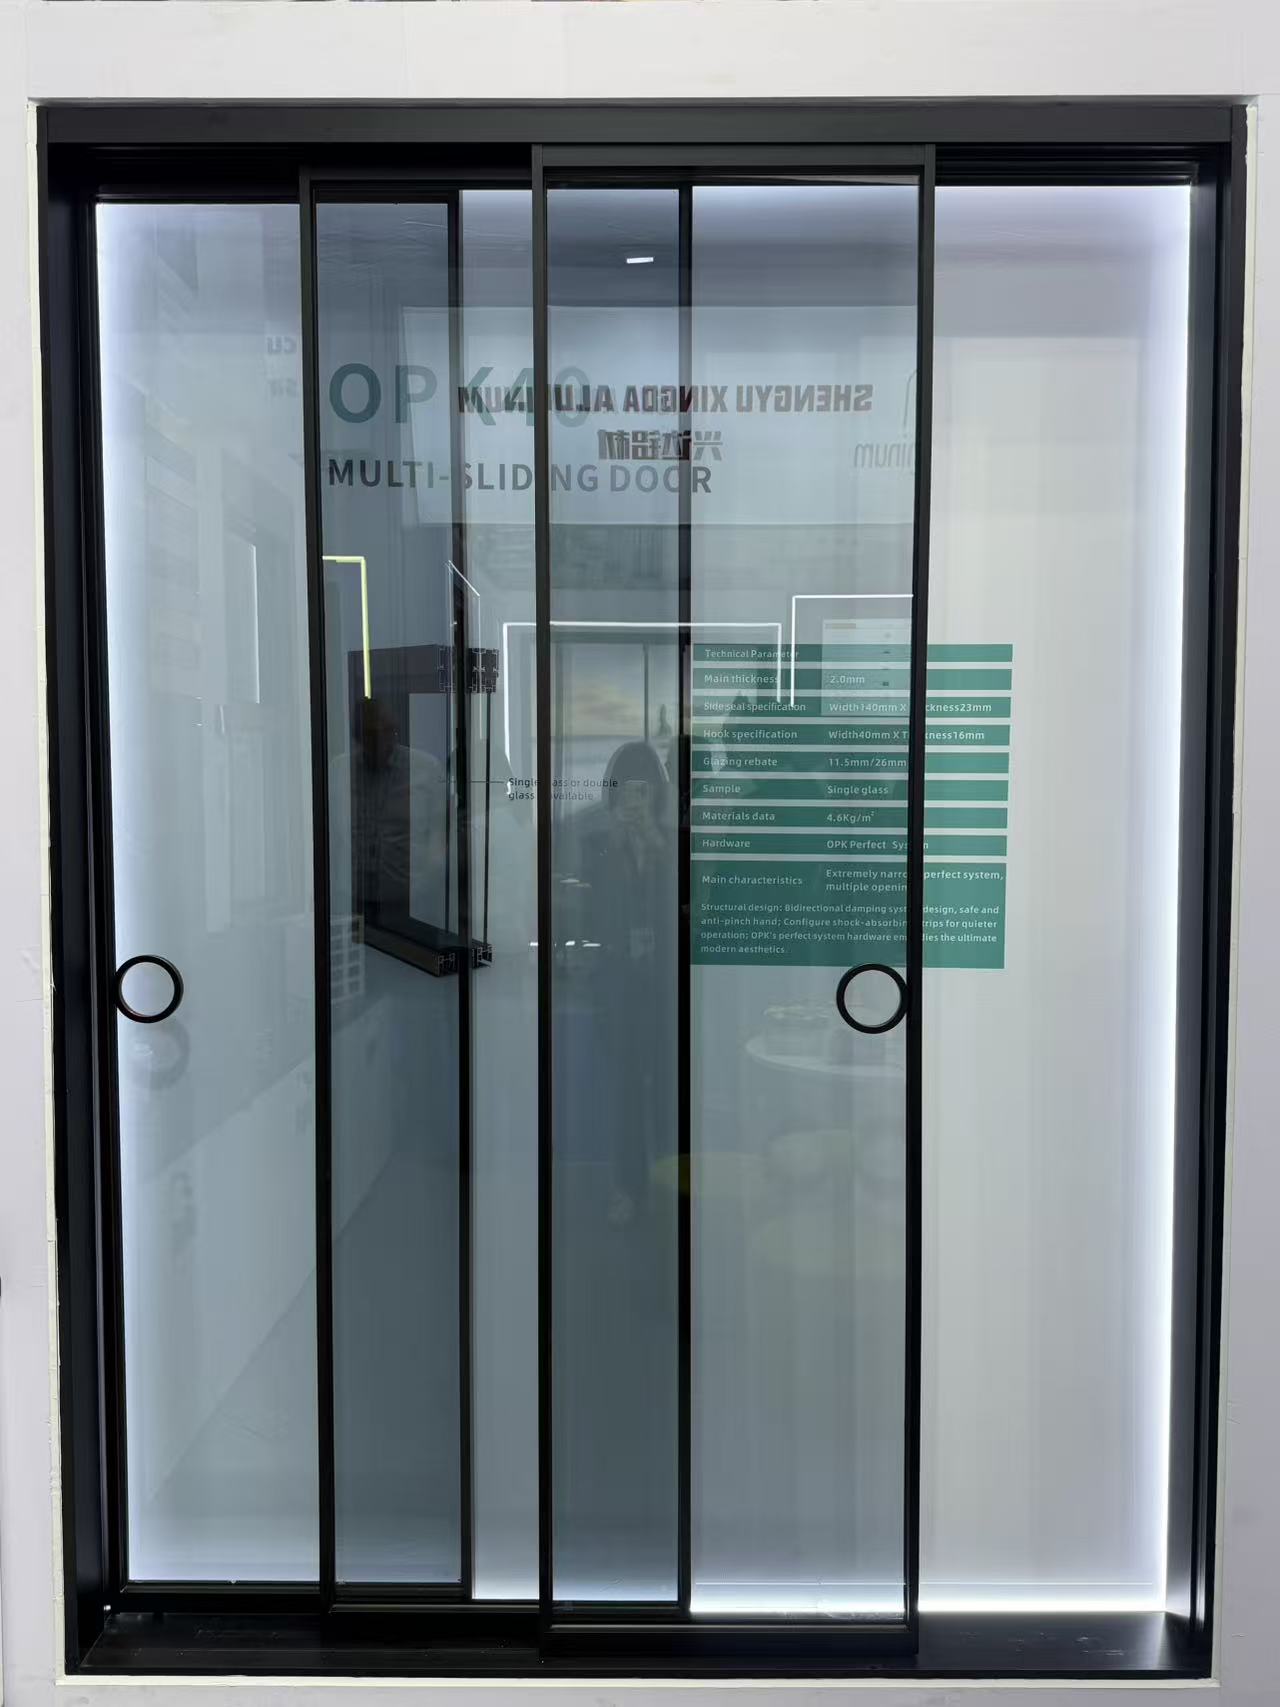
Can you design a slim frame profile for modern minimalist look?
How do I choose the right wind-resistant floding door for a coastal commercial building?
What key specs ensure a casement window can withstand heavy rain and high winds?
How do I choose the right aluminum alloy grade for heavy-duty industrial profiles?
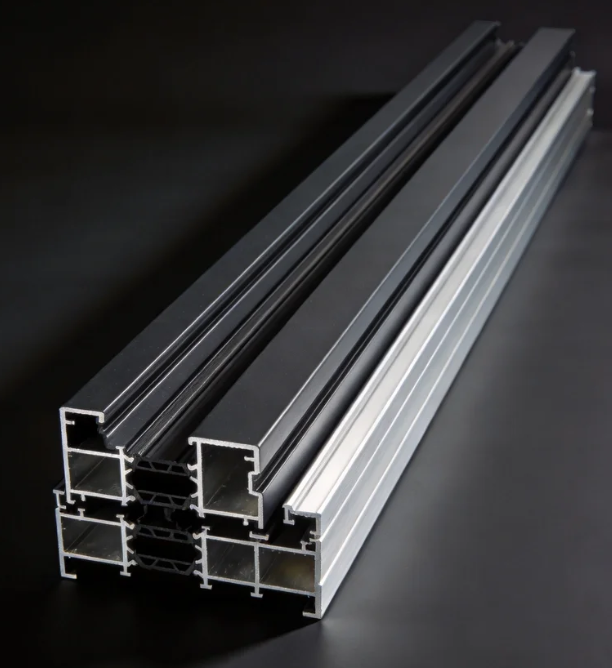
Which alloy grade of architecture profile is best for coastal areas to resist rust?
How do you pack windows to prevent glass breakage in transit?
Are slim-frame thermal break systems replacing traditional ones?
Does the price include the matching frame and installation kit?
How do you protect our proprietary design drawings from leaks?
How do I choose the right decorative profile for high-traffic hotel lobbies?
Is your factory the actual manufacturer or a trading partner?
Is it possible to 3D print a prototype before cutting steel?
Do you outsource any part of the painting process to others?
How do you handle replacement parts for damaged track rollers?
Do you accept escrow payments through third-party platforms?
Do you have ISO 9001 certification for your production line?
Are there extra fees if we pay via bank telegraphic transfer?
What is the price difference between powder coat and anodized?
What is the warranty period for the lock and hinge hardware?
What is your policy for dimensional deviations in the batch?
What happens if the shipment is delayed due to factory error?
Do you offer online technical support if color fading occurs?
Is it possible to engrave our brand logo on the tension screw?
Do you offer credit terms for long-term purchasing partners?
Can you palletize the shipments for easy forklift unloading?
What are the latest eco-friendly finish trends for decorative profiles in modern interior design?
What are the tooling cost and design limitations for customizing heavy-duty industrial profiles?
Has your architecture profile manufacturing facility passed ISO 9001 certification?
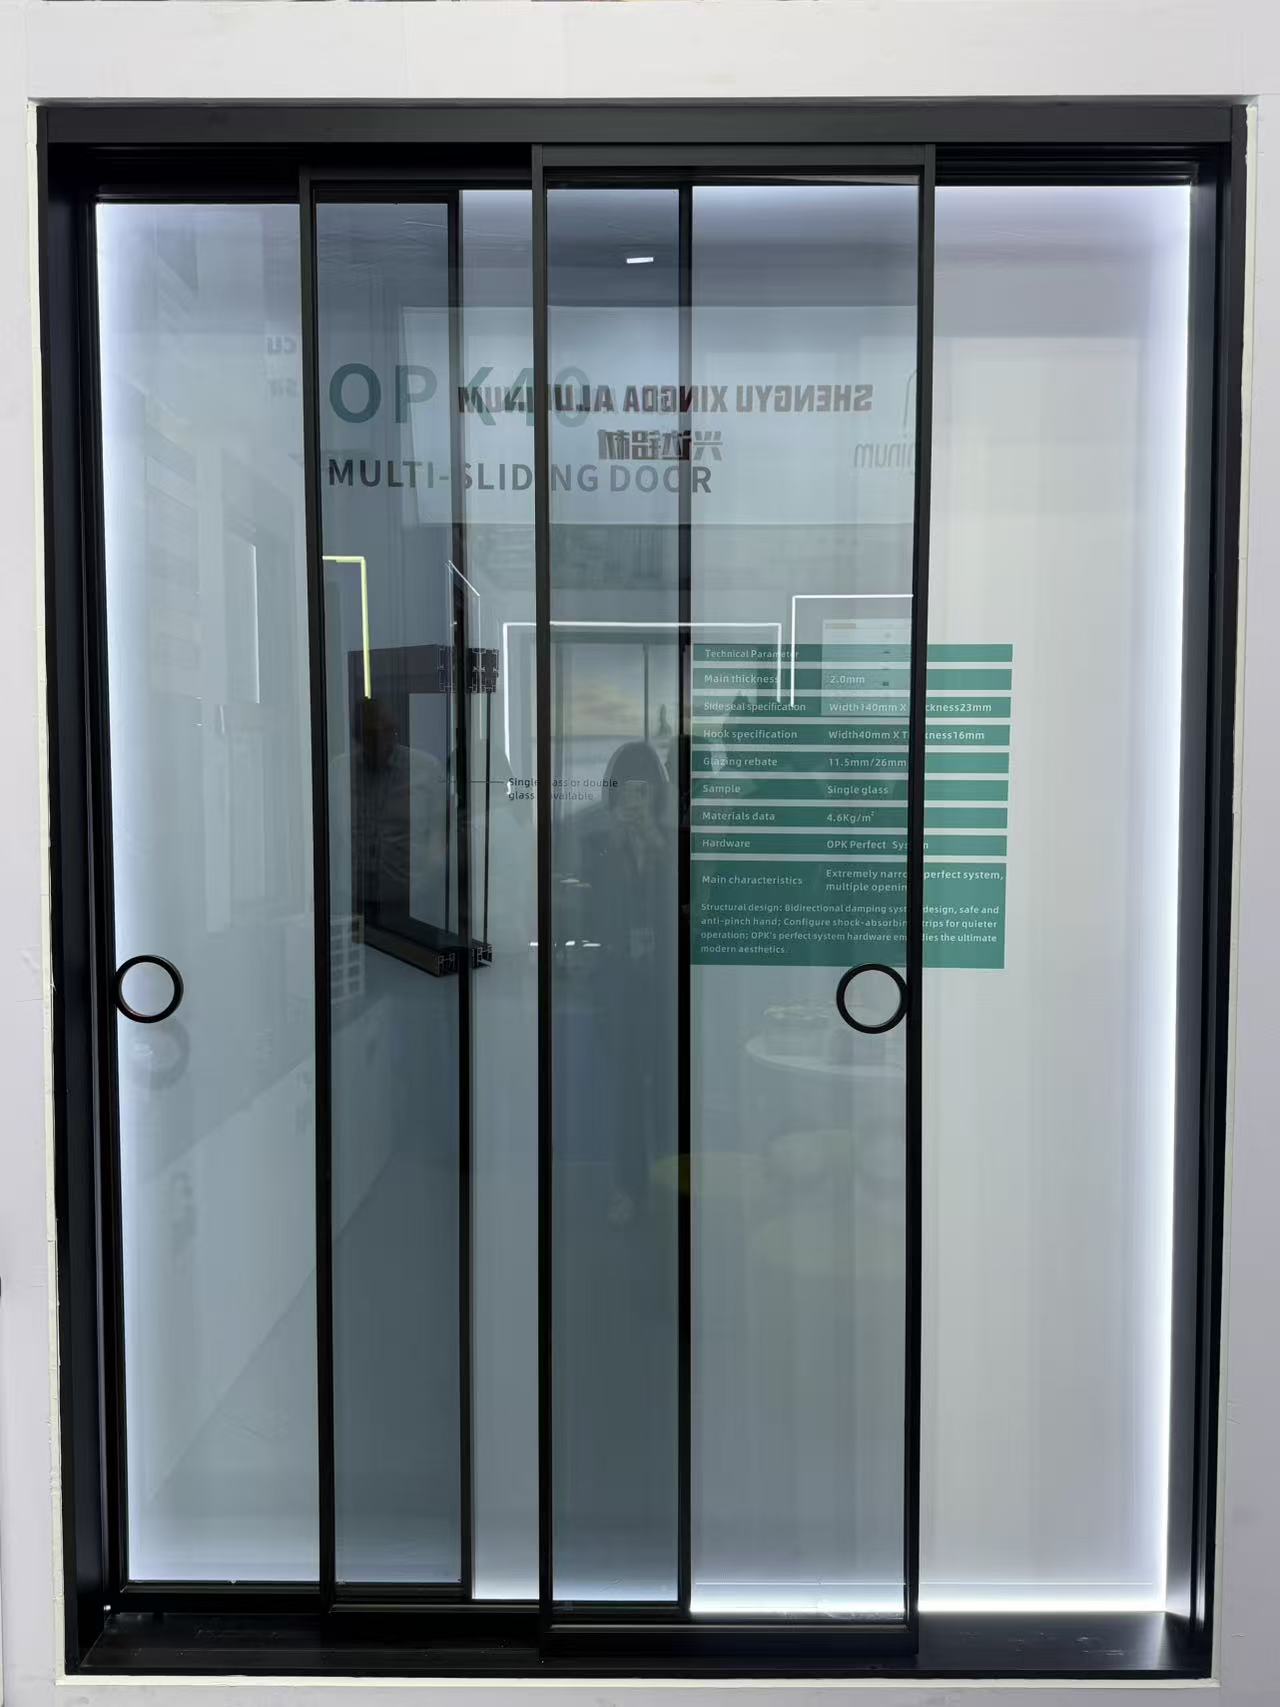
Can we use Alibaba Trade Assurance for our initial sliding door order to mitigate risk?
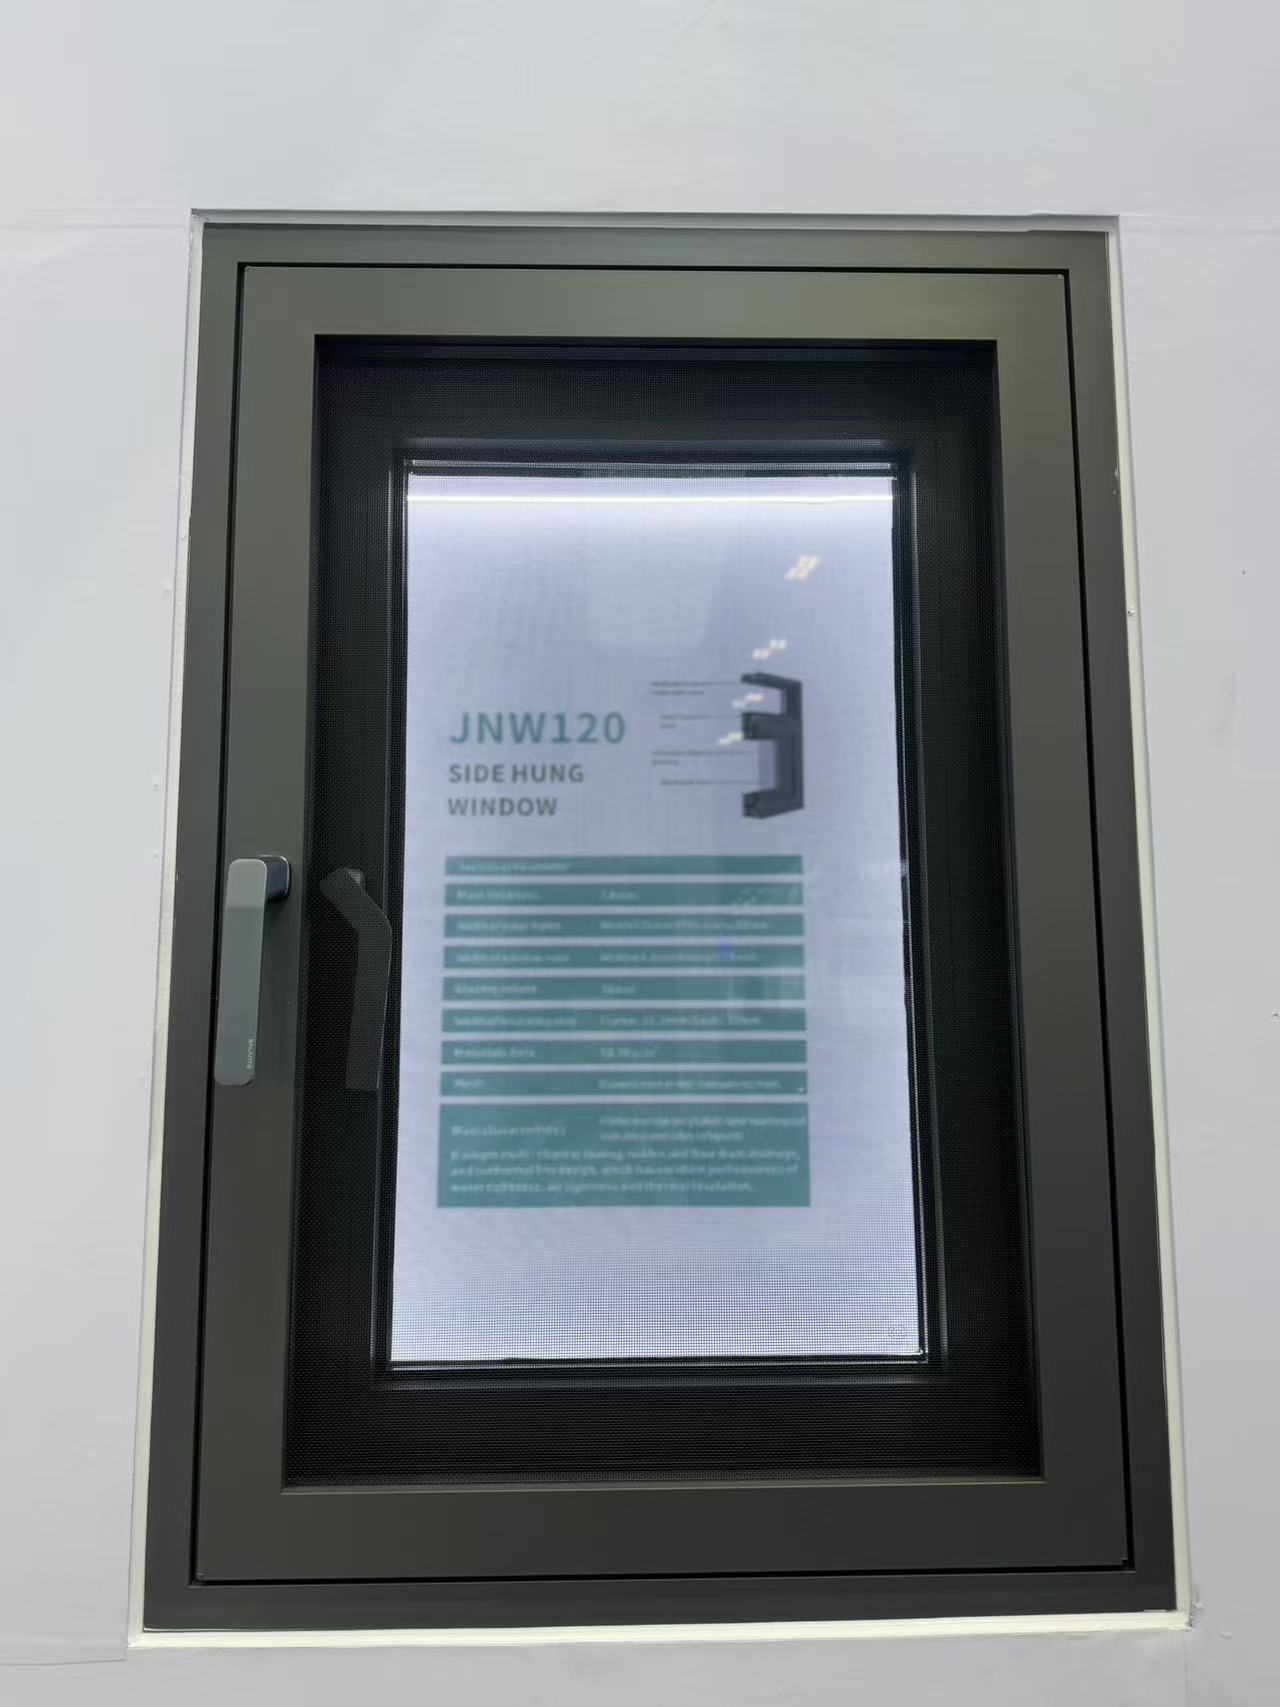
Do you provide free corner samples of the casement window frame for color verification?
Is it possible to custom-match a specific RAL color for a decorative profile order?
Can I request a 3D-printed sample before ordering a custom industrial profile mold?
Can you extrude an architecture profile based on our proprietary CAD drawings?
What thermal performance certifications does a sliding door need for the UK market?
How are heavy floding door panels crated to ensure safe unloading at the job site?
Can we arrange our own freight forwarder to pick up the casement door shipment FOB?
What is the estimated ocean freight transit time for a shutter shipment from China to Europe?
How can we source replacement seals for your awing window models in the future?
How are sliding windows typically packaged to prevent glass breakage during ocean transit?
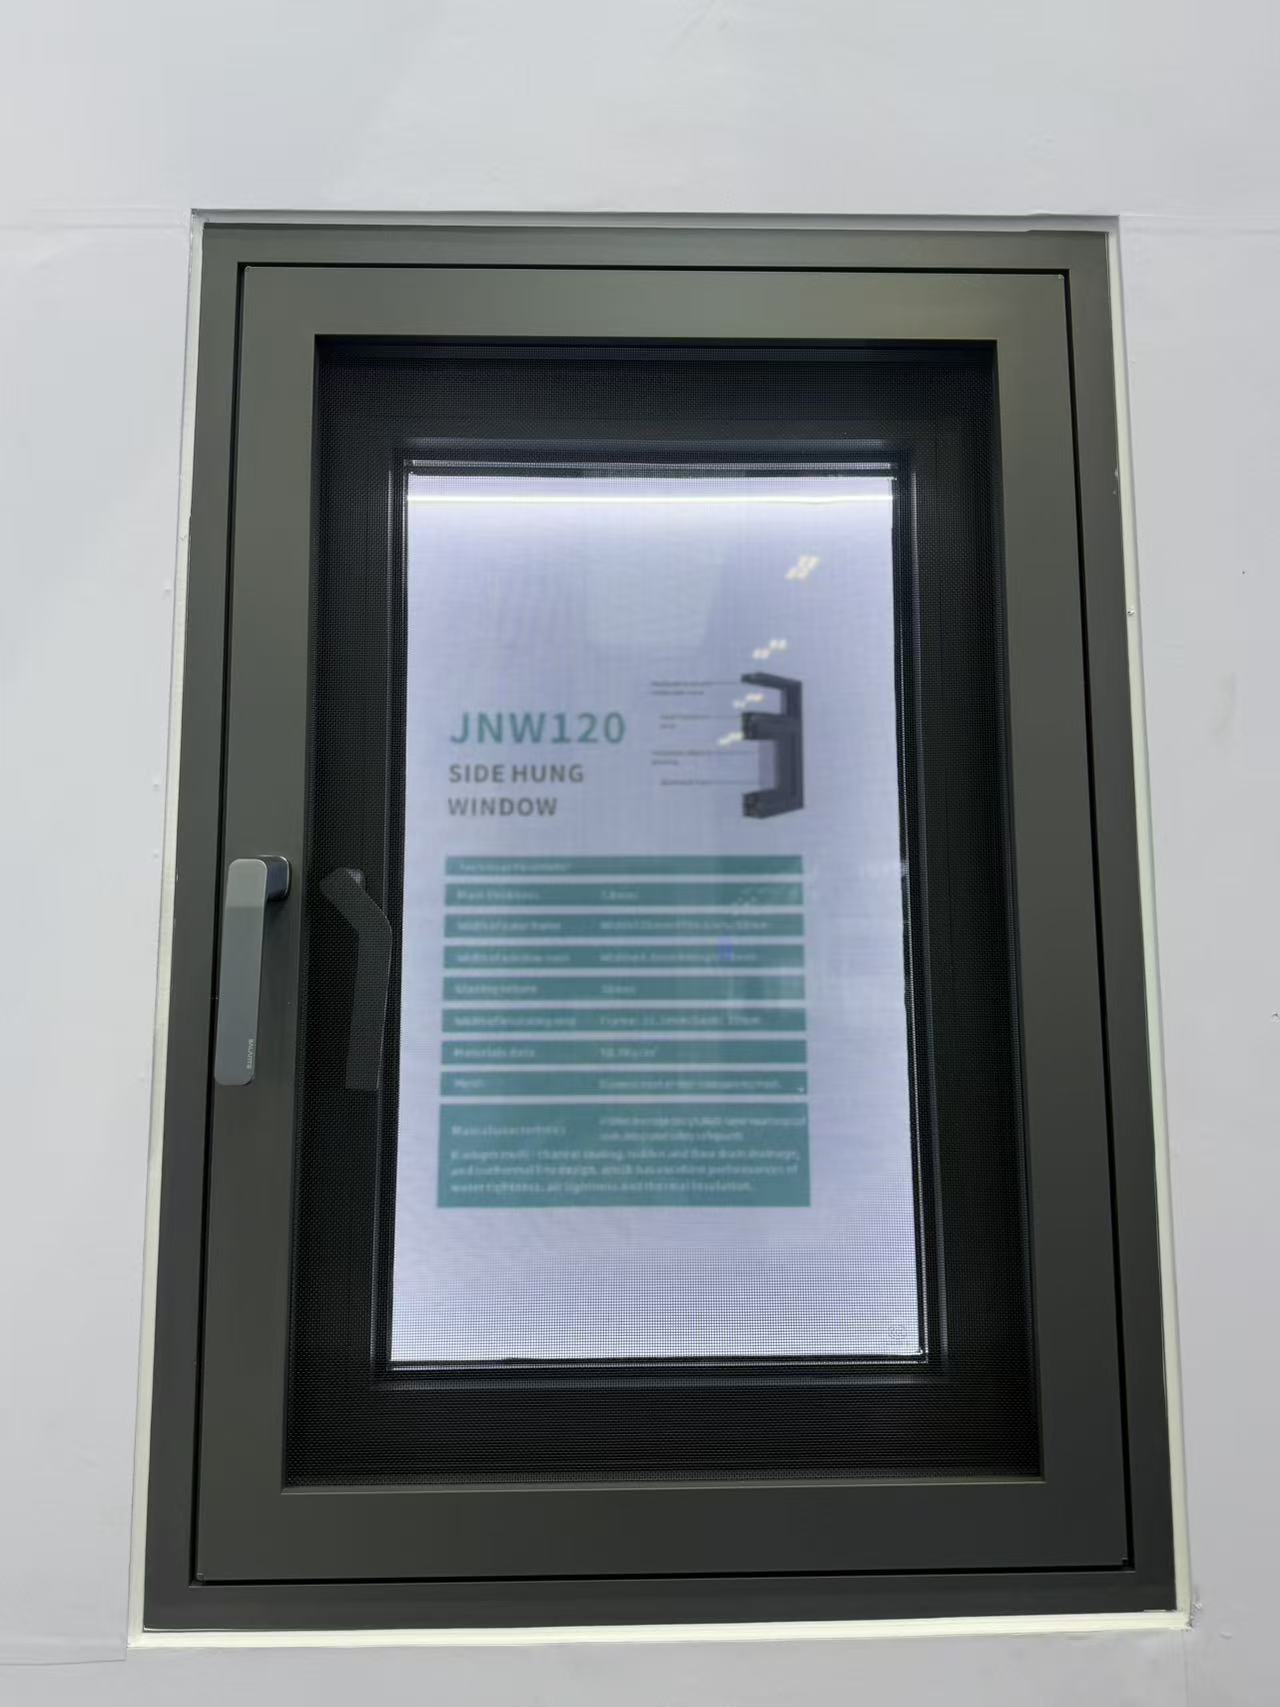
What is the average lead time for a 40ft container of standard aluminum casement windows?
Are there any extra tooling fees if my decorative profile order doesn’t meet the MOQ?
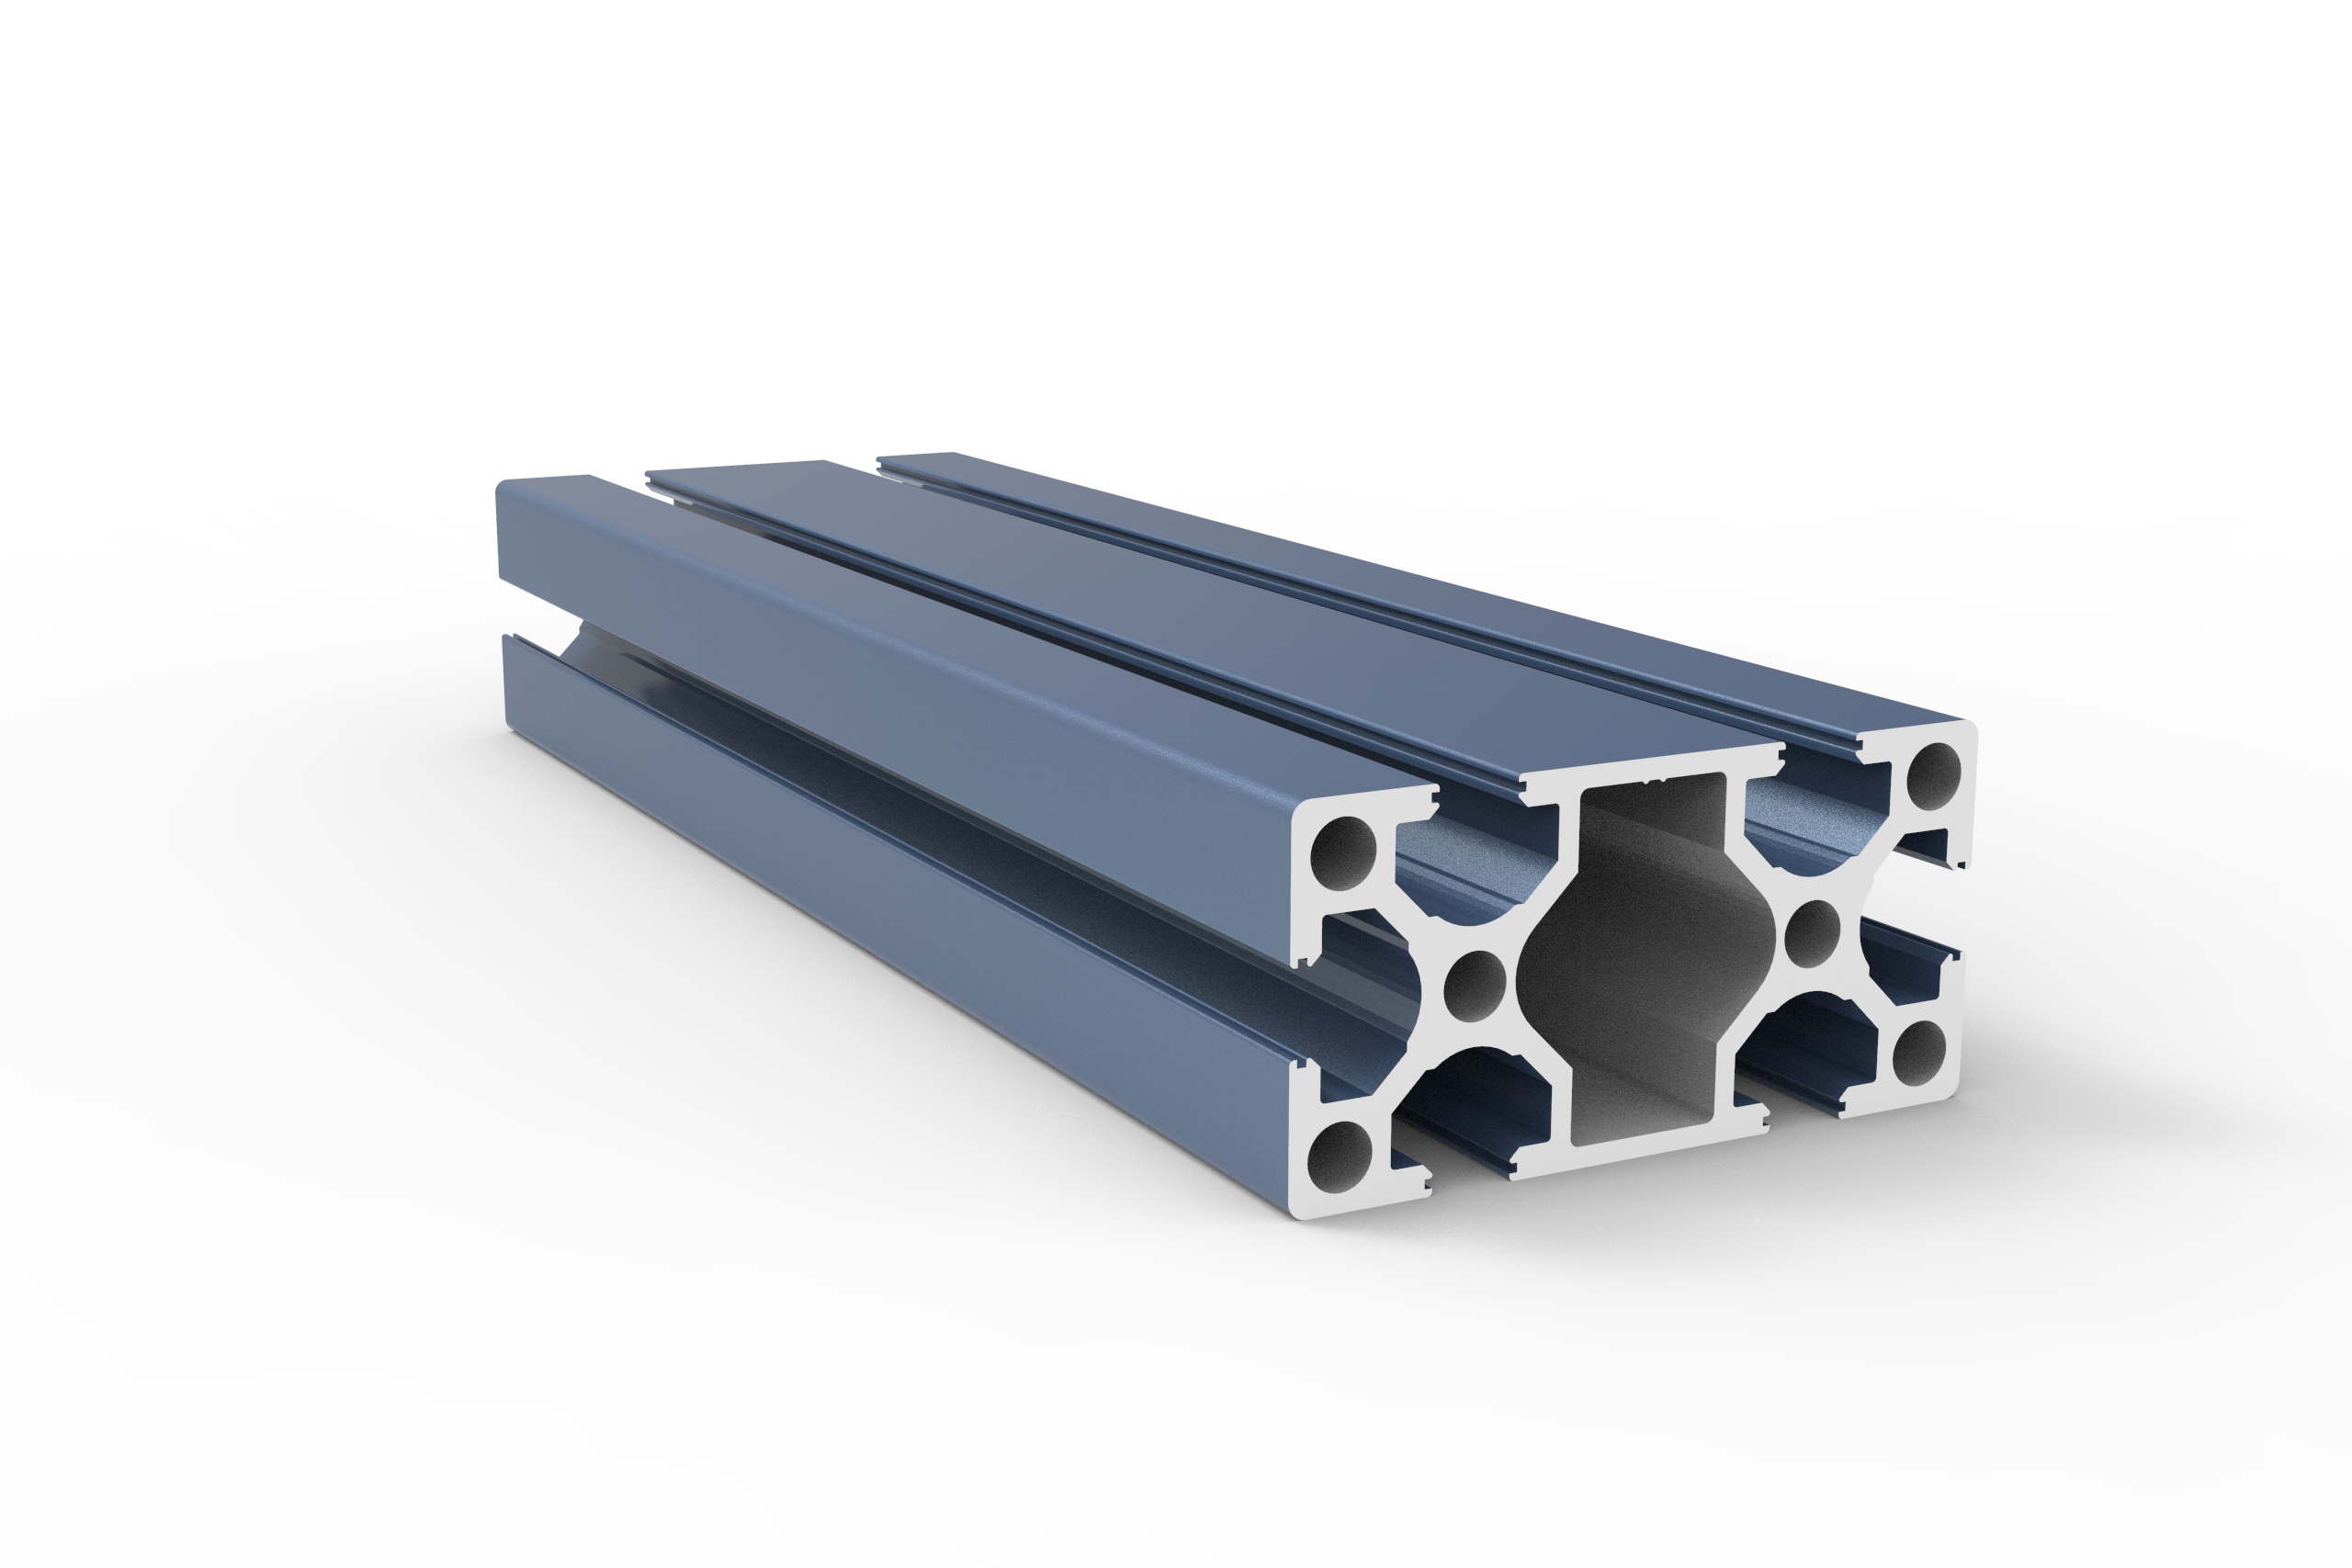
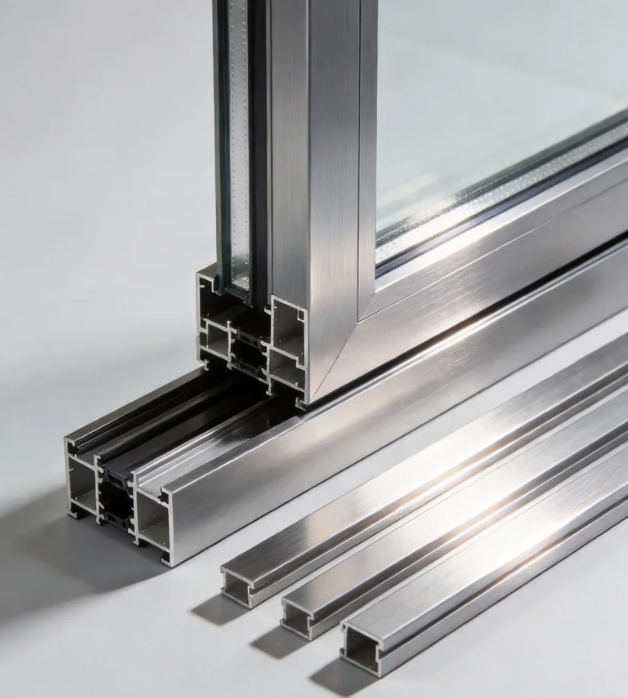
Can I get 3D printed prototypes of custom architecture profiles before committing to mold tooling?
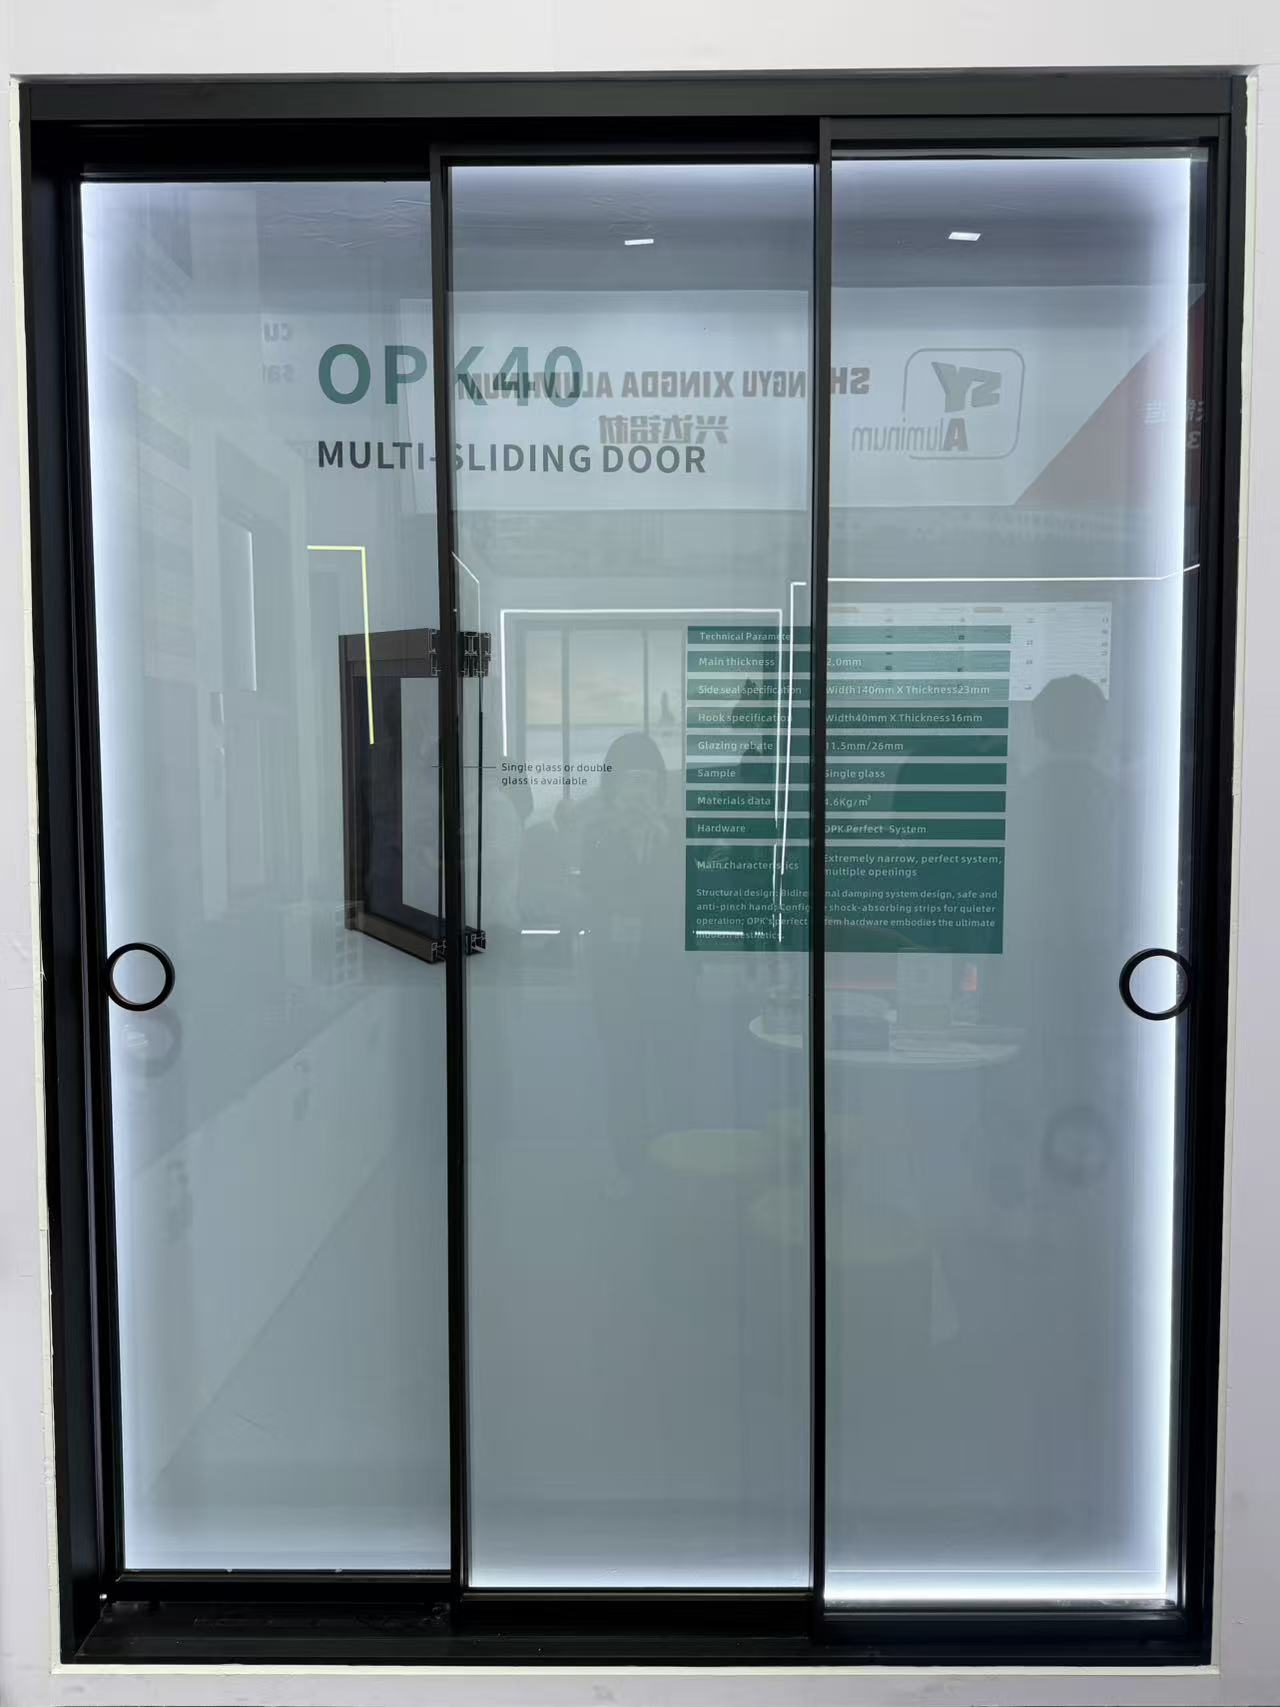
How is smart glass technology being integrated into modern residential sliding door units?
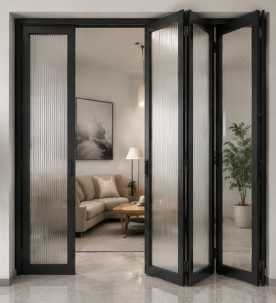
What options do you have for customizing the threshold height of an aluminum floding door?
What thermal break technology should I look for in a heavy-duty aluminum casement door?
What quality control processes do you perform on shutter hardware before final assembly?
Do you offer DDP shipping terms for awing window orders delivered to our warehouse?
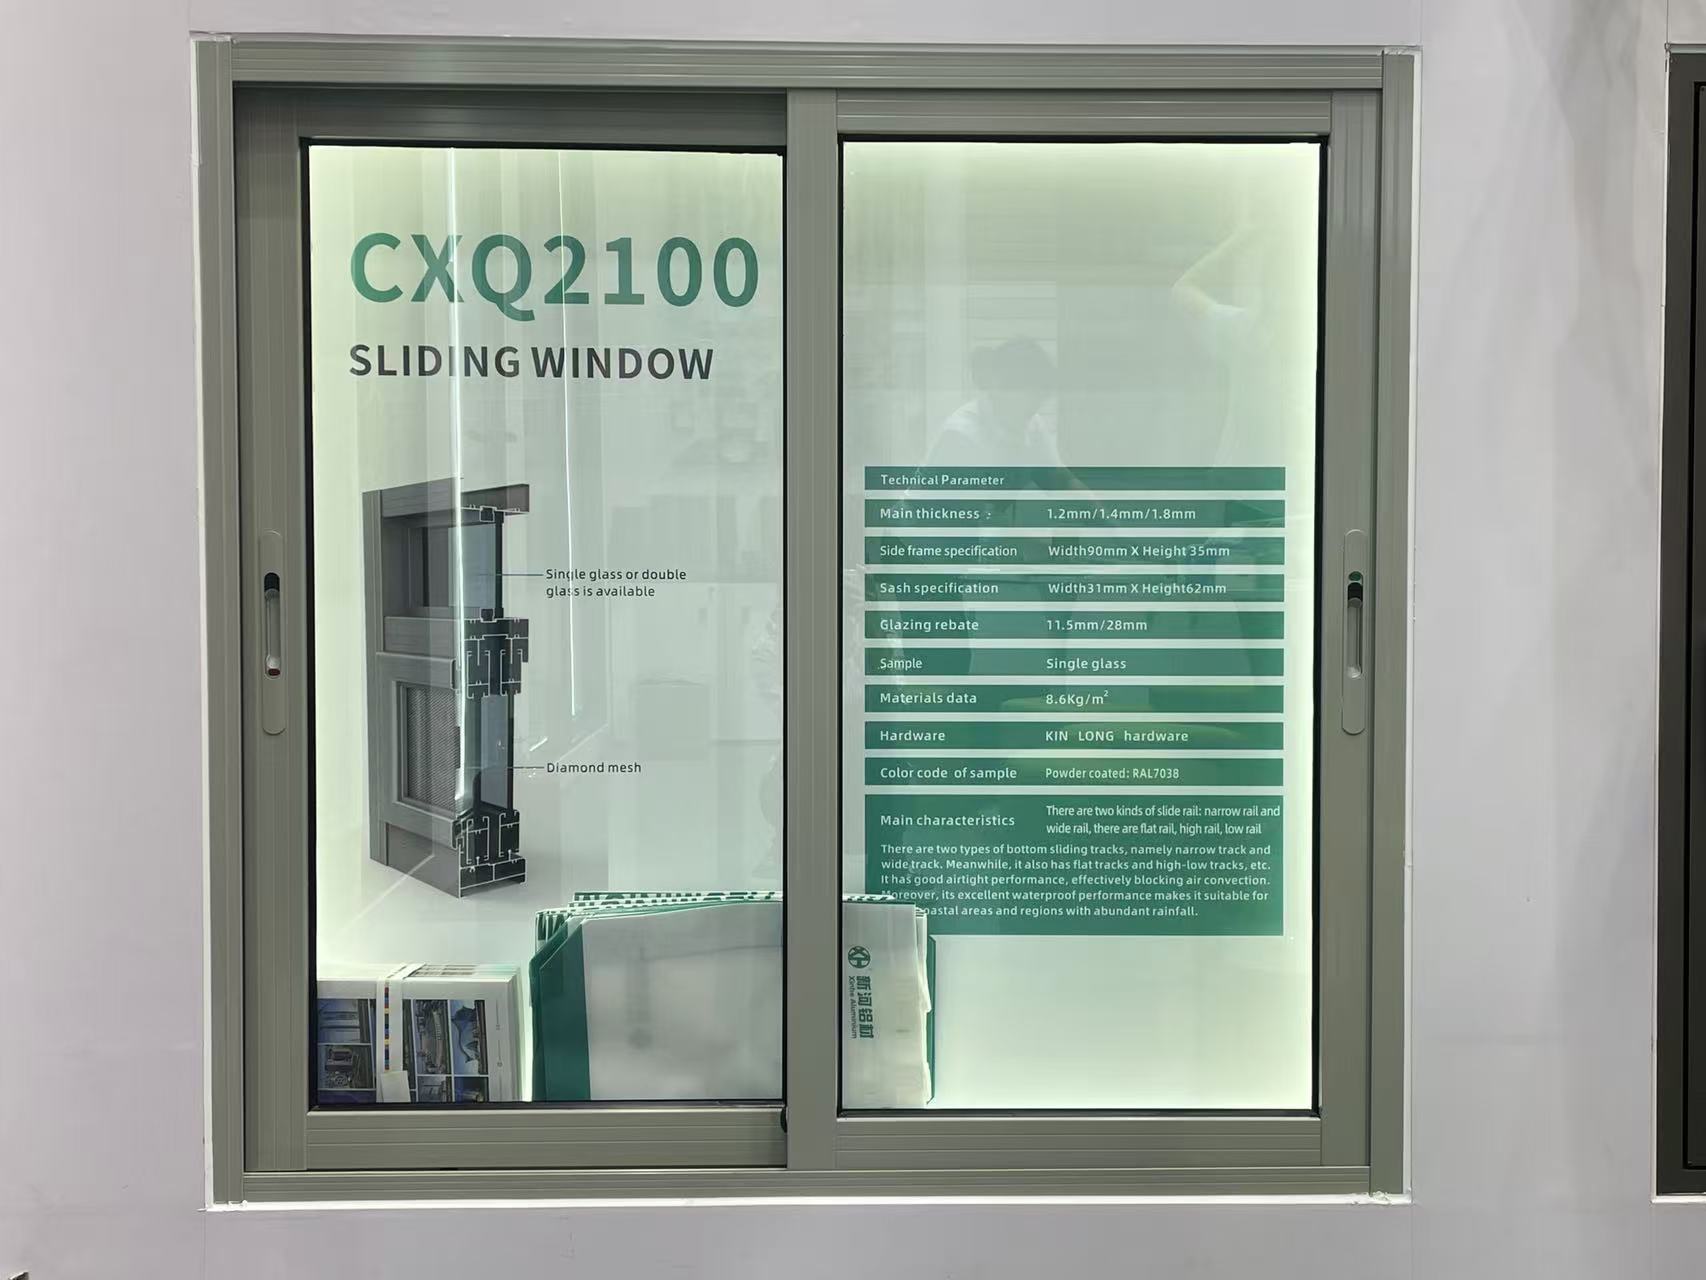
Is it possible to order a fully functional sliding window sample for mock-up testing?
Do you provide replacement hardware if the casement window hinges fail within 5 years?
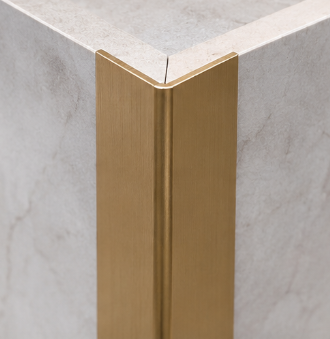
How do you handle claims for decorative profile items damaged during transit?
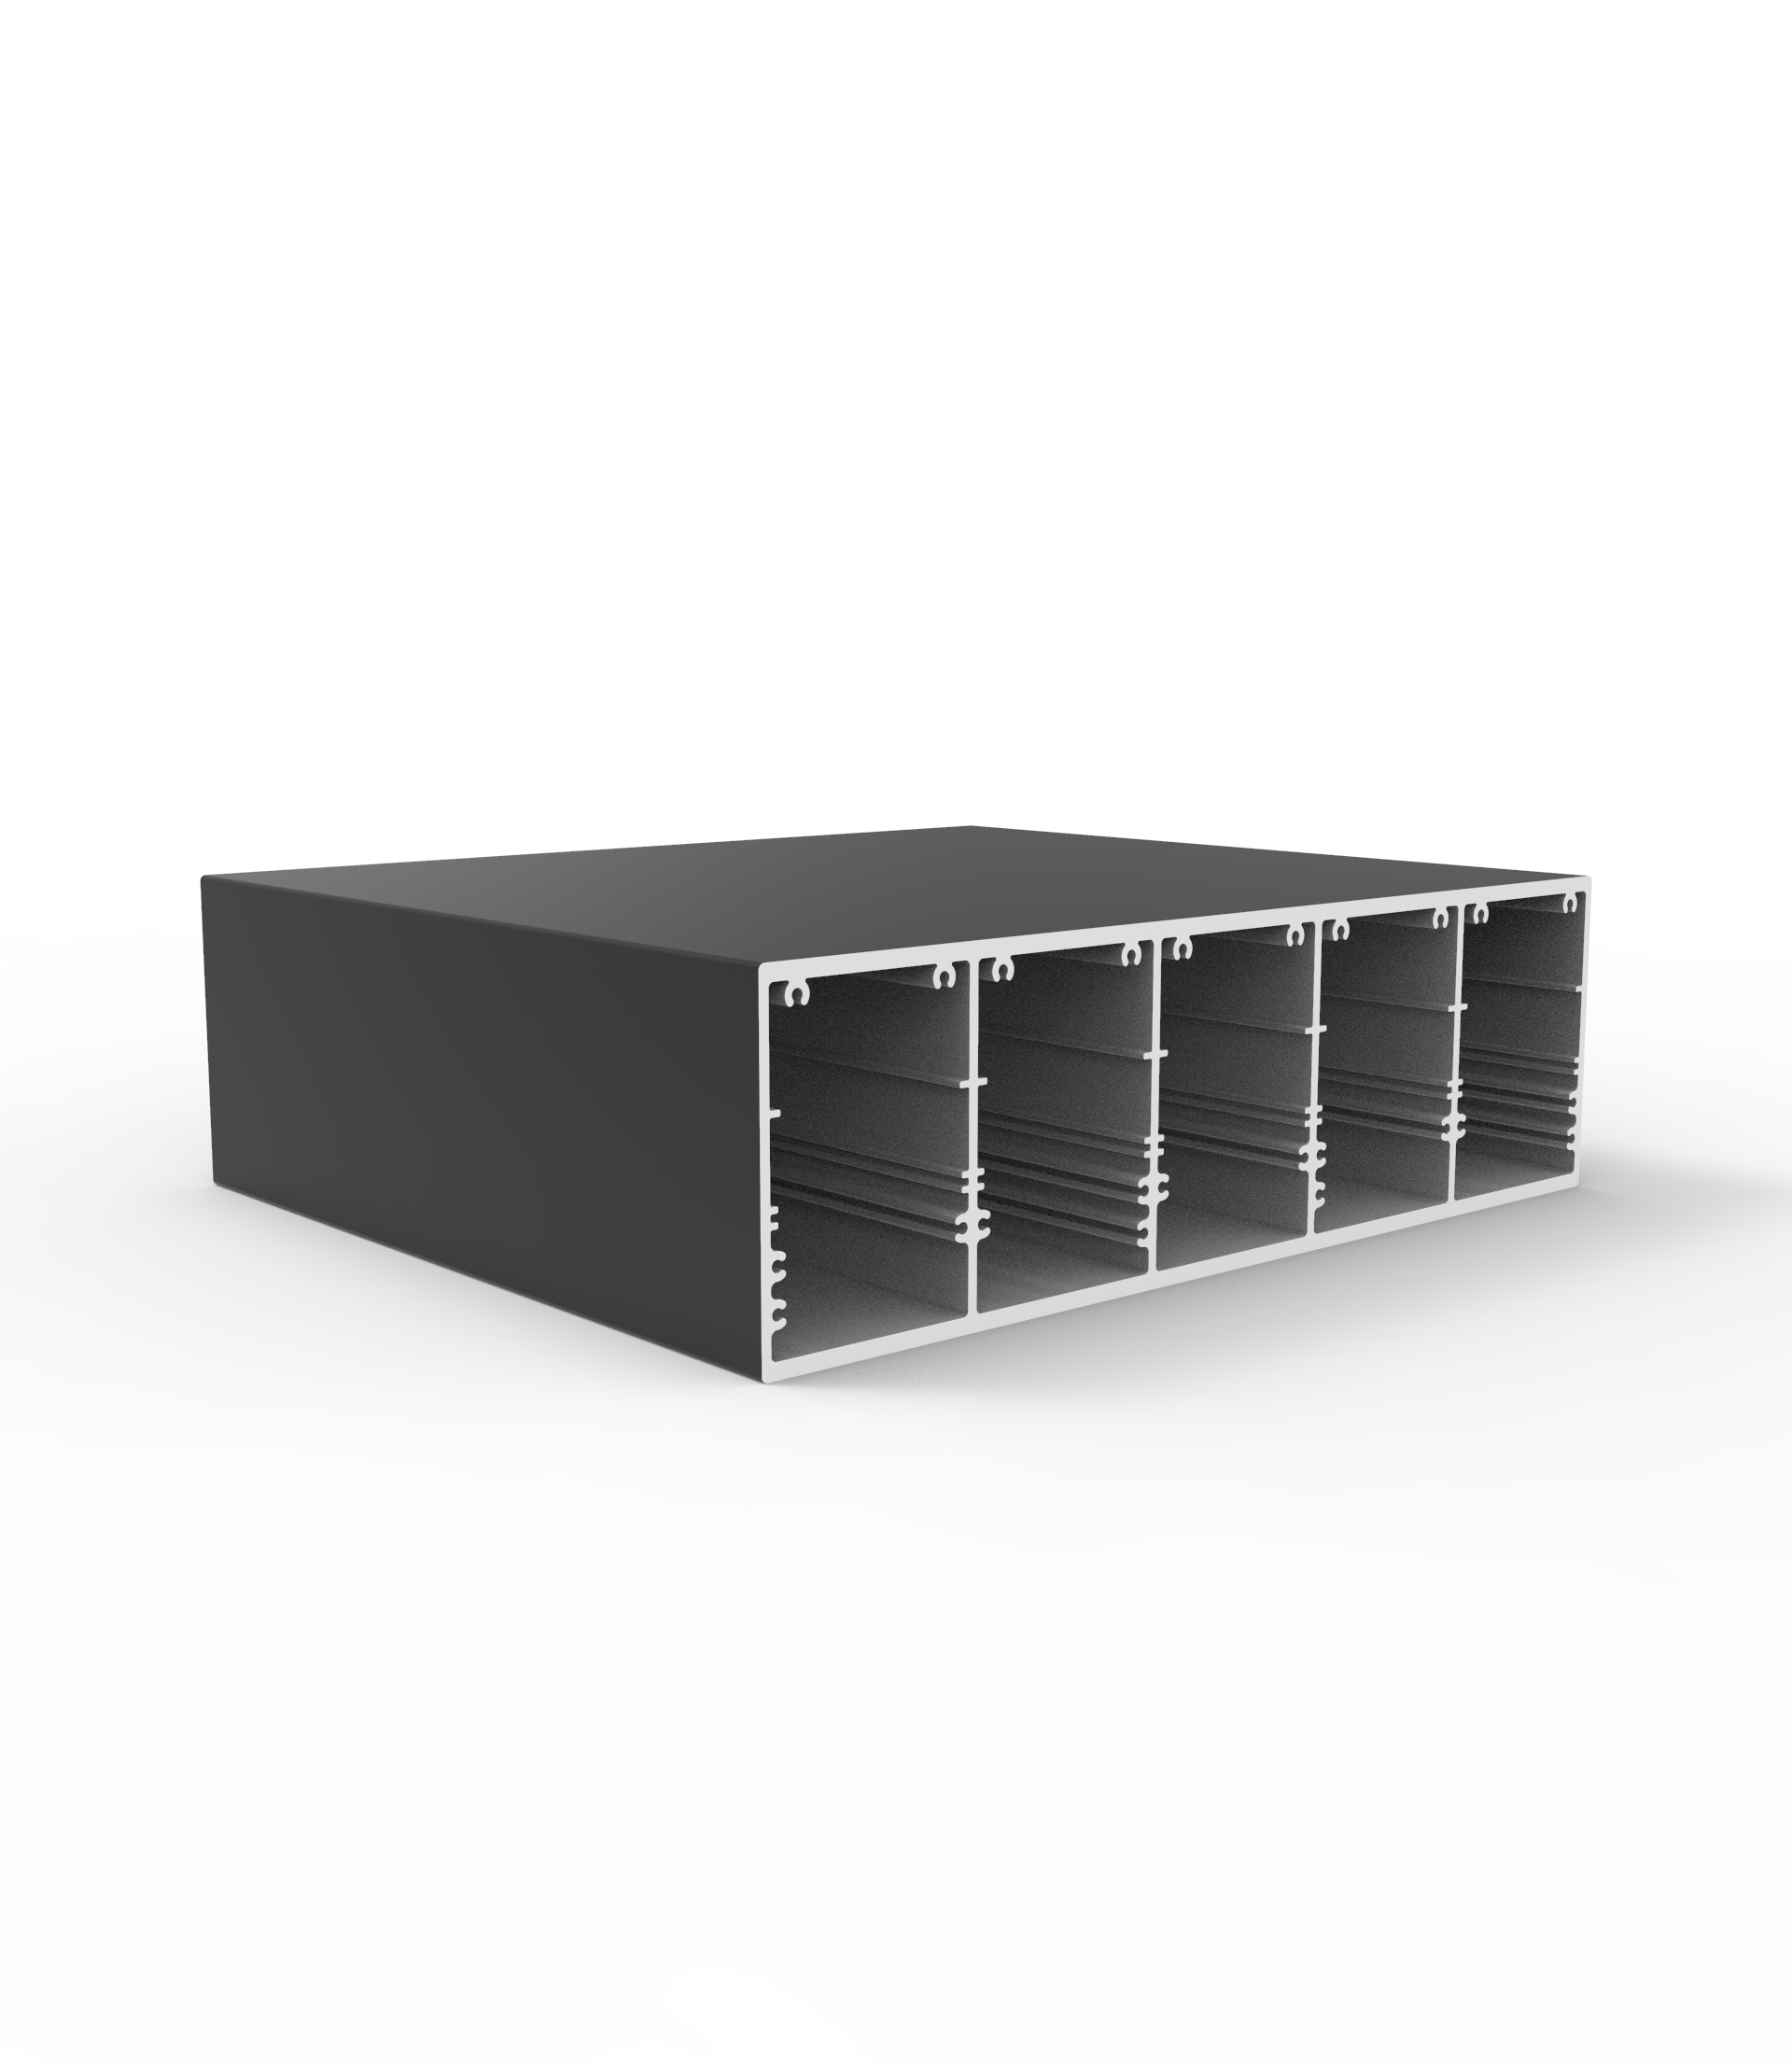
What is the standard MOQ for custom-extruded aluminum industrial profile orders?
How does the order volume affect the per-ton price of custom architecture profile designs?
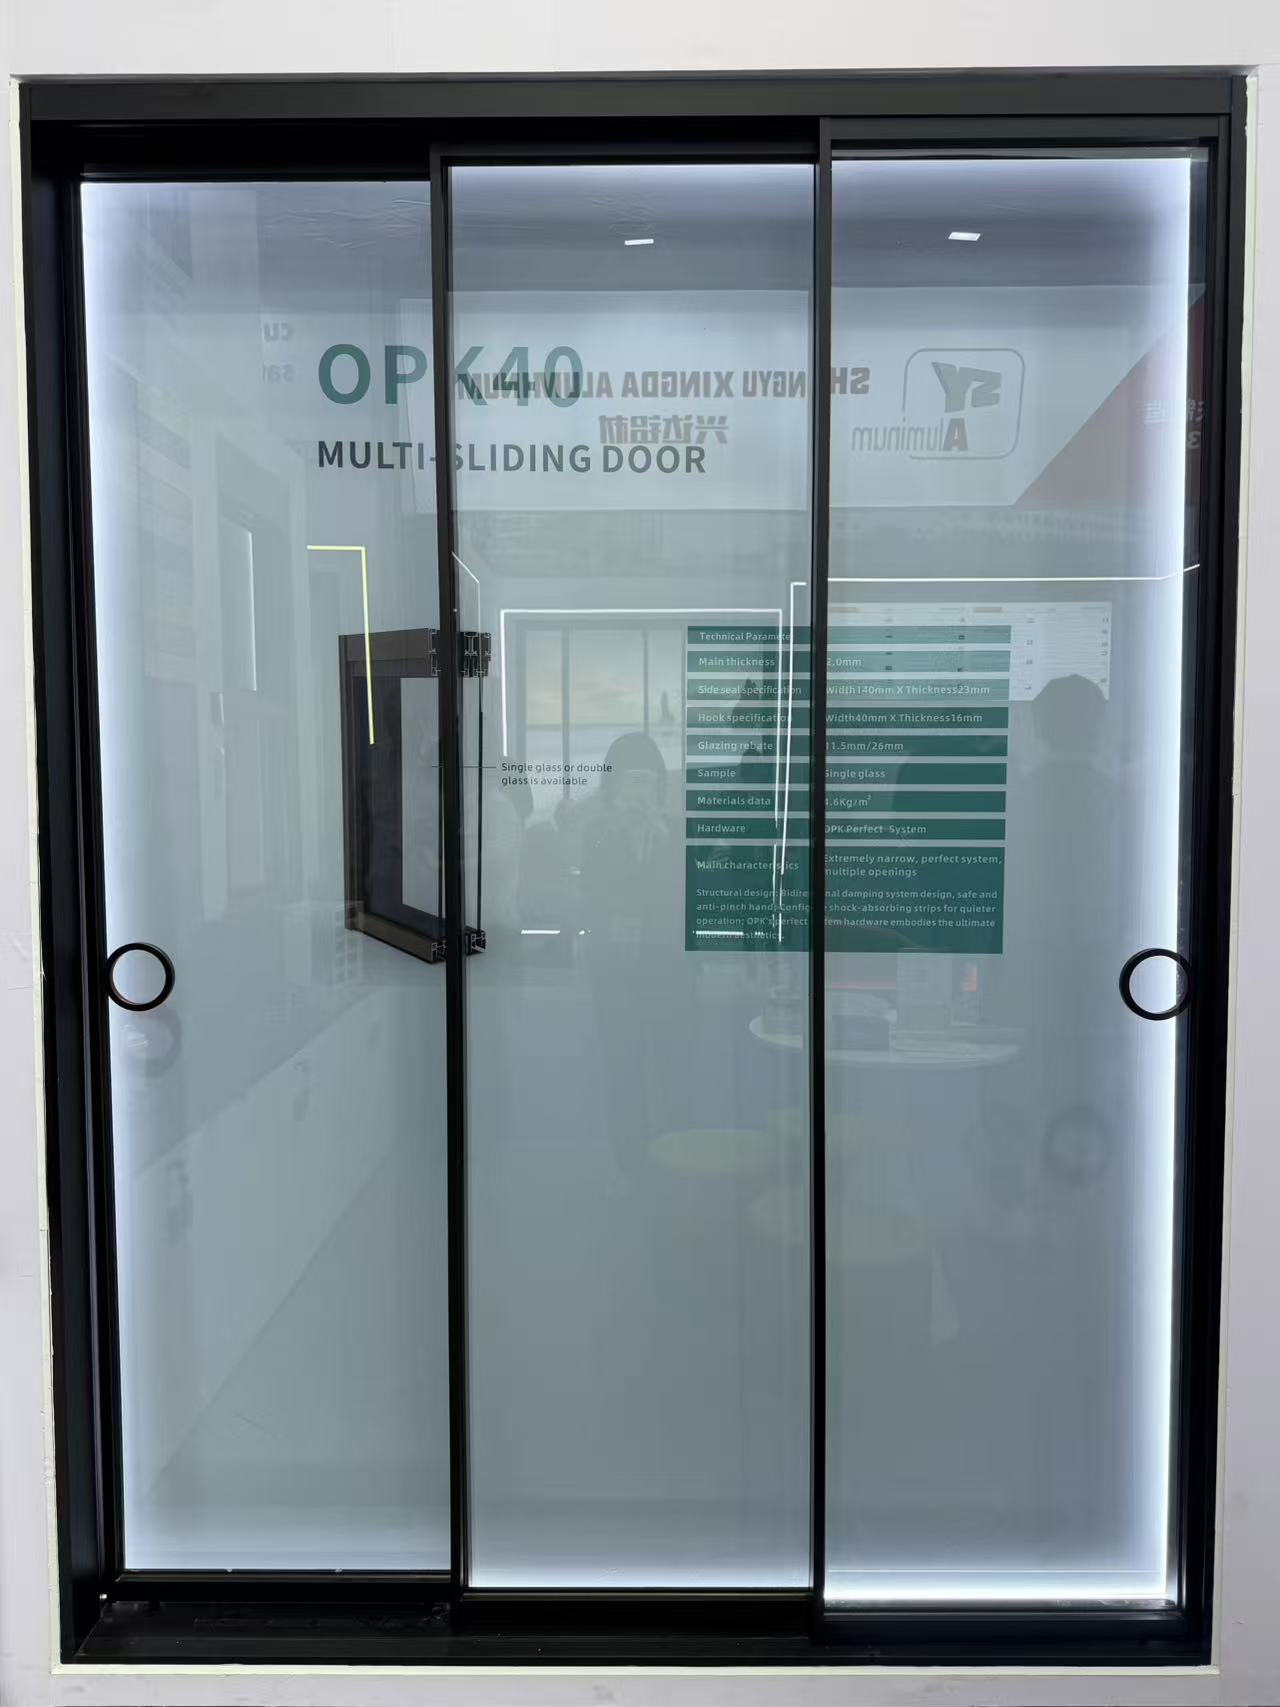
What is the warranty period for the rollers and tracks on your heavy-duty sliding doors?
How can we secure our deposit when purchasing high-value custom floding doors from a new supplier?
Can your factory match custom anodized colors for decorative profiles based on physical samples?
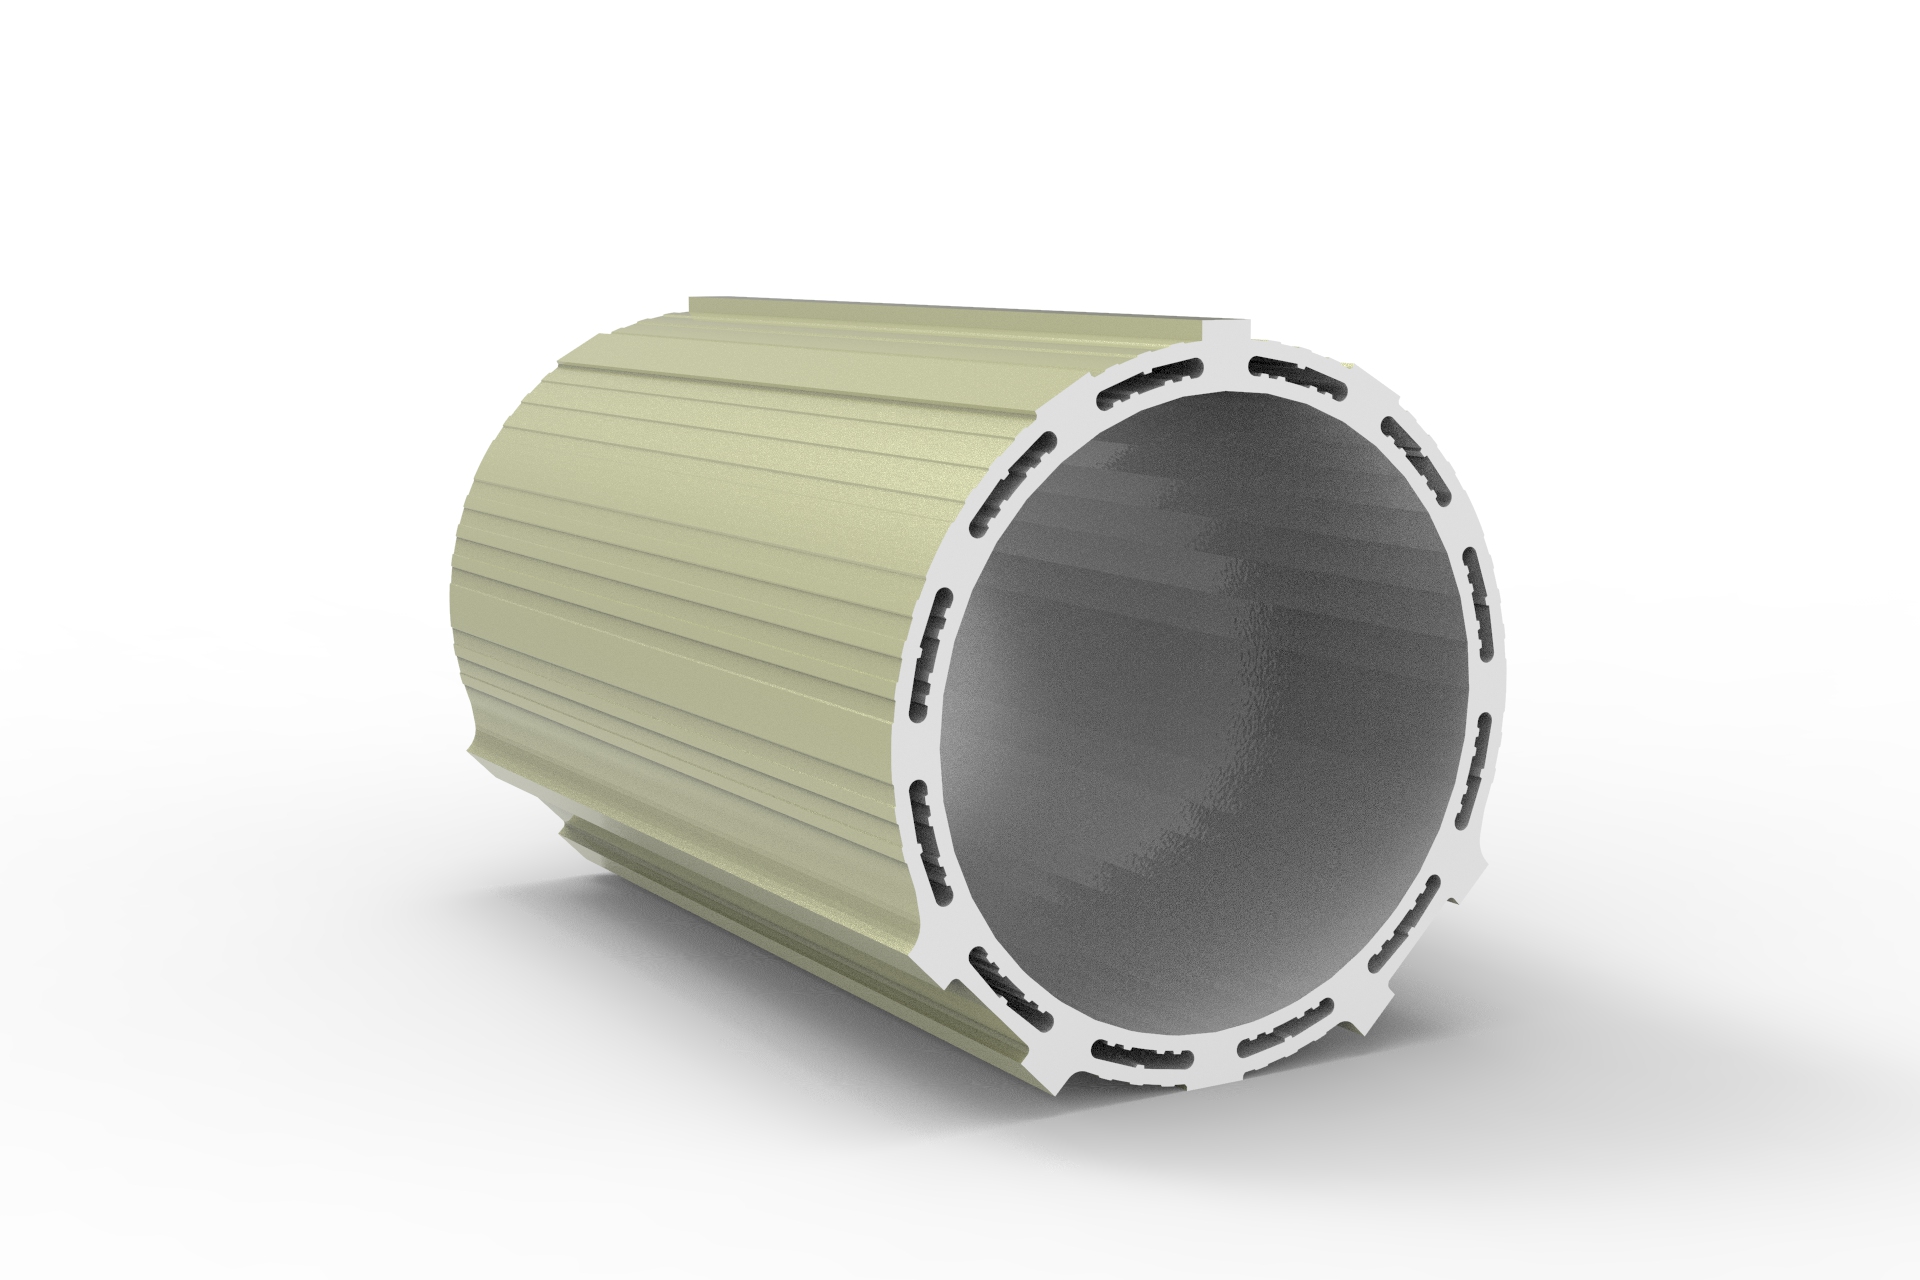
Is there a lighter alternative to aluminum industrial profile structures for robotics?
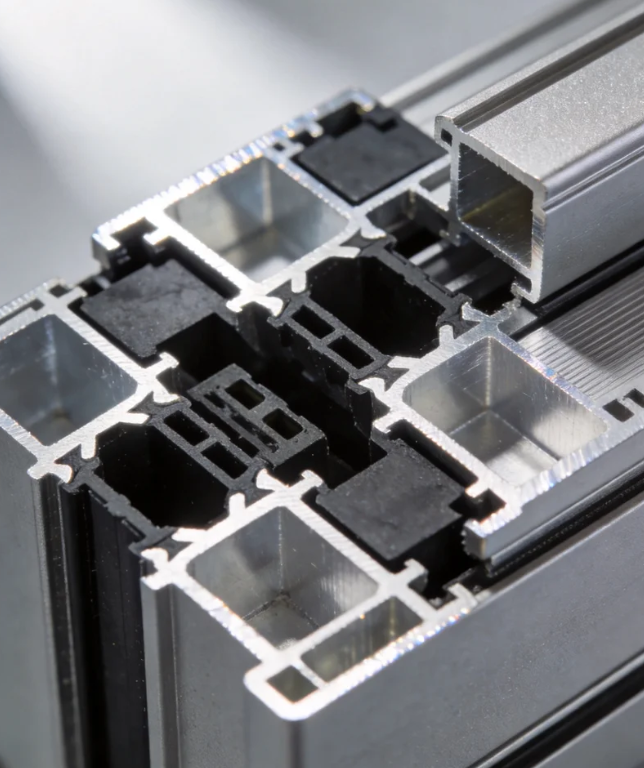
What payment security measures do you have for custom architecture profile tooling fees?
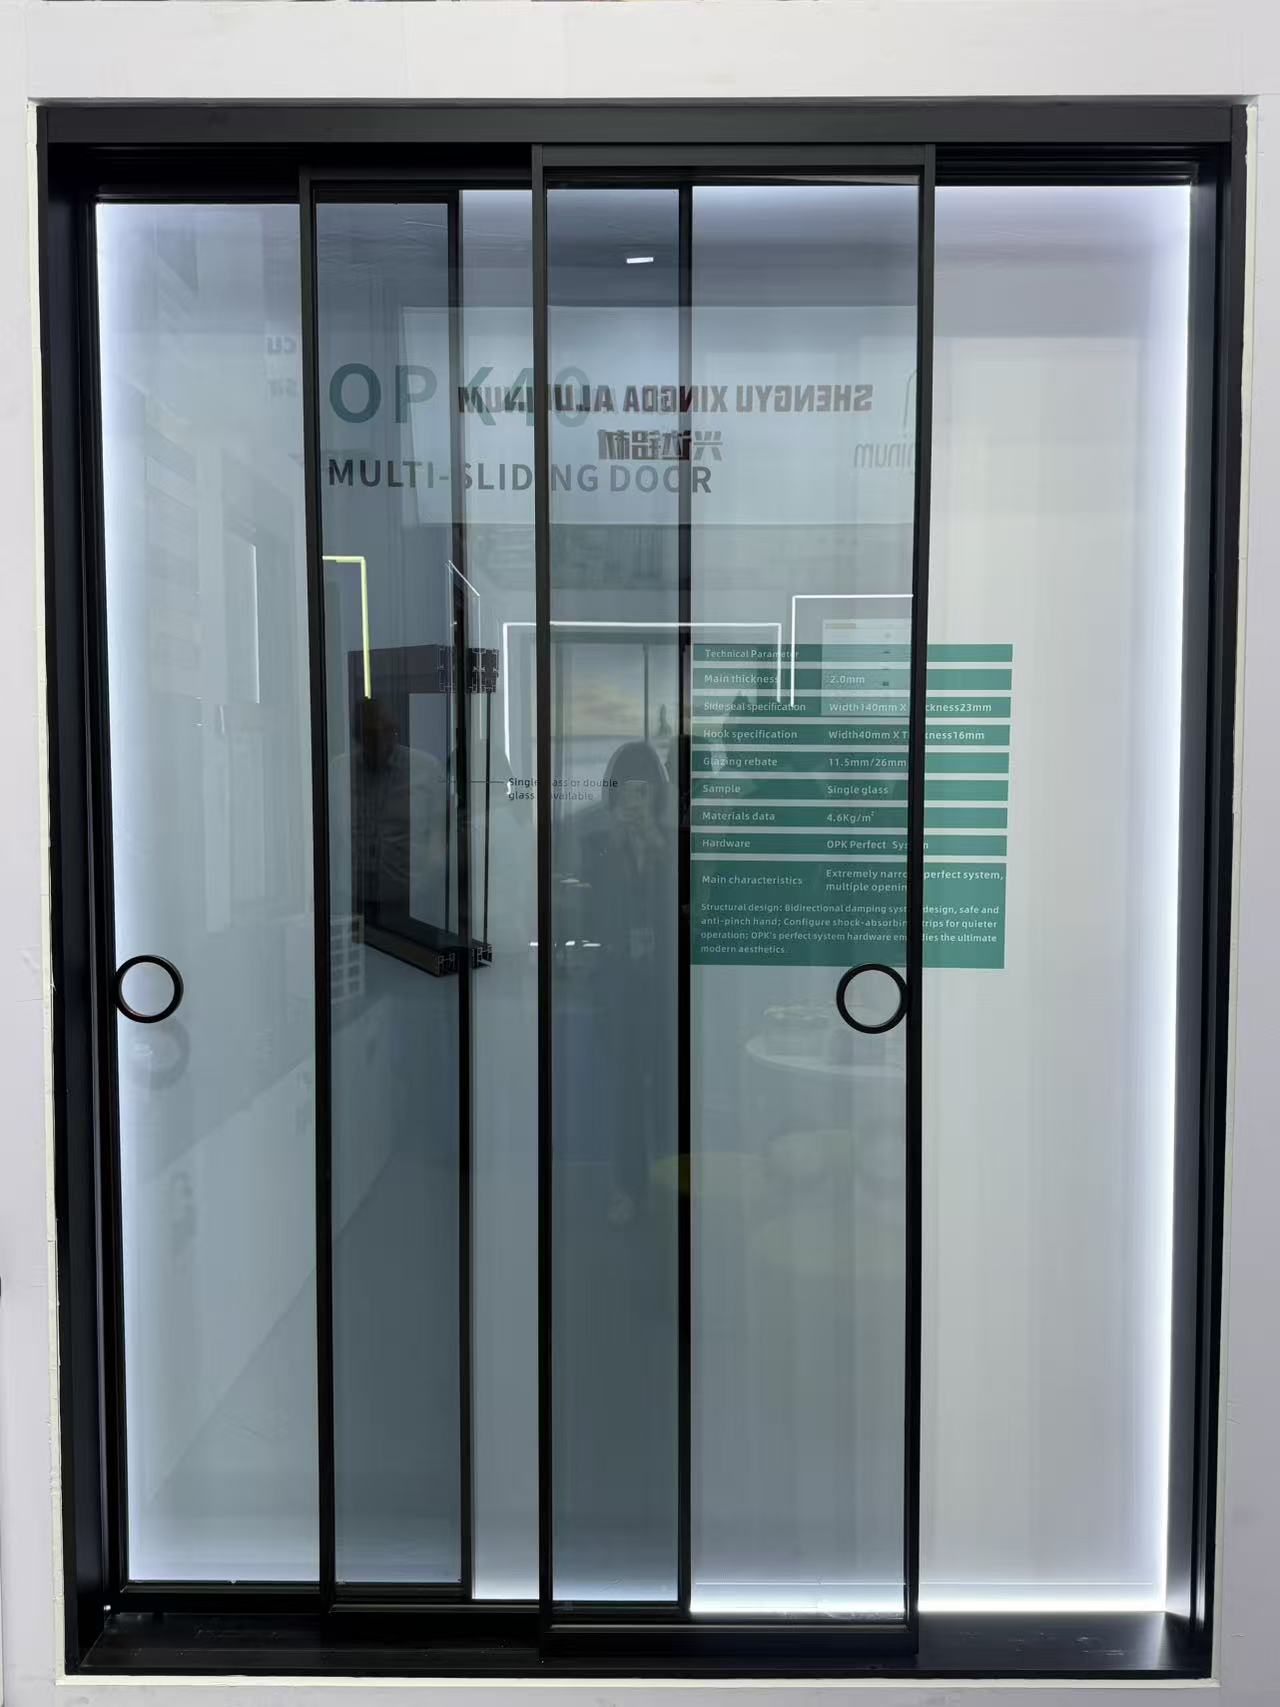
Can I order a sliding door with custom grid patterns between the glass panes?
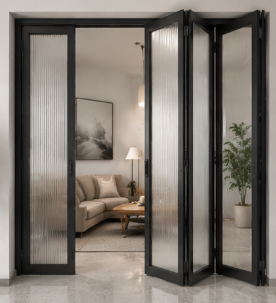
How do you protect buyers against financial loss if the floding door shipment is delayed?
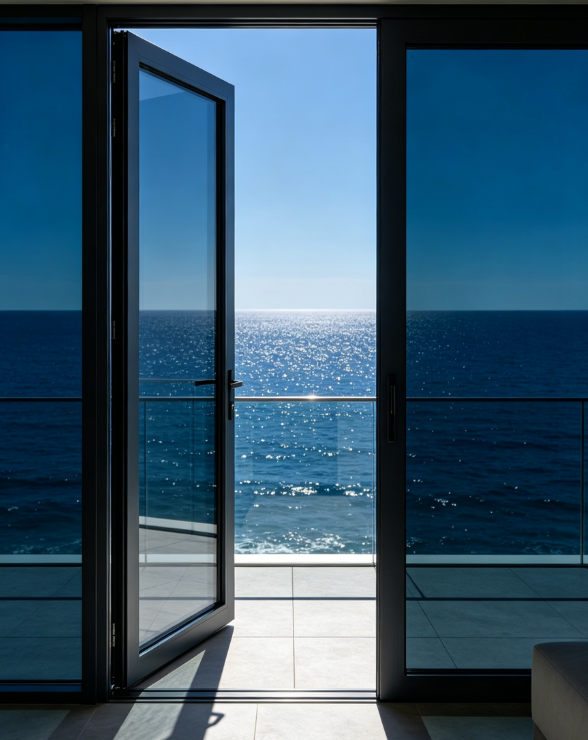
Are slim-frame aluminum casement door designs becoming more popular in modern offices?
What is your policy for replacing shutter components that arrive with color mismatch?
What kind of remote technical support do you offer for sliding window installation?
What is the maximum safe size for a top-hung awing window in commercial projects?
What environmental management standards does your decorative profile plant follow?
What is the standard lead time for producing a 40ft container of casement window orders?
What is the warranty period for the anodized finish on your industrial profile?
What are the latest eco-friendly trends in architecture profile manufacturing?
What is the average wholesale price per square meter for double-glazed sliding door systems?
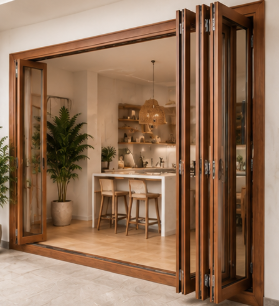
How do I calculate the structural load requirement for a 5-panel exterior floding door?
Do your exterior shutter systems comply with Florida building codes for hurricane protection?
Do you offer Letter of Credit (L/C) payment options for casement door bulk orders?
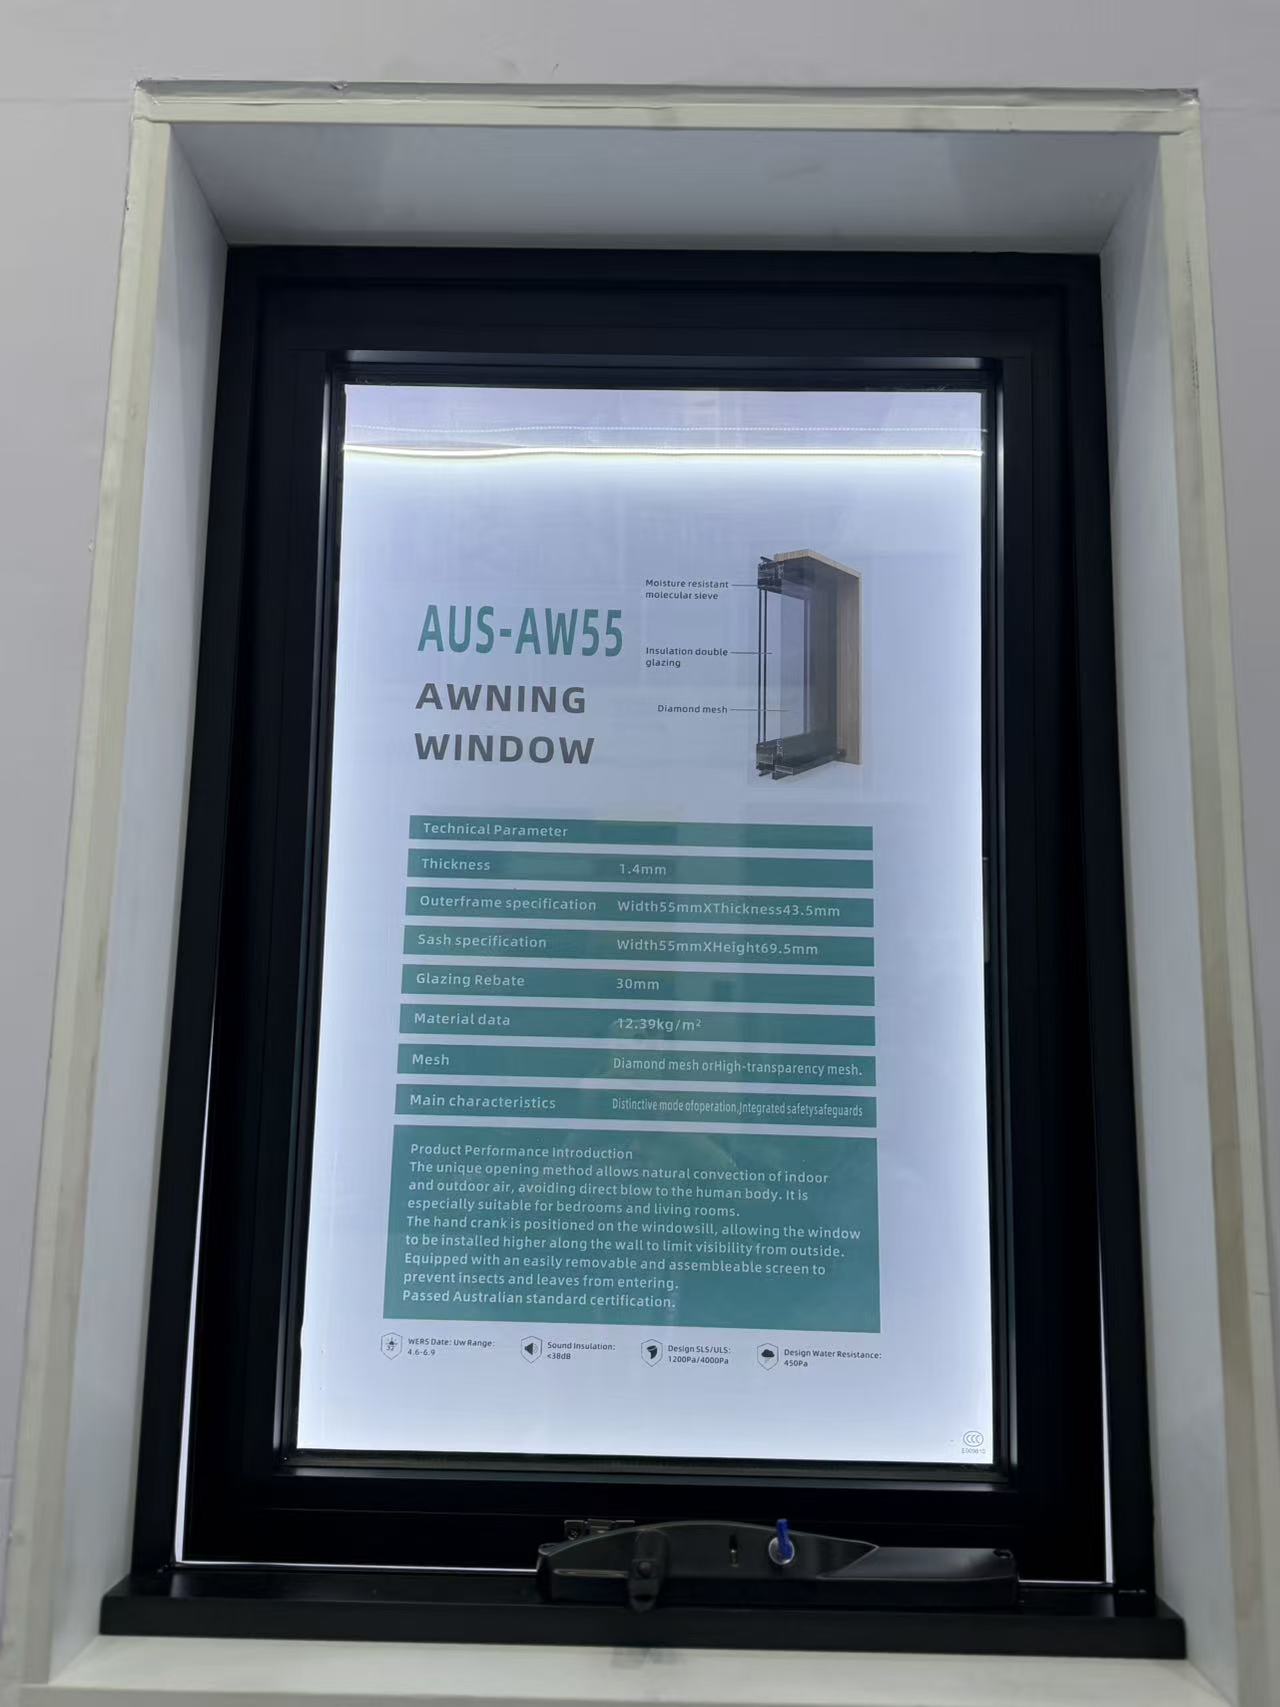
Which water tightness certifications are required for importing an awing window to Europe?
Do you allow virtual factory tours to inspect the sliding window assembly line?
What is the typical MOQ for ordering standard-sized aluminum casement window units?
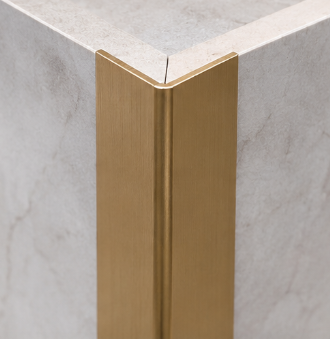
How long does it take to receive a physical sample of a gold-anodized decorative profile?
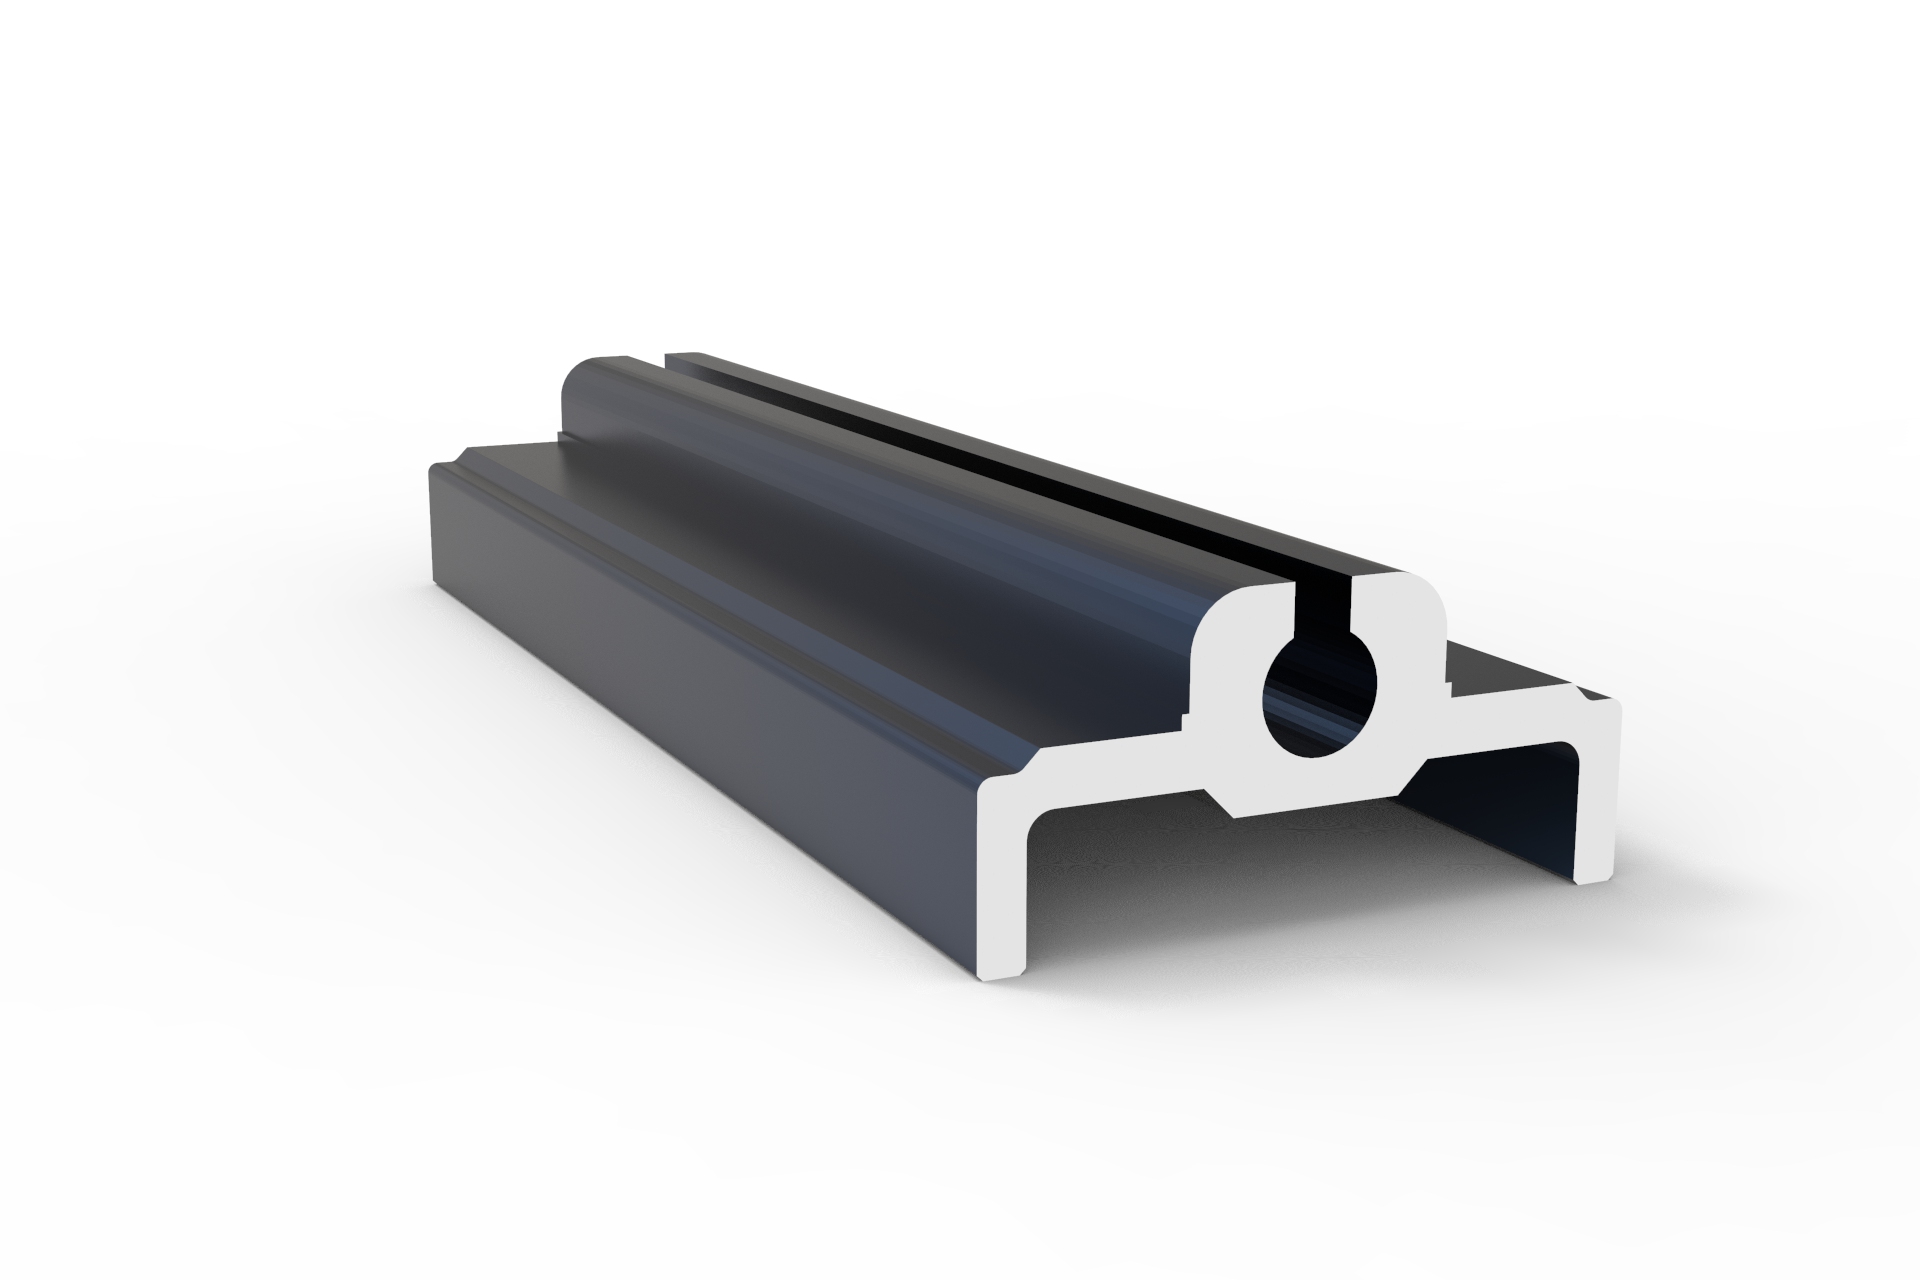
How do I choose the right alloy grade for architecture profiles in high-rise coastal buildings?
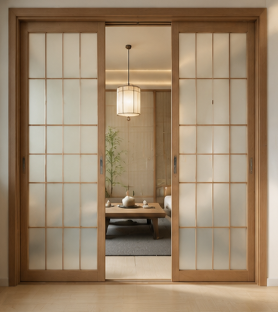
How do I choose the right track and roller specs for heavy-duty commercial sliding doors?
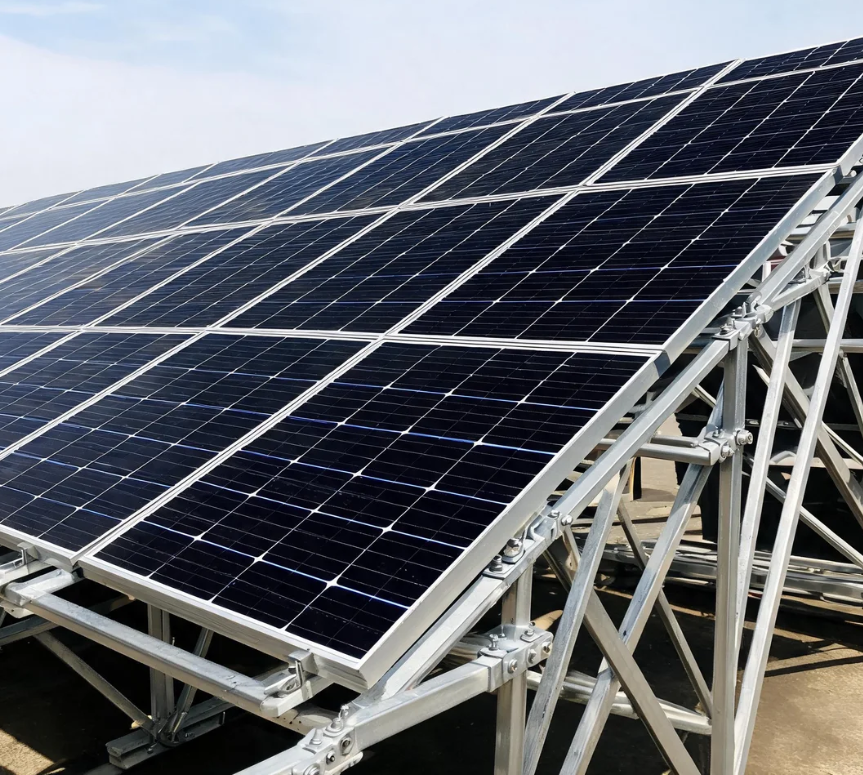
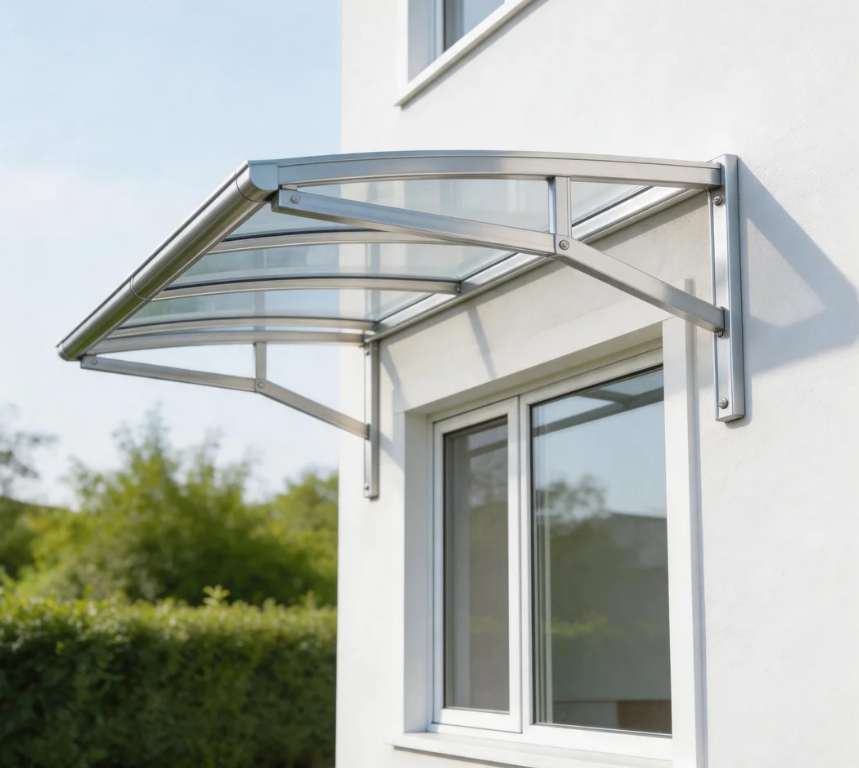
The core advantages of using aluminium profiles for the canopy
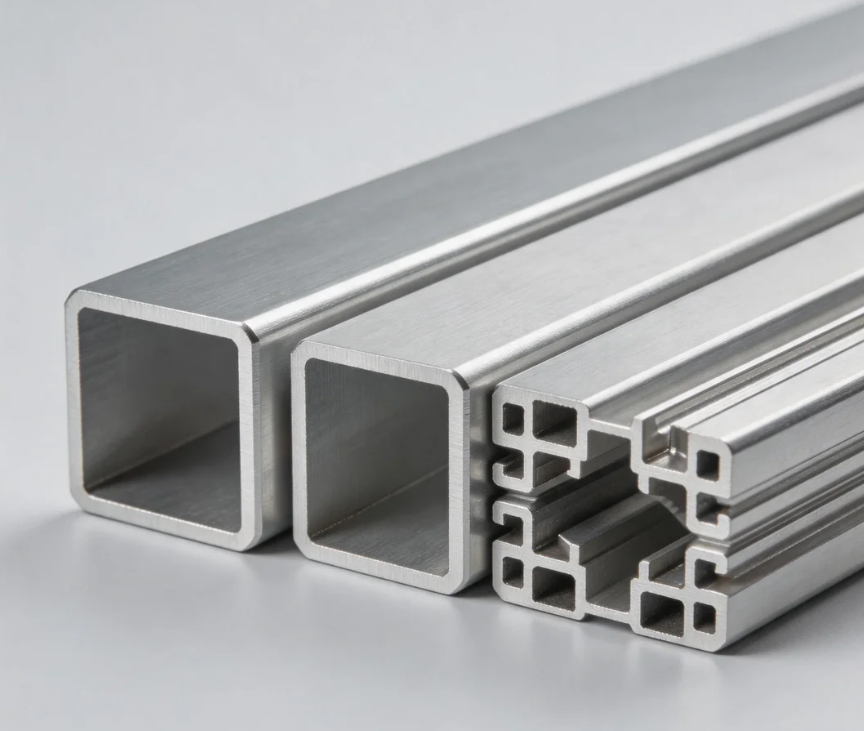
International demand: Dual drive by new energy and infrastructure
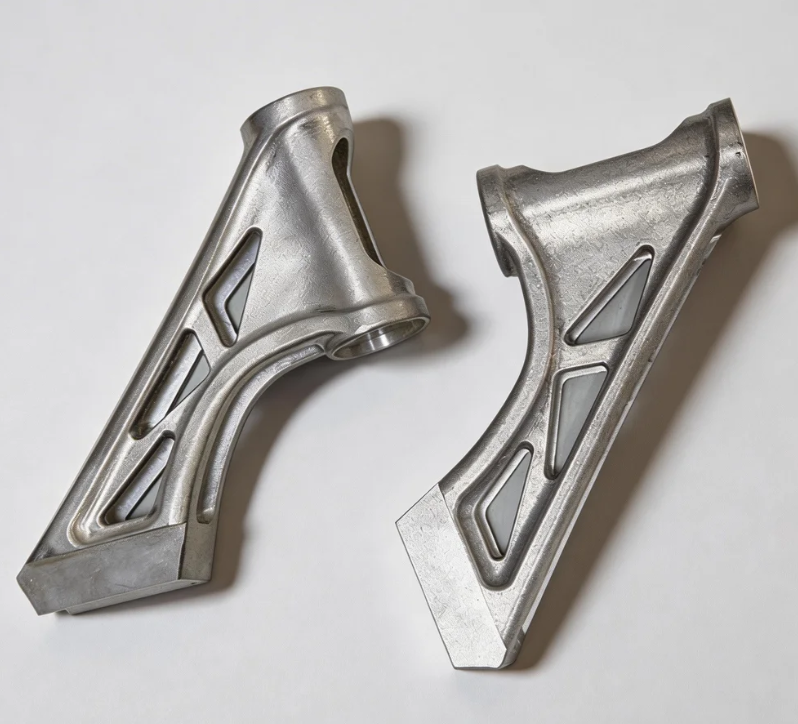
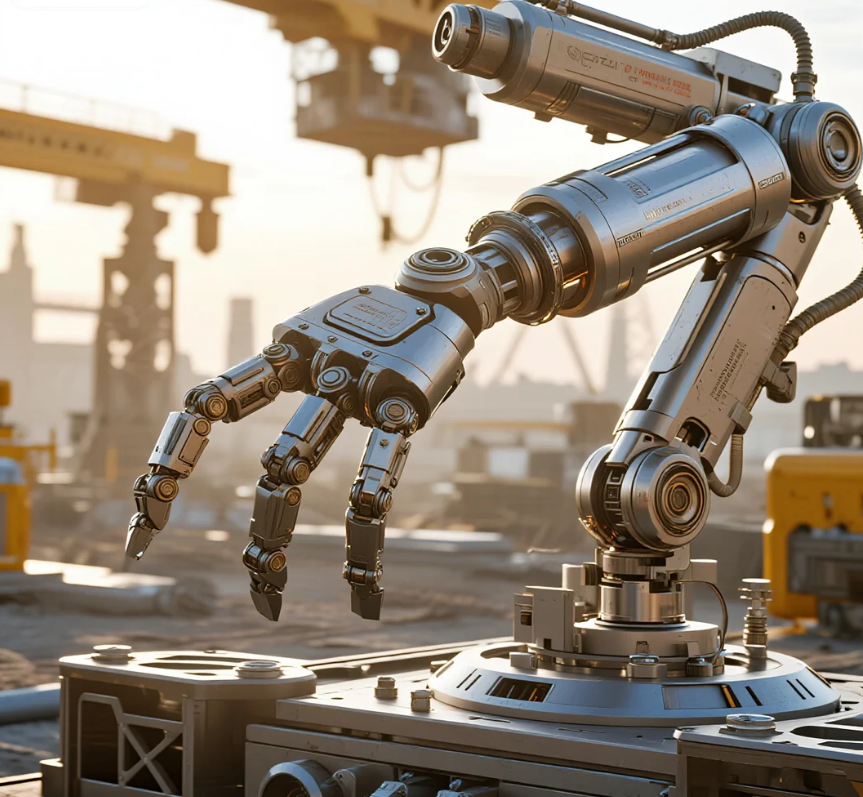
The advantages of using aluminium profiles to manufacture robot arms
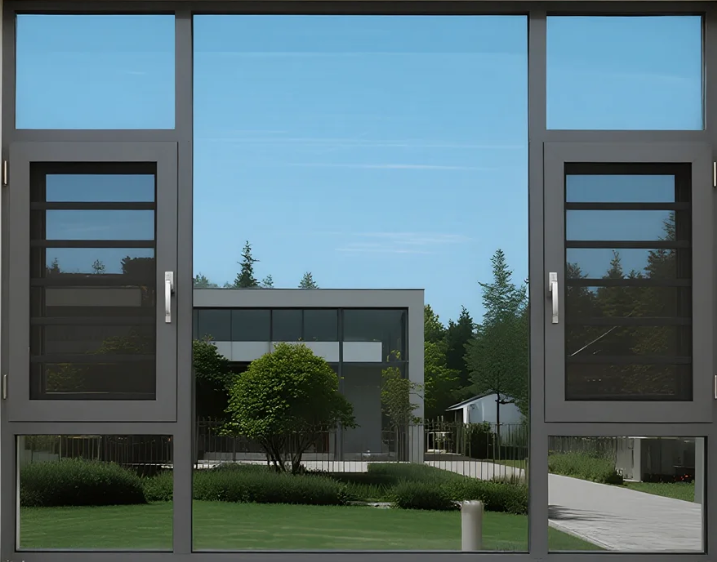
The advantages of using aluminum profiles for door and window frames
The impact of the conflict between the United States and Iran on the price of aluminum
The advantages of using aluminium alloy for the main structure of high-speed train carriages
Methods for distinguishing Indoor and Outdoor Aluminium Doors
Maintenance methods and tips for aluminium doors and windows
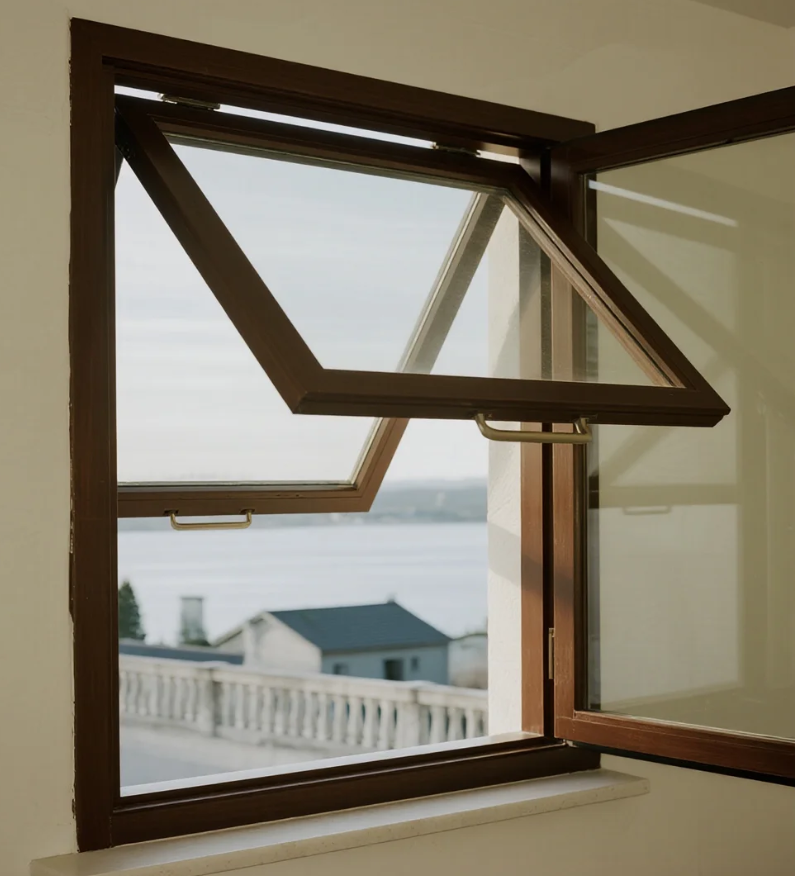
Characteristic of outward-opening and hung aluminium windows
Xinhe Aluminium Research: 7.14-7.18 Analysis of Aluminium Prices
Seven Benefits Of Using Aluminium Profiles In Curtain Wall Systems
The Application of Aluminium Profiles in New Energy Vehicles
The Composition and Application of Series 6 Aluminium Alloys
Top 5 Benefits of Using LED Aluminium Profiles in Modern Lighting
A Complete Guide to Aluminium Frame Profiles for Modern Structures
Exploring the Strength and Versatility of Aluminium Extrusion Profiles
How to Choose the Right Aluminium Profile Supplier for Your Project
COMPANY