Structural vulnerability almost always begins at the edges. Whether dealing with a towering glass facade or a residential tiled corner, sharp intersections face concentrated mechanical stress. Architects and engineers consistently turn to specific geometries to mitigate this vulnerability. Among these solutions, architectural aluminium profiles stand out as a foundational element.
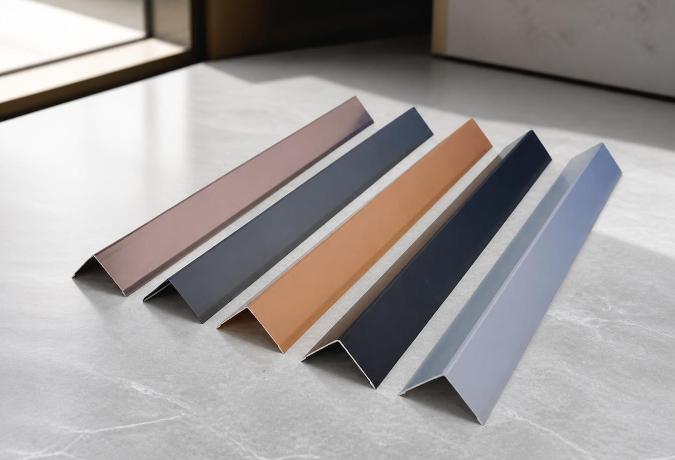
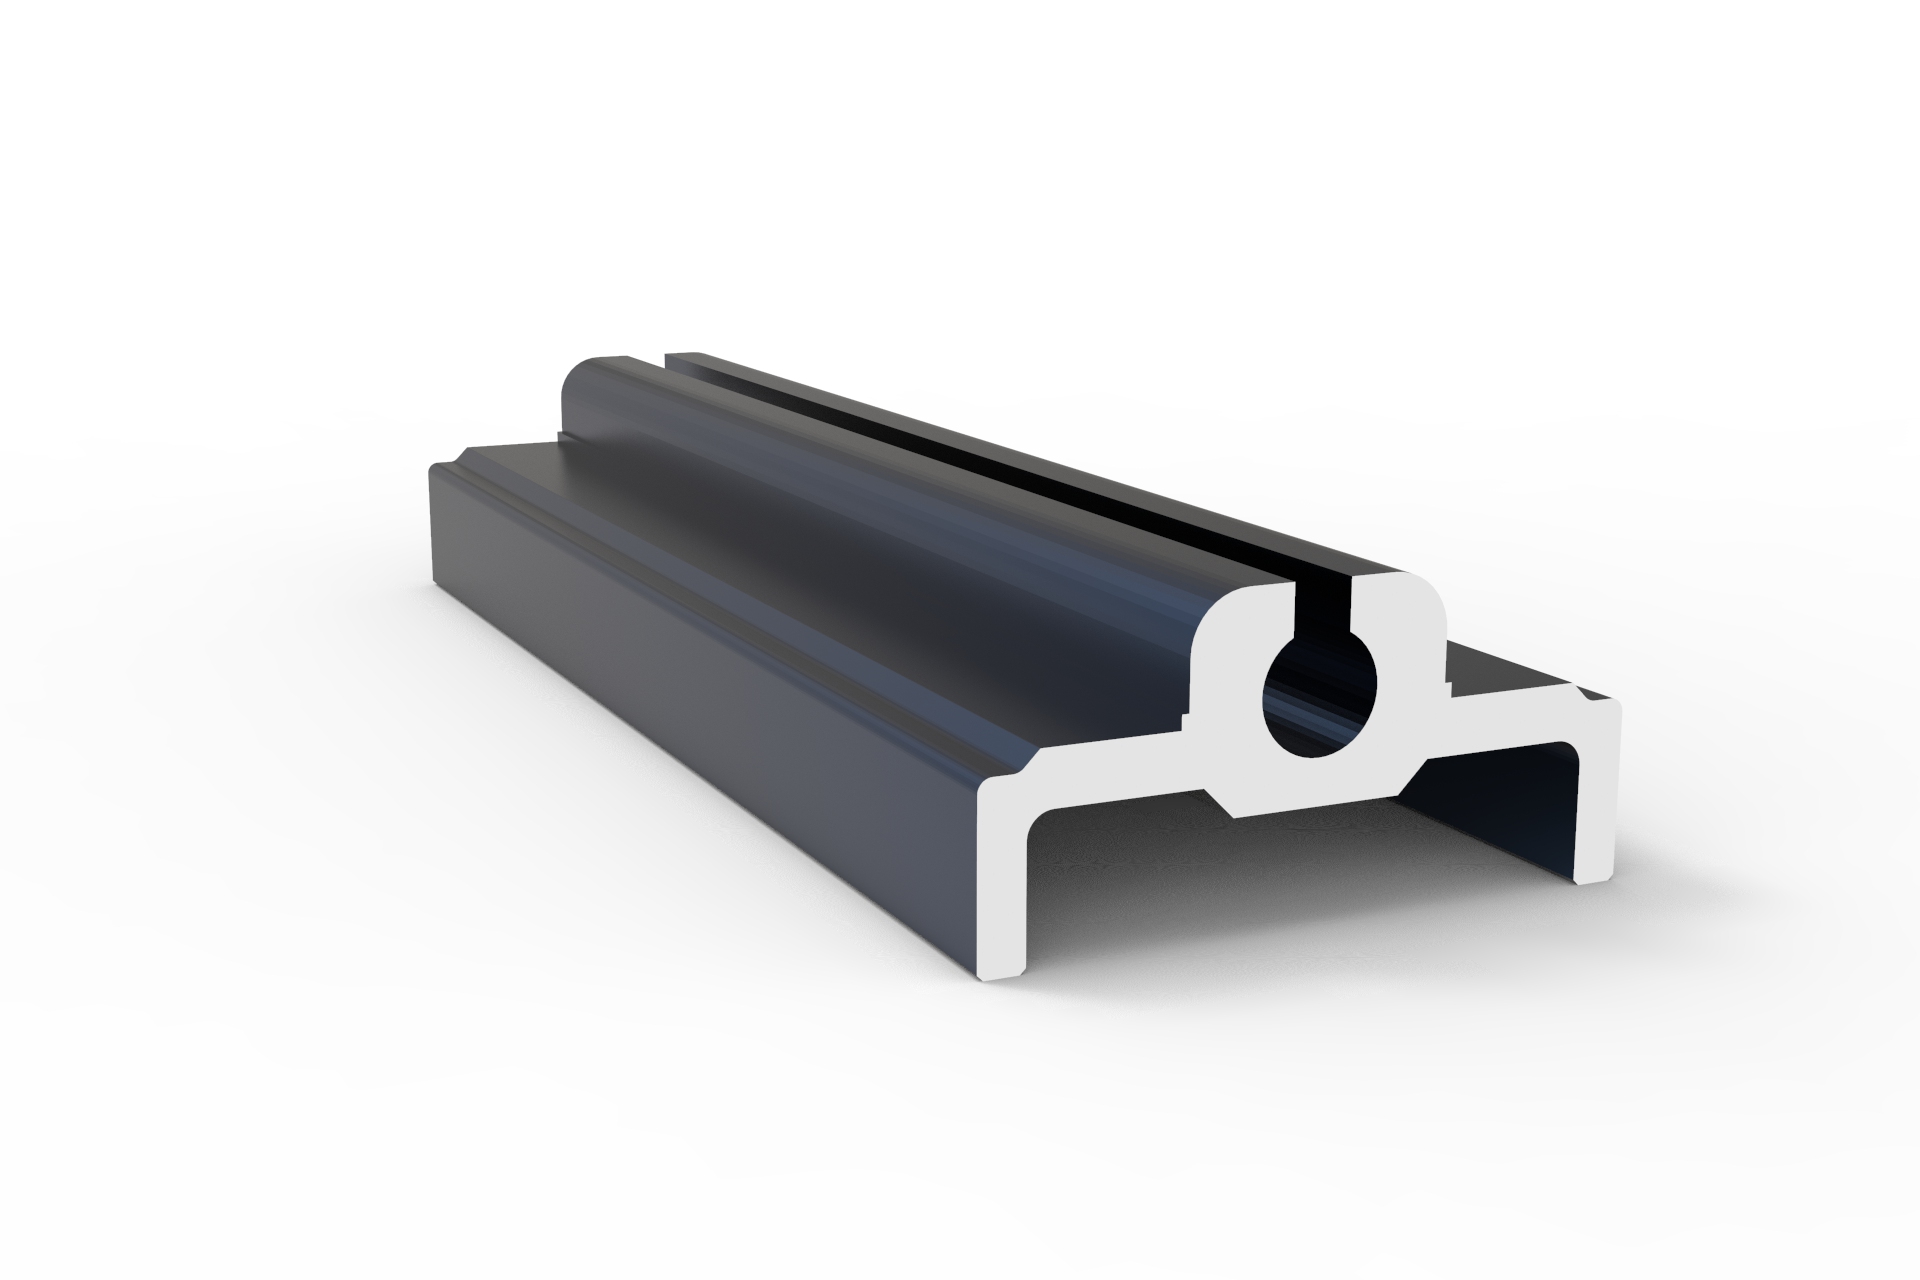
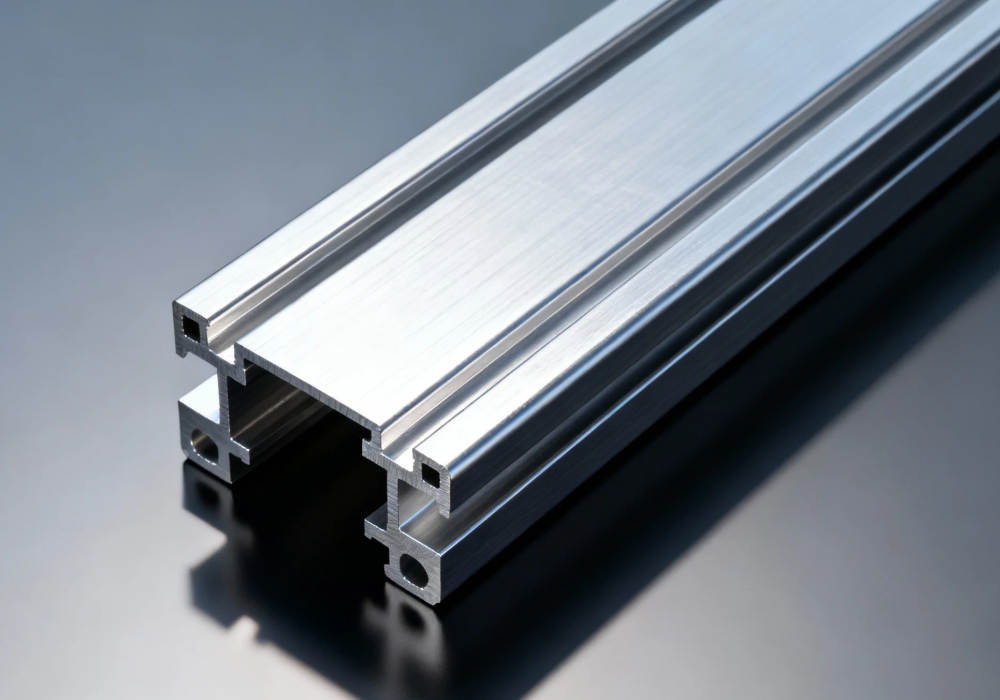
The L-shaped angle profile appears deceptively simple. It is merely a continuous extrusion of metal formed into a 90-degree intersection. Yet, this basic geometric configuration solves complex load distribution problems across countless construction scenarios. Understanding how this component functions requires looking past its visual simplicity. We must examine the underlying metallurgy, physical mechanics, and surface chemistry.
A flat rectangular strip of metal possesses severe limitations. Under a perpendicular load, it deflects easily due to its low moment of inertia along the bending axis. Bending or extruding that exact same mass of metal into a 90-degree angle completely alters its physical behavior.
By redistributing the material further away from the neutral axis, the structural rigidity increases exponentially. One leg of the angle acts as a stabilizing flange for the other. This mutual reinforcement prevents buckling under compressive forces. It effectively transforms a flexible strip into a rigid beam capable of bearing significant loads.
This geometric advantage is crucial in framing applications. When constructing door assemblies or industrial equipment brackets, the corner joints experience intense torsional forces. The standard 90-degree angle perfectly matches orthogonal corner designs. It provides a continuous anchor point that distributes stress evenly across both intersecting planes.
The performance of any extrusion is entirely dependent on its metallurgical composition. The 6000-series alloys are the absolute standard for architectural framing. These are alloyed primarily with magnesium and silicon.
Magnesium increases the overall solid solution strength of the metal. Silicon reduces the melting temperature, allowing the metal to flow smoothly through complex extrusion dies. The 6063 alloy offers an exceptional balance of tensile strength and surface finish quality. It is highly responsive to anodic oxidation.
The 6463 variant shares similar properties but is formulated with tighter controls on impurities like iron. This specific chemistry makes 6463 highly suitable for chemical brightening. It is often chosen when a highly reflective, mirror-like finish is demanded by the architectural design.
Heat treatment further dictates the mechanical capabilities of these profiles. The T5 temper involves rapidly cooling the extrusion as it exits the press. It is then artificially aged in an oven. This process aligns the crystalline structure, locking in the strength necessary for rigid structural support while maintaining enough ductility for fabrication.
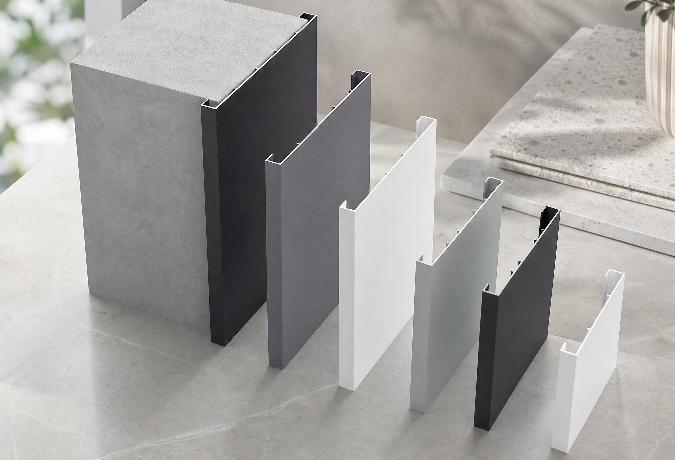
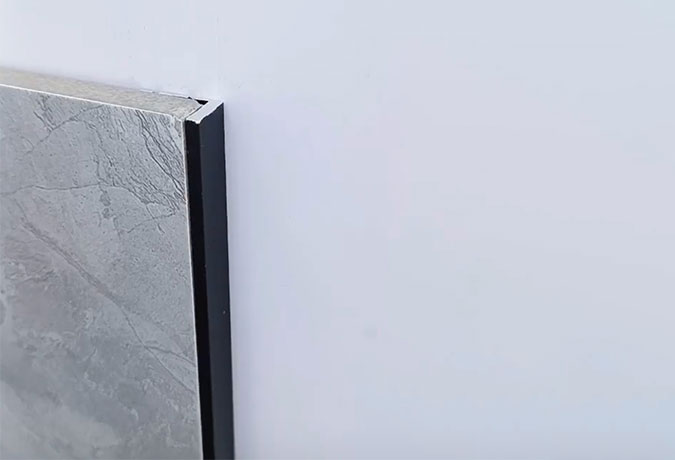
Modern interior design heavily utilizes ceramic tiles and polished stone panels. These materials boast massive compressive strength, meaning they can support heavy vertical loads. However, they are notoriously brittle and possess incredibly low tensile strength.
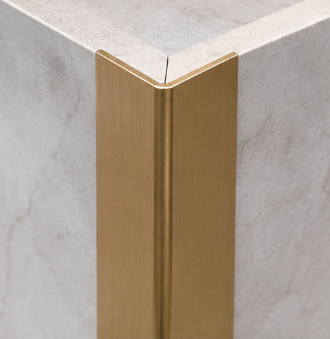
An exposed 90-degree edge on a marble or ceramic wall is a severe fracture risk. A minor lateral impact from heavy furniture or equipment will cause the glazed surface to chip. Once the glaze is compromised, moisture can penetrate the porous ceramic body beneath.

Installing an aluminium angle profile along this intersection fundamentally changes the impact mechanics. The metal acts as a highly resilient, sacrificial barrier. When an object strikes the corner, the aluminium absorbs the kinetic energy.
Because the metal is ductile, it disperses this energy along the length of the extrusion rather than allowing it to concentrate at a single point. It ensures the brittle ceramic edge remains completely isolated from the physical shock.
Bare aluminium naturally develops a thin layer of oxide when exposed to air. While this prevents rapid rusting, it is visually inconsistent and insufficiently durable for high-traffic environments. Surface treatments are not merely aesthetic choices; they are engineered functional barriers.
Anodizing is an electrochemical process that forces the growth of a dense, porous aluminum oxide layer on the surface. This layer is fully integrated into the metal substrate. It cannot peel or flake off. The pores are then sealed, creating an exceptionally hard, wear-resistant surface that withstands UV radiation without fading.

Powder coating relies on electrostatic attraction. Dry plastic powder is sprayed onto the grounded metal profile. The extrusion is then baked, causing the powder to melt and cross-link into a continuous polymeric shell.
This method allows for an infinite spectrum of colors while providing excellent chemical resistance. For extreme exterior applications, fluorocarbon coatings offer unparalleled resistance to atmospheric pollution and coastal salt spray.
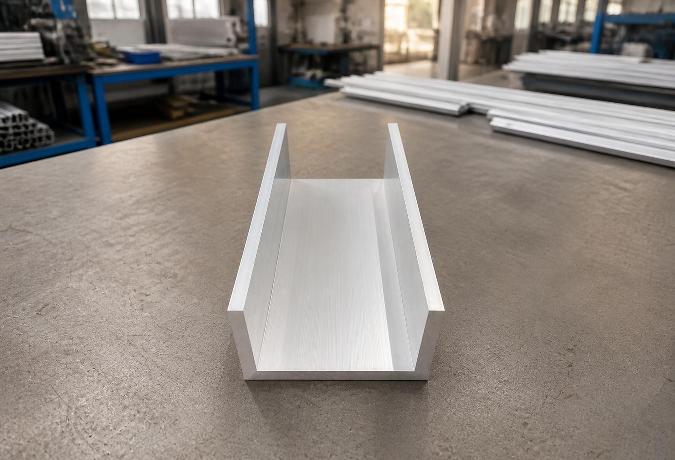
Angle profiles are extruded in two primary geometric configurations: equal legs and unequal legs. The choice between them depends entirely on the directional forces present in the specific application.
Equal leg profiles have symmetrical dimensions, such as a 20mm by 20mm configuration. The centroid of the shape is positioned symmetrically. This geometry is ideal for general corner protection, tile edging, and constructing square frames. It handles uniform stress distribution effectively.
Unequal leg profiles feature one leg longer than the other, like a 40mm by 20mm shape. This asymmetry is intentional. It provides higher resistance to bending along the axis of the longer leg. When used as a cantilevered bracket, the longer leg is anchored to the wall, offering a larger surface area for fasteners and reducing sheer stress on the anchor points.
Engineers and architects require precise data to integrate these components into larger structural assemblies. The following specifications represent the standard parameters for high-grade extrusion manufacturing.
All building materials expand and contract with temperature fluctuations. Aluminium has a relatively high coefficient of thermal expansion compared to concrete or ceramic. When mating these materials together, engineers must account for differential movement.
If an aluminium profile is rigidly pinned to a stone wall without any tolerance, thermal expansion will create severe internal stress. This stress can warp the metal or crack the adjacent stone.

In proper architectural installations, these profiles are bedded into flexible adhesives or caulking. The adhesive acts as a microscopic shock absorber. It allows the metal to expand slightly along its longitudinal axis without transferring destructive forces into the rigid wall structure. The L-shape also allows one leg to float slightly behind the paneling while the visible edge remains fixed.
Do aluminium angle profiles suffer from galvanic corrosion?
Yes, if installed incorrectly. When aluminium comes into direct, uninsulated contact with a dissimilar metal like carbon steel or copper in the presence of moisture, galvanic corrosion occurs. The aluminium acts as an anode and deteriorates. Using isolation tapes, non-metallic washers, or heavy surface coatings prevents this electrochemical reaction.
Is a T6 temper always better than a T5 temper for angle profiles?
Not necessarily. T6 offers higher ultimate tensile strength and yield strength, making it superior for heavy structural load-bearing. However, T6 is less ductile than T5. If the installation requires bending, curving, or extensive on-site manipulation, a T5 temper is much easier to work with and less prone to micro-cracking during fabrication.
Can powder coating hide extrusion die lines?
Powder coating builds a physical layer of plastic over the metal, typically ranging from 60 to 80 microns thick. This thickness is sufficient to fill in and mask minor surface imperfections and microscopic die lines resulting from the extrusion process. Anodizing, conversely, is only 10 to 25 microns thick and will highlight any existing surface textures.
The widespread adoption of these extrusions is partly due to their exceptional workability. Unlike steel, which requires heavy cutting torches or abrasive saws, aluminium can be processed with standard carbide-tipped woodworking tools.
A miter saw equipped with a non-ferrous cutting blade creates perfectly clean 45-degree cuts for seamless corner joints. The material is soft enough to drill quickly for anchoring but strong enough to hold a tapped thread if required for mechanical fastening.
When integrating these profiles into drywall or plasterboard assemblies, the metal often serves as a screed guide. Plasterers use the rigid edge of the profile to drag their trowels, ensuring a perfectly plumb wall finish. The flange of the profile is then buried beneath the joint compound, leaving only a clean, sharp metallic line visible.
For us, manufacturing these solutions means understanding the exact tolerances required on a busy job site. With decades of continuous refinement in extrusion technology, we maintain strict controls over wall thickness uniformity and geometric precision. A profile that is twisted by even a fraction of a degree will cause cascading alignment failures in a large window assembly.
Ultimately, the successful deployment of architectural aluminium profiles relies on matching the right alloy, temper, and geometry to the specific physical forces of the environment. From protecting fragile marble edges to holding industrial panels rigid against wind loads, the simple 90-degree angle remains one of the most mechanically efficient shapes in modern engineering.
Aluminium Profile Alloys 6063 T5 T6: Properties, Heat Treatment Differences, and Application Selecti
Inside an Aluminium Profile Factory: How Angle Profiles Are Made and Chosen
What is a realistic MOQ for a first Sliding window trial order?
Which factory records should I review before buying Industrial profile?
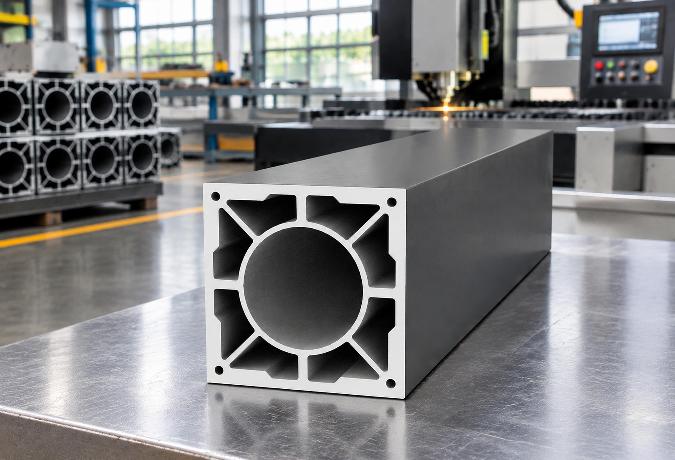
Aluminium Extrusion for Machinery: Choosing the Right Profile for Industrial Equipment
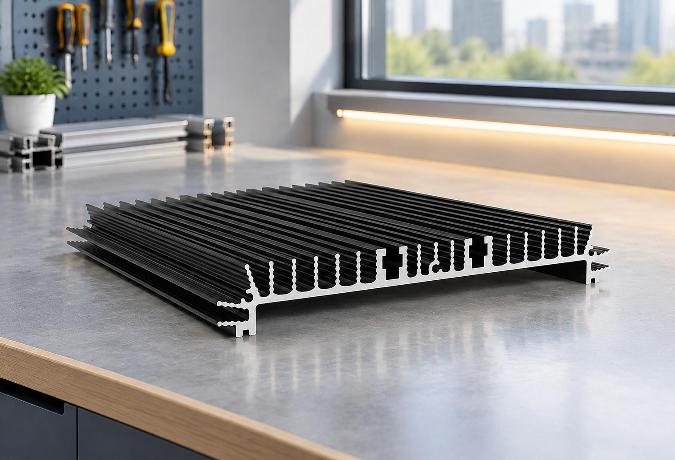
Aluminium Extrusion for LED Lighting: Choosing the Right Heatsink Profile
Can a Floding door supplier protect my private design from competitors?
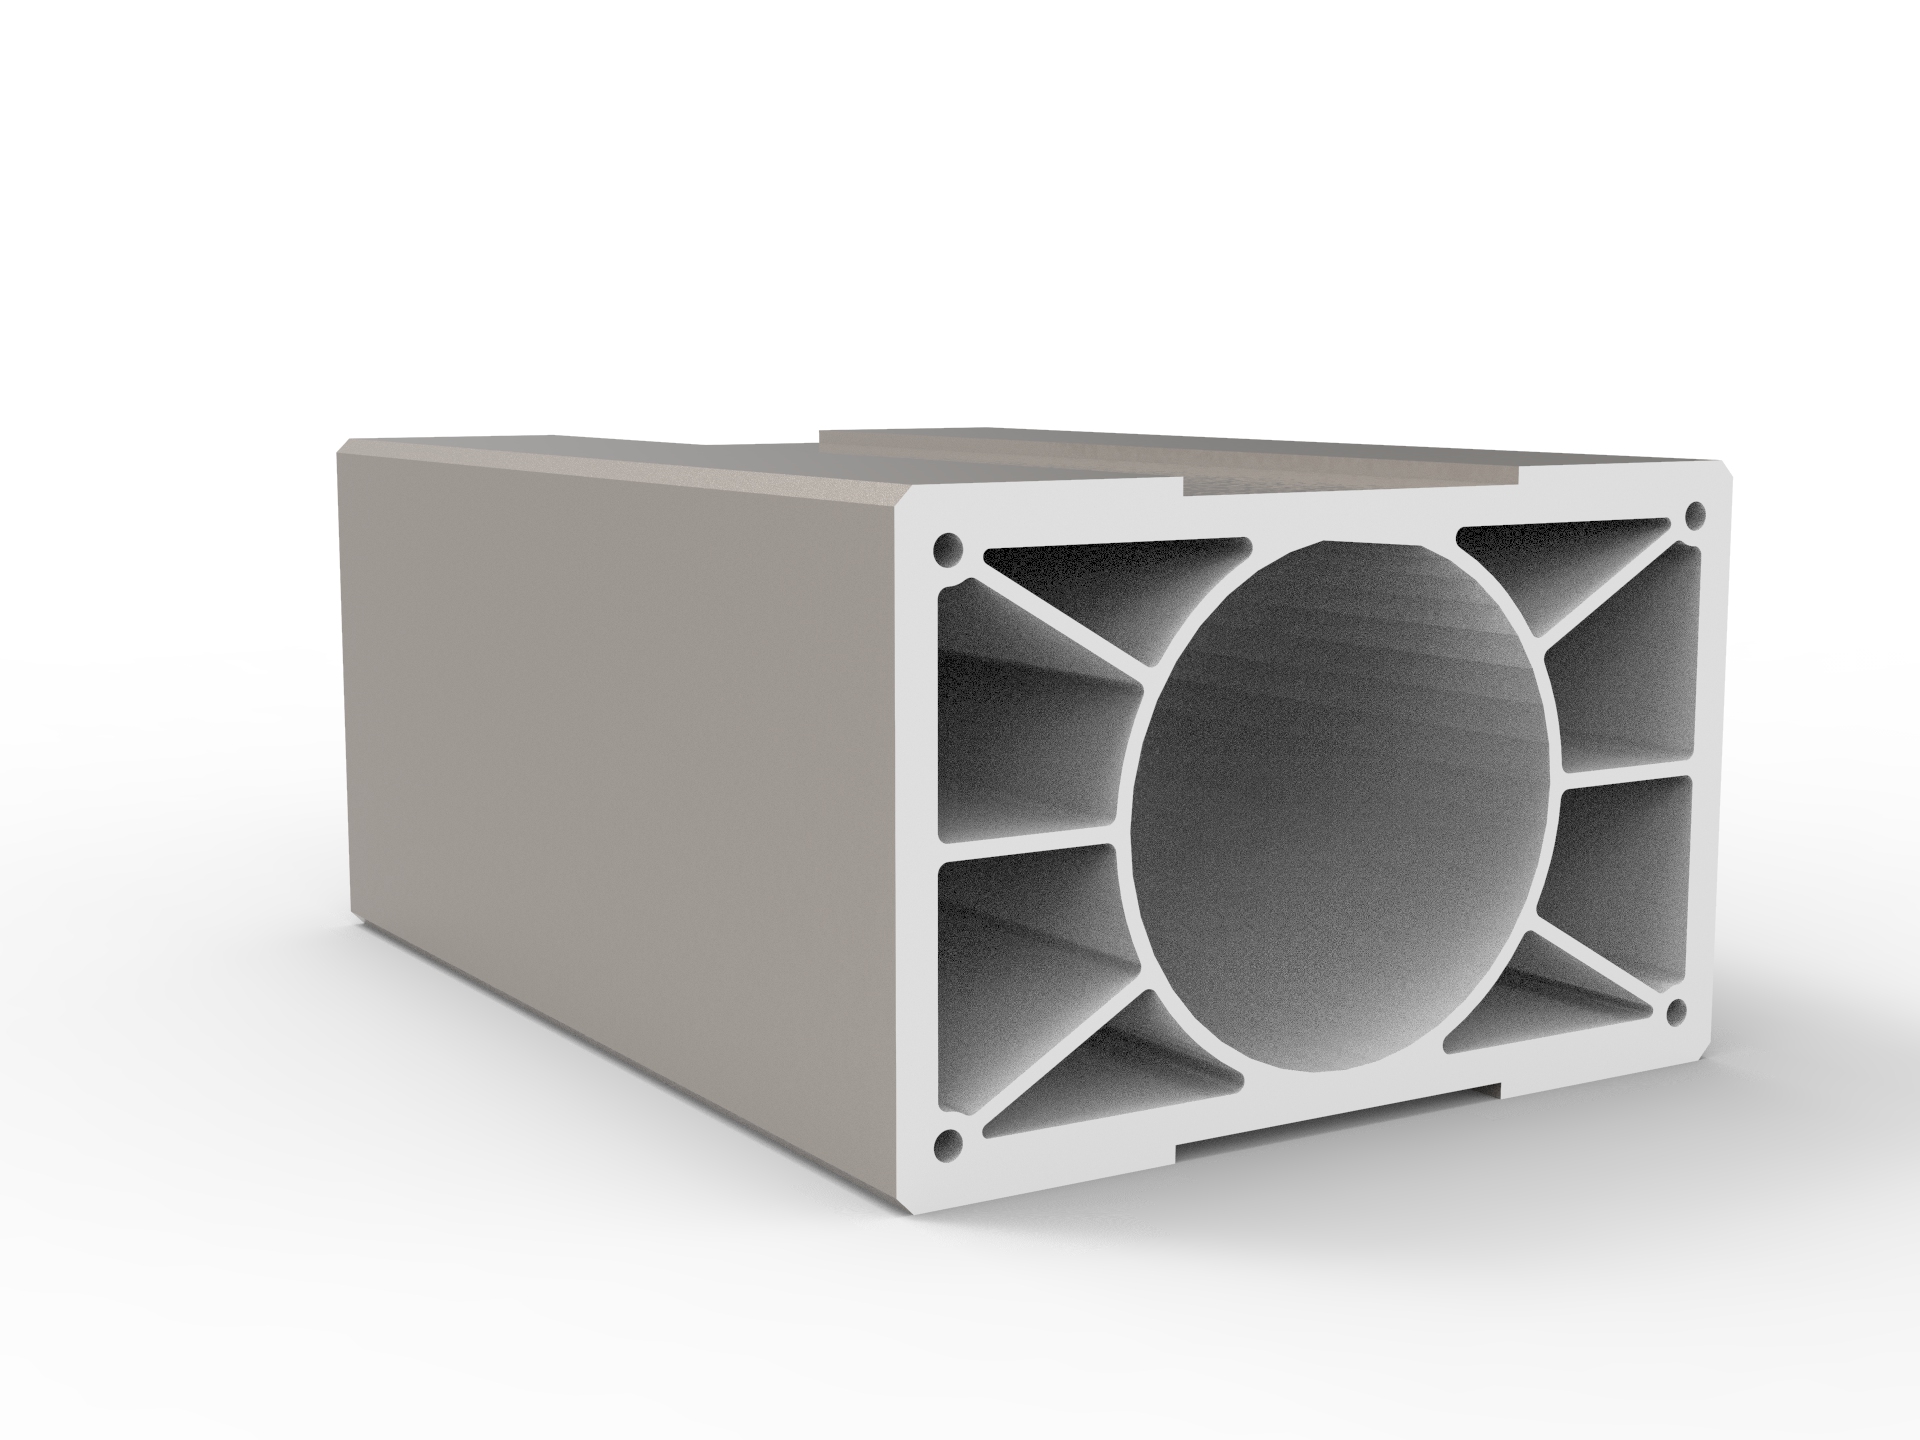
Which Industrial profile tolerances affect assembly accuracy and finished quality?
Can trade credit insurance cover my Architecture profile purchase risk?
Custom Aluminium Extrusion Profiles: Engineering Precision into Industrial Motion Systems
T-Slot Aluminium Extrusion: Structural Framework Design Without Welding
Which recycled-content records are credible for Sliding window procurement?
Aluminium Sliding Door Profiles: A Practical Guide to Frame Design and Performance
How Aluminium Extrusion Manufacturers in China Support Linear Motion Systems
What contract clauses protect my money if Casement door quality is unacceptable?
How do I confirm Sliding door testing equipment is calibrated and current?
Should I visit an Architecture profile plant before placing a large order?
Which compliance tests should a Floding door pass before international shipment?
How do I compare Decorative profile color samples under different lighting?
What payment and price terms make sense for a small Casement window order?
What lead time should I allow for a seasonal Floding door order?
How can I compare Floding door alternatives when supply costs suddenly rise?
Which new Sliding door technologies can lower maintenance costs over time?
How are recycled materials changing the future cost of Floding doors?
How long should a custom Casement door sample normally take to prepare?
What gap between a Sliding window sample and bulk order is acceptable?
Which Decorative profile finishes are becoming more sustainable and cost-effective?
What logistics fees should be listed separately in a Sliding window quote?
How might volatile aluminum prices affect future Sliding window sourcing?
Which audit questions reveal labor risks at a Casement door factory?
Can Decorative profile suppliers provide fast remote guidance for finish defects?
What should a Shutter sample include so I can assess production quality?
Do Sliding door materials need traceability records for customs clearance?
What environmental declarations are useful when importing Architecture profile?
Why Blade Geometry Determines Whether Aluminium Louvers Actually Work
Engineering an Aluminium Angle Profile: Structural Mechanics and Application Realities
What usually drives Architecture profile costs more, alloy or surface treatment?
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
Why the Thermal Break Cavity Matters More Than Frame Thickness in Aluminium Framed Windows and Doors
The T-Slot Groove Geometry That Makes Aluminium Framing Weld-Free
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
Structural Dynamics of Industrial Aluminium Profiles in Laser Cutting Gantries
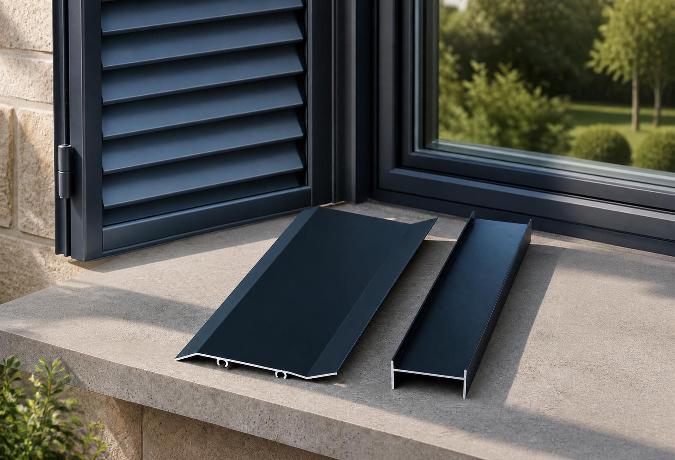
The Engineering Mechanics Behind High-Performance Aluminium Shutters
What factory documents should I request for a Floding door supplier review?
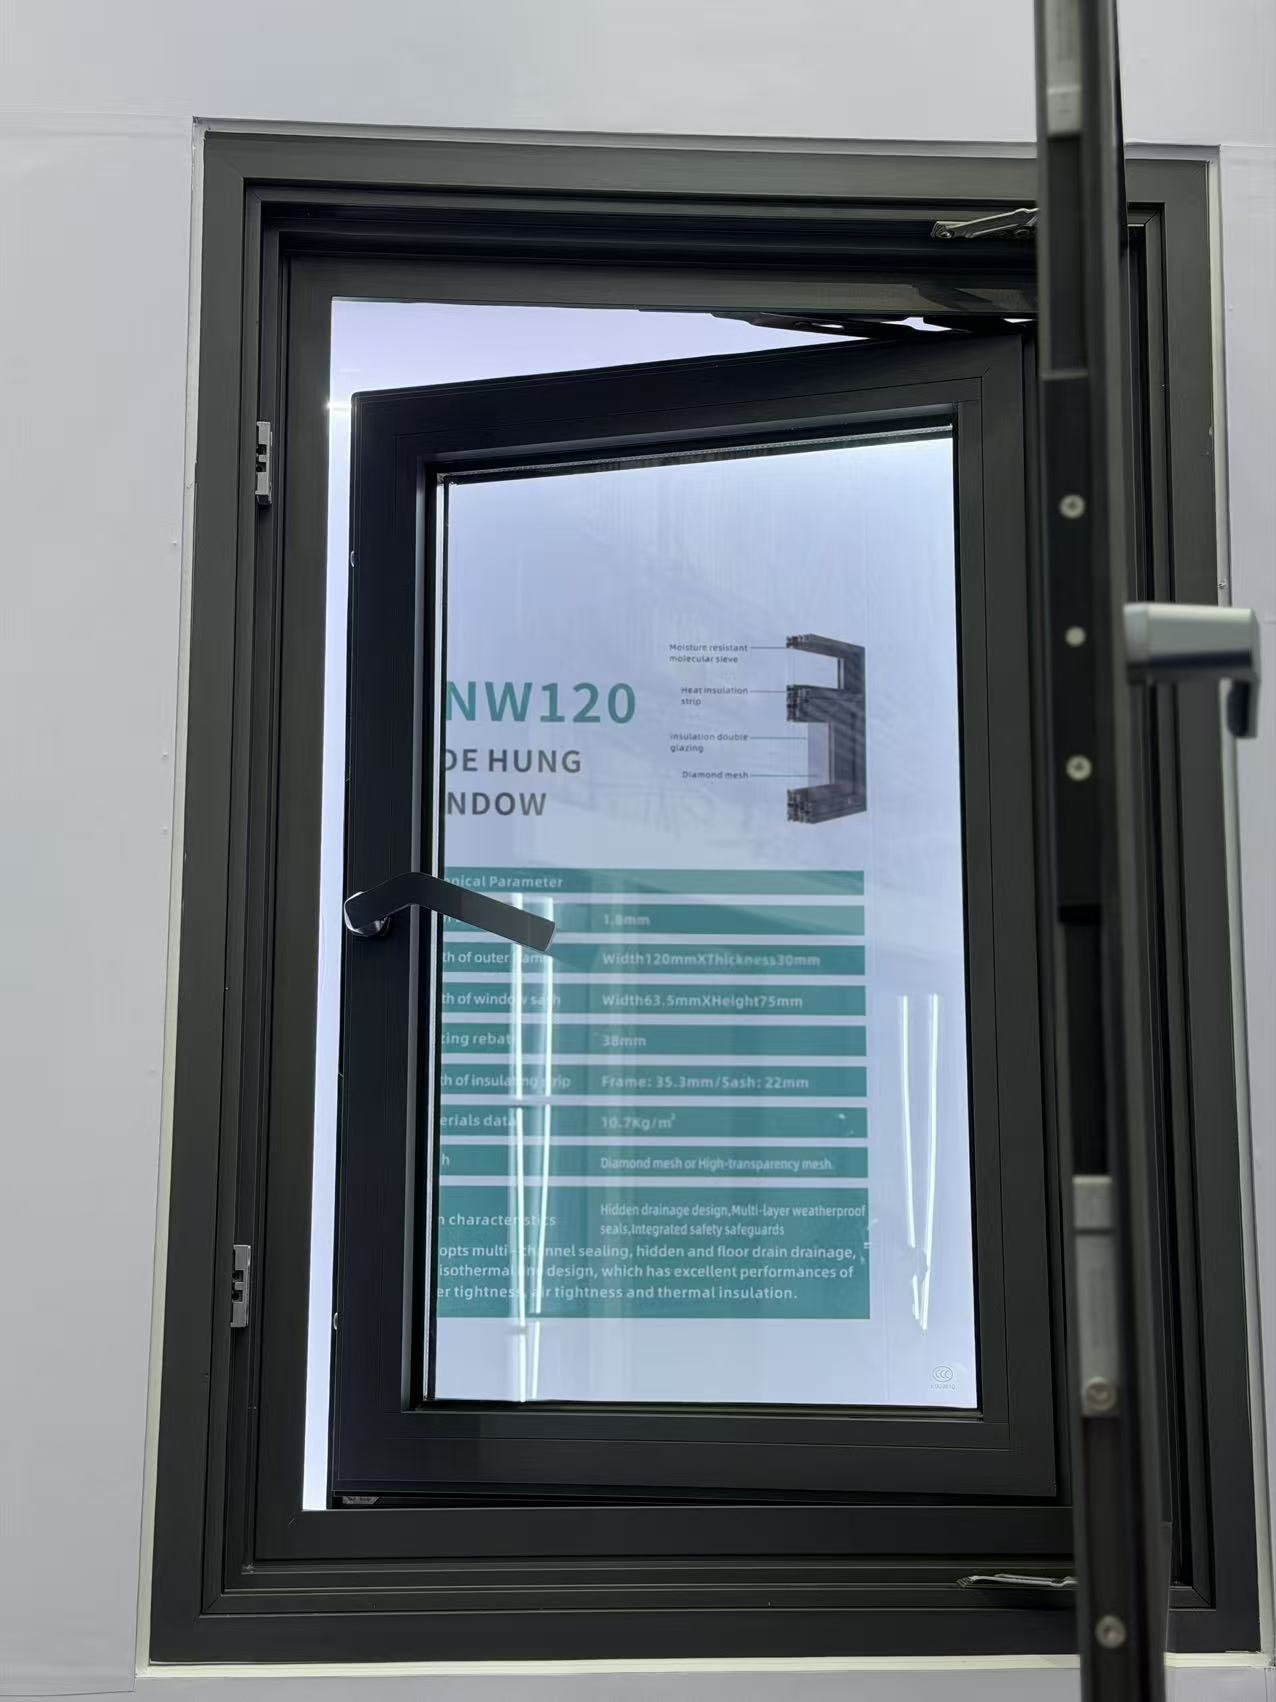
Which delivery term gives me better control over Decorative profile freight costs?
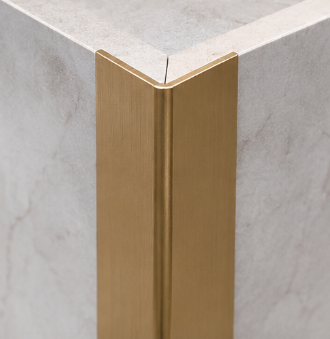
What low-carbon Awing window materials are gaining wider market acceptance?
Why Sliding Door Track Geometry Determines Wardrobe Longevity
Engineering Mechanics and Surface Dynamics of Aluminium Channel Profiles
Understanding Aluminium Round Tube Specifications for Structural Engineering
Why the 90-Degree Angle in Standard Aluminium Profiles Determines Structural Reliability
How can I ensure a Floding door sample matches the planned mass production?
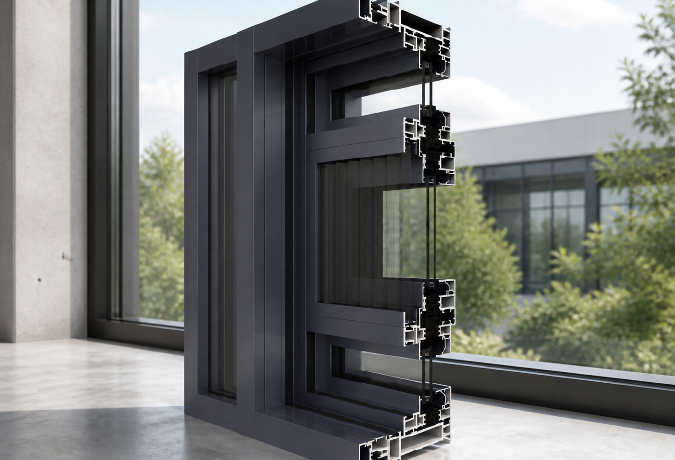
Why Mullion Thickness Determines How Much Glass an Aluminium Curtain Wall Can Actually Hold
Engineering Dimensional Stability in Aluminium Extrusions for Channel Profiles
Engineering the Structural Framework: The Mechanics of Aluminium Profiles for Kitchen Cabinets
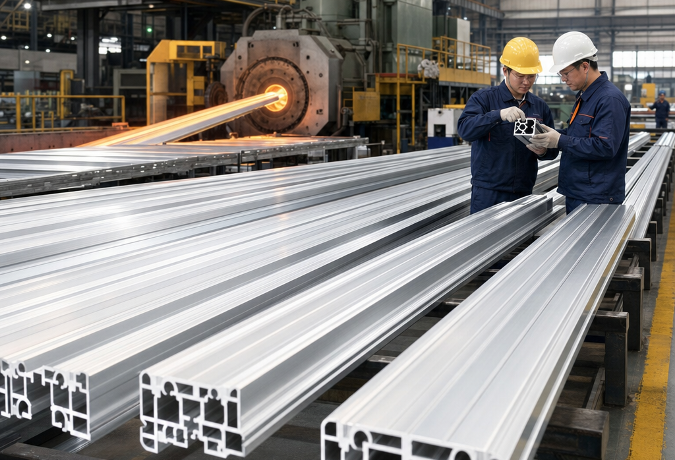
Choosing an Aluminium Profile Supplier: What Actually Separates the Reliable Ones from the Rest
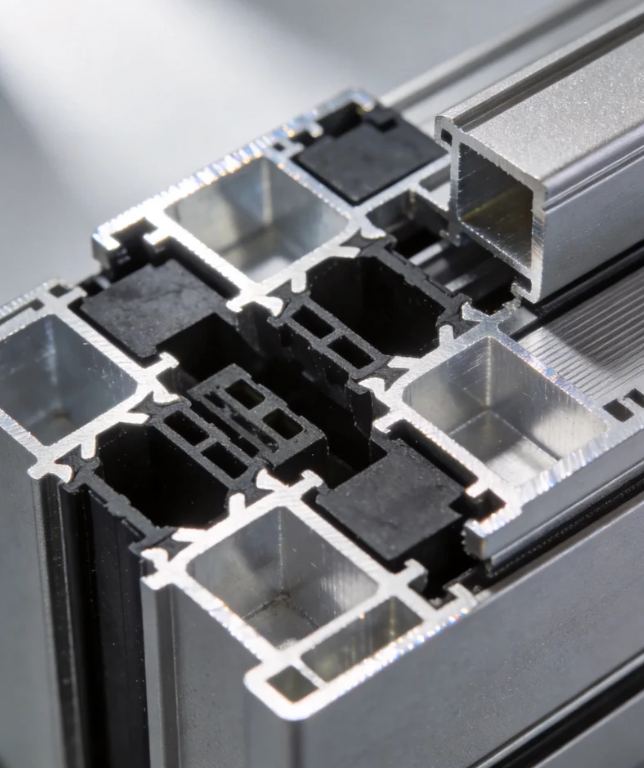
Can Awing window orders ship in batches to avoid project delays?
What response time should I expect for Awing window warranty claims?
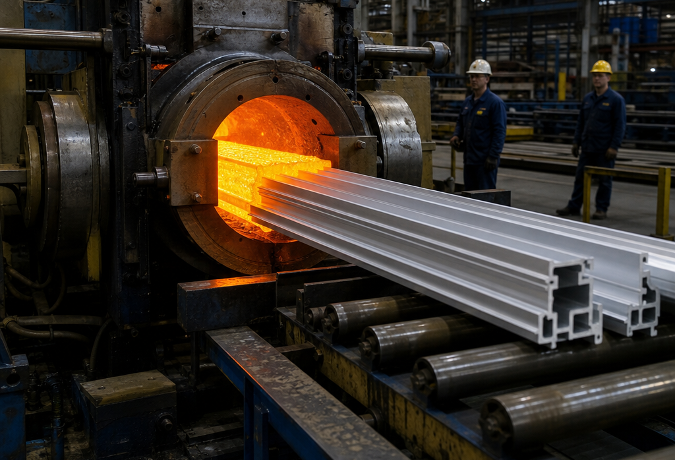
Navigating the Supply Chain: Evaluating an Aluminium Profile Manufacturer for B2B Procurement
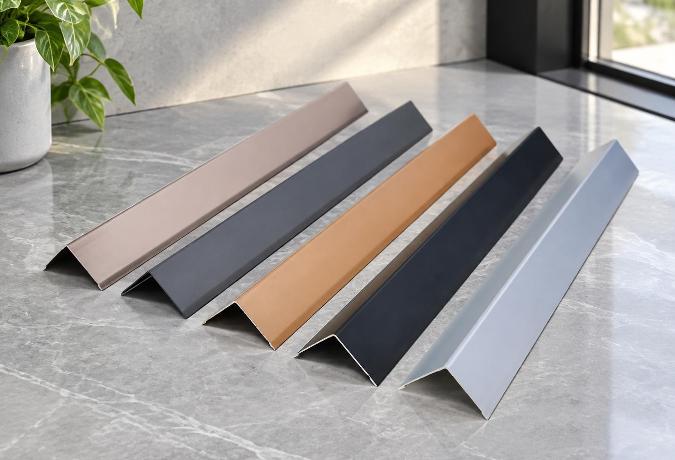
Engineering Structural Integrity Through Precision L-Shaped Aluminium Profiles
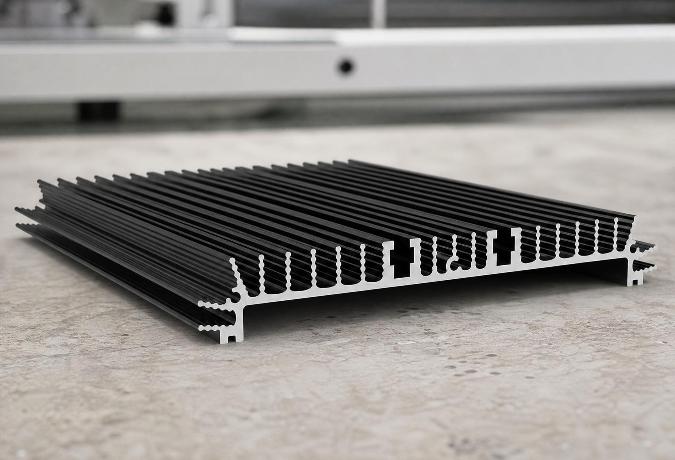
Thermal Dynamics in High-Power Electronics: Engineering Aluminium Heatsink Profiles
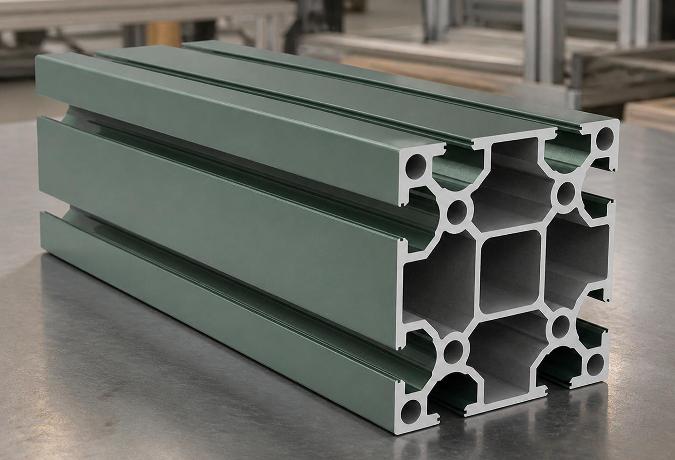
Why the T-Slot Design Determines the Real Strength of Structural Aluminium Extrusions
How long should replacement Sliding window parts remain available after purchase?
Should I expect volume discounts when reordering the same Sliding window model?
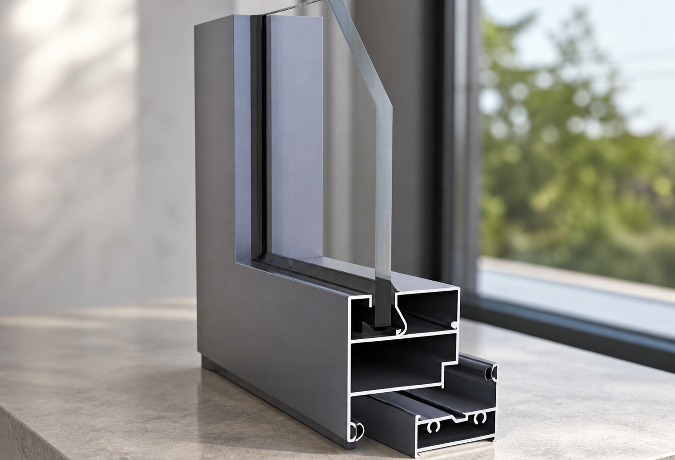
The Multi-Strip Sealing Structure Inside Aluminium Windows and Doors
Engineering Lightweight Rail Structures Through Extruded Aluminium Profiles
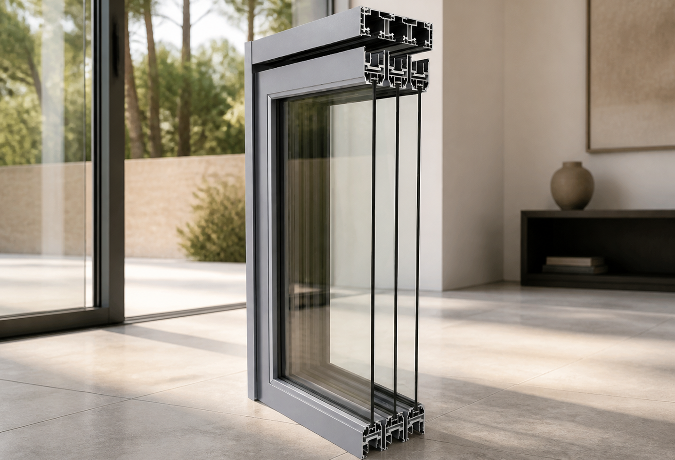
Why the Frame Width on an Aluminium Sliding Door Determines Your Room’s Light
The Engineering Behind Decorative Aluminium Profiles: Alloys, Surface Treatments, and Edge Protectio
What alternative materials could make Casement doors more resilient and recyclable?
How can I compare Awing window quotes without missing hidden packing costs?
Decoding Structural Tolerances in Aluminium Extrusion Profiles for Channel Applications
Engineering an Aluminium Square Tube for Modern Structural Integrity
Engineering Tolerances and Alloy Mechanics in Extruded Aluminium Construction Profiles
Can an Industrial profile be modified for my assembly without weakening it?
What warning signs suggest a Sliding door seller may disappear after payment?
What energy-efficient alternatives to Casement doors are worth comparing now?
Can a Casement window handle temperature changes without seal failure?
Who pays for unloading and destination handling under Casement door CIF terms?
Custom Aluminium Extrusion Profiles: The Engineering Mechanics of T-Slot Frameworks
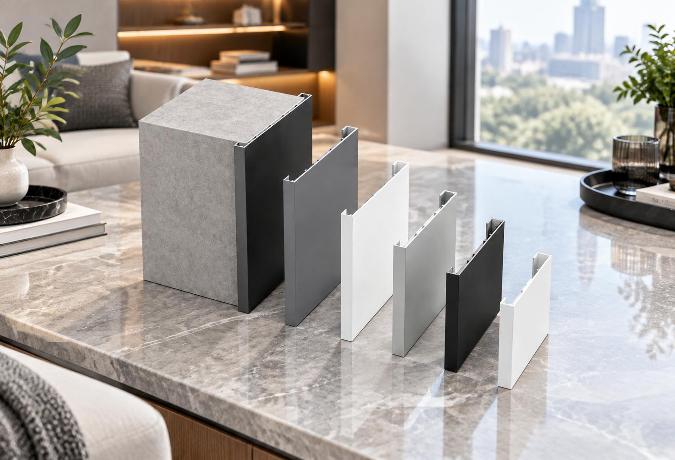
Material Transitions and Geometric Stability in Decorative Aluminium Profiles
Can I negotiate a lower Sliding door MOQ for a showroom launch?
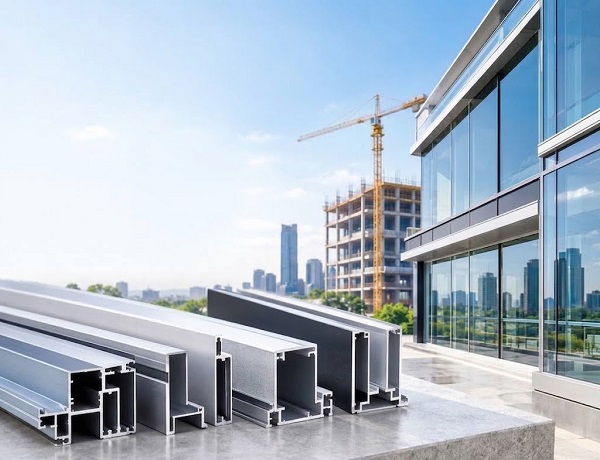
Key Advantages of Using Structural Aluminium Extrusion Profiles in Construction
What evidence shows an Awing window factory manages coating waste properly?
How can I protect my deposit when ordering custom Decorative profile?
How do I spot unusually low Industrial profile prices before committing funds?
How can I check that a Shutter supplier is not using unapproved subcontractors?
What contract terms protect my Casement door drawings and branding?
How can I compare Casement door insulation ratings before placing an order?
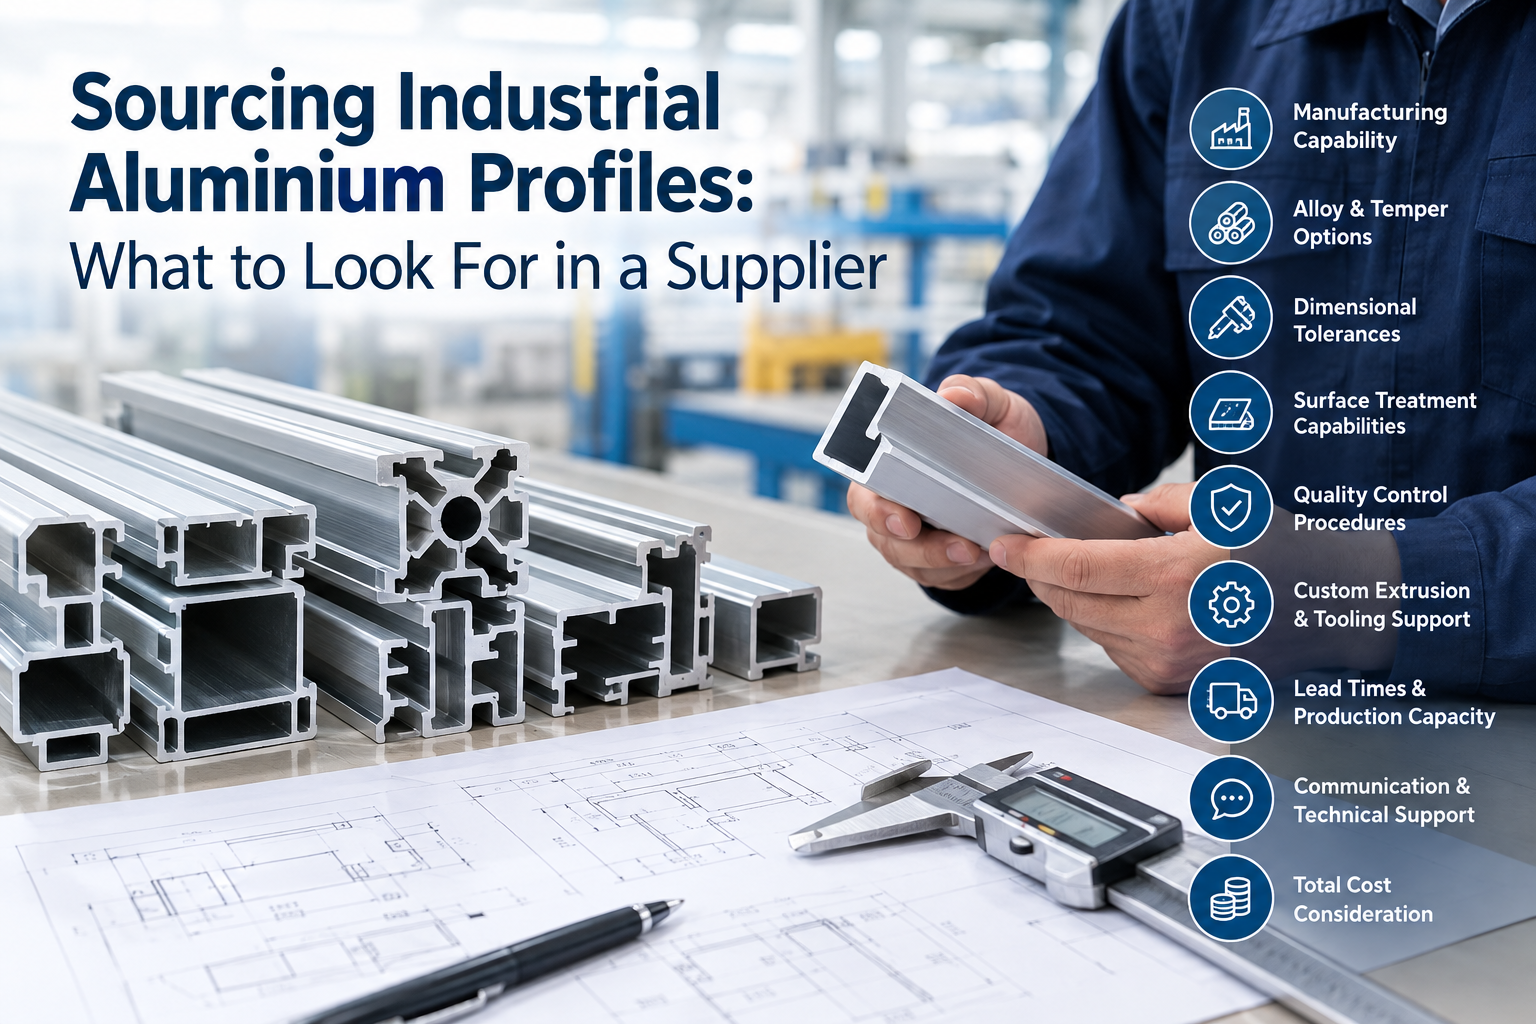
Sourcing Industrial Aluminium Profiles: What to Look For in a Supplier
How do I keep ownership of a custom Architecture profile extrusion die?
The Energy Efficiency Benefits of an Aluminium Frame Sliding Glass Window
How do I check Industrial profile alloy grades against the shipping documents?
What Casement window warranty period is reasonable for an overseas buyer?
How are defective Sliding window units usually replaced internationally?
How can I reduce breakage risks when shipping Casement windows overseas?
The Structural Mechanics Behind Decorative Aluminium Profiles
How Do Engineers Select Industrial Aluminium Profiles for High-Load Frameworks?
What payment structure reduces my risk on a first Industrial profile order?
Should I approve a Casement window sample before checking its hardware strength?
Structural Mechanics of Channel Extrusions in Architectural Aluminium Profiles
Engineering Mechanics of Aluminium Extrusion Profiles in Channel Systems
What functional tests should I perform on a Sliding door prototype?
What payment terms are fair when Decorative profile colors remain unconfirmed?
Is a letter of credit practical for a large Casement window shipment?
How should Industrial profile bundles be packed to prevent transit damage?
Which safety documents should I request for Awing window imports?
What shipping delays commonly affect Architecture profile orders during peak season?
How to Specify Extruded Aluminium Profiles: Costs, Alloys, and Tolerances
Is a Floding door suitable for a wide opening exposed to strong winds?
Structural Integrity in Modular Design: Engineering T-Slot Aluminium Extrusion Profiles
Resolving Corner Stress: The Engineering Mechanics Behind Aluminium Profiles in Architectural Framin
How do Floding door prices change with glass, hardware, and finish choices?
How can I prove Shutter defects remotely without returning every unit?
How can I shorten Awing window sampling without losing critical tests?
Does ordering mixed Shutter sizes usually change the unit price or MOQ?
How should Industrial profile warranty responsibility be shared after assembly?
How should I plan Shutter inventory when ocean freight schedules change?
How do escrow arrangements reduce risk for a new Floding door supplier?
What frame materials make a Sliding window last in harsh coastal weather?
How can I verify that a Shutter certificate matches the actual product?
Can automated Shutters replace manual systems without raising lifecycle costs?
How do I choose the right Casement window size for a windy building?
What should an ethical audit cover at a Decorative profile factory?
How should I document Industrial profile defects before disputing the final payment?
Are lightweight Industrial profile alloys reliable enough for demanding machinery?
Are thermal-break casement windows becoming a better long-term choice than standard frames?
What is a realistic MOQ for custom sliding windows without pushing up unit cost?
What casement window specs should I compare for windy and rainy project sites?
Are there better material options for sliding windows if aluminum prices rise?
How do I ensure aluminum casement windows can handle extreme coastal winds?
What is the typical minimum order quantity for commercial sliding windows?
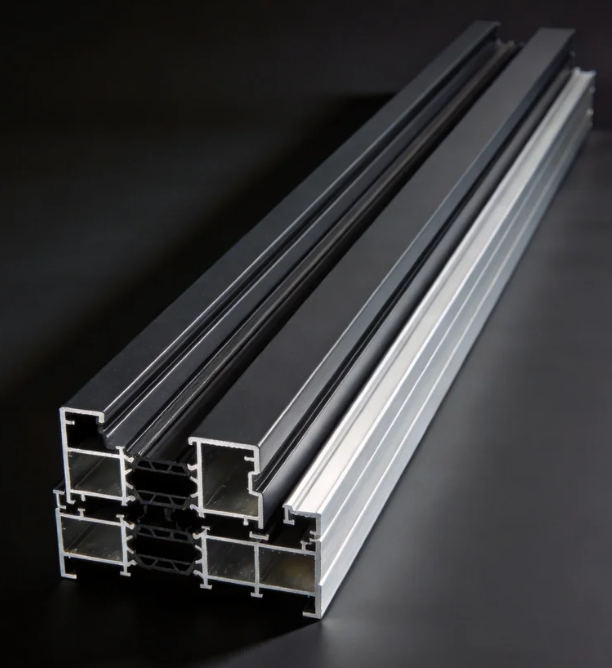
Are there energy-saving alternatives to sliding windows that reduce material and maintenance costs?
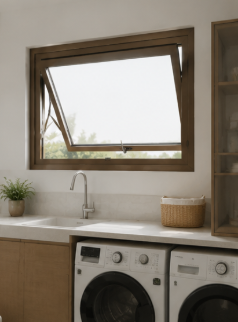
Are energy-efficient Awing windows a practical alternative for reducing long-term building costs?
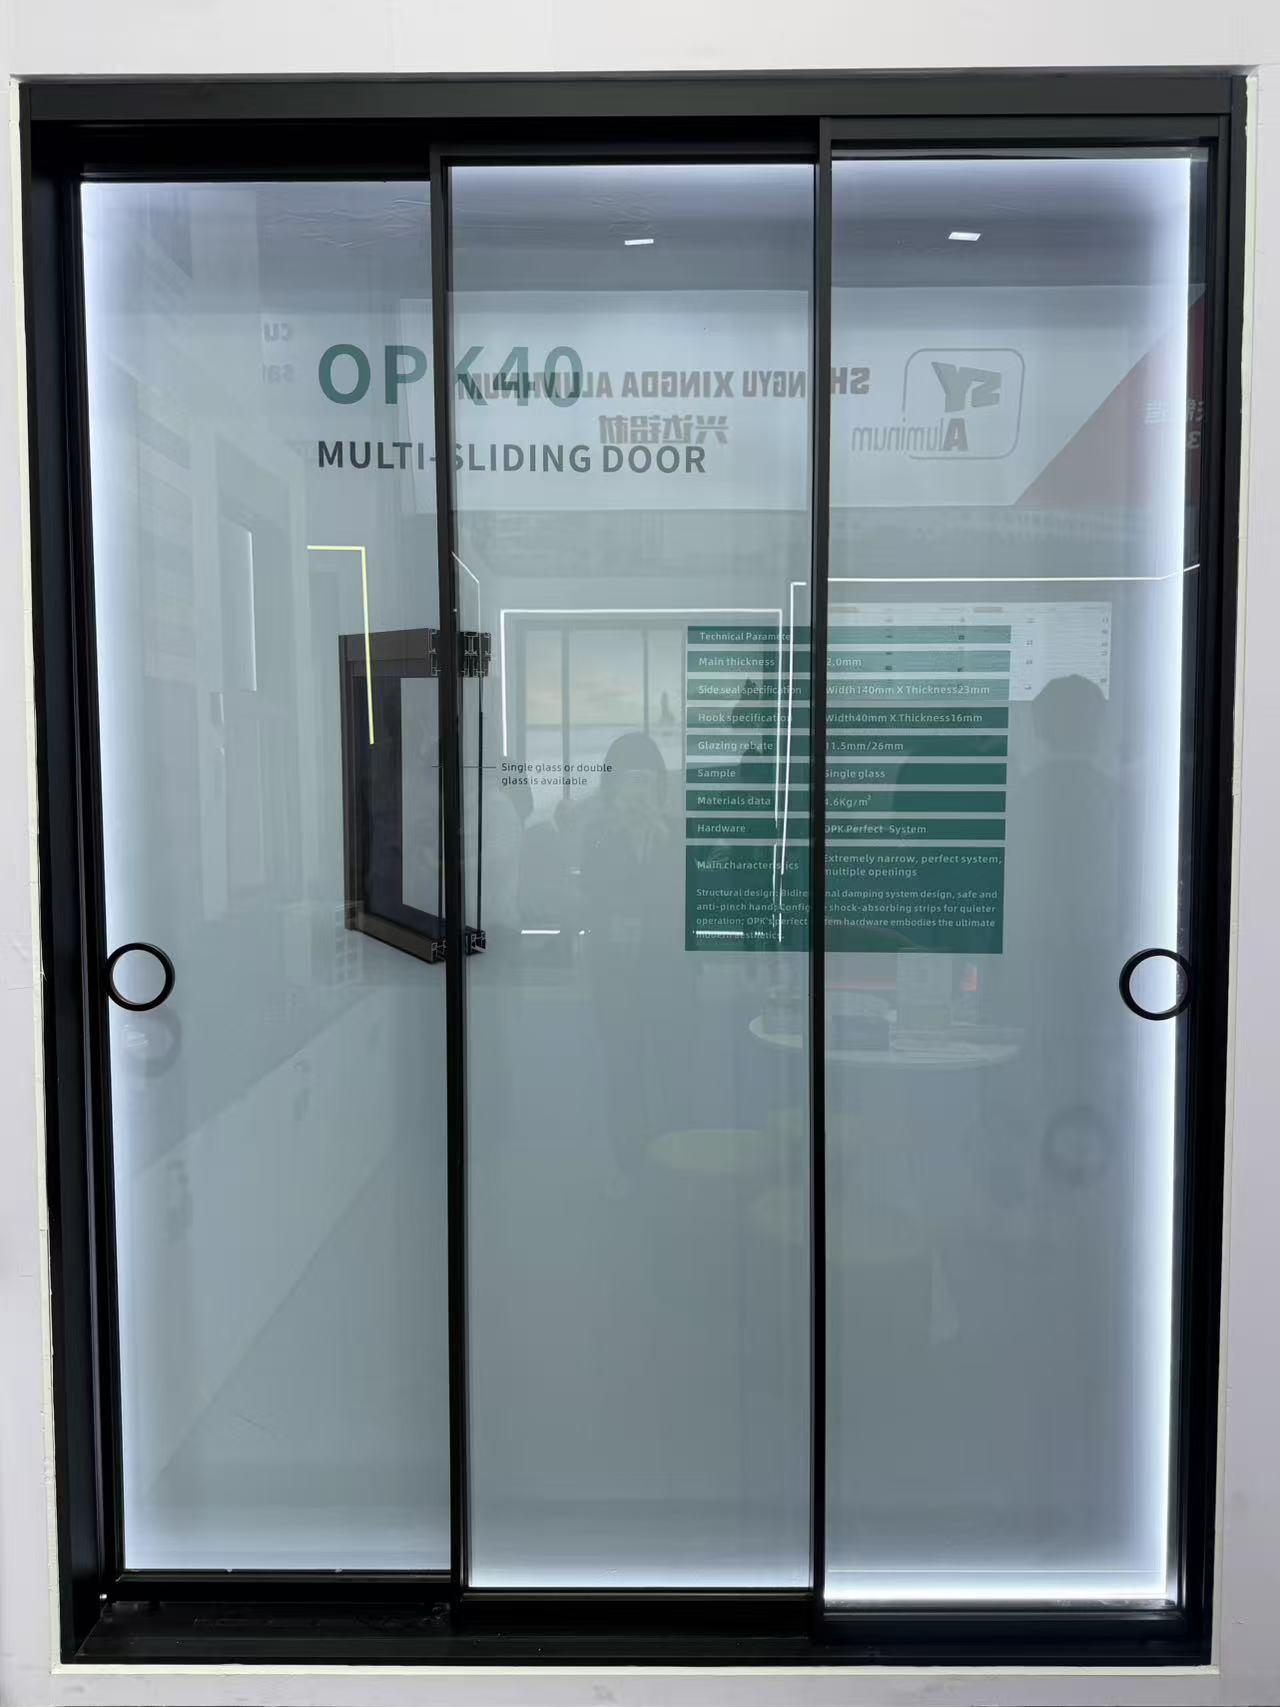
What alternatives to traditional sliding doors can lower costs without sacrificing durability?
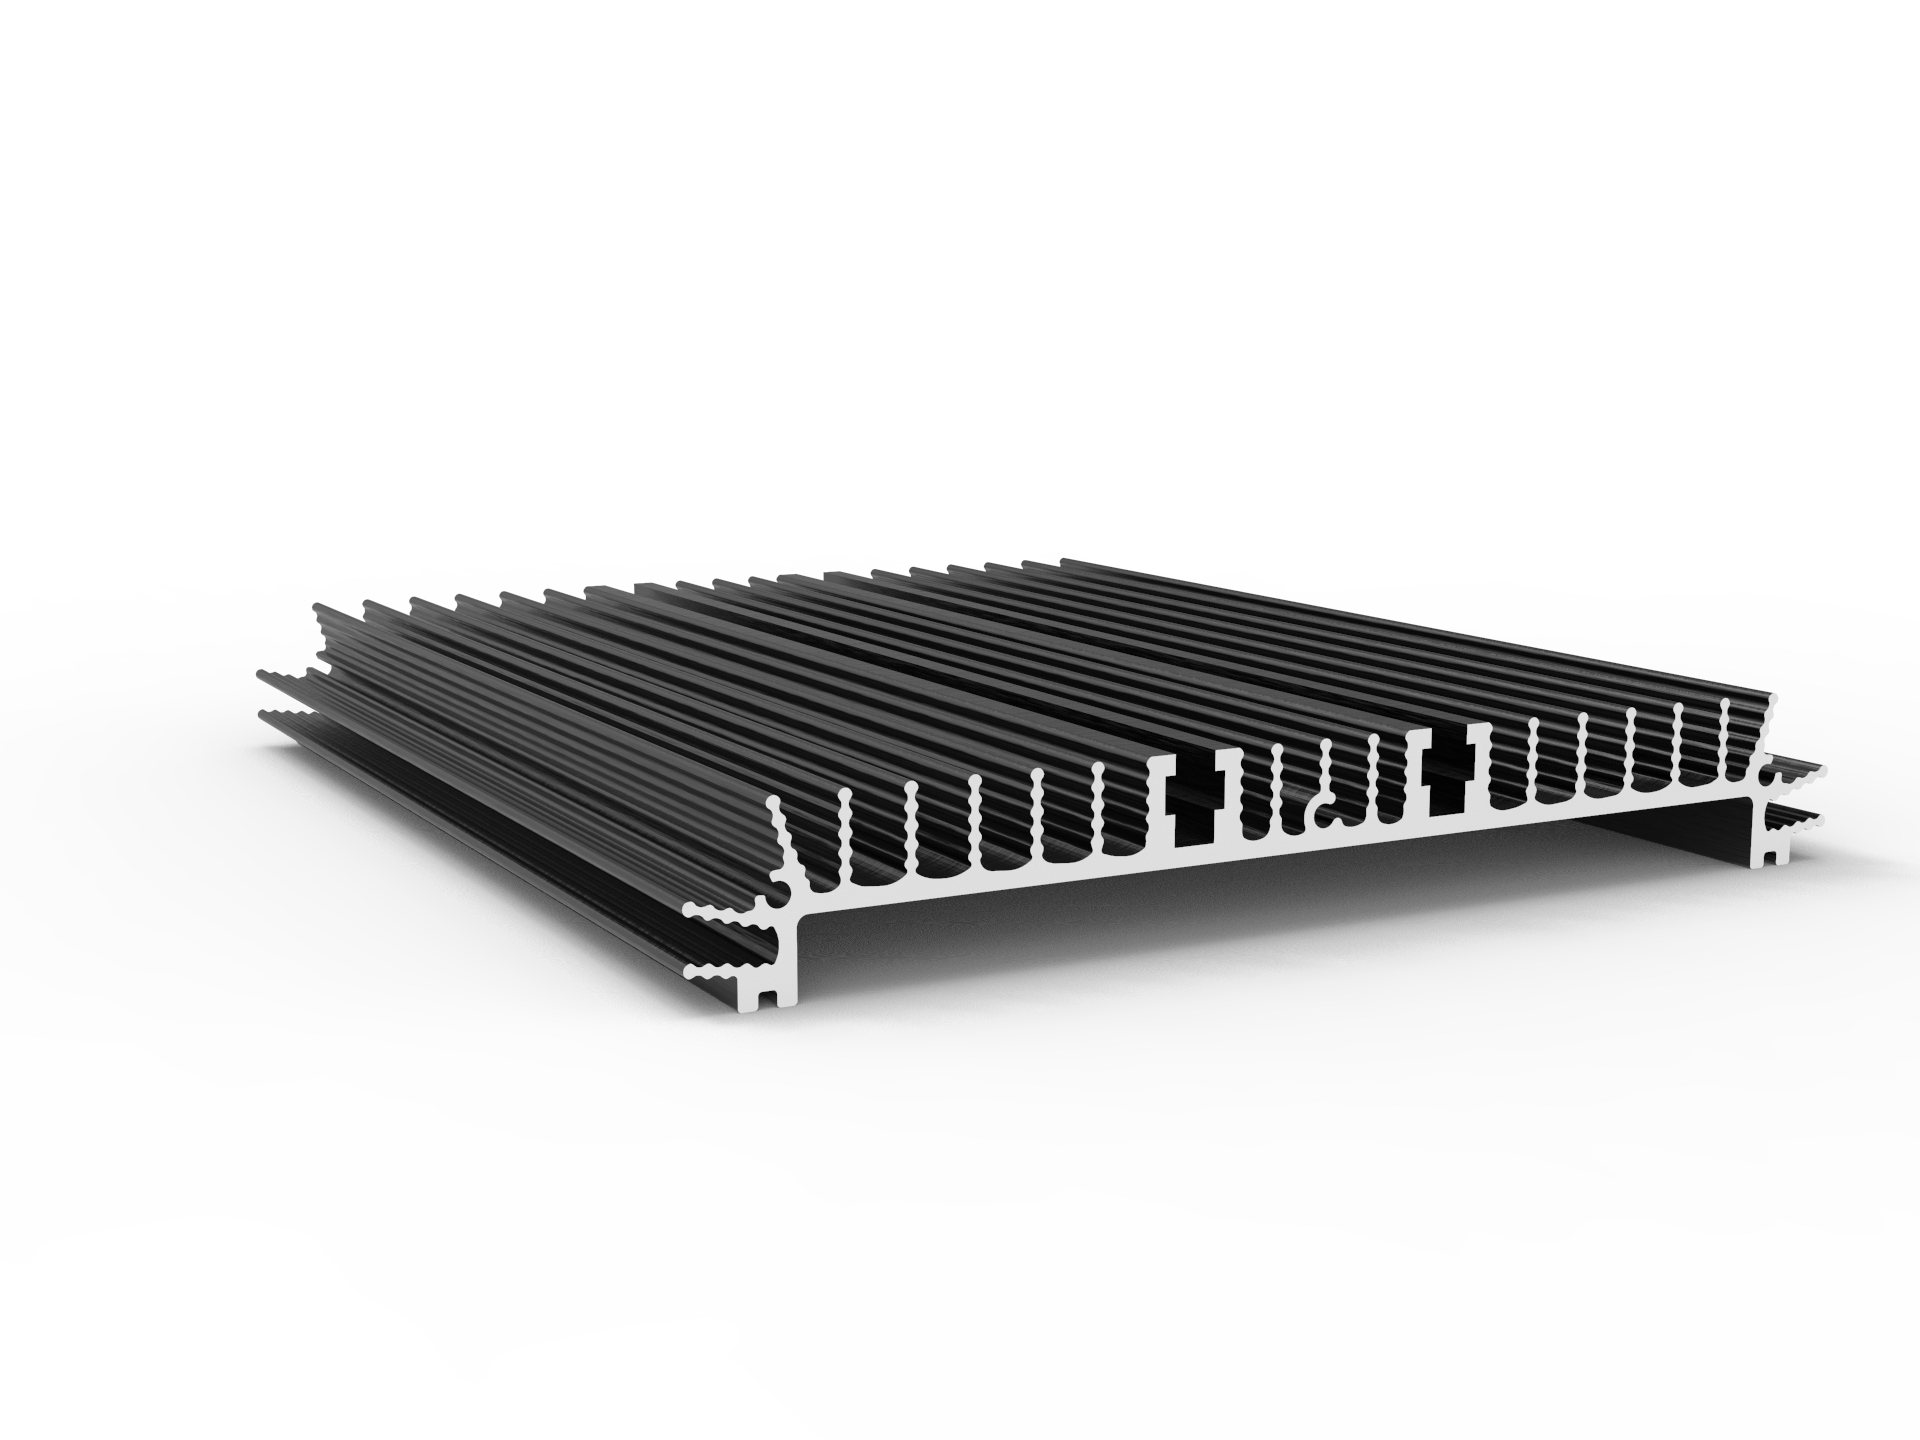
What alternatives to industrial profiles can reduce material costs without hurting strength?
Extruded Aluminium Profiles: Flexible Manufacturing for Diverse Customer Needs
Why Aluminium Curtain Walls Are Popular in Modern Architecture
How do I choose a decorative profile that stays stable in humid or harsh environments?
How do I choose an architecture profile that stays stable in harsh outdoor conditions?
How can I compare Awing window specs to avoid poor performance in harsh weather?
How can I compare Sliding door sizes and hardware ratings for harsh commercial environments?
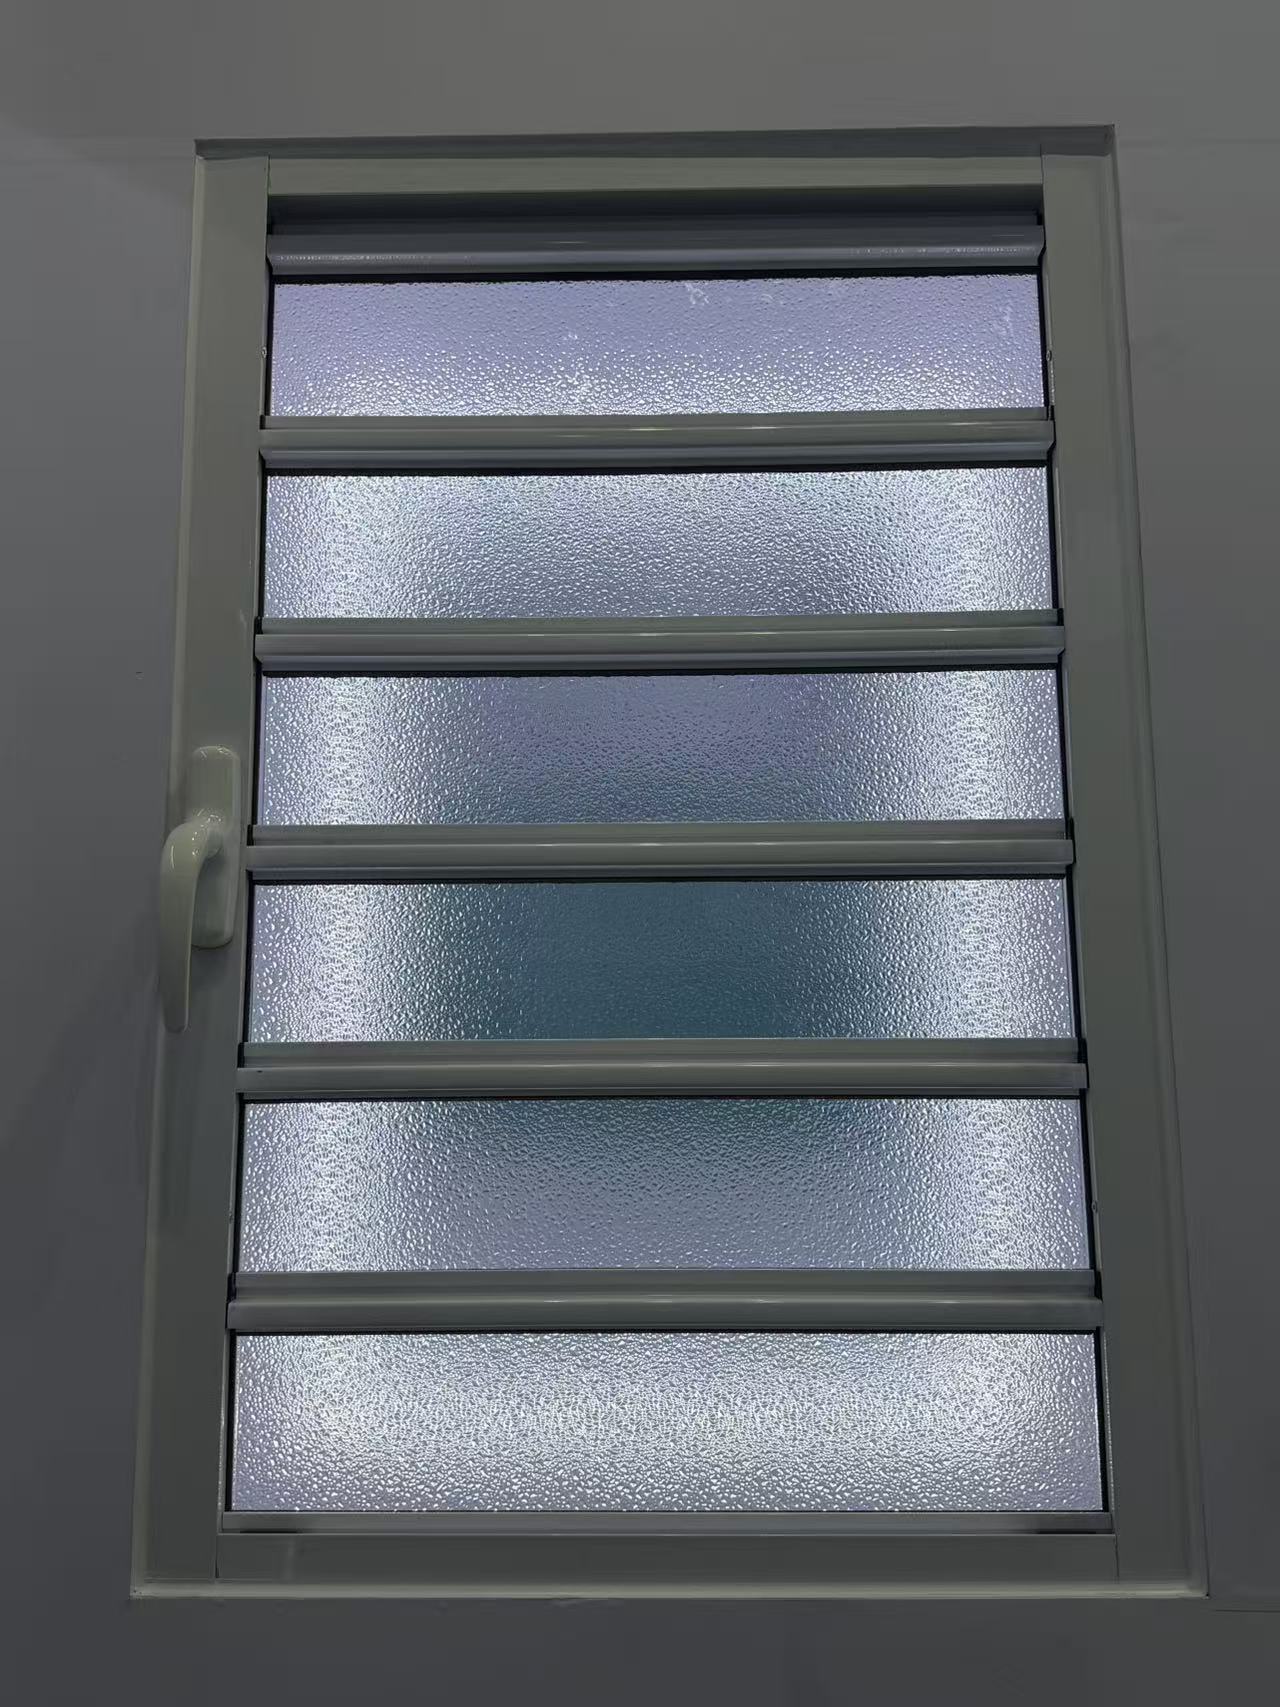
How do I choose the right shutter specifications for harsh climates without overpaying?
What eco-friendly alternatives to folding doors can cut costs without hurting durability?
How do I choose the right shutter specifications for harsh weather without overpaying?
What eco-friendly casement door materials can lower costs without hurting durability?
What newer materials can replace industrial profiles without raising costs or supply risks?
How do I choose a decorative profile that stays stable in humid, high-traffic spaces?
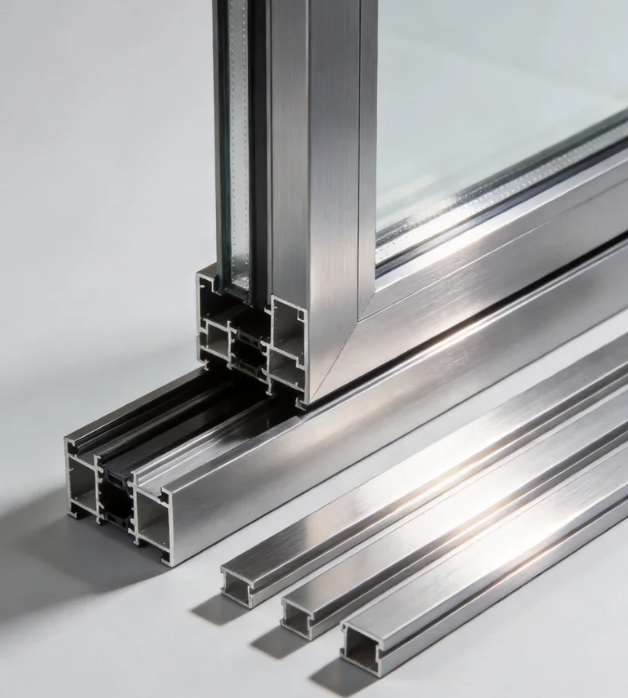
What sustainable material alternatives can replace aluminum architecture profiles?
What should I check in Awing window specs to ensure reliable performance in harsh weather?
How can I compare Sliding door sizes and thermal ratings for harsh climates before buying?
What newer materials can replace aluminum in awning windows without raising our costs?
How do I choose the right Sliding door specs for smooth operation in harsh environments?
How do I choose a folding door that stays stable in harsh weather and heavy daily use?
How can I choose the right shutter specifications for harsh weather and long-term use?
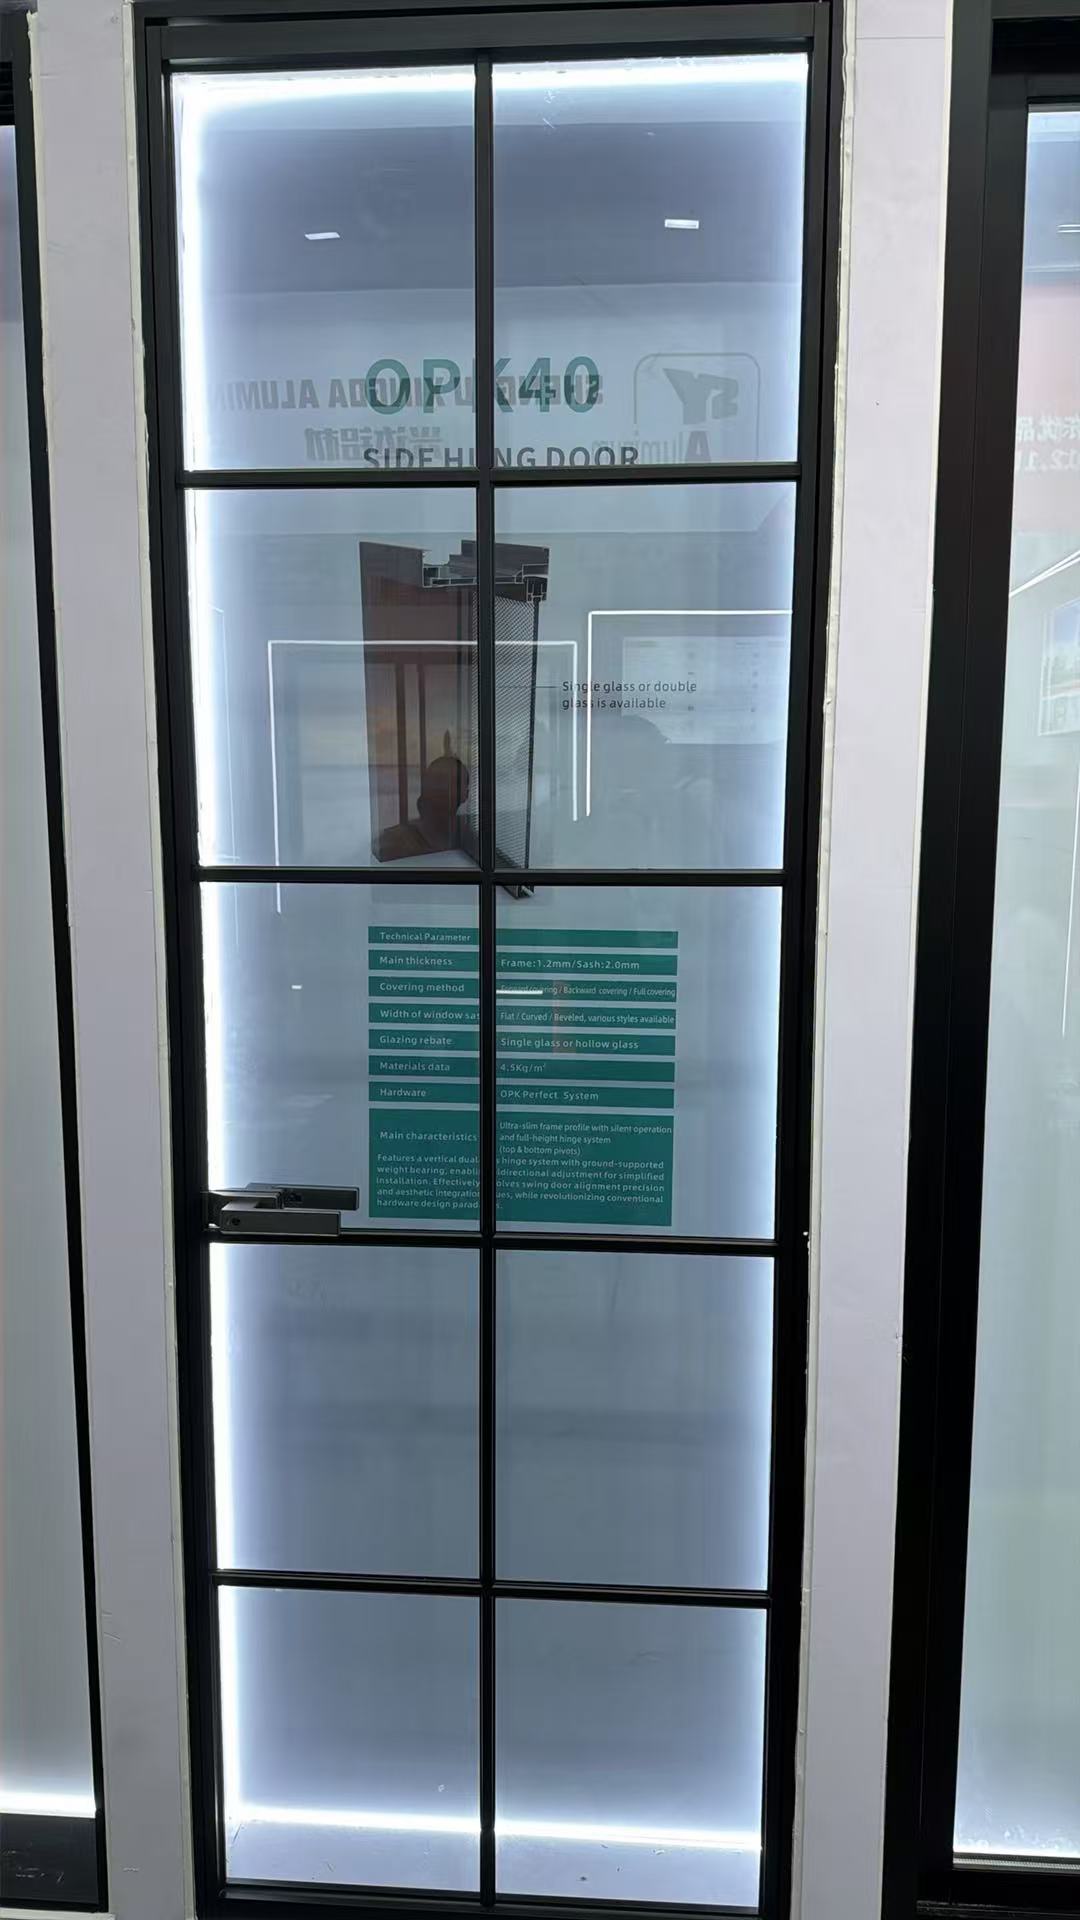
How do I compare casement door U-values, hardware, and weather sealing before buying?
How do I choose the right industrial profile size for strength and load needs?
How do I choose the right shutter specifications for harsh weather and long-term commercial use?
How do I choose the right Casement door size and hardware for harsh weather?
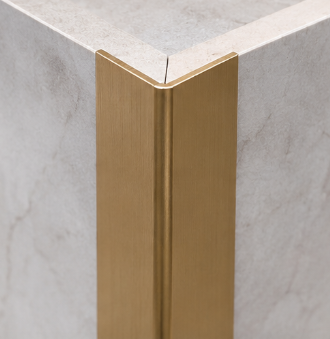
What greener alternatives to decorative profile can cut costs without hurting durability?
What lower-cost, eco-friendly materials can replace decorative profiles?
What lower-carbon alternatives to aluminum architecture profiles are practical for our project?
How can I compare sliding door systems for insulation, security, and long-term use?
What is the standard production lead time for bulk orders of folding doors?
How do I choose the right Awing window size and glass specification for harsh weather?
How can I test shutter samples so the final bulk order matches their quality and finish?
Can suppliers make custom double glass casement doors from my CAD drawings?
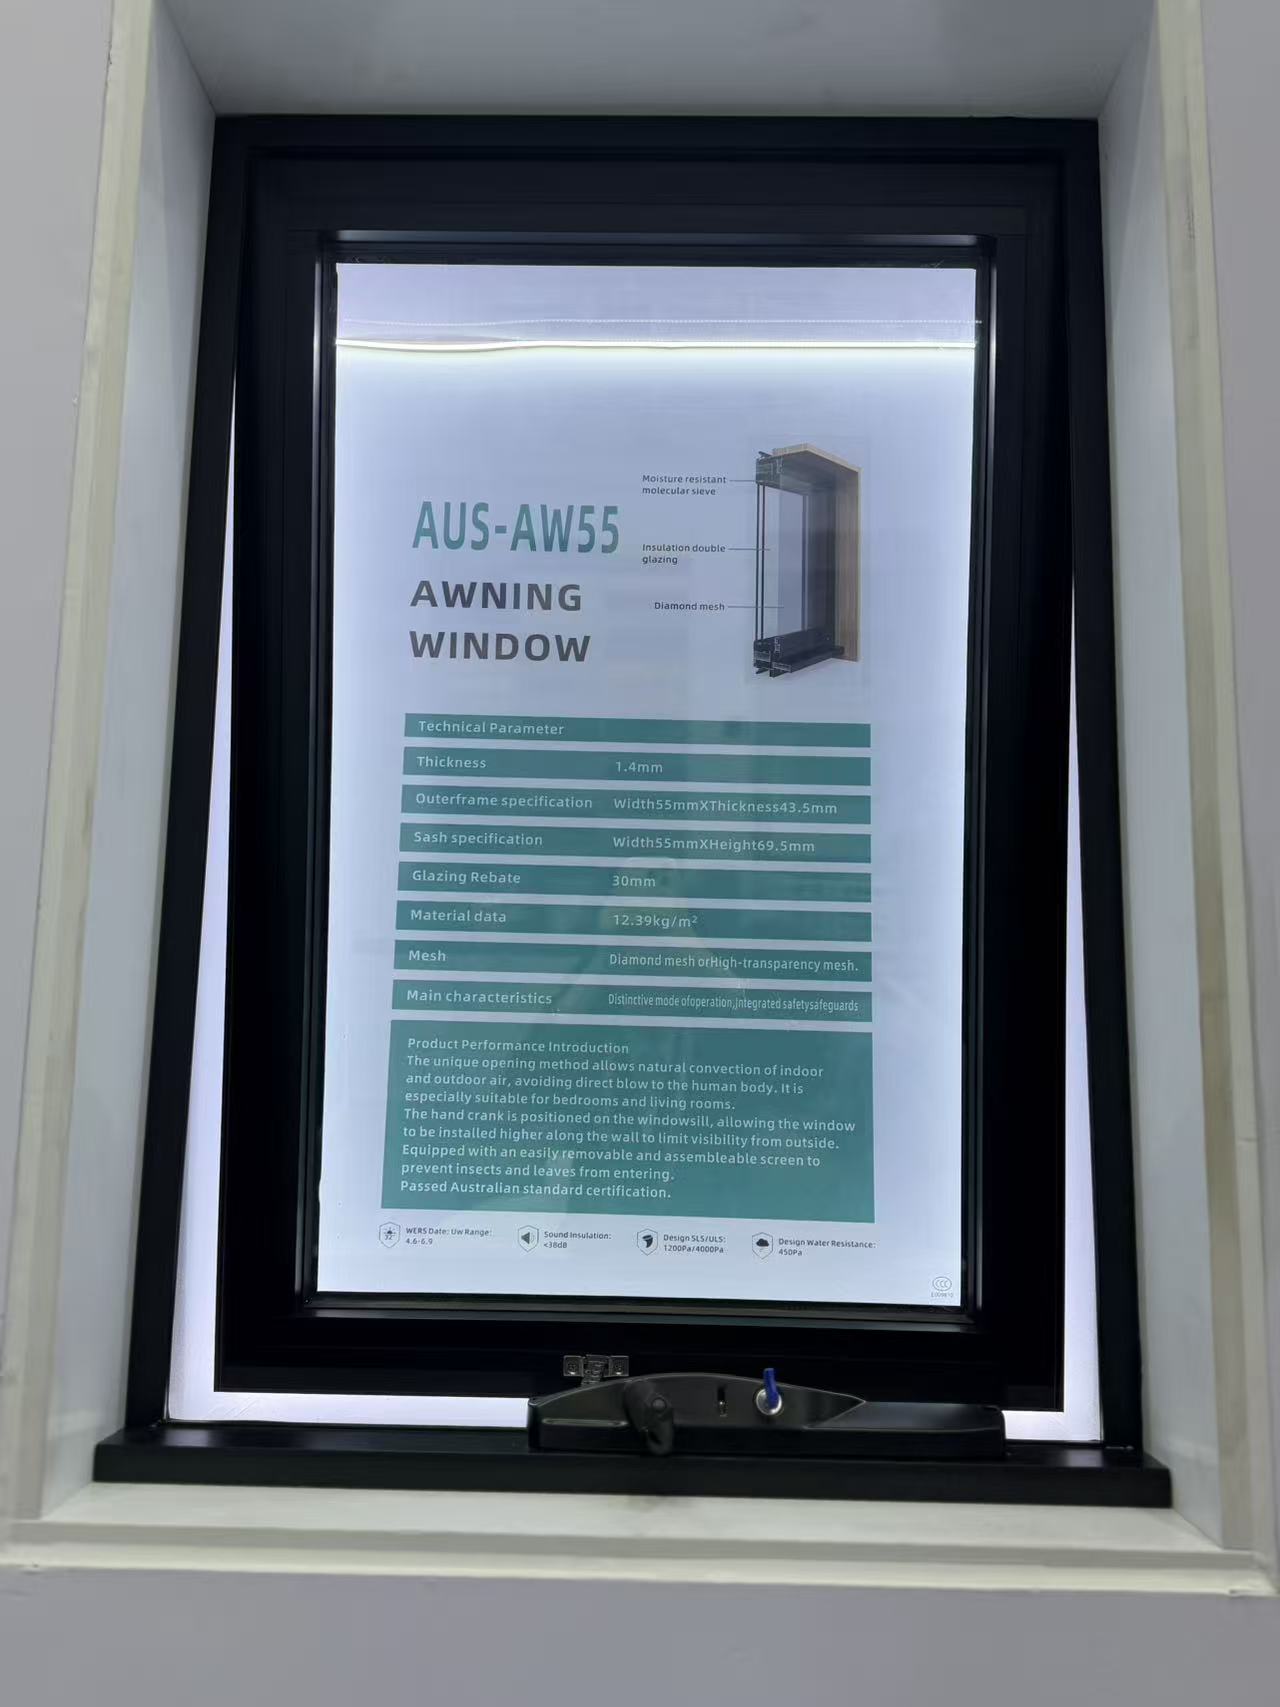
What safety certifications should I request when importing awning windows?
How long does it usually take a factory to make custom shutter samples?
What T-slot industrial profile size is best for a heavy duty machine frame?
How do I choose the right stainless steel decorative profile for high humidity areas?
How do I choose the right aluminum architecture profile for coastal buildings?
How do I choose the right stainless steel decorative profile for high humidity areas?
What wind load specs should I check for aluminum casement windows in coastal high-rises?
How do I know which aluminum industrial profile alloy is best for heavy machinery frames?
How do I choose the right alloy grade for aluminum architecture profiles?
How do I select the right heavy-duty hardware for exterior commercial floding doors?
How do I select the right glass thickness for bulk awing window orders?
What frame thickness is recommended for commercial aluminum casement doors?
What frame thickness is best for high-rise commercial sliding windows?
How to choose weather resistant aluminum floding door specs for commercial use?
How do I choose the best water tightness rating for commercial awing windows?
How do I choose the right frame material for commercial casement doors?
How do I choose the right wind load rating for sliding windows in coastal areas?
What is the best material for outdoor decorative profiles to prevent rust and fading?
How do I choose the right track thickness for high-traffic commercial sliding doors?
How do I choose between PVC and basswood shutters for high-humidity areas?
How do I choose between double and triple glazing for casement windows in cold climates?
How do I choose the right industrial profile thickness for heavy-duty cnc machine frames?
How do I choose the right alloy for outdoor architecture profiles to prevent corrosion?
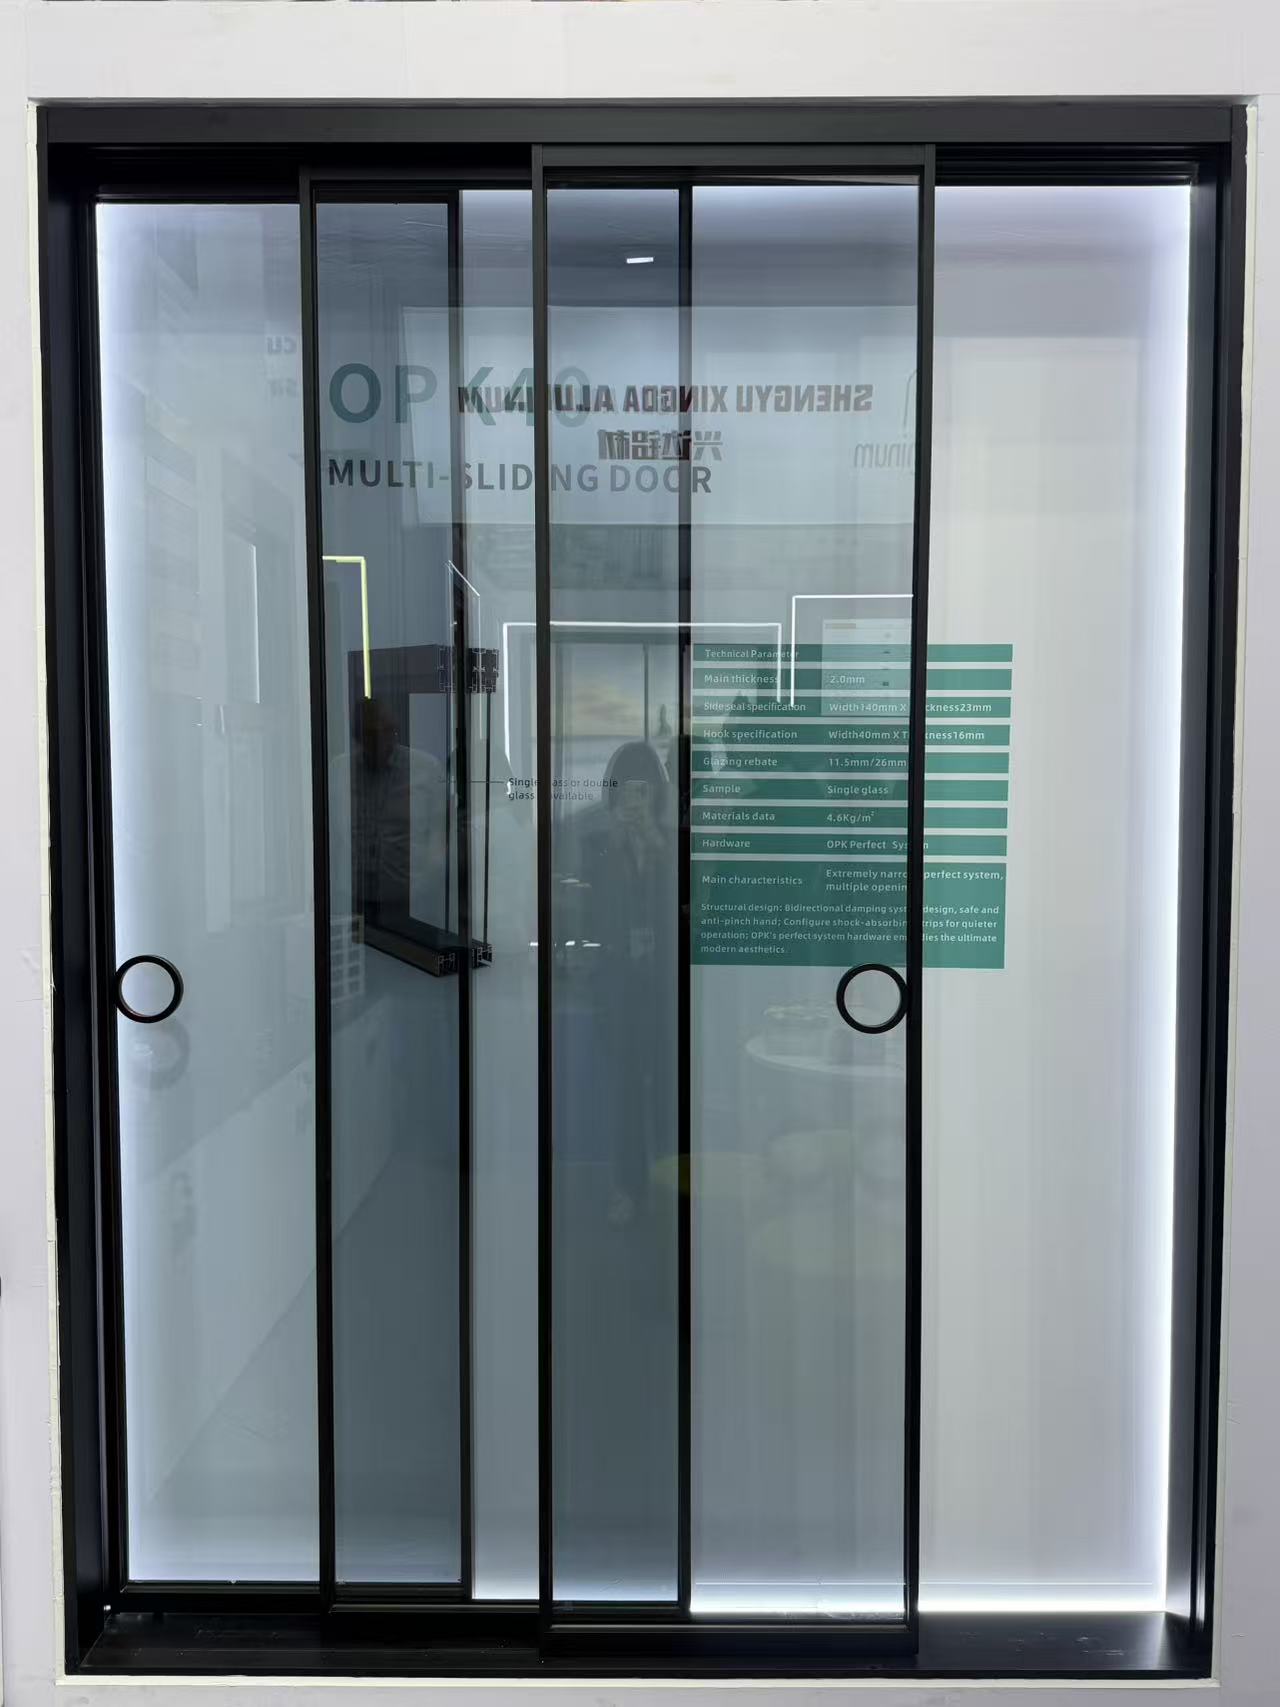
Can you design a slim frame profile for modern minimalist look?
How do I choose the right wind-resistant floding door for a coastal commercial building?
What key specs ensure a casement window can withstand heavy rain and high winds?
How do I choose the right aluminum alloy grade for heavy-duty industrial profiles?
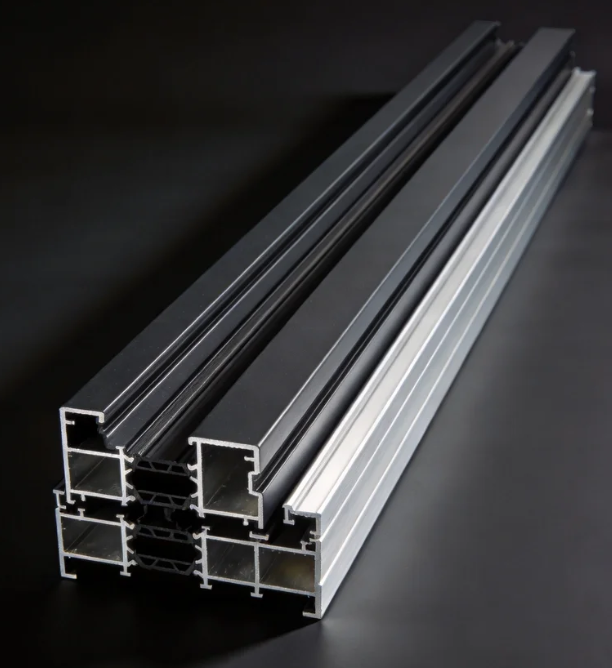
Which alloy grade of architecture profile is best for coastal areas to resist rust?
How do you pack windows to prevent glass breakage in transit?
Are slim-frame thermal break systems replacing traditional ones?
Does the price include the matching frame and installation kit?
How do you protect our proprietary design drawings from leaks?
How do I choose the right decorative profile for high-traffic hotel lobbies?
Is your factory the actual manufacturer or a trading partner?
Is it possible to 3D print a prototype before cutting steel?
Do you outsource any part of the painting process to others?
How do you handle replacement parts for damaged track rollers?
Do you accept escrow payments through third-party platforms?
Do you have ISO 9001 certification for your production line?
Are there extra fees if we pay via bank telegraphic transfer?
What is the price difference between powder coat and anodized?
What is the warranty period for the lock and hinge hardware?
What is your policy for dimensional deviations in the batch?
What happens if the shipment is delayed due to factory error?
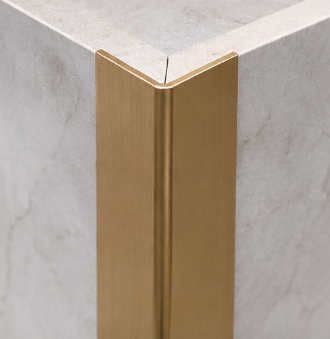
Do you offer online technical support if color fading occurs?
Is it possible to engrave our brand logo on the tension screw?
Do you offer credit terms for long-term purchasing partners?
Can you palletize the shipments for easy forklift unloading?
What are the latest eco-friendly finish trends for decorative profiles in modern interior design?
What are the tooling cost and design limitations for customizing heavy-duty industrial profiles?
Has your architecture profile manufacturing facility passed ISO 9001 certification?
Can we use Alibaba Trade Assurance for our initial sliding door order to mitigate risk?
Do you provide free corner samples of the casement window frame for color verification?
Is it possible to custom-match a specific RAL color for a decorative profile order?
Can I request a 3D-printed sample before ordering a custom industrial profile mold?
Can you extrude an architecture profile based on our proprietary CAD drawings?
What thermal performance certifications does a sliding door need for the UK market?
How are heavy floding door panels crated to ensure safe unloading at the job site?
Can we arrange our own freight forwarder to pick up the casement door shipment FOB?
What is the estimated ocean freight transit time for a shutter shipment from China to Europe?
How can we source replacement seals for your awing window models in the future?
How are sliding windows typically packaged to prevent glass breakage during ocean transit?
What is the average lead time for a 40ft container of standard aluminum casement windows?
Are there any extra tooling fees if my decorative profile order doesn’t meet the MOQ?
Can I get 3D printed prototypes of custom architecture profiles before committing to mold tooling?
How is smart glass technology being integrated into modern residential sliding door units?
What options do you have for customizing the threshold height of an aluminum floding door?
What thermal break technology should I look for in a heavy-duty aluminum casement door?
What quality control processes do you perform on shutter hardware before final assembly?
Do you offer DDP shipping terms for awing window orders delivered to our warehouse?
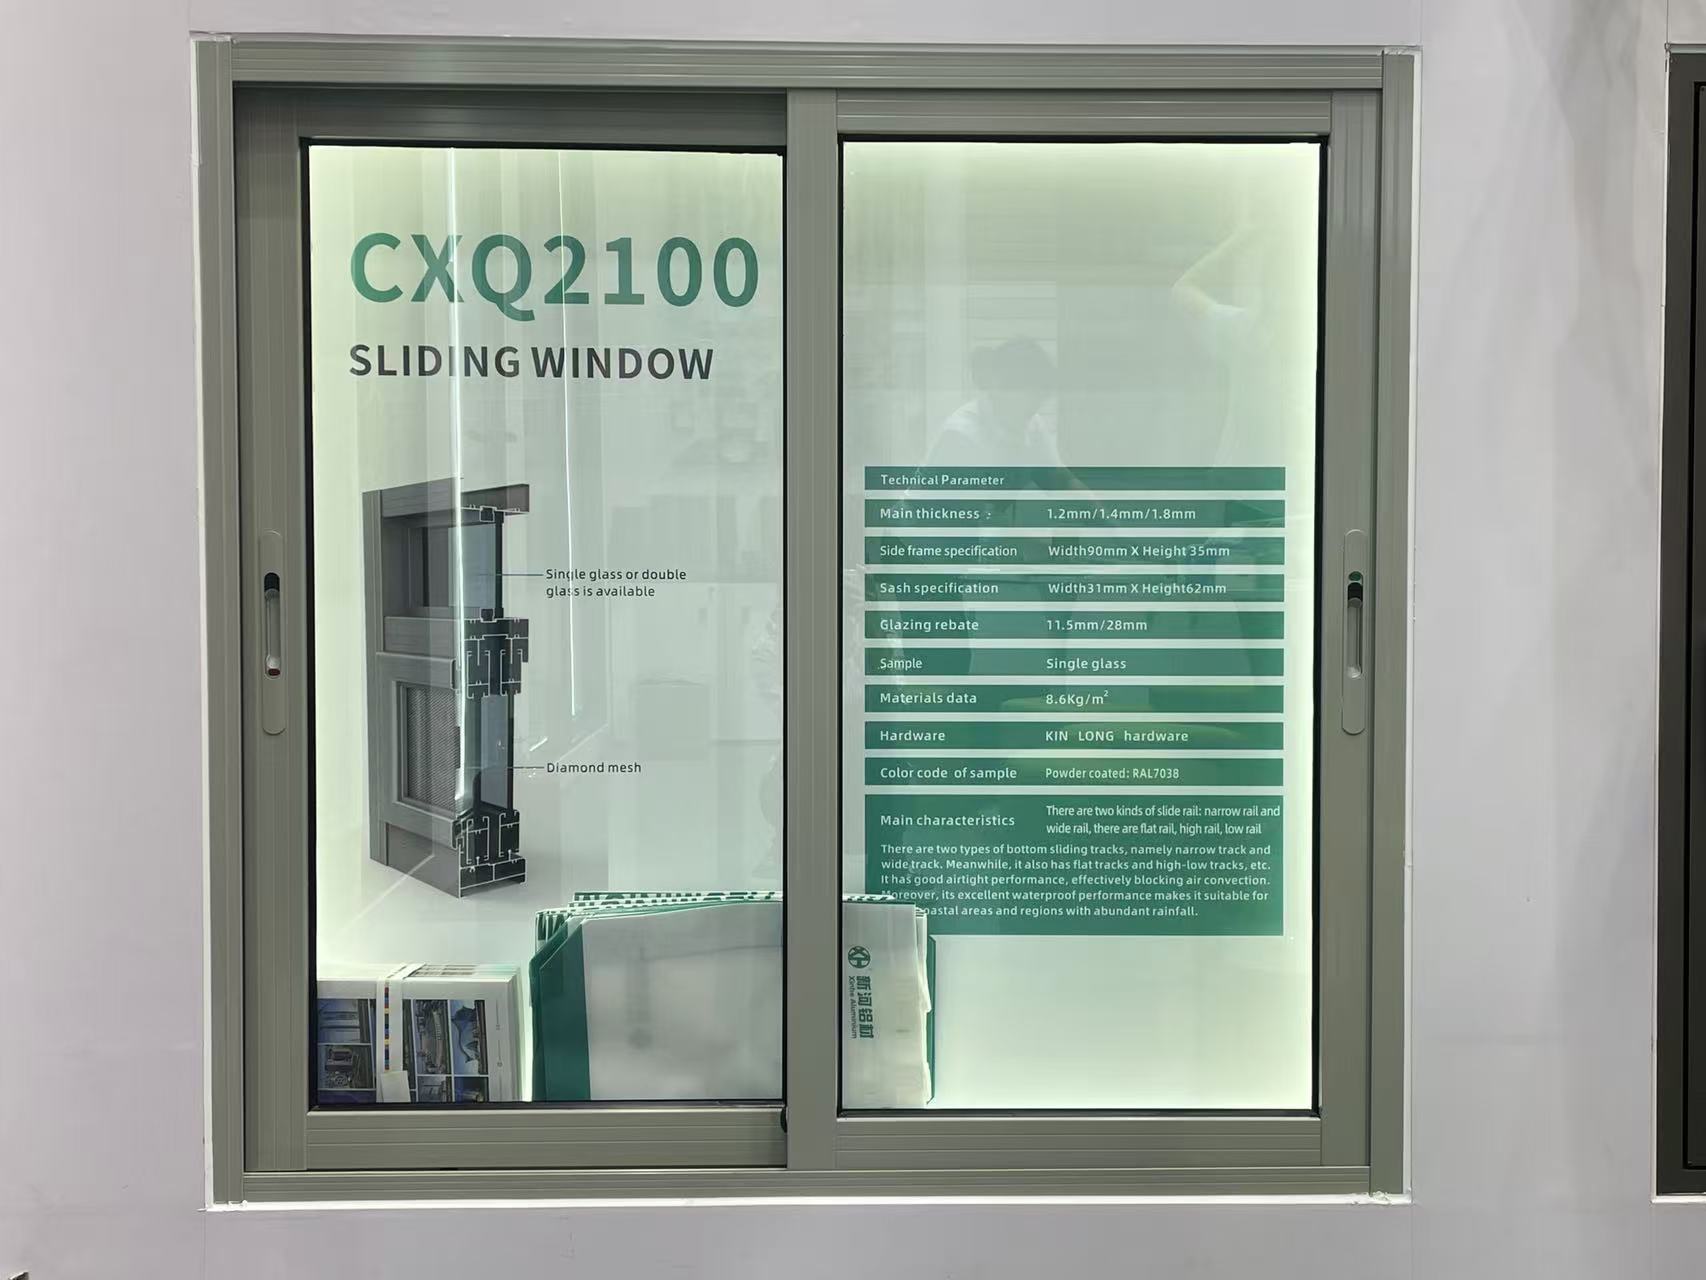
Is it possible to order a fully functional sliding window sample for mock-up testing?
Do you provide replacement hardware if the casement window hinges fail within 5 years?
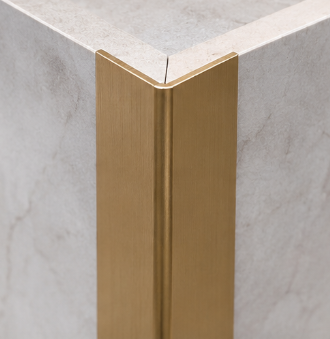
How do you handle claims for decorative profile items damaged during transit?
What is the standard MOQ for custom-extruded aluminum industrial profile orders?
How does the order volume affect the per-ton price of custom architecture profile designs?
What is the warranty period for the rollers and tracks on your heavy-duty sliding doors?
How can we secure our deposit when purchasing high-value custom floding doors from a new supplier?
Can your factory match custom anodized colors for decorative profiles based on physical samples?
Is there a lighter alternative to aluminum industrial profile structures for robotics?
What payment security measures do you have for custom architecture profile tooling fees?
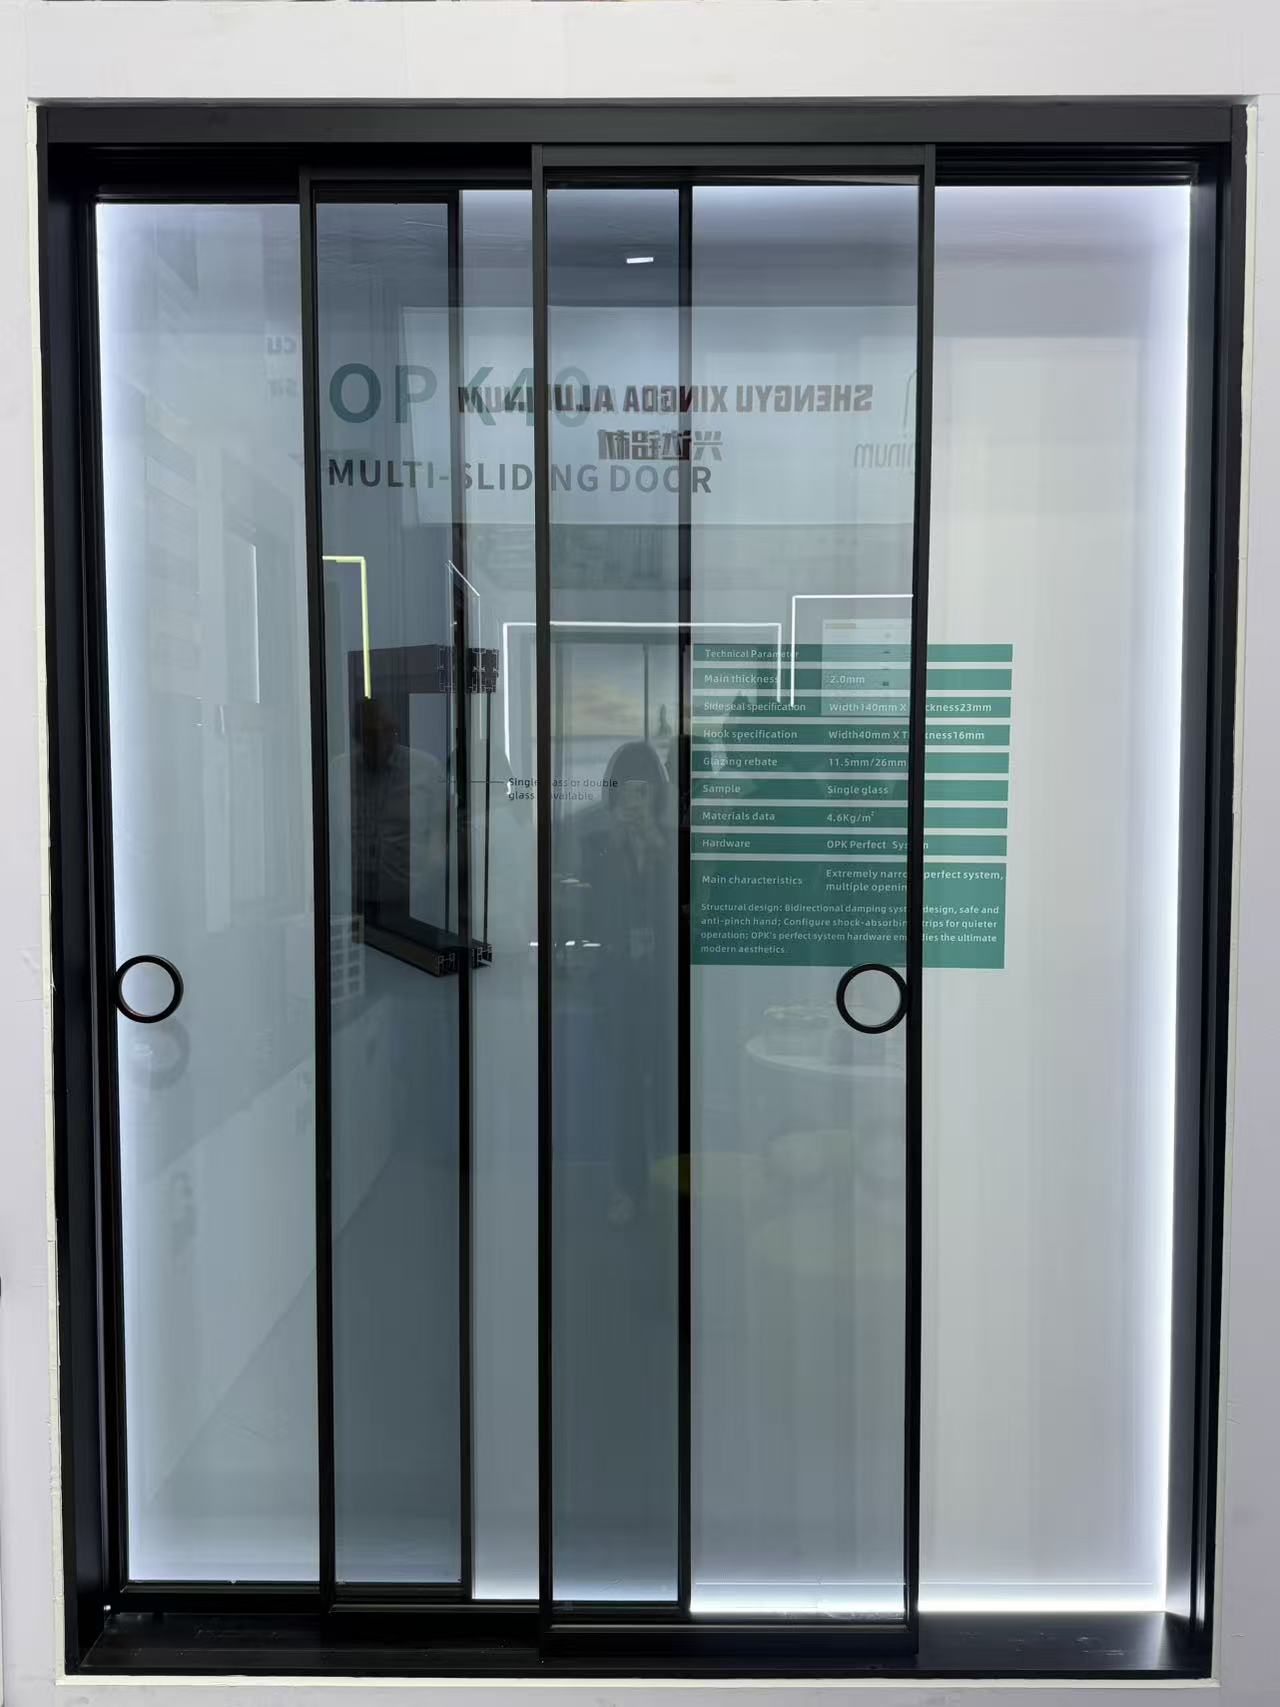
Can I order a sliding door with custom grid patterns between the glass panes?
How do you protect buyers against financial loss if the floding door shipment is delayed?
Are slim-frame aluminum casement door designs becoming more popular in modern offices?
What is your policy for replacing shutter components that arrive with color mismatch?
What kind of remote technical support do you offer for sliding window installation?
What is the maximum safe size for a top-hung awing window in commercial projects?
What environmental management standards does your decorative profile plant follow?
What is the standard lead time for producing a 40ft container of casement window orders?
What is the warranty period for the anodized finish on your industrial profile?
What are the latest eco-friendly trends in architecture profile manufacturing?
What is the average wholesale price per square meter for double-glazed sliding door systems?
How do I calculate the structural load requirement for a 5-panel exterior floding door?
Do your exterior shutter systems comply with Florida building codes for hurricane protection?
Do you offer Letter of Credit (L/C) payment options for casement door bulk orders?
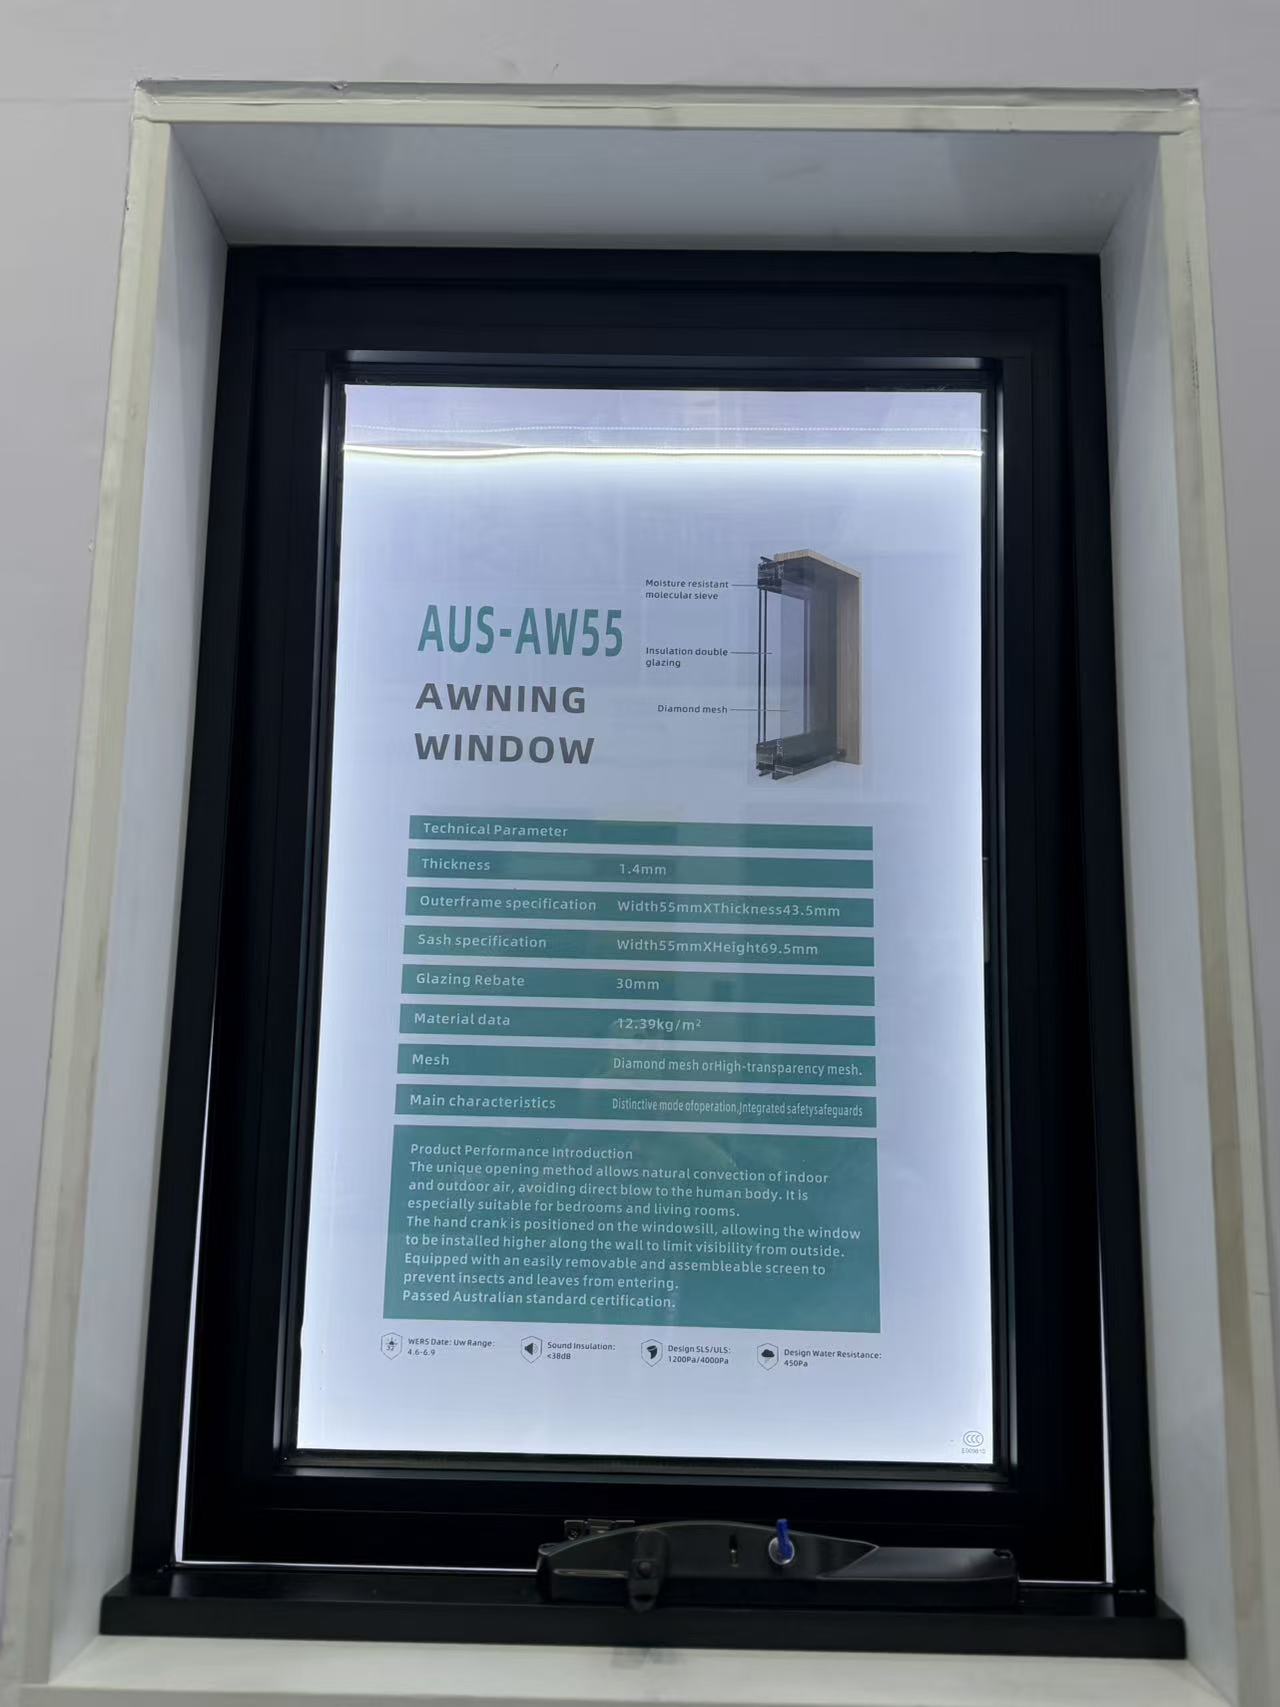
Which water tightness certifications are required for importing an awing window to Europe?
Do you allow virtual factory tours to inspect the sliding window assembly line?
What is the typical MOQ for ordering standard-sized aluminum casement window units?
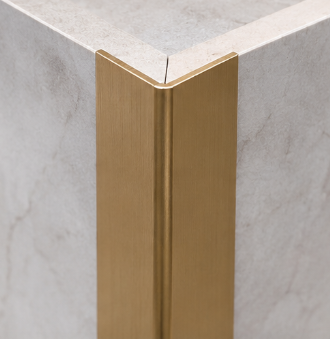
How long does it take to receive a physical sample of a gold-anodized decorative profile?
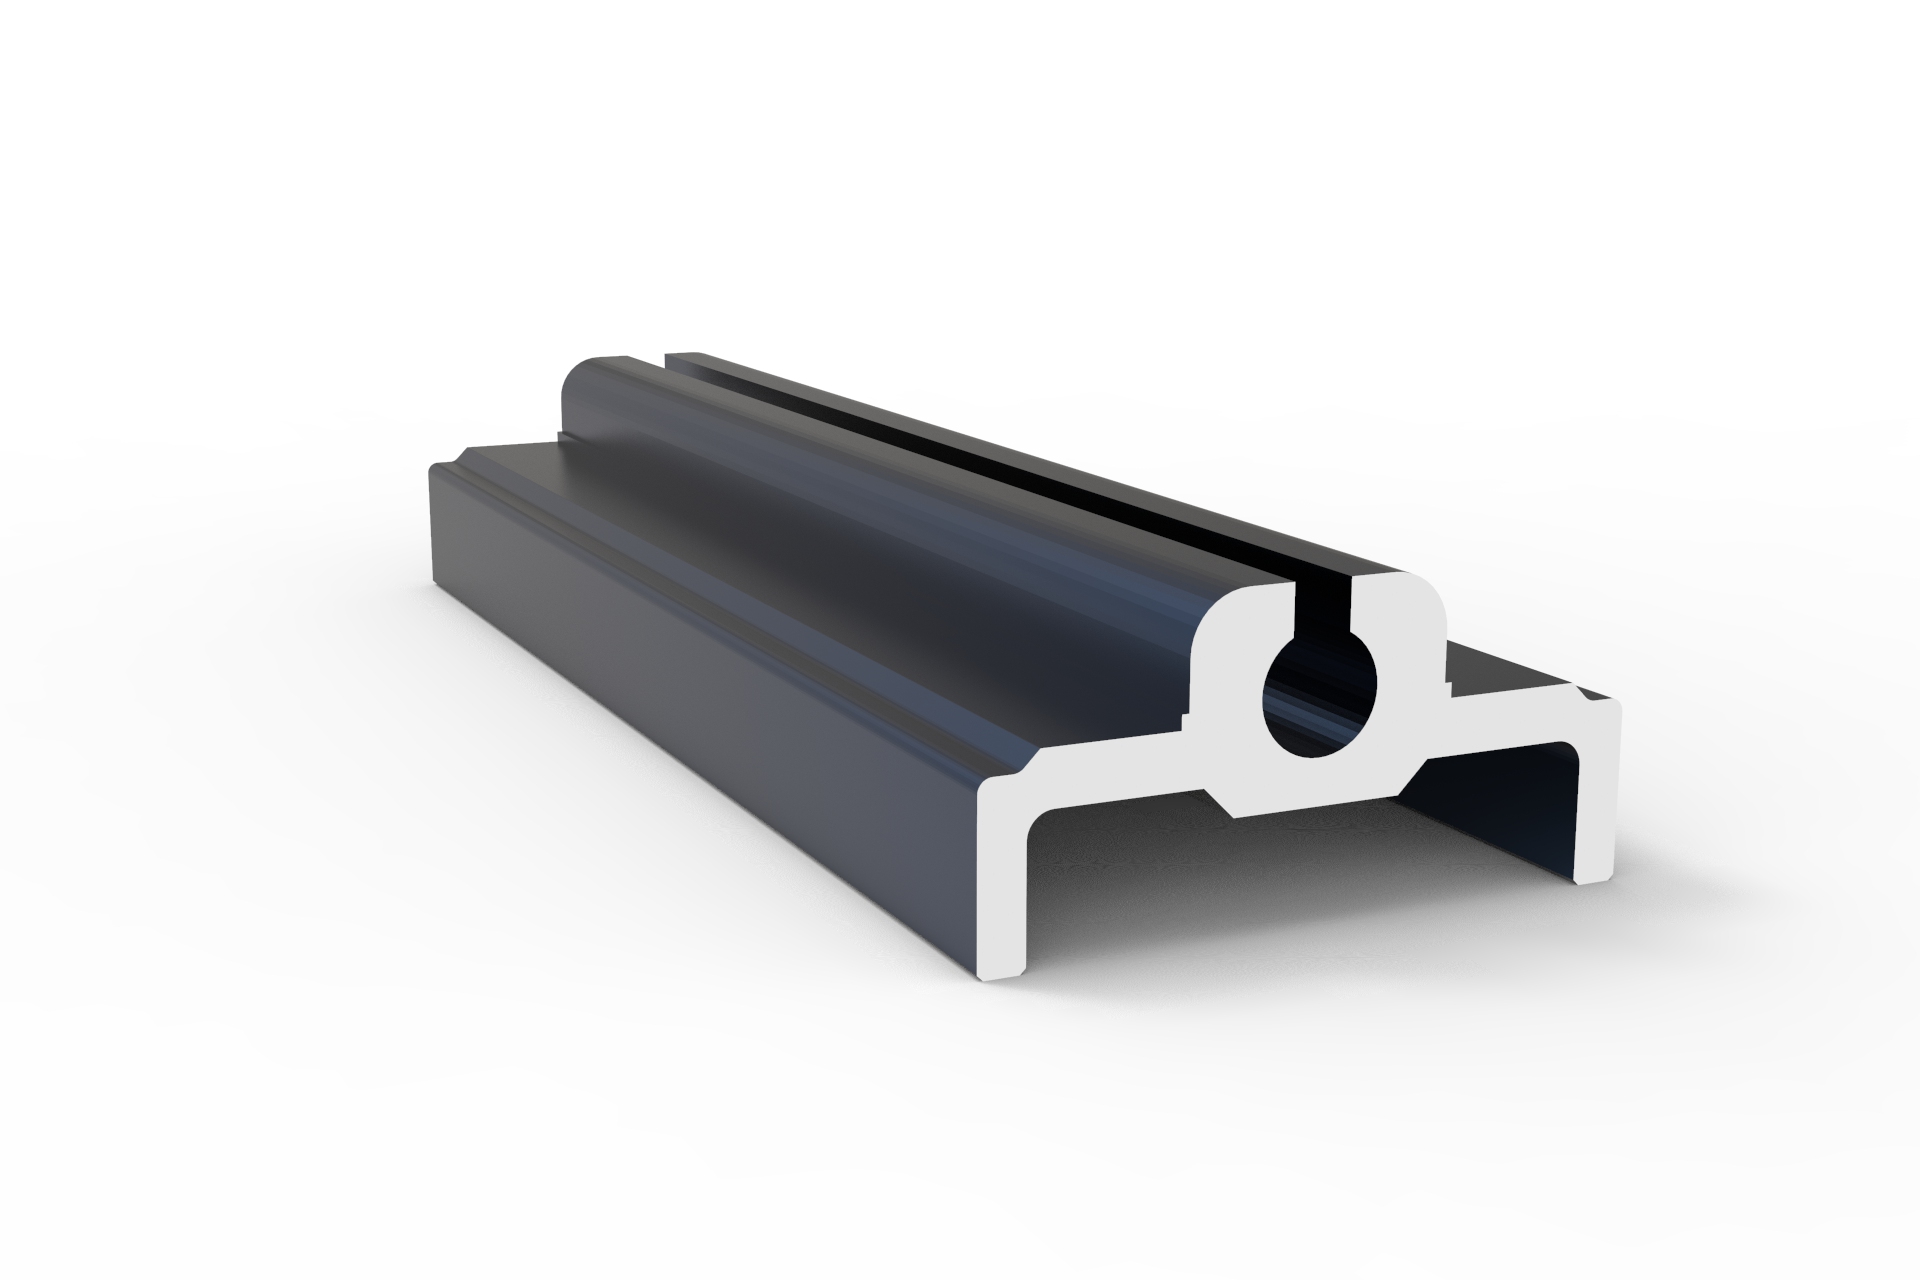
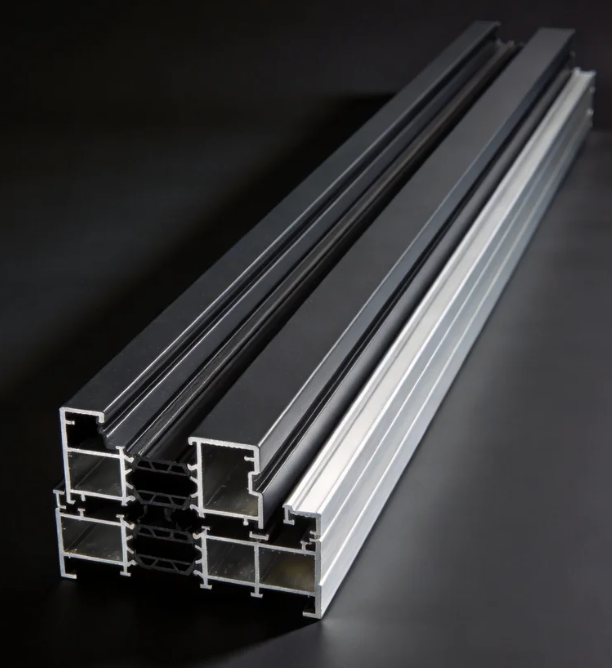
How do I choose the right alloy grade for architecture profiles in high-rise coastal buildings?
How do I choose the right track and roller specs for heavy-duty commercial sliding doors?
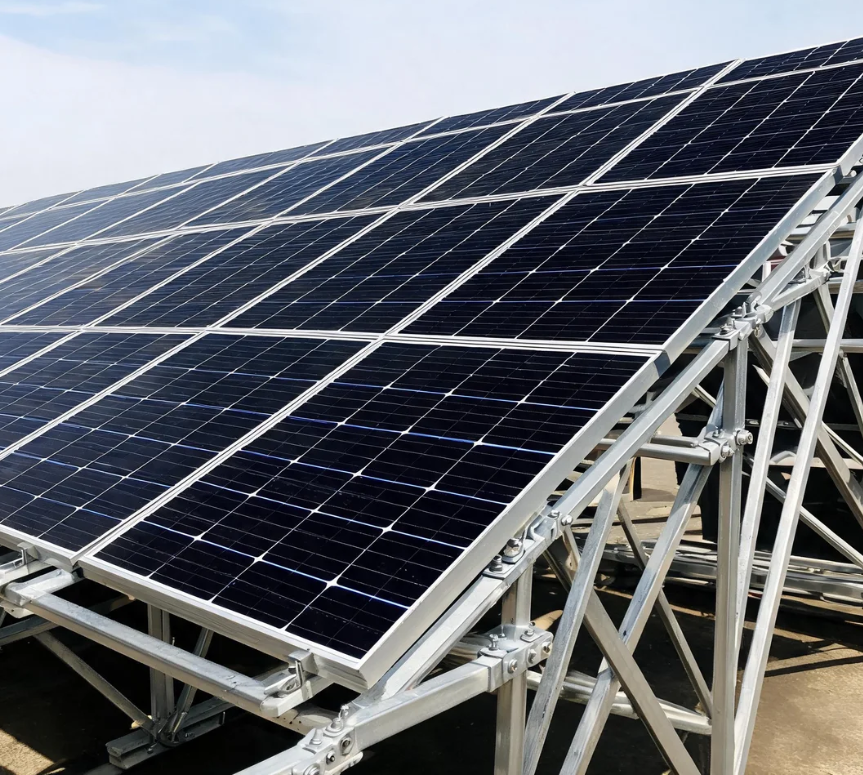
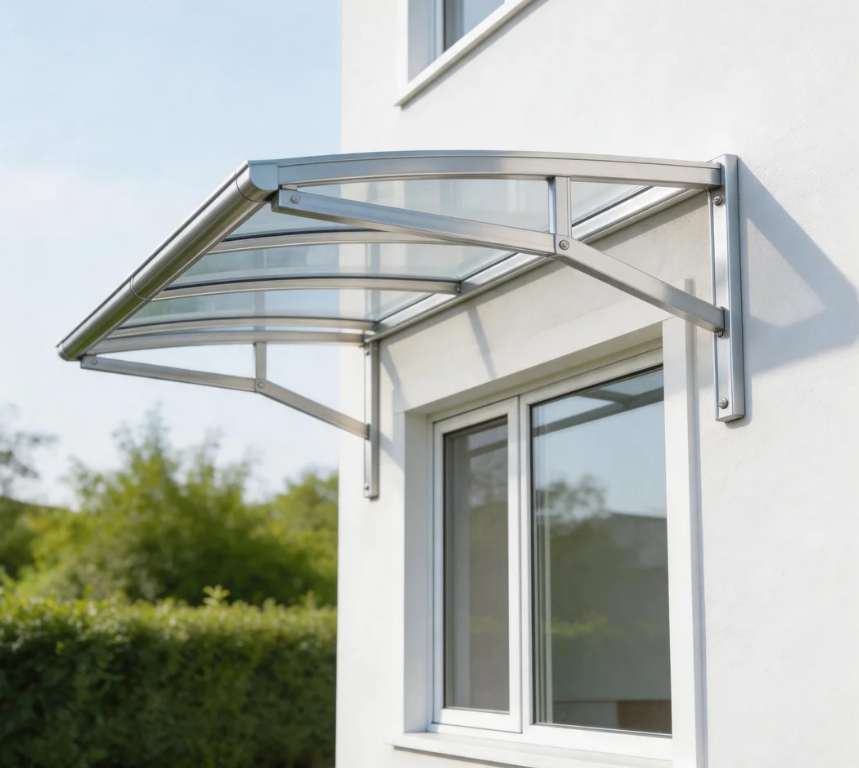
The core advantages of using aluminium profiles for the canopy
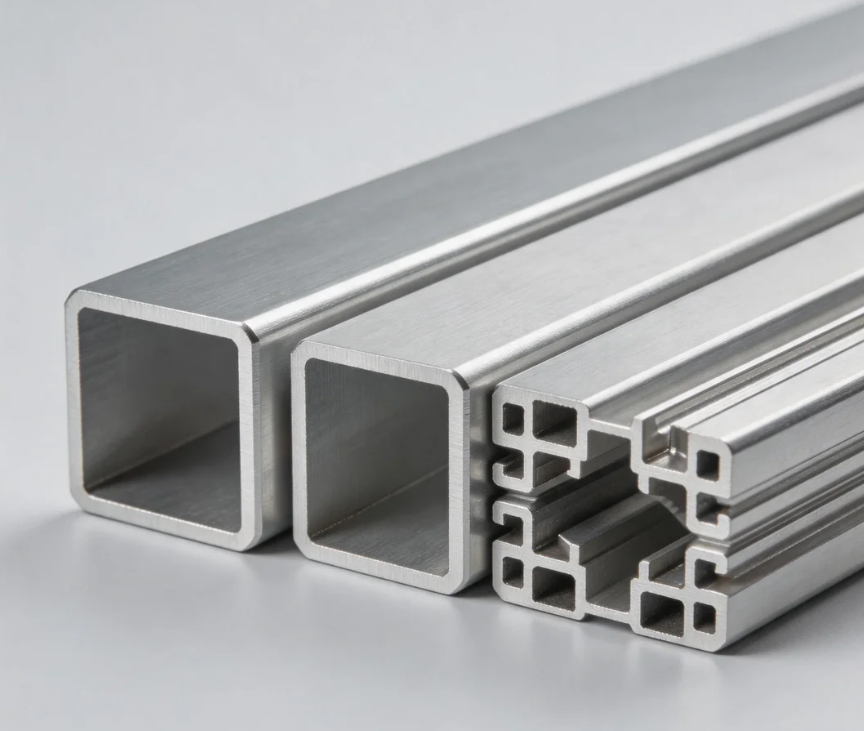
International demand: Dual drive by new energy and infrastructure
The advantages of using aluminium profiles to manufacture robot arms
The advantages of using aluminum profiles for door and window frames
The impact of the conflict between the United States and Iran on the price of aluminum
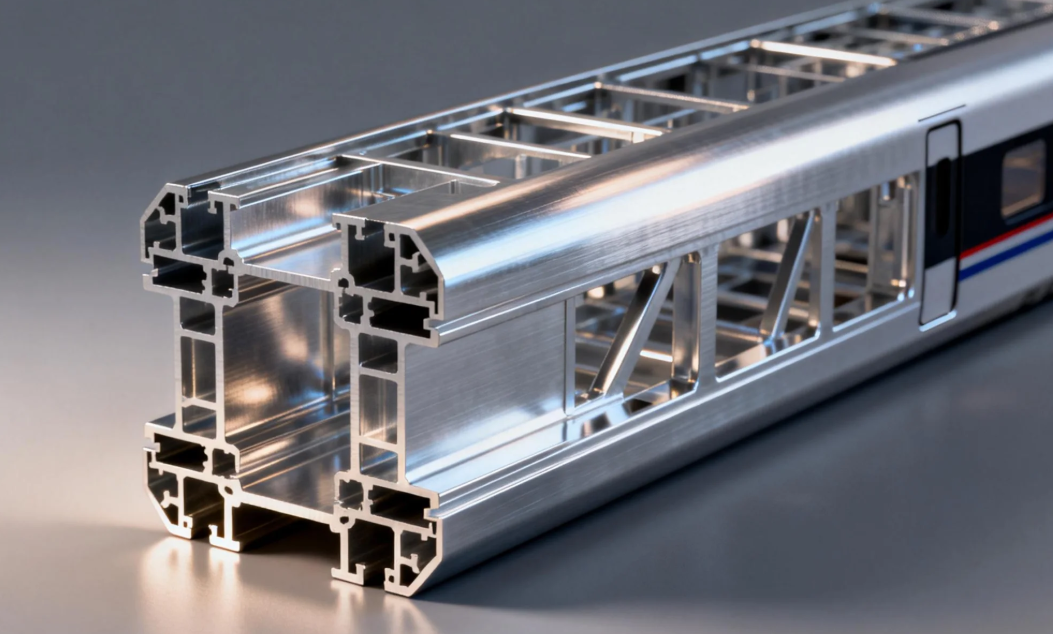
The advantages of using aluminium alloy for the main structure of high-speed train carriages
Methods for distinguishing Indoor and Outdoor Aluminium Doors
Maintenance methods and tips for aluminium doors and windows
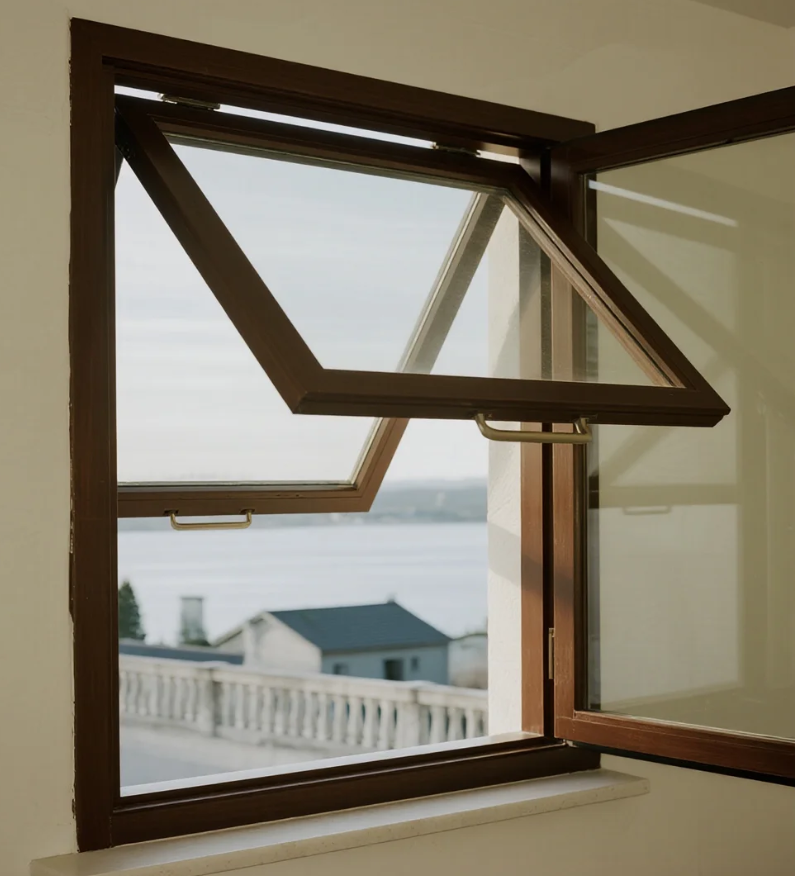
Characteristic of outward-opening and hung aluminium windows
Xinhe Aluminium Research: 7.14-7.18 Analysis of Aluminium Prices
Seven Benefits Of Using Aluminium Profiles In Curtain Wall Systems
The Application of Aluminium Profiles in New Energy Vehicles
The Composition and Application of Series 6 Aluminium Alloys
Top 5 Benefits of Using LED Aluminium Profiles in Modern Lighting
A Complete Guide to Aluminium Frame Profiles for Modern Structures
Exploring the Strength and Versatility of Aluminium Extrusion Profiles
How to Choose the Right Aluminium Profile Supplier for Your Project
COMPANY