Machine builders rarely think about aluminium until a frame starts to flex under load or a sliding axis begins to bind after a few thousand cycles. Aluminium extrusion for machinery sits at the center of these problems, because the structural member you choose decides whether a machine stays accurate for ten years or needs recalibration every few months. Picking the right profile is less about buying metal and more about engineering a stable foundation for motion, heat, and repeated mechanical stress.
Steel still dominates heavy construction, but machinery design has different priorities. Weight matters because gantries, moving beds, and robotic arms accelerate and decelerate constantly, and lighter structures reduce inertia and motor load.
Aluminium also resists corrosion without the painting and maintenance steel demands, which matters in workshops with coolant mist or humidity. Extrusion, unlike steel fabrication, produces complex cross-sections in a single pass. A profile can include built-in cable channels, mounting slots, and reinforcing ribs molded directly into the shape, removing the need for welding or secondary machining.
This is why 6000-series aluminium alloys, particularly 6063 and 6061 grades, became the default choice for structural frames in CNC equipment, packaging lines, and laser processing systems.
A machine frame that looks fine on a drawing can still fail in operation if it twists or vibrates under load. This is the single biggest reason OEM engineers obsess over extrusion tolerances.
When a gantry beam flexes even half a millimeter during a cutting pass, that error transfers directly into the finished part. Linear guide rails mounted on an uneven surface wear unevenly, and bearings begin to bind within months instead of years. The root cause is almost always traced back to inconsistent wall thickness or poor straightness tolerance in the original extrusion.
High-precision extrusion manufacturing addresses this by holding tight dimensional tolerances and producing smooth surface finishes along the full profile length. A straighter, more uniform beam means the moving axis stays parallel to its reference surface, which translates into repeatable, vibration-free motion over the machine’s working life.
Laser cutting, in particular, generates intense localized heat that steel structures absorb slowly and release even more slowly. Aluminium behaves differently, and that difference is not cosmetic.
Aluminium’s thermal conductivity is roughly four times that of structural steel. In a machine gantry, this means heat generated near the cutting head disperses across the structure rather than concentrating at one point. That matters because concentrated heat causes localized expansion, and localized expansion is what throws a cutting head out of alignment mid-job.
For OEMs building laser cutting systems, this thermal behavior is not a bonus feature, it’s a prerequisite. A frame that cannot shed heat quickly will drift dimensionally during long production runs, and drift is the enemy of precision cutting. Profiles engineered for this environment are expected to disperse heat fast enough to prevent thermal deformation during sustained high-temperature operation.

A lower-grade aluminium extrusion might save a few percent on material cost, but that saving rarely survives contact with a factory floor. Mechanical components mounted on a soft or inconsistent alloy wear faster, and replacing worn linear guides is far more expensive than the extrusion itself.
Premium 6000-series alloy compositions reduce wear on contact surfaces over extended operating periods, which directly extends the service interval of bearings, carriages, and slide blocks. Combined with resistance to oxidation and surface corrosion, this is why the alloy grade specified on a drawing matters just as much as the cross-sectional shape.
Think of it the way a machinist thinks about tool steel versus mild steel. The upfront price difference looks small, but the downstream maintenance cost is where the real number lives.
Not every structural member on a machine does the same job, and treating them as interchangeable is a common design mistake. Different parts of a gantry system face different mechanical demands:
A single extrusion family rarely covers all four needs well, which is why serious OEM suppliers offer modular profile ranges rather than one universal beam.

| Alloy / Temper | Typical Strength Profile | Best Suited For |
|---|---|---|
| 6063-T5 | Moderate strength, excellent surface finish | Enclosures, panel framing, light structural members |
| 6063-T6 | Higher strength than T5, good extrudability | General machine frames, cable channels, modular structures |
| 6060-T6 | Balanced strength and formability | Mid-weight structural components, mounting brackets |
| 6061-T6 | Highest strength of the three, good fatigue resistance | Gantry beams, load-bearing chassis, high-stress frames |
Choosing between these isn’t about picking the "strongest" option by default. A 6061-T6 beam is excellent for a heavily loaded gantry, but it adds unnecessary cost if you’re only building a lightweight enclosure panel.
Surface finish on a machinery profile does functional work, not just cosmetic work. An anodized surface adds a hard oxide layer that resists abrasion where cables or panels slide against the frame repeatedly. Powder coating adds a thicker protective barrier suited to workshops with coolant exposure or washdown cycles. Electrophoresis coating, often chosen for its uniform thin-film finish, works well on complex profiles with internal cavities that are hard to coat evenly by other methods. Mill finish, left untreated, is typically reserved for components that will be hidden inside an enclosure where corrosion exposure is minimal.
Modern laser cutting lines rarely run as standalone machines anymore. They’re integrated into automated material handling systems, robotic loading arms, and multi-axis gantries that move in several directions simultaneously.
This shift puts new demands on structural aluminium. A frame built for automation needs modular mounting slots so sensors, cable carriers, and pneumatic lines can attach without custom drilling on-site. Modular structural designs that adapt to automated gantries and linear slide systems let integrators build flexible configurations without redesigning the base extrusion for every project variant. This flexibility shortens the time between a machine concept and a working production line.
Is aluminium strong enough to replace steel in large machine frames?
For most CNC, laser cutting, and automated handling equipment, yes. Aluminium’s strength-to-weight ratio outperforms steel for applications where reducing moving mass improves speed and accuracy. For extremely heavy load-bearing applications, steel may still be preferred, but hybrid designs using aluminium for moving sections and steel for static bases are also common.
Does a smaller MOQ limit customization options?
Not necessarily. Many extrusion suppliers set MOQs around 250 to 500 kilograms per section, which is manageable for most OEM prototype runs and small-batch production, while still allowing fully custom cross-sections and surface treatments.
How long does custom profile production typically take?
Lead times for custom aluminium extrusion generally fall between 10 and 20 days, depending on die availability, order volume, and surface treatment complexity. Standard off-the-shelf profiles ship faster since no new tooling is required.
Can one profile design serve multiple machine models?
Often yes, if the design incorporates standardized mounting slots and modular dimensions. This is why many manufacturers lean toward flexible, multi-purpose cross-sections rather than designing a new die for every machine variant.

Standard catalog profiles cover a large share of machinery applications, but custom tooling becomes worthwhile once production volume justifies the die cost. Before committing to a custom cross-section, it helps to confirm a few practical points with your supplier:
Suppliers offering comprehensive customization across cross-section, length, wall thickness, and finish give engineering teams the freedom to solve structural problems precisely, rather than compromising around a generic stock shape.
The alloy certificate and the extrusion die matter, but consistency across production runs matters just as much. A profile that measures perfectly in a sample batch but drifts in tolerance three container loads later creates assembly problems on the factory floor. For us at Xinhe Aluminium, over 25 years of extrusion manufacturing has reinforced one lesson repeatedly: reliable aluminium extrusion for machinery depends on tight process control at the mill, not just a good die design on paper.
Machine builders evaluating a new supplier should ask for tolerance data across multiple production batches, not just a single certificate of conformance. It’s also worth confirming whether the supplier can support both prototype volumes and full-scale production runs, since switching vendors mid-project introduces its own risk of dimensional mismatch between old and new frame components.
Ultimately, the right aluminium extrusion for machinery is the one matched to its actual mechanical role, built from an alloy suited to its load and thermal environment, and sourced from a supplier capable of holding tolerance consistently across every batch produced.
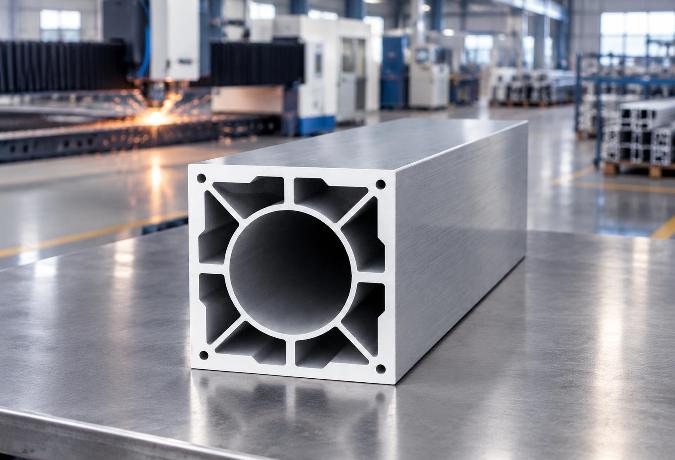
Choosing Industrial Aluminium Profiles for Laser Cutting Machines: A Technical Guide
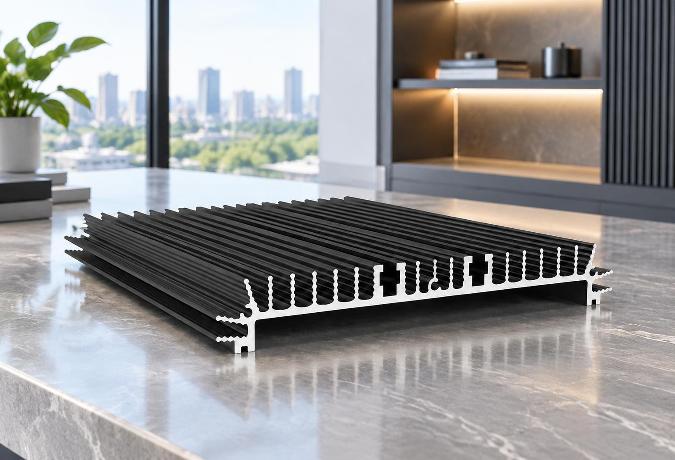
How LED Aluminium Profile Heatsinks Manage Thermal Challenges in High-Performance Lighting
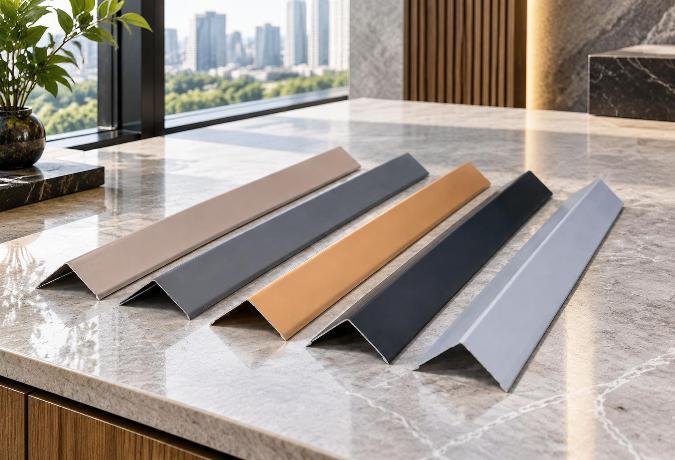
Architectural Aluminium Profiles: Choosing the Right Angle Design for Framing and Trim
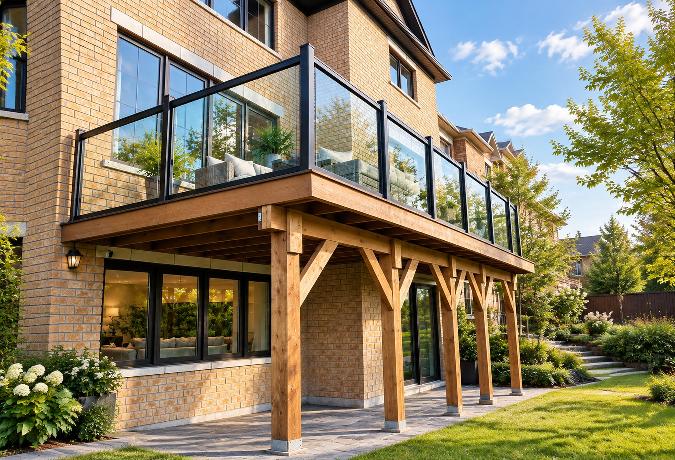
Choosing the Right Aluminium Balustrade Profiles for Your Project
Choosing the Right Aluminium Door Profiles for Narrow-Frame Sliding Systems
Aluminium Window Profiles: Engineering Durable Facades for Modern Buildings
Aluminium Thermal Break Profiles: Design Principles and Practical Applications
Aluminium Extrusion for Furniture: Structural Logic Behind Lightweight Precision
Aluminium Wardrobe Profiles: A Practical Guide to Frames, Tracks, and Finishes
Choosing the Right Aluminium Linear Rail Profile for Motion Systems
Anodized Aluminium Profiles: Material Selection and Practical Applications in Modern Design
Anodized Aluminium Profiles: Material Selection and Practical Applications in Modern Design
Aluminium Decorative Profiles: Design, Installation, and Interior Applications
Aluminium Profiles for Automation: A Practical Guide to Modular Frame Design
Aluminium Extrusion for Furniture: Structural Logic Behind Lightweight Precision
Aluminium Thermal Break Profiles: Design Principles and Practical Applications
How do suppliers normally handle Sliding door installation problems overseas?
Choosing the Right Aluminium Balustrade Profiles for Your Project
Aluminium Louver Profiles: Light Control and Ventilation in Modern Architecture
Aluminium Curtain Wall Profiles: Structural Design and Performance in Modern Architecture
Aluminium Trim Profiles: Bridging Aesthetics and Performance in Modern Interior Design
How do I verify Casement window production capacity before signing a contract?
Powder Coated Aluminium Profiles: Durability and Design in Modern Applications
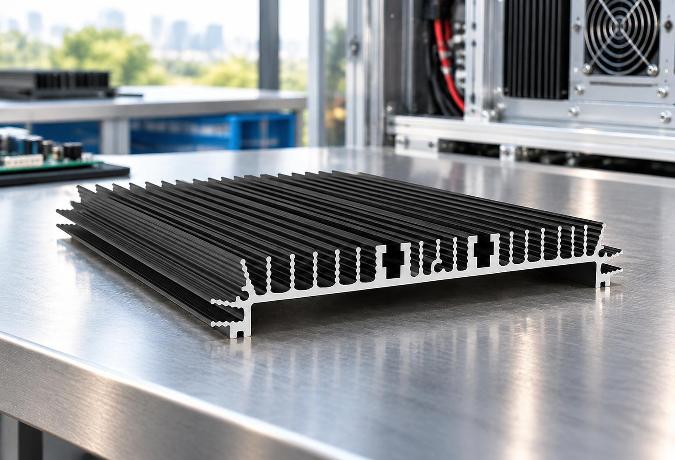
How Aluminium Heatsink Profiles Keep Electronics From Cooking Themselves
How do FOB and CIF change my risks when importing Sliding doors?
What support should I receive if Architecture profile dimensions are wrong?
Aluminium Profile Alloys 6063 T5 T6: Properties, Heat Treatment Differences, and Application Selecti
Inside an Aluminium Profile Factory: How Angle Profiles Are Made and Chosen
What is a realistic MOQ for a first Sliding window trial order?
Which factory records should I review before buying Industrial profile?
Aluminium Extrusion for LED Lighting: Choosing the Right Heatsink Profile
Can a Floding door supplier protect my private design from competitors?
Which Industrial profile tolerances affect assembly accuracy and finished quality?
Can trade credit insurance cover my Architecture profile purchase risk?
Custom Aluminium Extrusion Profiles: Engineering Precision into Industrial Motion Systems
T-Slot Aluminium Extrusion: Structural Framework Design Without Welding
Which recycled-content records are credible for Sliding window procurement?
Aluminium Sliding Door Profiles: A Practical Guide to Frame Design and Performance
How Aluminium Extrusion Manufacturers in China Support Linear Motion Systems
What contract clauses protect my money if Casement door quality is unacceptable?
How do I confirm Sliding door testing equipment is calibrated and current?
Should I visit an Architecture profile plant before placing a large order?
Which compliance tests should a Floding door pass before international shipment?
How do I compare Decorative profile color samples under different lighting?
What payment and price terms make sense for a small Casement window order?
What lead time should I allow for a seasonal Floding door order?
How can I compare Floding door alternatives when supply costs suddenly rise?
Which new Sliding door technologies can lower maintenance costs over time?
How are recycled materials changing the future cost of Floding doors?
How long should a custom Casement door sample normally take to prepare?
What gap between a Sliding window sample and bulk order is acceptable?
Which Decorative profile finishes are becoming more sustainable and cost-effective?
What logistics fees should be listed separately in a Sliding window quote?
How might volatile aluminum prices affect future Sliding window sourcing?
Which audit questions reveal labor risks at a Casement door factory?
Can Decorative profile suppliers provide fast remote guidance for finish defects?
What should a Shutter sample include so I can assess production quality?
Do Sliding door materials need traceability records for customs clearance?
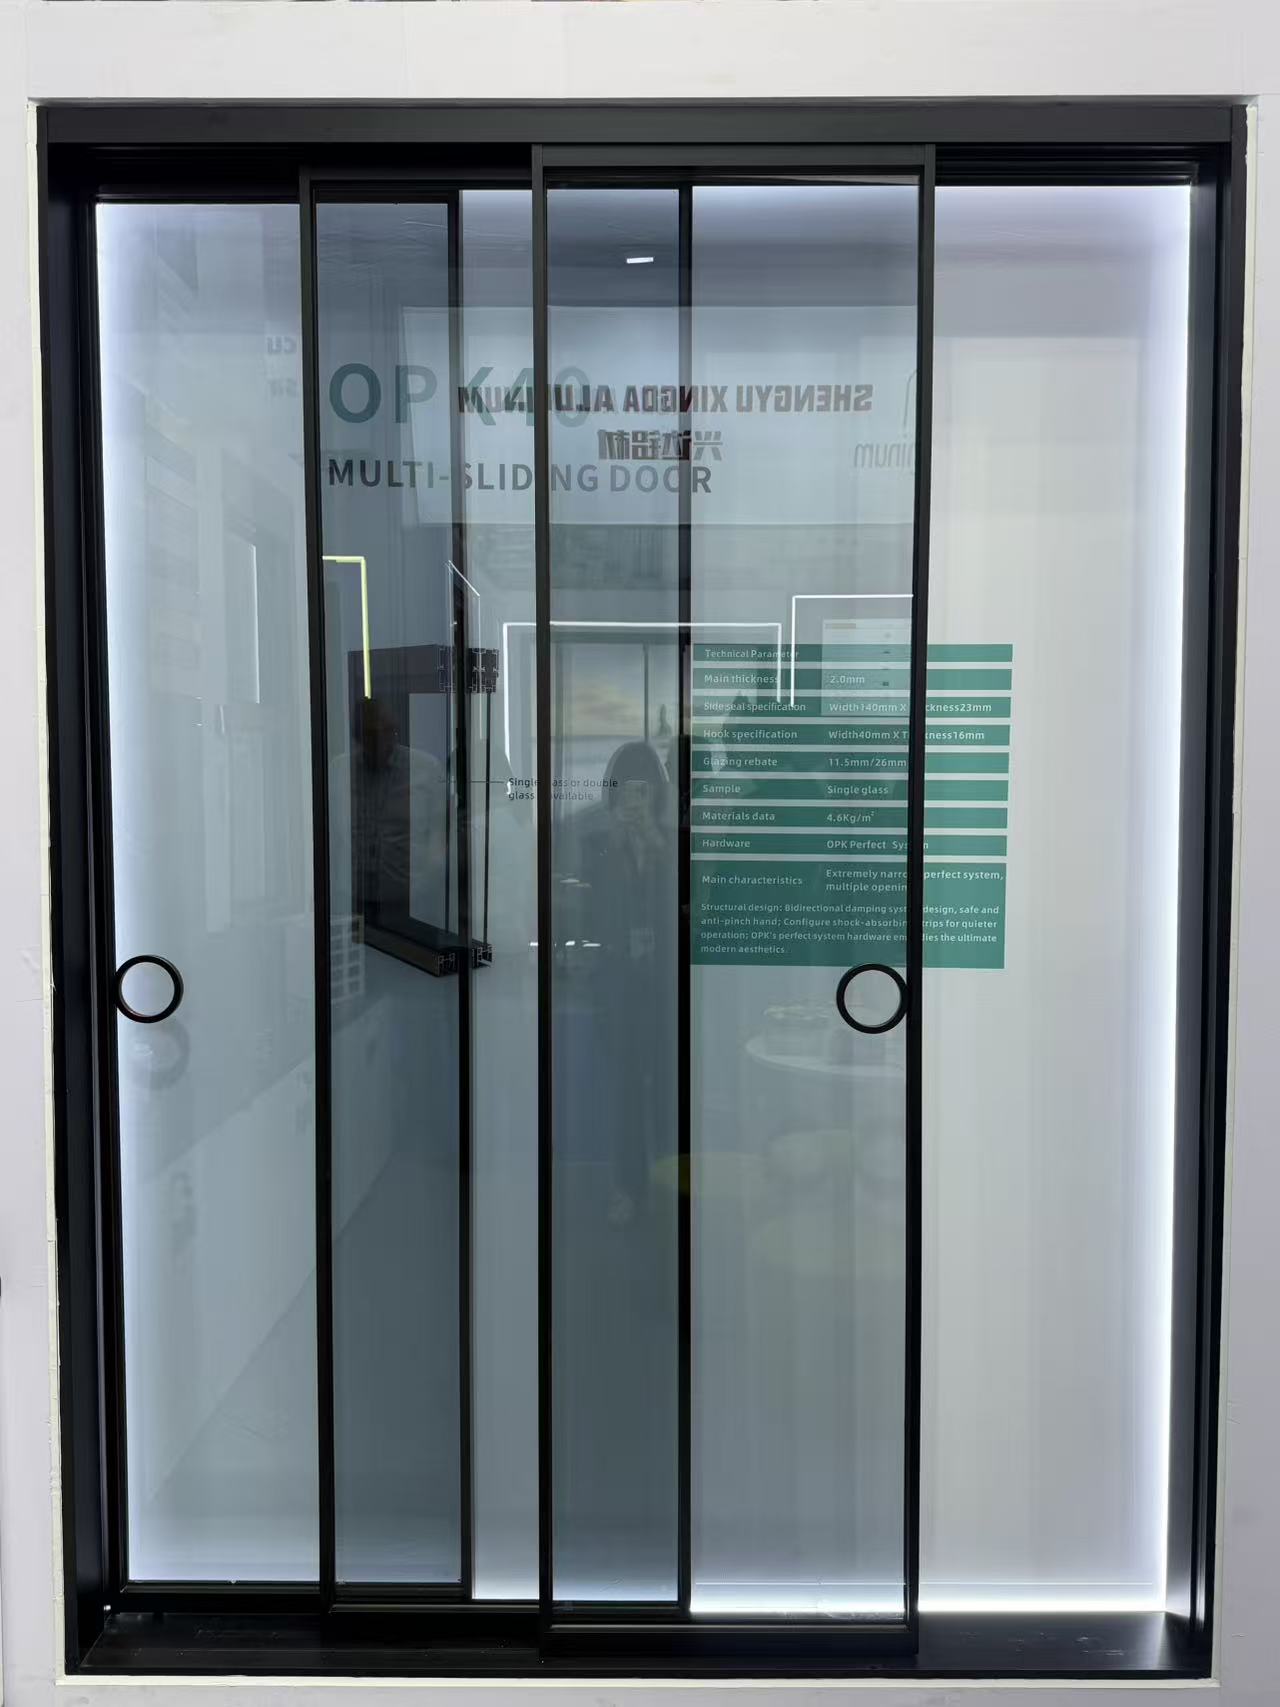
What environmental declarations are useful when importing Architecture profile?
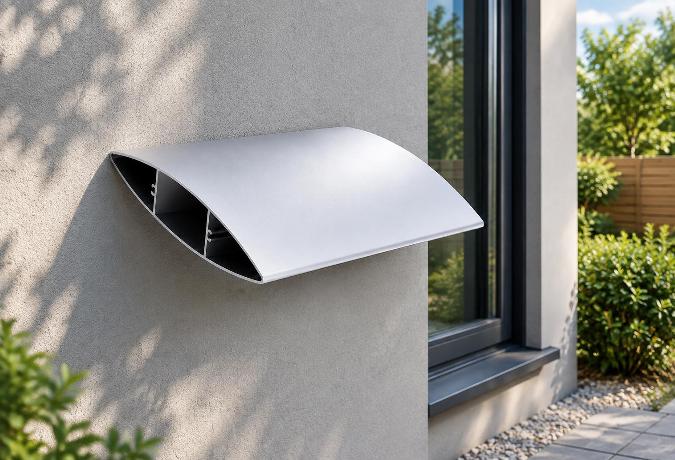
Why Blade Geometry Determines Whether Aluminium Louvers Actually Work
Engineering an Aluminium Angle Profile: Structural Mechanics and Application Realities
What usually drives Architecture profile costs more, alloy or surface treatment?
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
Why the Thermal Break Cavity Matters More Than Frame Thickness in Aluminium Framed Windows and Doors
The T-Slot Groove Geometry That Makes Aluminium Framing Weld-Free
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
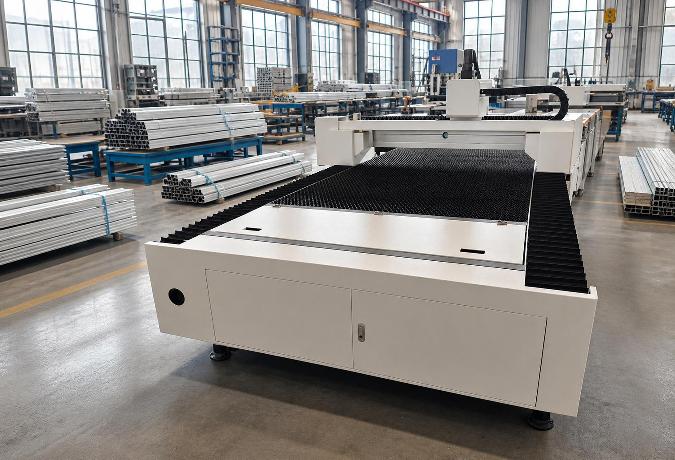
Structural Dynamics of Industrial Aluminium Profiles in Laser Cutting Gantries
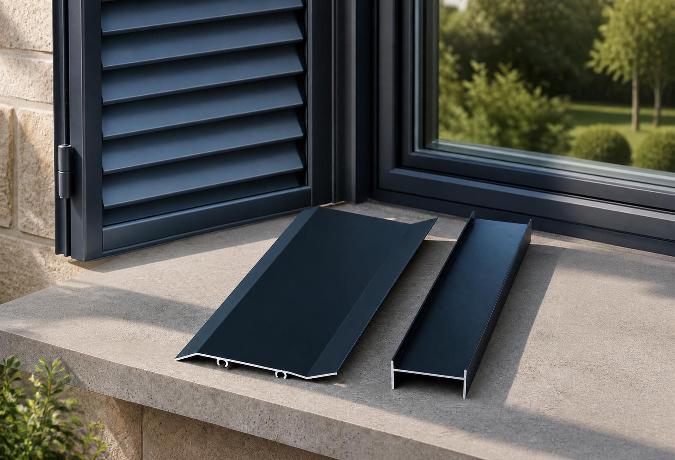
The Engineering Mechanics Behind High-Performance Aluminium Shutters
What factory documents should I request for a Floding door supplier review?
Which delivery term gives me better control over Decorative profile freight costs?
What low-carbon Awing window materials are gaining wider market acceptance?
Why Sliding Door Track Geometry Determines Wardrobe Longevity
Engineering Mechanics and Surface Dynamics of Aluminium Channel Profiles
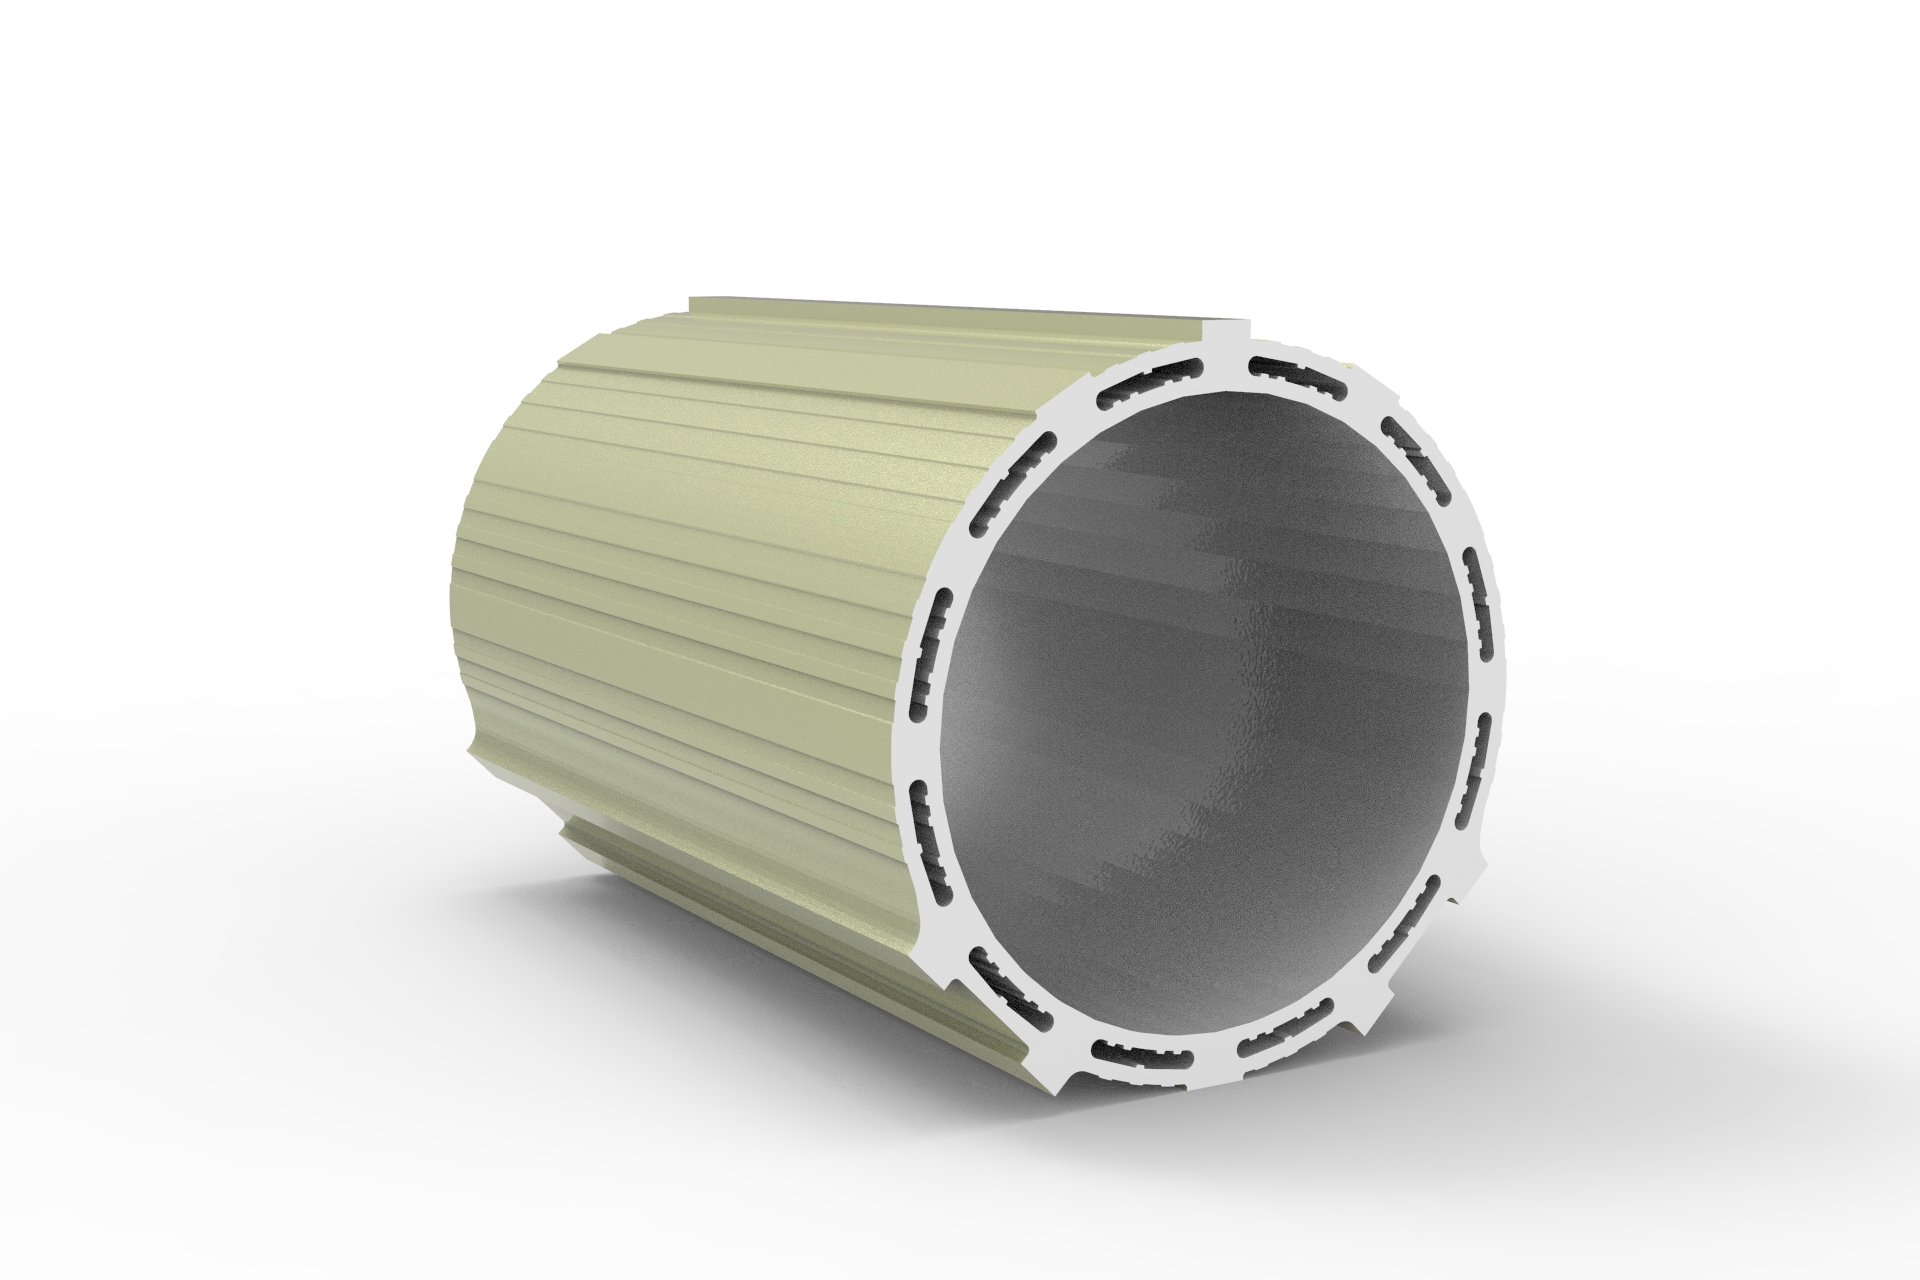
Understanding Aluminium Round Tube Specifications for Structural Engineering
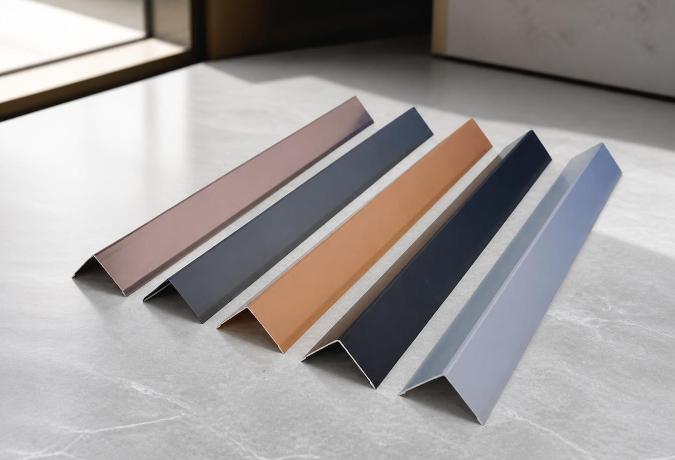
Why the 90-Degree Angle in Standard Aluminium Profiles Determines Structural Reliability
How can I ensure a Floding door sample matches the planned mass production?
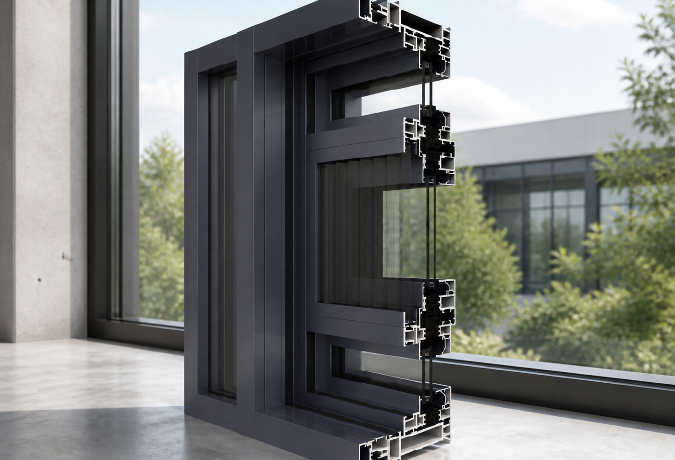
Why Mullion Thickness Determines How Much Glass an Aluminium Curtain Wall Can Actually Hold
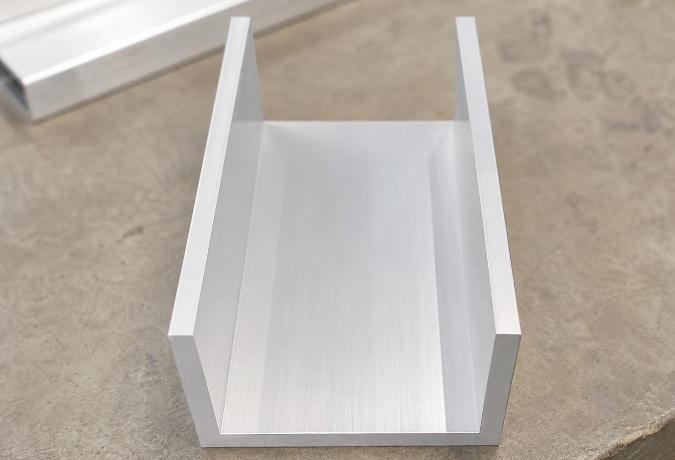
Engineering Dimensional Stability in Aluminium Extrusions for Channel Profiles
Engineering the Structural Framework: The Mechanics of Aluminium Profiles for Kitchen Cabinets
Choosing an Aluminium Profile Supplier: What Actually Separates the Reliable Ones from the Rest
Can Awing window orders ship in batches to avoid project delays?
What response time should I expect for Awing window warranty claims?
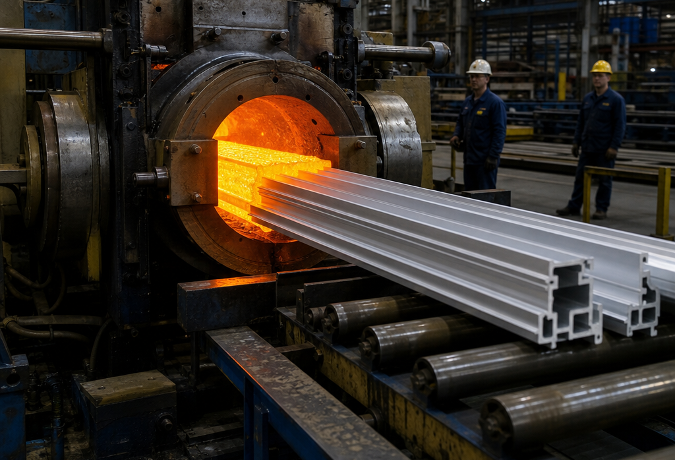
Navigating the Supply Chain: Evaluating an Aluminium Profile Manufacturer for B2B Procurement
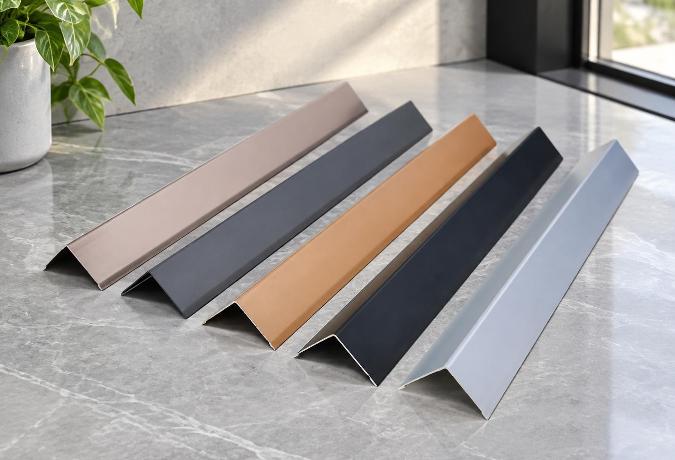
Engineering Structural Integrity Through Precision L-Shaped Aluminium Profiles
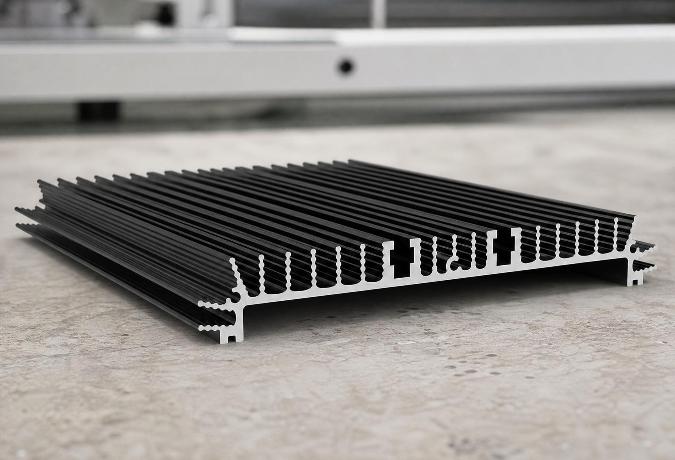
Thermal Dynamics in High-Power Electronics: Engineering Aluminium Heatsink Profiles
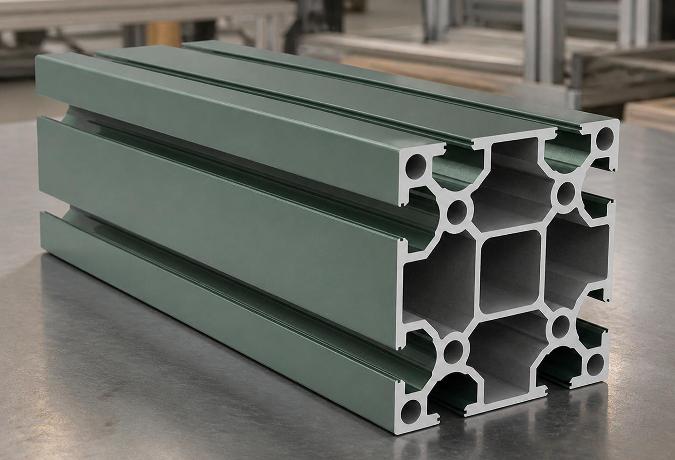
Why the T-Slot Design Determines the Real Strength of Structural Aluminium Extrusions
How long should replacement Sliding window parts remain available after purchase?
Should I expect volume discounts when reordering the same Sliding window model?
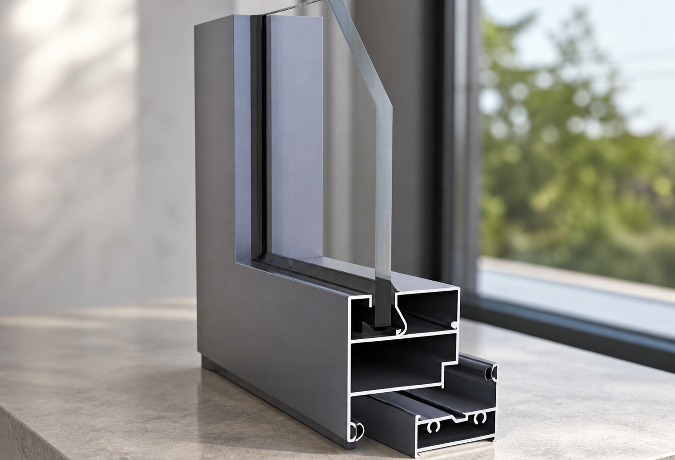
The Multi-Strip Sealing Structure Inside Aluminium Windows and Doors
Engineering Lightweight Rail Structures Through Extruded Aluminium Profiles
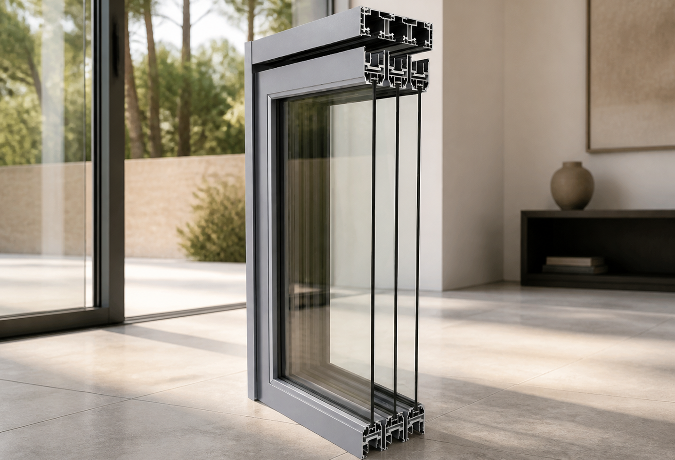
Why the Frame Width on an Aluminium Sliding Door Determines Your Room’s Light
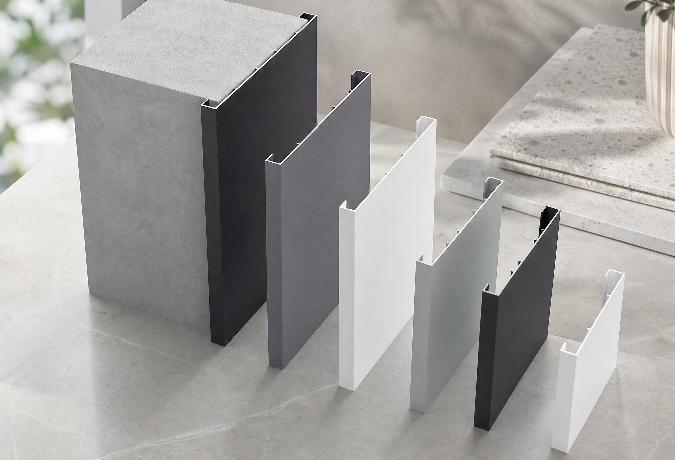
The Engineering Behind Decorative Aluminium Profiles: Alloys, Surface Treatments, and Edge Protectio
What alternative materials could make Casement doors more resilient and recyclable?
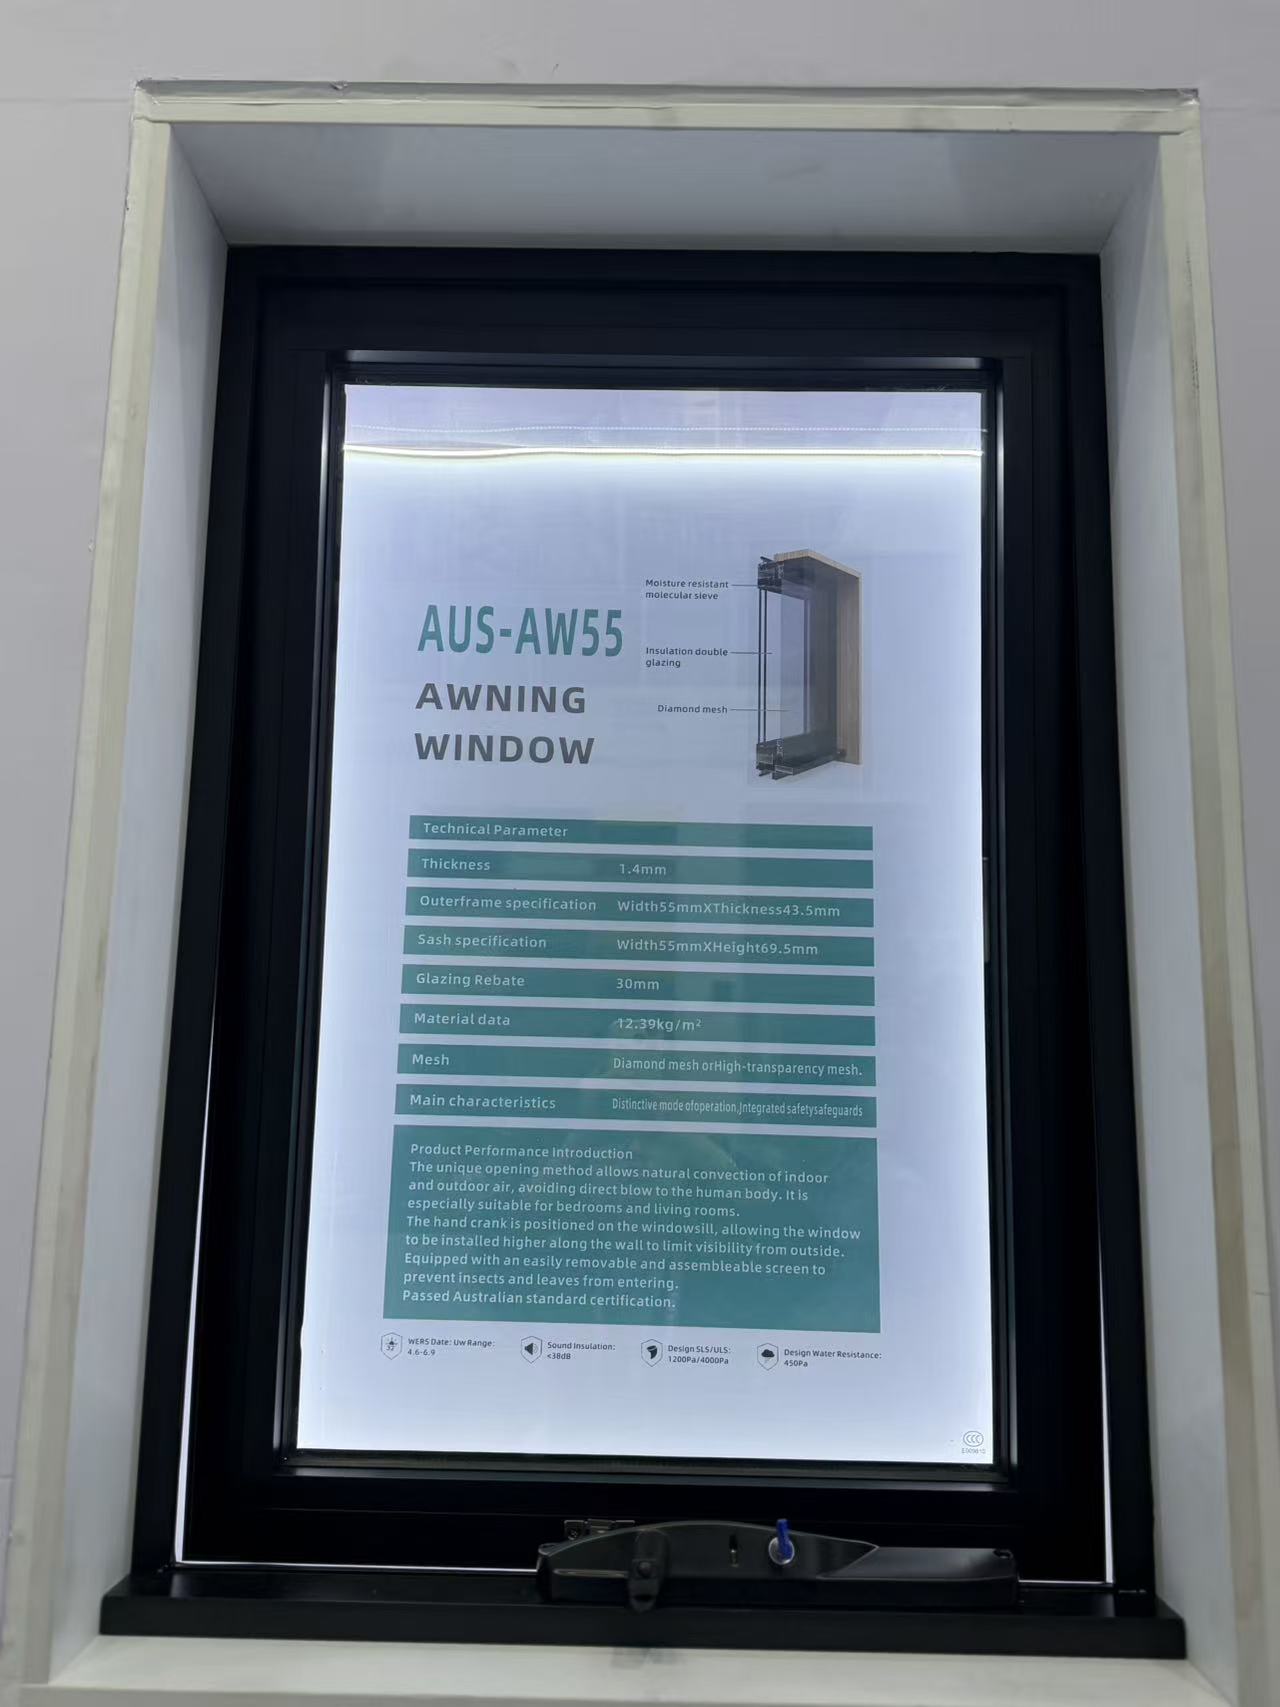
How can I compare Awing window quotes without missing hidden packing costs?
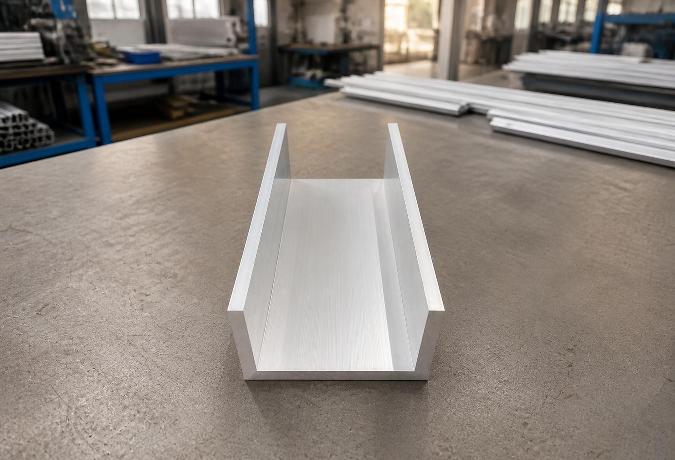
Decoding Structural Tolerances in Aluminium Extrusion Profiles for Channel Applications
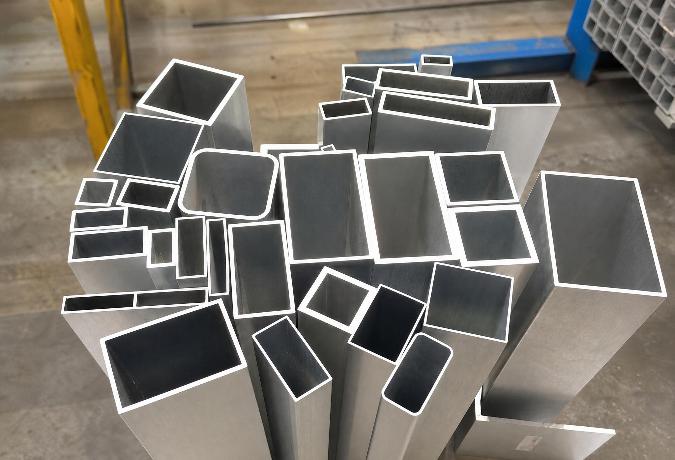
Engineering an Aluminium Square Tube for Modern Structural Integrity
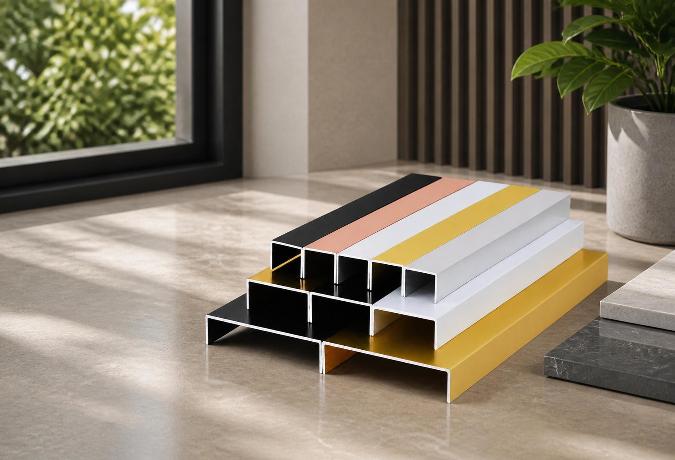
Engineering Tolerances and Alloy Mechanics in Extruded Aluminium Construction Profiles
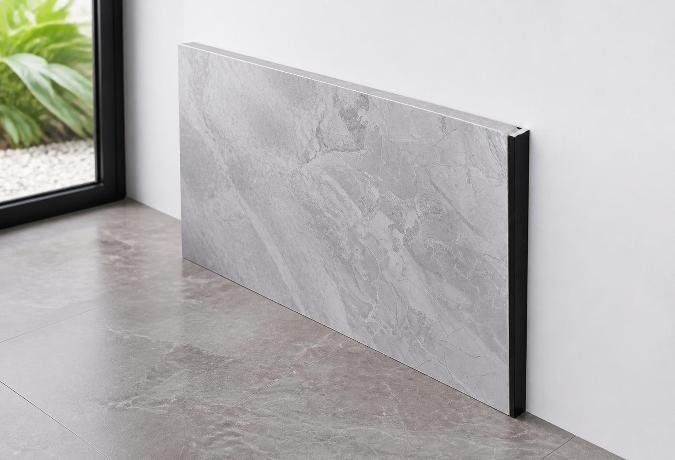
The Engineering Mechanics Behind Aluminium Angle Profiles in Modern Construction
Can an Industrial profile be modified for my assembly without weakening it?
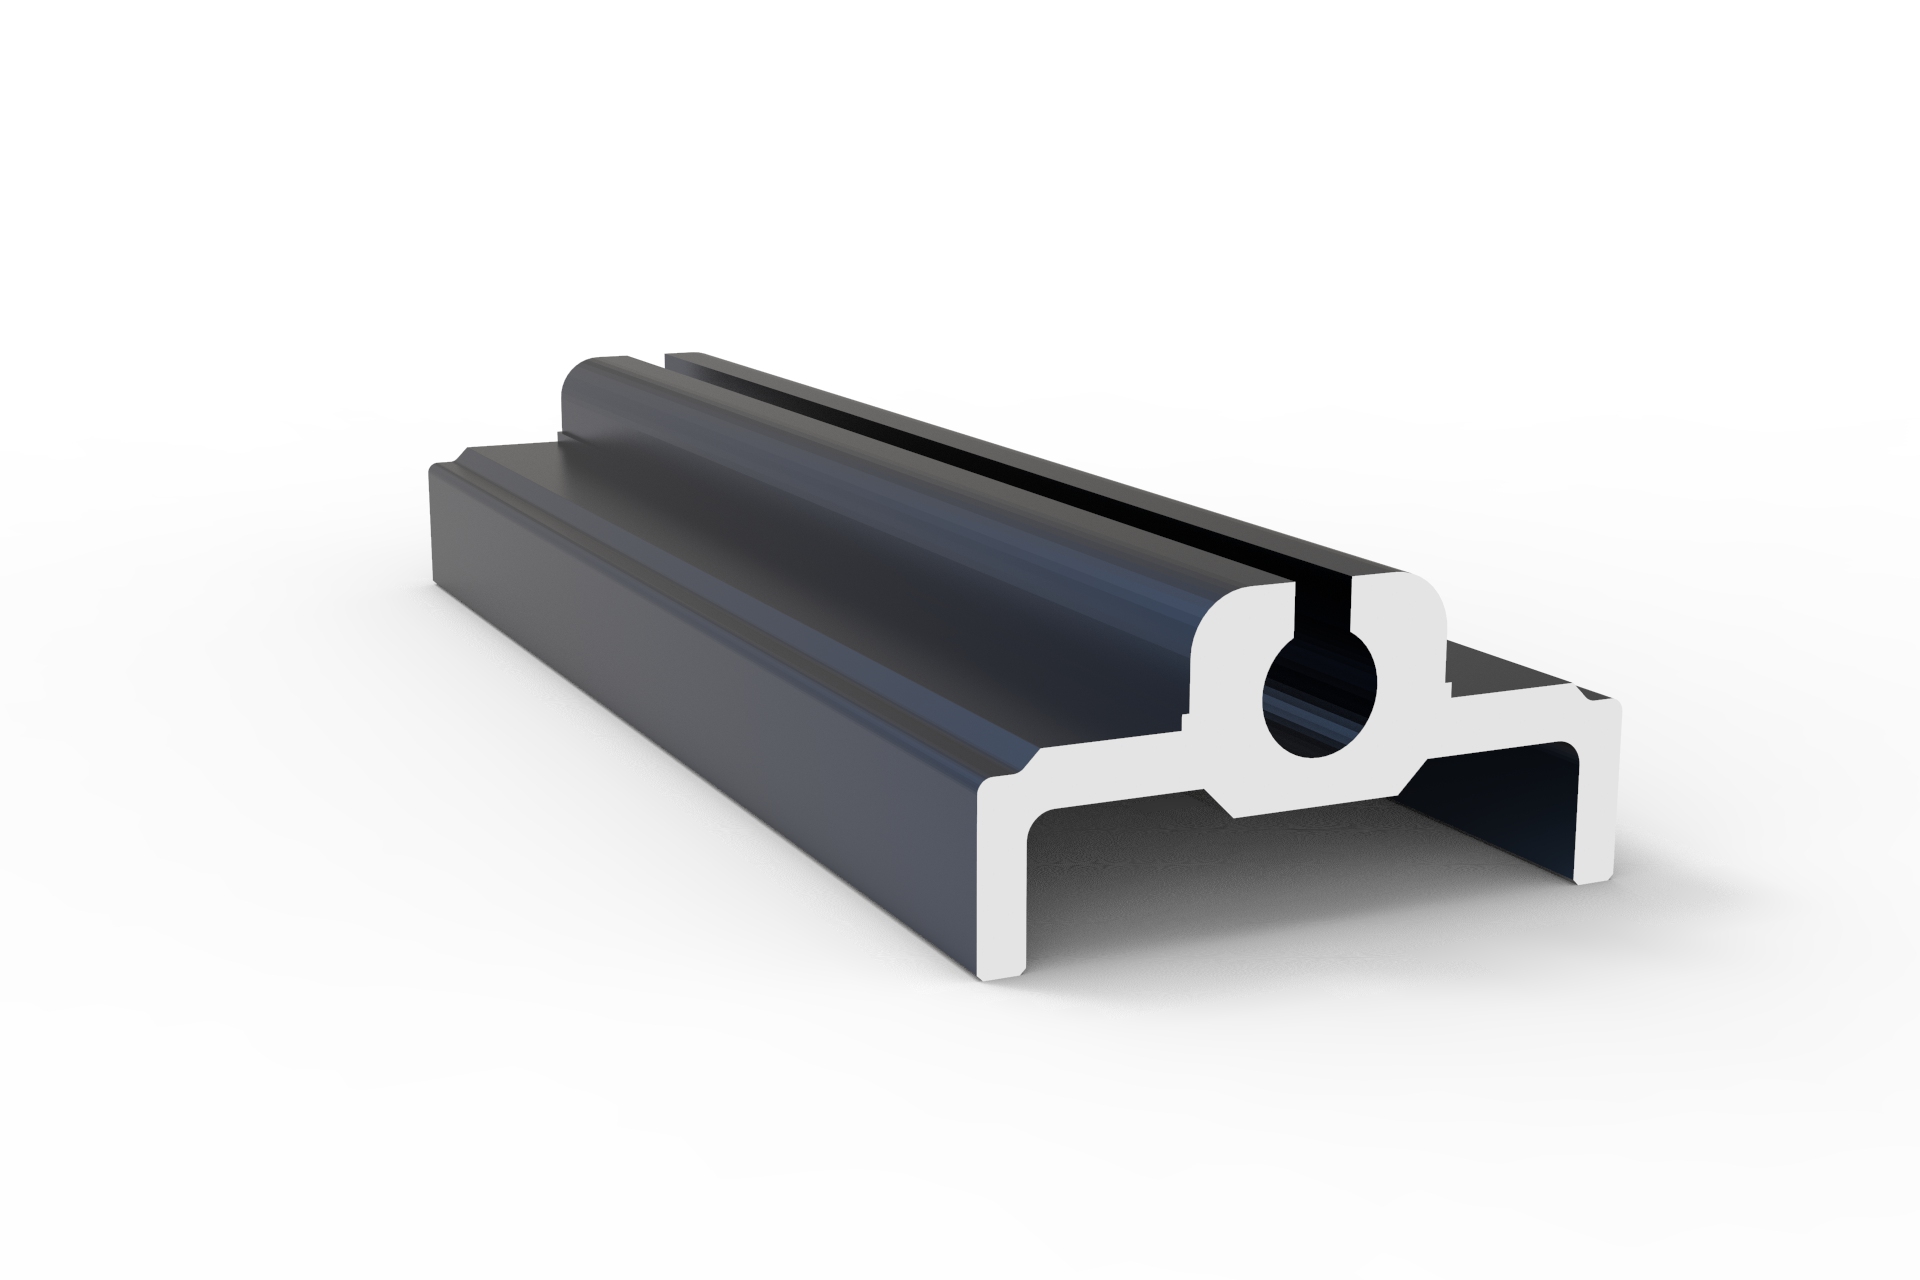
What warning signs suggest a Sliding door seller may disappear after payment?
What energy-efficient alternatives to Casement doors are worth comparing now?
Can a Casement window handle temperature changes without seal failure?
Who pays for unloading and destination handling under Casement door CIF terms?
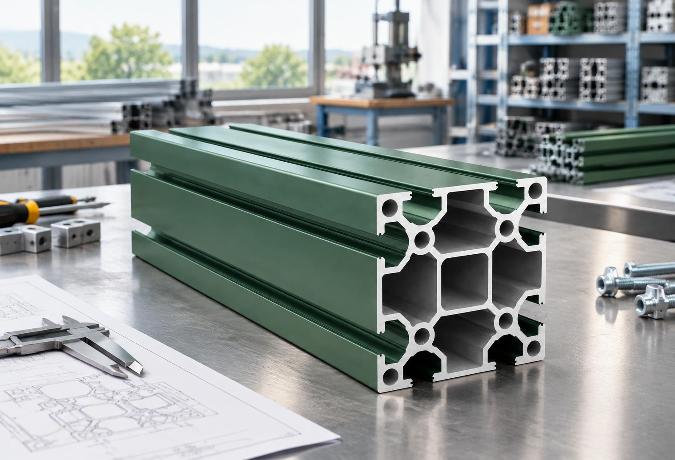
Custom Aluminium Extrusion Profiles: The Engineering Mechanics of T-Slot Frameworks
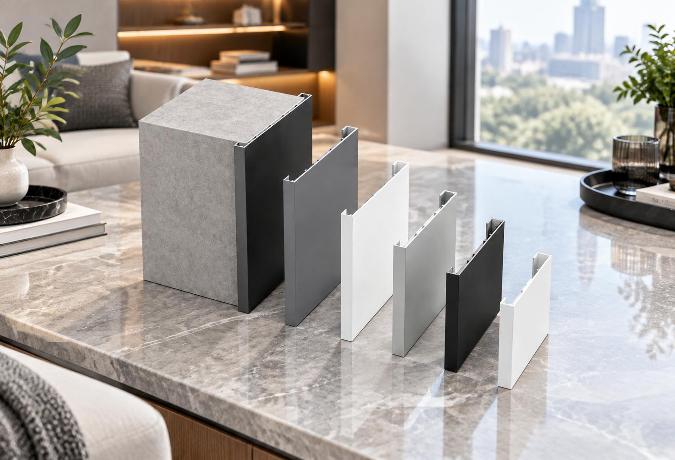
Material Transitions and Geometric Stability in Decorative Aluminium Profiles
Can I negotiate a lower Sliding door MOQ for a showroom launch?
Key Advantages of Using Structural Aluminium Extrusion Profiles in Construction
What evidence shows an Awing window factory manages coating waste properly?
How can I protect my deposit when ordering custom Decorative profile?
How do I spot unusually low Industrial profile prices before committing funds?
How can I check that a Shutter supplier is not using unapproved subcontractors?
What contract terms protect my Casement door drawings and branding?
How can I compare Casement door insulation ratings before placing an order?
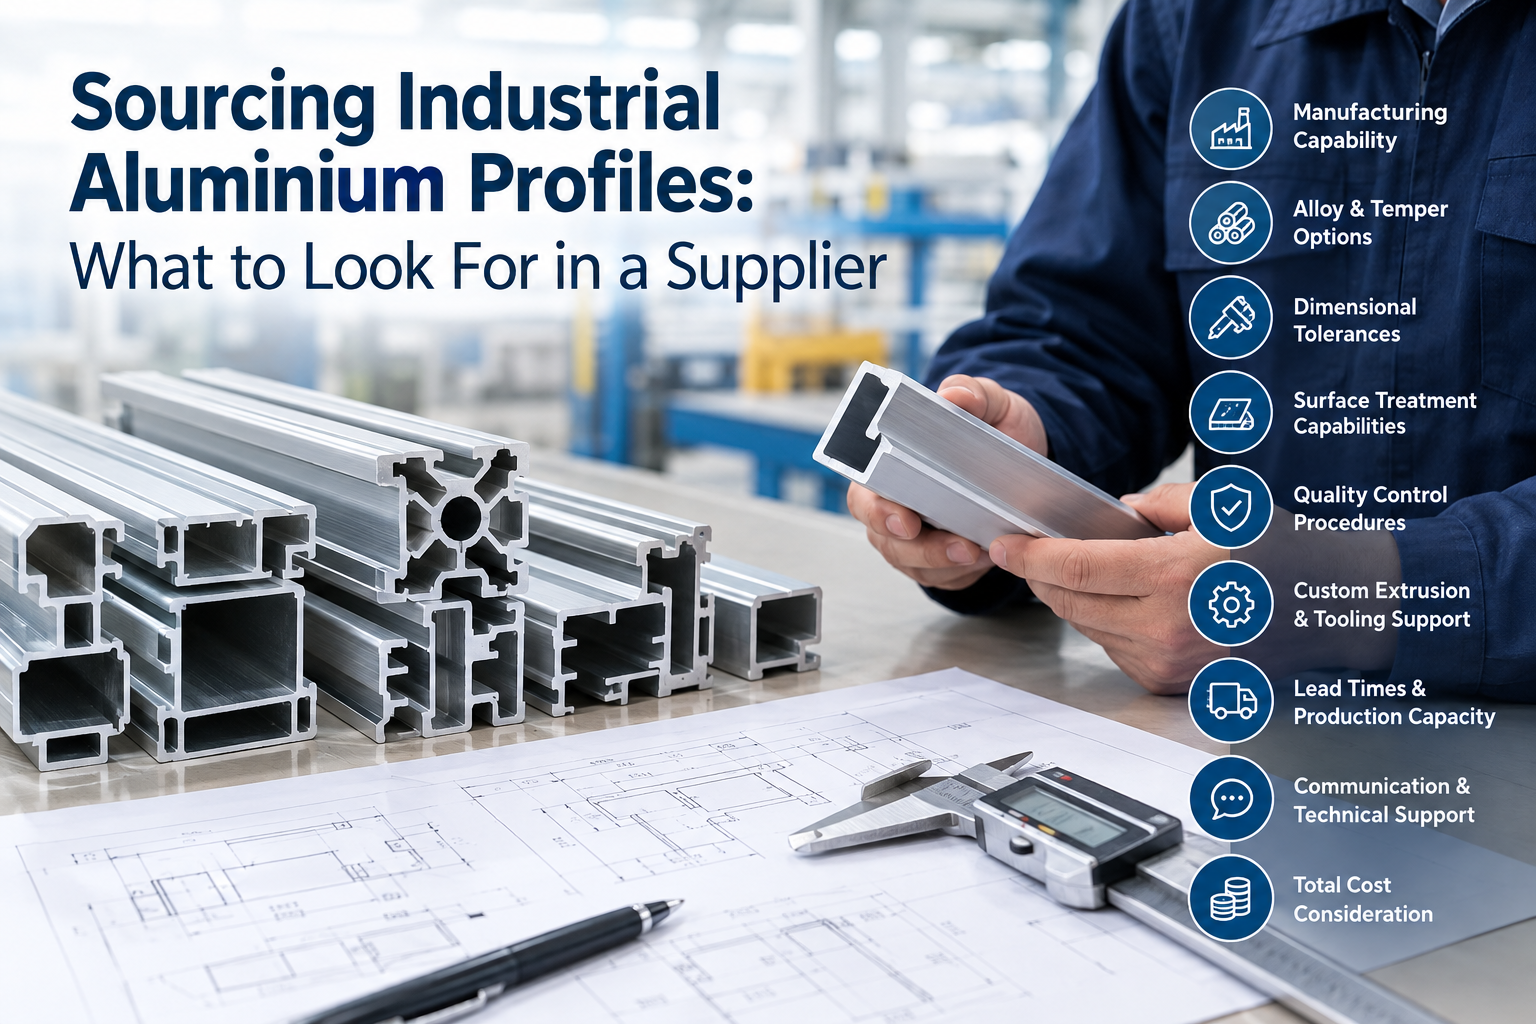
Sourcing Industrial Aluminium Profiles: What to Look For in a Supplier
How do I keep ownership of a custom Architecture profile extrusion die?
The Energy Efficiency Benefits of an Aluminium Frame Sliding Glass Window
How do I check Industrial profile alloy grades against the shipping documents?
What Casement window warranty period is reasonable for an overseas buyer?
How are defective Sliding window units usually replaced internationally?
How can I reduce breakage risks when shipping Casement windows overseas?
The Structural Mechanics Behind Decorative Aluminium Profiles
How Do Engineers Select Industrial Aluminium Profiles for High-Load Frameworks?
What payment structure reduces my risk on a first Industrial profile order?
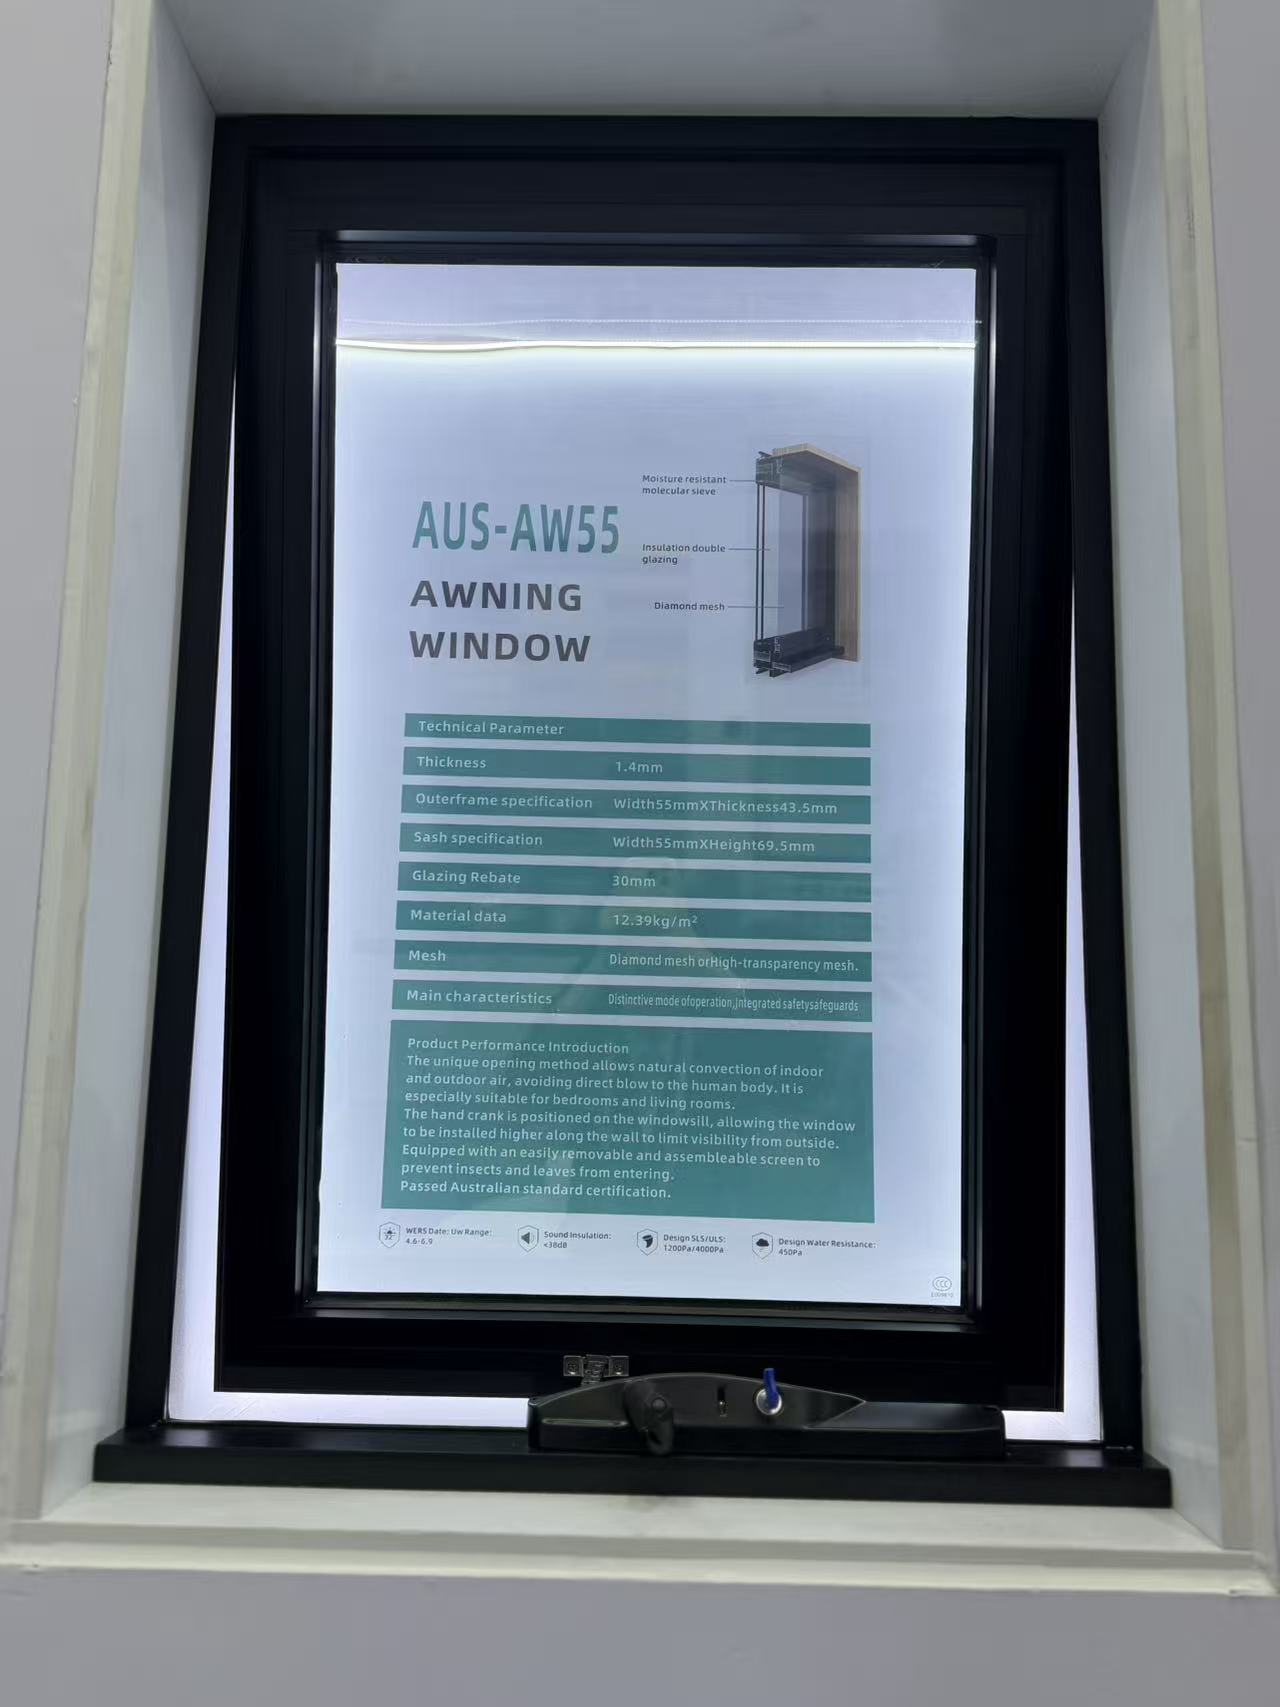
Should I approve a Casement window sample before checking its hardware strength?
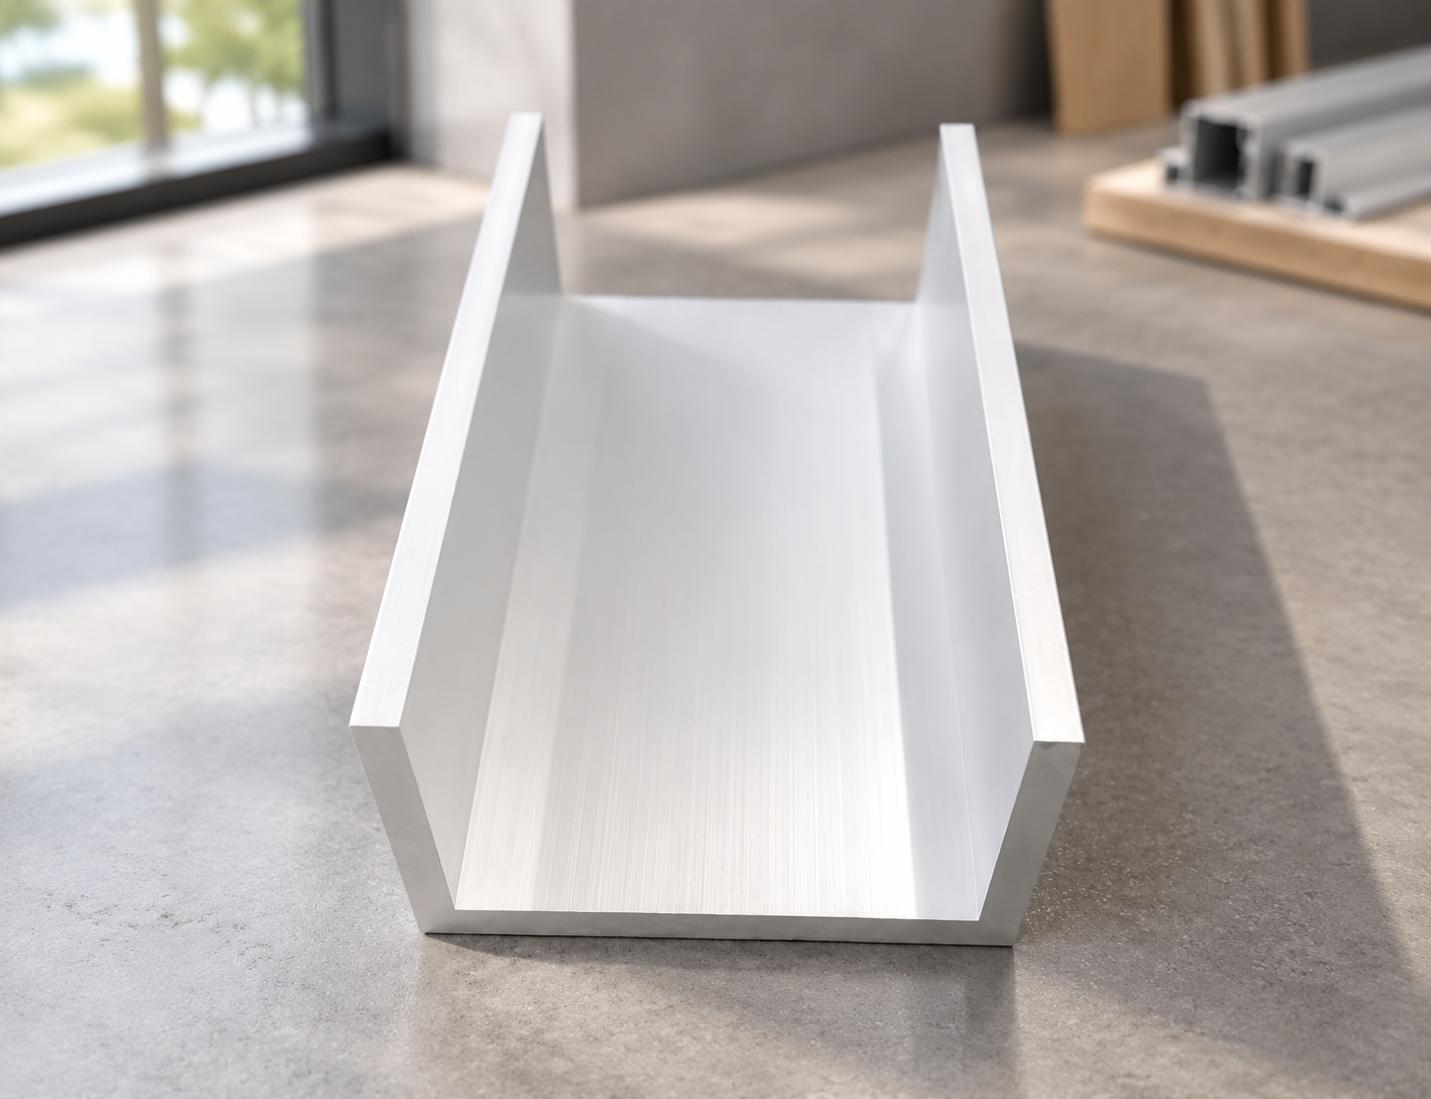
Structural Mechanics of Channel Extrusions in Architectural Aluminium Profiles
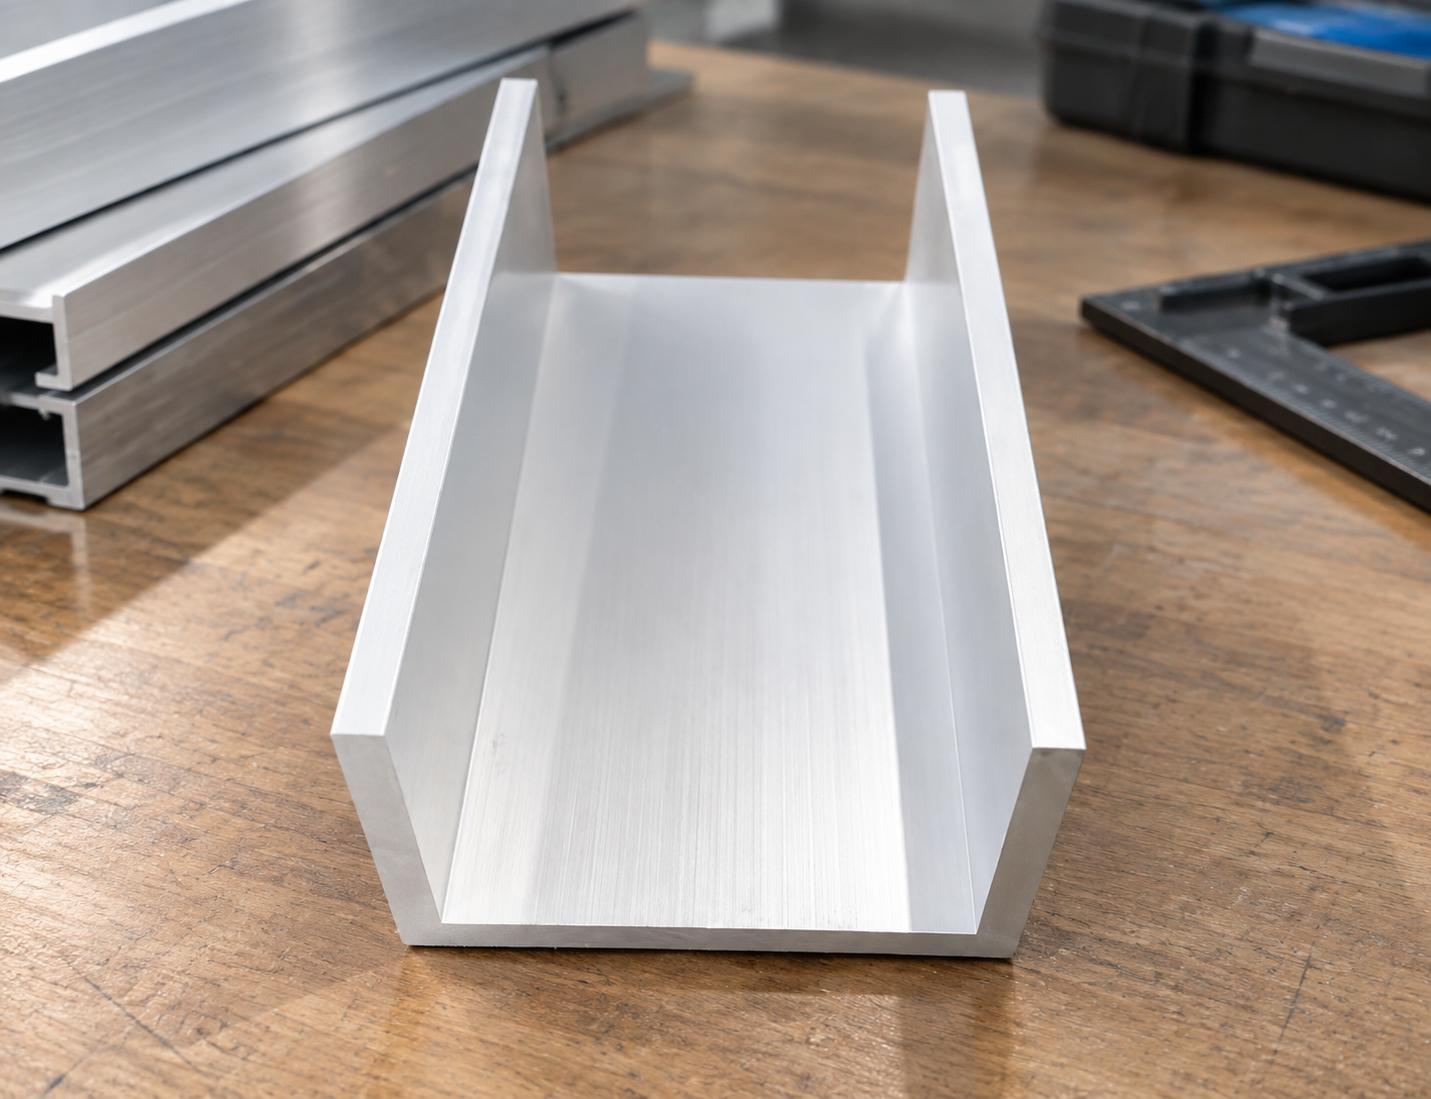
Engineering Mechanics of Aluminium Extrusion Profiles in Channel Systems
What functional tests should I perform on a Sliding door prototype?
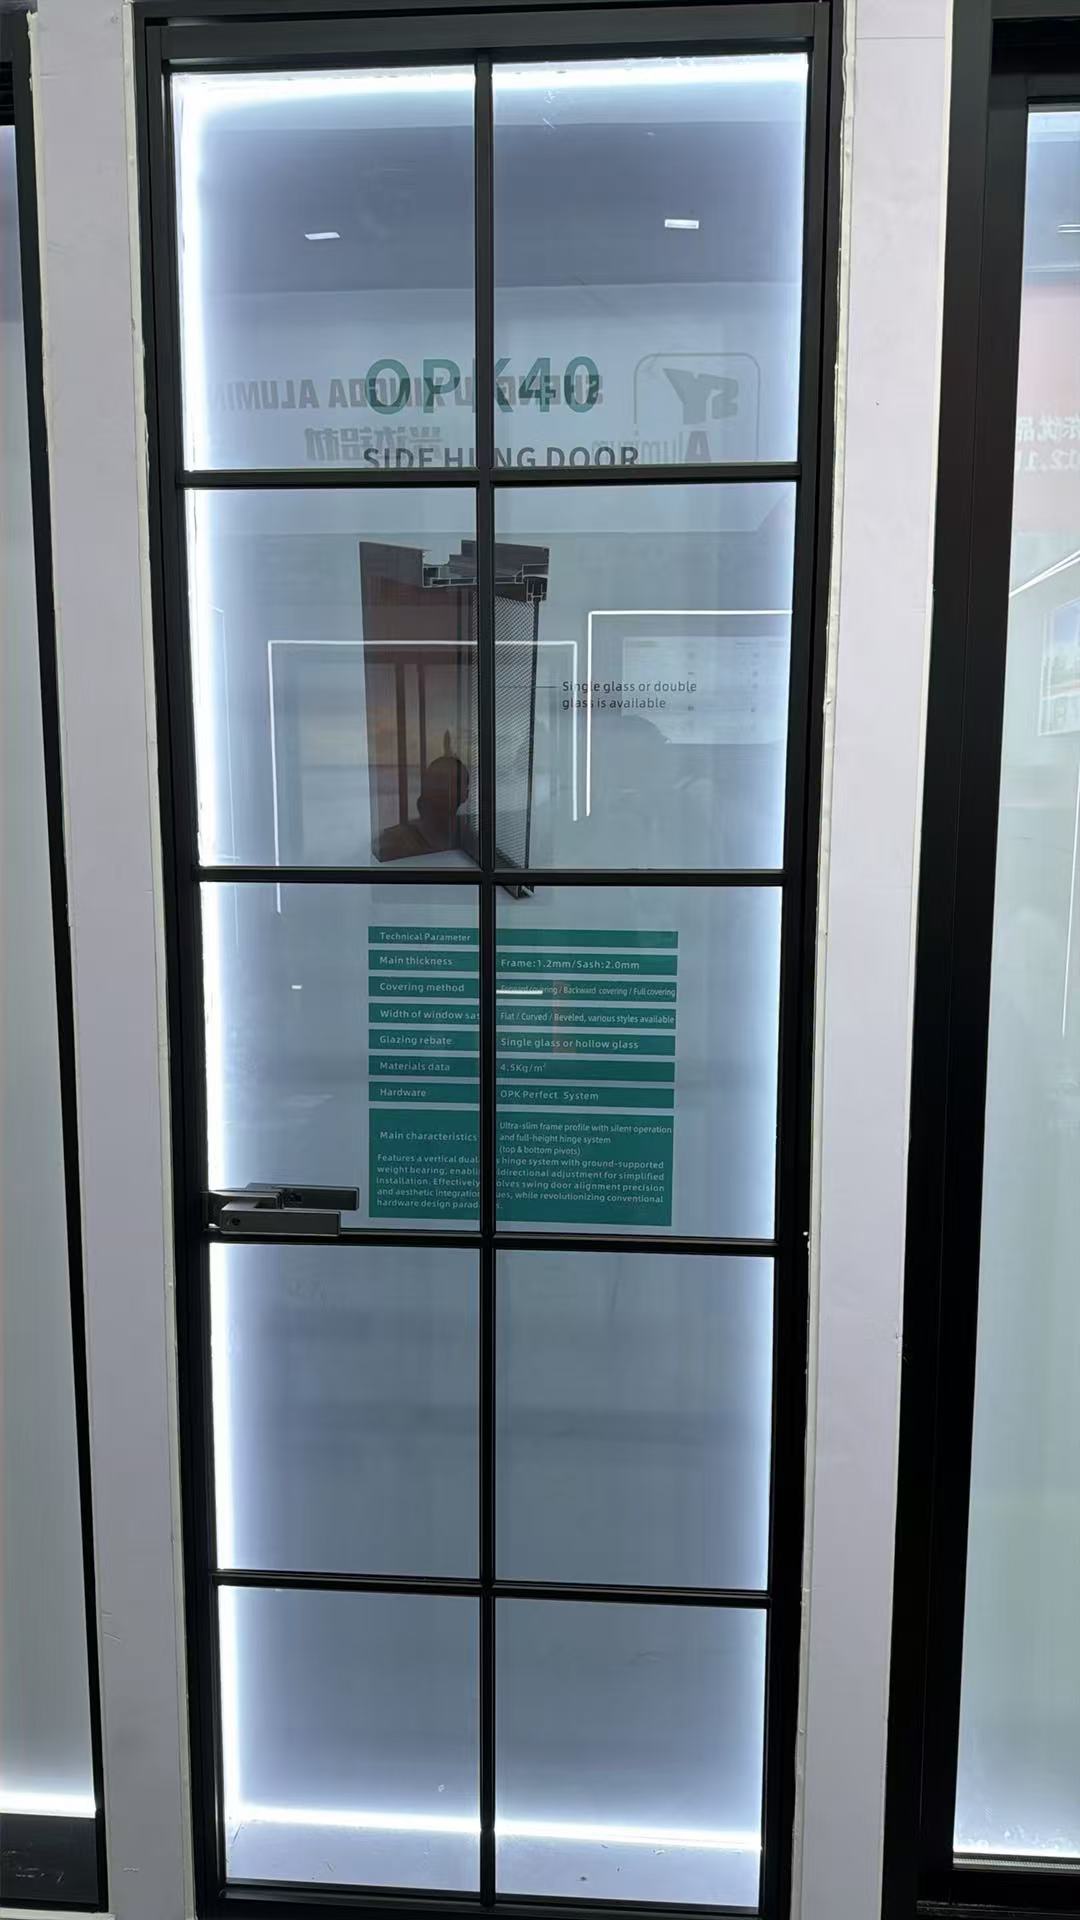
What payment terms are fair when Decorative profile colors remain unconfirmed?
Is a letter of credit practical for a large Casement window shipment?
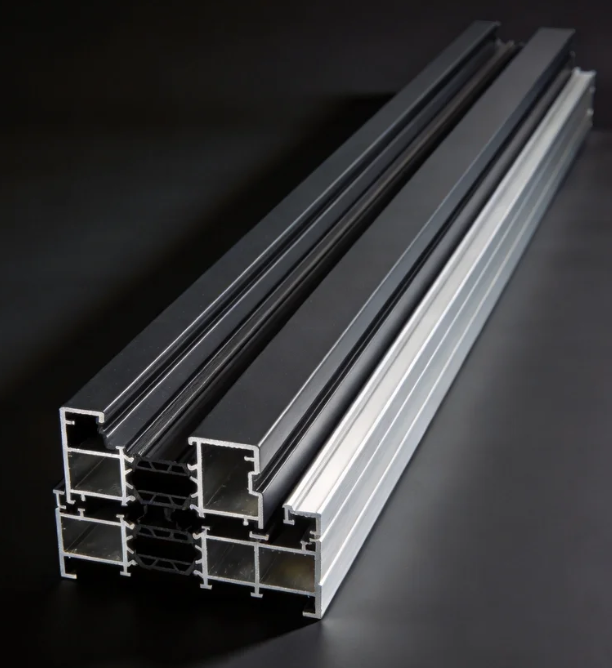
How should Industrial profile bundles be packed to prevent transit damage?
Which safety documents should I request for Awing window imports?
What shipping delays commonly affect Architecture profile orders during peak season?
How to Specify Extruded Aluminium Profiles: Costs, Alloys, and Tolerances
Is a Floding door suitable for a wide opening exposed to strong winds?
Structural Integrity in Modular Design: Engineering T-Slot Aluminium Extrusion Profiles
Resolving Corner Stress: The Engineering Mechanics Behind Aluminium Profiles in Architectural Framin
How do Floding door prices change with glass, hardware, and finish choices?
How can I prove Shutter defects remotely without returning every unit?
How can I shorten Awing window sampling without losing critical tests?
Does ordering mixed Shutter sizes usually change the unit price or MOQ?
How should Industrial profile warranty responsibility be shared after assembly?
How should I plan Shutter inventory when ocean freight schedules change?
How do escrow arrangements reduce risk for a new Floding door supplier?
What frame materials make a Sliding window last in harsh coastal weather?
How can I verify that a Shutter certificate matches the actual product?
Can automated Shutters replace manual systems without raising lifecycle costs?
How do I choose the right Casement window size for a windy building?
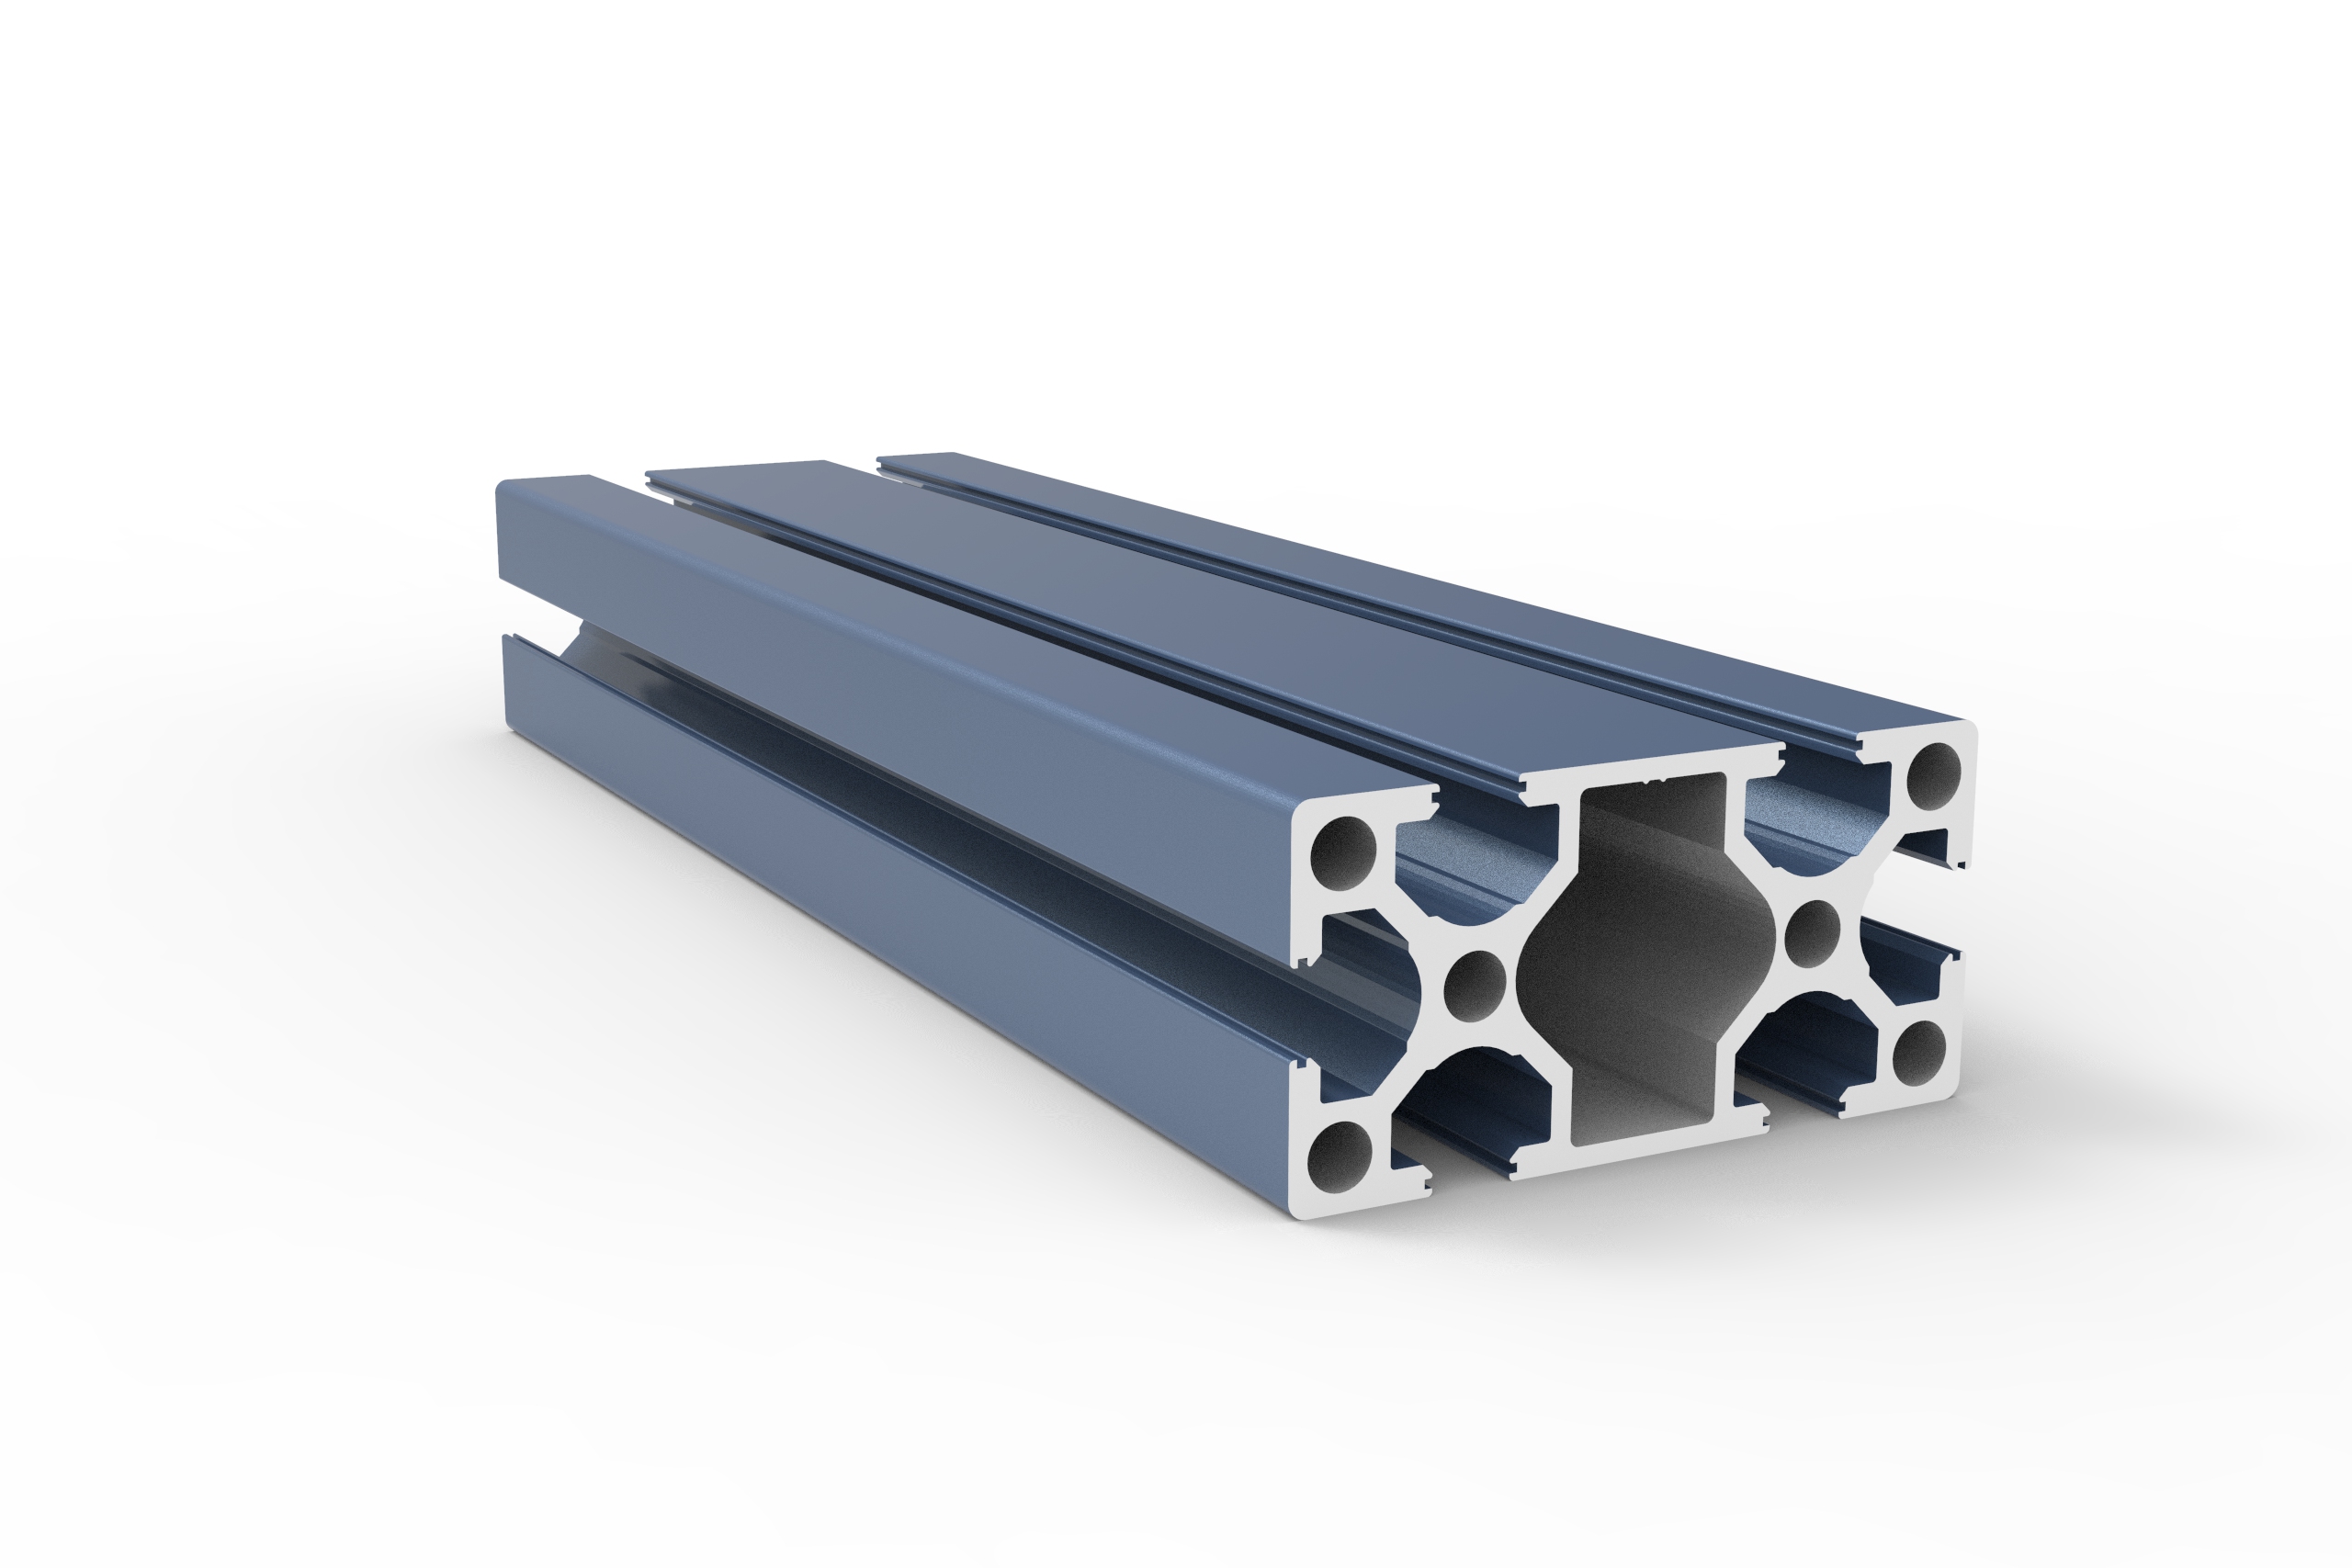
What should an ethical audit cover at a Decorative profile factory?
How should I document Industrial profile defects before disputing the final payment?
Are lightweight Industrial profile alloys reliable enough for demanding machinery?
Are thermal-break casement windows becoming a better long-term choice than standard frames?
What is a realistic MOQ for custom sliding windows without pushing up unit cost?
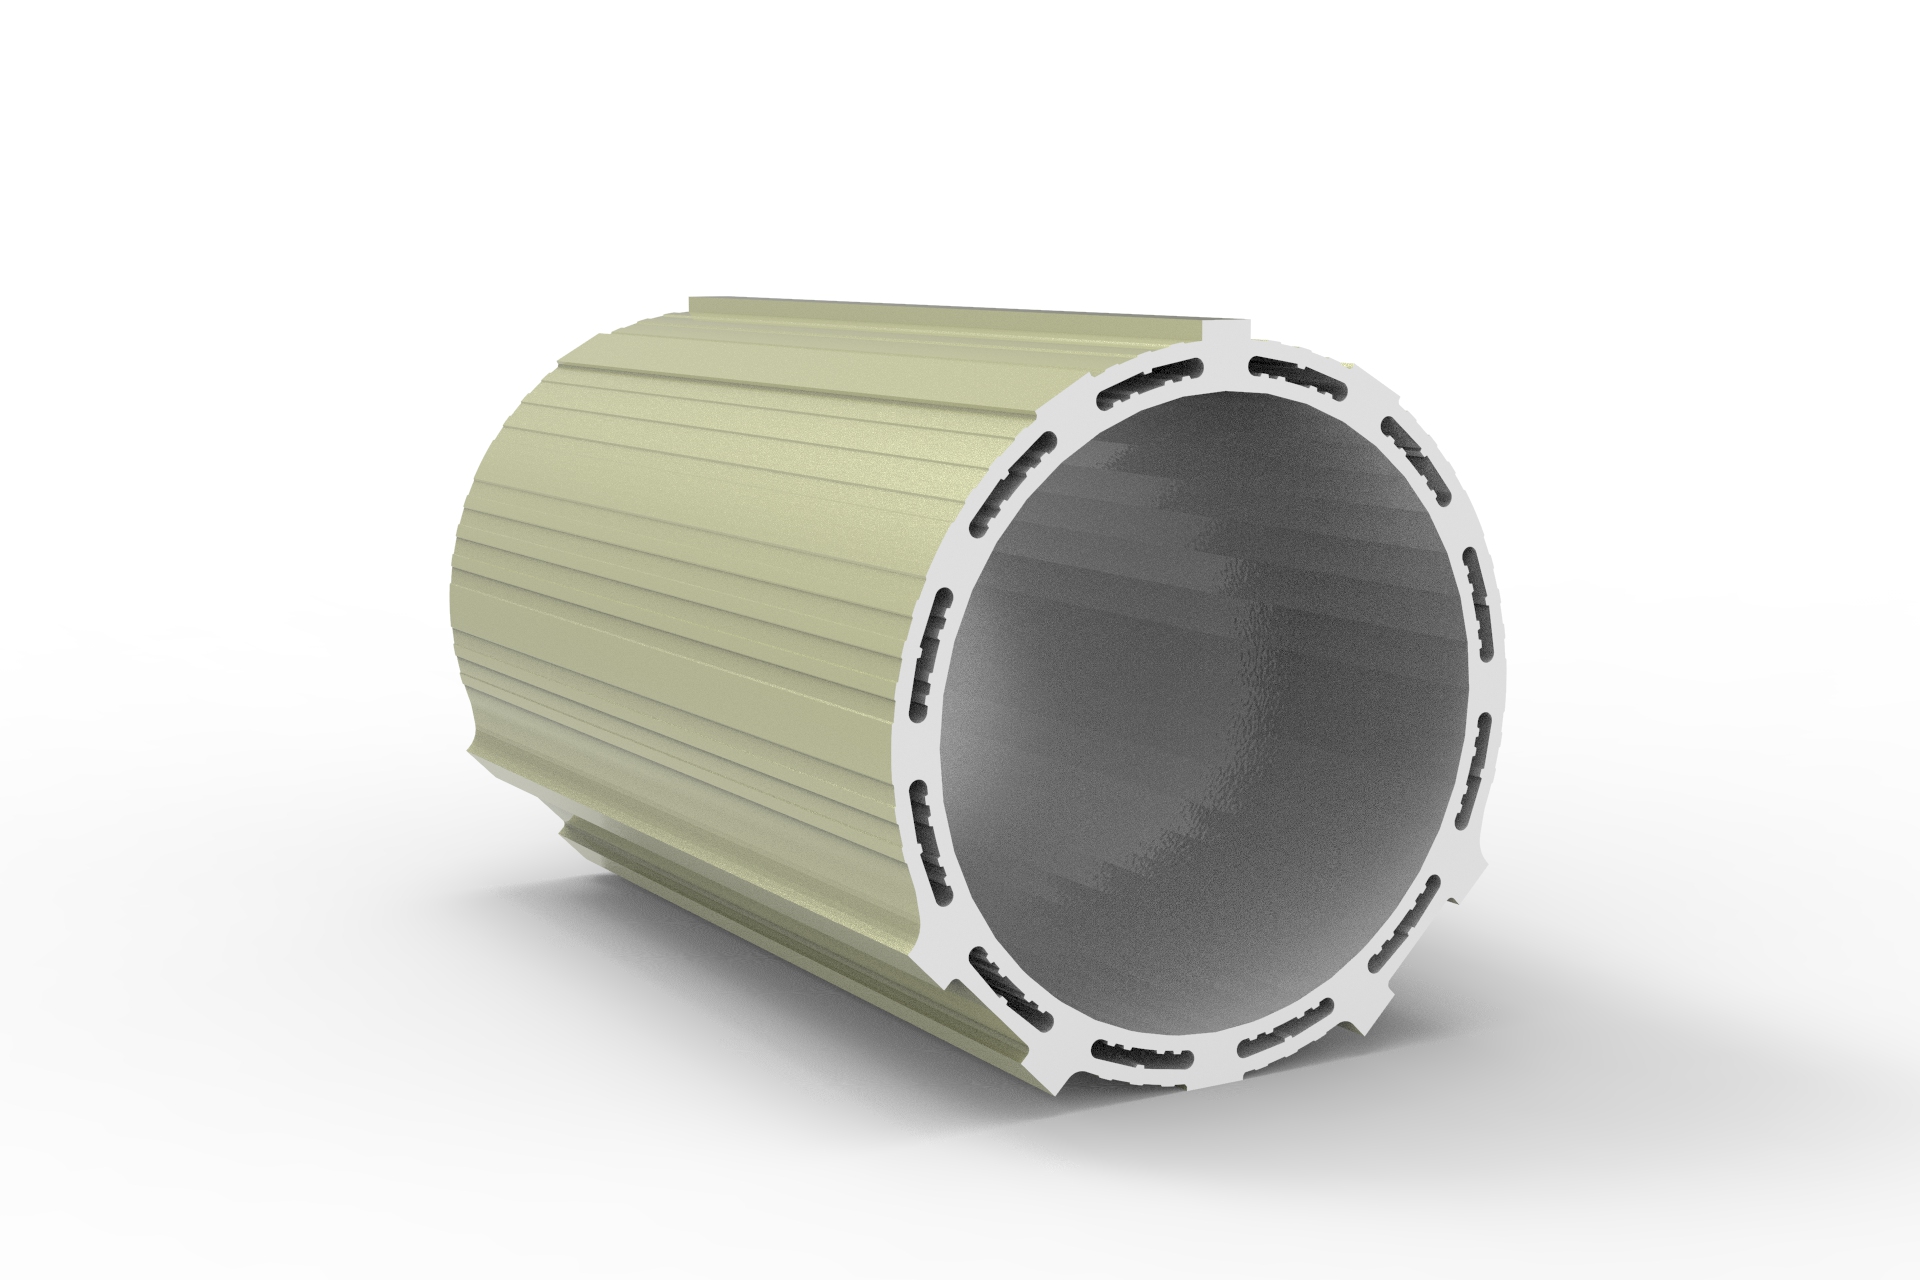
What casement window specs should I compare for windy and rainy project sites?
Are there better material options for sliding windows if aluminum prices rise?
How do I ensure aluminum casement windows can handle extreme coastal winds?
What is the typical minimum order quantity for commercial sliding windows?
Are there energy-saving alternatives to sliding windows that reduce material and maintenance costs?
Are energy-efficient Awing windows a practical alternative for reducing long-term building costs?
What alternatives to traditional sliding doors can lower costs without sacrificing durability?
What alternatives to industrial profiles can reduce material costs without hurting strength?
Extruded Aluminium Profiles: Flexible Manufacturing for Diverse Customer Needs
Why Aluminium Curtain Walls Are Popular in Modern Architecture
How do I choose a decorative profile that stays stable in humid or harsh environments?
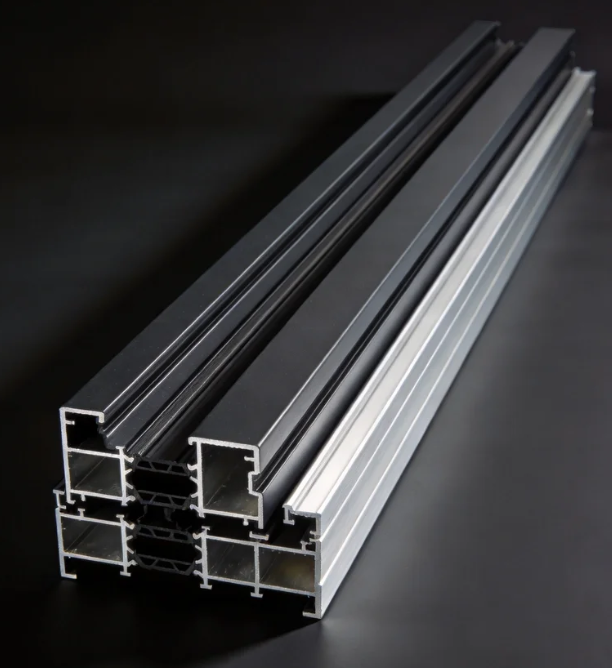
How do I choose an architecture profile that stays stable in harsh outdoor conditions?
How can I compare Awing window specs to avoid poor performance in harsh weather?
How can I compare Sliding door sizes and hardware ratings for harsh commercial environments?
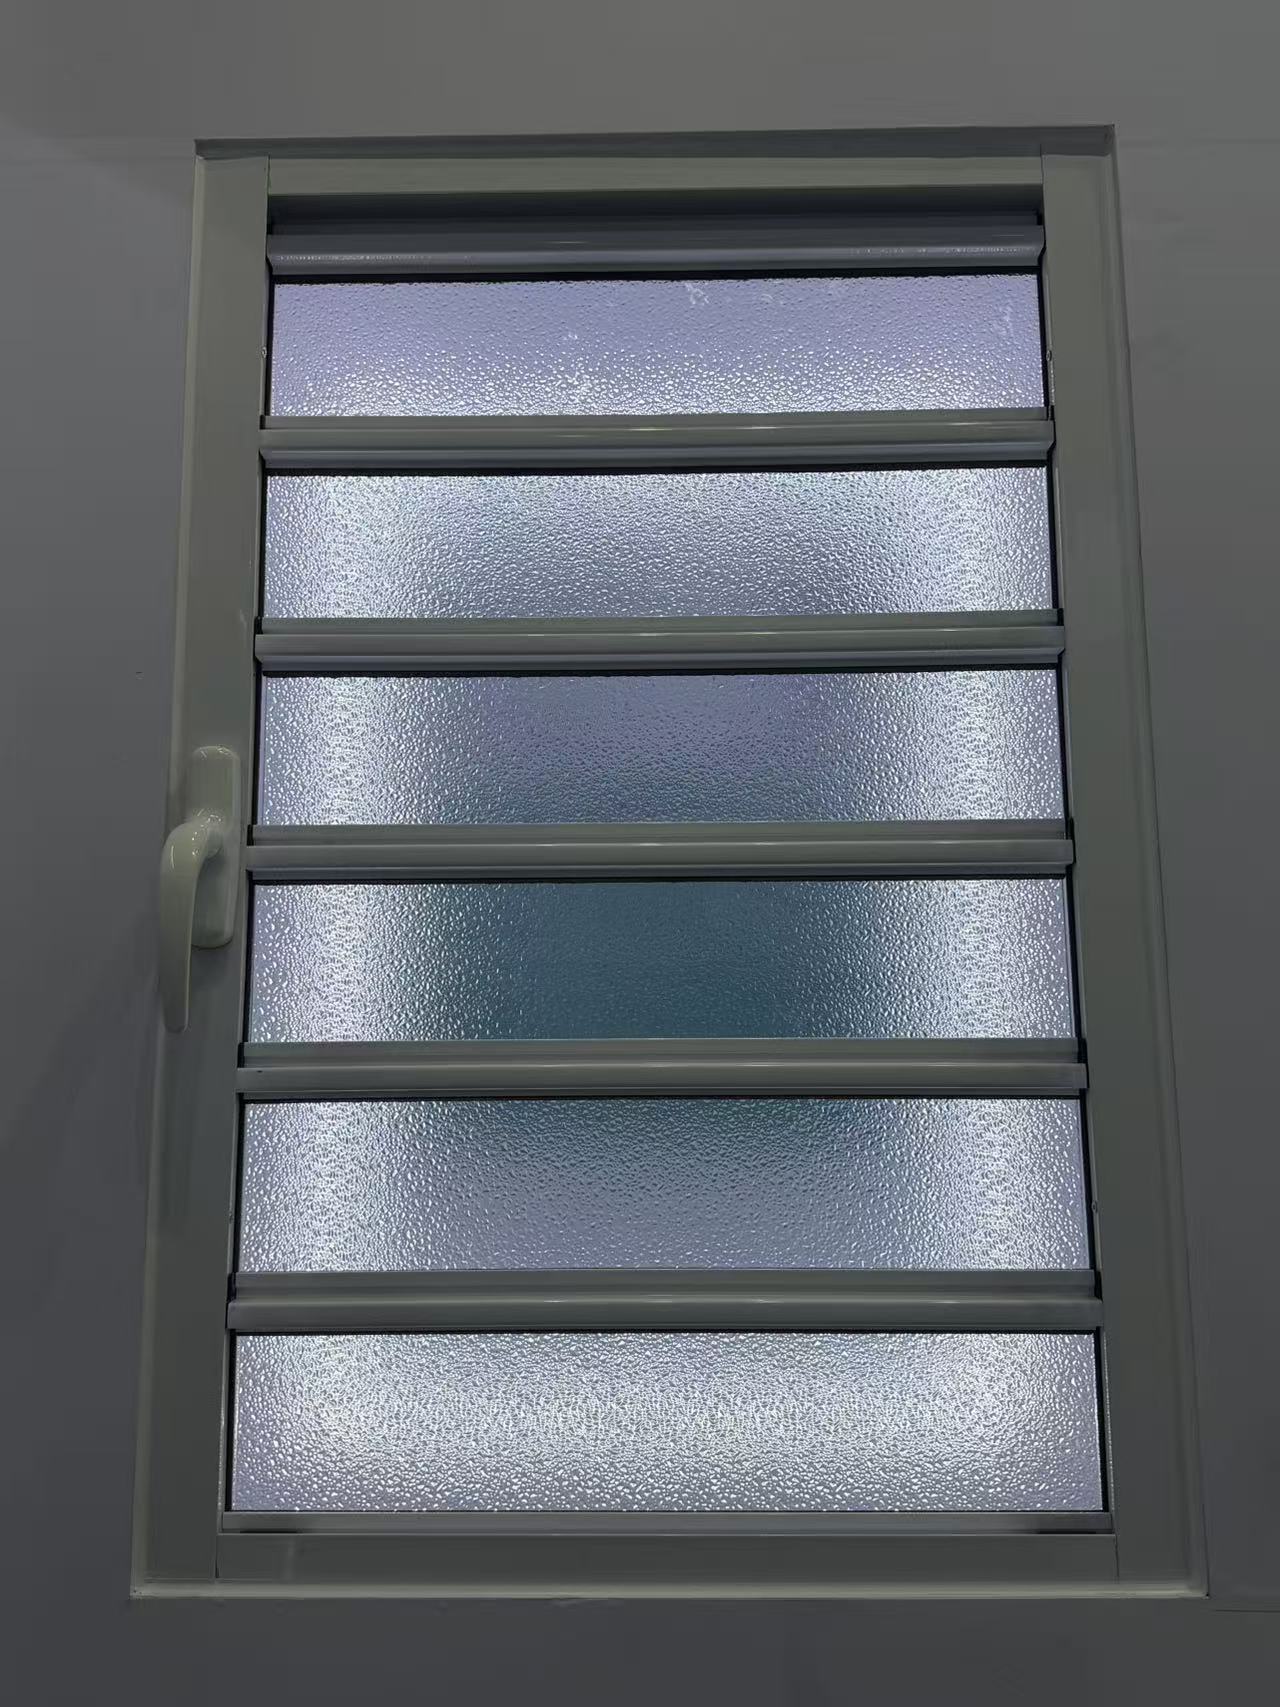
How do I choose the right shutter specifications for harsh climates without overpaying?
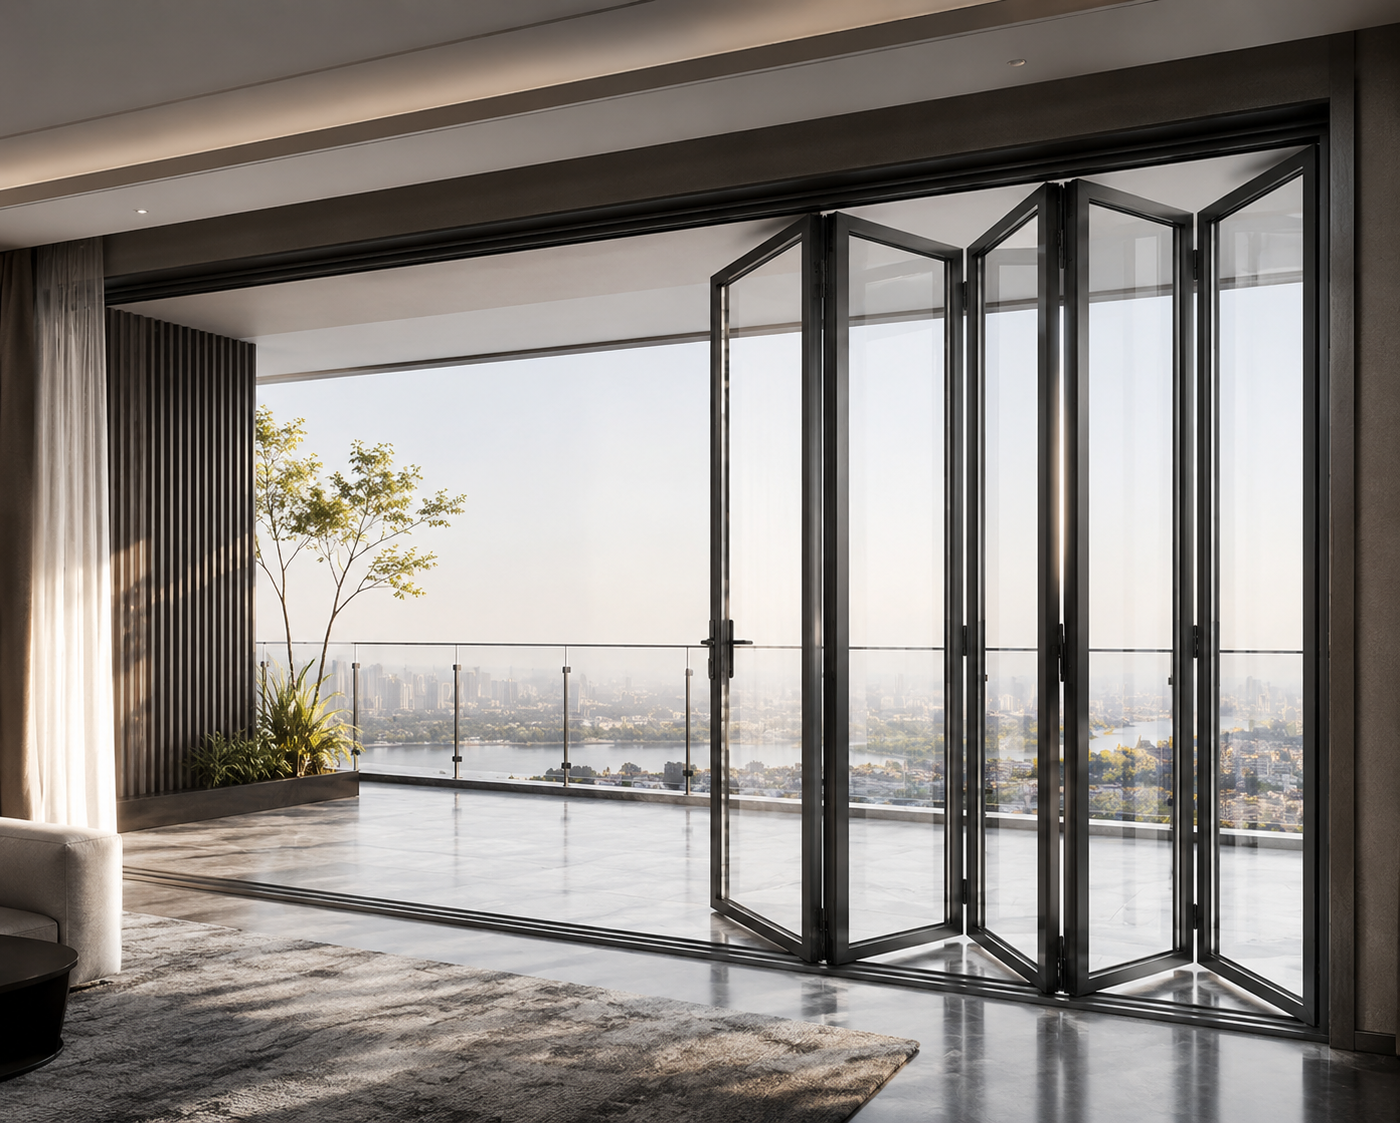
What eco-friendly alternatives to folding doors can cut costs without hurting durability?
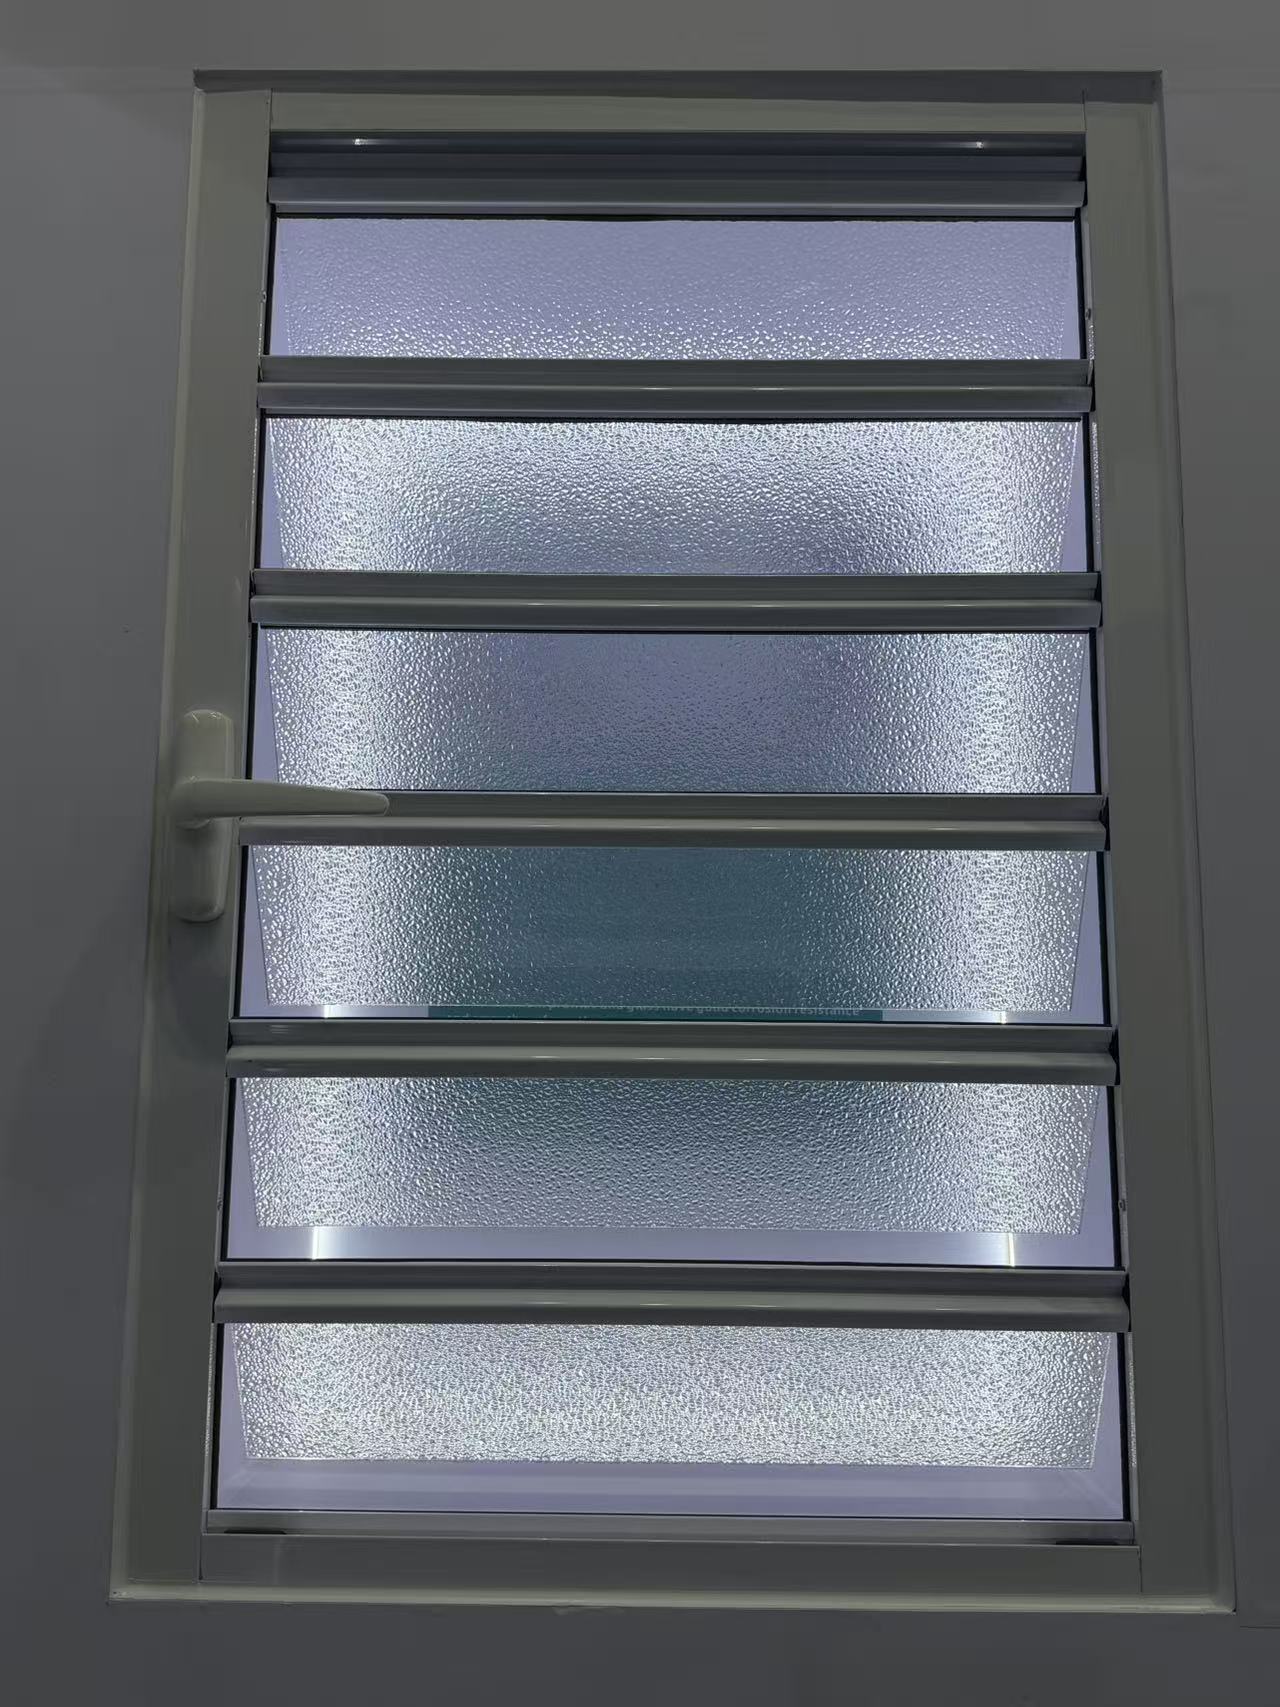
How do I choose the right shutter specifications for harsh weather without overpaying?
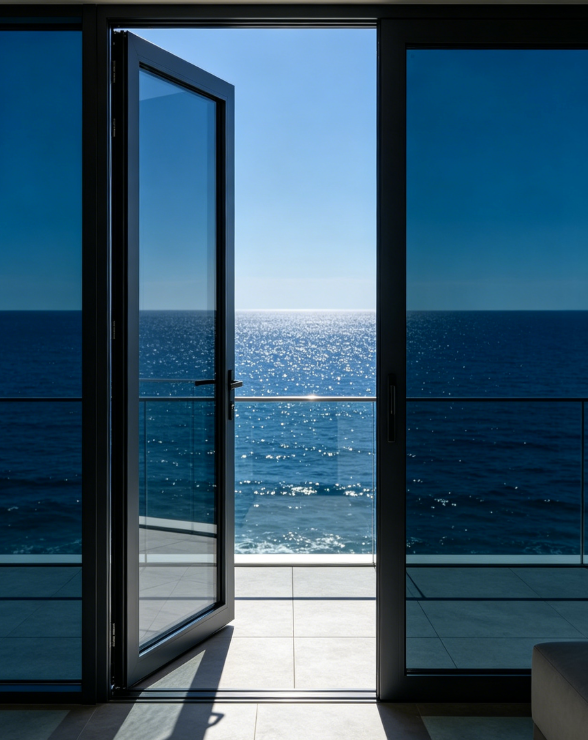
What eco-friendly casement door materials can lower costs without hurting durability?
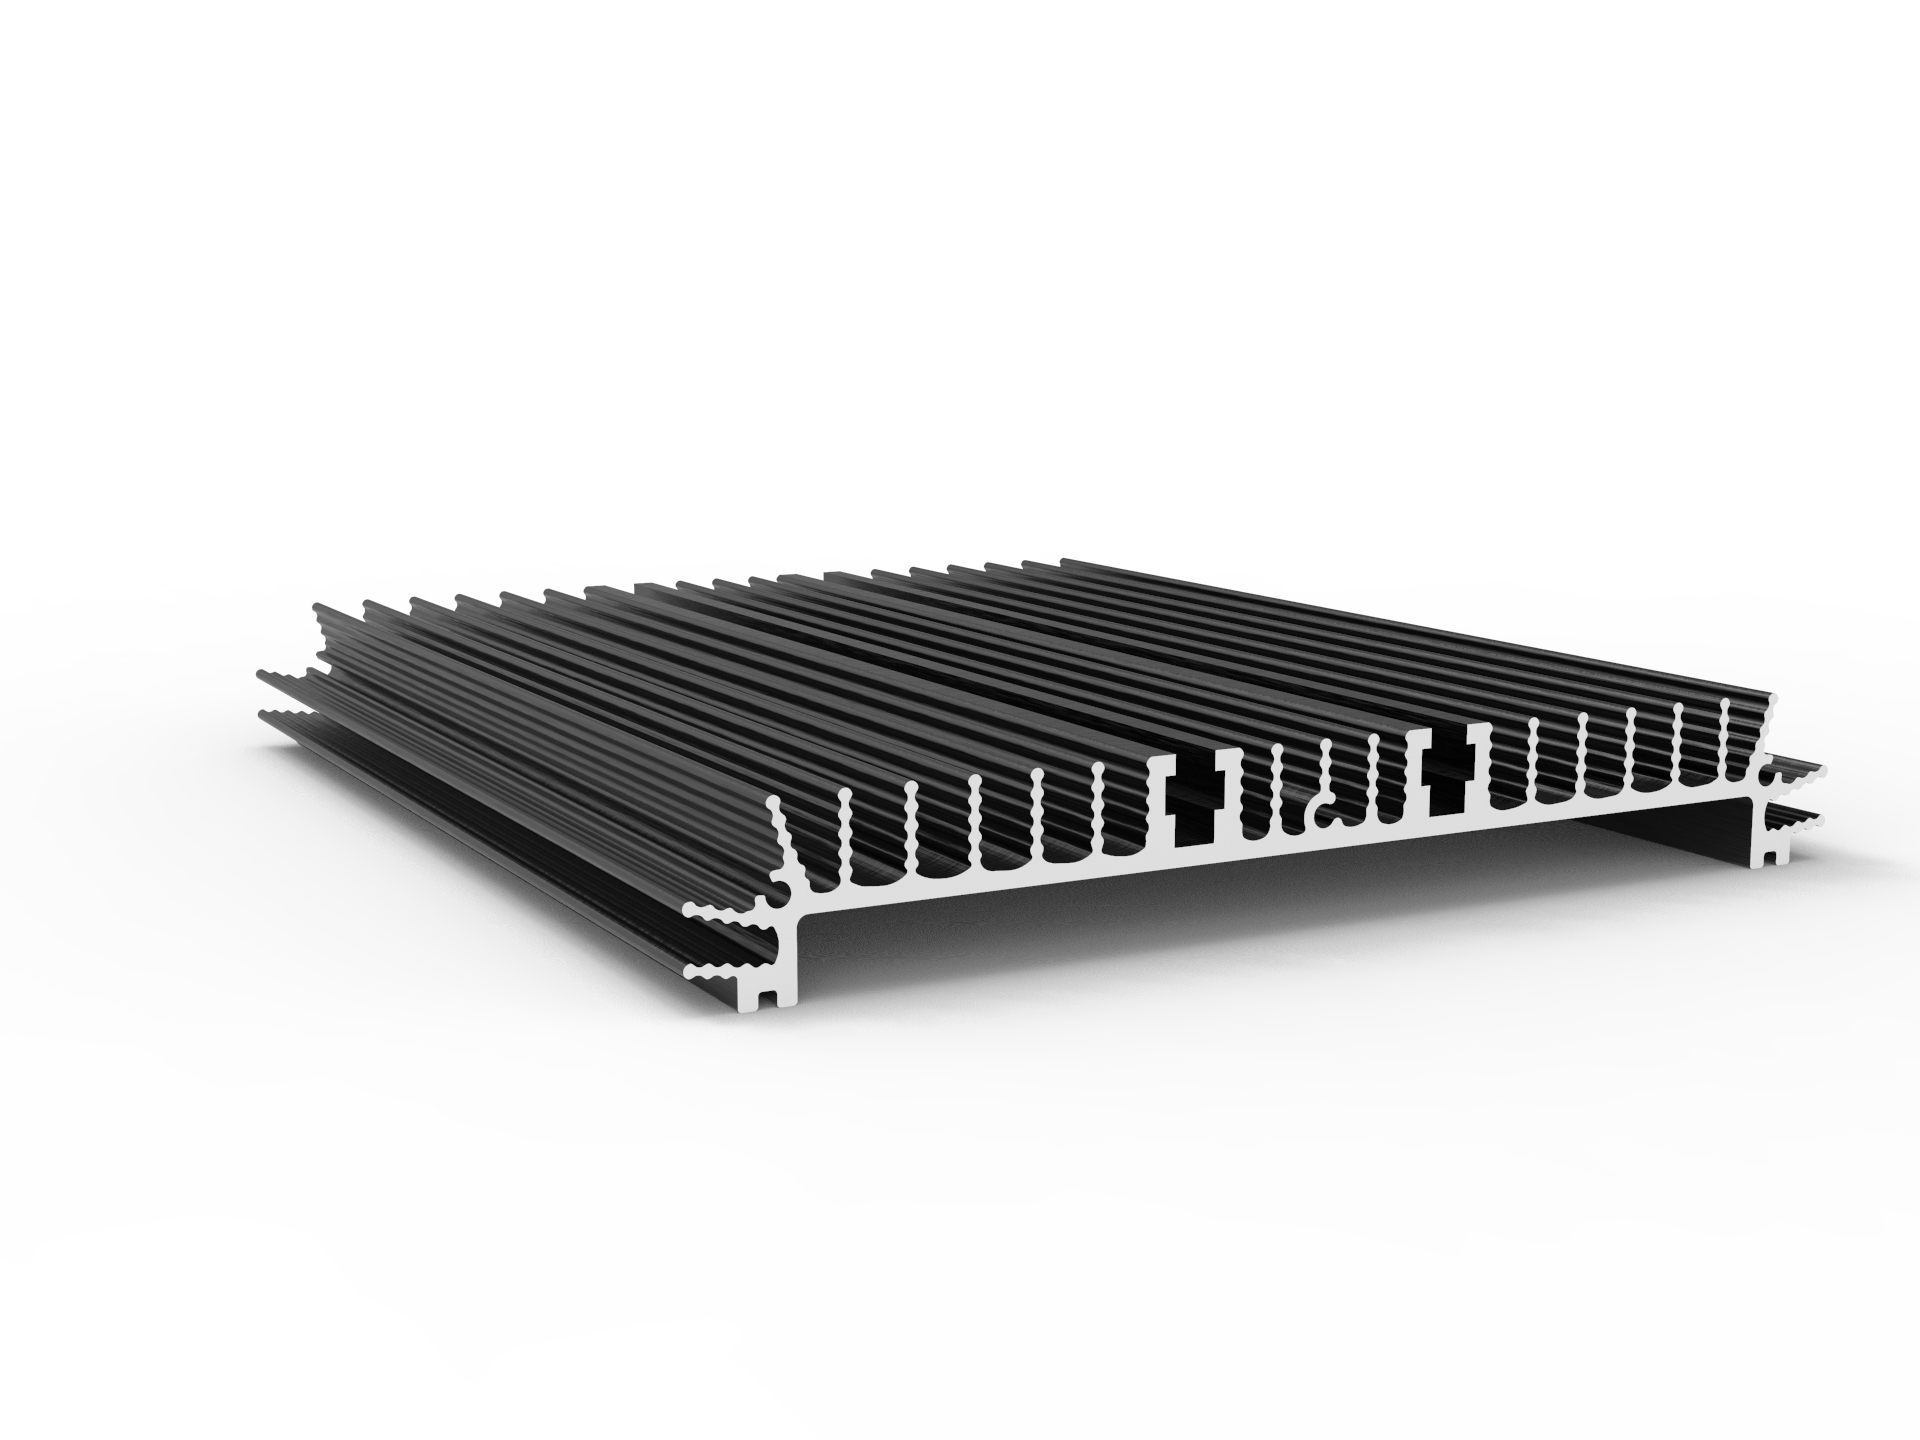
What newer materials can replace industrial profiles without raising costs or supply risks?
How do I choose a decorative profile that stays stable in humid, high-traffic spaces?
What sustainable material alternatives can replace aluminum architecture profiles?
What should I check in Awing window specs to ensure reliable performance in harsh weather?
How can I compare Sliding door sizes and thermal ratings for harsh climates before buying?
What newer materials can replace aluminum in awning windows without raising our costs?
How do I choose the right Sliding door specs for smooth operation in harsh environments?
How do I choose a folding door that stays stable in harsh weather and heavy daily use?
How can I choose the right shutter specifications for harsh weather and long-term use?
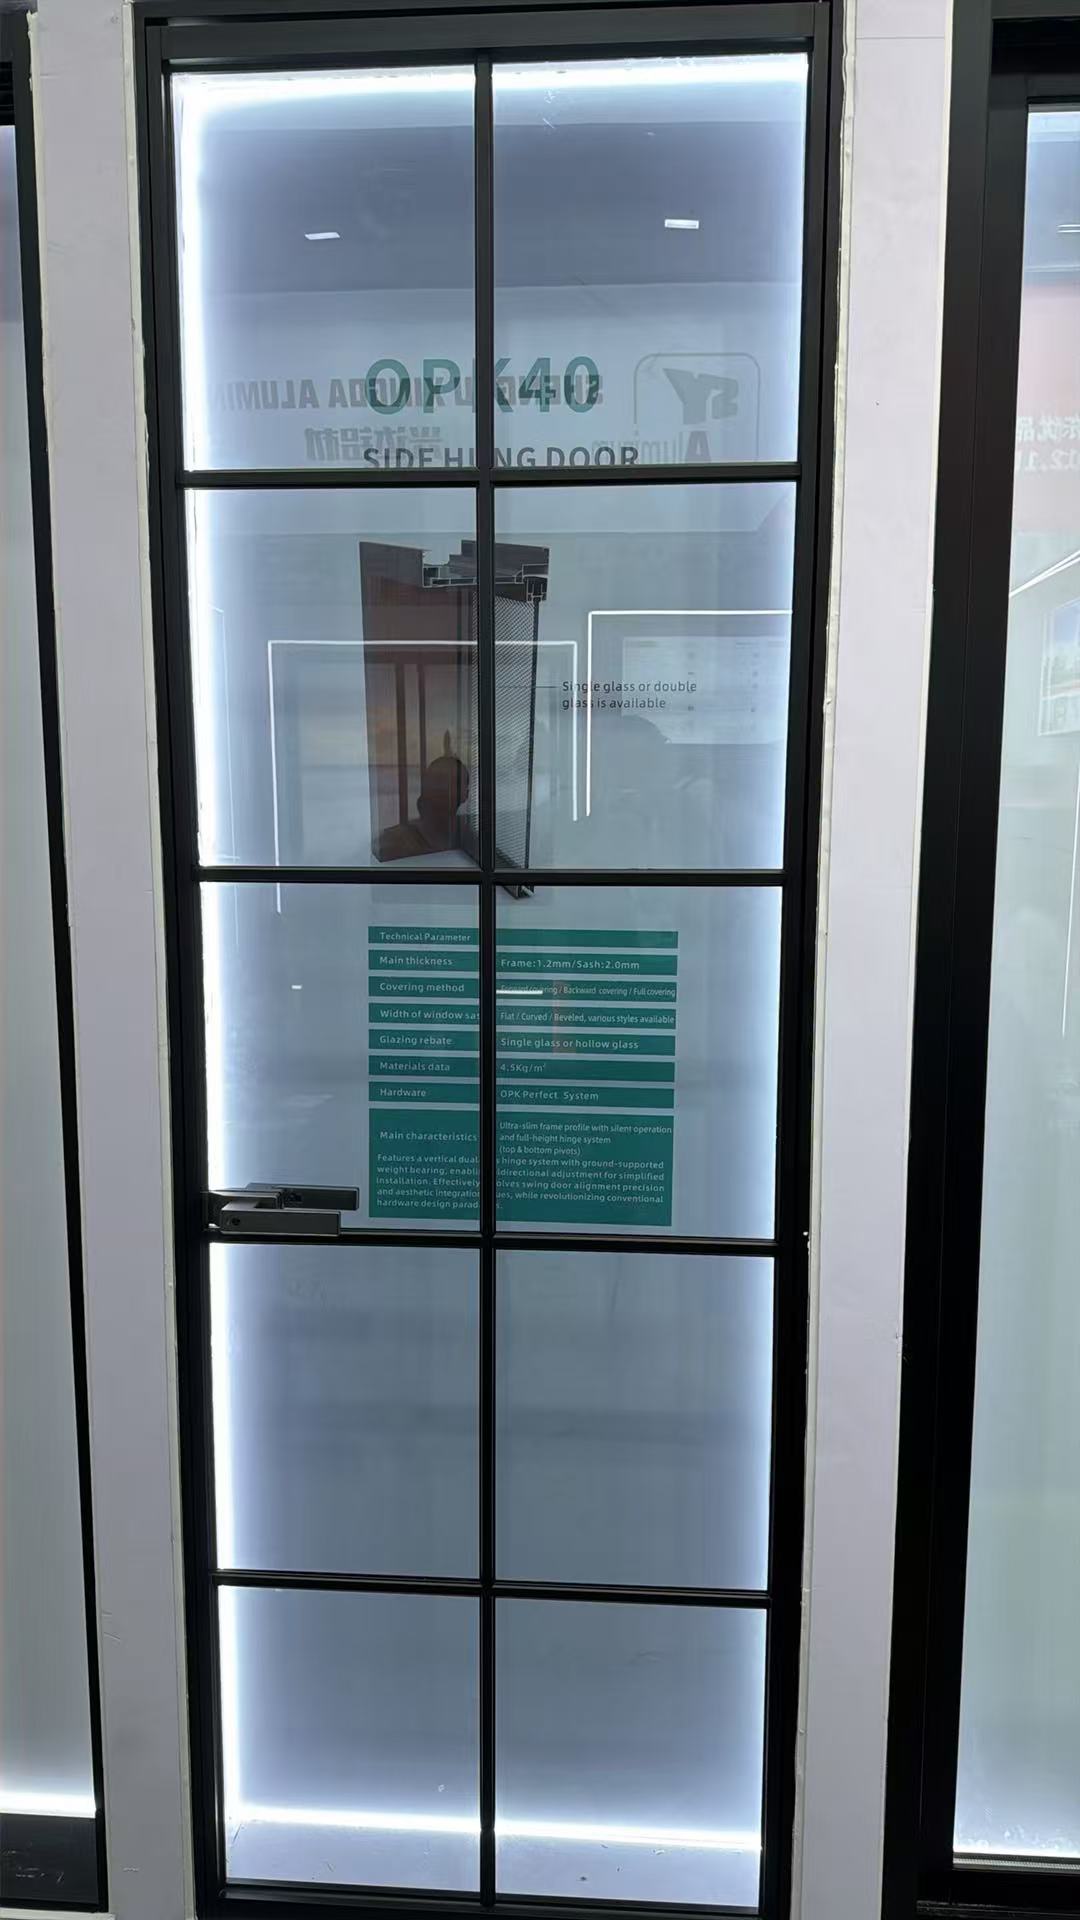
How do I compare casement door U-values, hardware, and weather sealing before buying?
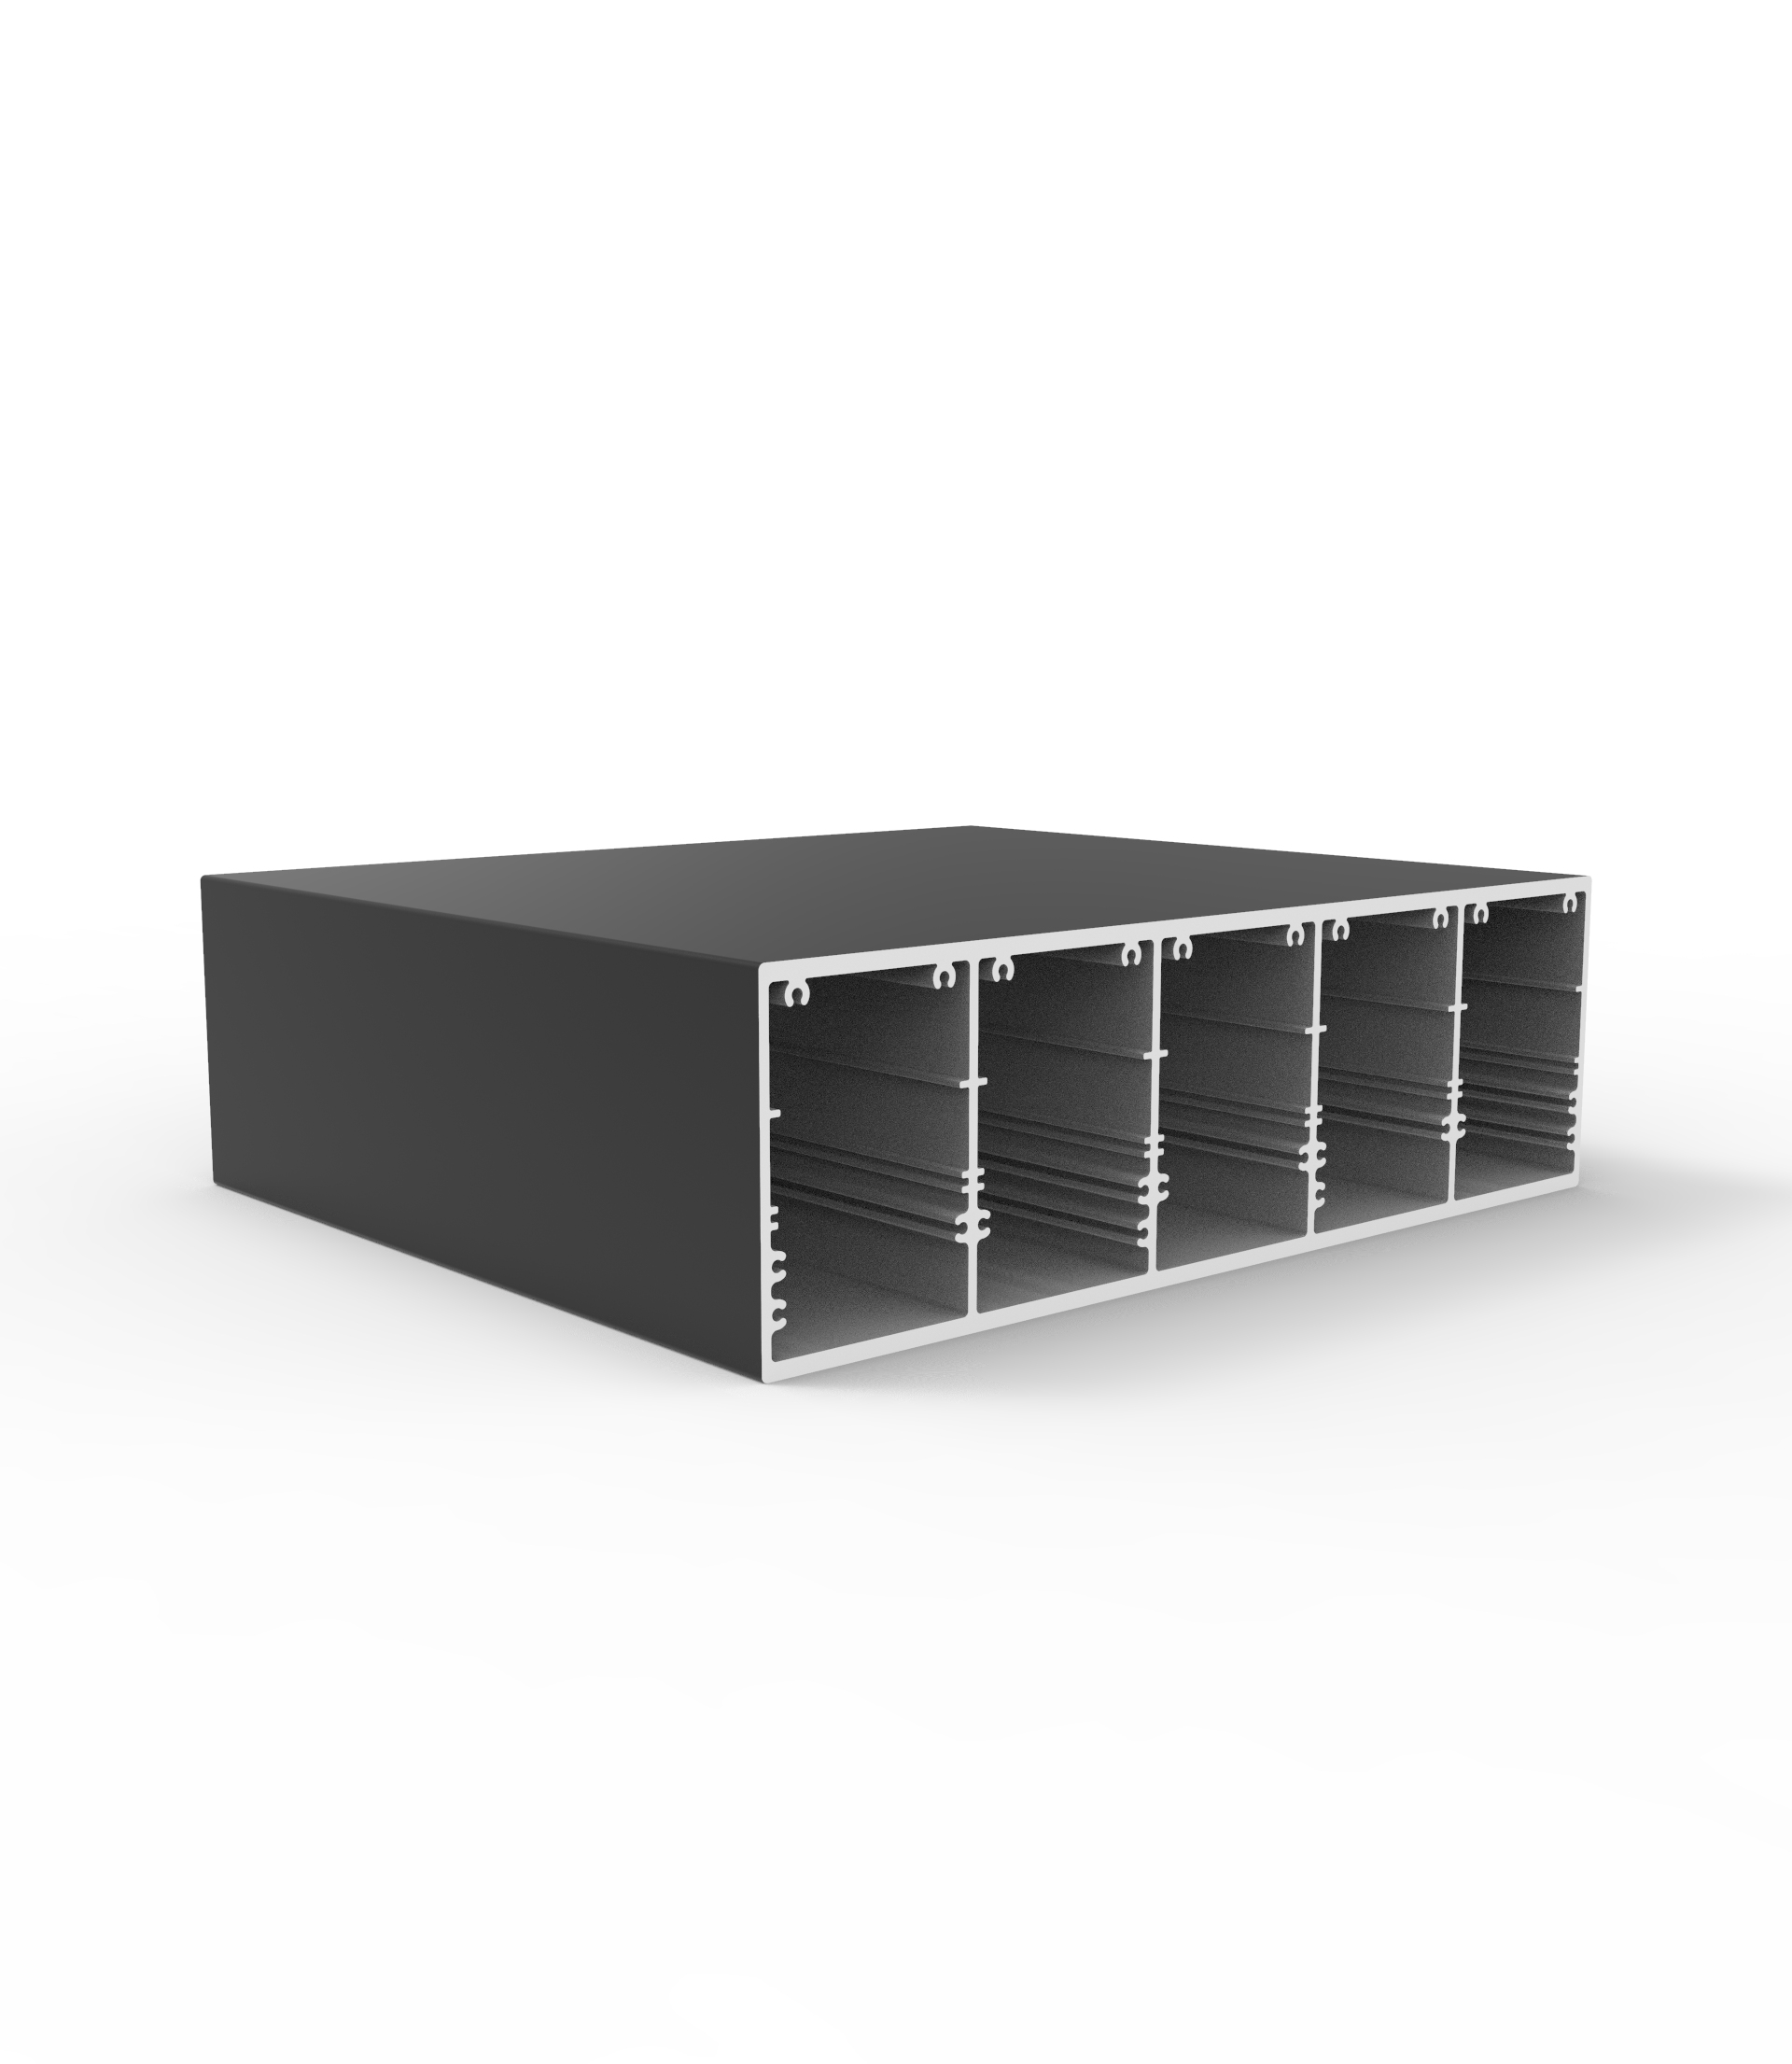
How do I choose the right industrial profile size for strength and load needs?
How do I choose the right shutter specifications for harsh weather and long-term commercial use?
How do I choose the right Casement door size and hardware for harsh weather?
What greener alternatives to decorative profile can cut costs without hurting durability?
What lower-cost, eco-friendly materials can replace decorative profiles?
What lower-carbon alternatives to aluminum architecture profiles are practical for our project?
How can I compare sliding door systems for insulation, security, and long-term use?
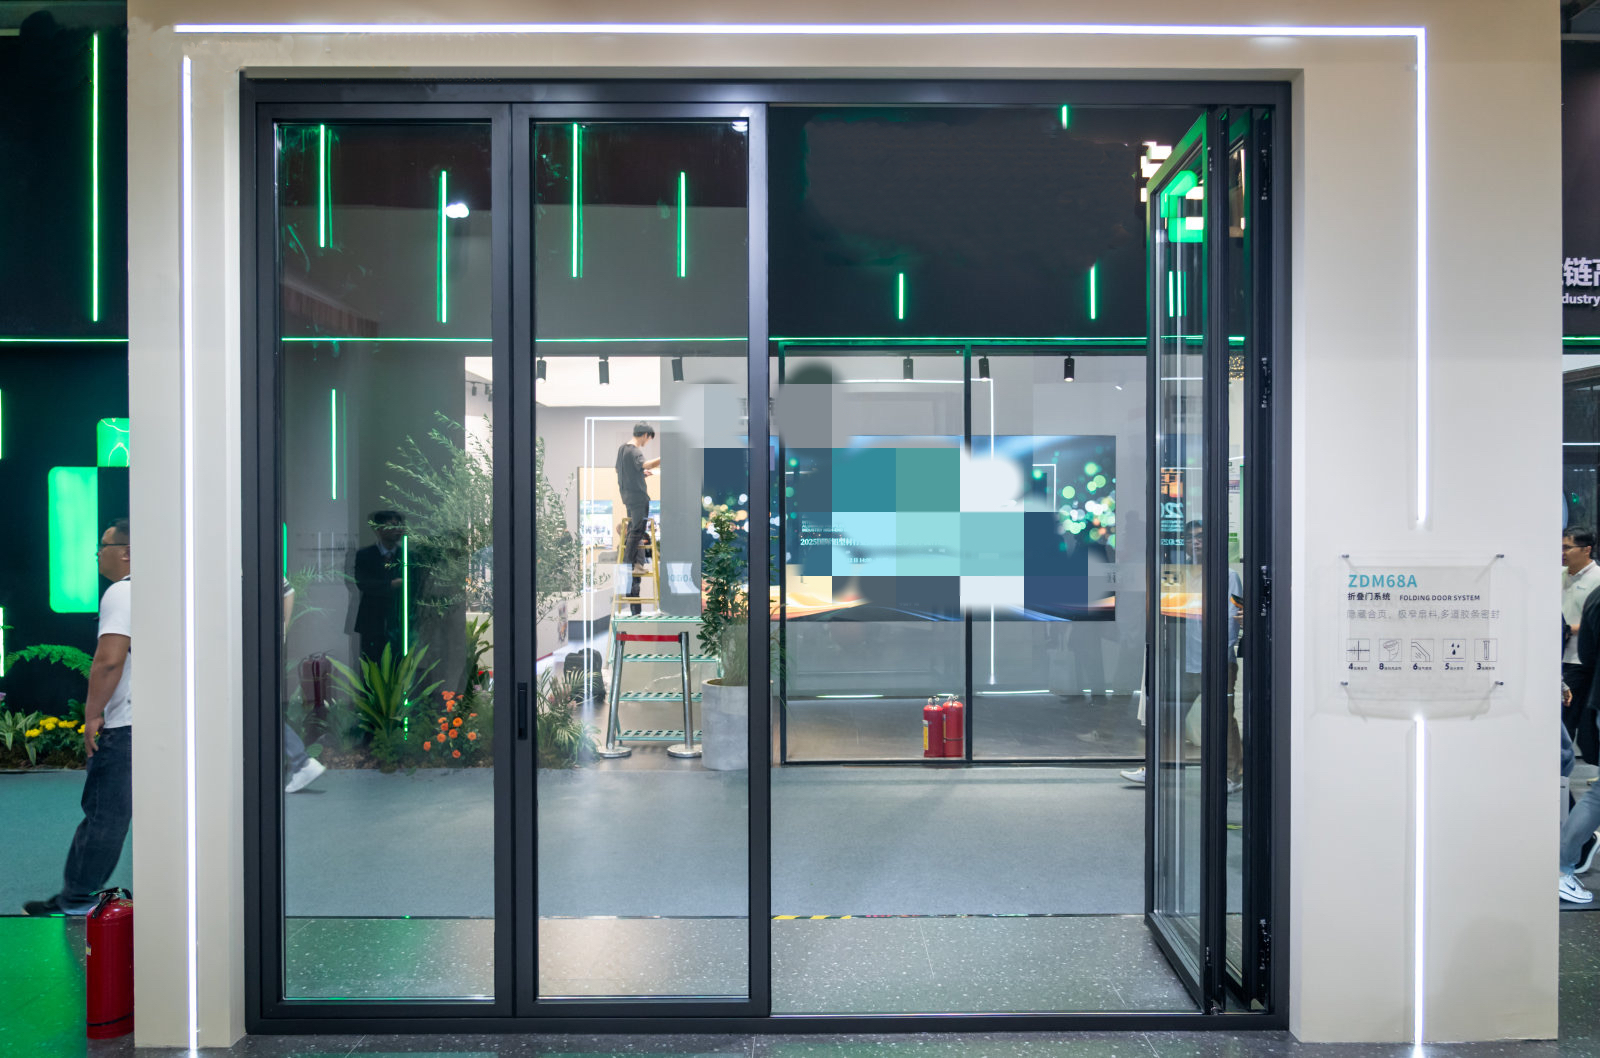
What is the standard production lead time for bulk orders of folding doors?
How do I choose the right Awing window size and glass specification for harsh weather?
How can I test shutter samples so the final bulk order matches their quality and finish?
Can suppliers make custom double glass casement doors from my CAD drawings?
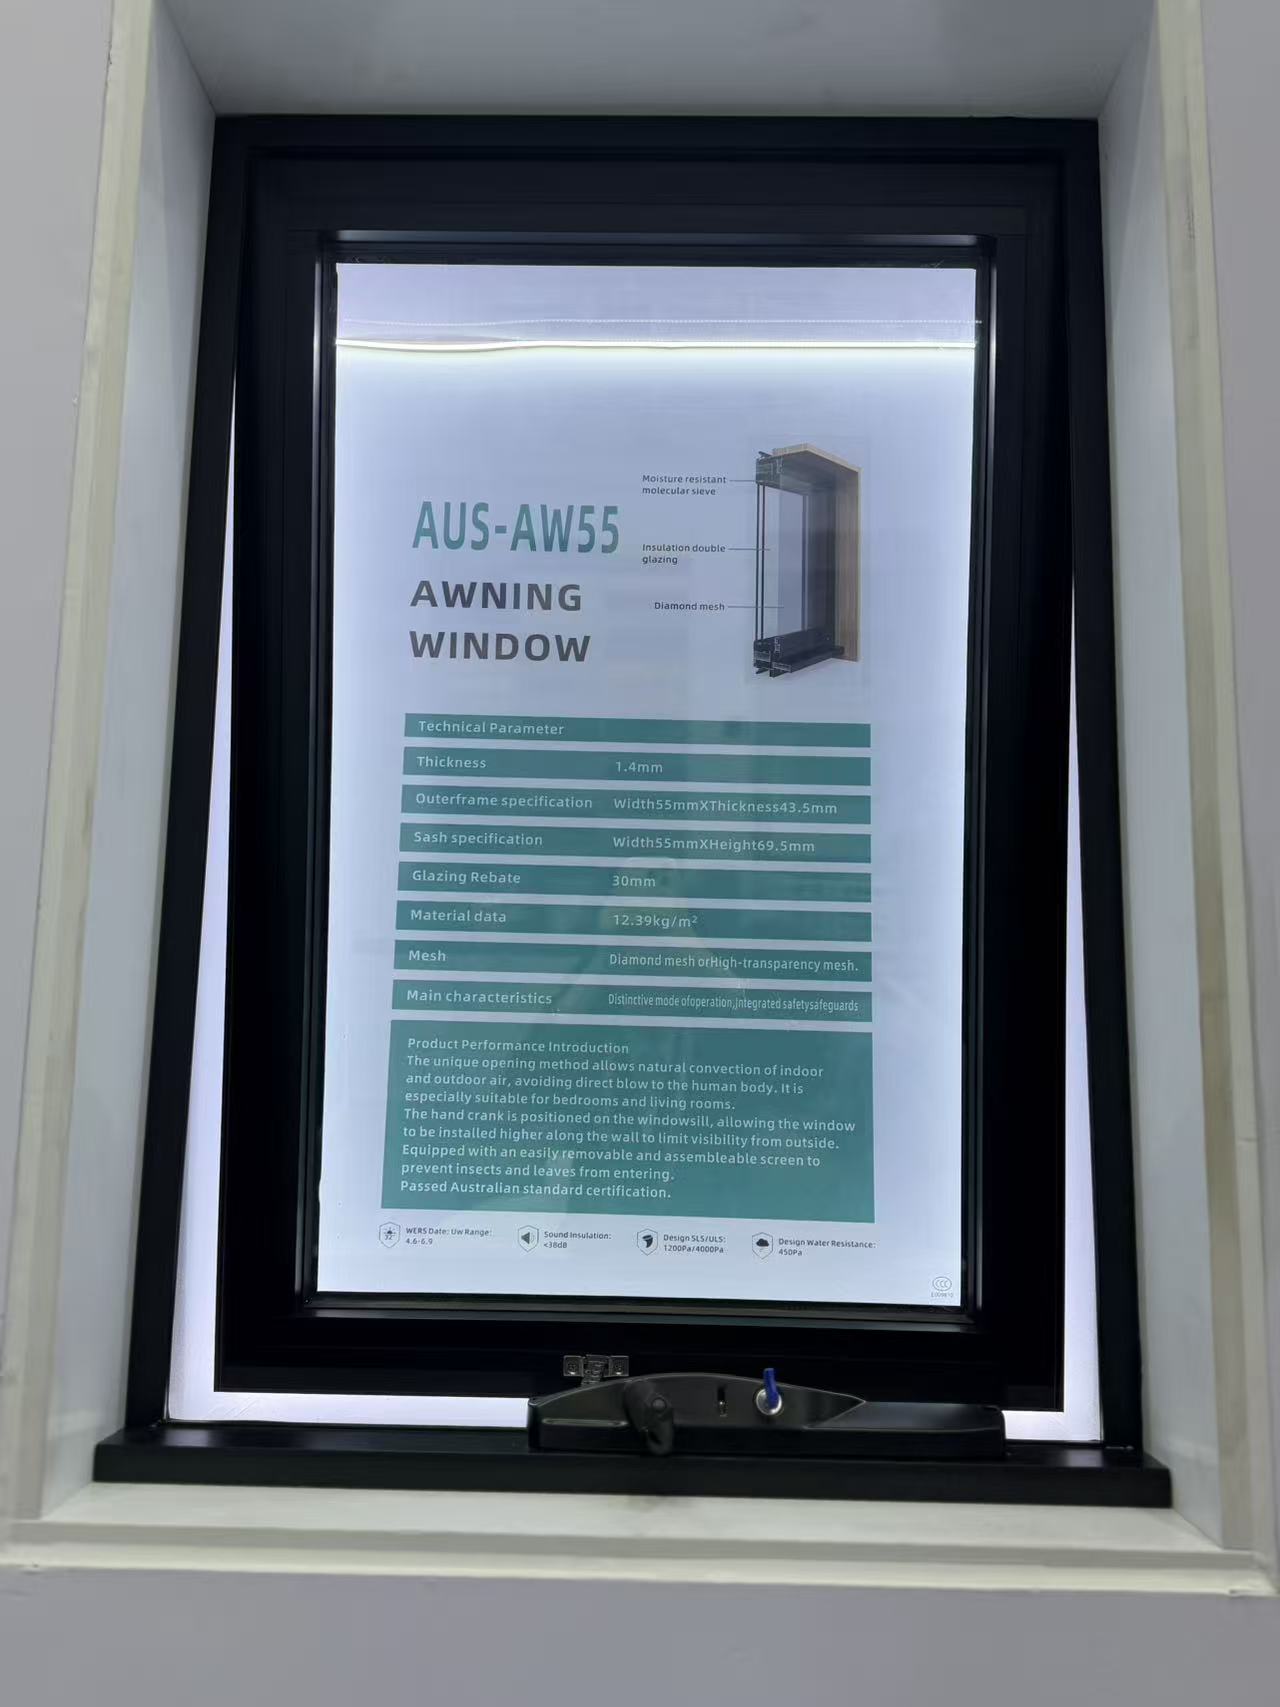
What safety certifications should I request when importing awning windows?
How long does it usually take a factory to make custom shutter samples?
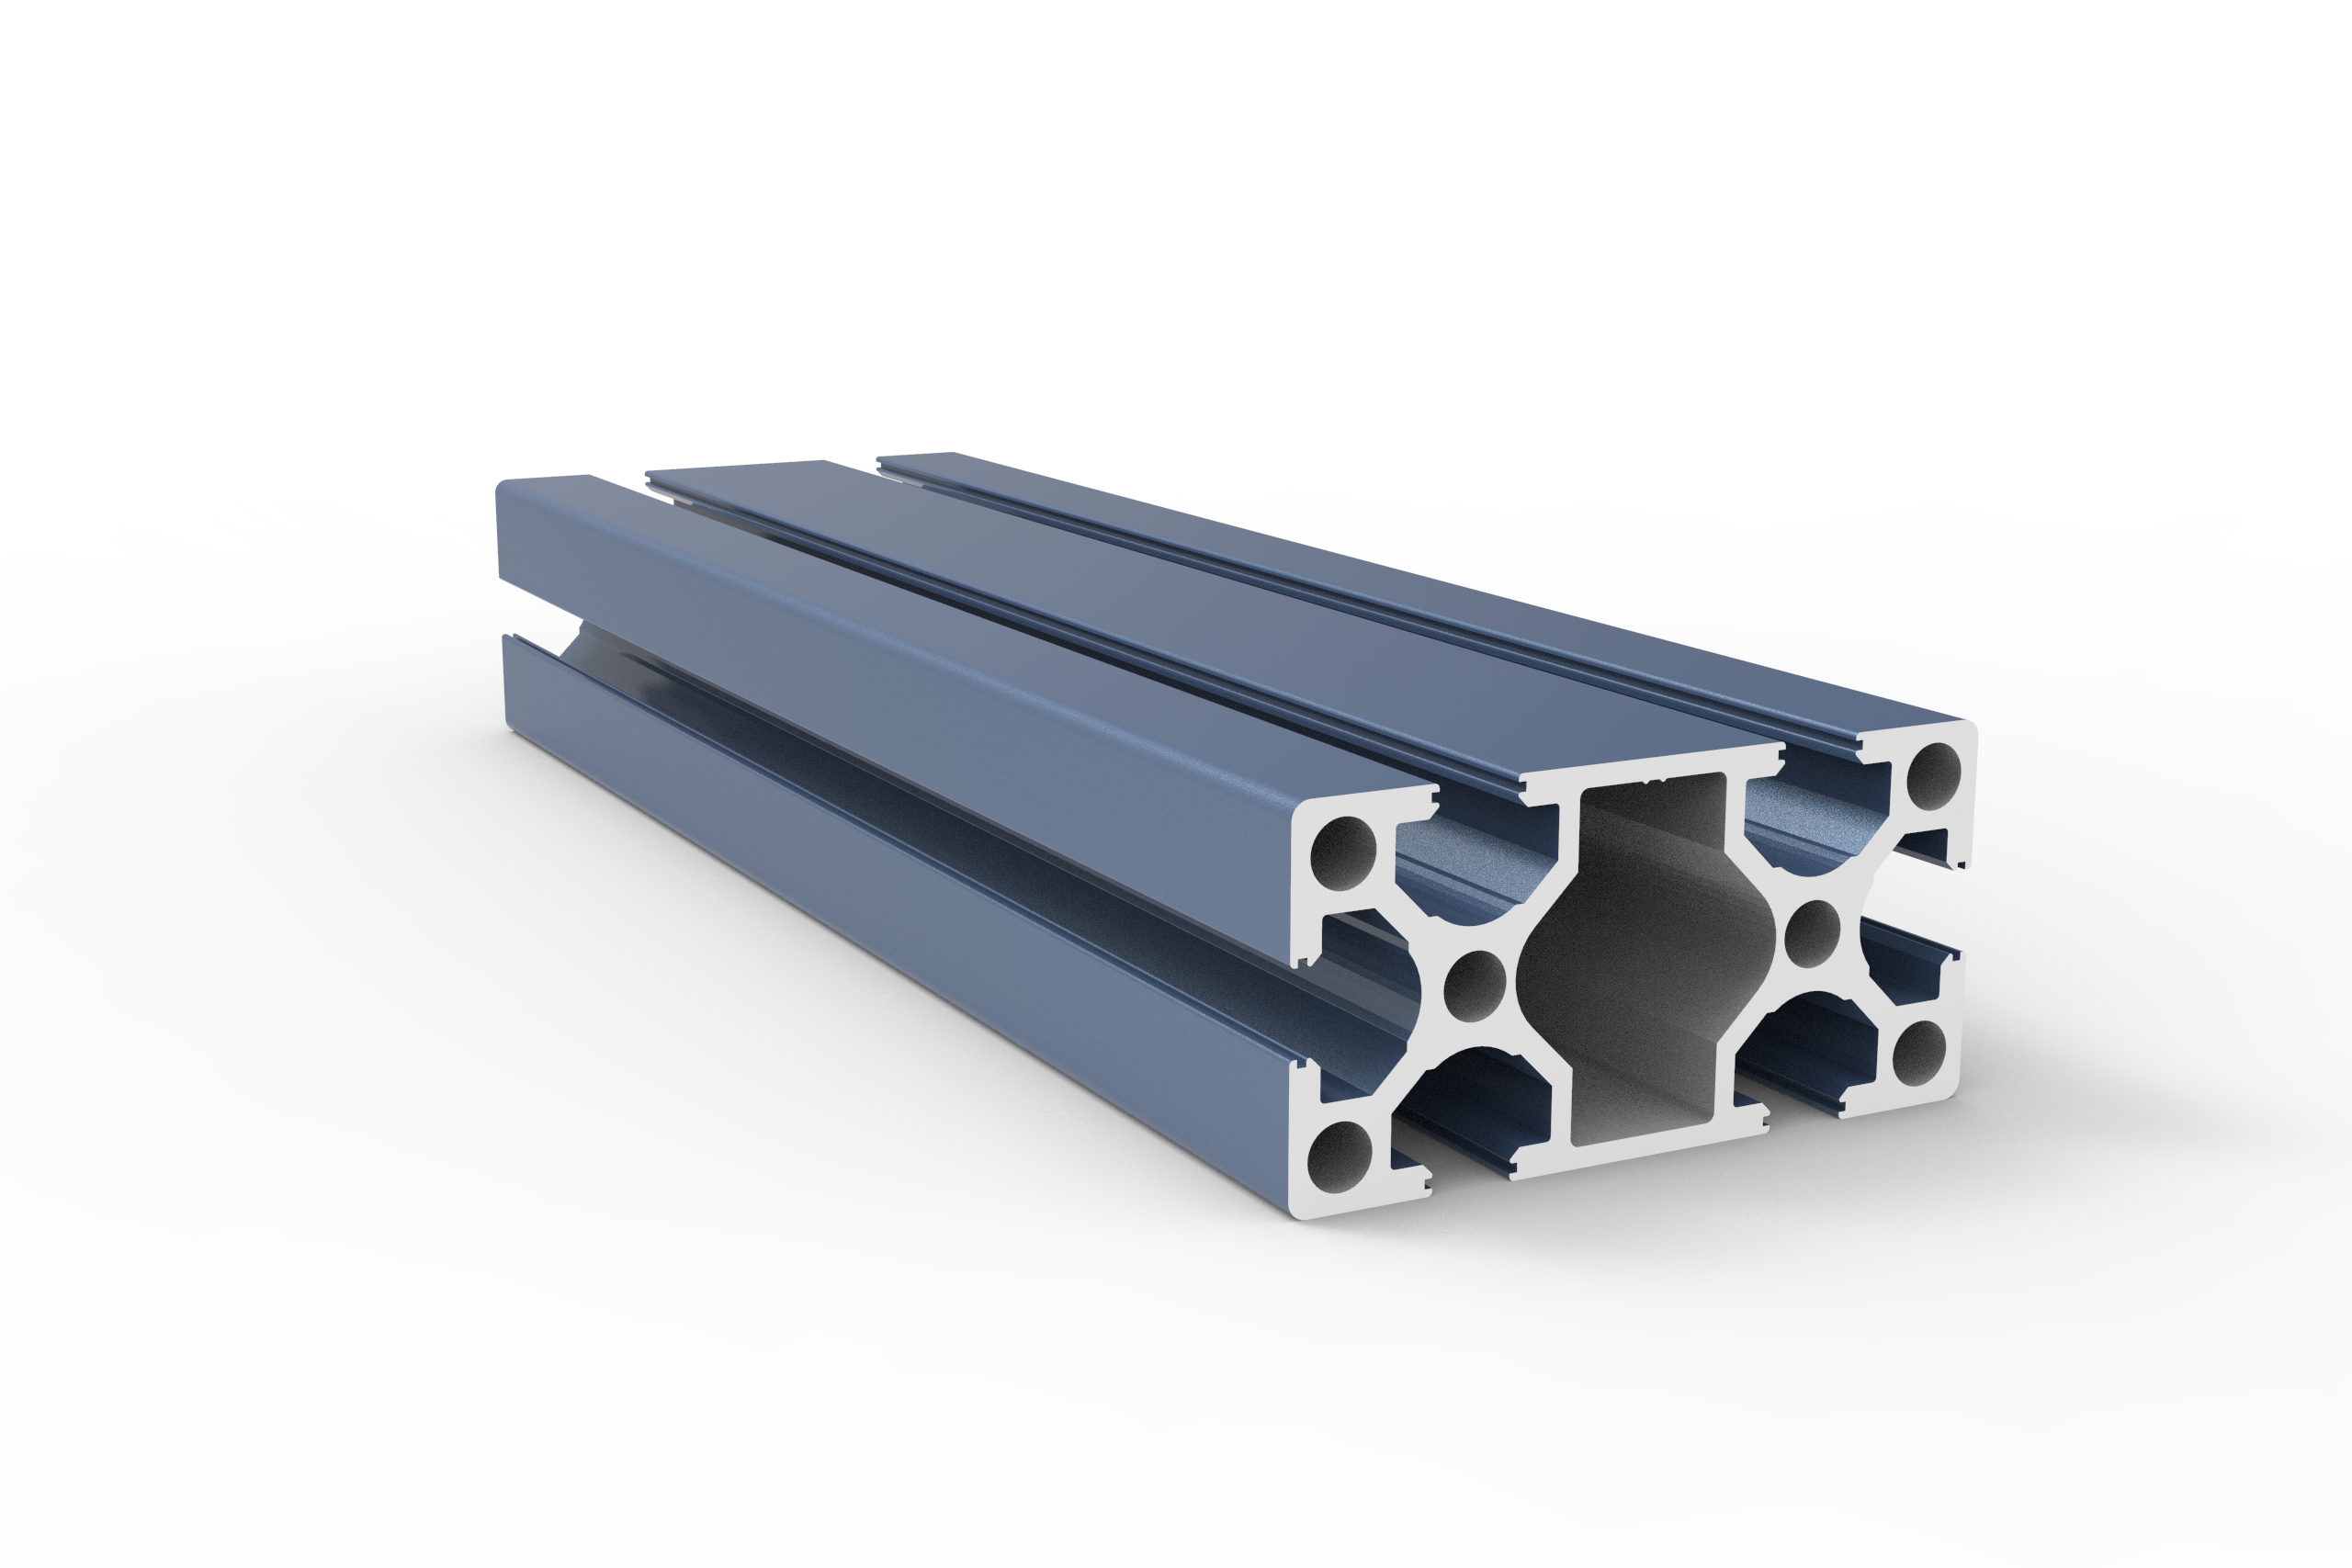
What T-slot industrial profile size is best for a heavy duty machine frame?
How do I choose the right stainless steel decorative profile for high humidity areas?
How do I choose the right aluminum architecture profile for coastal buildings?
How do I choose the right stainless steel decorative profile for high humidity areas?
What wind load specs should I check for aluminum casement windows in coastal high-rises?
How do I know which aluminum industrial profile alloy is best for heavy machinery frames?
How do I choose the right alloy grade for aluminum architecture profiles?
How do I select the right heavy-duty hardware for exterior commercial floding doors?
How do I select the right glass thickness for bulk awing window orders?
What frame thickness is recommended for commercial aluminum casement doors?
What frame thickness is best for high-rise commercial sliding windows?
How to choose weather resistant aluminum floding door specs for commercial use?
How do I choose the best water tightness rating for commercial awing windows?
How do I choose the right frame material for commercial casement doors?
How do I choose the right wind load rating for sliding windows in coastal areas?
What is the best material for outdoor decorative profiles to prevent rust and fading?
How do I choose the right track thickness for high-traffic commercial sliding doors?
How do I choose between PVC and basswood shutters for high-humidity areas?
How do I choose between double and triple glazing for casement windows in cold climates?
How do I choose the right industrial profile thickness for heavy-duty cnc machine frames?
How do I choose the right alloy for outdoor architecture profiles to prevent corrosion?
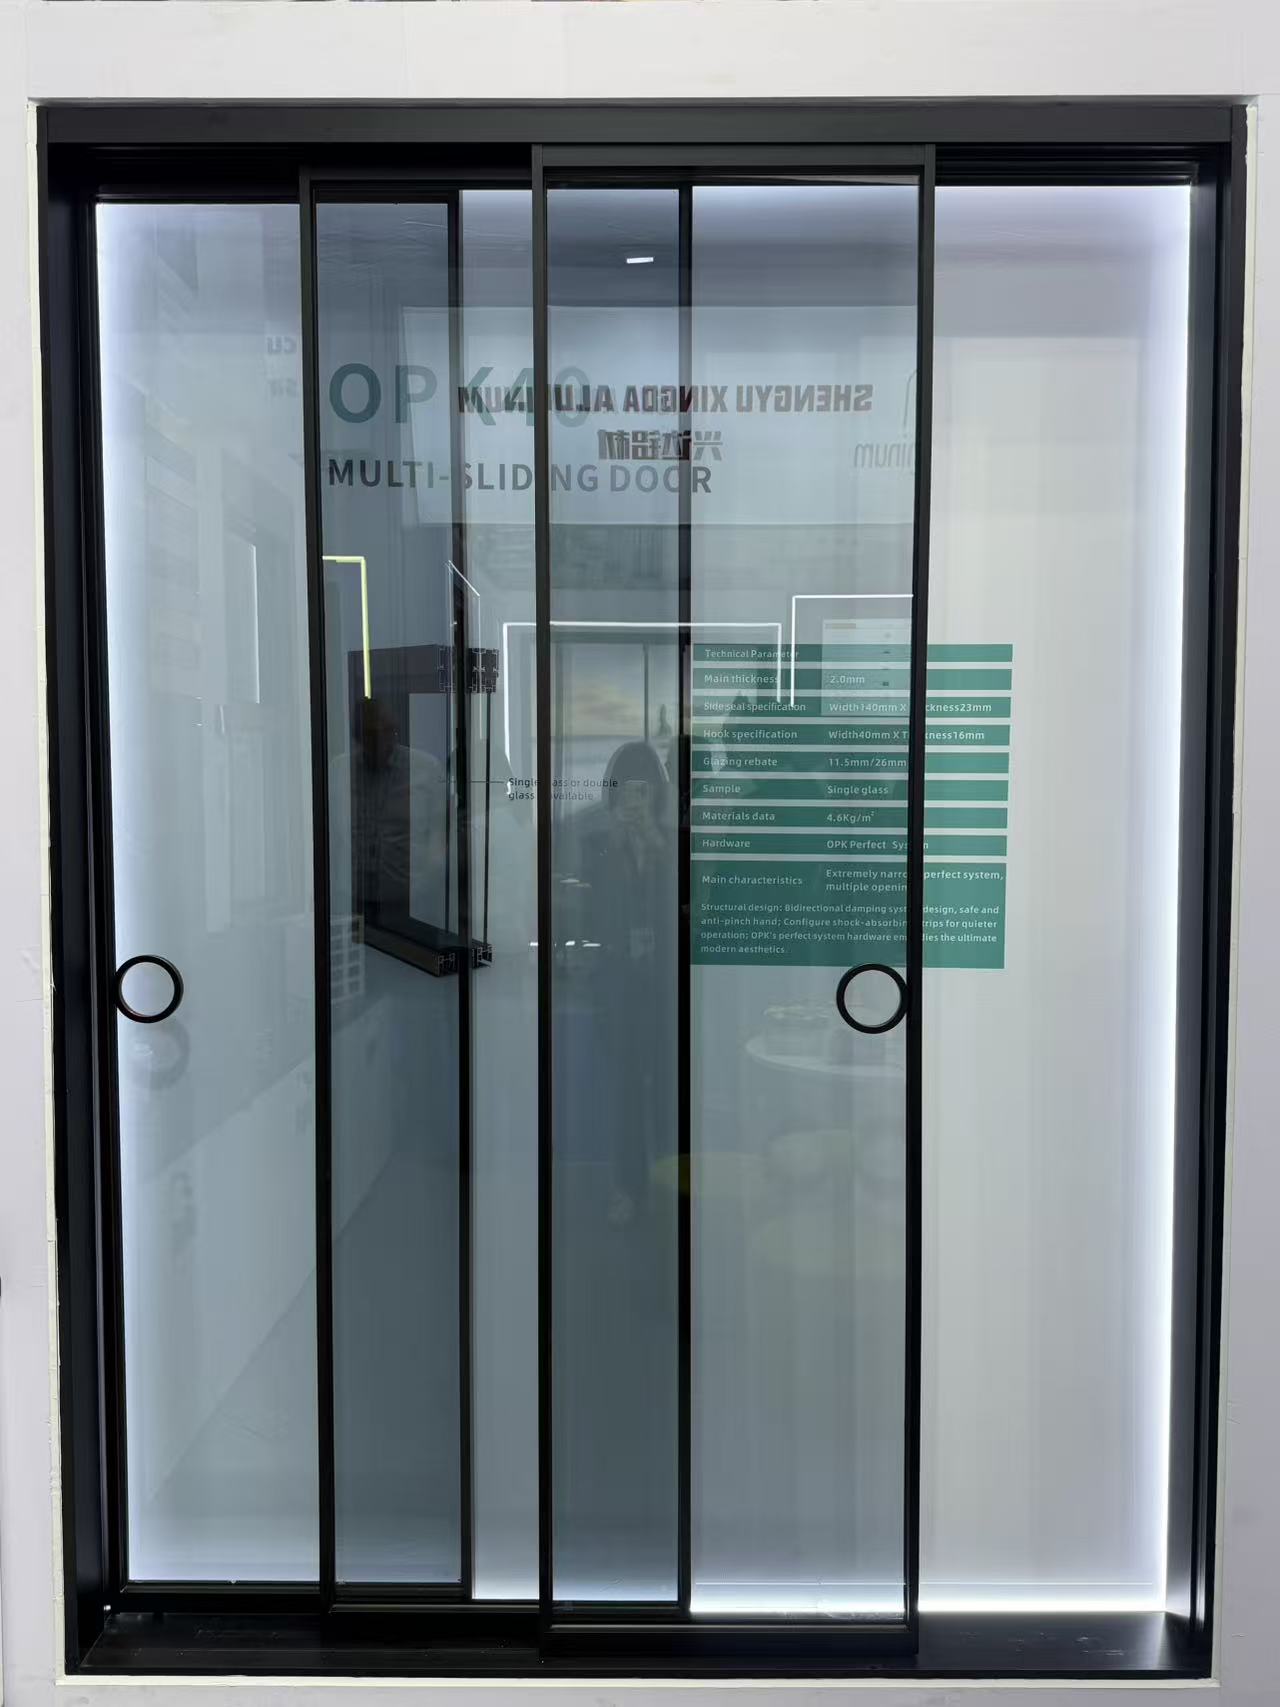
Can you design a slim frame profile for modern minimalist look?
How do I choose the right wind-resistant floding door for a coastal commercial building?
What key specs ensure a casement window can withstand heavy rain and high winds?
How do I choose the right aluminum alloy grade for heavy-duty industrial profiles?
Which alloy grade of architecture profile is best for coastal areas to resist rust?
How do you pack windows to prevent glass breakage in transit?
Are slim-frame thermal break systems replacing traditional ones?
Does the price include the matching frame and installation kit?
How do you protect our proprietary design drawings from leaks?
How do I choose the right decorative profile for high-traffic hotel lobbies?
Is your factory the actual manufacturer or a trading partner?
Is it possible to 3D print a prototype before cutting steel?
Do you outsource any part of the painting process to others?
How do you handle replacement parts for damaged track rollers?
Do you accept escrow payments through third-party platforms?
Do you have ISO 9001 certification for your production line?
Are there extra fees if we pay via bank telegraphic transfer?
What is the price difference between powder coat and anodized?
What is the warranty period for the lock and hinge hardware?
What is your policy for dimensional deviations in the batch?
What happens if the shipment is delayed due to factory error?
Do you offer online technical support if color fading occurs?
Is it possible to engrave our brand logo on the tension screw?
Do you offer credit terms for long-term purchasing partners?
Can you palletize the shipments for easy forklift unloading?
What are the latest eco-friendly finish trends for decorative profiles in modern interior design?
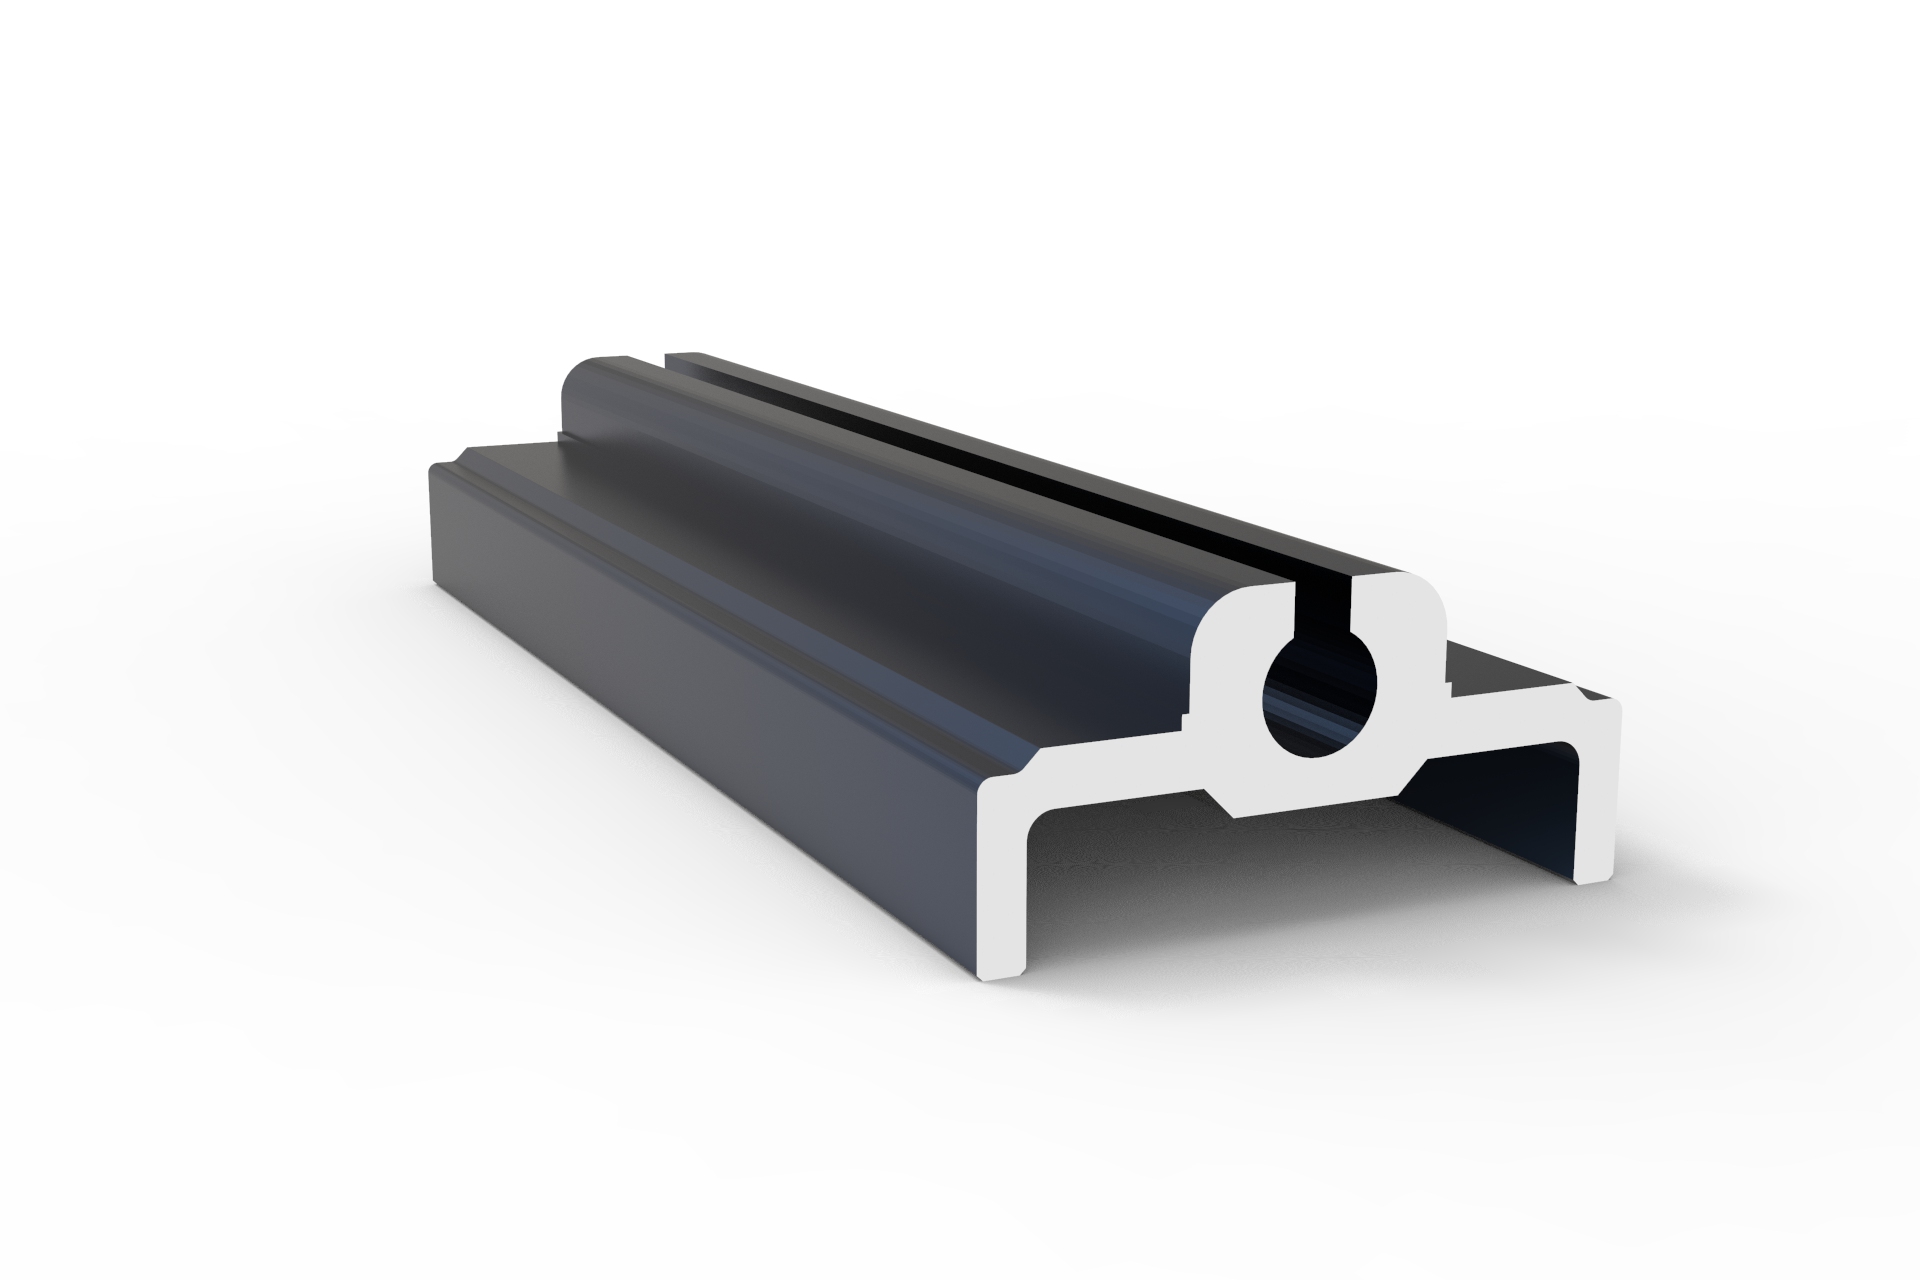
What are the tooling cost and design limitations for customizing heavy-duty industrial profiles?
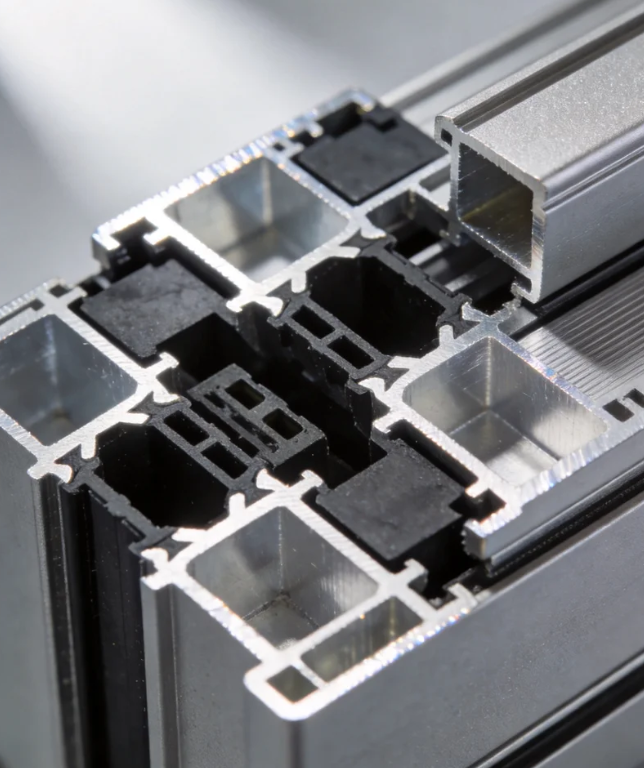
Has your architecture profile manufacturing facility passed ISO 9001 certification?
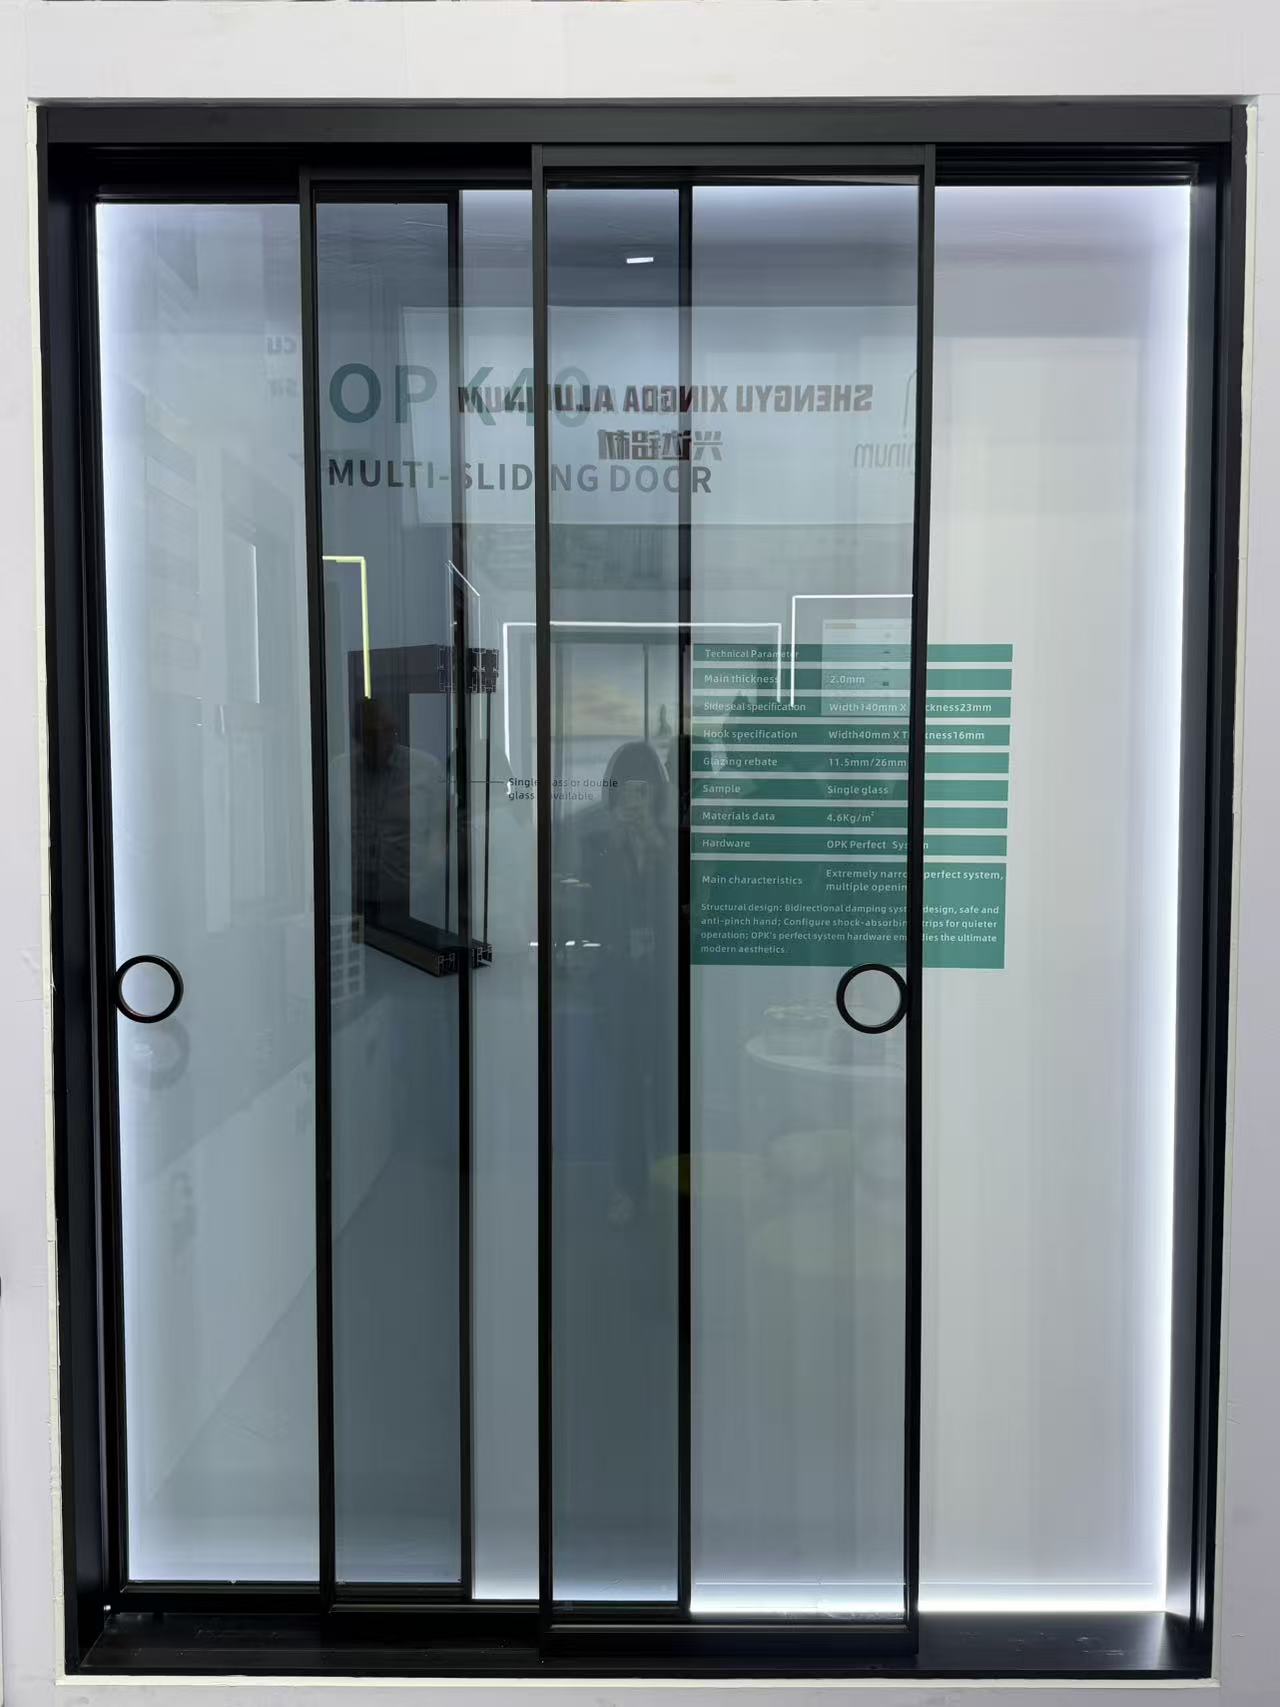
Can we use Alibaba Trade Assurance for our initial sliding door order to mitigate risk?
Do you provide free corner samples of the casement window frame for color verification?
Is it possible to custom-match a specific RAL color for a decorative profile order?
Can I request a 3D-printed sample before ordering a custom industrial profile mold?
Can you extrude an architecture profile based on our proprietary CAD drawings?
What thermal performance certifications does a sliding door need for the UK market?
How are heavy floding door panels crated to ensure safe unloading at the job site?
Can we arrange our own freight forwarder to pick up the casement door shipment FOB?
What is the estimated ocean freight transit time for a shutter shipment from China to Europe?
How can we source replacement seals for your awing window models in the future?
How are sliding windows typically packaged to prevent glass breakage during ocean transit?
What is the average lead time for a 40ft container of standard aluminum casement windows?
Are there any extra tooling fees if my decorative profile order doesn’t meet the MOQ?
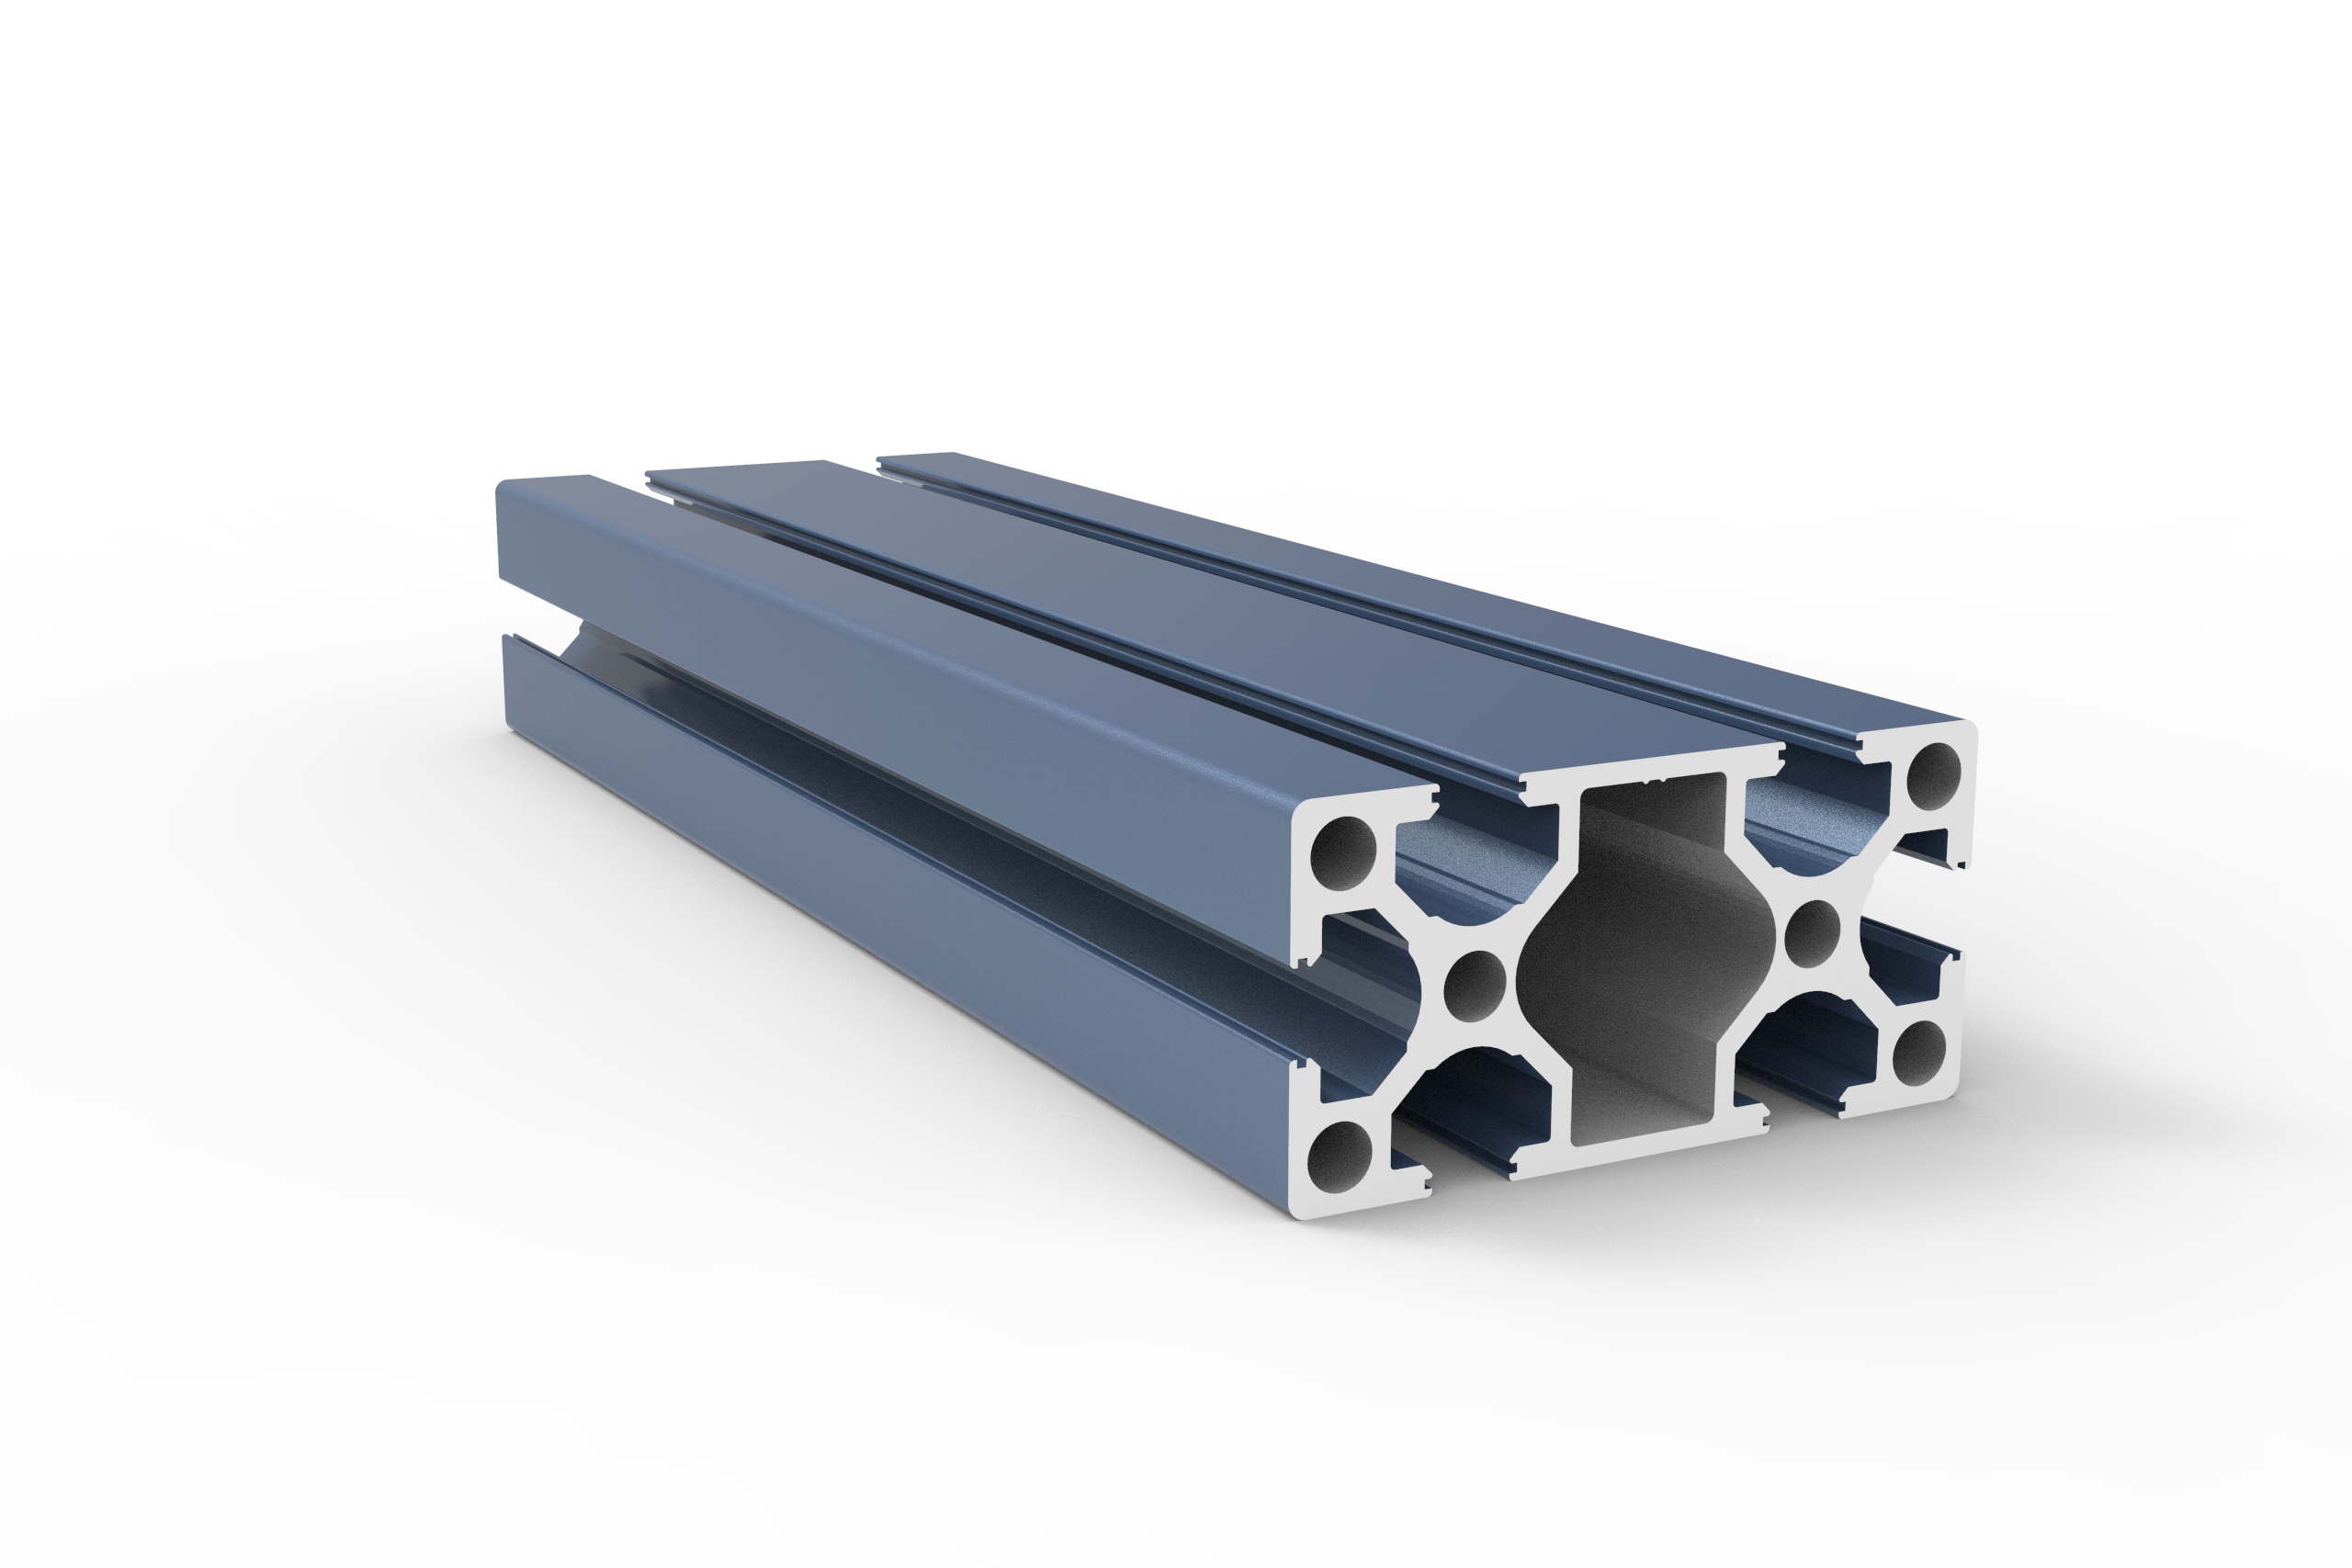
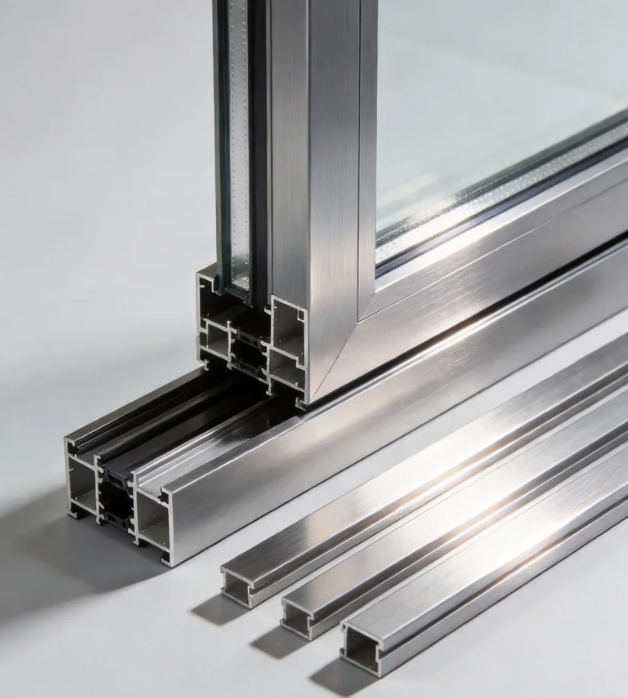
Can I get 3D printed prototypes of custom architecture profiles before committing to mold tooling?
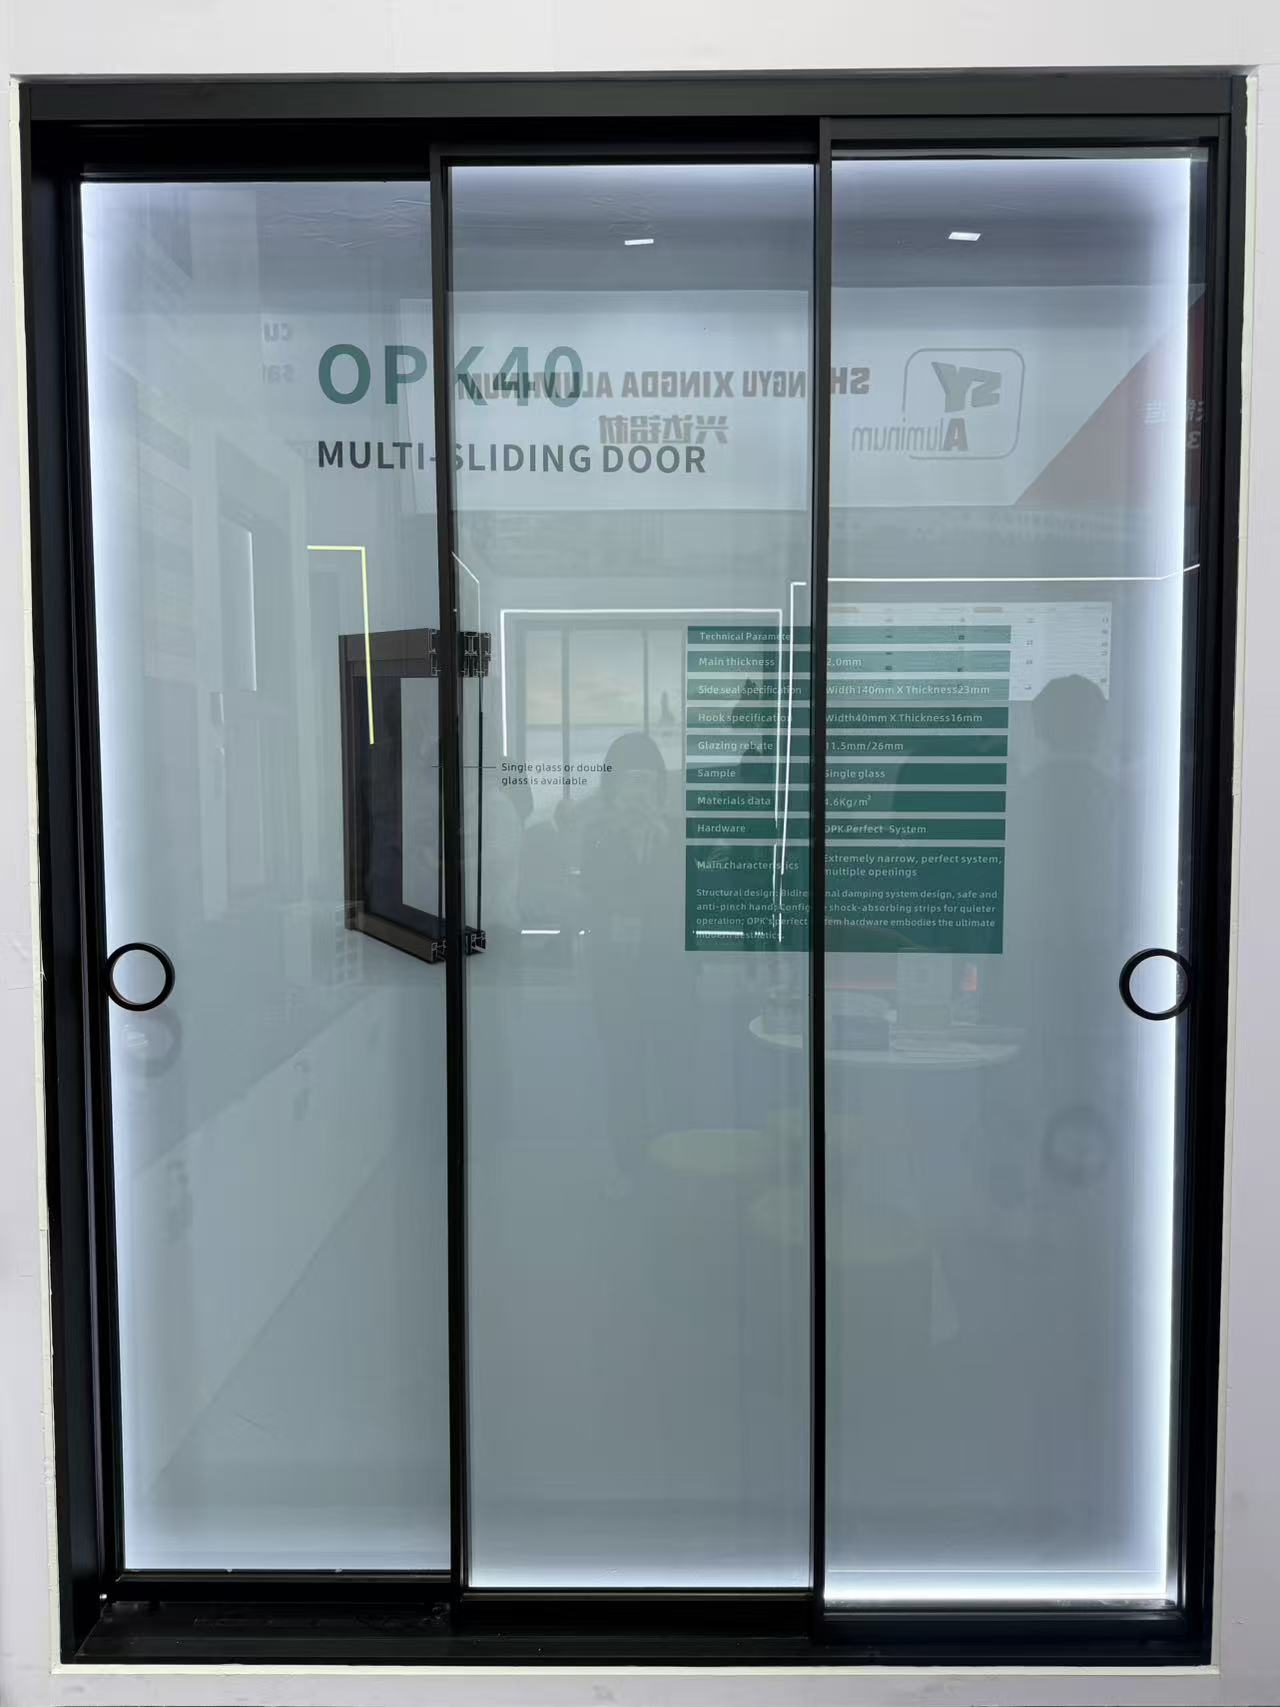
How is smart glass technology being integrated into modern residential sliding door units?
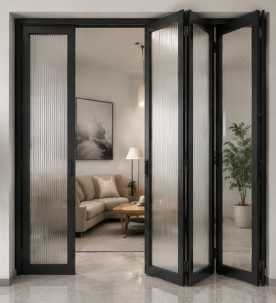
What options do you have for customizing the threshold height of an aluminum floding door?
What thermal break technology should I look for in a heavy-duty aluminum casement door?
What quality control processes do you perform on shutter hardware before final assembly?
Do you offer DDP shipping terms for awing window orders delivered to our warehouse?
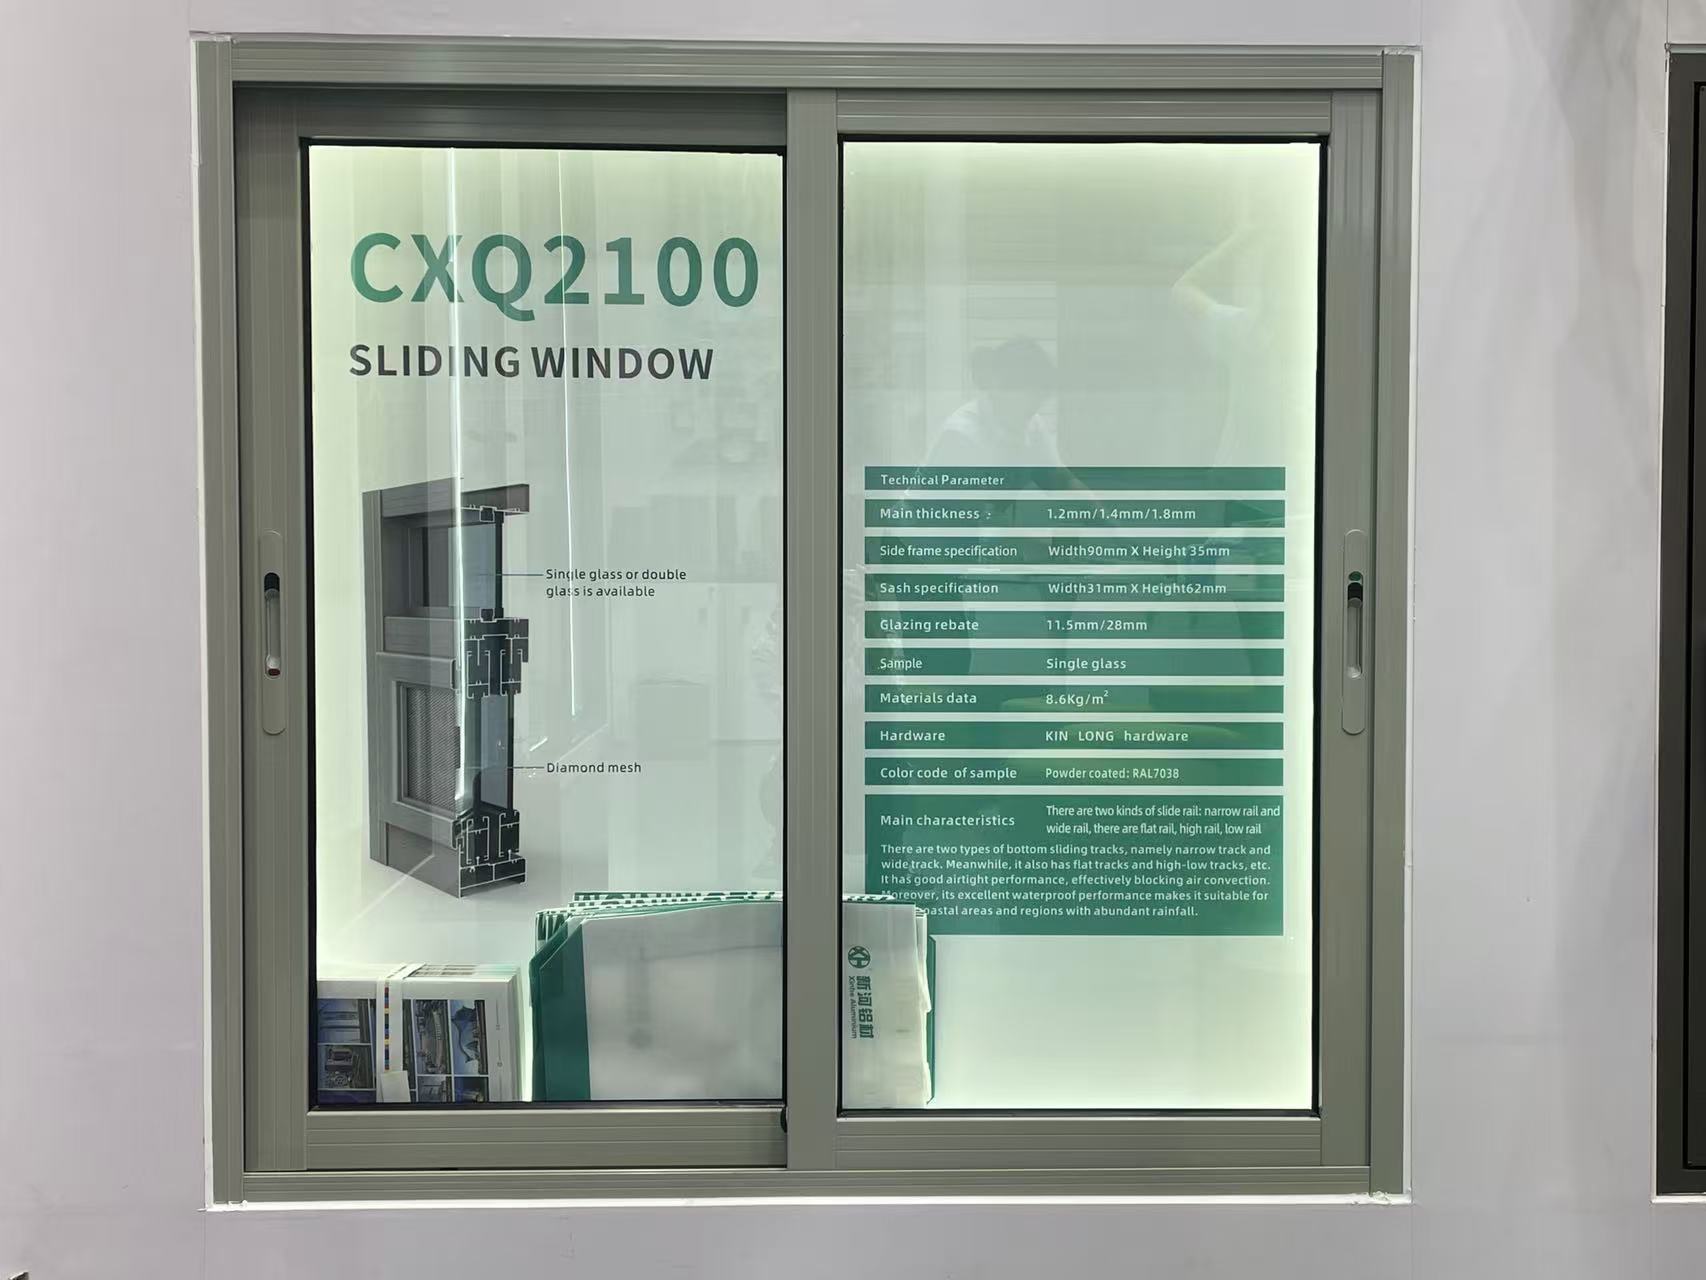
Is it possible to order a fully functional sliding window sample for mock-up testing?
Do you provide replacement hardware if the casement window hinges fail within 5 years?
How do you handle claims for decorative profile items damaged during transit?
What is the standard MOQ for custom-extruded aluminum industrial profile orders?
How does the order volume affect the per-ton price of custom architecture profile designs?
What is the warranty period for the rollers and tracks on your heavy-duty sliding doors?
How can we secure our deposit when purchasing high-value custom floding doors from a new supplier?
Can your factory match custom anodized colors for decorative profiles based on physical samples?
Is there a lighter alternative to aluminum industrial profile structures for robotics?
What payment security measures do you have for custom architecture profile tooling fees?
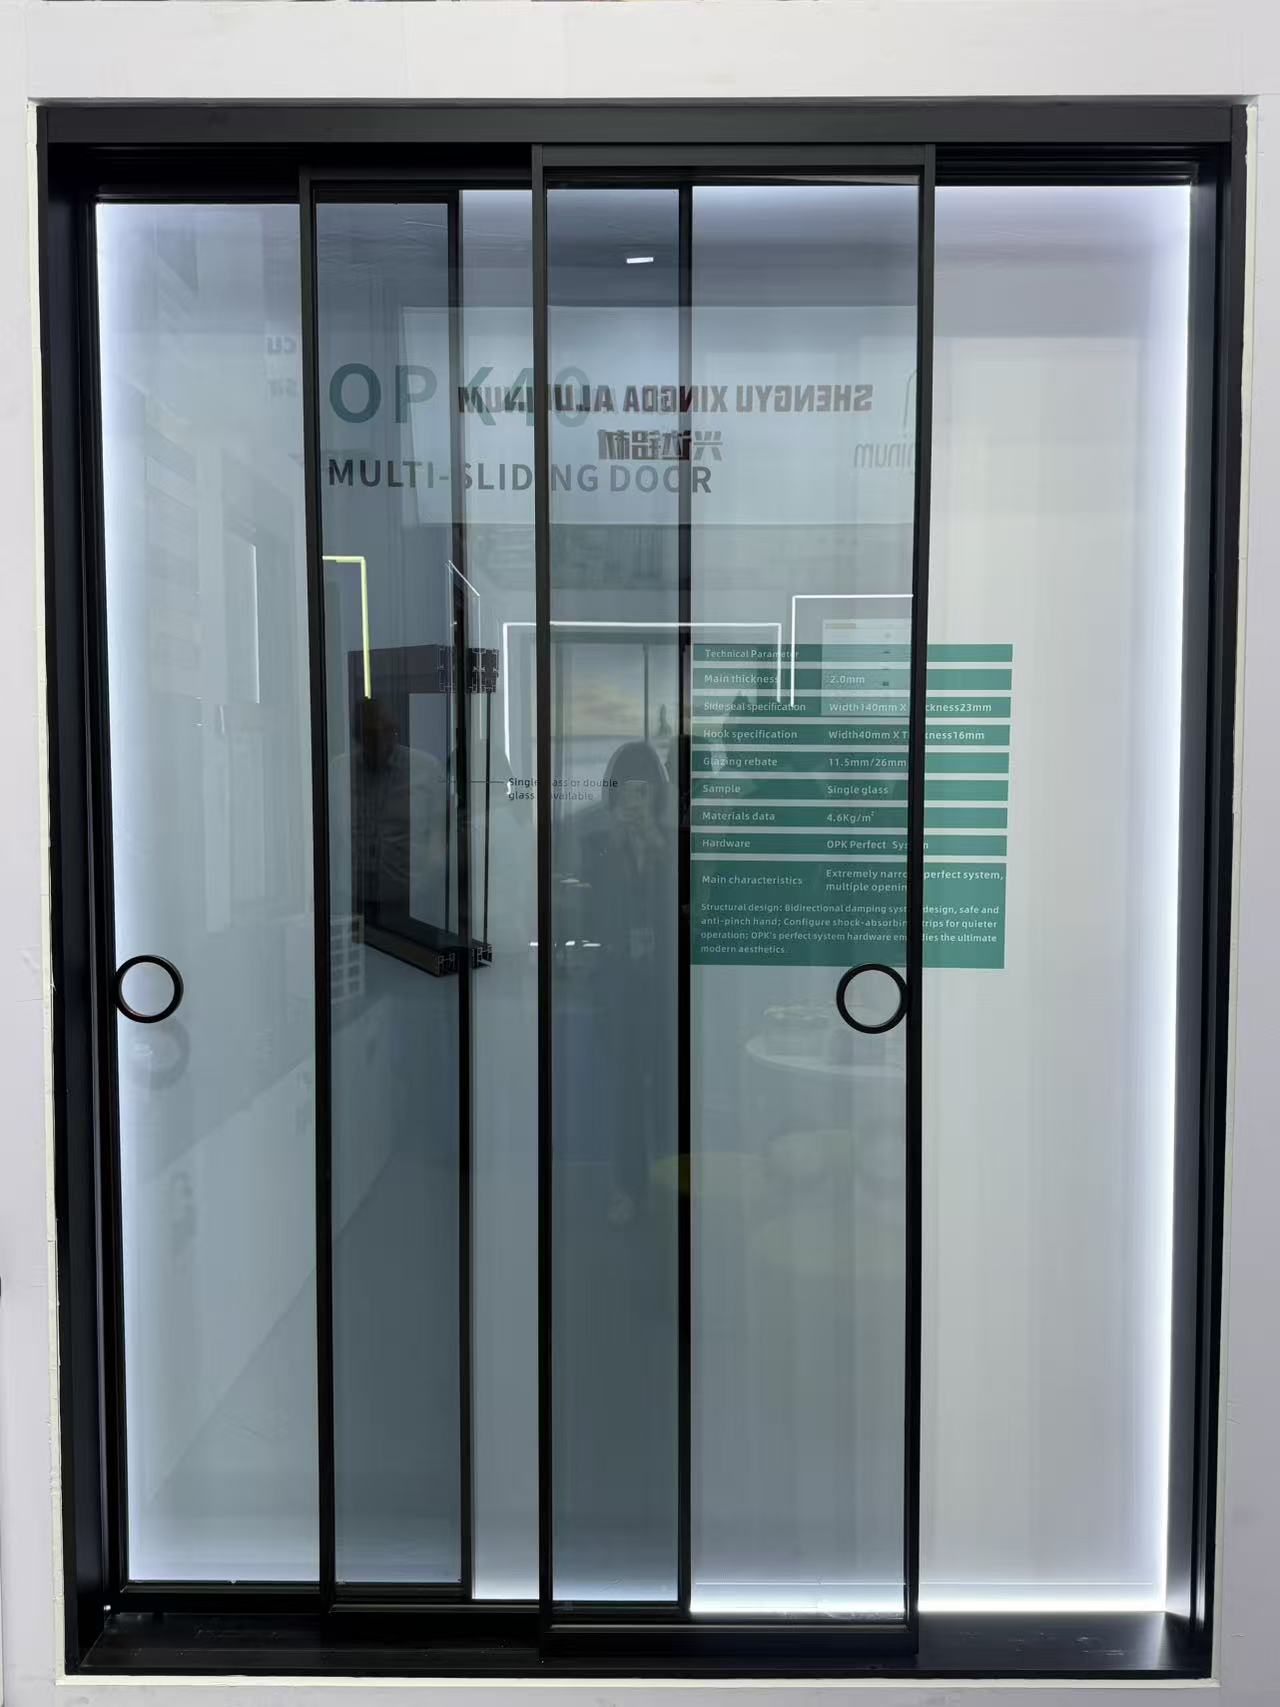
Can I order a sliding door with custom grid patterns between the glass panes?
How do you protect buyers against financial loss if the floding door shipment is delayed?
Are slim-frame aluminum casement door designs becoming more popular in modern offices?
What is your policy for replacing shutter components that arrive with color mismatch?
What kind of remote technical support do you offer for sliding window installation?
What is the maximum safe size for a top-hung awing window in commercial projects?
What environmental management standards does your decorative profile plant follow?
What is the standard lead time for producing a 40ft container of casement window orders?
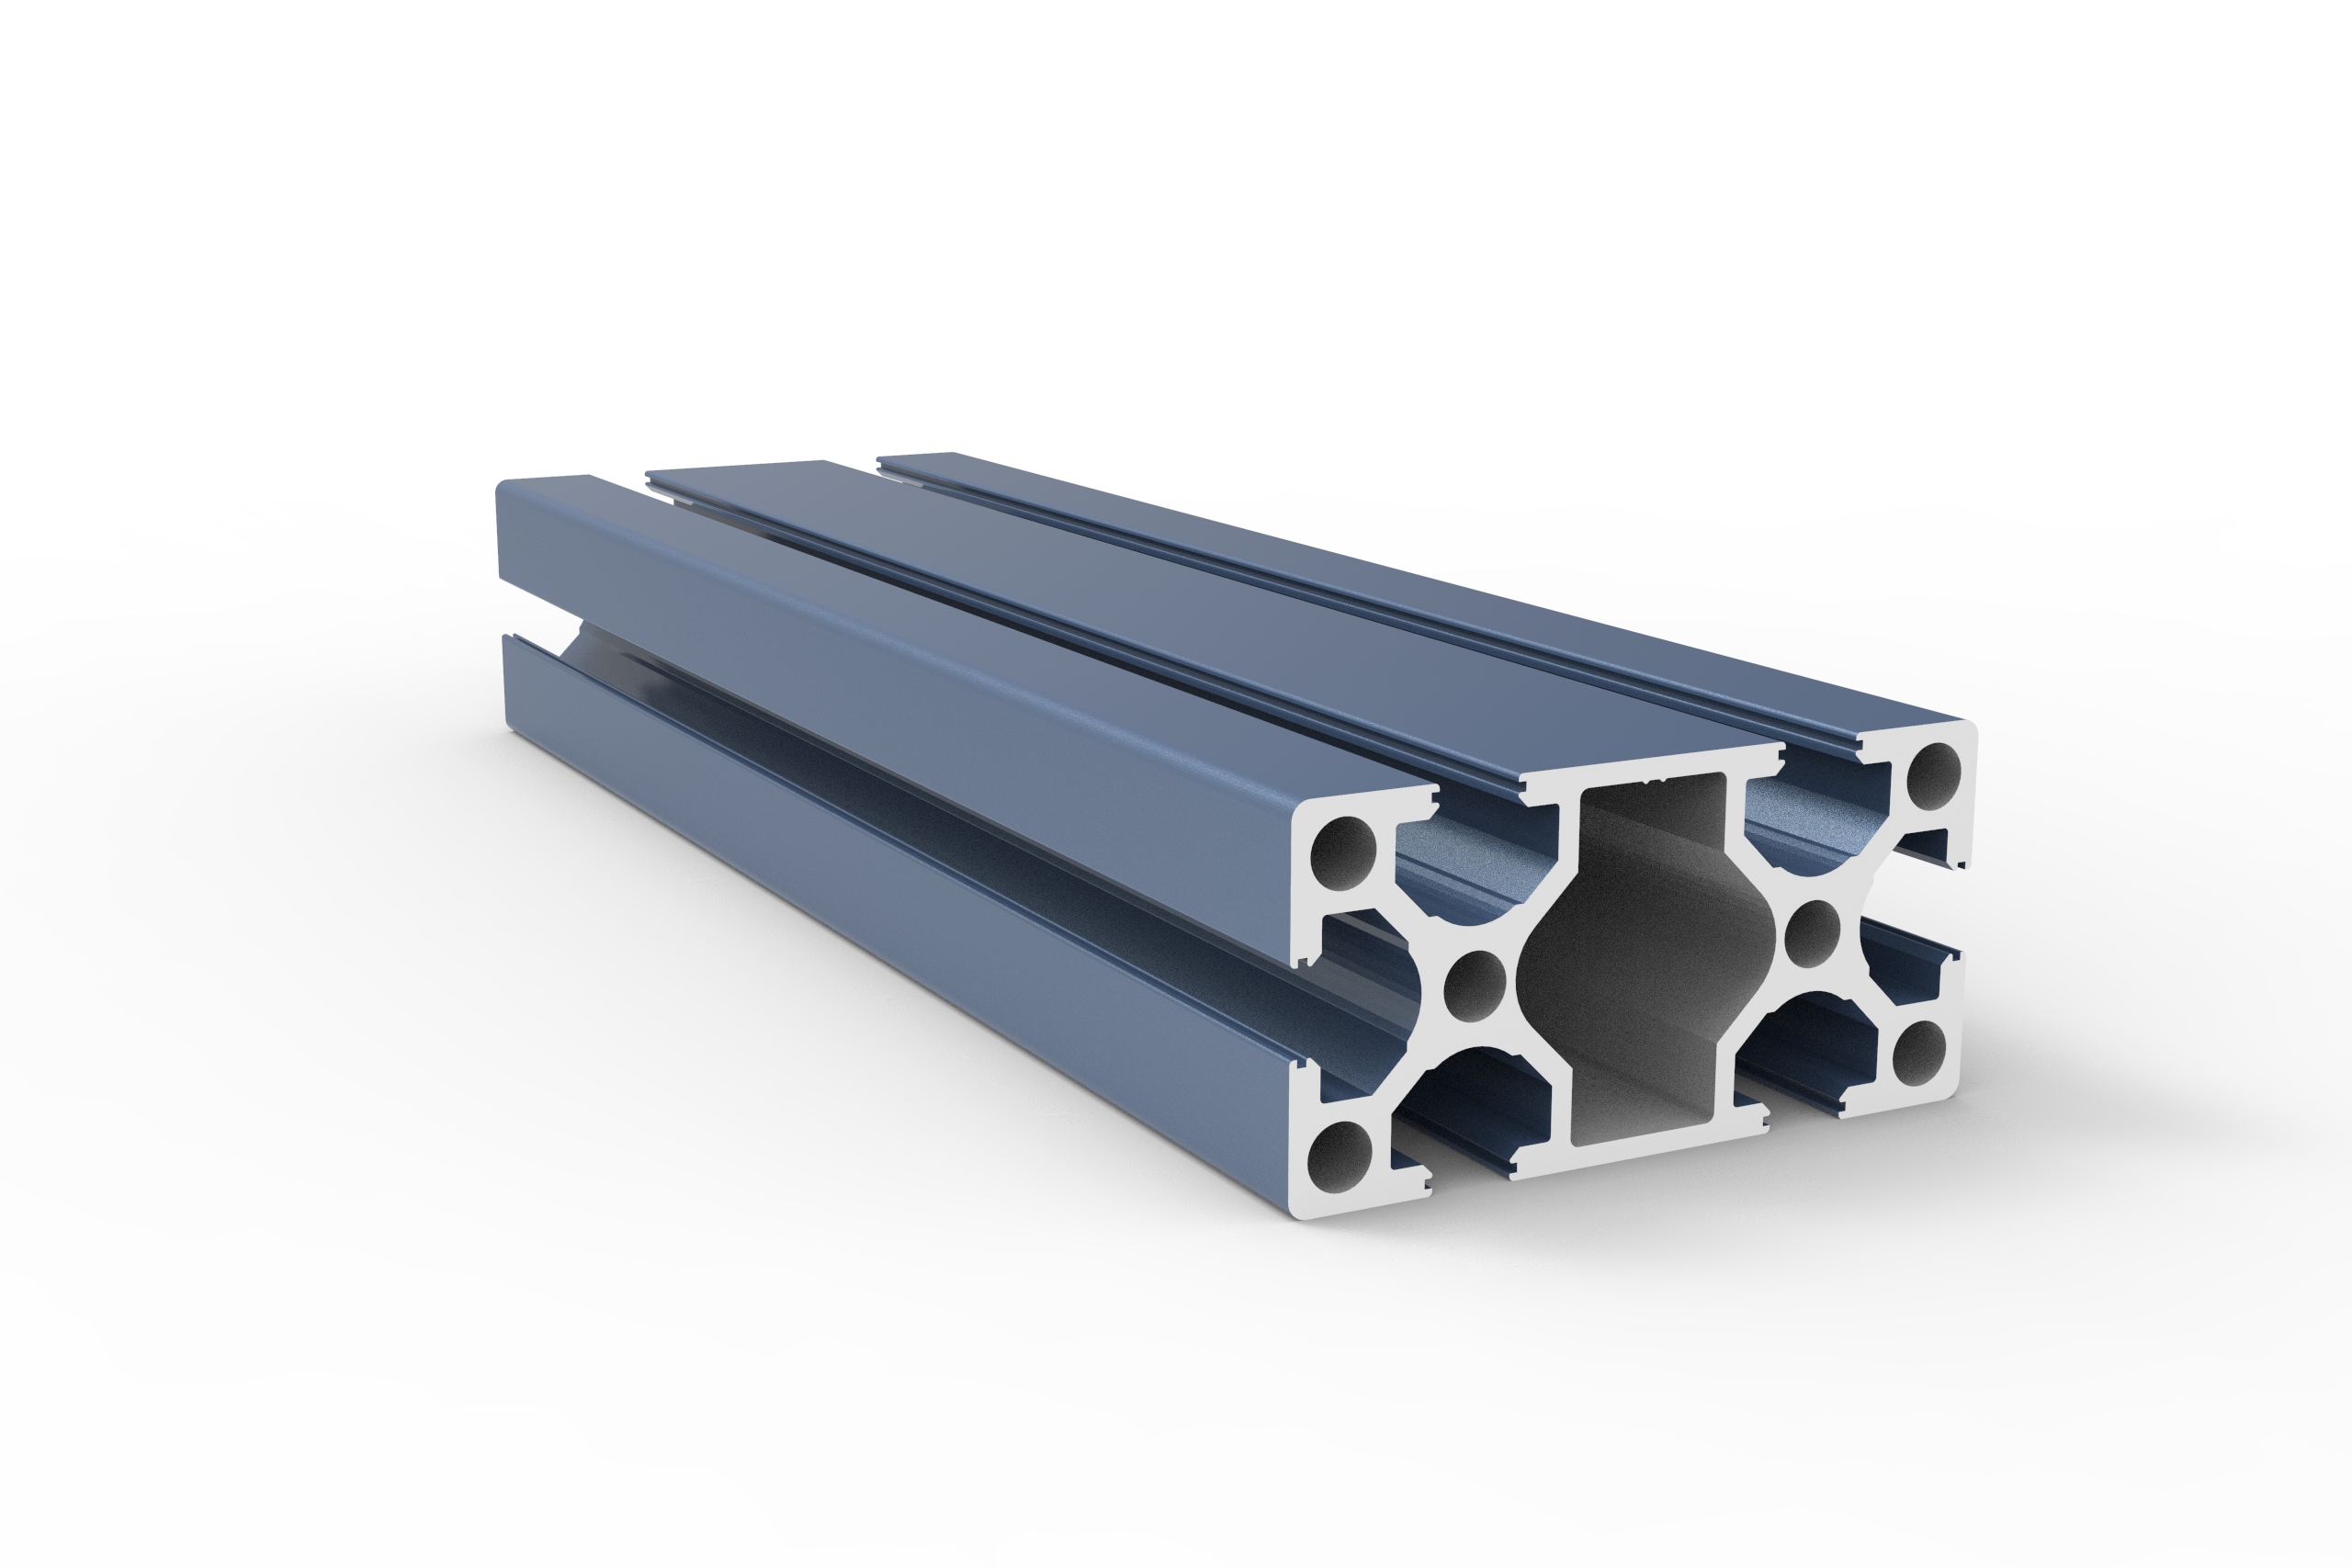
What is the warranty period for the anodized finish on your industrial profile?
What are the latest eco-friendly trends in architecture profile manufacturing?
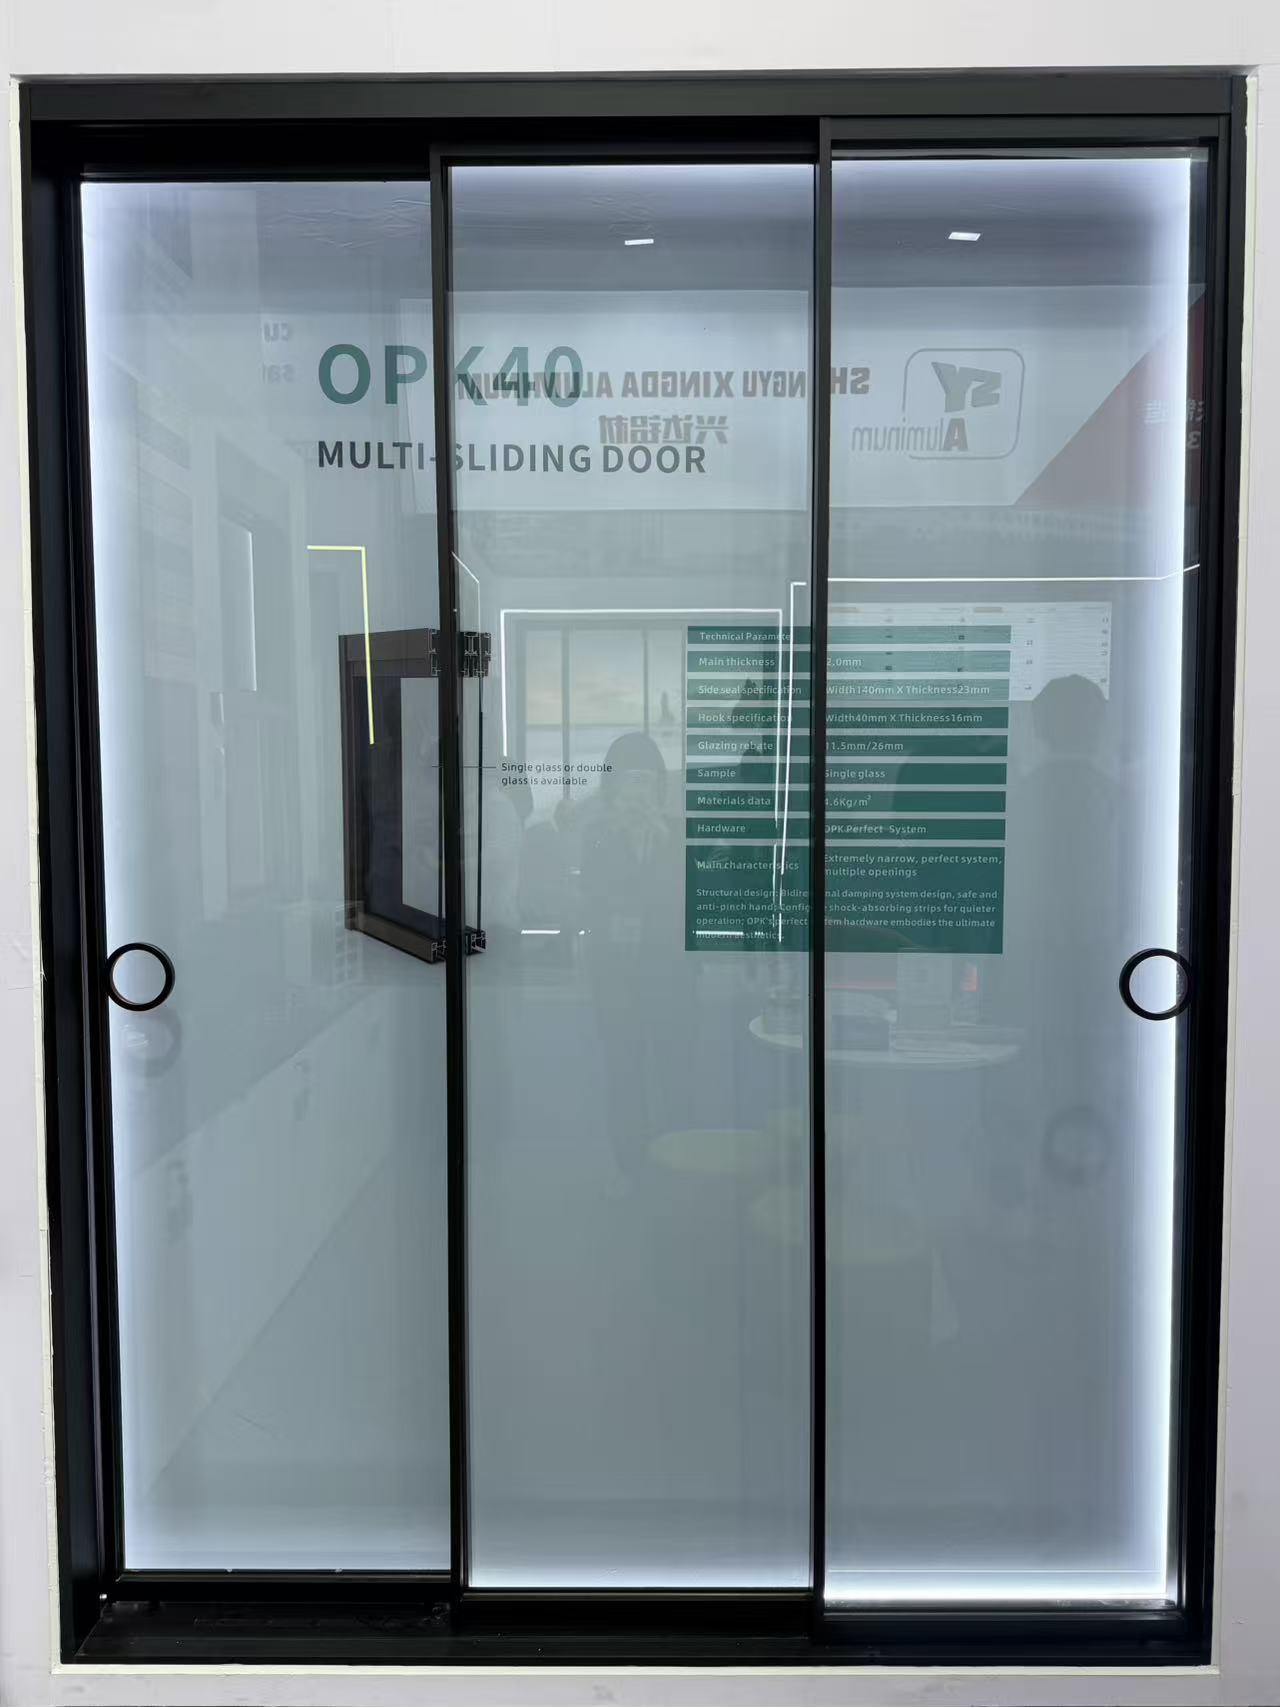
What is the average wholesale price per square meter for double-glazed sliding door systems?
How do I calculate the structural load requirement for a 5-panel exterior floding door?
Do your exterior shutter systems comply with Florida building codes for hurricane protection?
Do you offer Letter of Credit (L/C) payment options for casement door bulk orders?
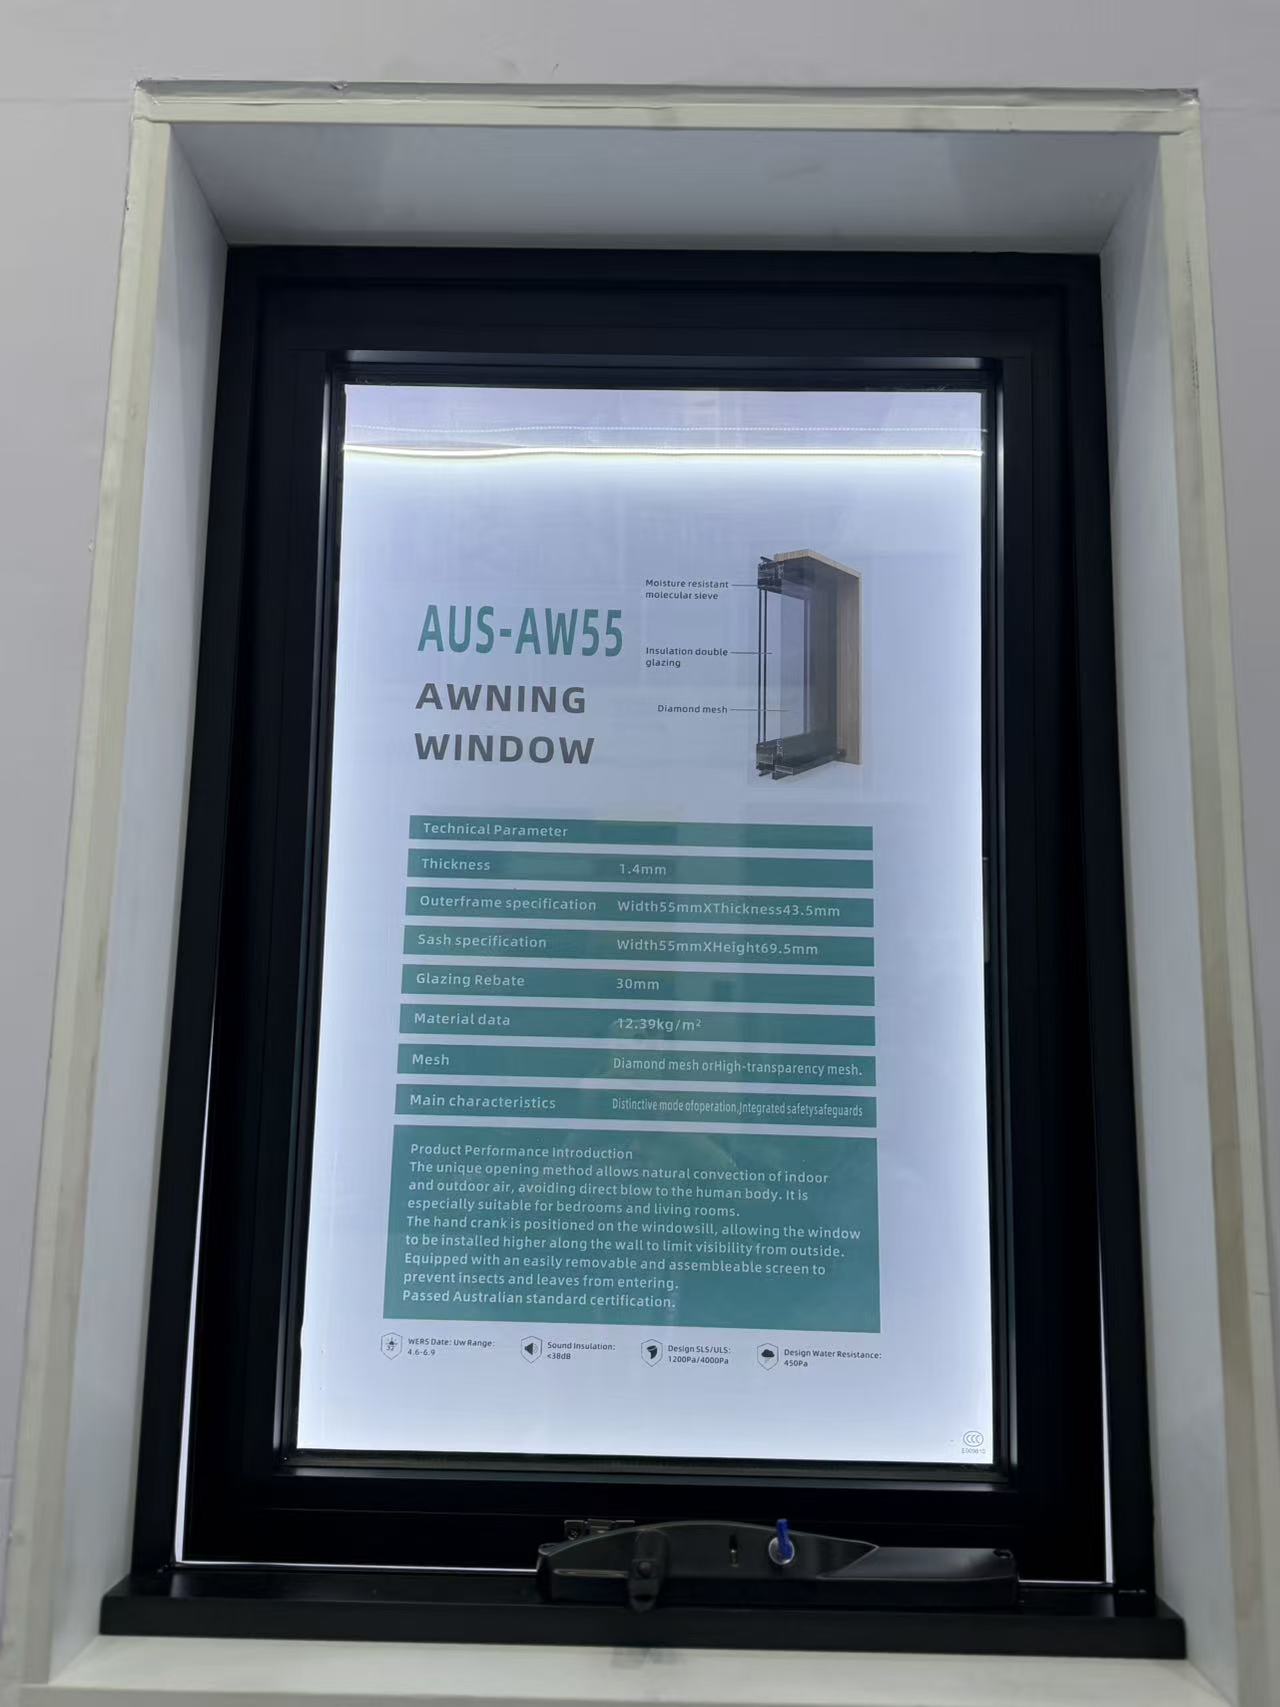
Which water tightness certifications are required for importing an awing window to Europe?
Do you allow virtual factory tours to inspect the sliding window assembly line?
What is the typical MOQ for ordering standard-sized aluminum casement window units?
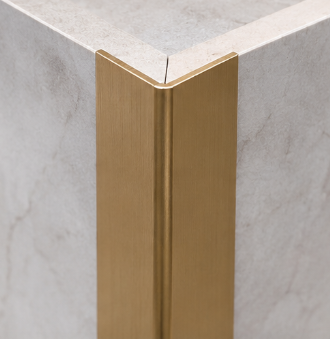
How long does it take to receive a physical sample of a gold-anodized decorative profile?
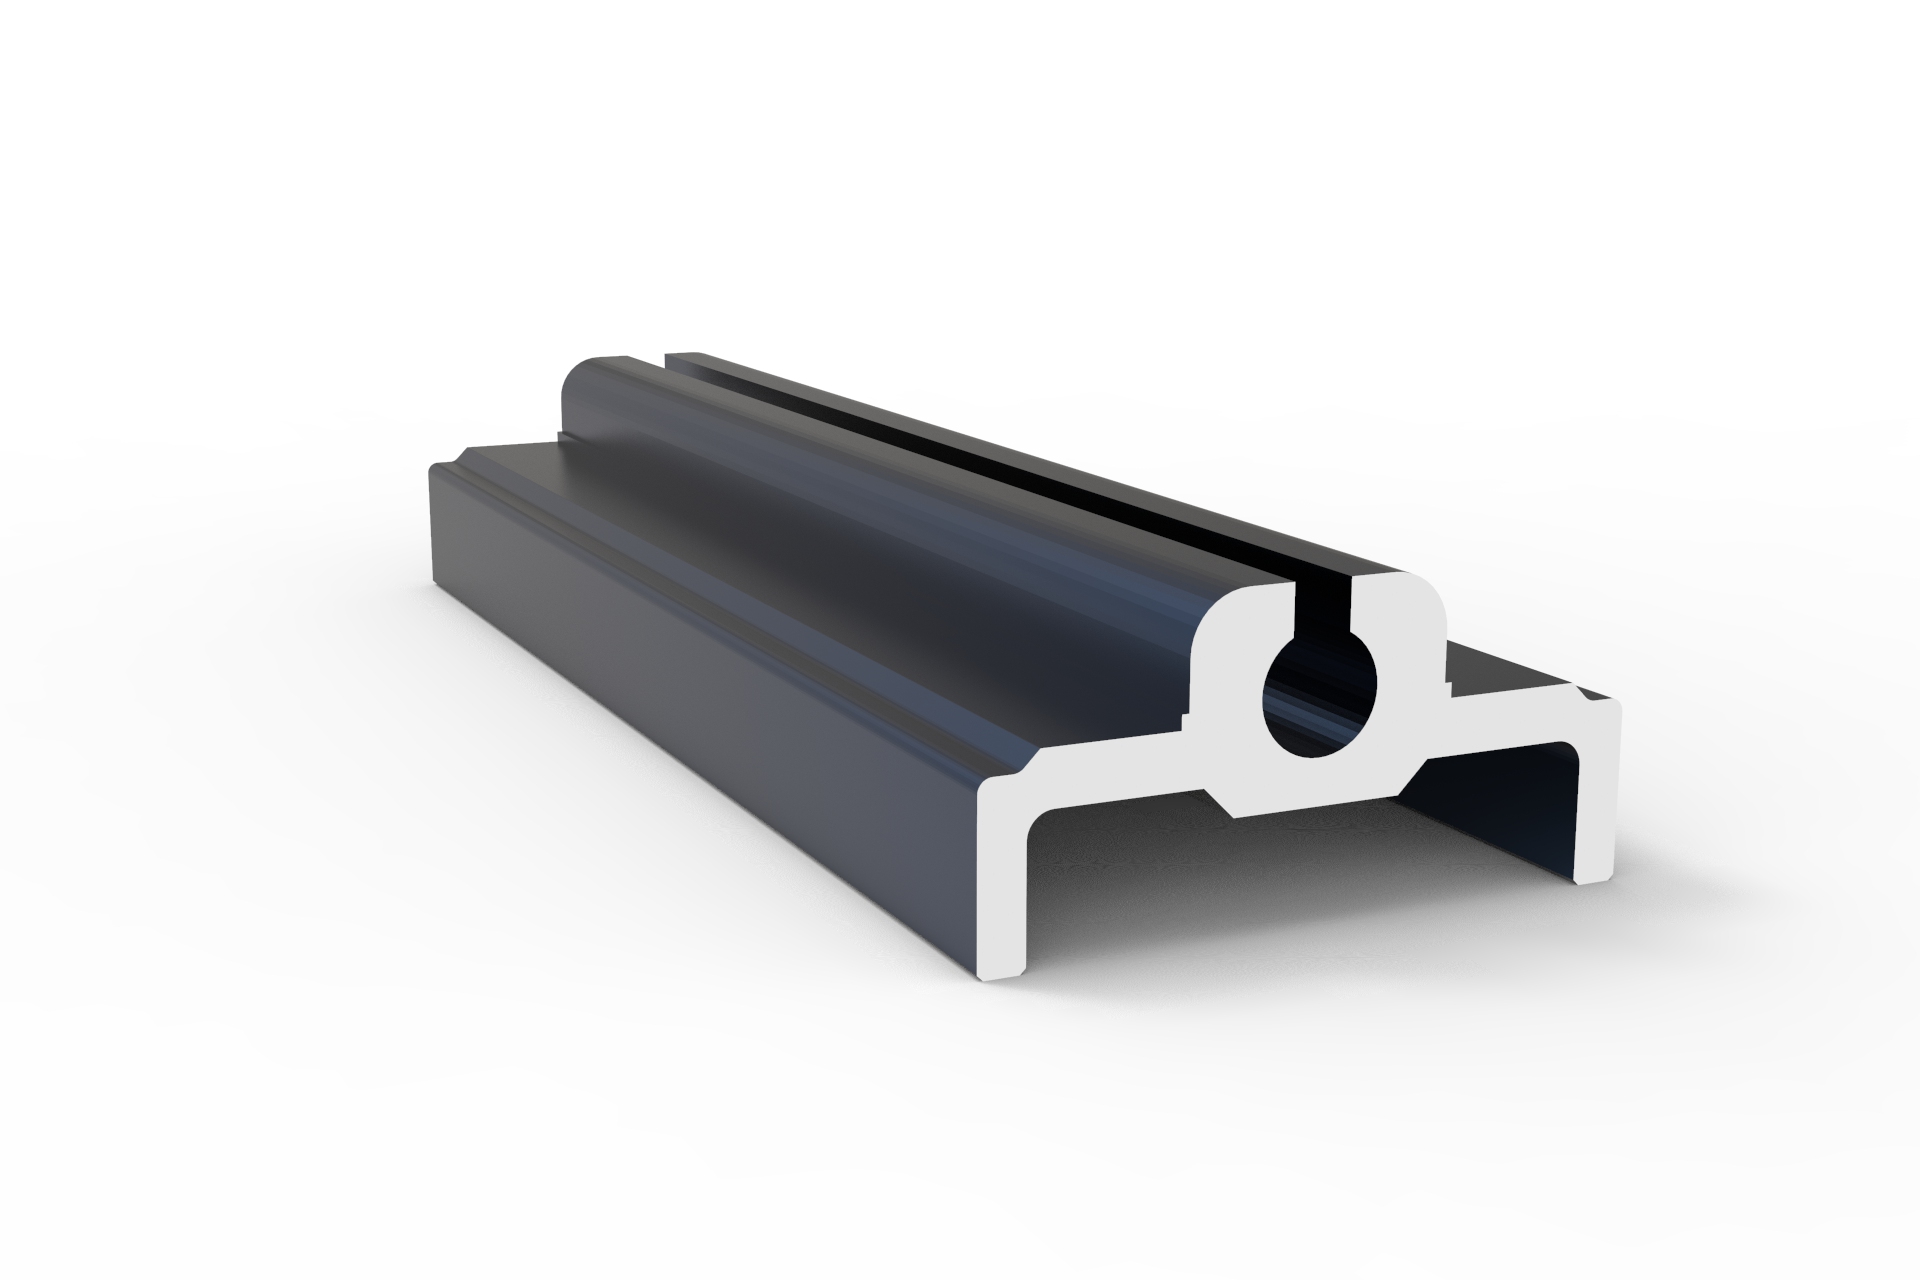
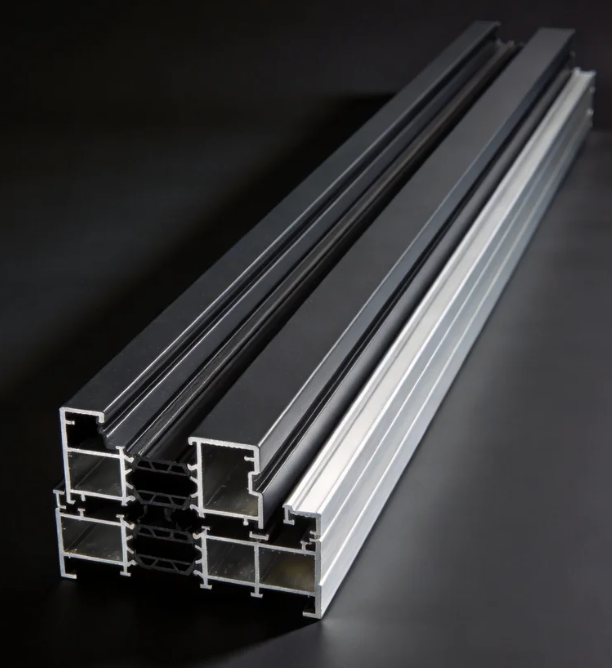
How do I choose the right alloy grade for architecture profiles in high-rise coastal buildings?
How do I choose the right track and roller specs for heavy-duty commercial sliding doors?
The core advantages of using aluminium profiles for the canopy
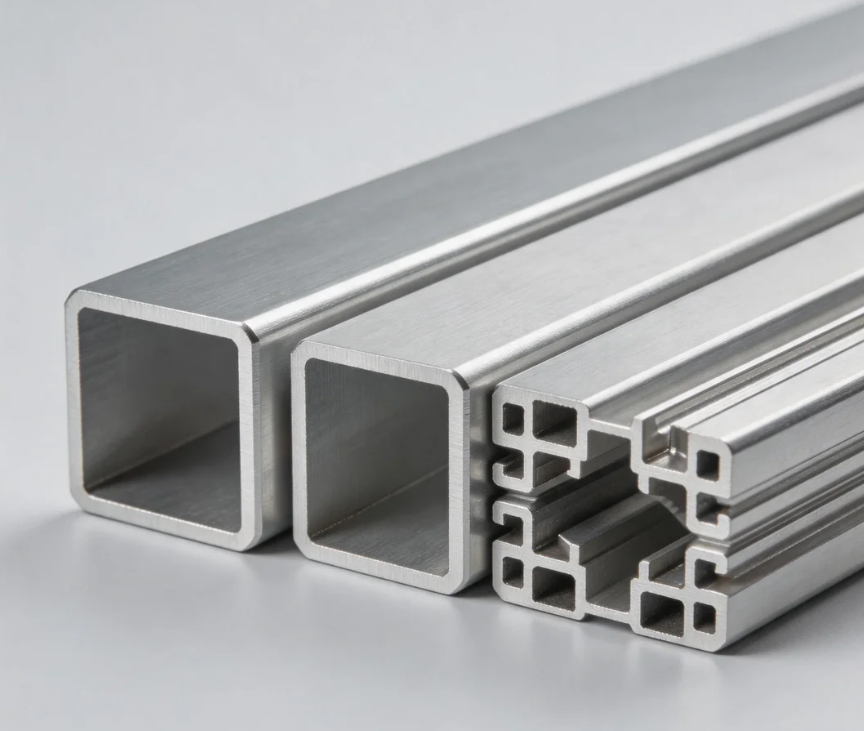
International demand: Dual drive by new energy and infrastructure
The advantages of using aluminium profiles to manufacture robot arms
The advantages of using aluminum profiles for door and window frames
The impact of the conflict between the United States and Iran on the price of aluminum
The advantages of using aluminium alloy for the main structure of high-speed train carriages
Methods for distinguishing Indoor and Outdoor Aluminium Doors
Maintenance methods and tips for aluminium doors and windows
Characteristic of outward-opening and hung aluminium windows
Xinhe Aluminium Research: 7.14-7.18 Analysis of Aluminium Prices
Seven Benefits Of Using Aluminium Profiles In Curtain Wall Systems
The Application of Aluminium Profiles in New Energy Vehicles
The Composition and Application of Series 6 Aluminium Alloys
Top 5 Benefits of Using LED Aluminium Profiles in Modern Lighting
A Complete Guide to Aluminium Frame Profiles for Modern Structures
Exploring the Strength and Versatility of Aluminium Extrusion Profiles
How to Choose the Right Aluminium Profile Supplier for Your Project
COMPANY