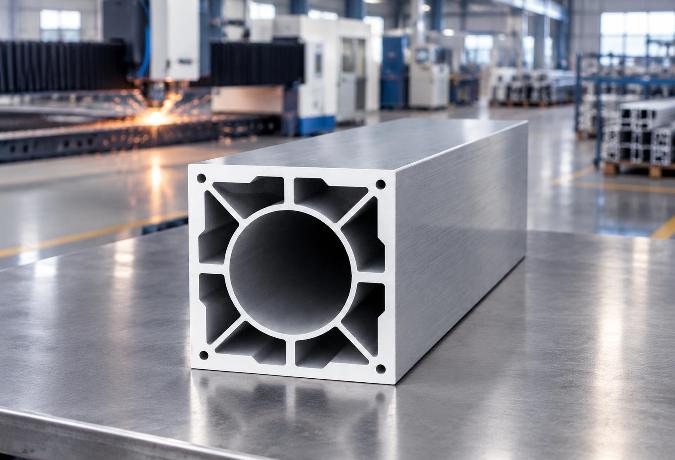
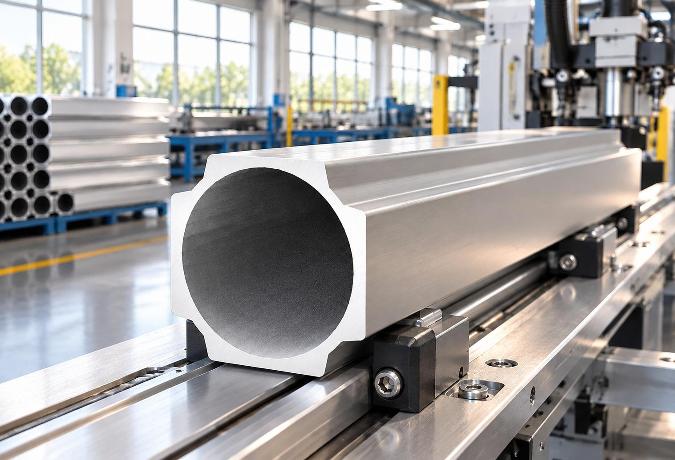
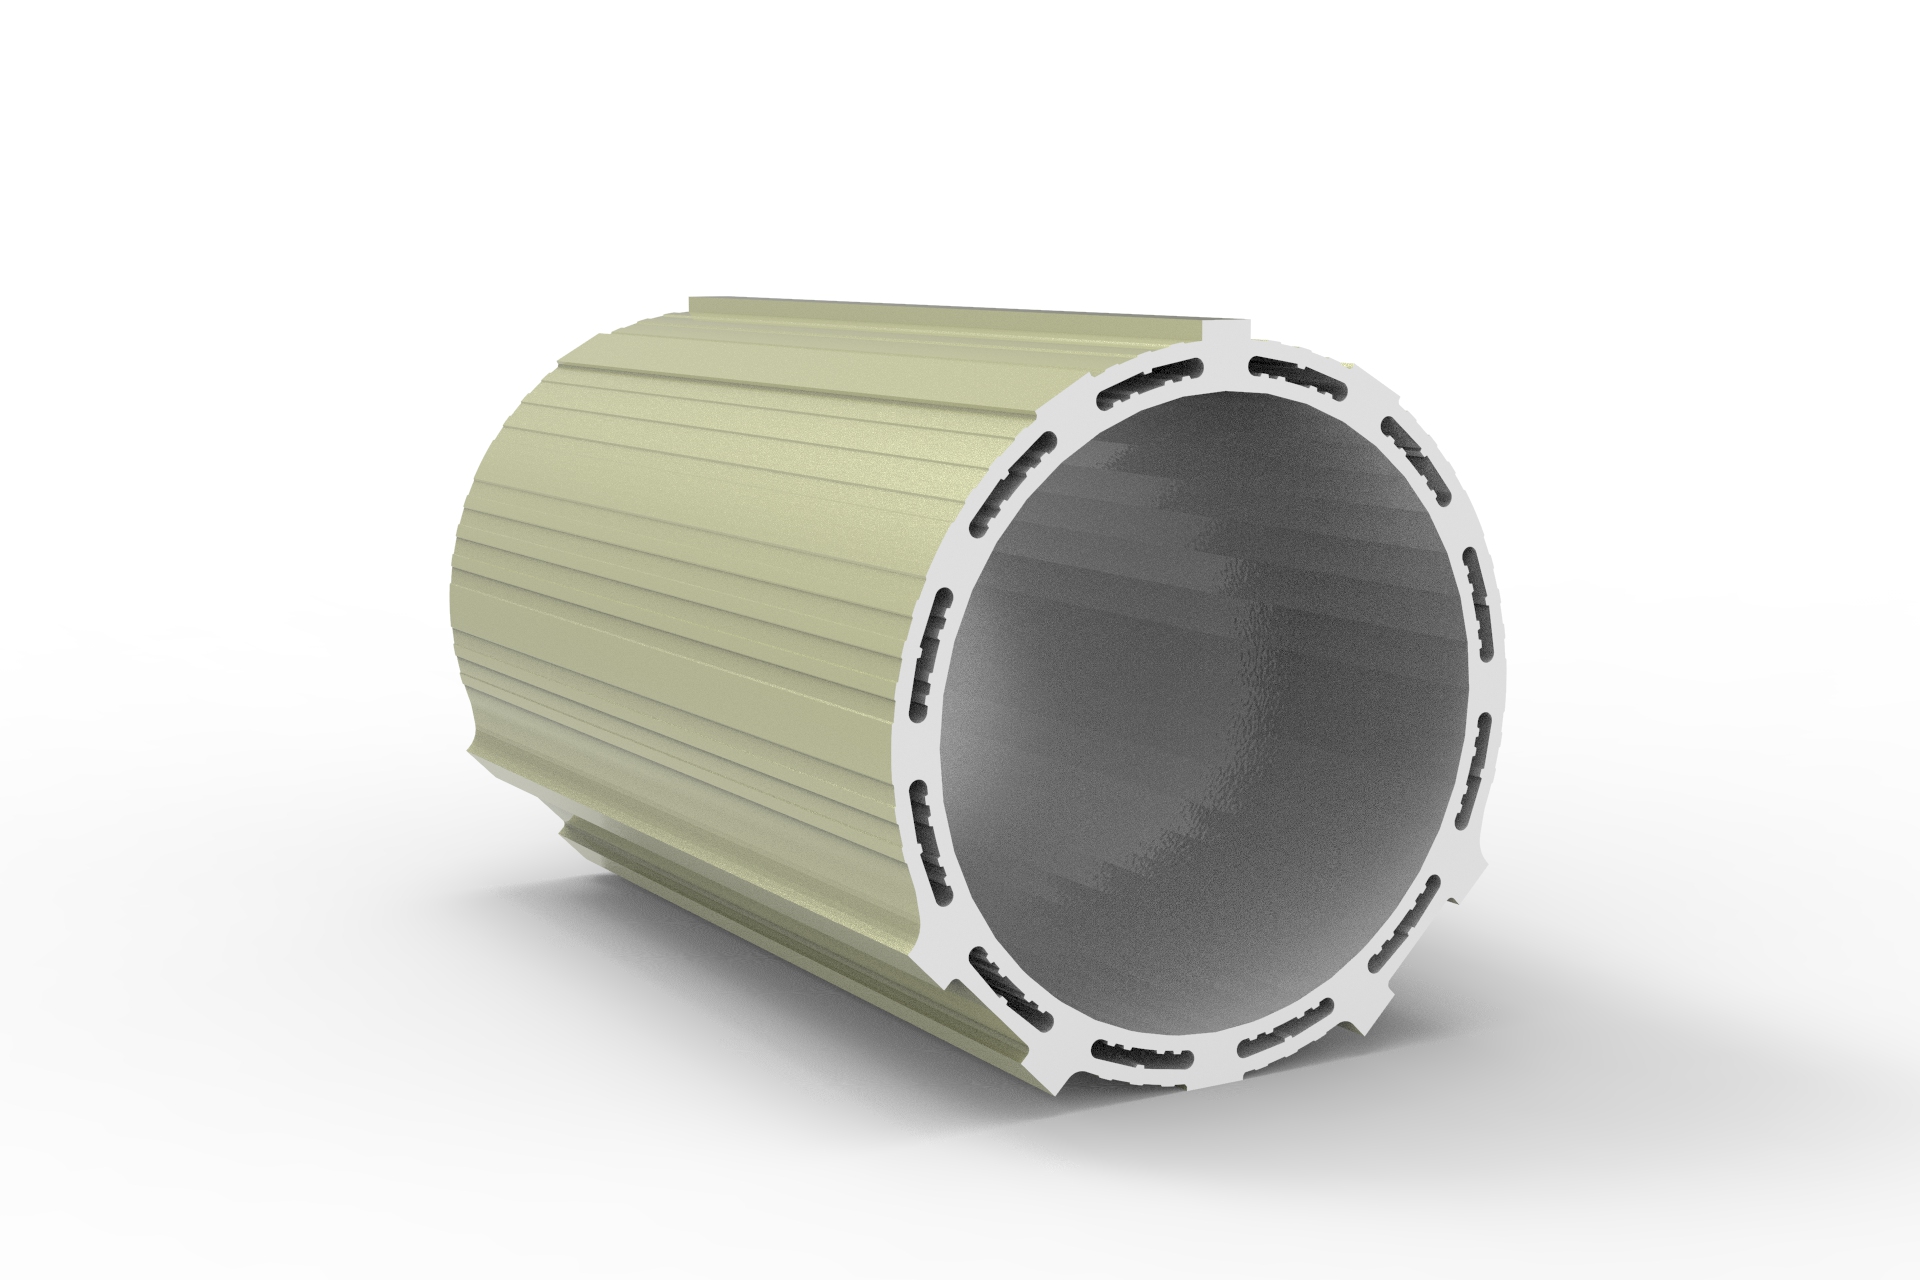
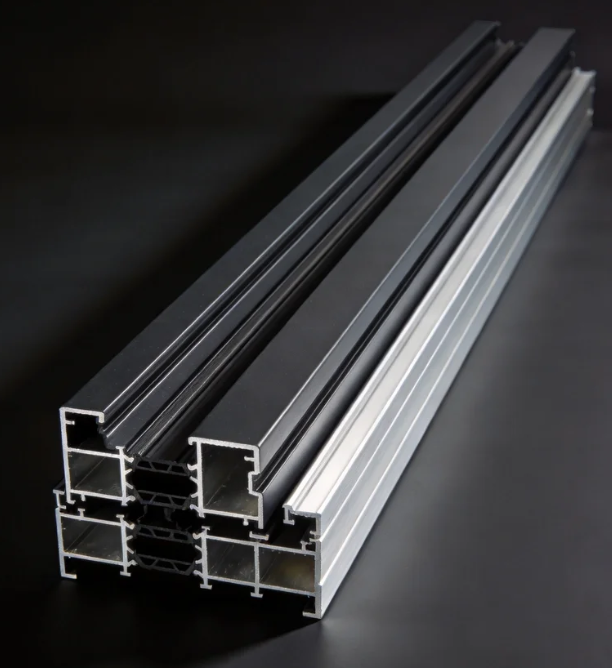
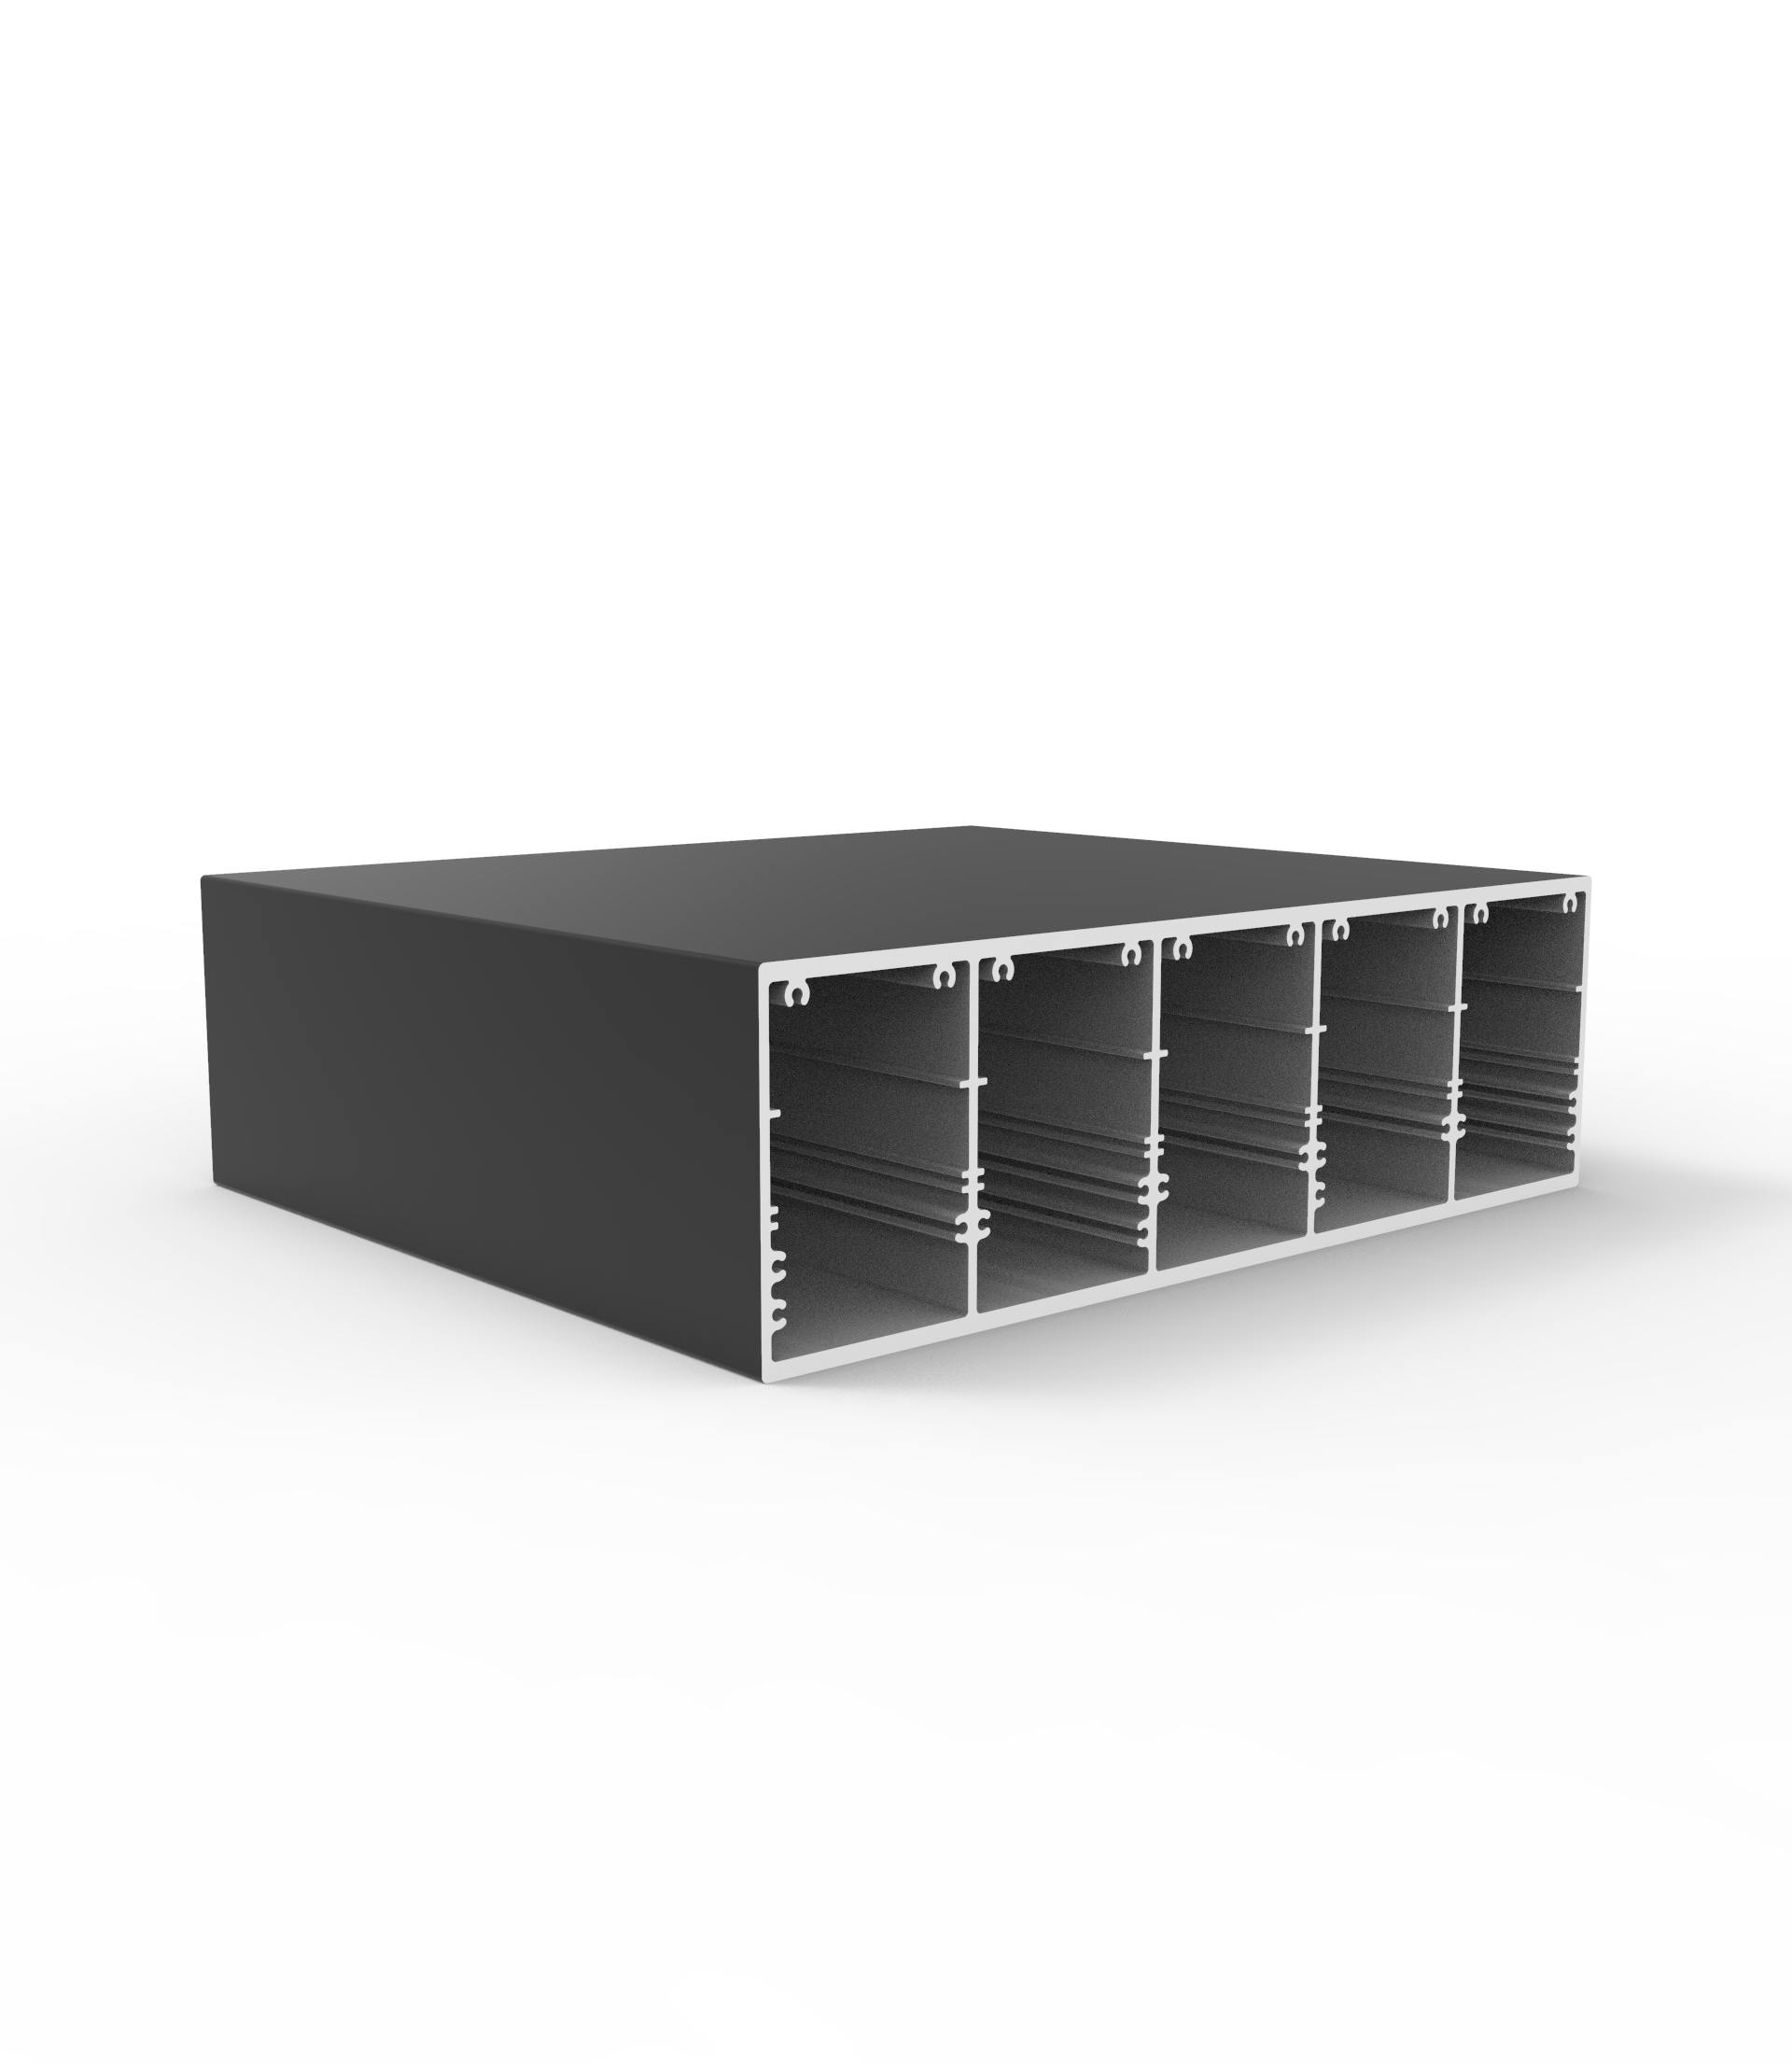
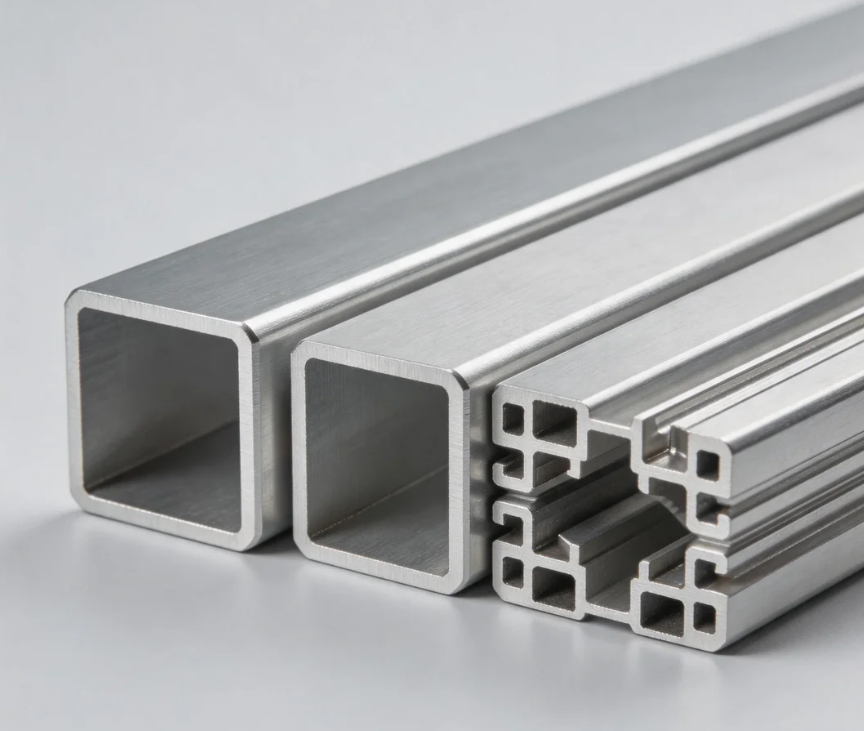
Architects and mechanical engineers face a persistent weight penalty when designing structural frameworks. Solid steel delivers immense raw yield strength but imposes massive dead loads on supporting foundations. The aluminium square tube emerges as a highly calculated engineering alternative in these specific load-bearing scenarios.
This hollow profile relies entirely on geometric mechanics rather than sheer material mass. By pushing the metal away from the center axis, the cross-section resists bending forces efficiently. You will find these extruded sections stabilizing modern architectural facades and heavy equipment chassis globally.
Understanding how this hollow geometry interacts with metallurgical tempering processes is absolutely vital. We must dismantle the physical forces acting upon these profiles to deploy them correctly. Incorrect specification often leads to premature mechanical deflection or localized buckling under sustained compression.
The objective is to establish exactly how this material behaves in real-world structural environments. This analysis bypasses superficial marketing claims to focus on applied physics and material science. Selecting the correct extrusion involves balancing alloy chemistry with precise dimensional scaling.
A solid metal bar is rarely the most efficient use of material in bending applications. When a beam is subjected to a vertical load, the internal stresses vary drastically. The top edge experiences extreme compression while the bottom edge undergoes severe tension.
The center layer of a solid beam experiences practically zero stress during this flexion. This central plane is known in mechanical engineering as the neutral axis. Leaving dense material near the neutral axis adds significant dead weight without contributing to structural stiffness.
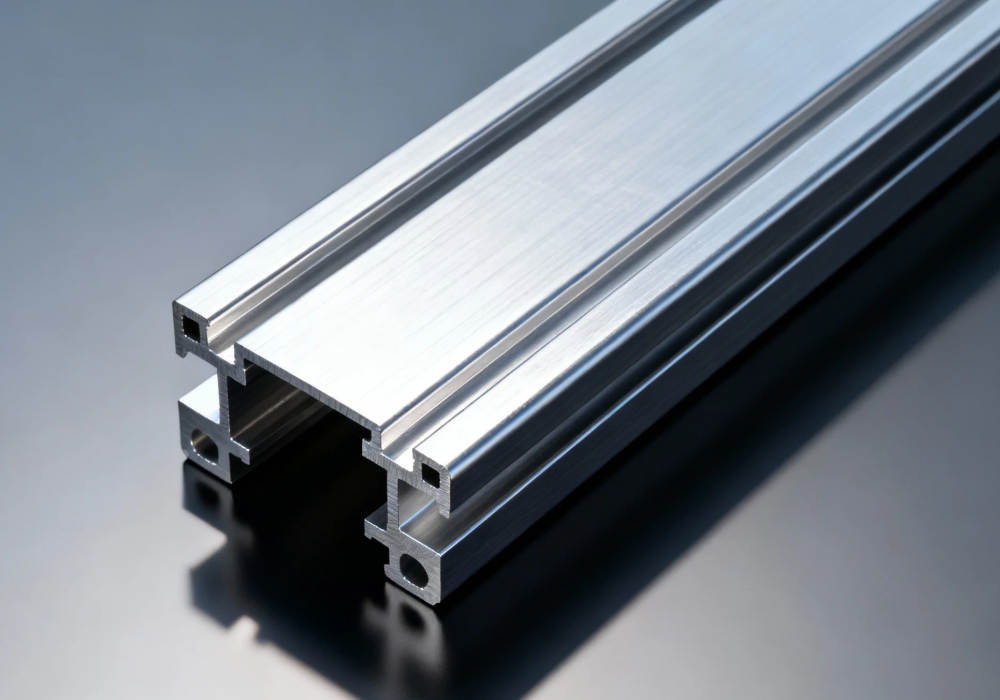
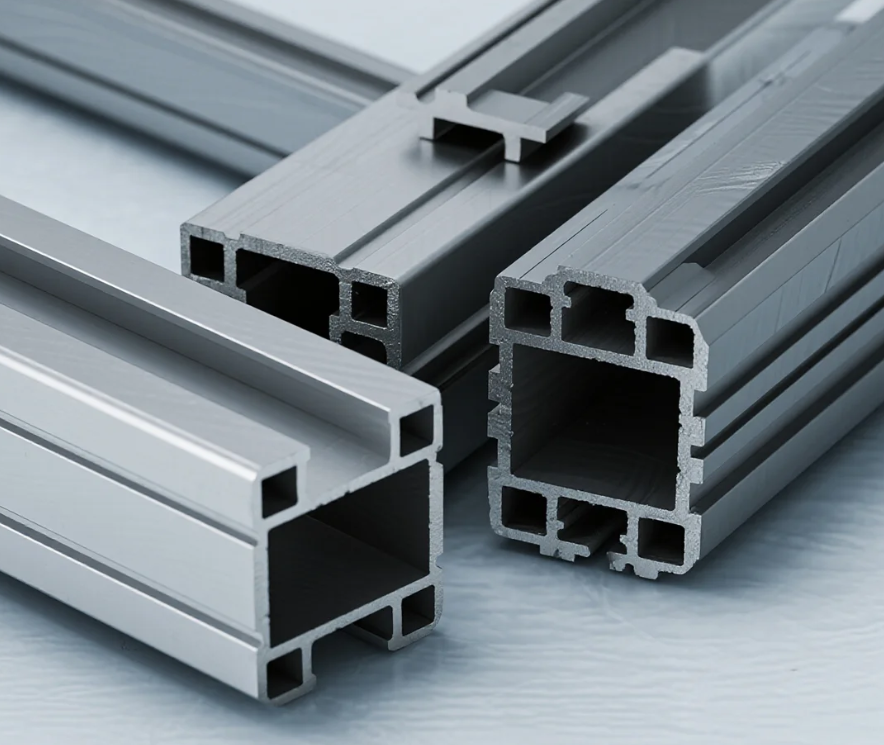
By removing this center mass, the extrusion process creates a continuous hollow section. This distributes the remaining metal further from the neutral bending axis. The physical parameter that measures this resistance to bending is called the moment of inertia.

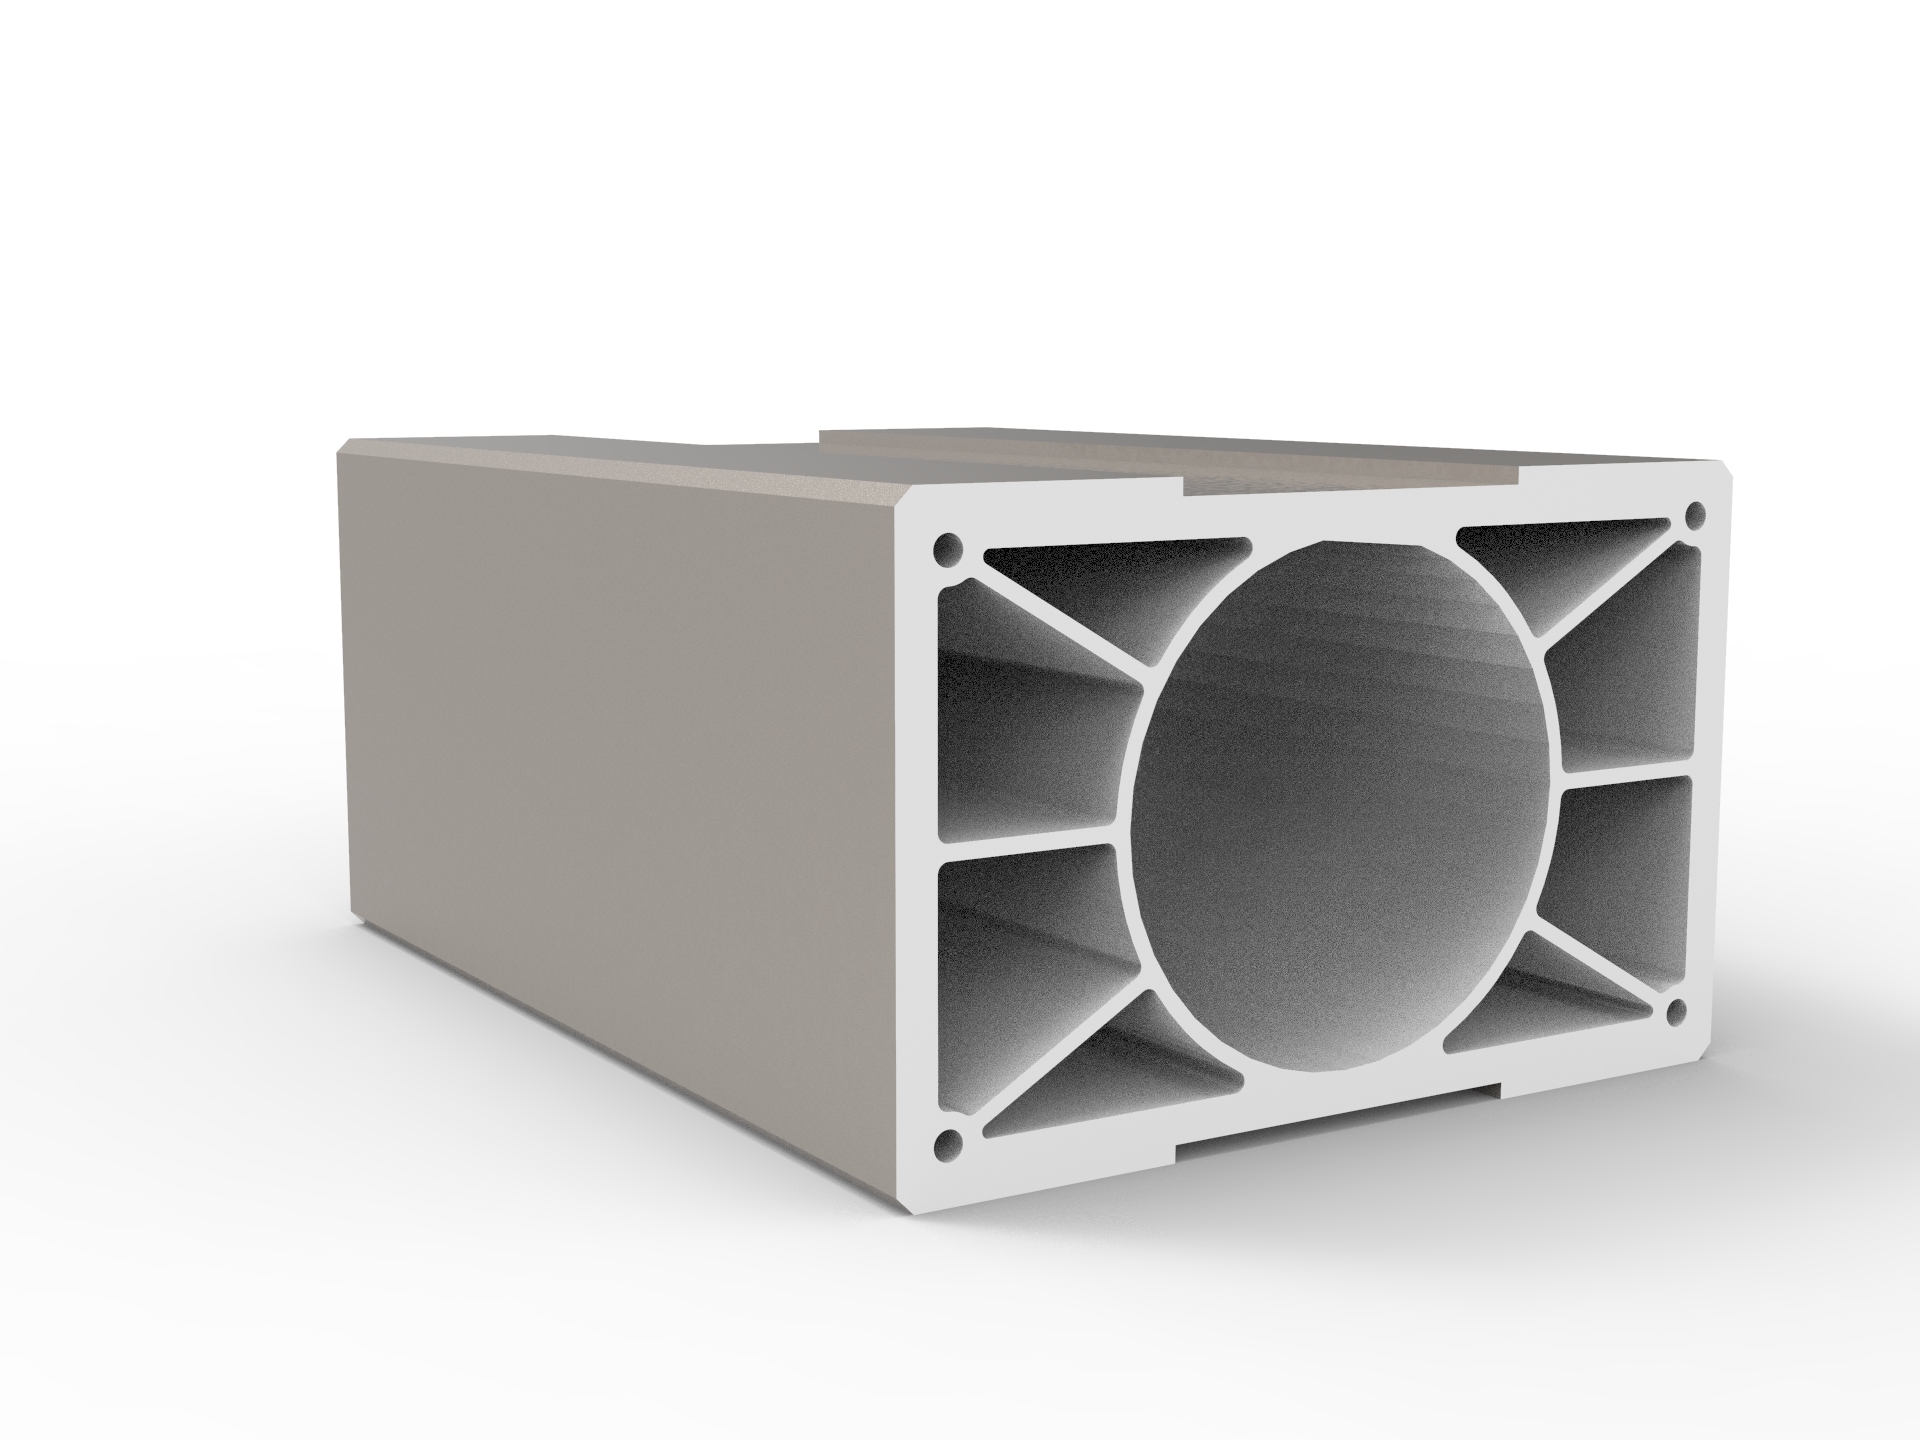
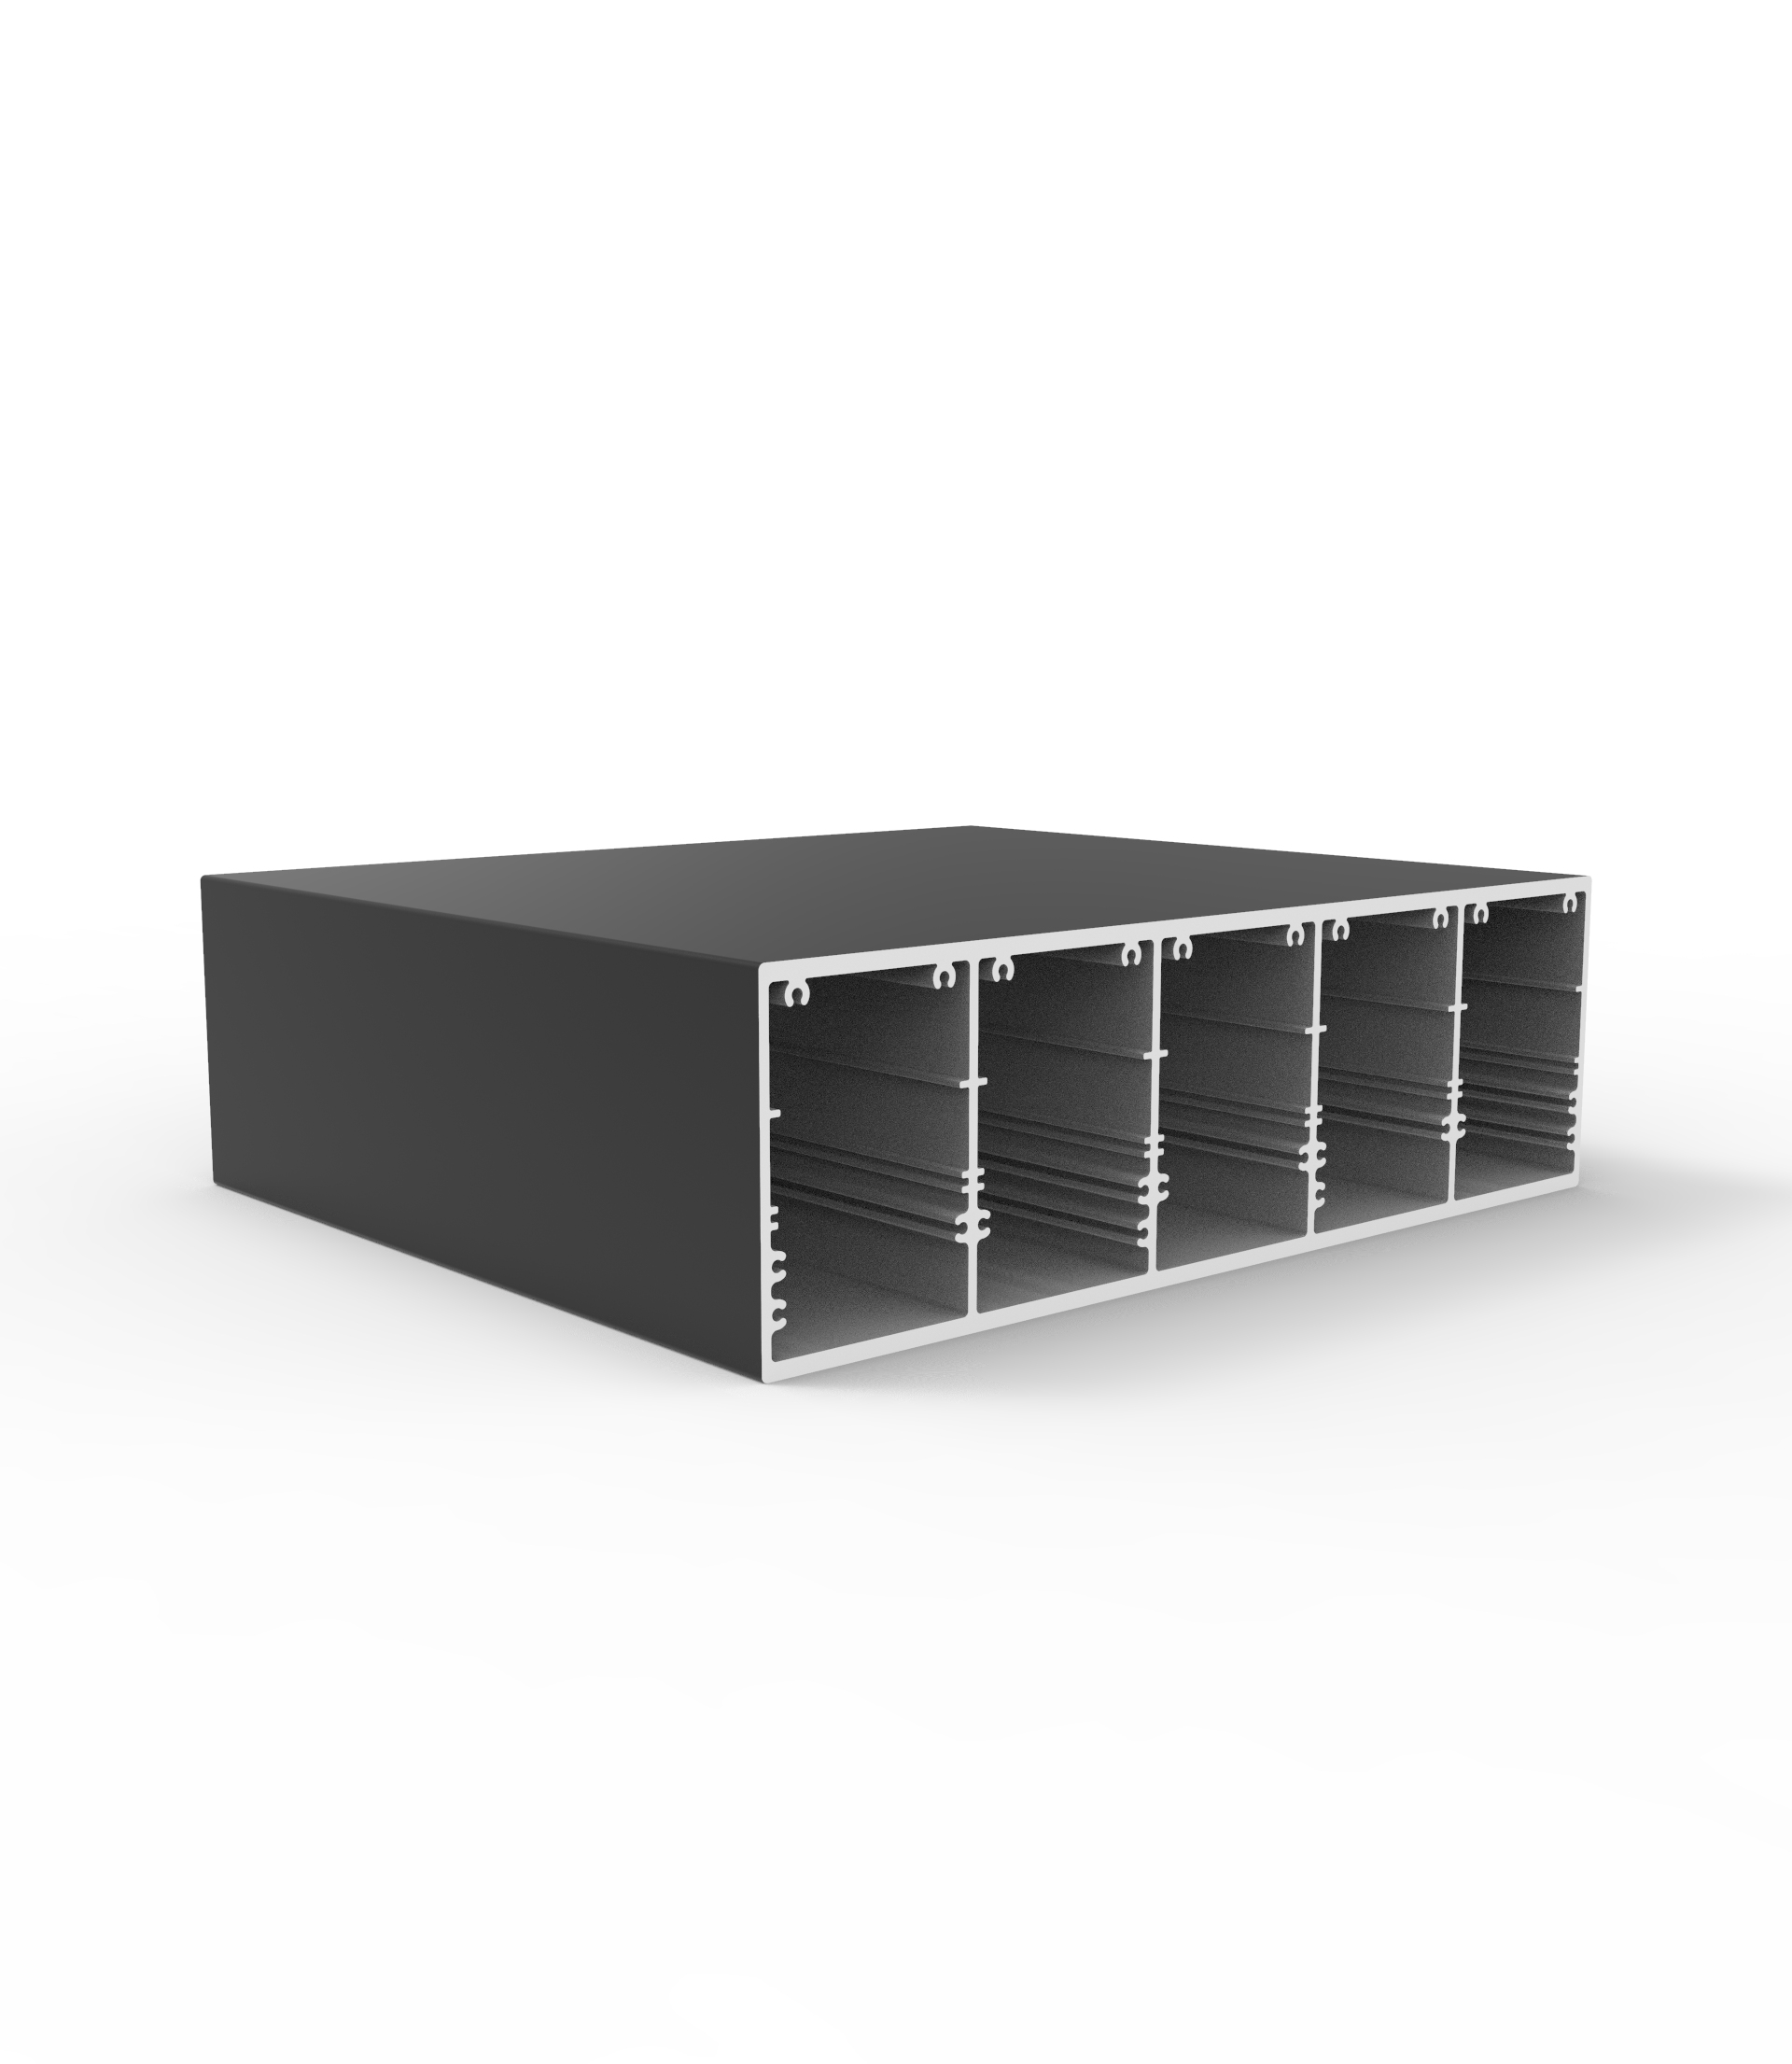
An aluminium square tube optimizes this moment of inertia by maximizing outer perimeter geometry. This specific distribution drastically increases stiffness compared to a solid bar of equivalent weight. Engineers utilize this geometric principle to achieve high structural rigidity with minimal raw material.
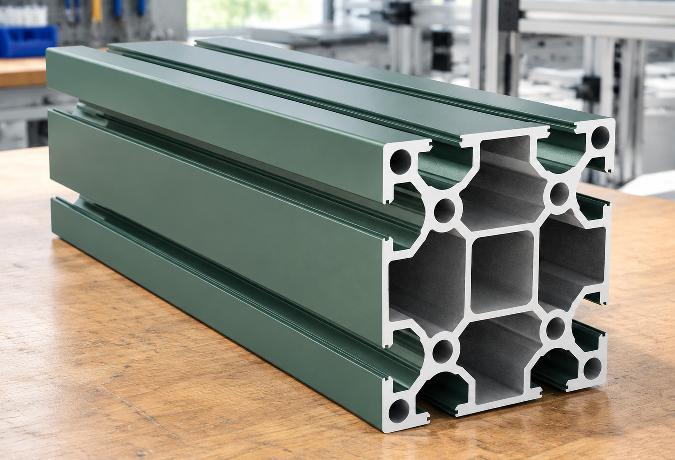
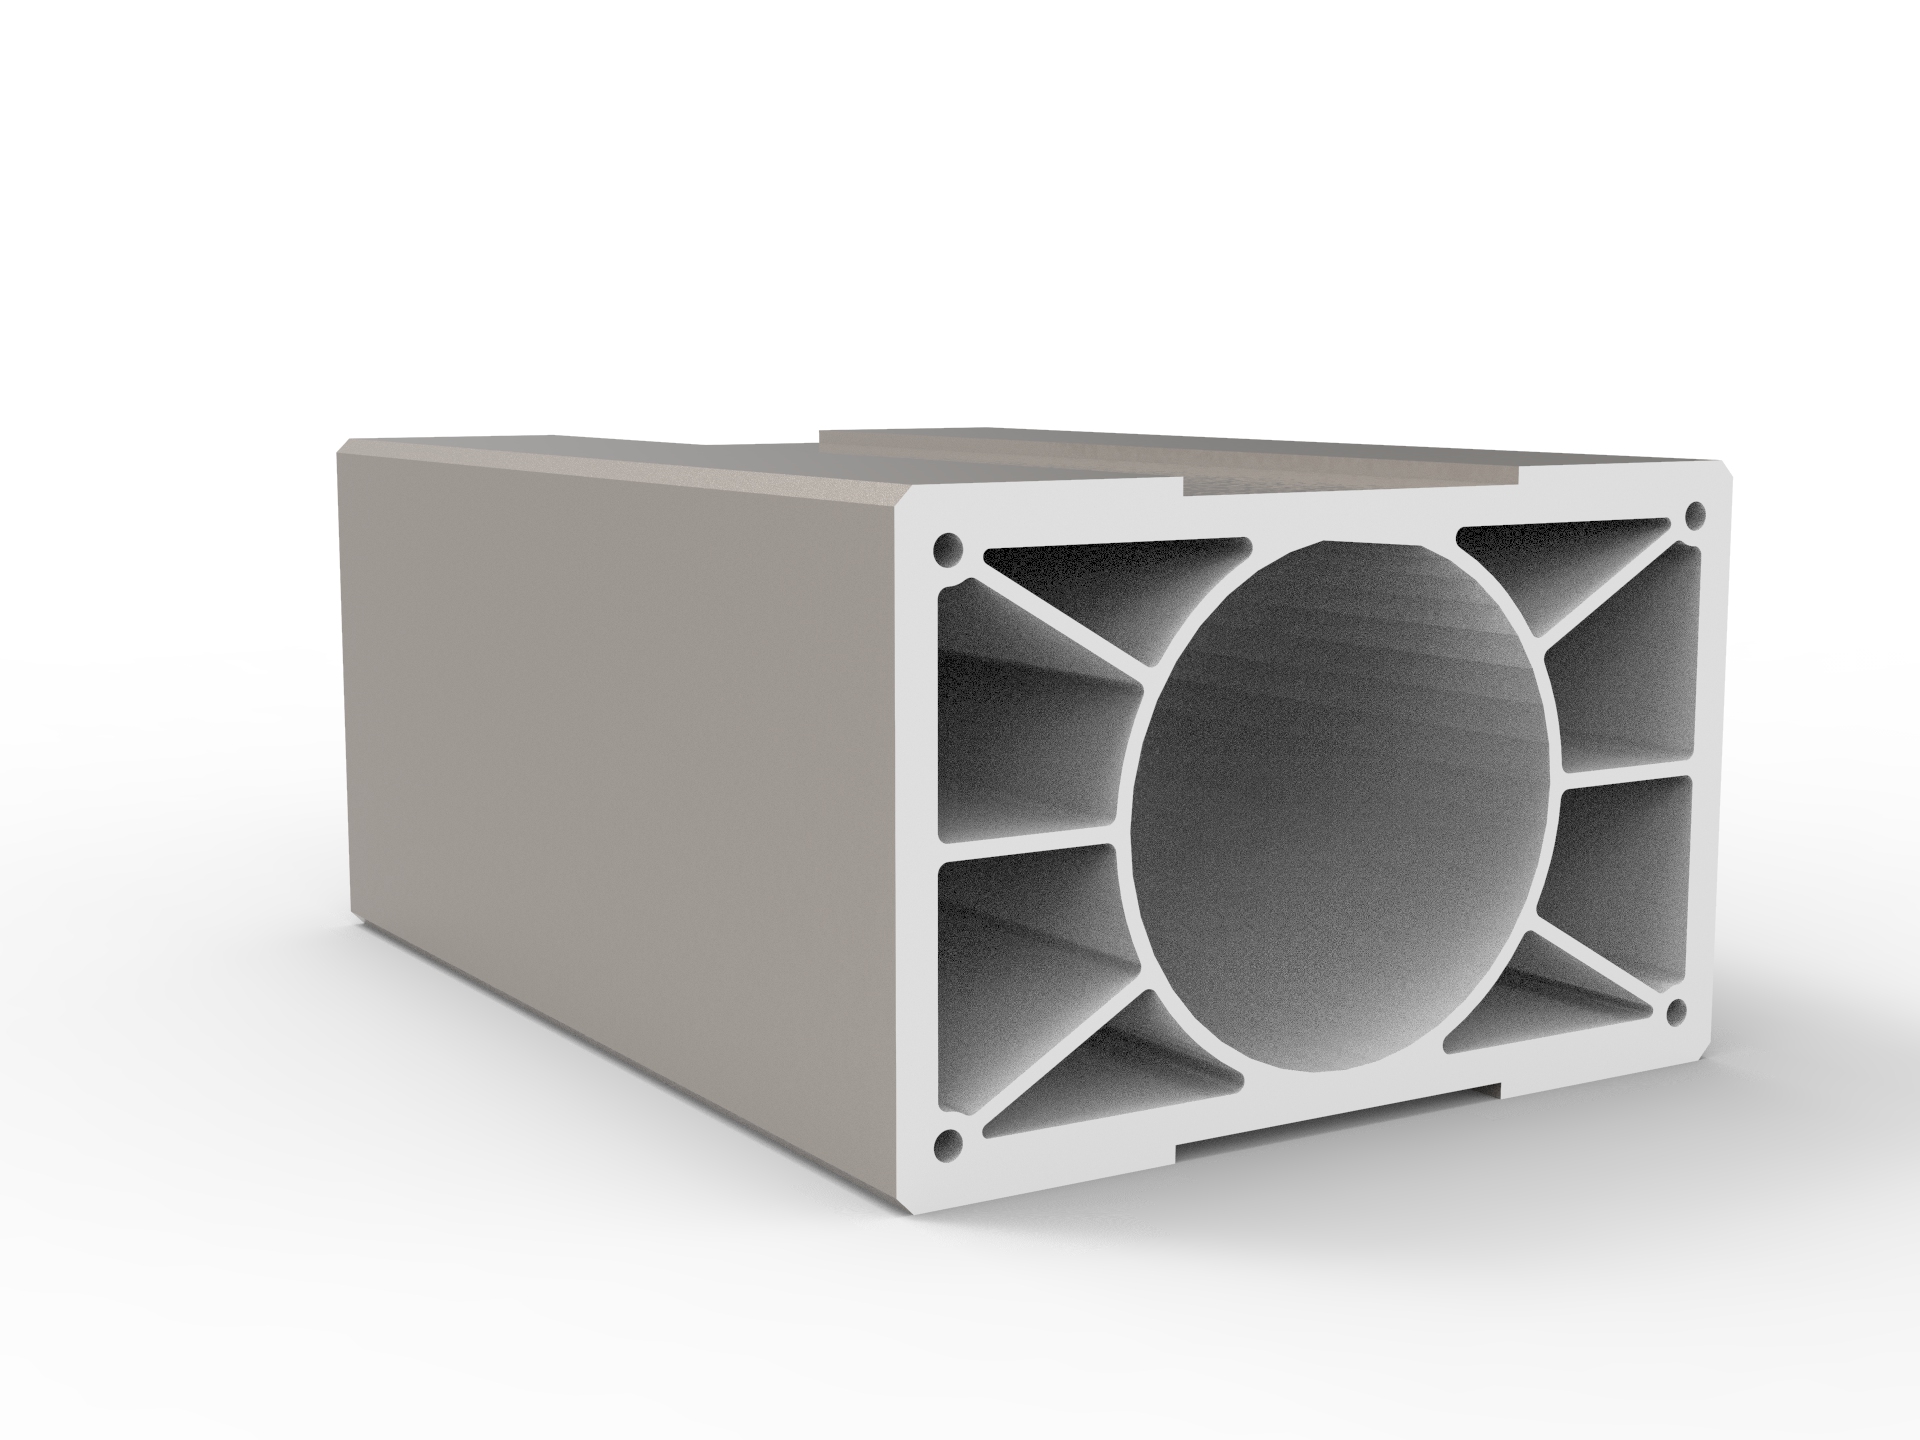
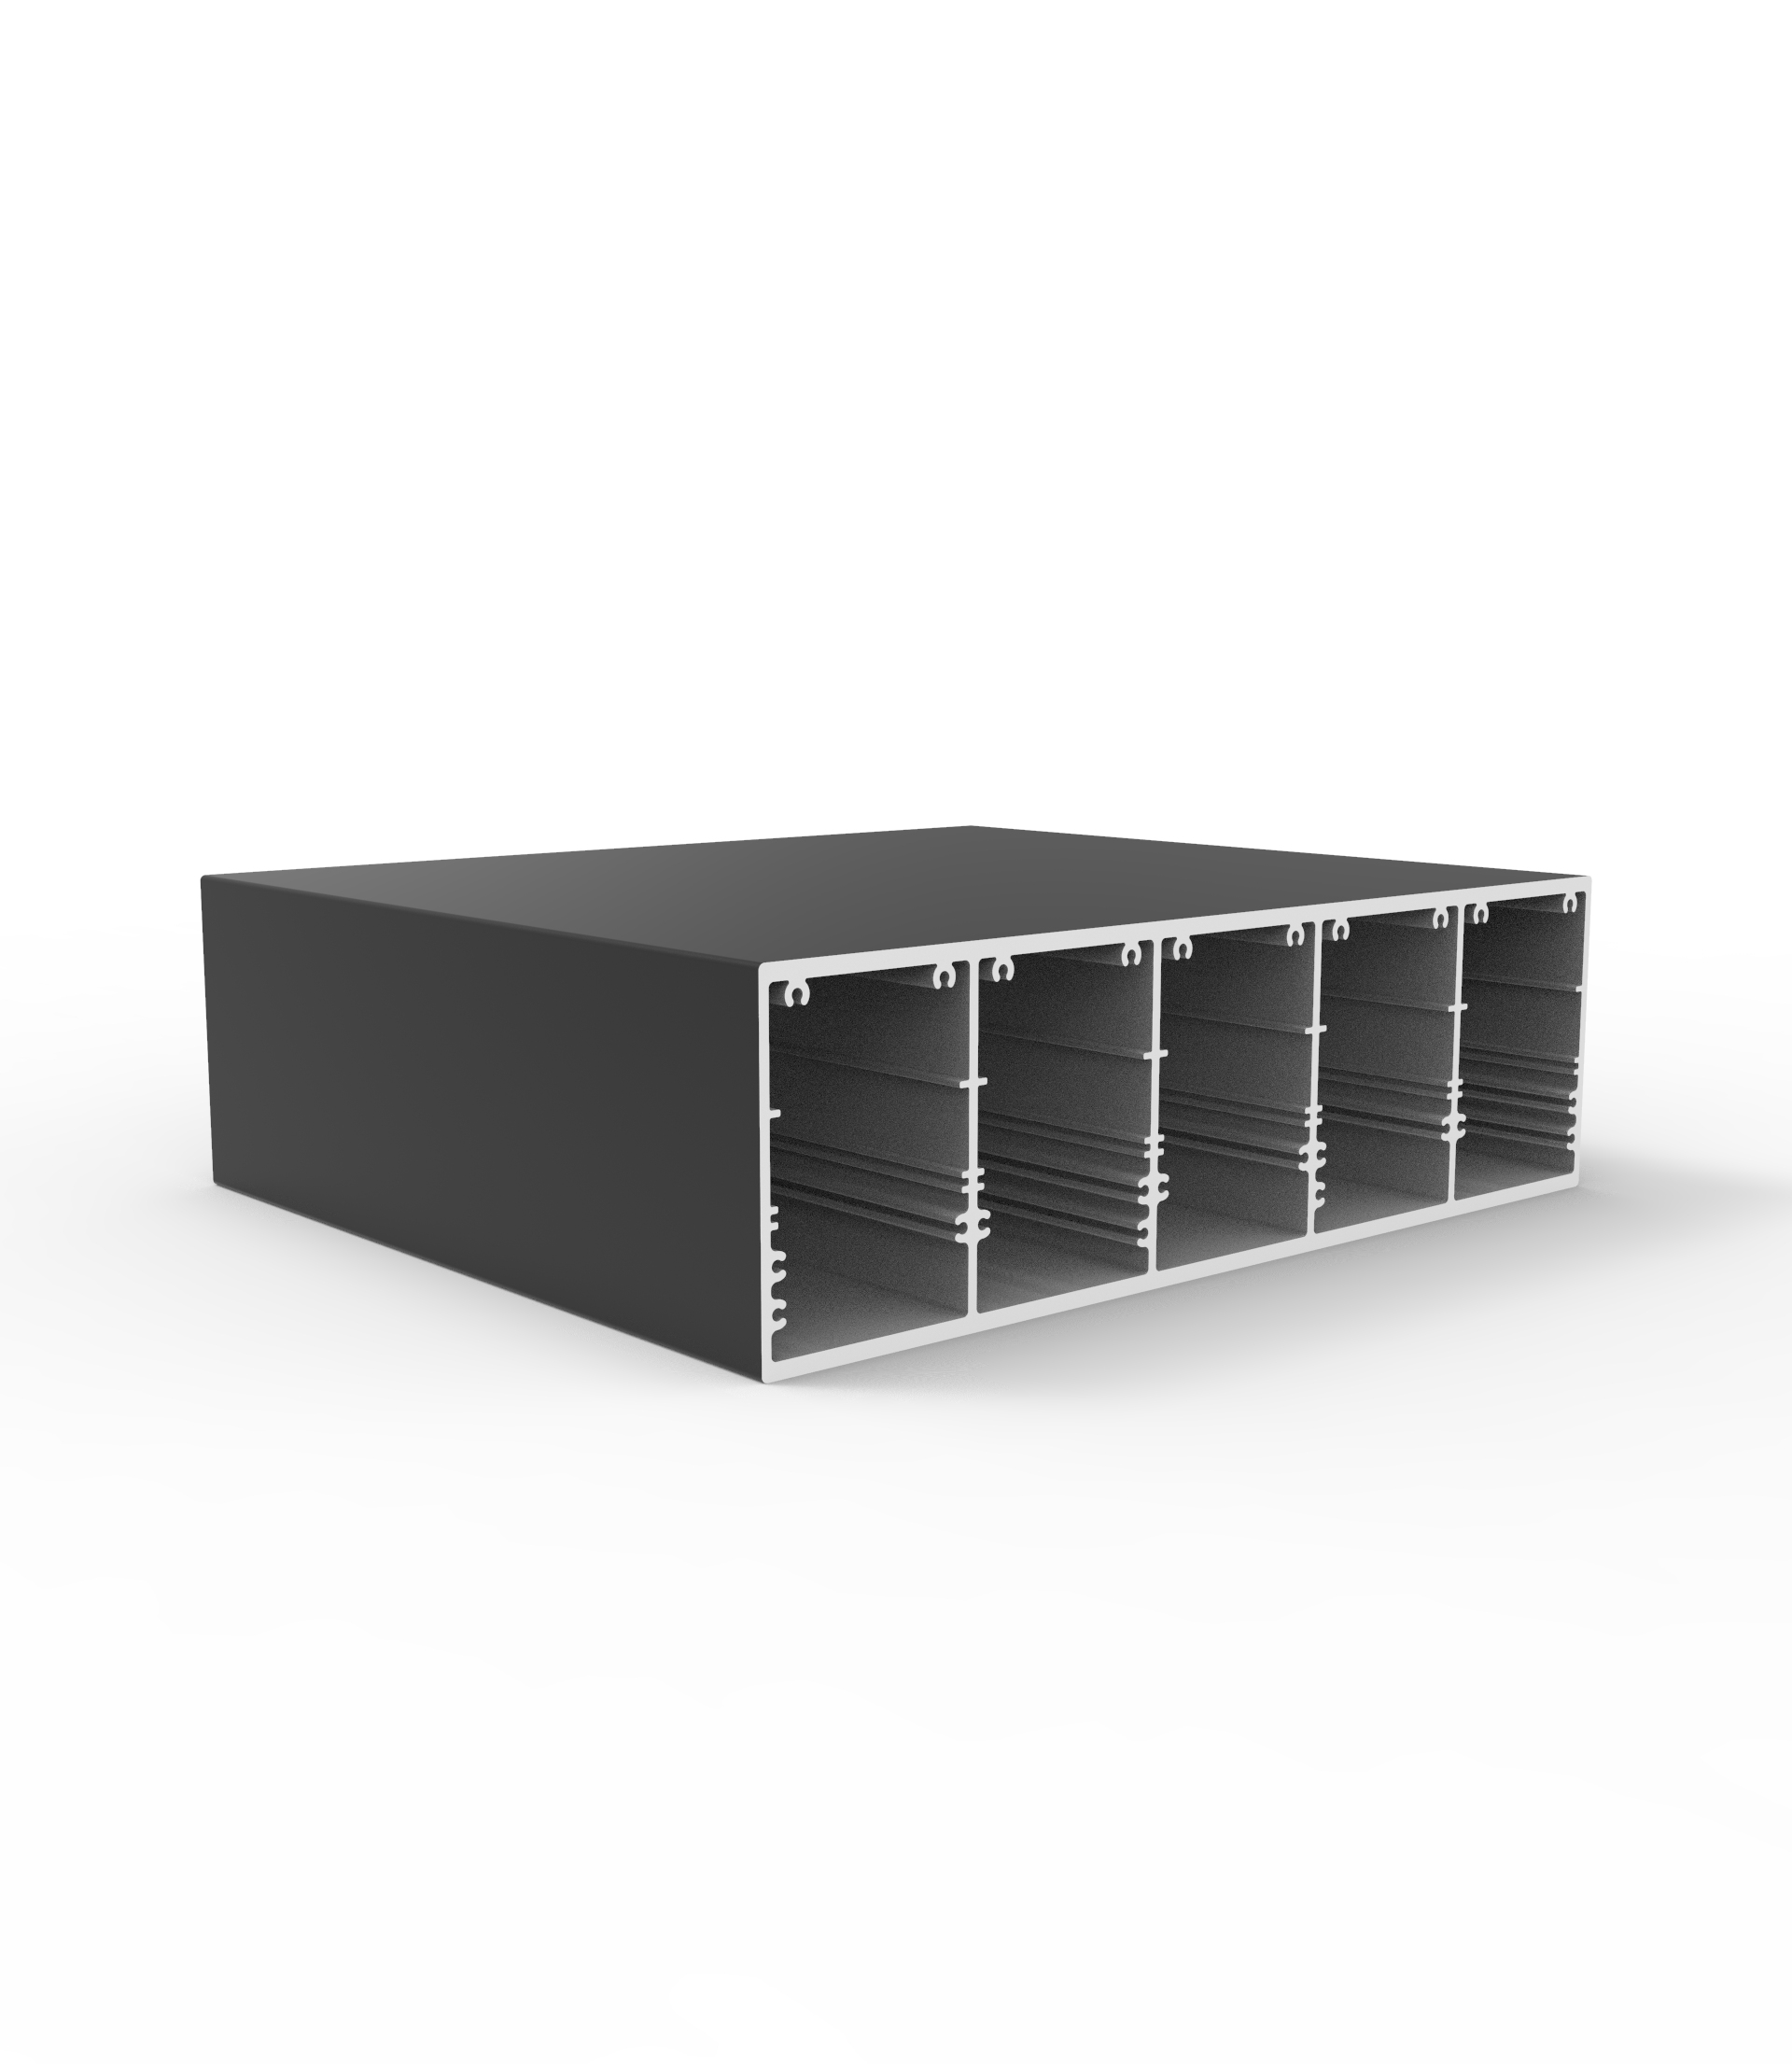
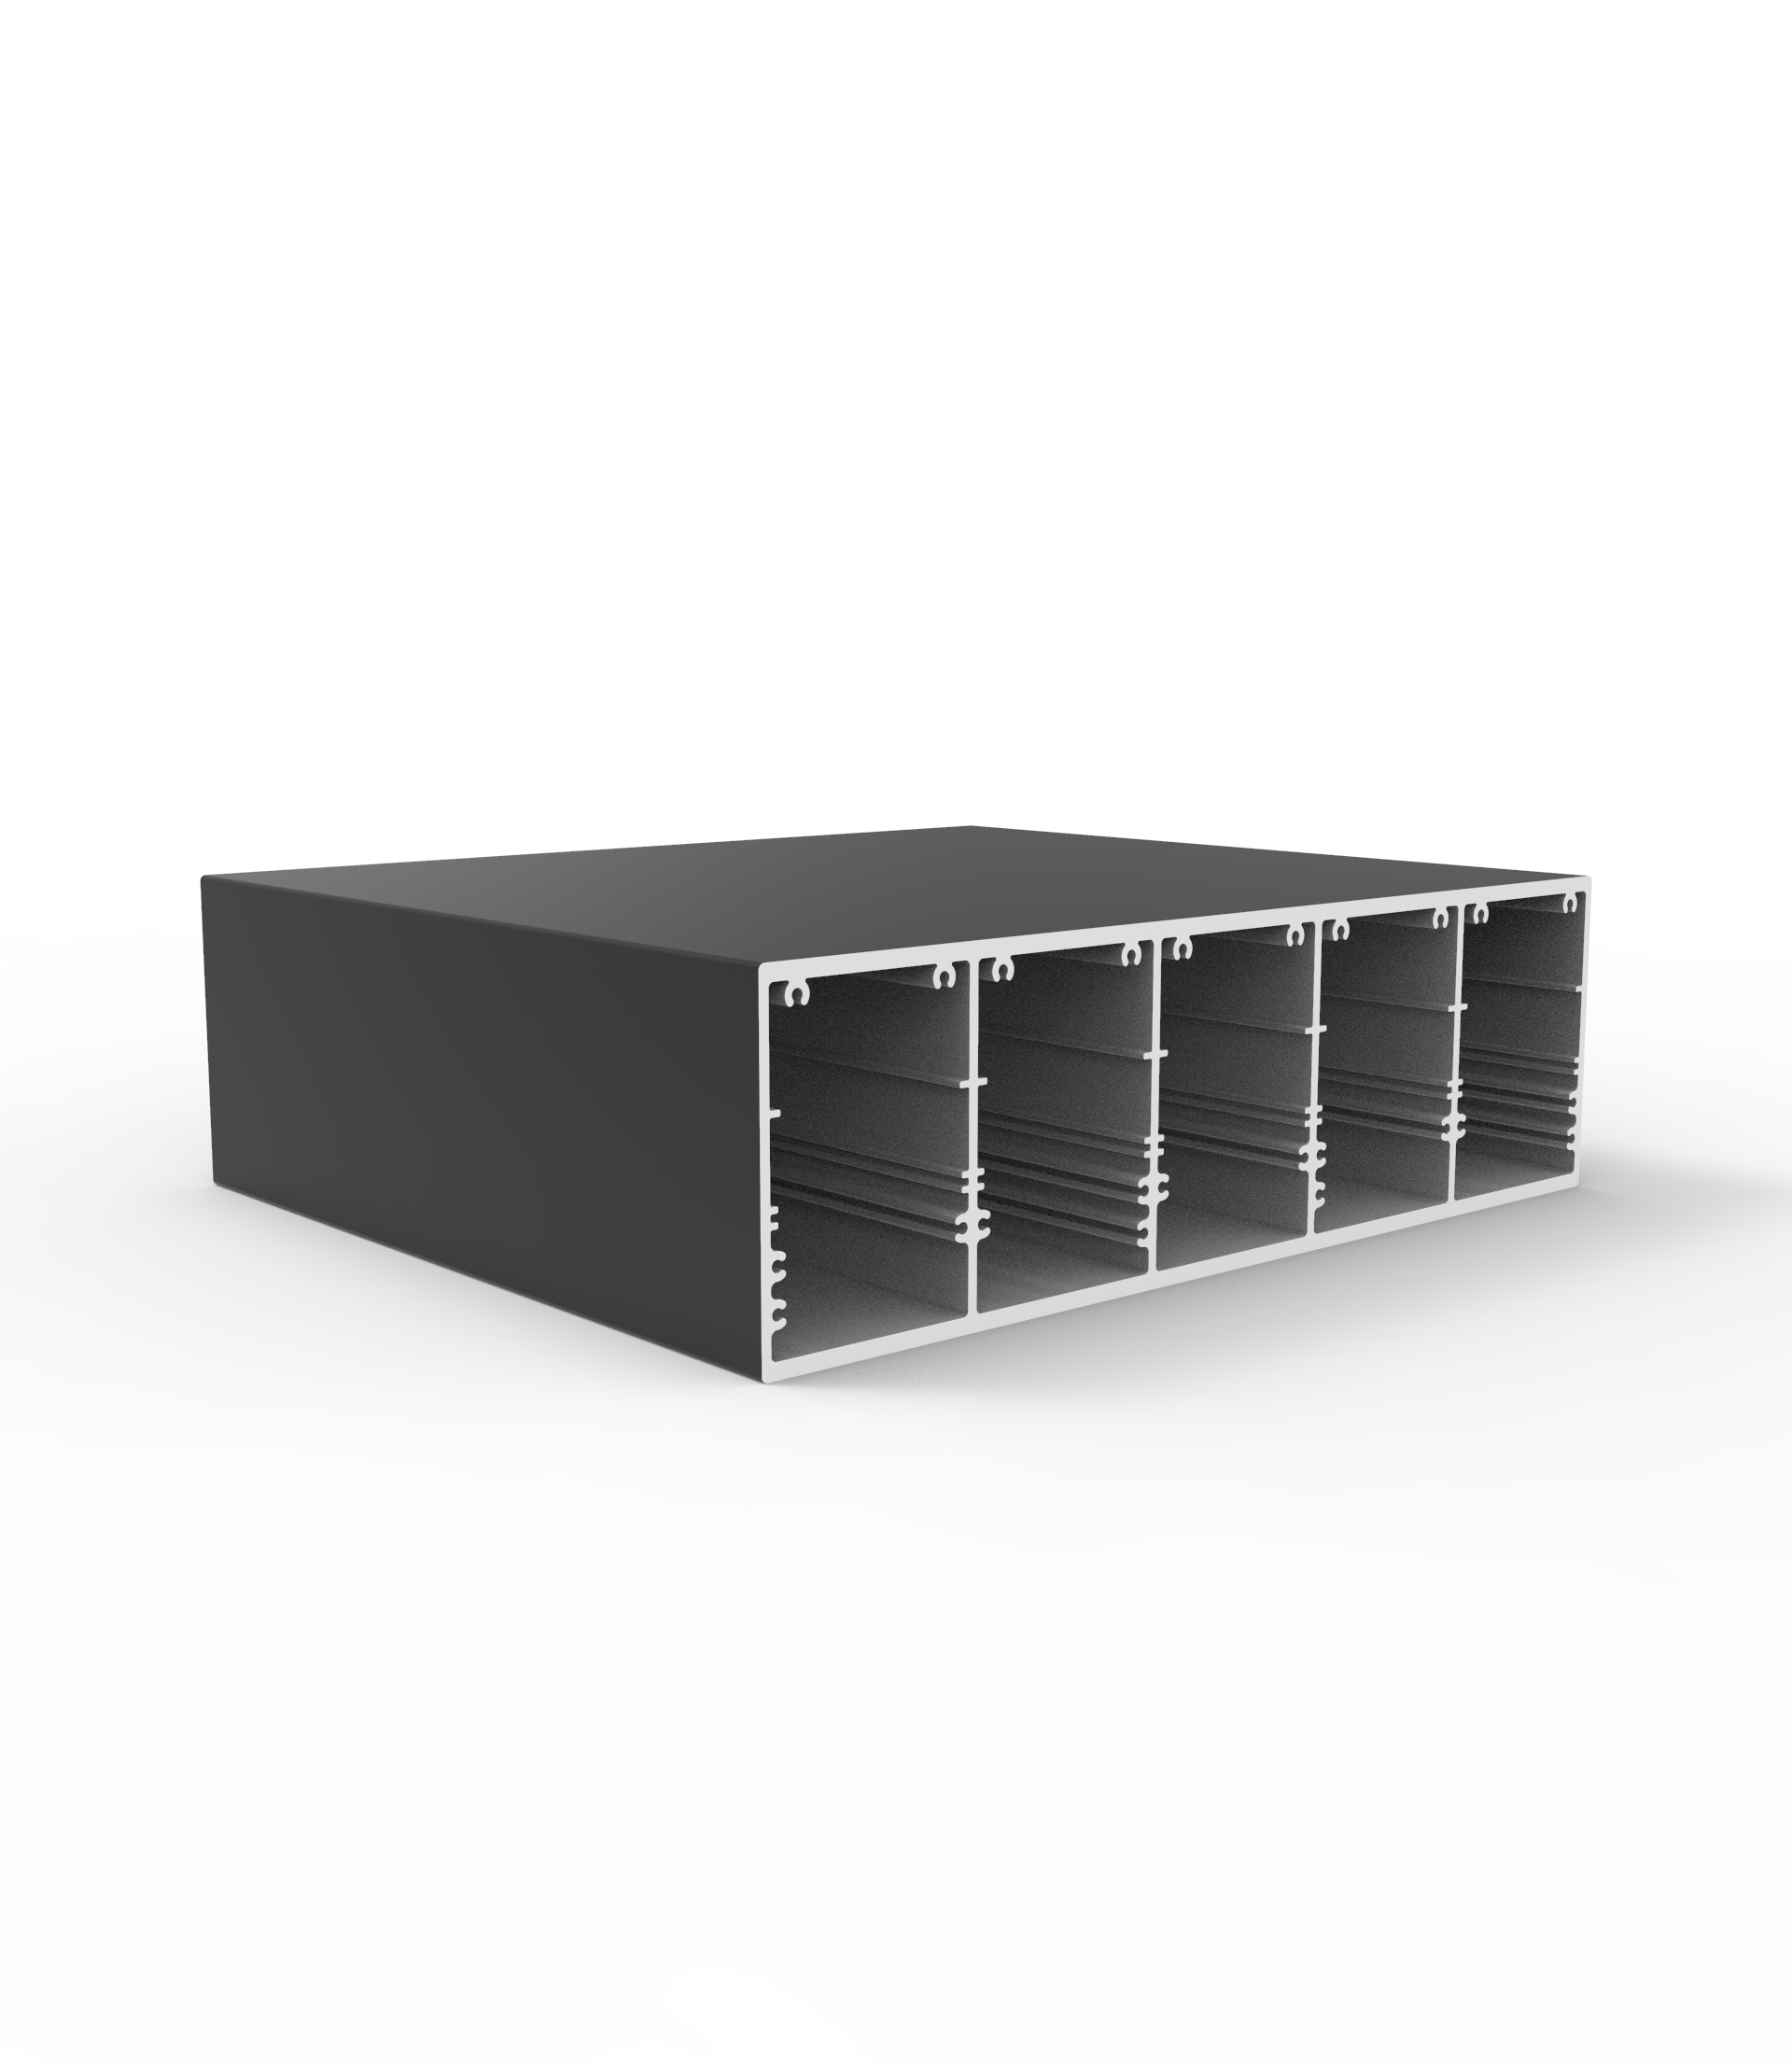
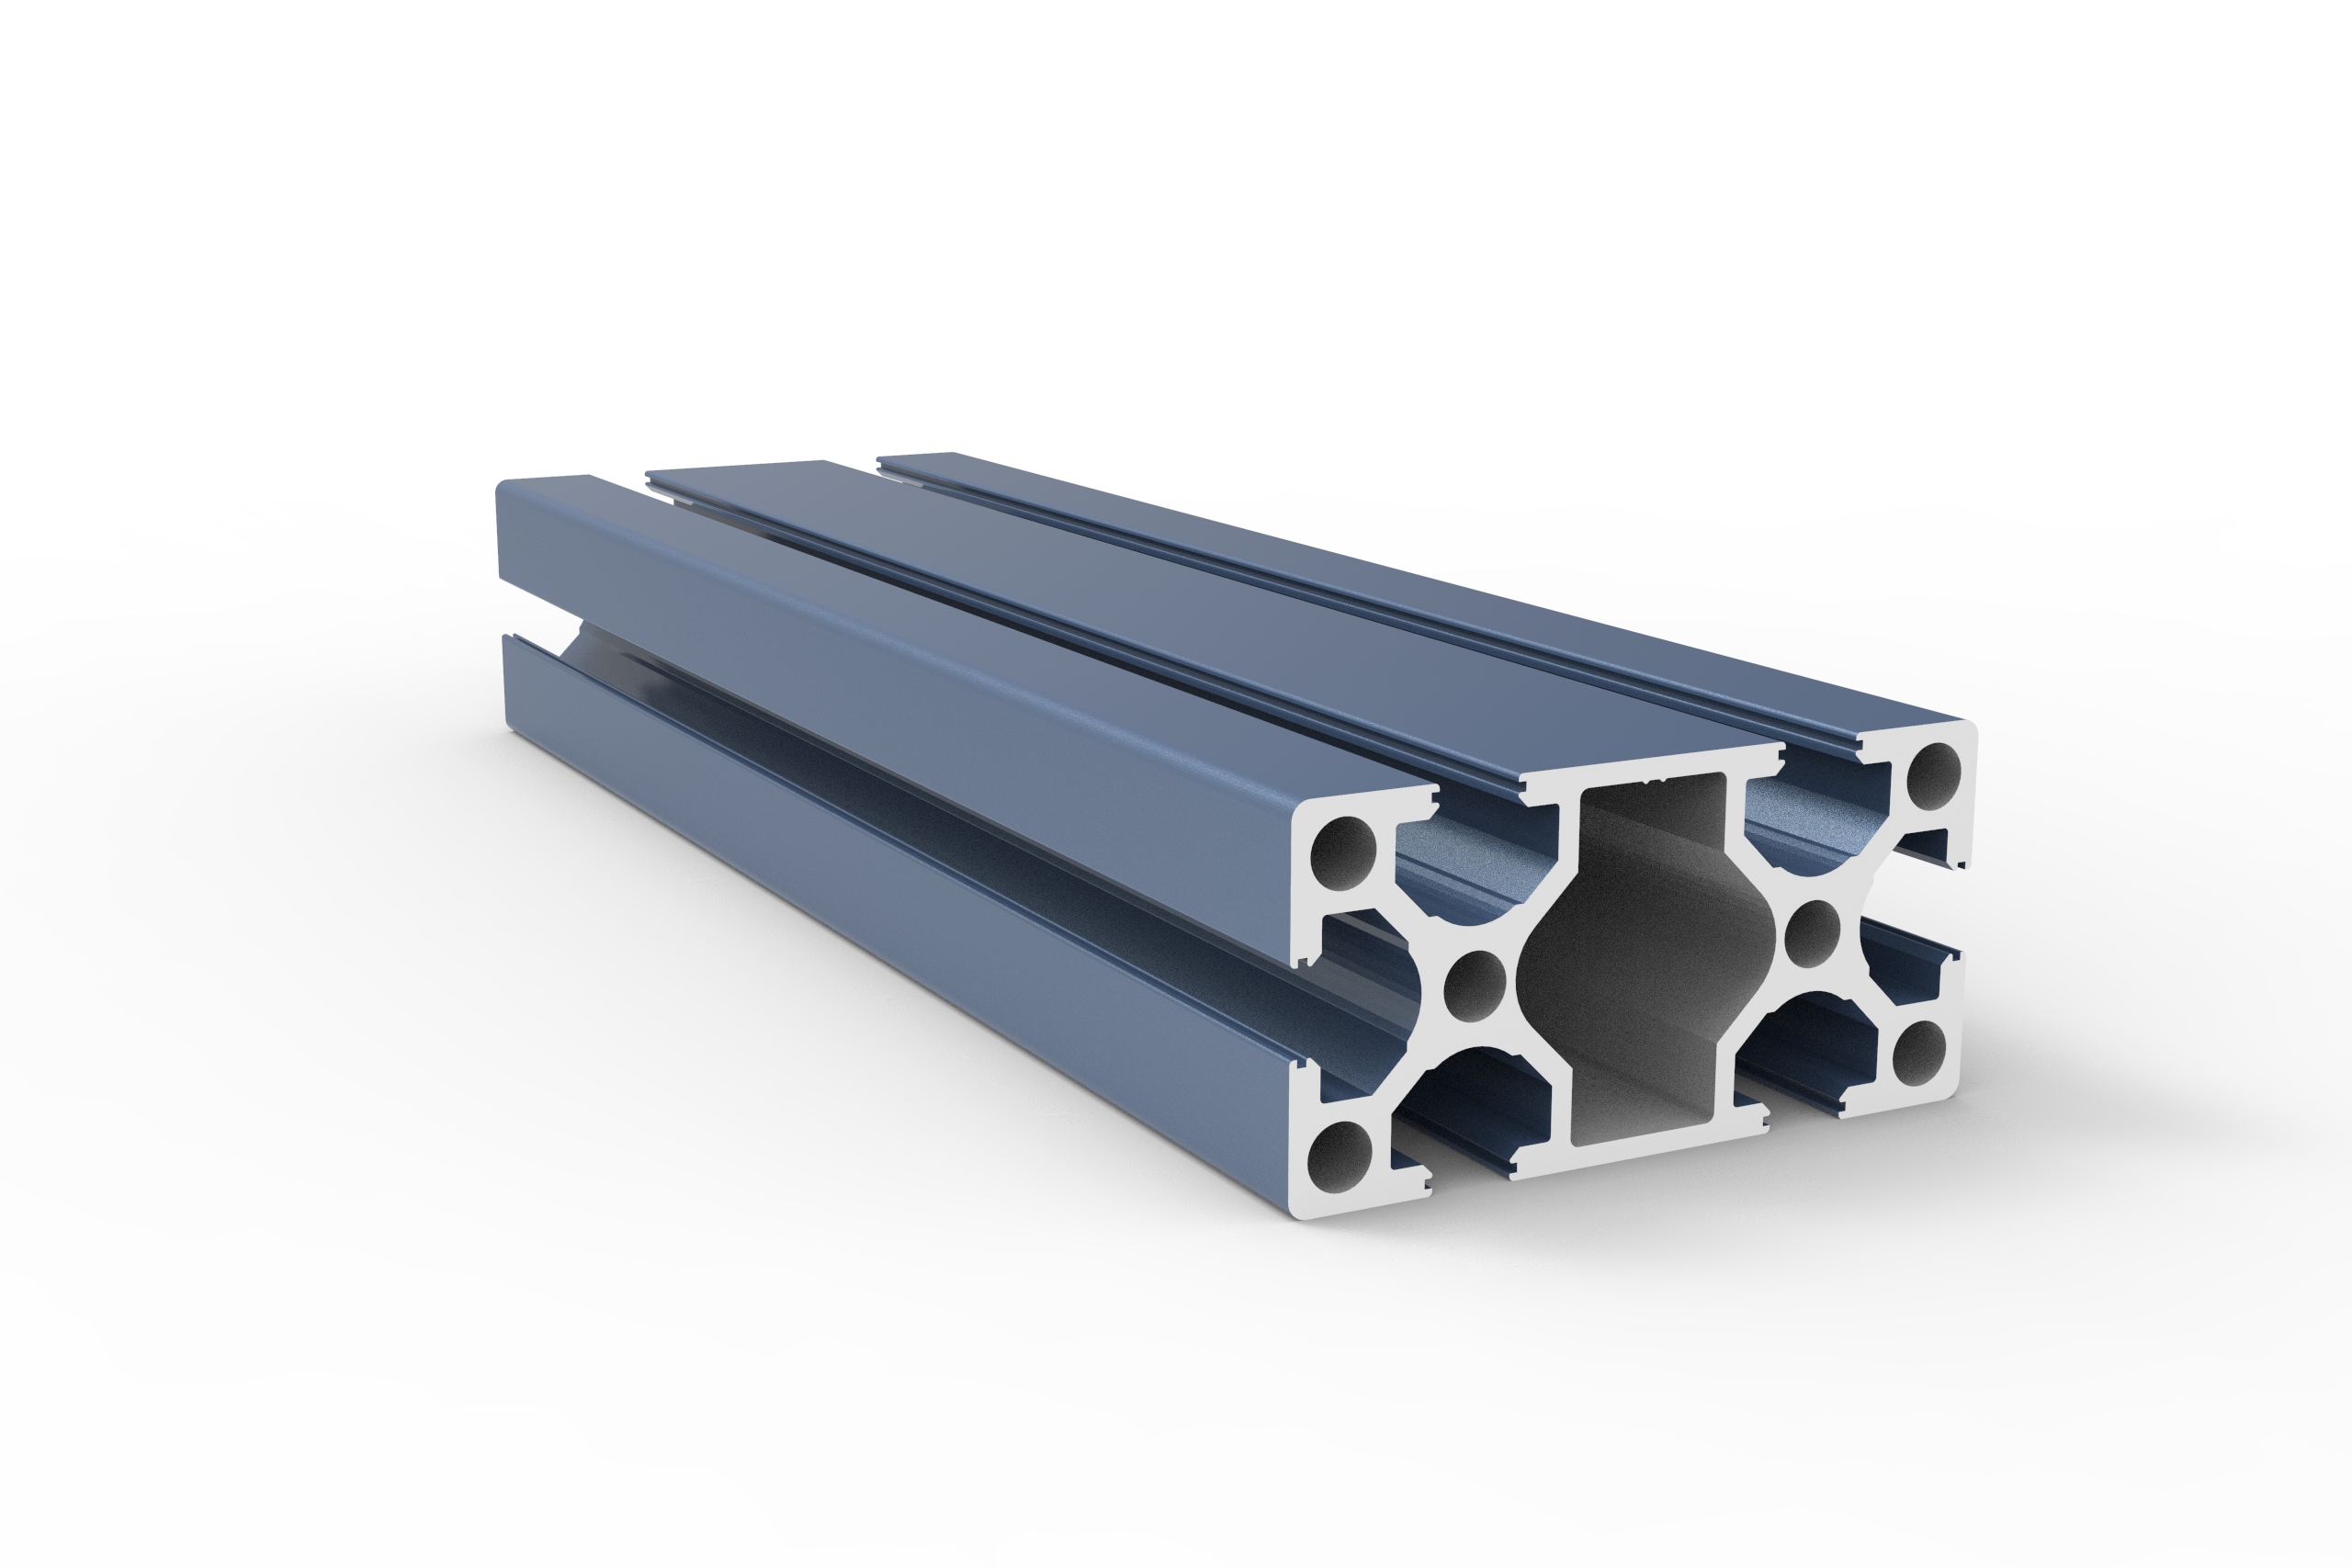
When examining the cross-section of these extrusions, uniform wall thickness is critically important. This uniformity ensures that stresses distribute evenly across the four perpendicular walls. Uneven walls would create dangerous stress concentrations, leading to unpredictable buckling under heavy axial loads.
Round tubes offer exceptional resistance to internal fluid pressure and torsional twisting forces. Square configurations excel in entirely different structural loading scenarios across construction applications. Flat exterior surfaces provide inherent geometric advantages for mechanical joining and mating.
Connecting round tubes requires complex saddle cuts or specialized notching during the fabrication phase. A square cross-section aligns perfectly with Cartesian coordinate systems used in architectural framing grids. When a vertical load is applied, the two parallel vertical walls act as load-bearing webs.
The top and bottom horizontal walls function precisely as structural flanges. These flanges effectively resist the primary tension and compression forces generated by the bending moment. This behavior mimics the mechanics of a traditional steel I-beam while maintaining a closed envelope.
A closed tubular envelope provides significant advantages in preventing torsional buckling under eccentric loads. An open I-beam can twist dramatically if the applied load is not perfectly centered. The closed square profile naturally resists this twisting motion, providing a more stable structural member.
Commercially pure aluminum lacks the mechanical yield strength required for rigorous structural applications. Metallurgists must introduce precise quantities of magnesium and silicon into the base metal. This specific combination creates the highly versatile 6000-series structural alloy family.
These alloying elements react during heat treatment to form microscopic magnesium silicide particles. This specific intermetallic compound acts as the primary hardening agent within the crystalline matrix. The precipitates physically block dislocation movements within the metal grains, raising the yield threshold.
The construction industry standardizes heavily around 6063 and 6463 alloys for architectural extruded profiles. These specific variations perfectly balance mechanical yield strength with hot working extrudability. A high-strength aerospace alloy like 7075 is notoriously difficult to push through complex dies.
The 6063 alloy flows predictably and smoothly through the heated steel extrusion die. This fluid behavior ensures precise, sharp external corners on the resulting hollow profiles. It prevents surface tearing and maintains the strict dimensional tolerances required for structural interlocking.
Extruding the hollow shape represents only half of the required metallurgical equation. The subsequent thermal processing dictates the final mechanical properties of the finished profile. These thermal cycles are formally known as tempering processes within the metals industry.
The standardized designations T5 and T6 represent specific cooling and artificial aging methodologies. These precise thermal cycles manipulate the precipitation of magnesium silicide within the aluminum microstructure. Controlling this precipitation is the key to unlocking structural rigidity.
A T5 temper involves cooling the hot extrusion naturally in the air after exiting the die. The metal is then placed in a specialized oven for artificial aging at controlled temperatures. This process provides a baseline rigidity suitable for interior decorative partitions or light frames.
The T6 temper requires rapid quenching with pressurized water or forced air immediately after extrusion. This severe, rapid cooling locks the alloying elements into a supersaturated solid solution. Subsequent artificial aging creates a much finer, highly uniform dispersion of hardening precipitates.
The rigorous T6 process yields significantly higher tensile strength and proportional yield limits. Engineers explicitly specify the T6 temper when the member must function as a primary load-bearing truss. Using a T5 temper in a T6 application would invite dangerous structural deflection.
The decision between alloy tempers fundamentally alters the safety margins of the constructed framework. Understanding the numerical differences helps prevent over-engineering or unsafe material specification.
Raw machined metal naturally forms a thin, invisible layer of aluminum oxide upon oxygen exposure. This microscopic passivation layer technically prevents further rapid oxidation of the underlying metal matrix. Relying solely on this natural, fragile defense is structurally risky in harsh environments.
Coastal salt spray or industrial sulfur pollutants can easily breach this native oxide film. Once breached, localized pitting corrosion can rapidly undermine the structural integrity of the wall. Engineers demand controlled surface treatments to ensure the long-term viability of the framework.
These industrial surface treatments either modify the surface chemistry or apply a tough physical barrier. The selected method directly impacts the life expectancy and maintenance schedule of the installation.
Anodizing is an advanced electrochemical process that forces the natural oxide layer to grow thicker. It does not apply a foreign layer of paint over the raw metal substrate. Instead, it physically transforms the surface of the aluminium square tube into dense aluminum oxide.

This resulting porous oxide structure is incredibly hard, mimicking the molecular structure of a sapphire. After the anodic pores are sealed, the profile becomes highly resistant to mechanical scratching. This makes anodized finishes ideal for high-traffic architectural railings and exposed tactile surfaces.
Electrostatic powder coating provides a completely different but equally effective protective mechanism. Electrostatically charged dry polymer powder is sprayed directly onto the electrically grounded metal profile. The coated profile is then baked at high temperatures, melting the powder into a continuous skin.
This thick polymeric skin allows for vast aesthetic customization across architectural projects. It enables accurate wood grain transfer techniques used frequently for decorative exterior louvers. The tough coating prevents moisture and atmospheric salts from reaching the reactive metal substrate.
Fluorocarbon coatings represent the absolute highest tier of liquid architectural paint protection available today. The complex resin contains incredibly strong carbon-fluorine chemical bonds that resist ultraviolet degradation. This specific chemical resistance makes fluorocarbon finishes the default specification for high-rise exterior cladding.
Integrating these hollow sections into a building requires strict adherence to strict deflection limits. A structural member might not actually break under a heavy load, but it could bend excessively. Excessive deflection causes immediate secondary damage to rigidly attached components like glass panes.

When deployed as architectural ceiling grilles, gravity acts as the primary downward force. The dead load of the profile itself must be calculated alongside any attached mechanical fixtures. The hollow interior geometry keeps this parasitic dead load remarkably low across long spans.
This low mass allows architects to design expansive, complex overhead grid features safely. They can achieve striking visual aesthetics without overburdening the primary steel or concrete ceiling structure. Managing dead weight is critical when retrofitting older buildings with modernized architectural facades.
Exterior architectural applications face highly dynamic and unpredictable environmental forces. Garden boundary screens and architectural privacy fences must safely resist severe lateral wind pressure. A dense privacy screen acts essentially as a solid sail, capturing massive wind energy.

This kinetic wind energy is transferred directly to the vertical support posts as a bending moment. The concentrated bending stress reaches its absolute maximum at the fixed base of the post. Structural engineers must carefully select a profile capable of resisting this specific lateral bending force.
Engineers calculate the required spacing of vertical supports based on the section modulus. Increasing the wall thickness of the tube provides a linear increase in structural bending strength. However, increasing the outer dimensions of the tube provides an exponential increase in strength.
It is almost always more structurally economical to use a larger tube with thinner walls. A small tube with excessively thick walls wastes material near the neutral axis. Understanding this geometric relationship dictates efficient material procurement for large exterior shading structures.
The practical application of any structural profile depends entirely on its dimensional predictability. Extrusion dies inevitably wear down as thousands of tons of heated metal pass through them. This microscopic abrasive wear subtly alters the external dimensions of the resulting profiles over time.
Industry manufacturing standards dictate strict tolerance bands to ensure consistent mechanical assembly. When a designer attempts to slide one tube inside another for a telescopic joint, tolerances rule. If the inner tube runs slightly large and the outer tube runs small, the joint binds.
High-quality extrusion manufacturing involves continuous die maintenance and precise laser measurement protocols. When the hot profile exits the die, it is rapidly stretched by a massive hydraulic machine. This stretch-leveling process straightens the profile and relieves internal thermal residual stresses.

Relieving these residual stresses prevents the tube from warping wildly when it is later cut. A machinist expects a long structural beam to remain perfectly straight after a section is removed. Without proper stretch-leveling, internal forces would cause the remaining metal to twist unpredictably.
The structural 6000-series alloys are renowned for being readily machinable in fabrication shops. They can be cleanly cut, drilled, routed, and tapped using standard industrial metalworking equipment. However, joining these specific heat-treated profiles through thermal welding requires deep metallurgical understanding.
Tungsten Inert Gas welding introduces intense, highly localized heat into the metal framework. This severe thermal input essentially reverses the artificial aging process near the molten weld pool. The surrounding metal, known precisely as the heat-affected zone, loses its engineered T6 temper.
This localized area suffers a dramatic and permanent drop in tensile yield strength. Engineers must mathematically design structural nodes assuming this specific localized drop in capacity. Ignoring the weakness of the heat-affected zone is a primary cause of welded frame failures.
To circumvent this thermal degradation, engineers frequently employ specialized mechanical fastening methods. Concealed steel brackets, high-strength structural adhesives, and mechanical blind rivets offer highly reliable connections. Mechanical joints also accommodate natural thermal expansion and contraction in long continuous architectural assemblies.
The integration of lightweight metal extrusions into traditional heavy steel workflows generates technical friction. Assumptions carried over directly from ferrous metallurgy do not always apply accurately to non-ferrous profiles. Clarifying these mechanical realities is necessary for safe, efficient structural framework design.
Wall thickness is only one singular variable in the complex structural deflection equation. As previously noted, outer dimensions exert a profoundly greater influence on bending resistance than wall mass. A 100mm profile with a 2mm wall will resist deflection far better than a 50mm profile with a 4mm wall. If spatial constraints force the use of a small profile, increasing wall thickness is required, but it is rarely weight-efficient.
The interior channels of these specific extrusions rarely receive powder coating coverage. This is caused by the Faraday cage effect repelling charged powder during the electrostatic spraying process. However, the alloy still forms its natural protective oxide layer internally. Standing water mixed with acidic pollutants can eventually degrade this internal native layer. Proper engineering requires drilling deliberate weep holes at the lowest points to ensure moisture drains completely.
Direct physical contact between dissimilar metals in a moist environment initiates severe galvanic corrosion. The less noble metal, which is the extruded profile in this scenario, will act as an anode and sacrifice itself. It will rapidly corrode away at the exact point of contact with the steel bracket. Structural engineers must mandate the installation of isolating neoprene gaskets or dielectric nylon washers to break the electrical circuit between the metals.
Sourcing material for a large-scale architectural facade requires aligning engineering specifications with manufacturing realities. Minimum order quantities typically range heavily from 100 to 500 kilograms per distinct profile section. This volume dictates the economic feasibility of designing custom extrusions versus relying on standard modular sizes.
Lead times for standard structural alloys and common surface treatments usually span 10 to 20 days. Requesting custom color matching for fluorocarbon exterior coatings will naturally extend this production timeline. The supplier must manage the complex scheduling of extrusion, heat treatment, surface finishing, and quality inspection.
For us, integrating research and manufacturing across a 200,000-ton annual capacity provides distinct insights. Operating for over 25 years and supplying custom profile services to more than fifty countries requires deep metallurgical discipline. This operational scale ensures that raw alloy billets are transformed consistently into reliable architectural components.
The precise specification of an aluminium square tube demands a thorough understanding of structural geometry. It is never merely a lightweight, visual replacement for heavy traditional structural steel. It is a highly specialized component designed for environments demanding strict weight control and geometric precision.
By balancing the engineered temper of a structural alloy with appropriate dimensional scaling, designers solve complex load-bearing problems. Selecting the mathematically correct hollow profile dictates the fundamental stability of the installation. This careful engineering ensures the lasting safety and aesthetic endurance of the final constructed framework.
Choosing Industrial Aluminium Profiles for Laser Cutting Machines: A Technical Guide
How LED Aluminium Profile Heatsinks Manage Thermal Challenges in High-Performance Lighting
Architectural Aluminium Profiles: Choosing the Right Angle Design for Framing and Trim
Choosing the Right Aluminium Balustrade Profiles for Your Project
Choosing the Right Aluminium Door Profiles for Narrow-Frame Sliding Systems
Aluminium Window Profiles: Engineering Durable Facades for Modern Buildings
Aluminium Thermal Break Profiles: Design Principles and Practical Applications
Aluminium Extrusion for Furniture: Structural Logic Behind Lightweight Precision
Aluminium Wardrobe Profiles: A Practical Guide to Frames, Tracks, and Finishes
Choosing the Right Aluminium Linear Rail Profile for Motion Systems
Anodized Aluminium Profiles: Material Selection and Practical Applications in Modern Design
Anodized Aluminium Profiles: Material Selection and Practical Applications in Modern Design
Aluminium Decorative Profiles: Design, Installation, and Interior Applications
Aluminium Profiles for Automation: A Practical Guide to Modular Frame Design
Aluminium Extrusion for Furniture: Structural Logic Behind Lightweight Precision
Aluminium Thermal Break Profiles: Design Principles and Practical Applications
How do suppliers normally handle Sliding door installation problems overseas?
Choosing the Right Aluminium Balustrade Profiles for Your Project
Aluminium Louver Profiles: Light Control and Ventilation in Modern Architecture
Aluminium Curtain Wall Profiles: Structural Design and Performance in Modern Architecture
Aluminium Trim Profiles: Bridging Aesthetics and Performance in Modern Interior Design
How do I verify Casement window production capacity before signing a contract?
Powder Coated Aluminium Profiles: Durability and Design in Modern Applications
How Aluminium Heatsink Profiles Keep Electronics From Cooking Themselves
How do FOB and CIF change my risks when importing Sliding doors?
What support should I receive if Architecture profile dimensions are wrong?
Aluminium Profile Alloys 6063 T5 T6: Properties, Heat Treatment Differences, and Application Selecti
Inside an Aluminium Profile Factory: How Angle Profiles Are Made and Chosen
What is a realistic MOQ for a first Sliding window trial order?
Which factory records should I review before buying Industrial profile?
Aluminium Extrusion for Machinery: Choosing the Right Profile for Industrial Equipment
Aluminium Extrusion for LED Lighting: Choosing the Right Heatsink Profile
Can a Floding door supplier protect my private design from competitors?
Which Industrial profile tolerances affect assembly accuracy and finished quality?
Can trade credit insurance cover my Architecture profile purchase risk?
Custom Aluminium Extrusion Profiles: Engineering Precision into Industrial Motion Systems
T-Slot Aluminium Extrusion: Structural Framework Design Without Welding
Which recycled-content records are credible for Sliding window procurement?
Aluminium Sliding Door Profiles: A Practical Guide to Frame Design and Performance
How Aluminium Extrusion Manufacturers in China Support Linear Motion Systems
What contract clauses protect my money if Casement door quality is unacceptable?
How do I confirm Sliding door testing equipment is calibrated and current?
Should I visit an Architecture profile plant before placing a large order?
Which compliance tests should a Floding door pass before international shipment?
How do I compare Decorative profile color samples under different lighting?
What payment and price terms make sense for a small Casement window order?
What lead time should I allow for a seasonal Floding door order?
How can I compare Floding door alternatives when supply costs suddenly rise?
Which new Sliding door technologies can lower maintenance costs over time?
How are recycled materials changing the future cost of Floding doors?
How long should a custom Casement door sample normally take to prepare?
What gap between a Sliding window sample and bulk order is acceptable?
Which Decorative profile finishes are becoming more sustainable and cost-effective?
What logistics fees should be listed separately in a Sliding window quote?
How might volatile aluminum prices affect future Sliding window sourcing?
Which audit questions reveal labor risks at a Casement door factory?
Can Decorative profile suppliers provide fast remote guidance for finish defects?
What should a Shutter sample include so I can assess production quality?
Do Sliding door materials need traceability records for customs clearance?
What environmental declarations are useful when importing Architecture profile?
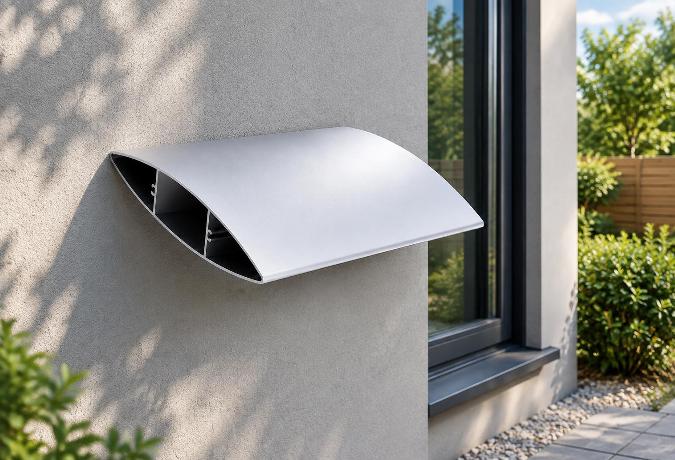
Why Blade Geometry Determines Whether Aluminium Louvers Actually Work
Engineering an Aluminium Angle Profile: Structural Mechanics and Application Realities
What usually drives Architecture profile costs more, alloy or surface treatment?
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
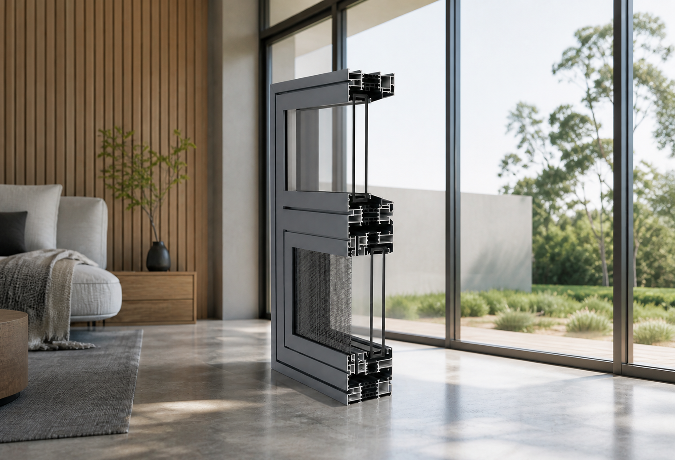
Why the Thermal Break Cavity Matters More Than Frame Thickness in Aluminium Framed Windows and Doors
The T-Slot Groove Geometry That Makes Aluminium Framing Weld-Free
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
Structural Dynamics of Industrial Aluminium Profiles in Laser Cutting Gantries
The Engineering Mechanics Behind High-Performance Aluminium Shutters
What factory documents should I request for a Floding door supplier review?
Which delivery term gives me better control over Decorative profile freight costs?
What low-carbon Awing window materials are gaining wider market acceptance?
Why Sliding Door Track Geometry Determines Wardrobe Longevity
Engineering Mechanics and Surface Dynamics of Aluminium Channel Profiles
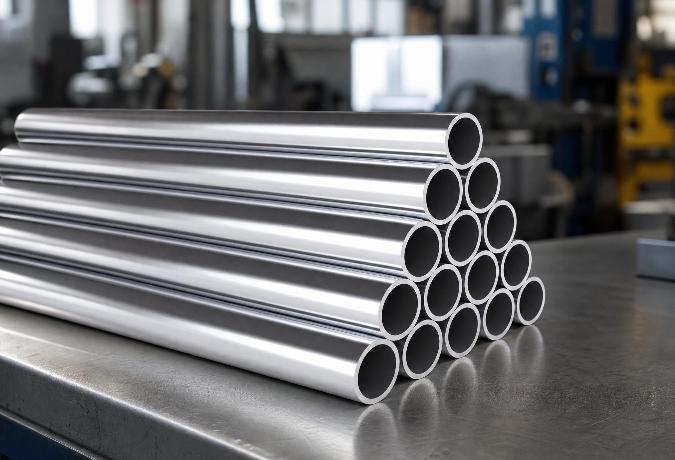
Understanding Aluminium Round Tube Specifications for Structural Engineering
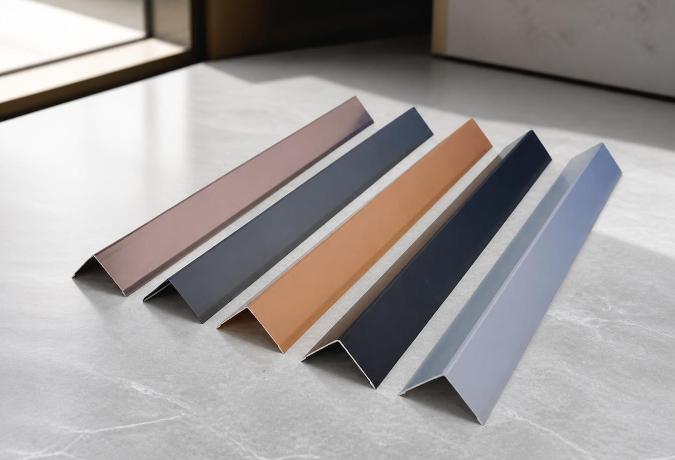
Why the 90-Degree Angle in Standard Aluminium Profiles Determines Structural Reliability
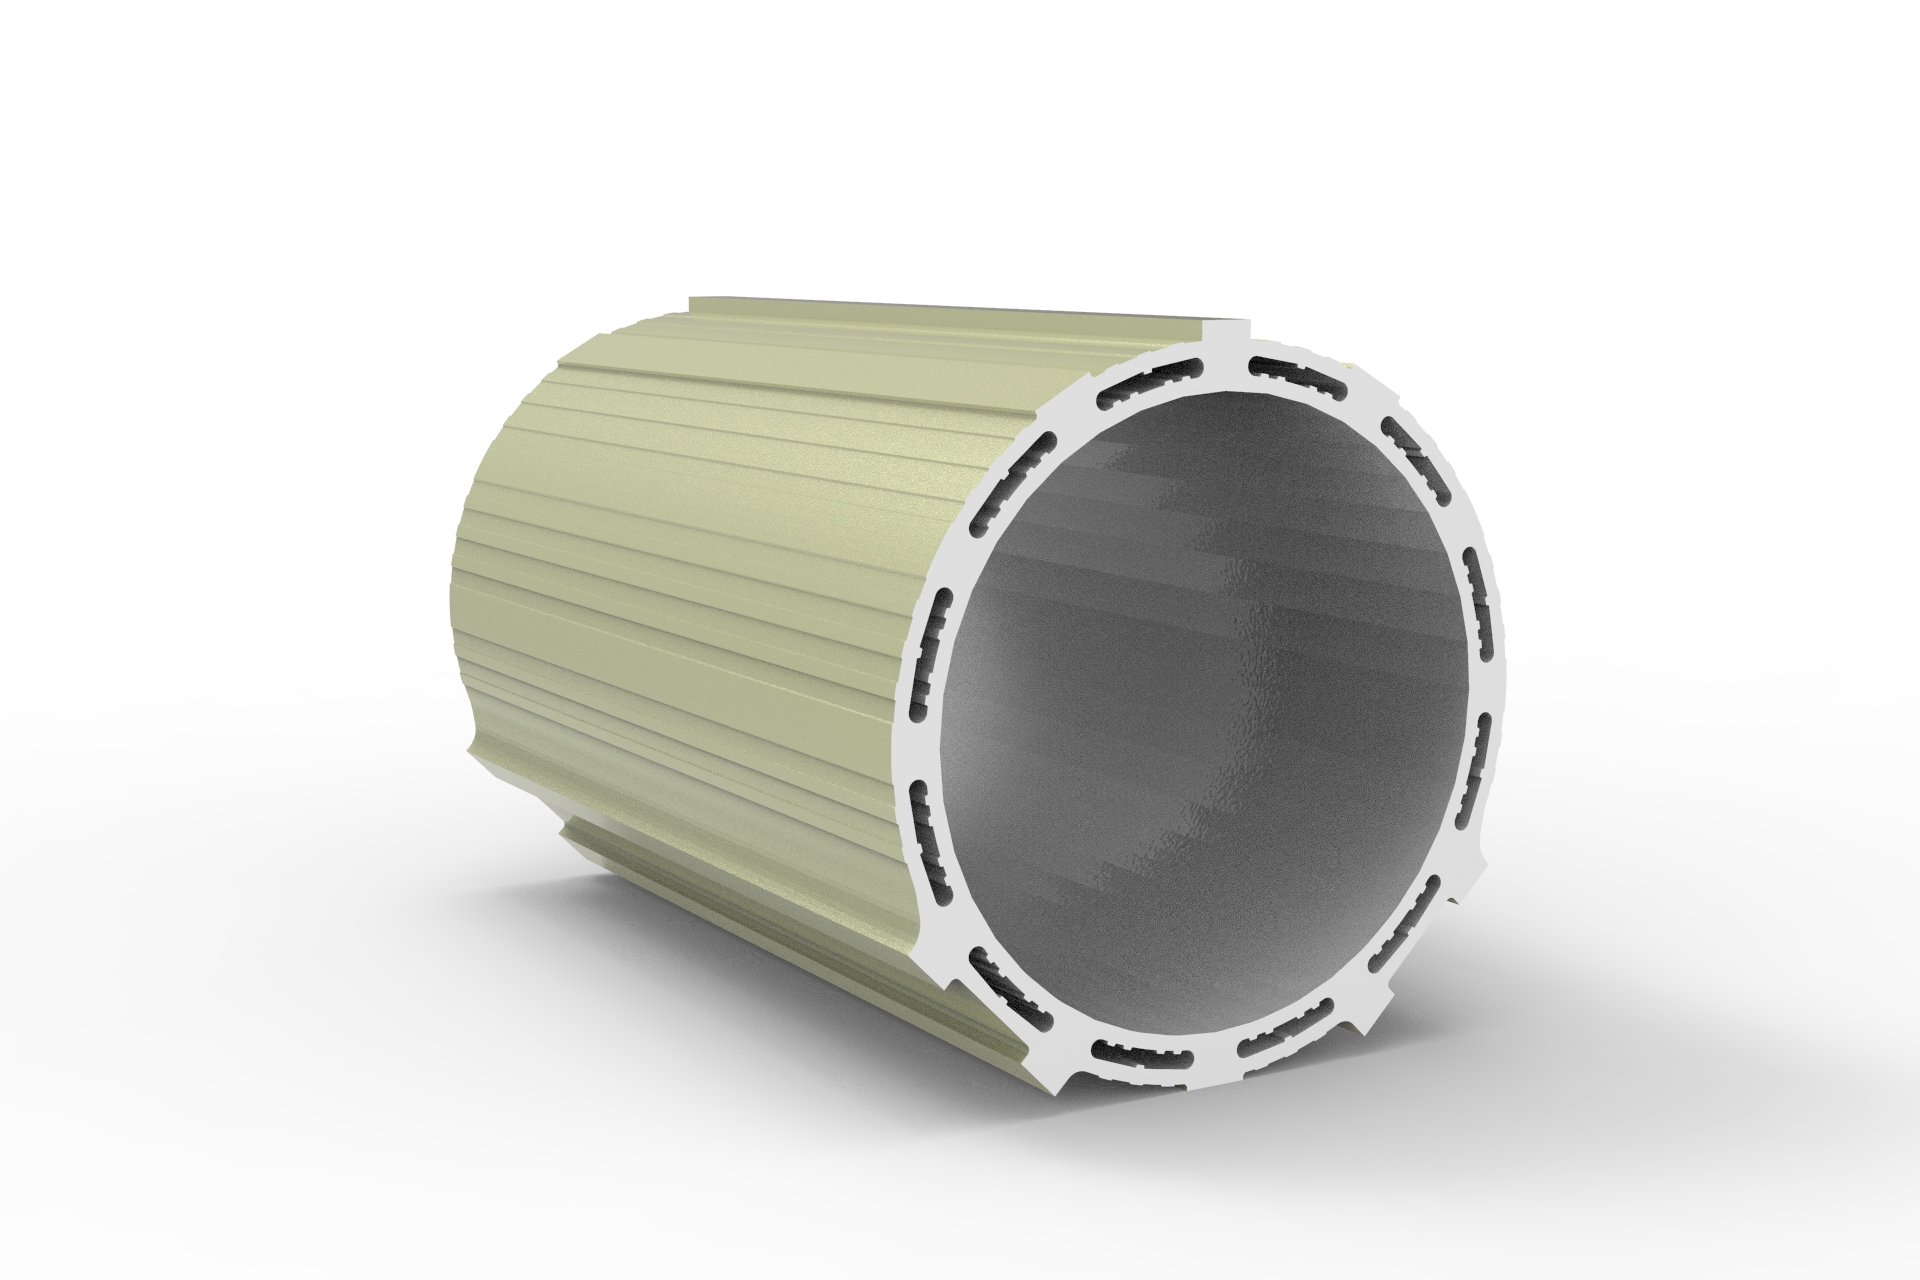
How can I ensure a Floding door sample matches the planned mass production?
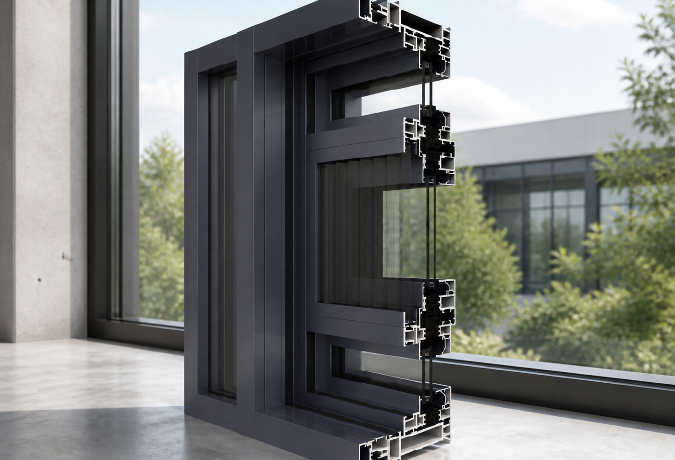
Why Mullion Thickness Determines How Much Glass an Aluminium Curtain Wall Can Actually Hold
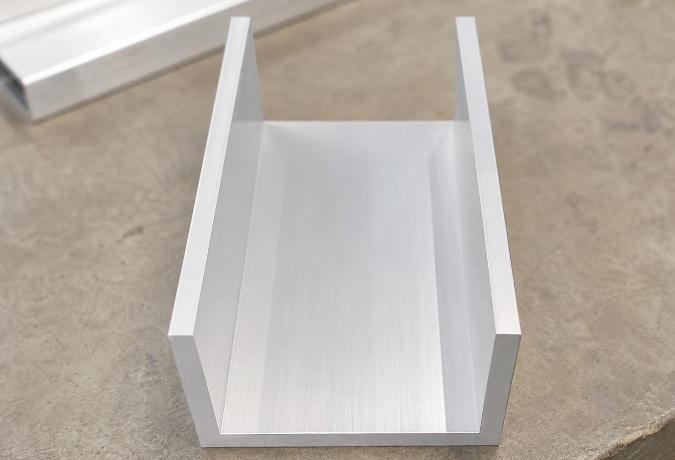
Engineering Dimensional Stability in Aluminium Extrusions for Channel Profiles
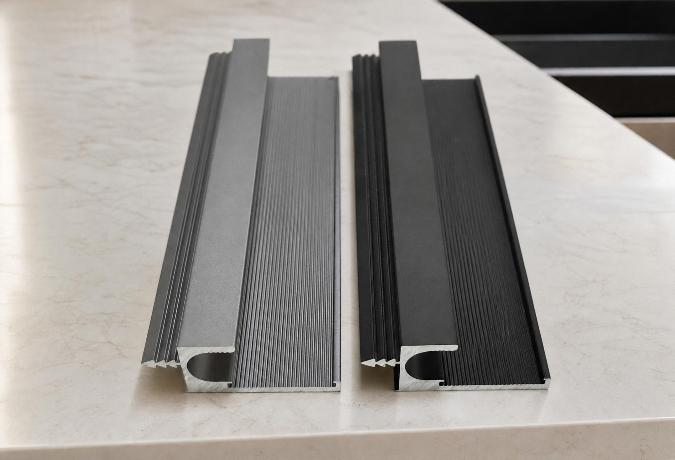
Engineering the Structural Framework: The Mechanics of Aluminium Profiles for Kitchen Cabinets
Choosing an Aluminium Profile Supplier: What Actually Separates the Reliable Ones from the Rest
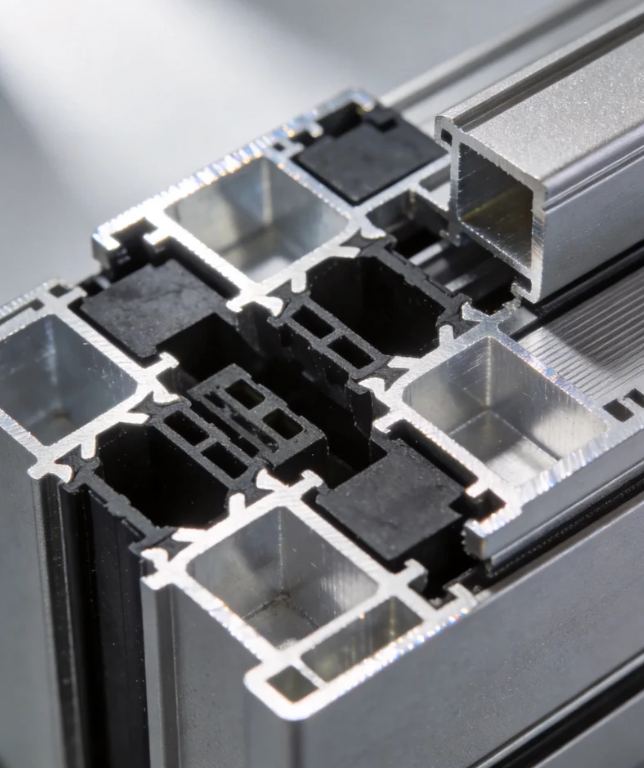
Can Awing window orders ship in batches to avoid project delays?
What response time should I expect for Awing window warranty claims?
Navigating the Supply Chain: Evaluating an Aluminium Profile Manufacturer for B2B Procurement
Engineering Structural Integrity Through Precision L-Shaped Aluminium Profiles
Thermal Dynamics in High-Power Electronics: Engineering Aluminium Heatsink Profiles
Why the T-Slot Design Determines the Real Strength of Structural Aluminium Extrusions
How long should replacement Sliding window parts remain available after purchase?
Should I expect volume discounts when reordering the same Sliding window model?
The Multi-Strip Sealing Structure Inside Aluminium Windows and Doors
Engineering Lightweight Rail Structures Through Extruded Aluminium Profiles
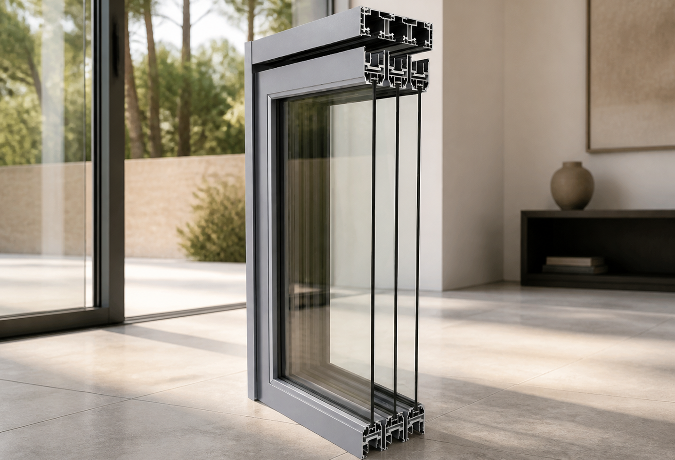
Why the Frame Width on an Aluminium Sliding Door Determines Your Room’s Light
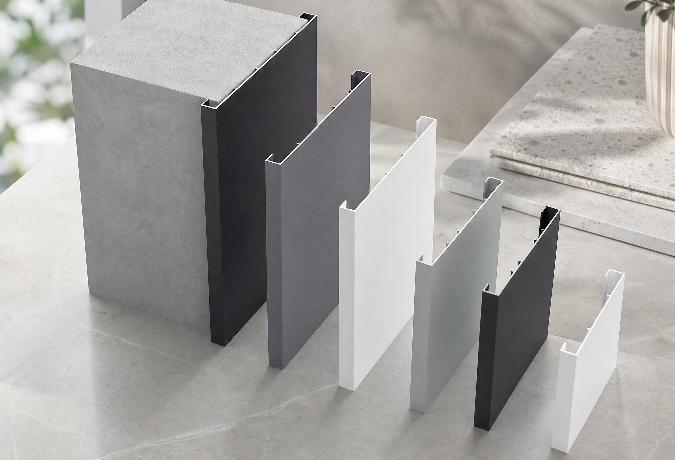
The Engineering Behind Decorative Aluminium Profiles: Alloys, Surface Treatments, and Edge Protectio
What alternative materials could make Casement doors more resilient and recyclable?
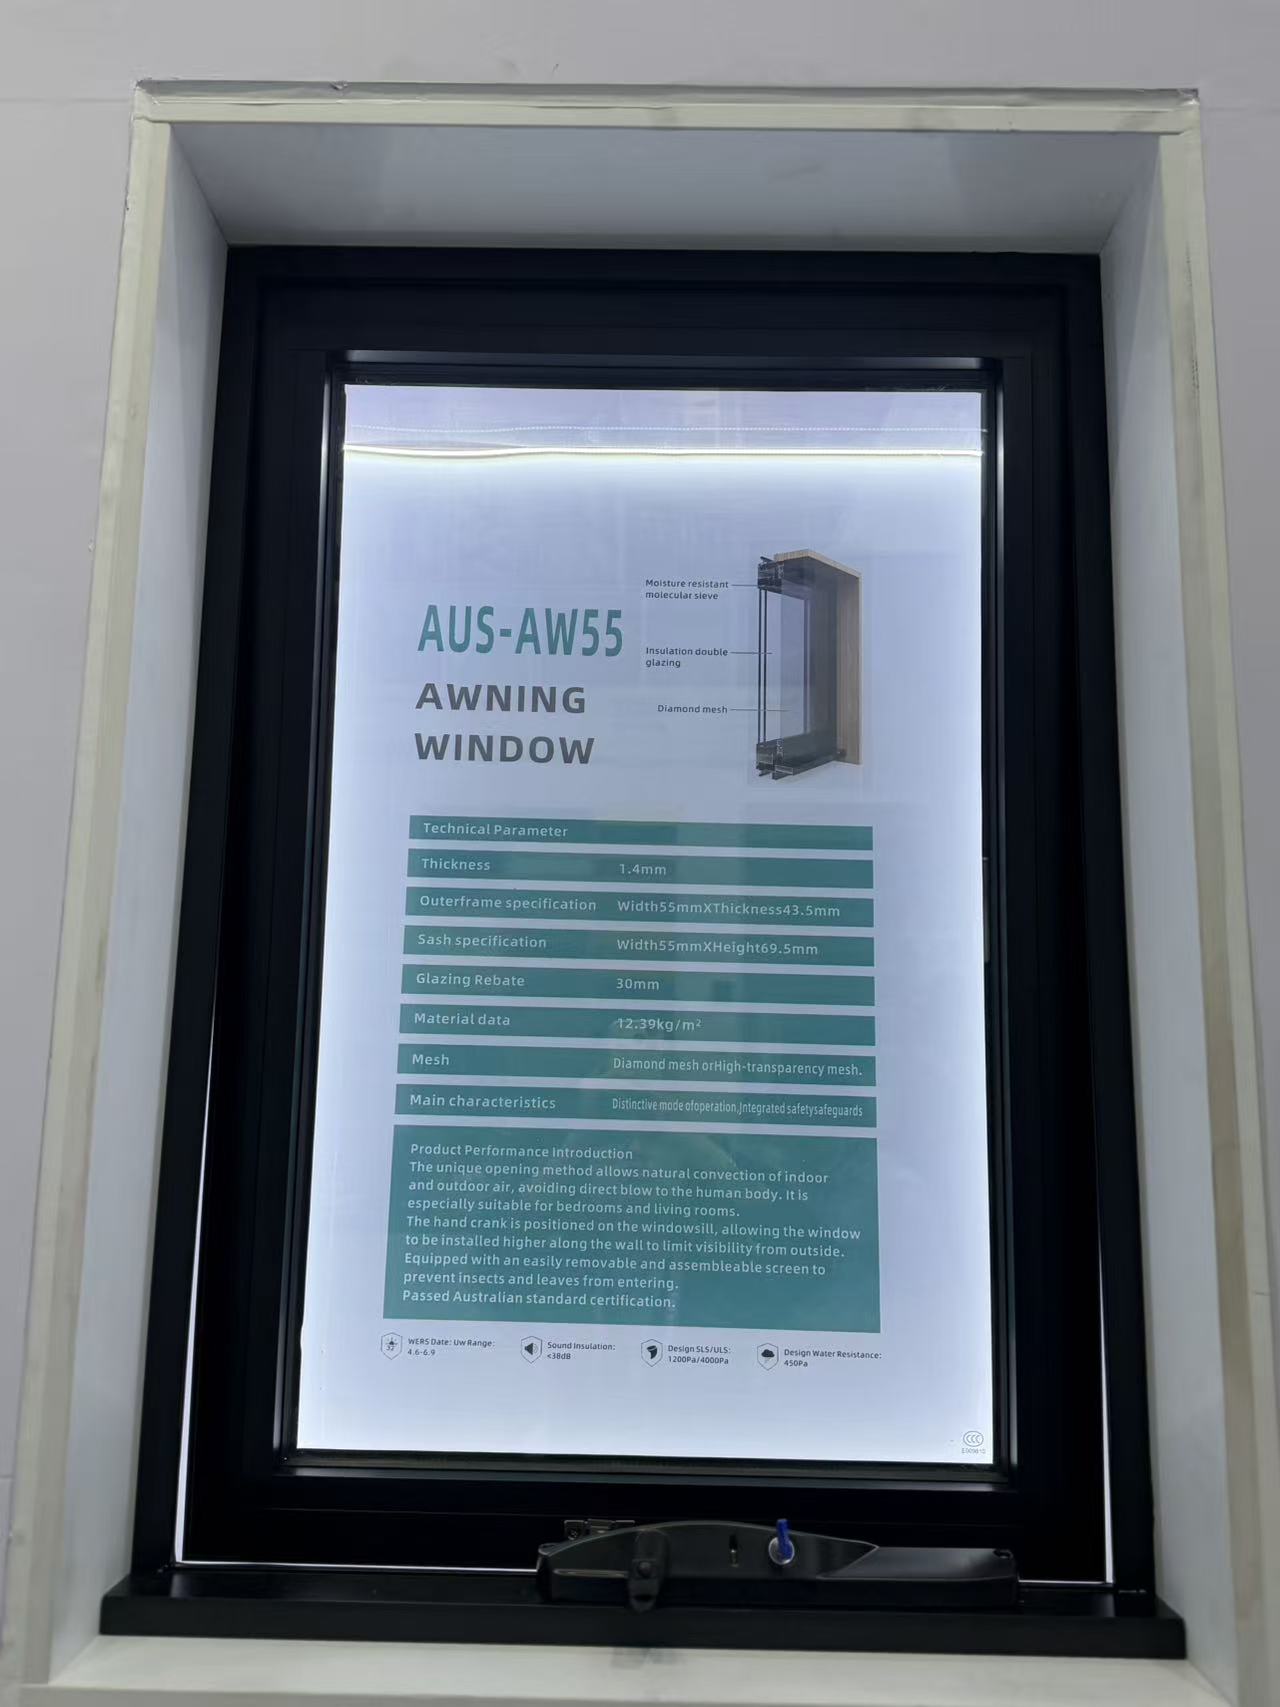
How can I compare Awing window quotes without missing hidden packing costs?
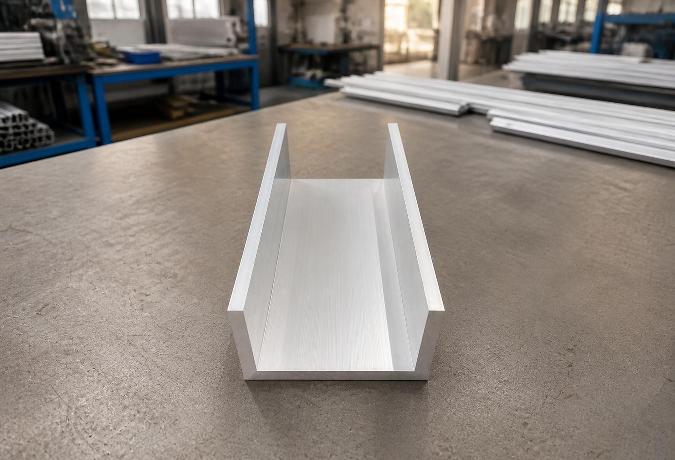
Decoding Structural Tolerances in Aluminium Extrusion Profiles for Channel Applications
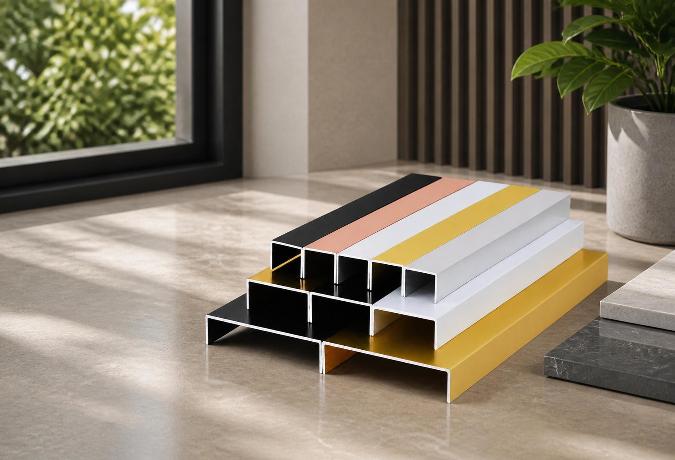
Engineering Tolerances and Alloy Mechanics in Extruded Aluminium Construction Profiles
The Engineering Mechanics Behind Aluminium Angle Profiles in Modern Construction
Can an Industrial profile be modified for my assembly without weakening it?
What warning signs suggest a Sliding door seller may disappear after payment?
What energy-efficient alternatives to Casement doors are worth comparing now?
Can a Casement window handle temperature changes without seal failure?
Who pays for unloading and destination handling under Casement door CIF terms?
Custom Aluminium Extrusion Profiles: The Engineering Mechanics of T-Slot Frameworks
Material Transitions and Geometric Stability in Decorative Aluminium Profiles
Can I negotiate a lower Sliding door MOQ for a showroom launch?
Key Advantages of Using Structural Aluminium Extrusion Profiles in Construction
What evidence shows an Awing window factory manages coating waste properly?
How can I protect my deposit when ordering custom Decorative profile?
How do I spot unusually low Industrial profile prices before committing funds?
How can I check that a Shutter supplier is not using unapproved subcontractors?
What contract terms protect my Casement door drawings and branding?
How can I compare Casement door insulation ratings before placing an order?
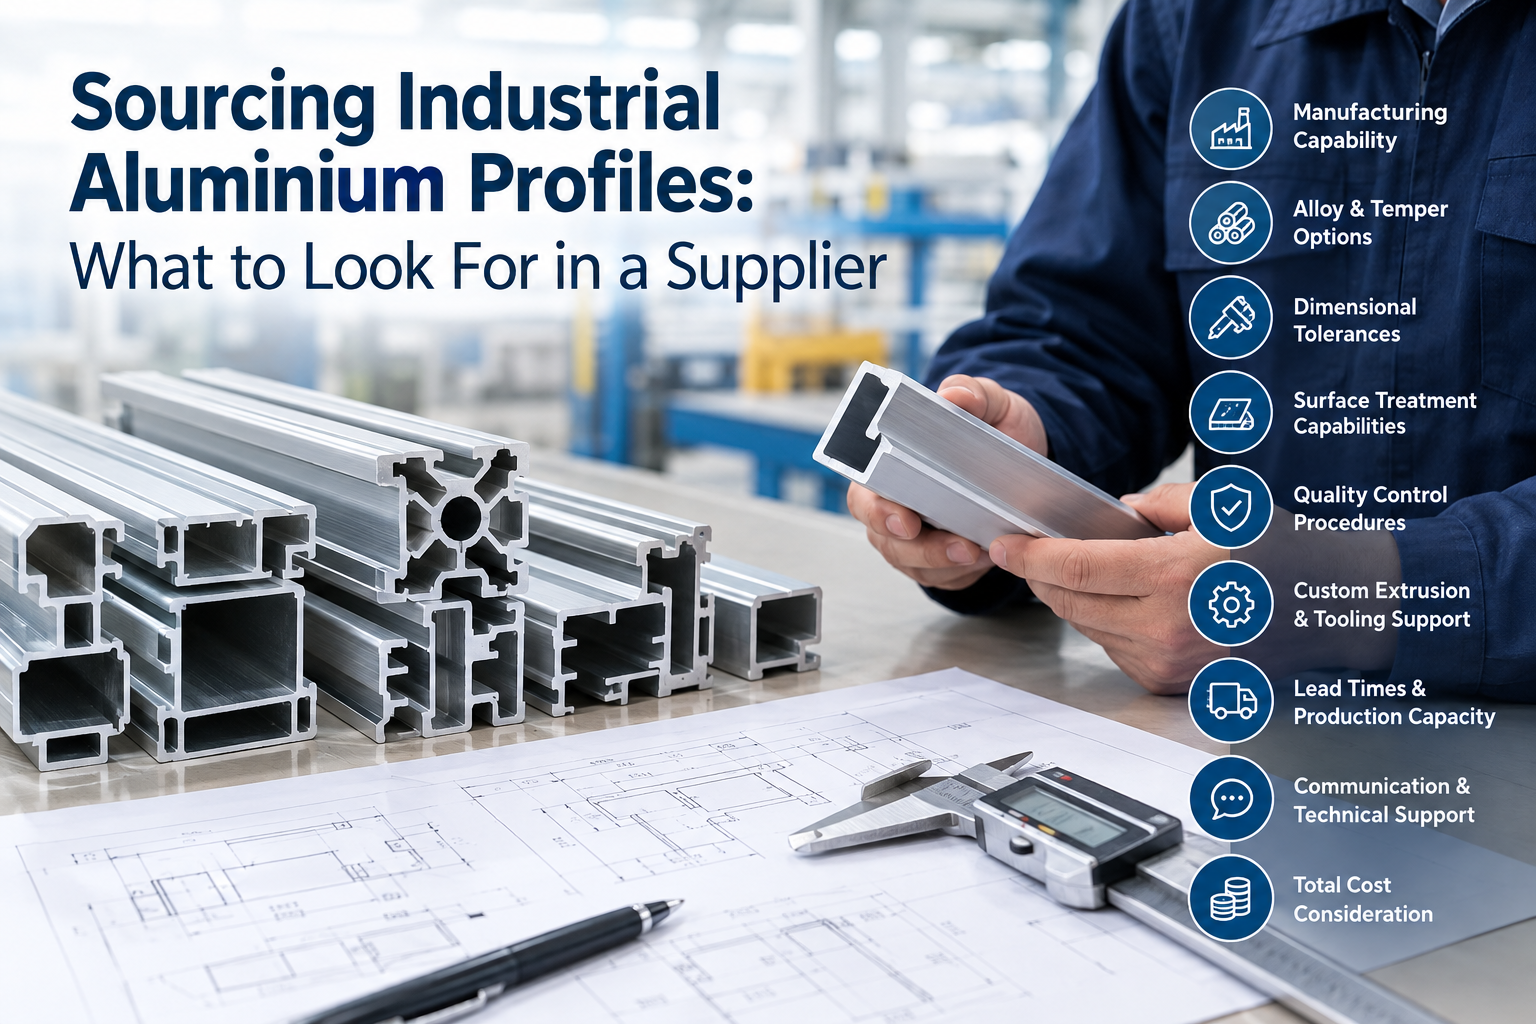
Sourcing Industrial Aluminium Profiles: What to Look For in a Supplier
How do I keep ownership of a custom Architecture profile extrusion die?
The Energy Efficiency Benefits of an Aluminium Frame Sliding Glass Window
How do I check Industrial profile alloy grades against the shipping documents?
What Casement window warranty period is reasonable for an overseas buyer?
How are defective Sliding window units usually replaced internationally?
How can I reduce breakage risks when shipping Casement windows overseas?
The Structural Mechanics Behind Decorative Aluminium Profiles
How Do Engineers Select Industrial Aluminium Profiles for High-Load Frameworks?
What payment structure reduces my risk on a first Industrial profile order?
Should I approve a Casement window sample before checking its hardware strength?
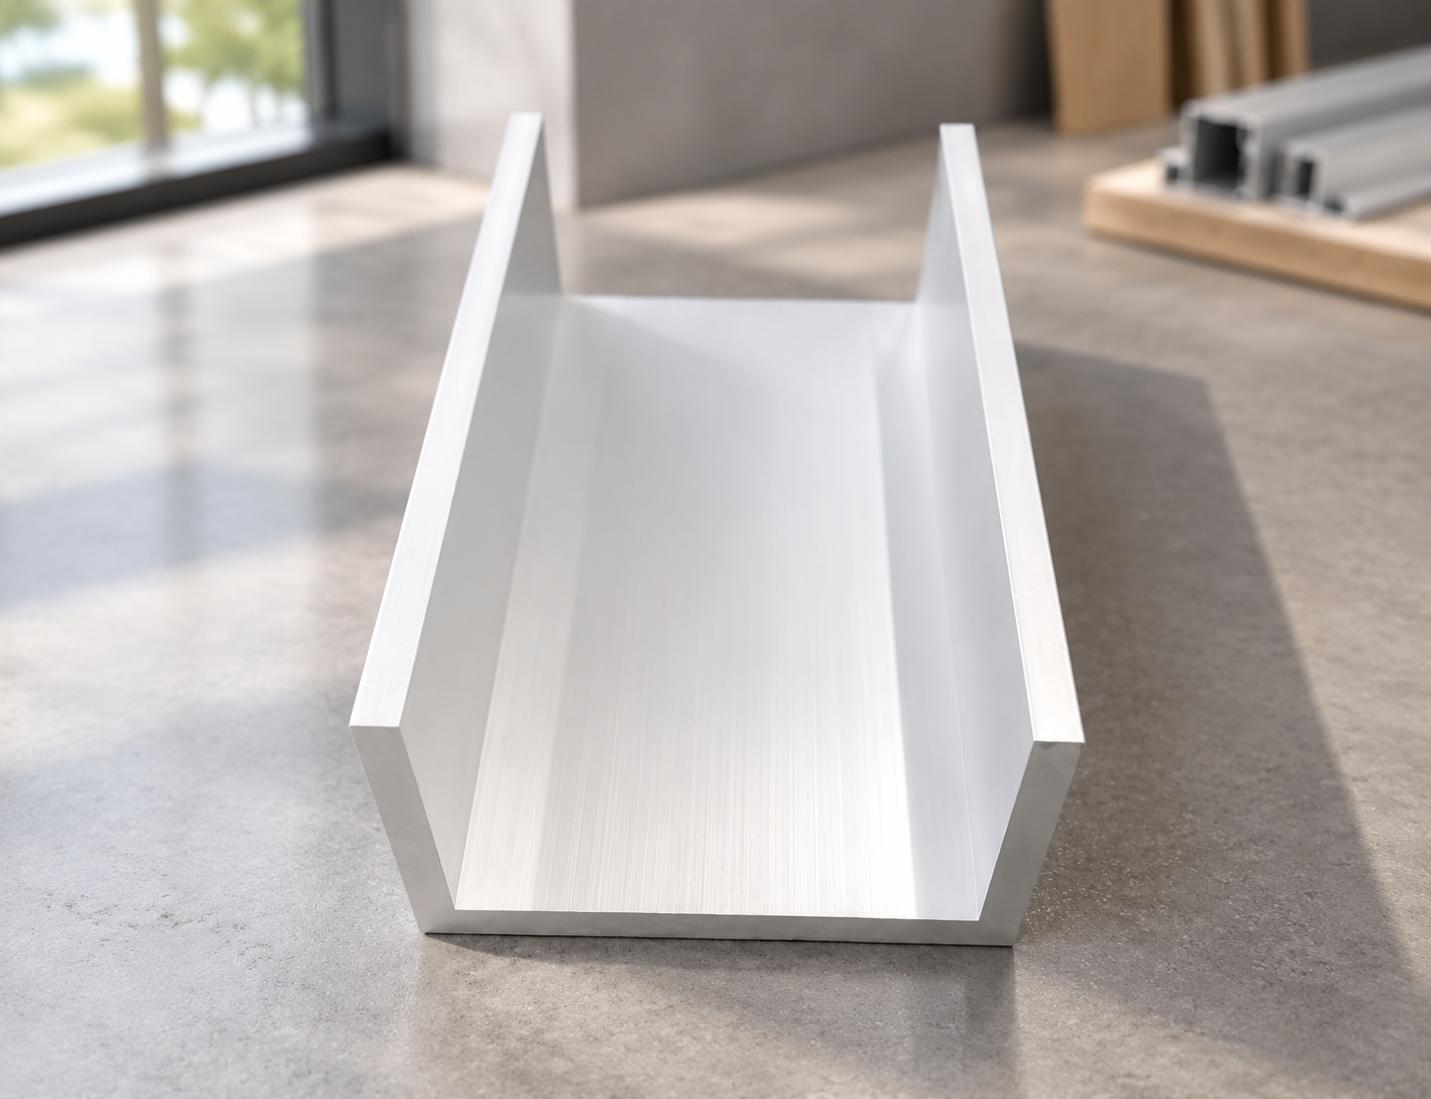
Structural Mechanics of Channel Extrusions in Architectural Aluminium Profiles
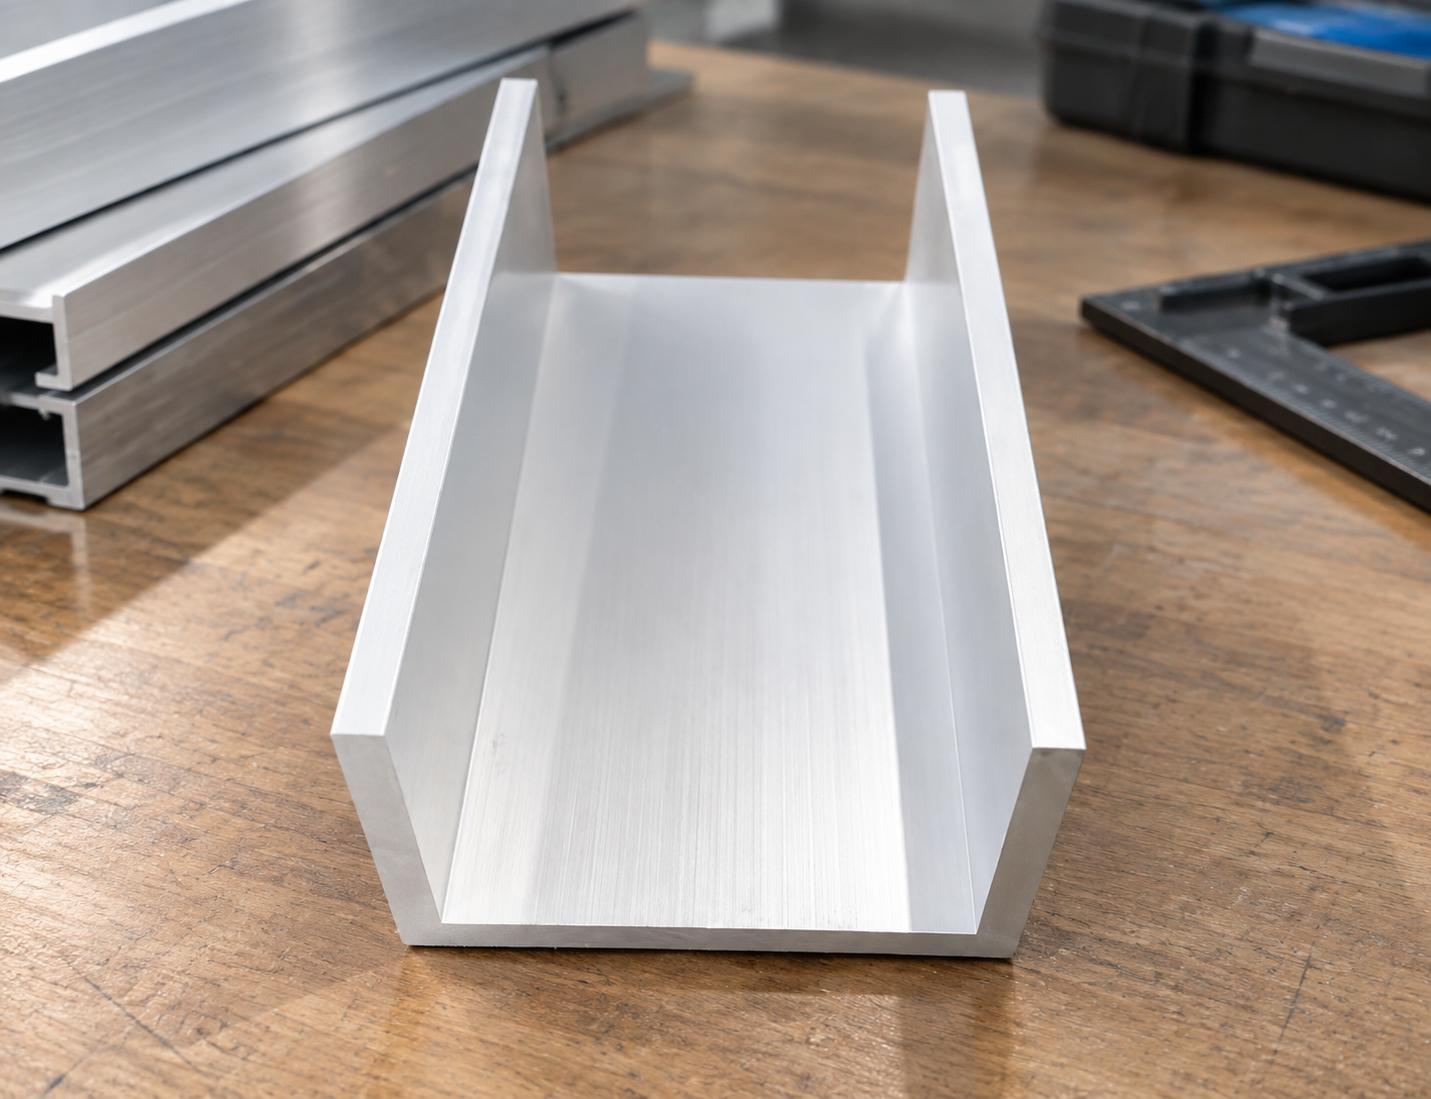
Engineering Mechanics of Aluminium Extrusion Profiles in Channel Systems
What functional tests should I perform on a Sliding door prototype?
What payment terms are fair when Decorative profile colors remain unconfirmed?
Is a letter of credit practical for a large Casement window shipment?
How should Industrial profile bundles be packed to prevent transit damage?
Which safety documents should I request for Awing window imports?
What shipping delays commonly affect Architecture profile orders during peak season?
How to Specify Extruded Aluminium Profiles: Costs, Alloys, and Tolerances
Is a Floding door suitable for a wide opening exposed to strong winds?
Structural Integrity in Modular Design: Engineering T-Slot Aluminium Extrusion Profiles
Resolving Corner Stress: The Engineering Mechanics Behind Aluminium Profiles in Architectural Framin
How do Floding door prices change with glass, hardware, and finish choices?
How can I prove Shutter defects remotely without returning every unit?
How can I shorten Awing window sampling without losing critical tests?
Does ordering mixed Shutter sizes usually change the unit price or MOQ?
How should Industrial profile warranty responsibility be shared after assembly?
How should I plan Shutter inventory when ocean freight schedules change?
How do escrow arrangements reduce risk for a new Floding door supplier?
What frame materials make a Sliding window last in harsh coastal weather?
How can I verify that a Shutter certificate matches the actual product?
Can automated Shutters replace manual systems without raising lifecycle costs?
How do I choose the right Casement window size for a windy building?
What should an ethical audit cover at a Decorative profile factory?
How should I document Industrial profile defects before disputing the final payment?
Are lightweight Industrial profile alloys reliable enough for demanding machinery?
Are thermal-break casement windows becoming a better long-term choice than standard frames?
What is a realistic MOQ for custom sliding windows without pushing up unit cost?
What casement window specs should I compare for windy and rainy project sites?
Are there better material options for sliding windows if aluminum prices rise?
How do I ensure aluminum casement windows can handle extreme coastal winds?
What is the typical minimum order quantity for commercial sliding windows?
Are there energy-saving alternatives to sliding windows that reduce material and maintenance costs?
Are energy-efficient Awing windows a practical alternative for reducing long-term building costs?
What alternatives to traditional sliding doors can lower costs without sacrificing durability?
What alternatives to industrial profiles can reduce material costs without hurting strength?
Extruded Aluminium Profiles: Flexible Manufacturing for Diverse Customer Needs
Why Aluminium Curtain Walls Are Popular in Modern Architecture
How do I choose a decorative profile that stays stable in humid or harsh environments?
How do I choose an architecture profile that stays stable in harsh outdoor conditions?
How can I compare Awing window specs to avoid poor performance in harsh weather?
How can I compare Sliding door sizes and hardware ratings for harsh commercial environments?
How do I choose the right shutter specifications for harsh climates without overpaying?
What eco-friendly alternatives to folding doors can cut costs without hurting durability?
How do I choose the right shutter specifications for harsh weather without overpaying?
What eco-friendly casement door materials can lower costs without hurting durability?
What newer materials can replace industrial profiles without raising costs or supply risks?
How do I choose a decorative profile that stays stable in humid, high-traffic spaces?
What sustainable material alternatives can replace aluminum architecture profiles?
What should I check in Awing window specs to ensure reliable performance in harsh weather?
How can I compare Sliding door sizes and thermal ratings for harsh climates before buying?
What newer materials can replace aluminum in awning windows without raising our costs?
How do I choose the right Sliding door specs for smooth operation in harsh environments?
How do I choose a folding door that stays stable in harsh weather and heavy daily use?
How can I choose the right shutter specifications for harsh weather and long-term use?
How do I compare casement door U-values, hardware, and weather sealing before buying?
How do I choose the right industrial profile size for strength and load needs?
How do I choose the right shutter specifications for harsh weather and long-term commercial use?
How do I choose the right Casement door size and hardware for harsh weather?
What greener alternatives to decorative profile can cut costs without hurting durability?
What lower-cost, eco-friendly materials can replace decorative profiles?
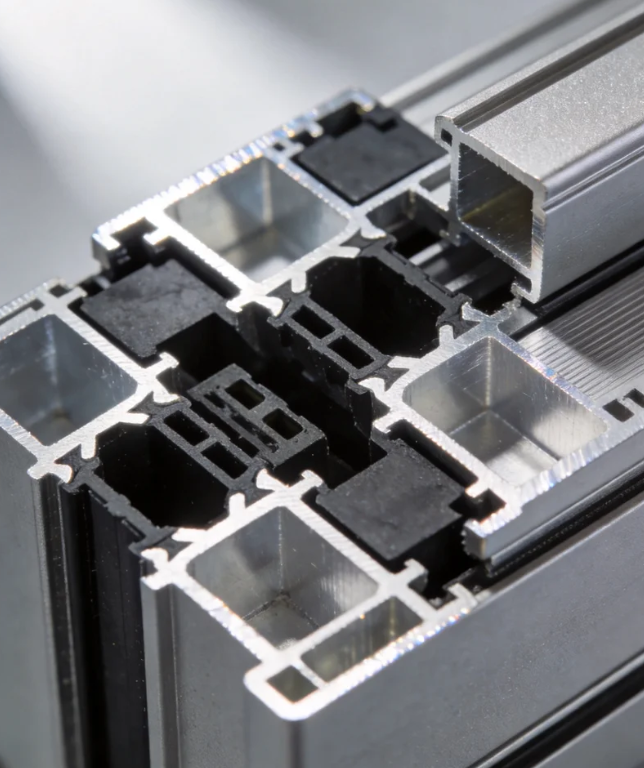
What lower-carbon alternatives to aluminum architecture profiles are practical for our project?
How can I compare sliding door systems for insulation, security, and long-term use?
What is the standard production lead time for bulk orders of folding doors?
How do I choose the right Awing window size and glass specification for harsh weather?
How can I test shutter samples so the final bulk order matches their quality and finish?
Can suppliers make custom double glass casement doors from my CAD drawings?
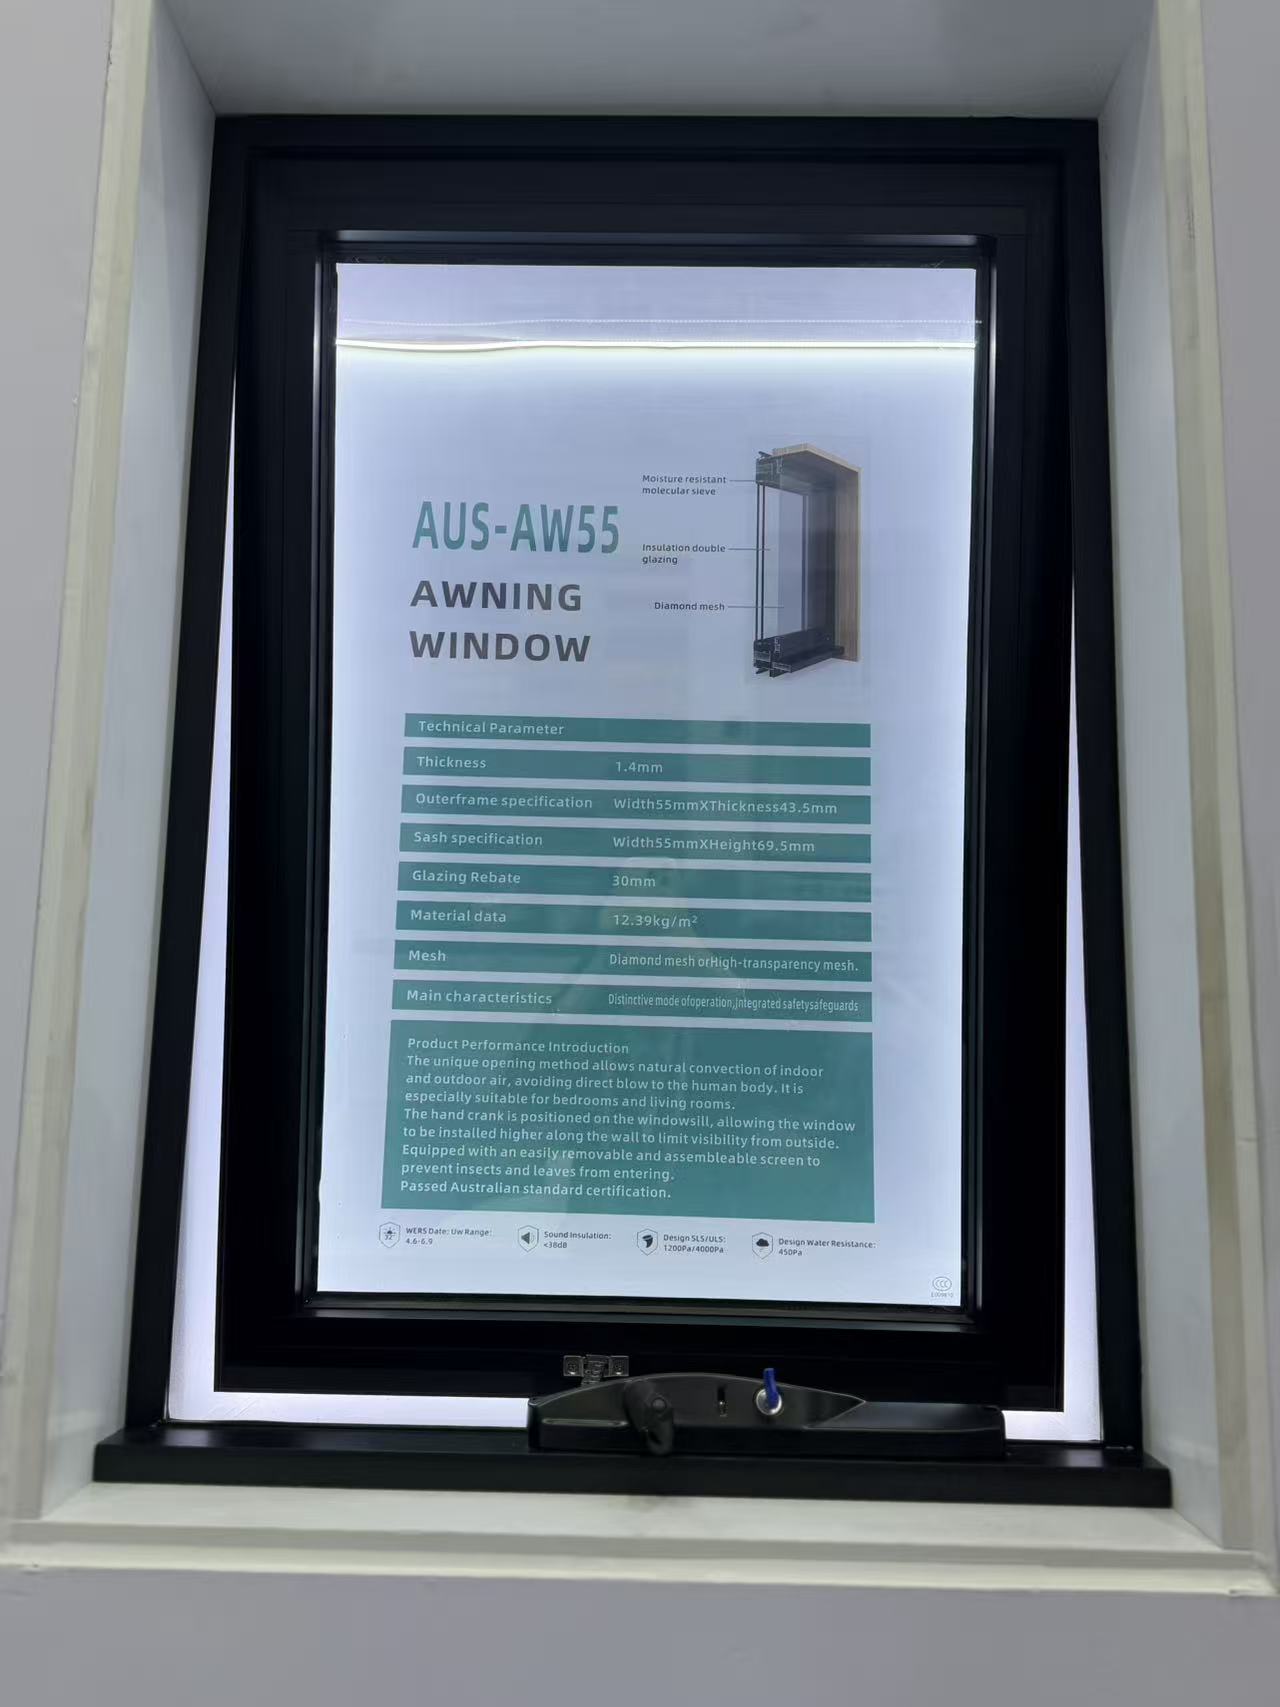
What safety certifications should I request when importing awning windows?
How long does it usually take a factory to make custom shutter samples?
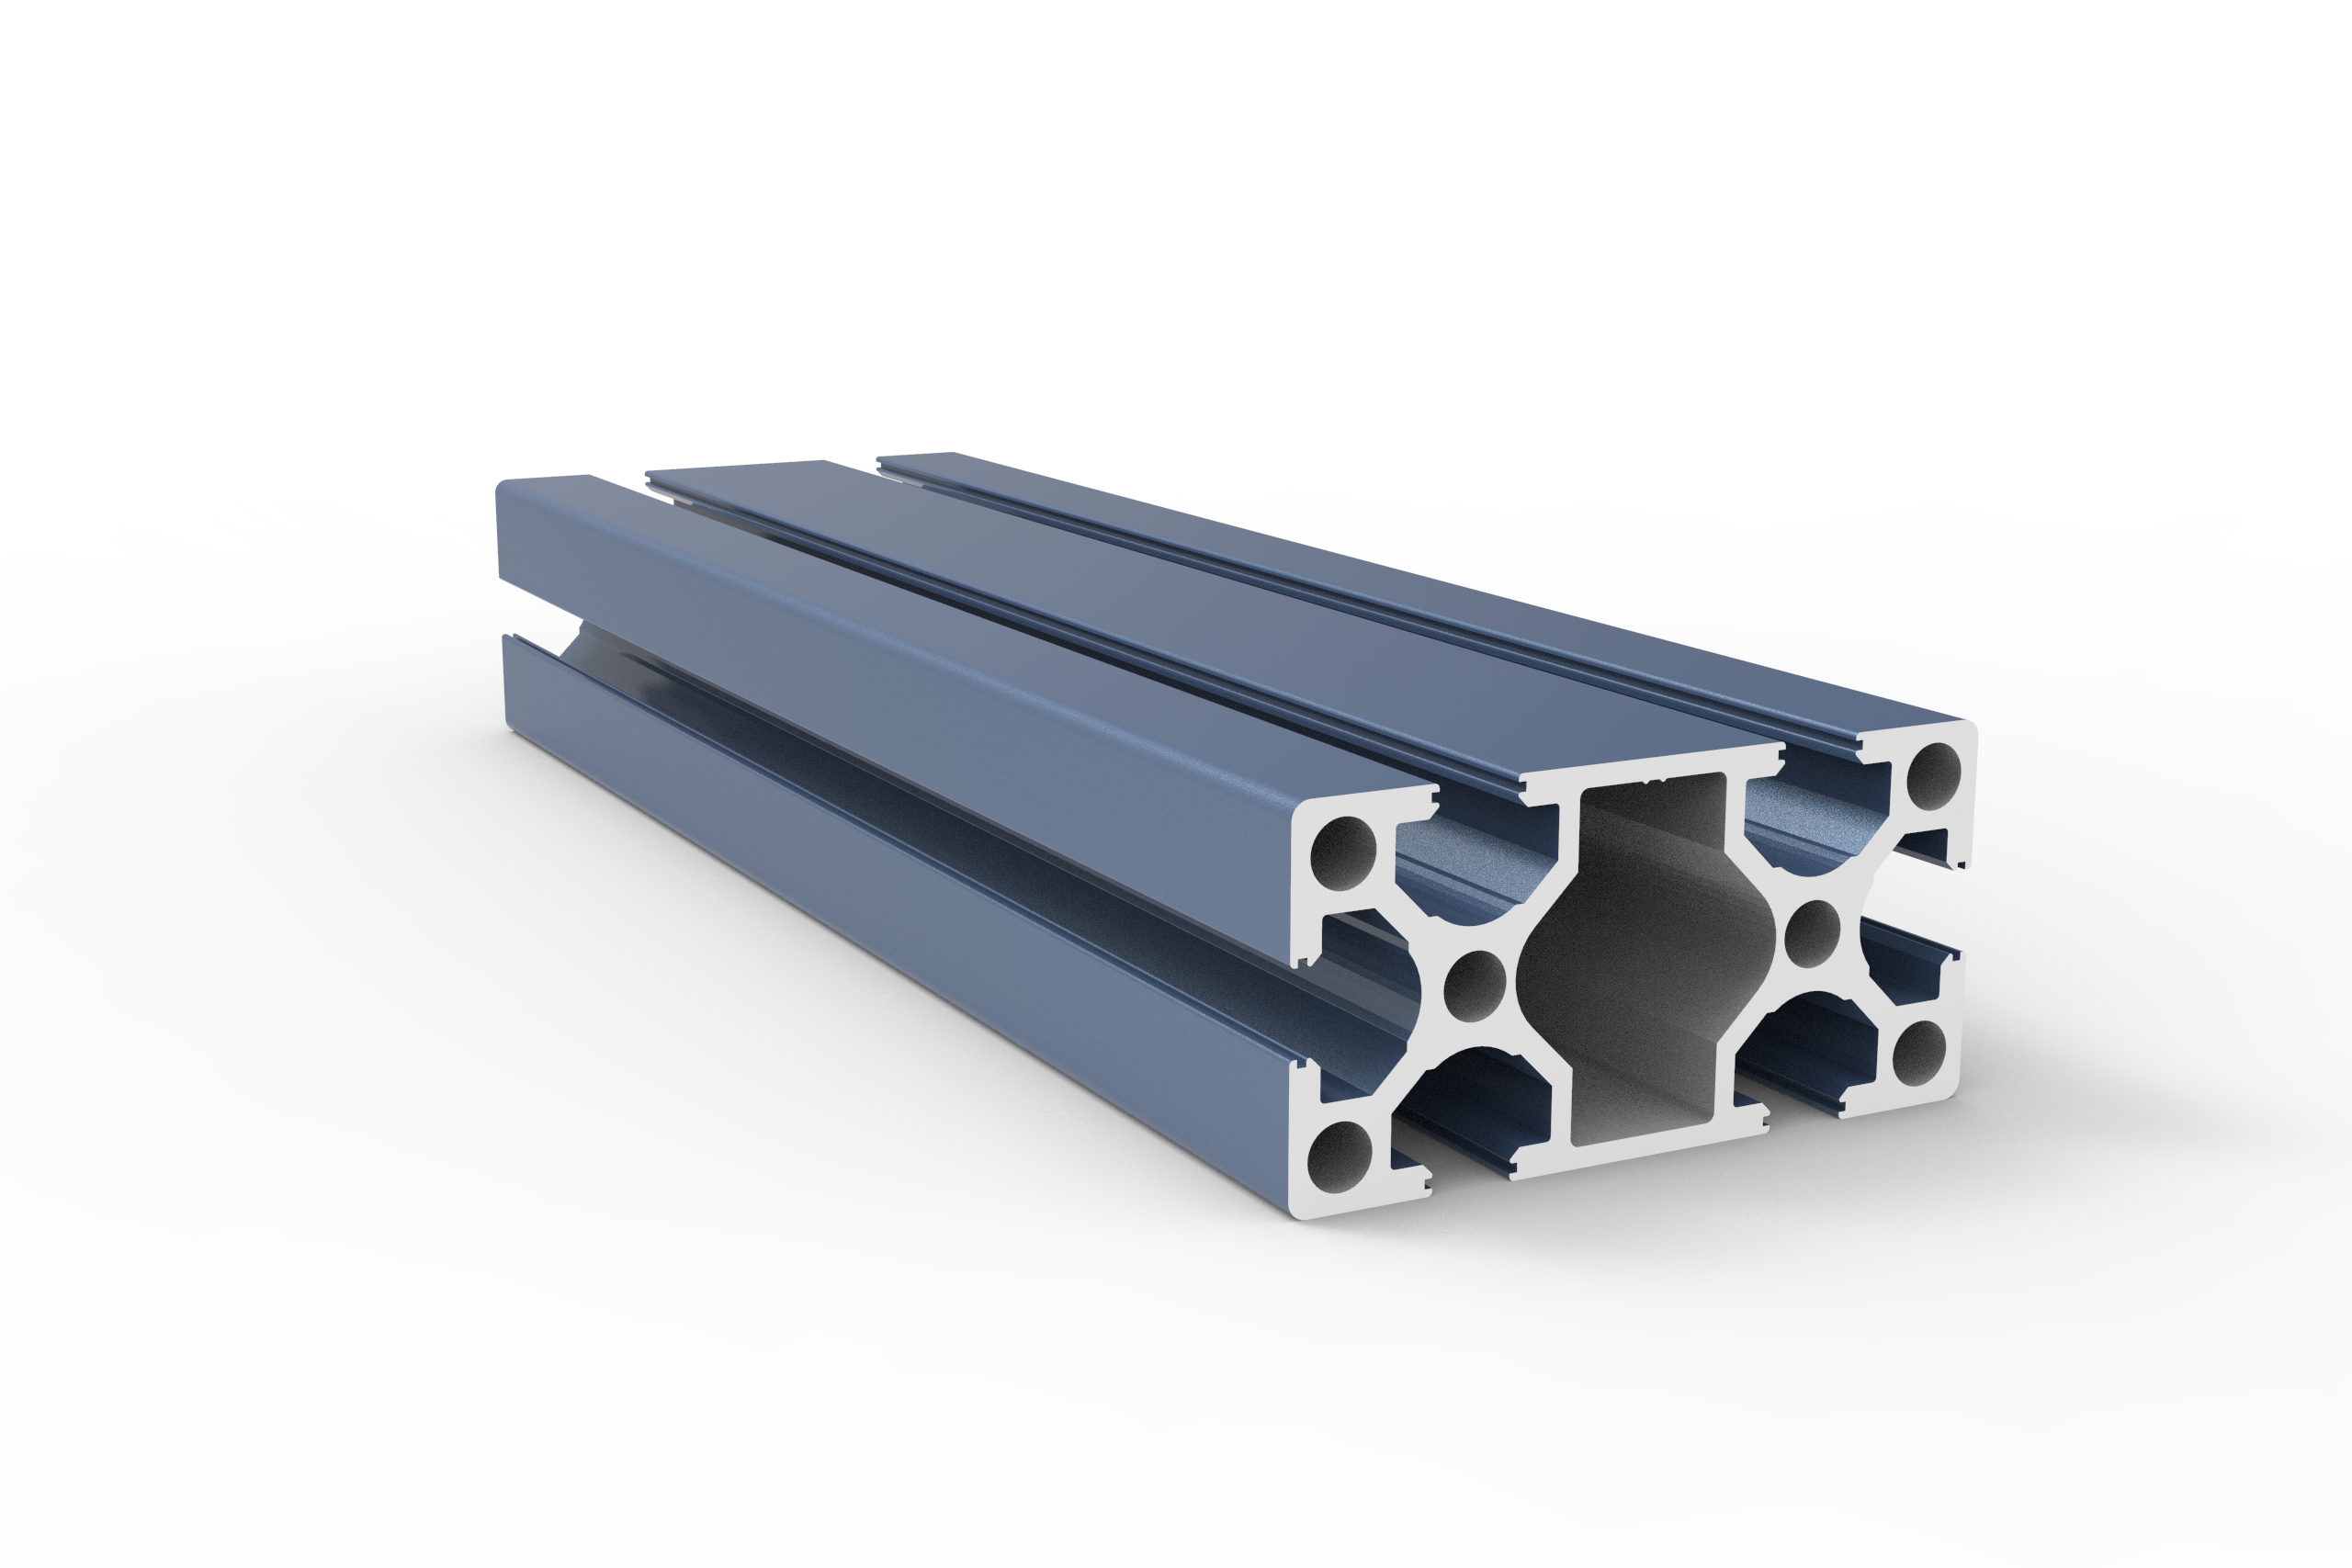
What T-slot industrial profile size is best for a heavy duty machine frame?
How do I choose the right stainless steel decorative profile for high humidity areas?
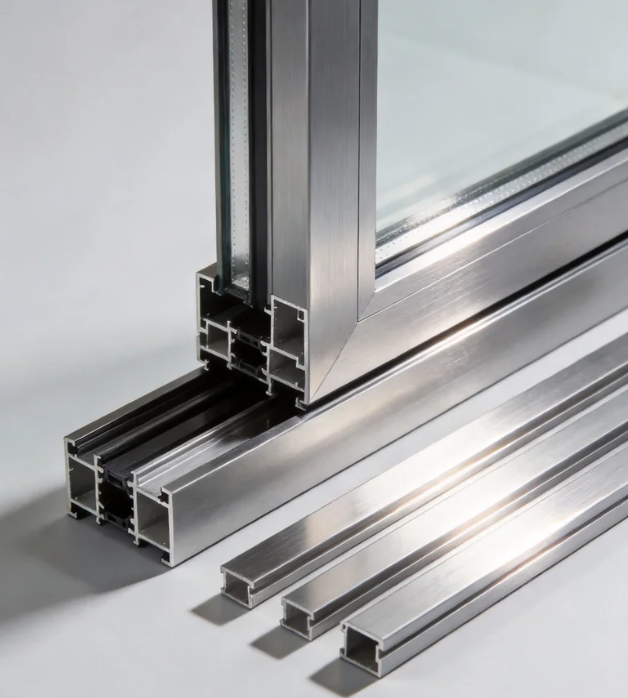
How do I choose the right aluminum architecture profile for coastal buildings?
How do I choose the right stainless steel decorative profile for high humidity areas?
What wind load specs should I check for aluminum casement windows in coastal high-rises?
How do I know which aluminum industrial profile alloy is best for heavy machinery frames?
How do I choose the right alloy grade for aluminum architecture profiles?
How do I select the right heavy-duty hardware for exterior commercial floding doors?
How do I select the right glass thickness for bulk awing window orders?
What frame thickness is recommended for commercial aluminum casement doors?
What frame thickness is best for high-rise commercial sliding windows?
How to choose weather resistant aluminum floding door specs for commercial use?
How do I choose the best water tightness rating for commercial awing windows?
How do I choose the right frame material for commercial casement doors?
How do I choose the right wind load rating for sliding windows in coastal areas?
What is the best material for outdoor decorative profiles to prevent rust and fading?
How do I choose the right track thickness for high-traffic commercial sliding doors?
How do I choose between PVC and basswood shutters for high-humidity areas?
How do I choose between double and triple glazing for casement windows in cold climates?
How do I choose the right industrial profile thickness for heavy-duty cnc machine frames?
How do I choose the right alloy for outdoor architecture profiles to prevent corrosion?
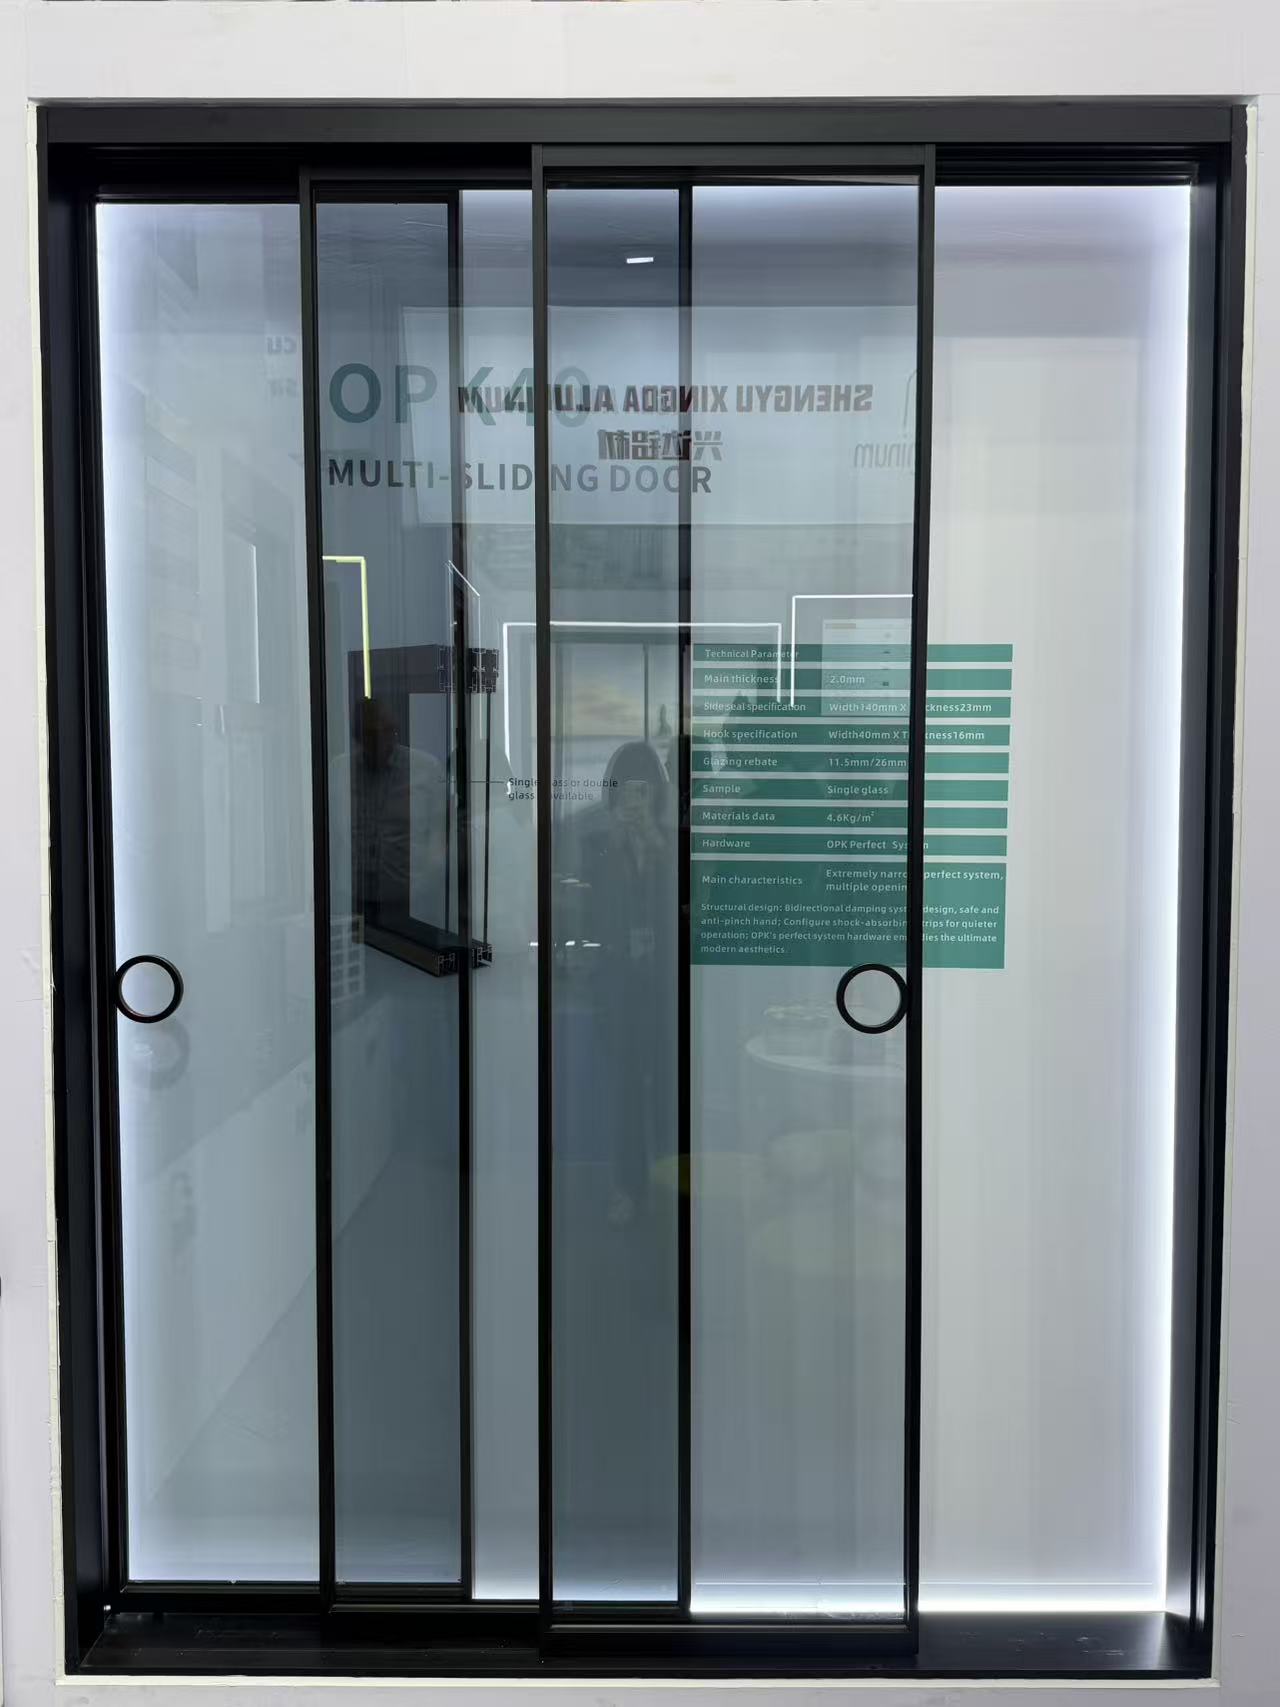
Can you design a slim frame profile for modern minimalist look?
How do I choose the right wind-resistant floding door for a coastal commercial building?
What key specs ensure a casement window can withstand heavy rain and high winds?
How do I choose the right aluminum alloy grade for heavy-duty industrial profiles?
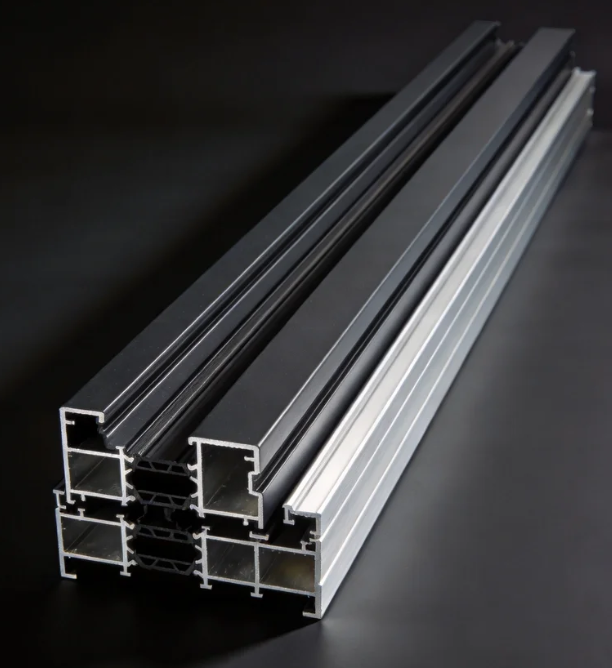
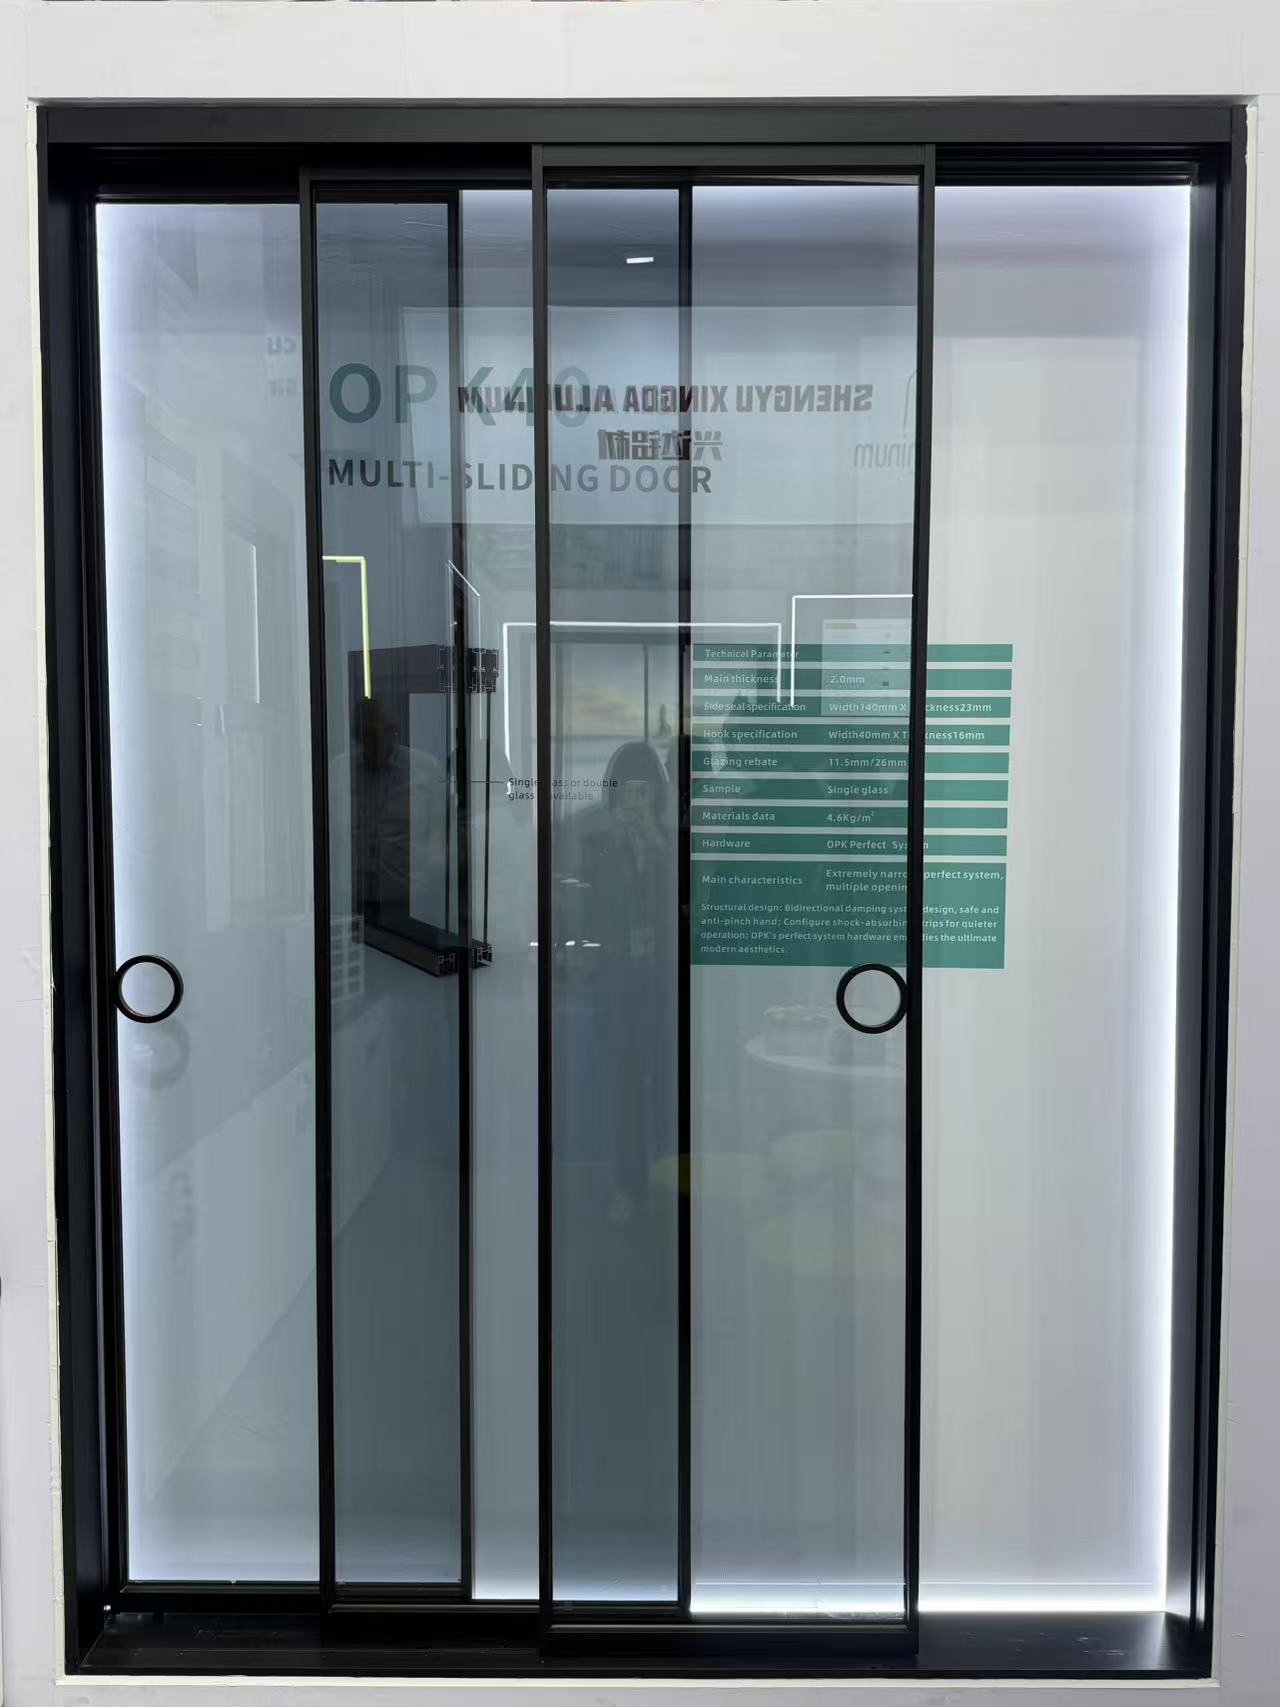
Which alloy grade of architecture profile is best for coastal areas to resist rust?
How do you pack windows to prevent glass breakage in transit?
Are slim-frame thermal break systems replacing traditional ones?
Does the price include the matching frame and installation kit?
How do you protect our proprietary design drawings from leaks?
How do I choose the right decorative profile for high-traffic hotel lobbies?
Is your factory the actual manufacturer or a trading partner?
Is it possible to 3D print a prototype before cutting steel?
Do you outsource any part of the painting process to others?
How do you handle replacement parts for damaged track rollers?
Do you accept escrow payments through third-party platforms?
Do you have ISO 9001 certification for your production line?
Are there extra fees if we pay via bank telegraphic transfer?
What is the price difference between powder coat and anodized?
What is the warranty period for the lock and hinge hardware?
What is your policy for dimensional deviations in the batch?
What happens if the shipment is delayed due to factory error?
Do you offer online technical support if color fading occurs?
Is it possible to engrave our brand logo on the tension screw?
Do you offer credit terms for long-term purchasing partners?
Can you palletize the shipments for easy forklift unloading?
What are the latest eco-friendly finish trends for decorative profiles in modern interior design?
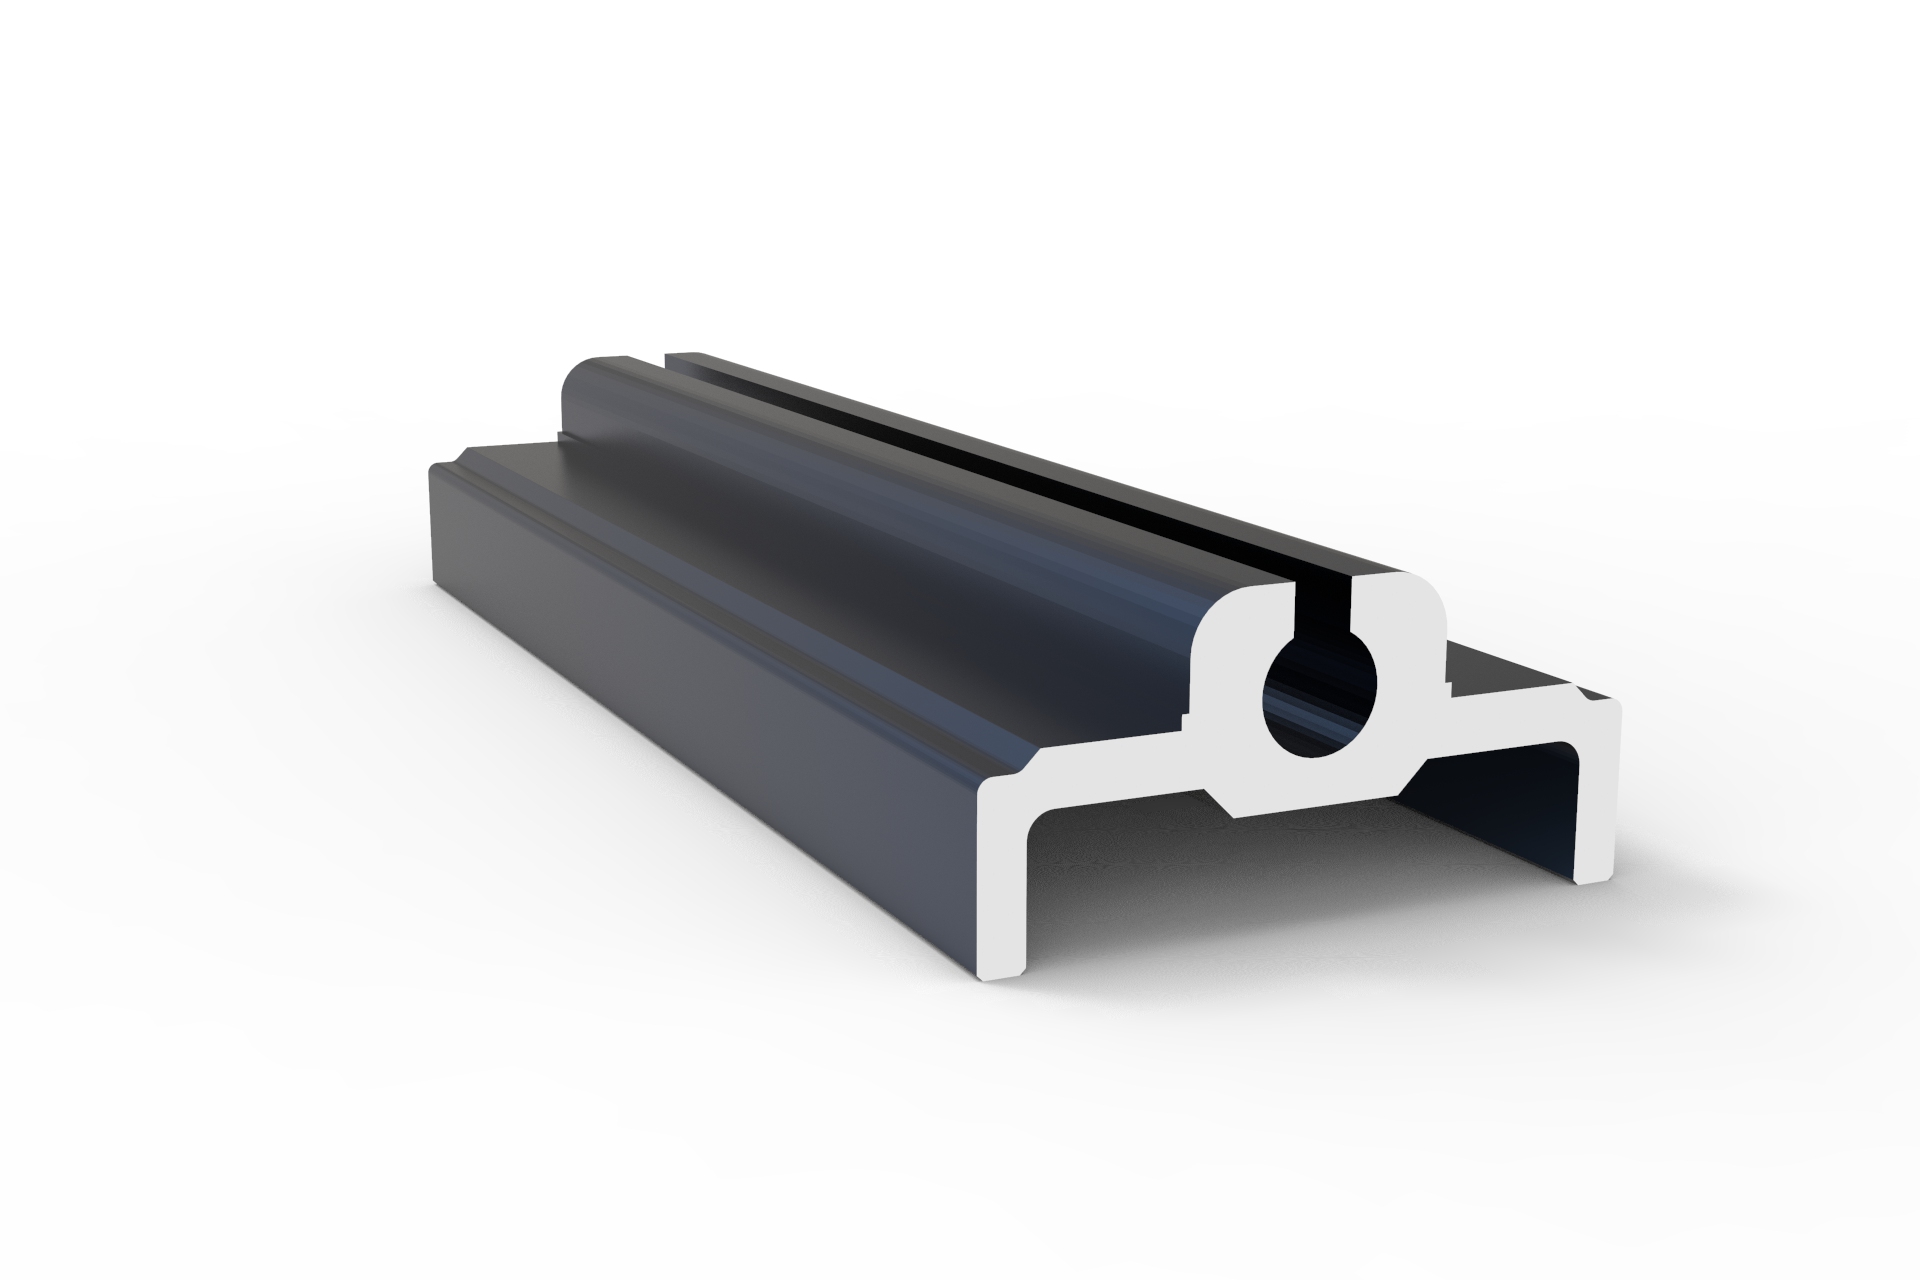
What are the tooling cost and design limitations for customizing heavy-duty industrial profiles?
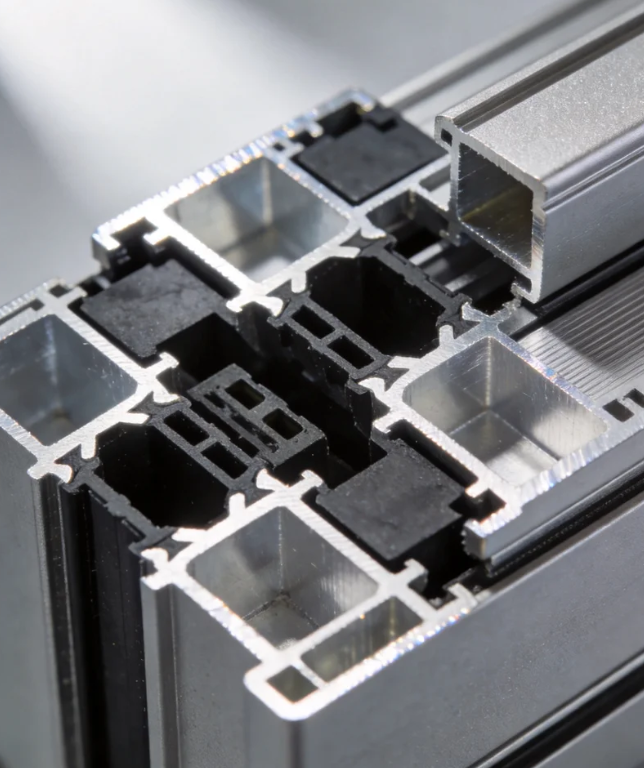
Has your architecture profile manufacturing facility passed ISO 9001 certification?
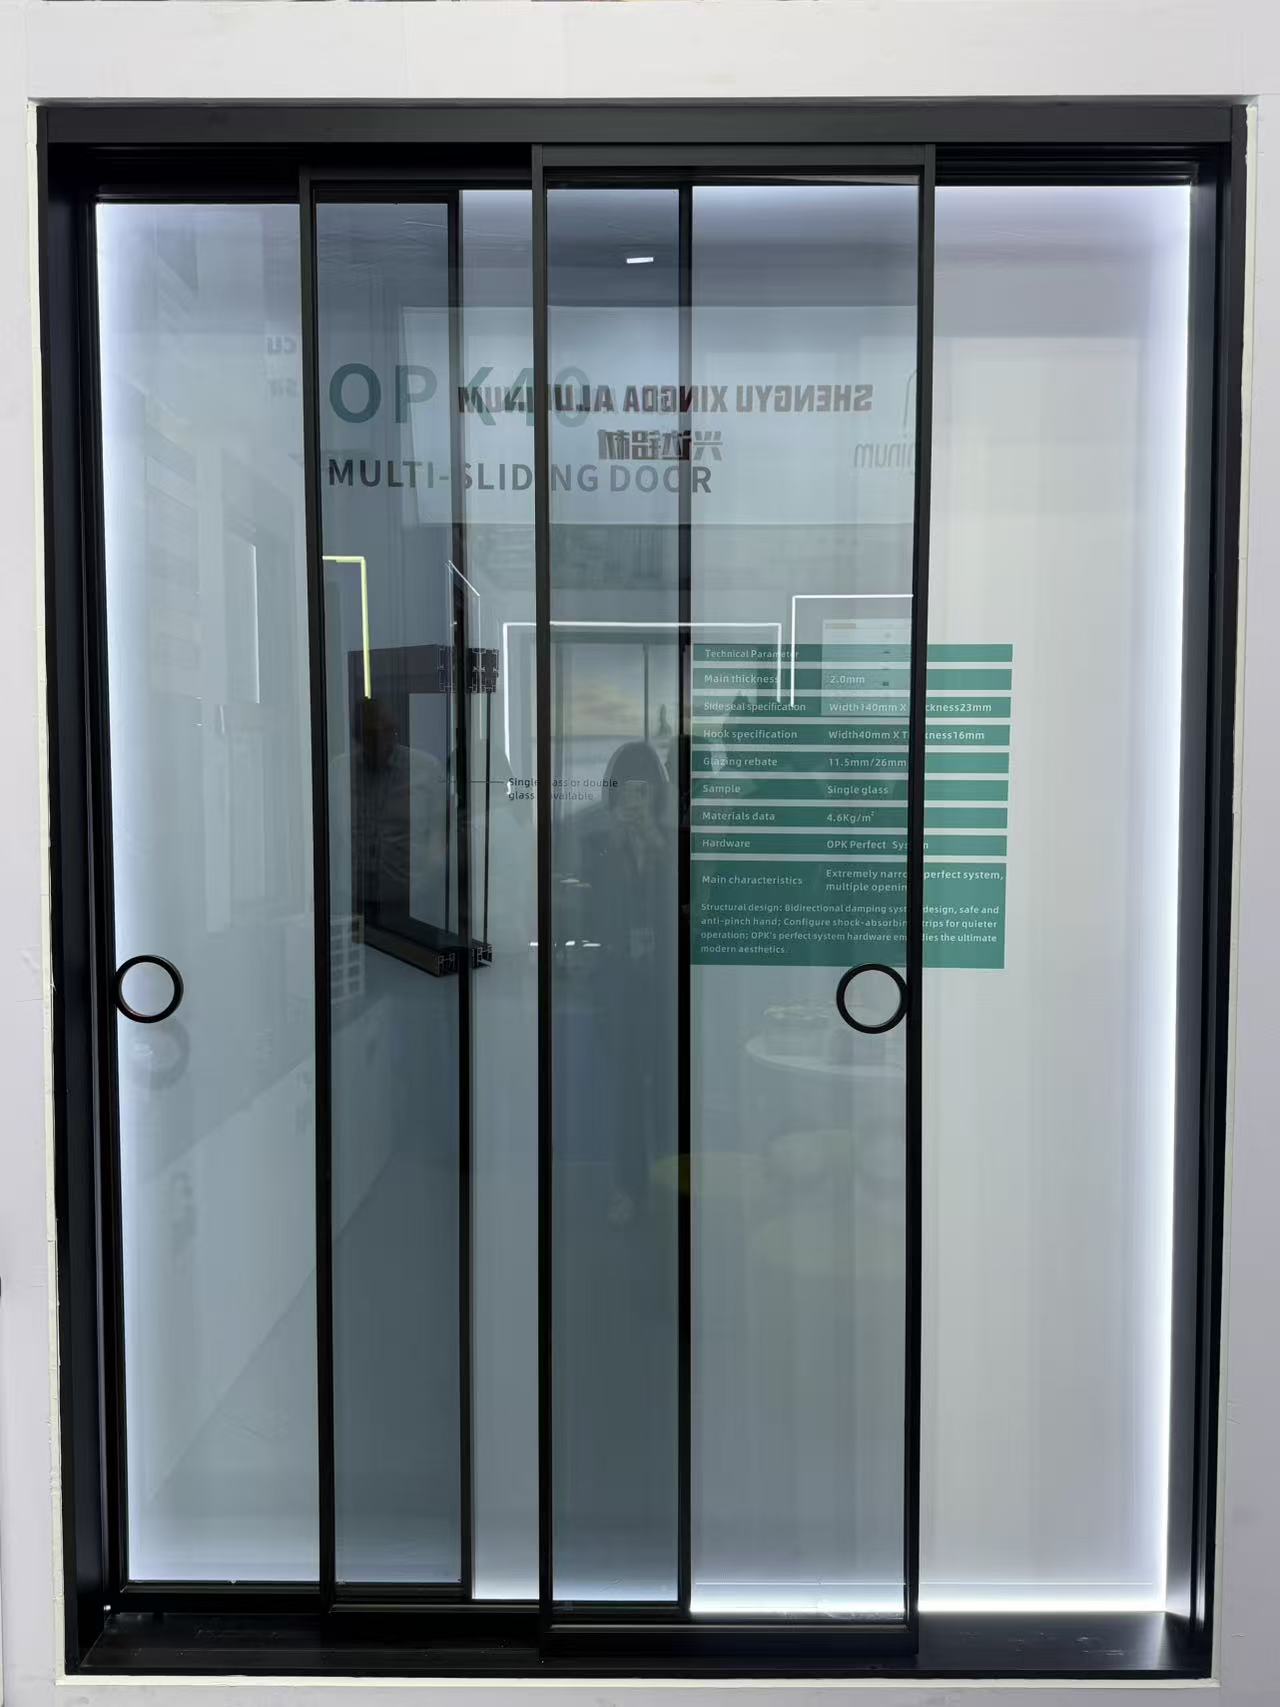
Can we use Alibaba Trade Assurance for our initial sliding door order to mitigate risk?
Do you provide free corner samples of the casement window frame for color verification?
Is it possible to custom-match a specific RAL color for a decorative profile order?
Can I request a 3D-printed sample before ordering a custom industrial profile mold?
Can you extrude an architecture profile based on our proprietary CAD drawings?
What thermal performance certifications does a sliding door need for the UK market?
How are heavy floding door panels crated to ensure safe unloading at the job site?
Can we arrange our own freight forwarder to pick up the casement door shipment FOB?
What is the estimated ocean freight transit time for a shutter shipment from China to Europe?
How can we source replacement seals for your awing window models in the future?
How are sliding windows typically packaged to prevent glass breakage during ocean transit?
What is the average lead time for a 40ft container of standard aluminum casement windows?
Are there any extra tooling fees if my decorative profile order doesn’t meet the MOQ?
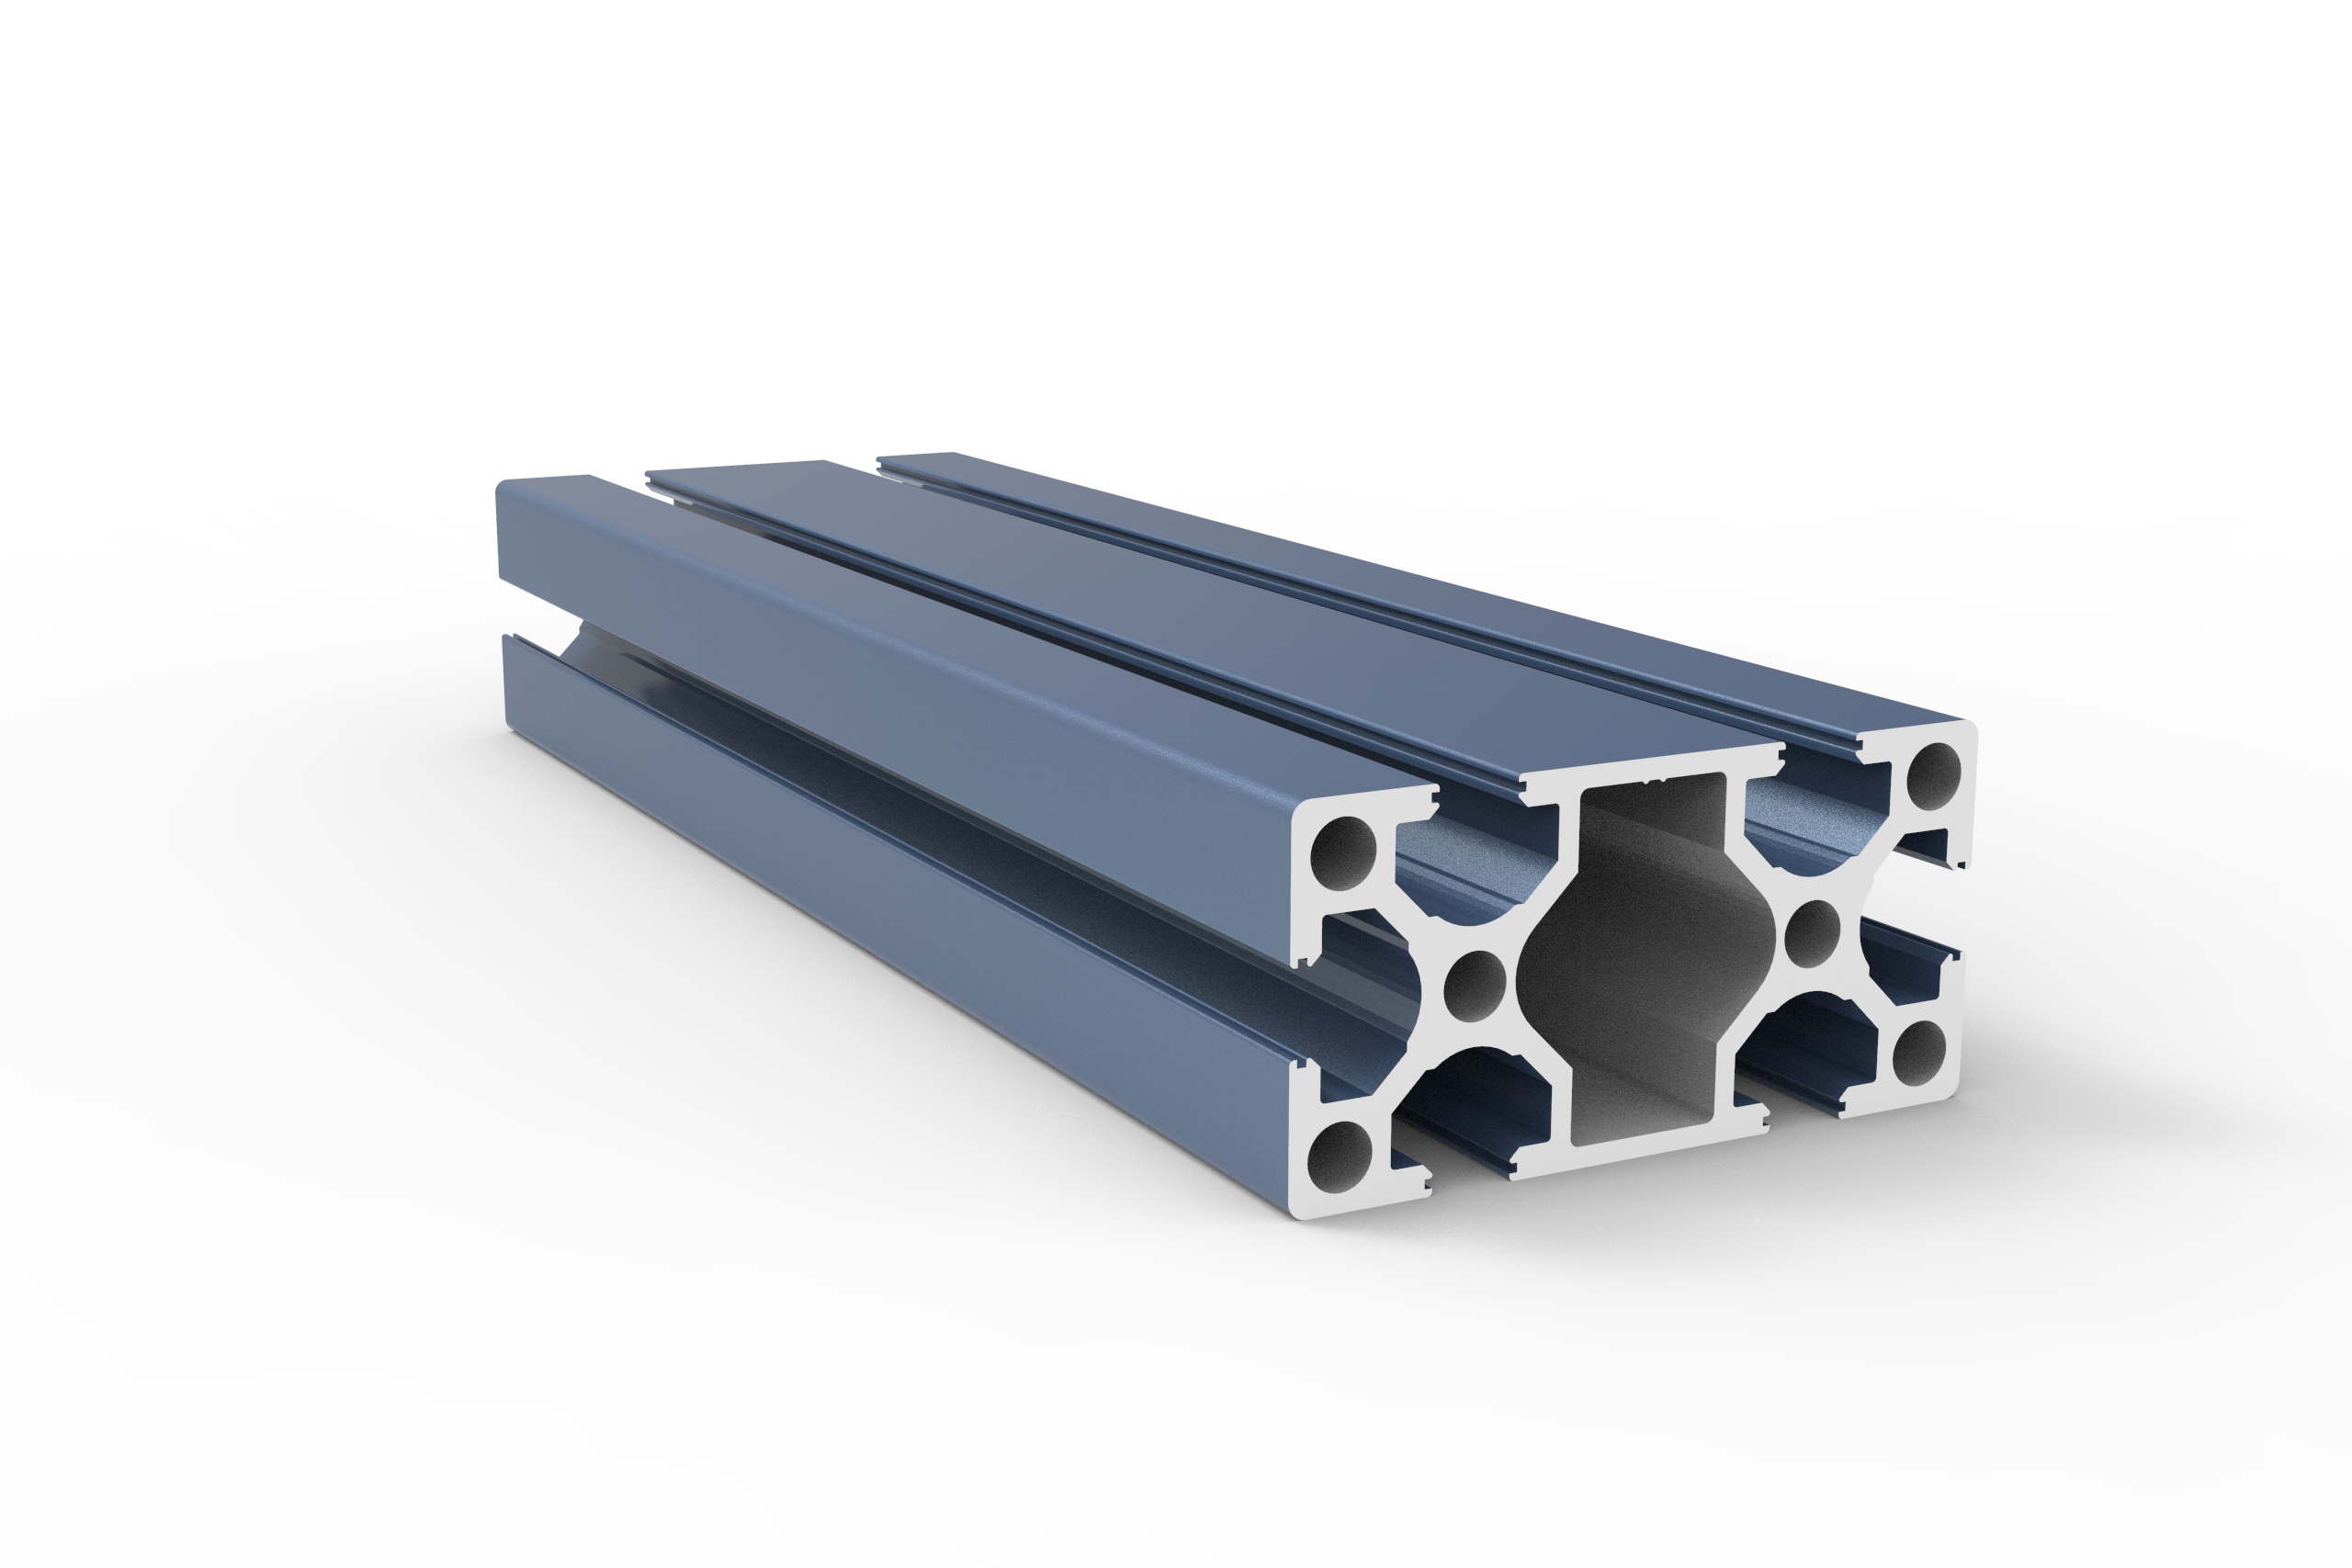
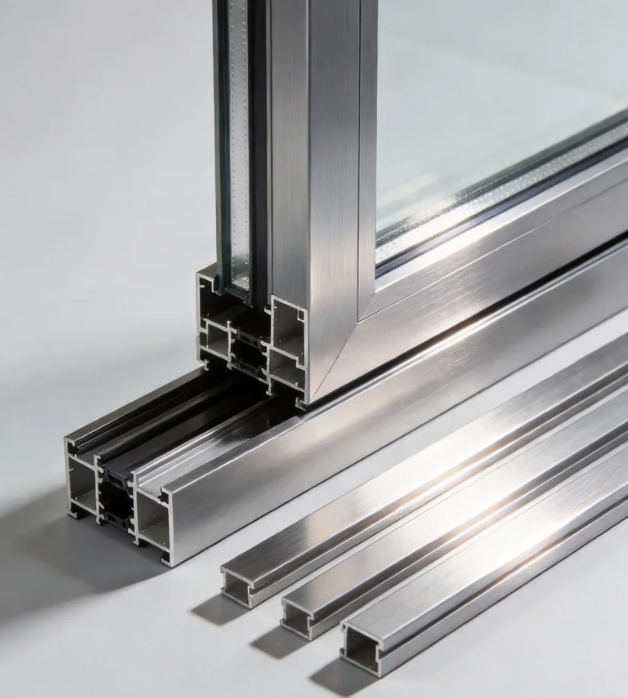
Can I get 3D printed prototypes of custom architecture profiles before committing to mold tooling?
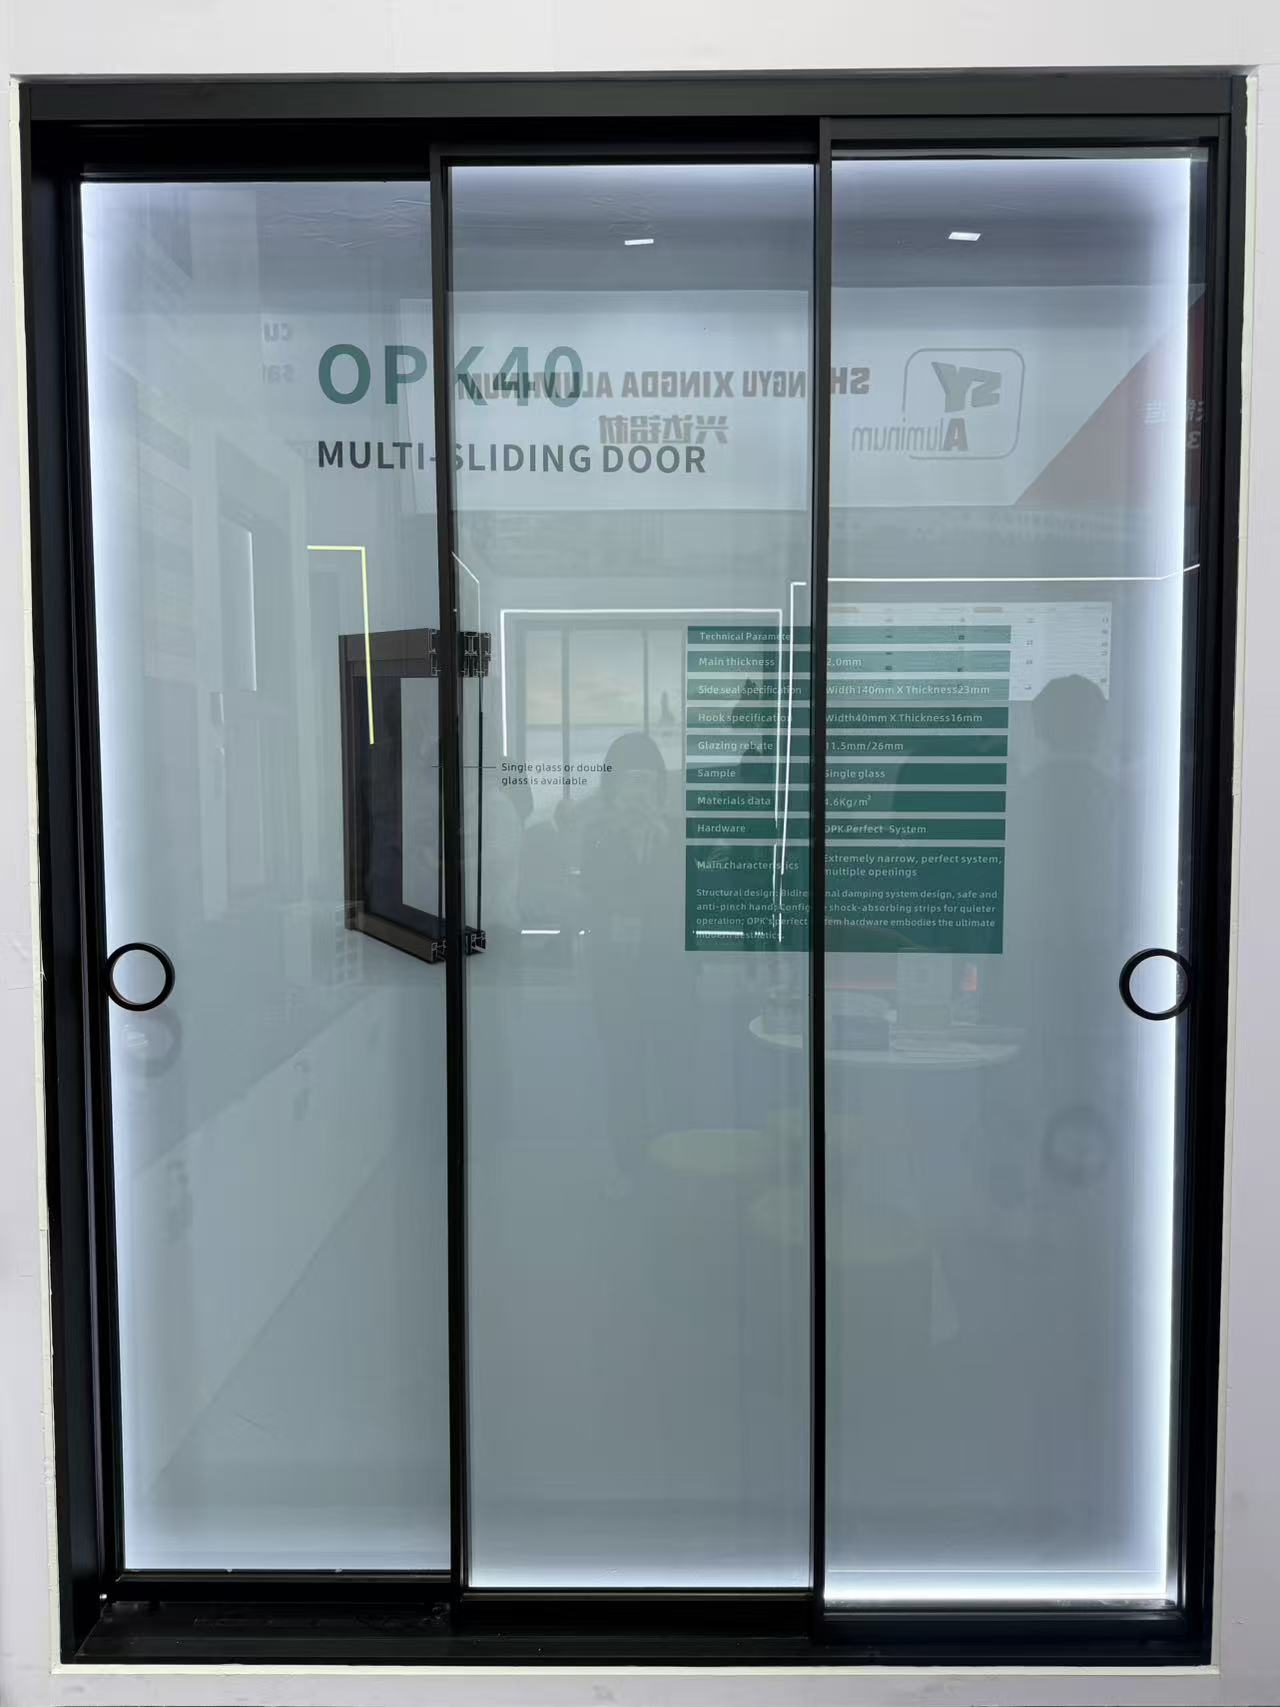
How is smart glass technology being integrated into modern residential sliding door units?
What options do you have for customizing the threshold height of an aluminum floding door?
What thermal break technology should I look for in a heavy-duty aluminum casement door?
What quality control processes do you perform on shutter hardware before final assembly?
Do you offer DDP shipping terms for awing window orders delivered to our warehouse?
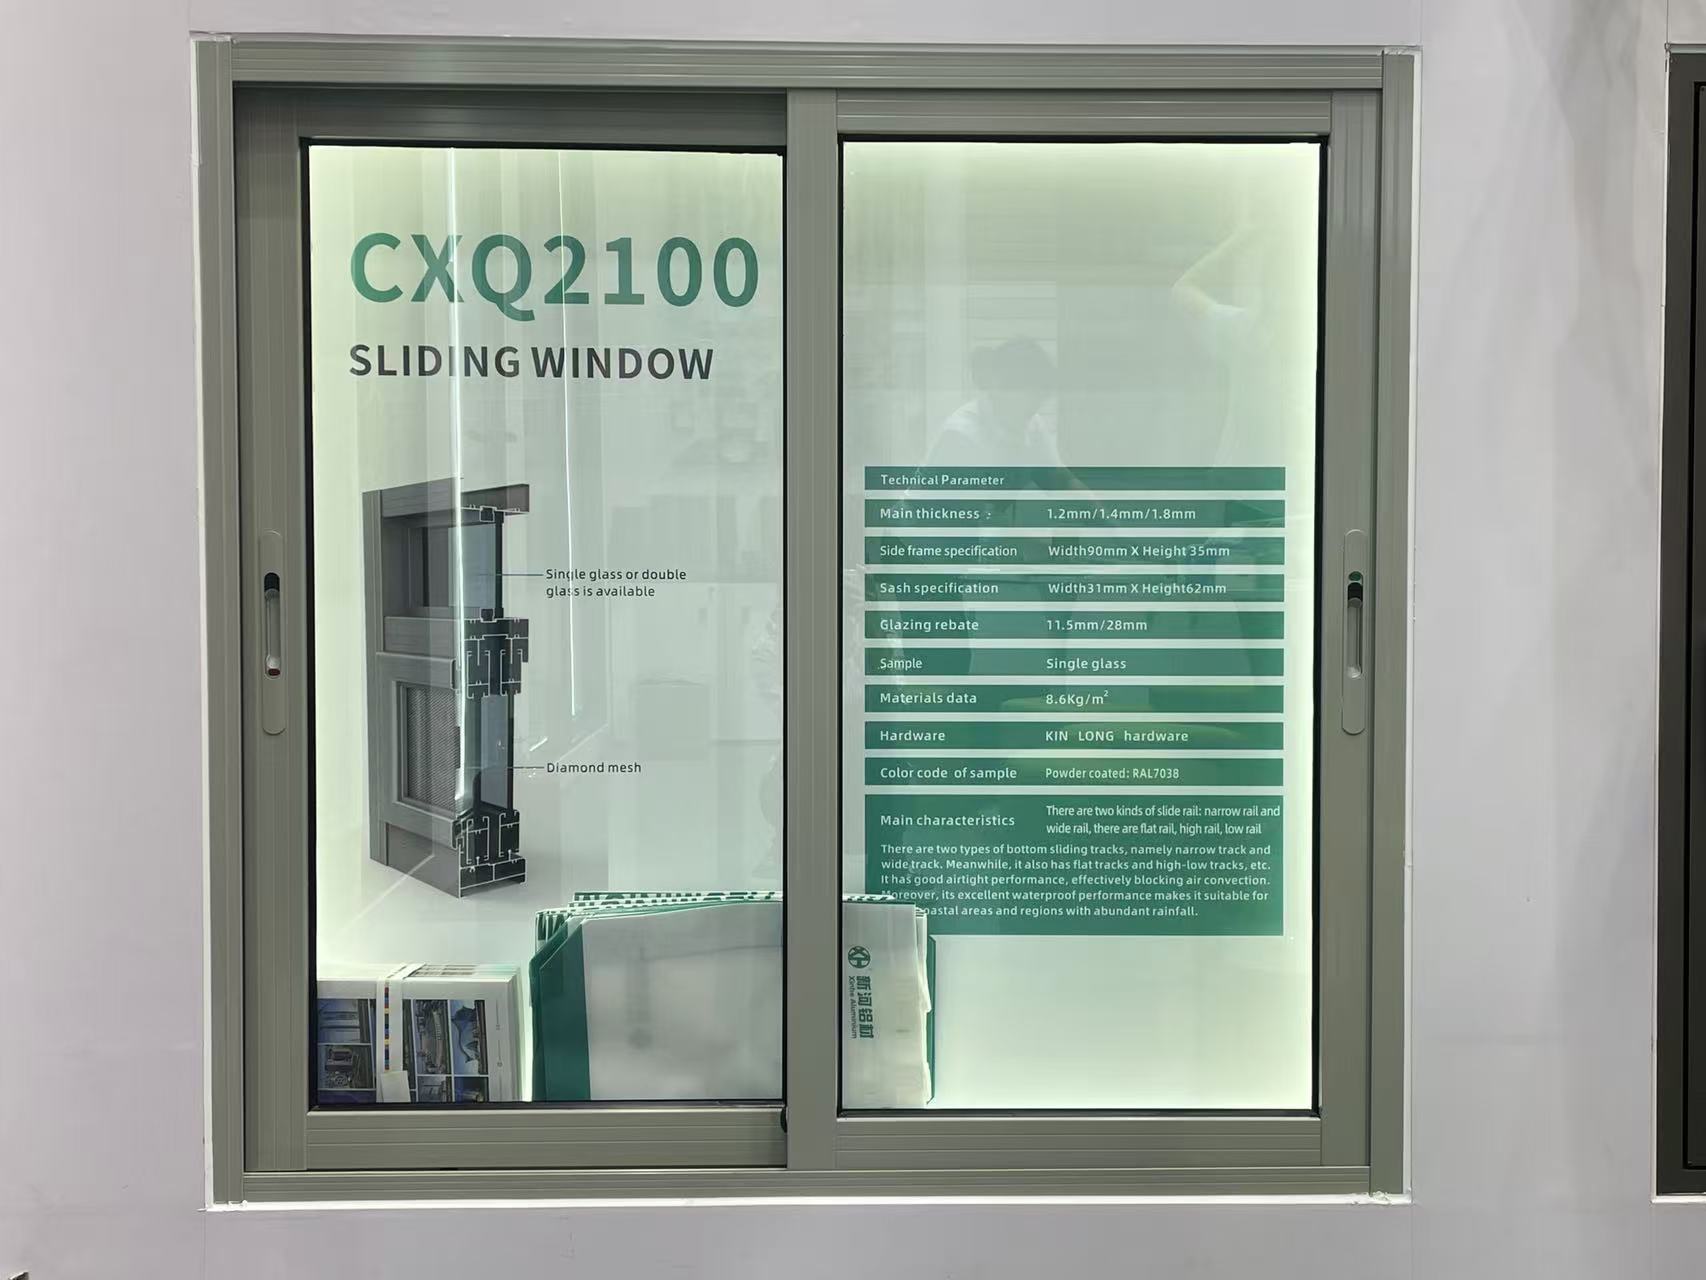
Is it possible to order a fully functional sliding window sample for mock-up testing?
Do you provide replacement hardware if the casement window hinges fail within 5 years?
How do you handle claims for decorative profile items damaged during transit?
What is the standard MOQ for custom-extruded aluminum industrial profile orders?
How does the order volume affect the per-ton price of custom architecture profile designs?
What is the warranty period for the rollers and tracks on your heavy-duty sliding doors?
How can we secure our deposit when purchasing high-value custom floding doors from a new supplier?
Can your factory match custom anodized colors for decorative profiles based on physical samples?
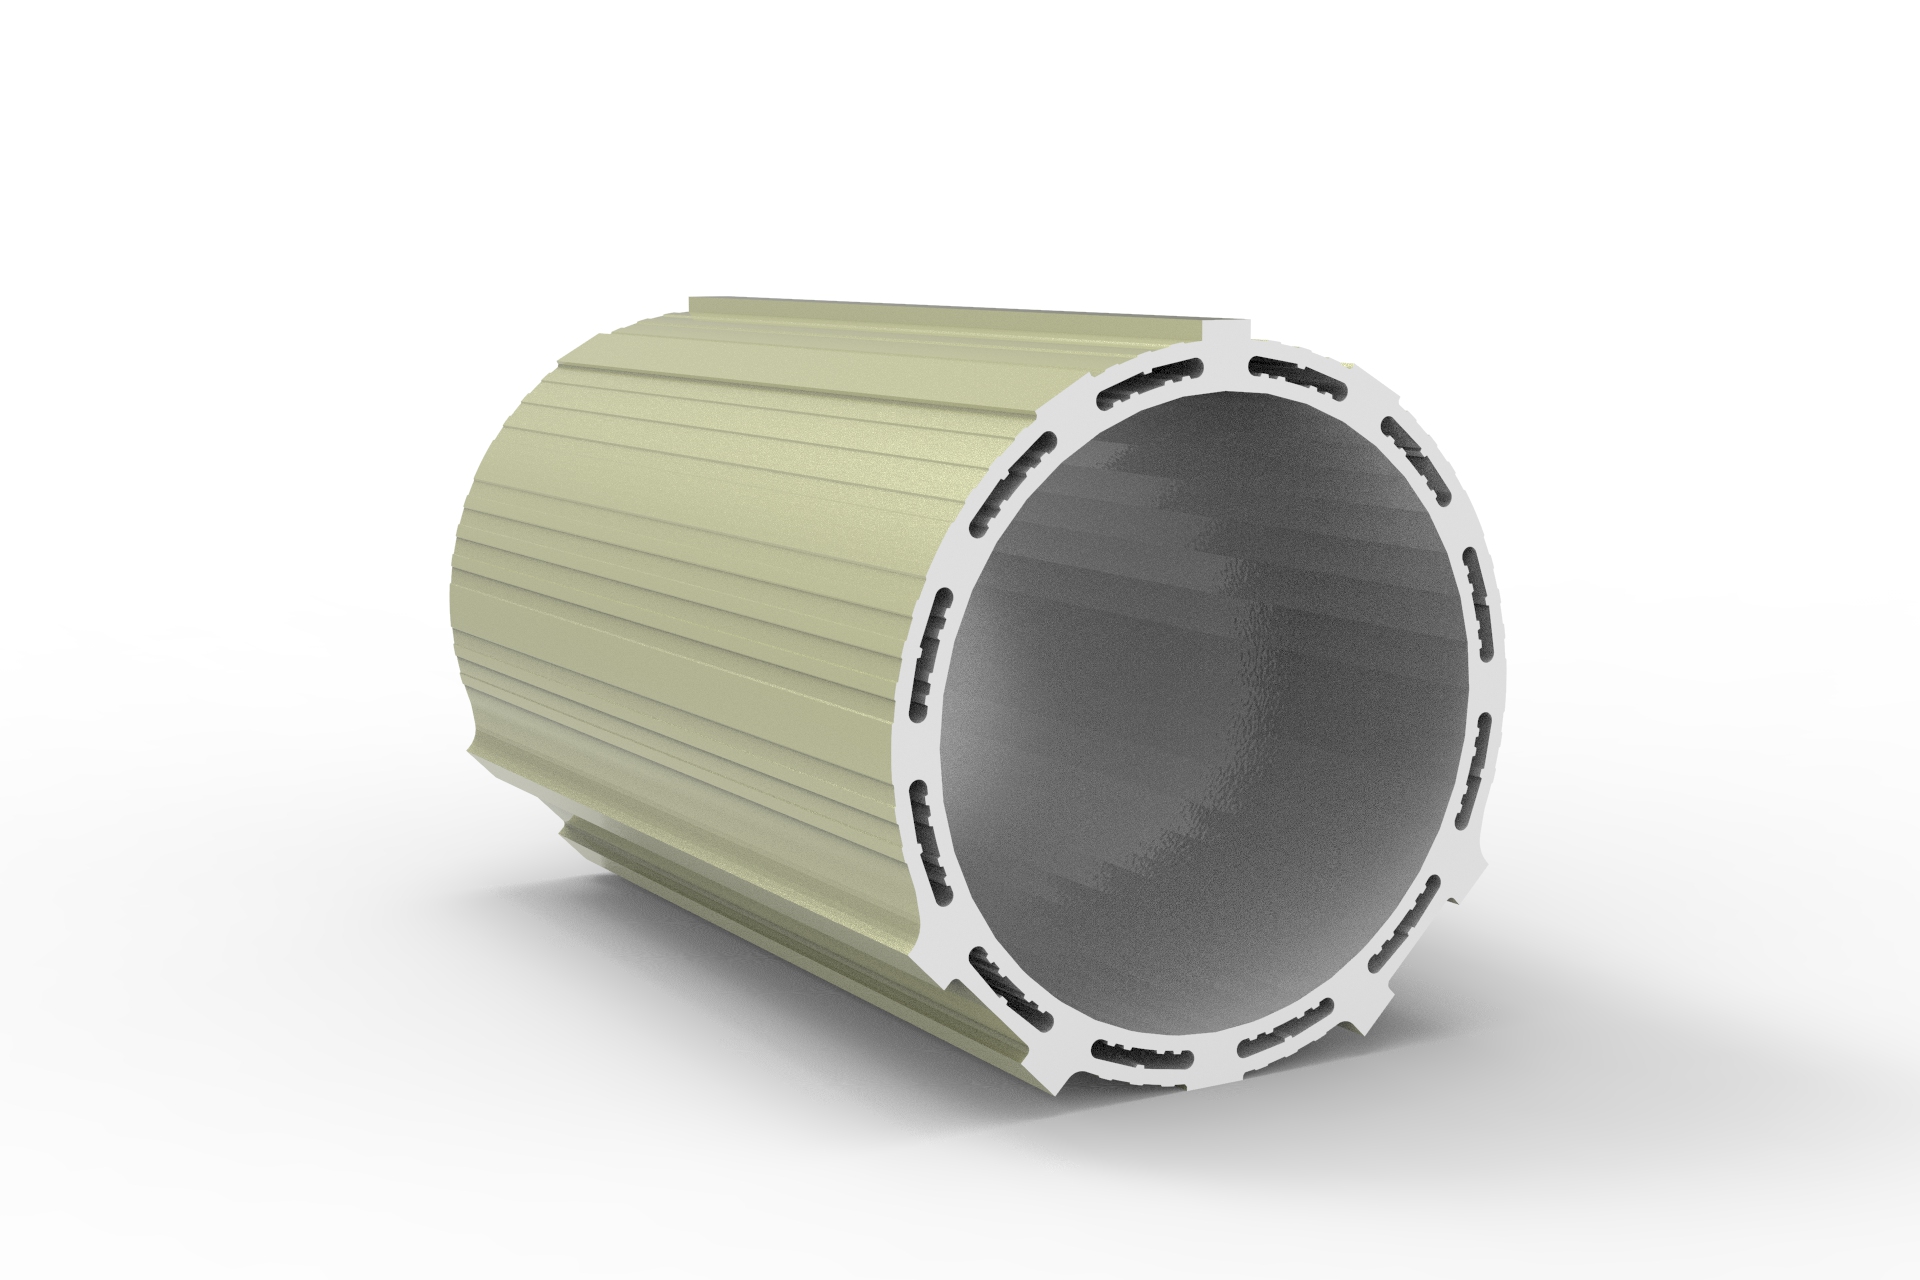
Is there a lighter alternative to aluminum industrial profile structures for robotics?
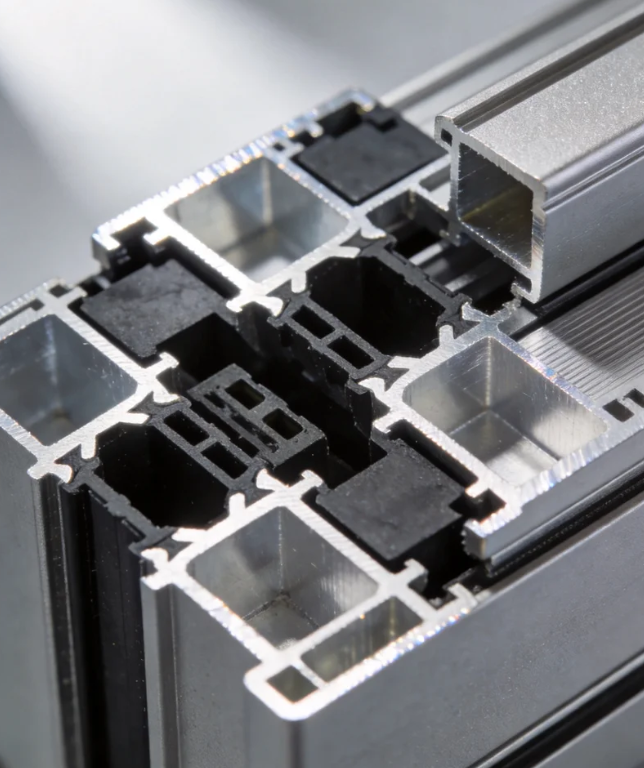
What payment security measures do you have for custom architecture profile tooling fees?
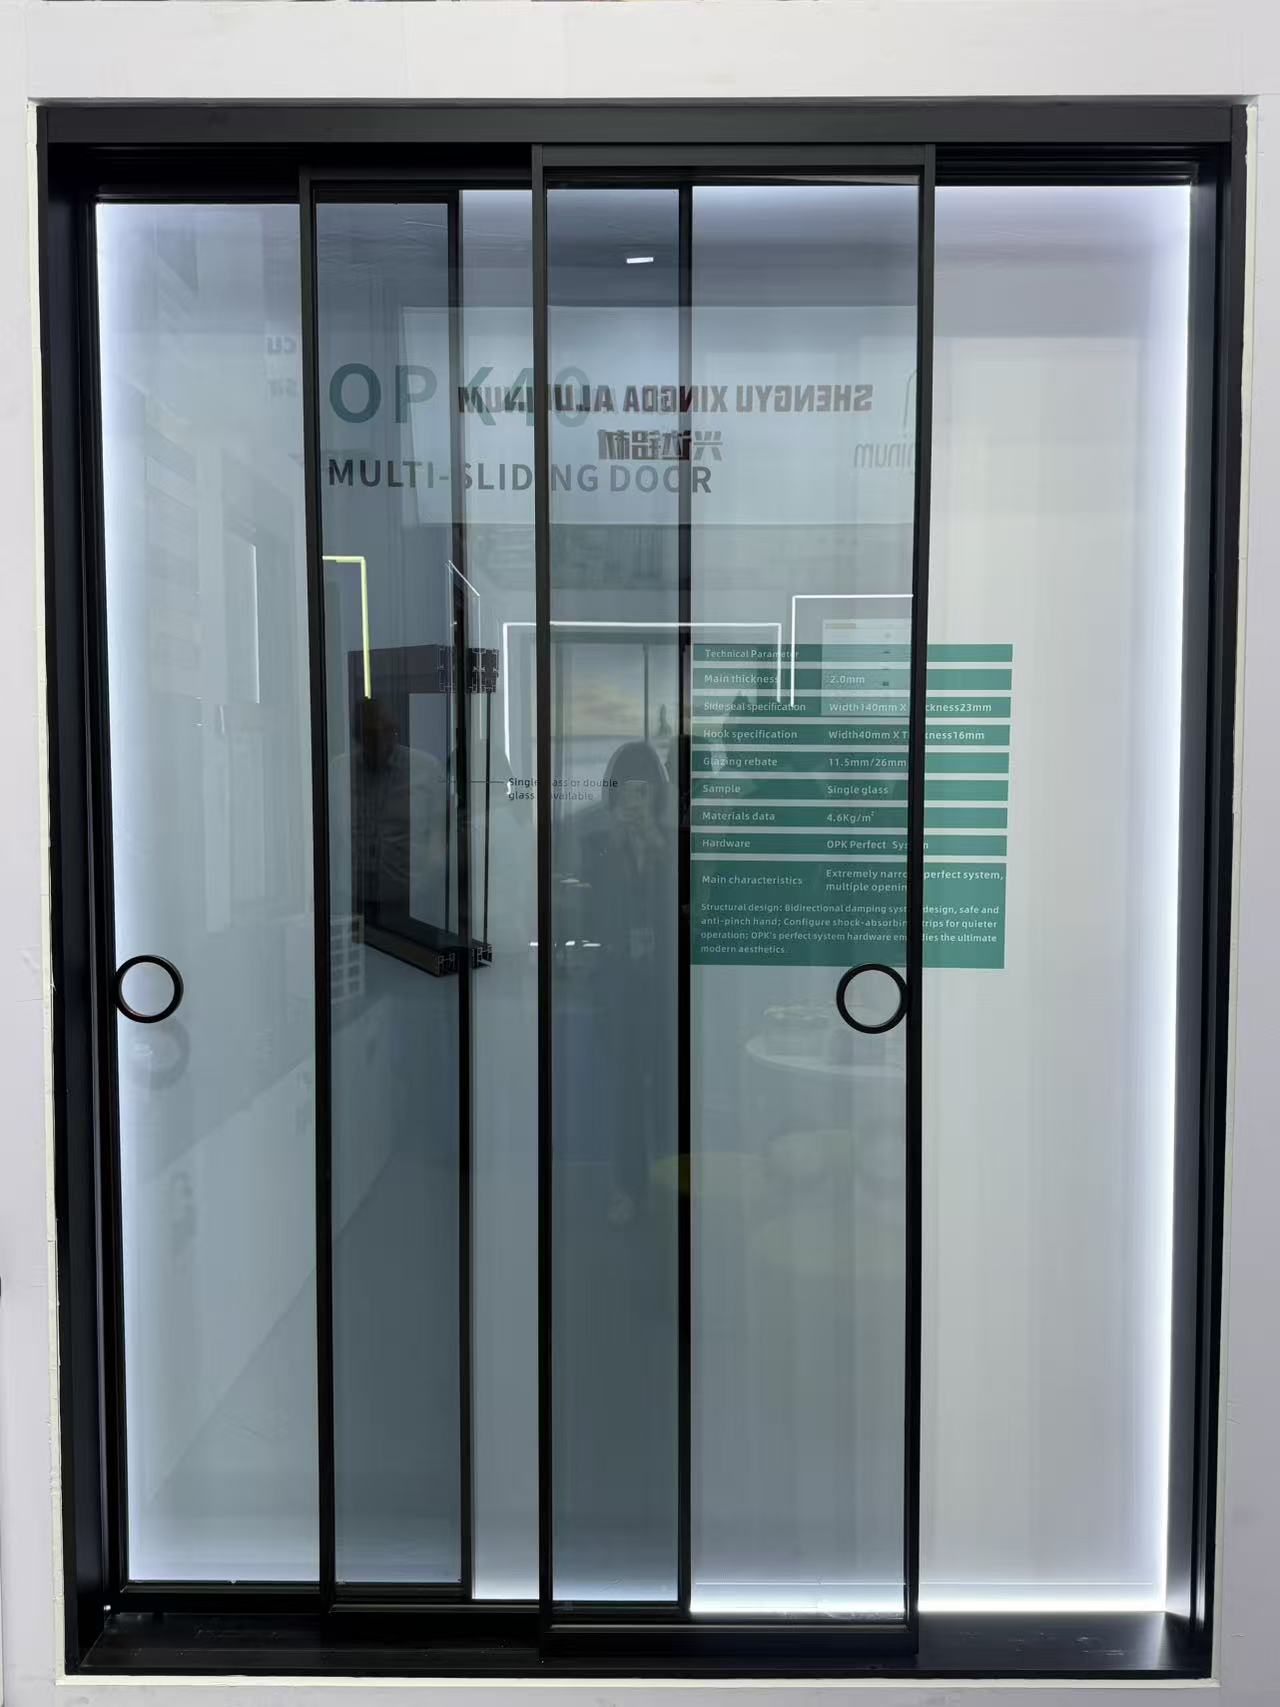
Can I order a sliding door with custom grid patterns between the glass panes?
How do you protect buyers against financial loss if the floding door shipment is delayed?
Are slim-frame aluminum casement door designs becoming more popular in modern offices?
What is your policy for replacing shutter components that arrive with color mismatch?
What kind of remote technical support do you offer for sliding window installation?
What is the maximum safe size for a top-hung awing window in commercial projects?
What environmental management standards does your decorative profile plant follow?
What is the standard lead time for producing a 40ft container of casement window orders?
What is the warranty period for the anodized finish on your industrial profile?
What are the latest eco-friendly trends in architecture profile manufacturing?
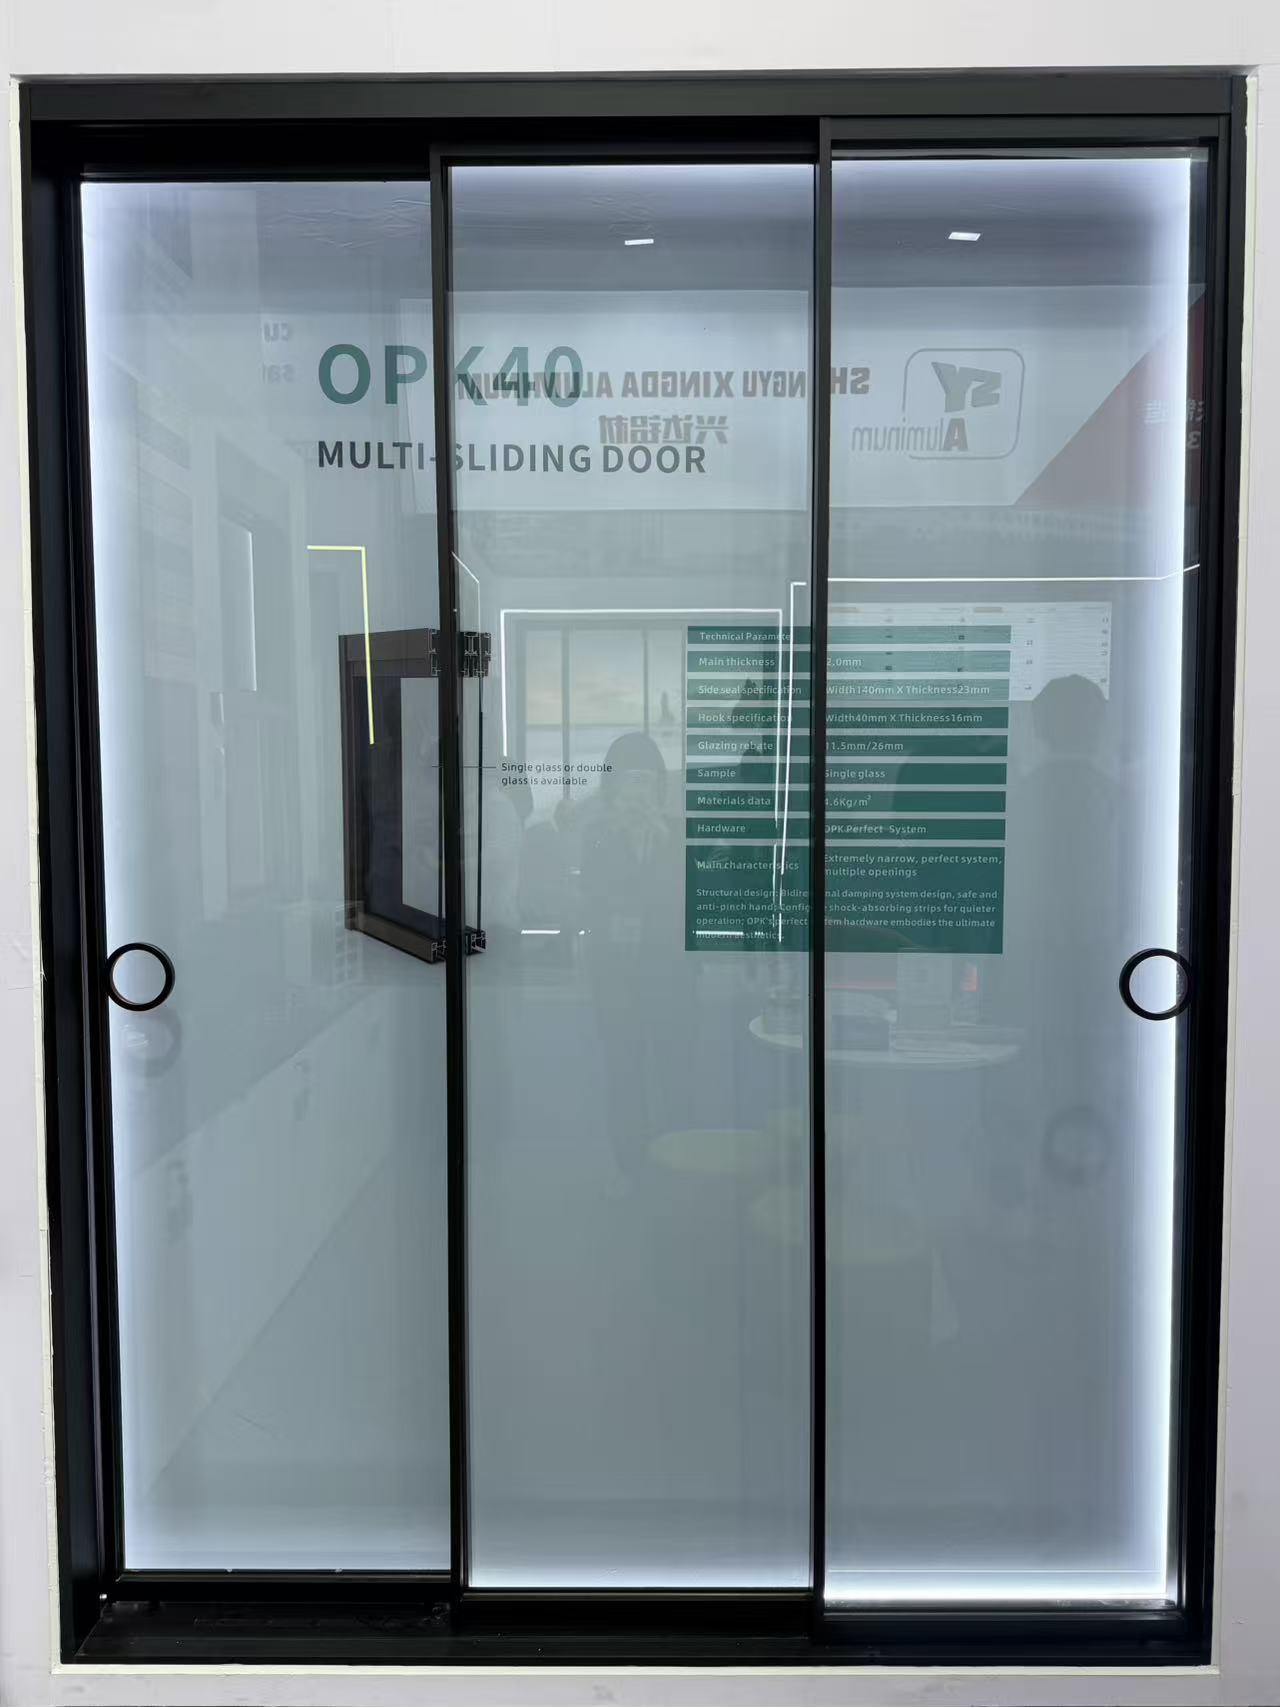
What is the average wholesale price per square meter for double-glazed sliding door systems?
How do I calculate the structural load requirement for a 5-panel exterior floding door?
Do your exterior shutter systems comply with Florida building codes for hurricane protection?
Do you offer Letter of Credit (L/C) payment options for casement door bulk orders?
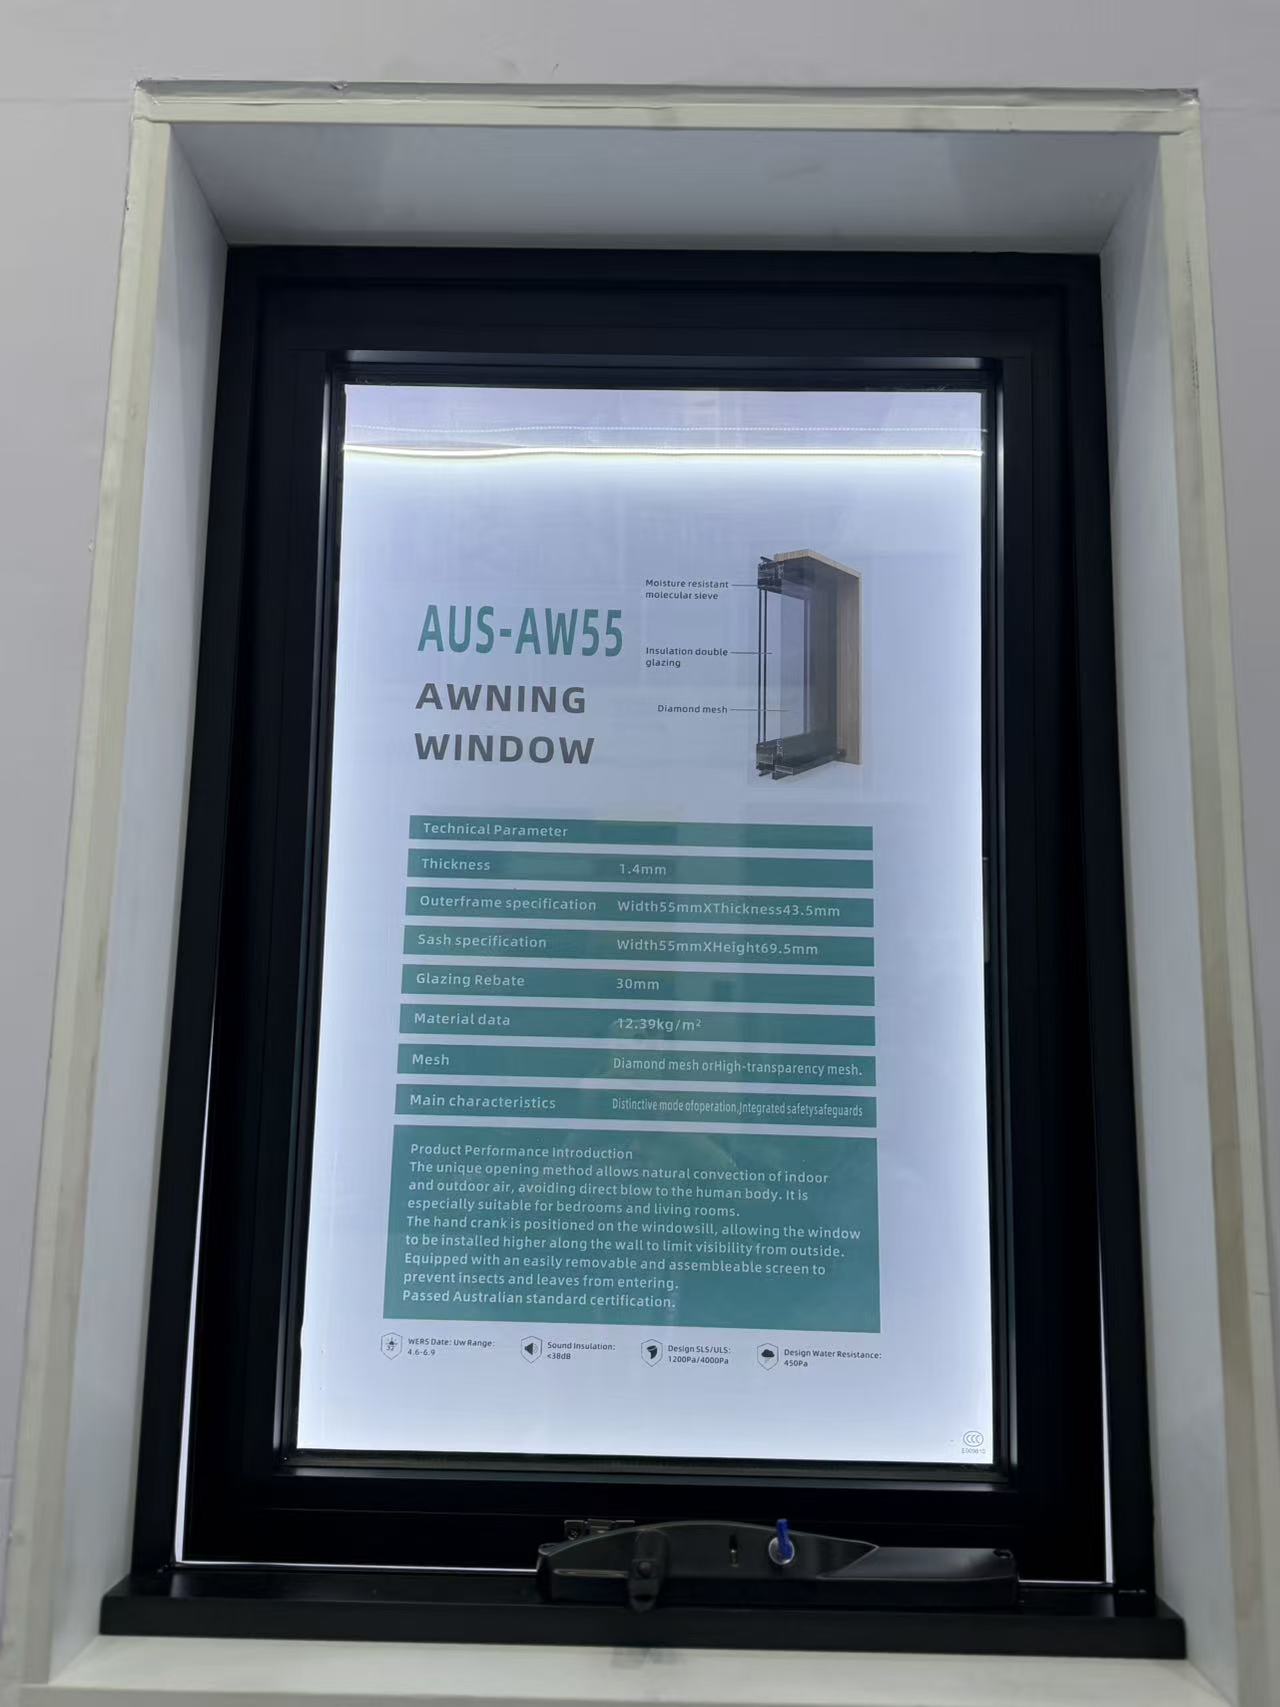
Which water tightness certifications are required for importing an awing window to Europe?
Do you allow virtual factory tours to inspect the sliding window assembly line?
What is the typical MOQ for ordering standard-sized aluminum casement window units?
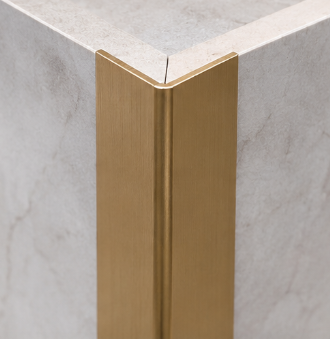
How long does it take to receive a physical sample of a gold-anodized decorative profile?
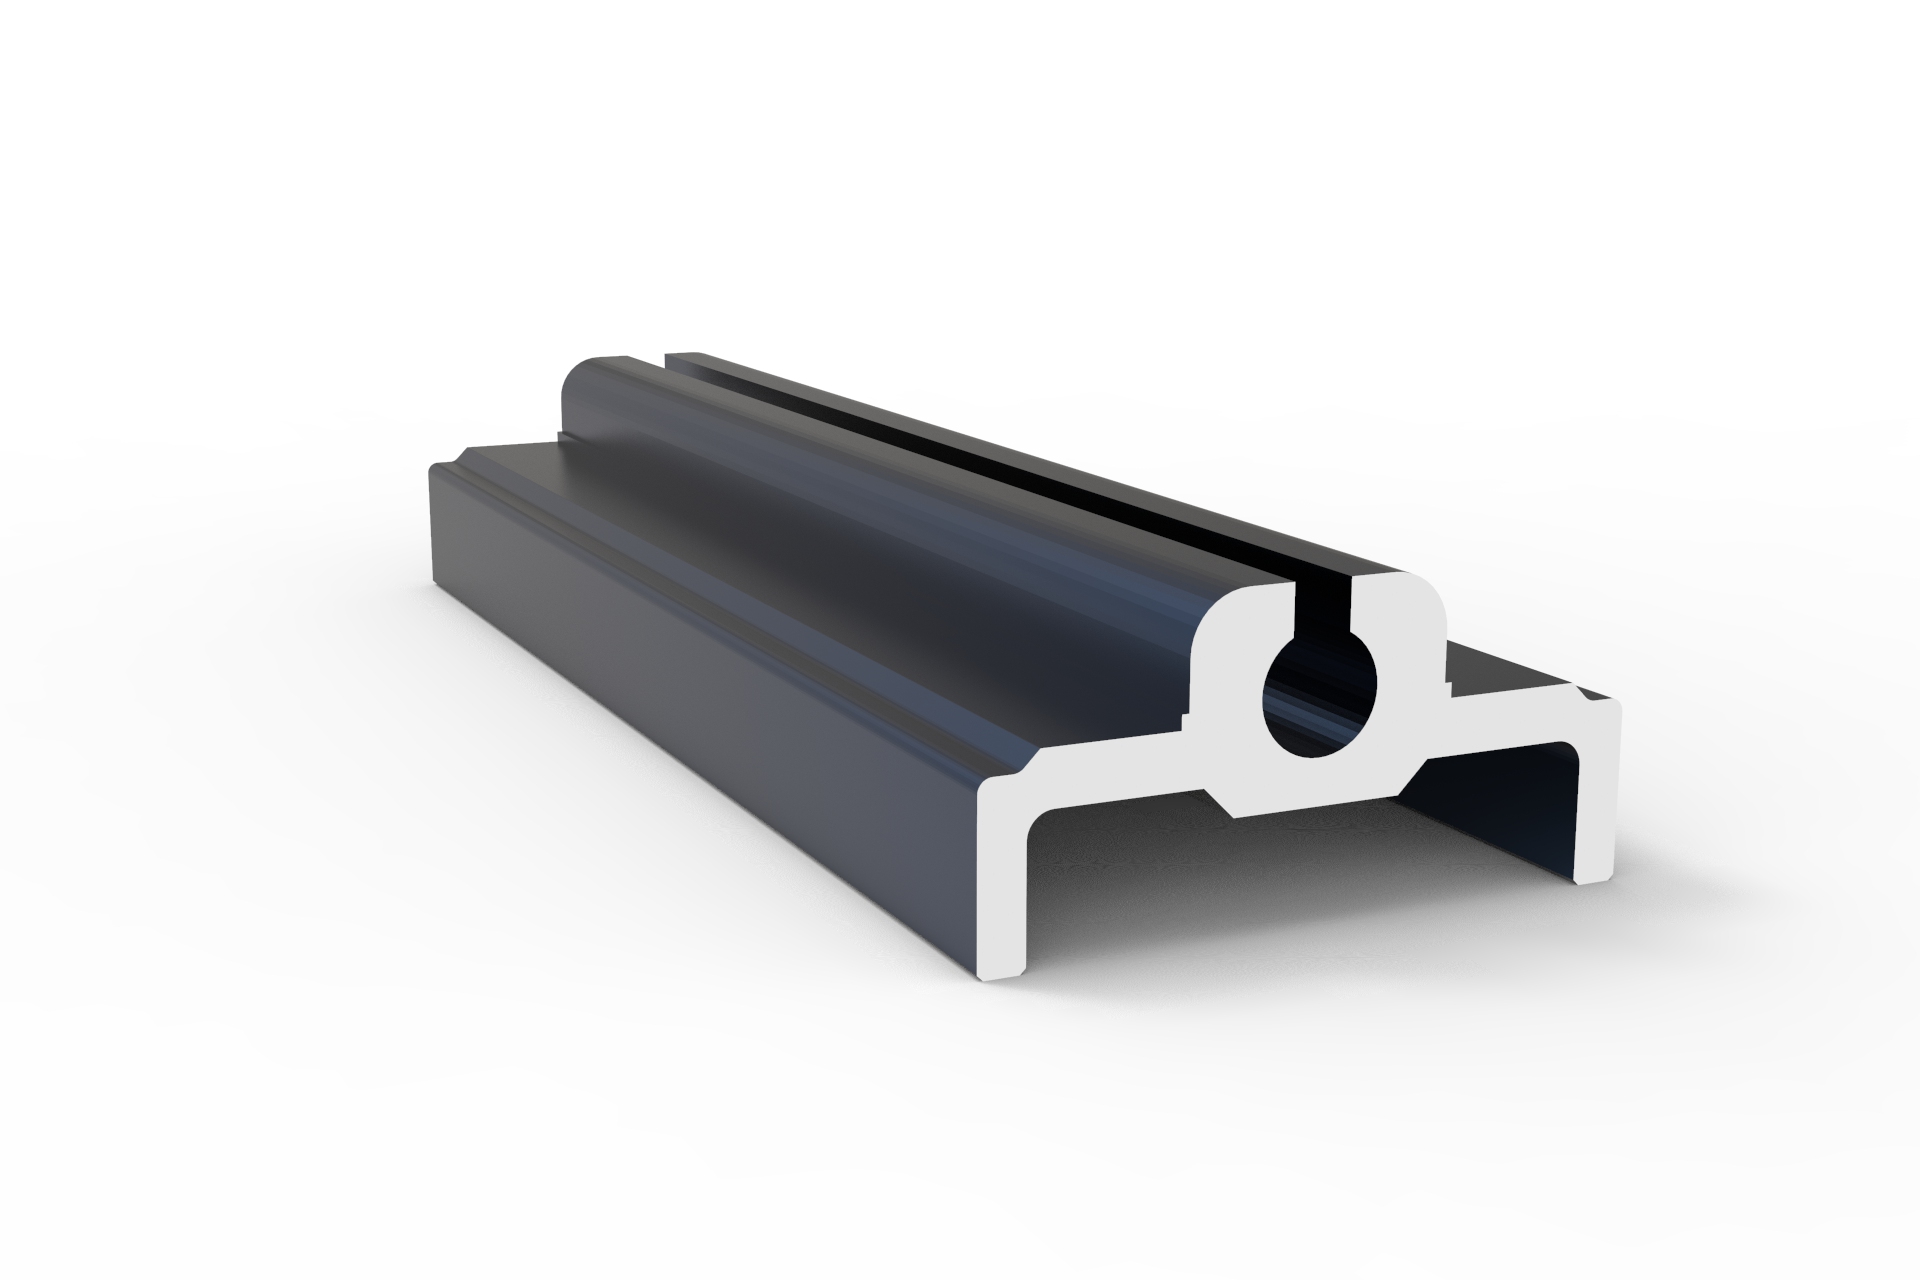
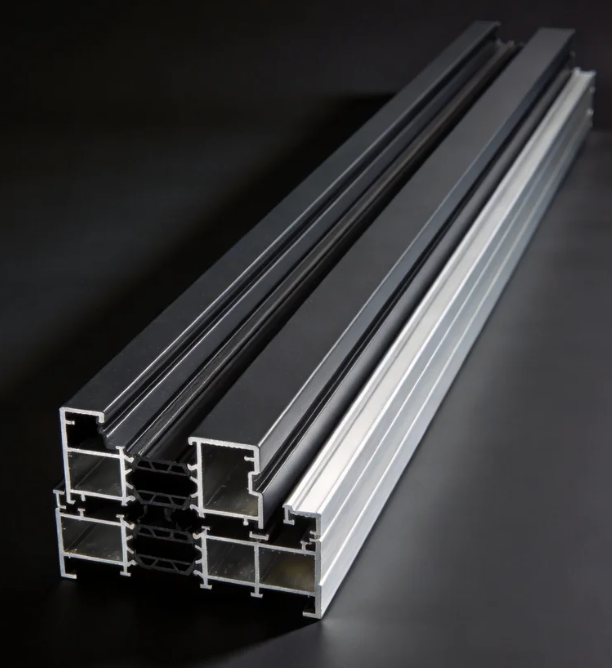
How do I choose the right alloy grade for architecture profiles in high-rise coastal buildings?
How do I choose the right track and roller specs for heavy-duty commercial sliding doors?
The core advantages of using aluminium profiles for the canopy
International demand: Dual drive by new energy and infrastructure
The advantages of using aluminium profiles to manufacture robot arms
The advantages of using aluminum profiles for door and window frames
The impact of the conflict between the United States and Iran on the price of aluminum
The advantages of using aluminium alloy for the main structure of high-speed train carriages
Methods for distinguishing Indoor and Outdoor Aluminium Doors
Maintenance methods and tips for aluminium doors and windows
Characteristic of outward-opening and hung aluminium windows
Xinhe Aluminium Research: 7.14-7.18 Analysis of Aluminium Prices
Seven Benefits Of Using Aluminium Profiles In Curtain Wall Systems
The Application of Aluminium Profiles in New Energy Vehicles
The Composition and Application of Series 6 Aluminium Alloys
Top 5 Benefits of Using LED Aluminium Profiles in Modern Lighting
A Complete Guide to Aluminium Frame Profiles for Modern Structures
Exploring the Strength and Versatility of Aluminium Extrusion Profiles
How to Choose the Right Aluminium Profile Supplier for Your Project
COMPANY