Selecting a reliable vendor in the metals sector is rarely a simple calculation of unit price per kilogram. Procurement teams often face a complex web of varying lead times, inconsistent yield rates, and hidden logistical hurdles that impact the bottom line.
The friction in global supply chains forces engineering and purchasing departments to scrutinize their vendor networks carefully. Finding the right aluminium profile manufacturer dictates not just the cost of raw materials, but the efficiency of your entire downstream assembly process.
An incompetent supplier introduces dimensional variations that cascade into secondary machining lines. When tolerances drift across different production runs, labor costs spike as factory workers struggle to force ill-fitting components together.
This operational drag represents a massive hidden tax on your production. Shifting the focus from raw material costs to total installed costs reveals the true value of a technically proficient extrusion partner.
Many procurement managers fall into the trap of prioritizing raw billet prices over actual defect-free yield. A low initial quote frequently masks high scrap rates that will eventually disrupt your inventory management.
When an extrusion partner lacks strict process controls, the variance in wall thickness can subtly increase the weight per meter. You end up paying for extra, useless metal that throws off your calculated shipping weights and product margins.
Delayed die trials represent another severe bottleneck in product development. Waiting weeks for a corrected custom geometry paralyzes your engineering team and pushes back critical product launch dates.
The financial impact of a delayed launch often dwarfs the pennies saved on a cheaper initial quotation. Realizing these hidden risks is the first step toward establishing a resilient procurement strategy.
Installed press tonnage is a metric frequently flaunted on factory brochures, but it tells an incomplete story. Massive machinery means nothing if the facility lacks the thermal management systems necessary to prevent warpage during the cooling phase.
True yield is defined by the volume of material that arrives at your facility ready for immediate assembly. It is the ratio of perfect, usable profiles against the total tonnage pushed through the extrusion press.
Assessing a facility requires looking past the raw output numbers and examining their scrap recycling practices. High-volume facilities that rely heavily on low-grade recycled scrap often struggle to maintain consistent structural properties across batches.
For us, operating since 1998, we learned that balancing scale with precision is the only sustainable path forward. By maintaining an annual production capacity of 200,000 tons across 5,000 distinct products, our facility supports clients in over 50 countries without compromising exact dimensional tolerances.
Managing high-mix, volume production means dedicating specific press lines to different industrial requirements. Architecture demands flawless surface finishes, while machinery components prioritize absolute structural rigidity and temper accuracy.
The behavior of the 6000 series alloys during extrusion is highly sensitive to temperature fluctuations. Pushing aluminum through a steel die generates immense friction, and controlling that heat determines the final grain structure of the metal.
Standardizing on the 6063 alloy for architectural purposes offers excellent finish quality, but it requires precise homogenization. If the raw billets are not properly pre-treated, hard spots develop that will inevitably score the extrusion die.
These microscopic die lines become glaring defects once the material undergoes anodizing or powder coating. A proficient extrusion partner maintains strict metallurgical checks on their incoming billets to prevent these surface failures.
Structural applications relying on 6061 alloys demand rigorous artificial aging processes. Achieving a consistent T6 temper requires massive curing ovens that maintain uniform heat distribution across a twenty-foot profile.
Inadequate aging leaves the center of a long extrusion softer than its ends. This hidden weakness only reveals itself under load in the field, leading to catastrophic mechanical failures and severe liability issues.
Raw extruded metal is highly susceptible to atmospheric oxidation and galvanic corrosion. The purpose of surface treatment extends far beyond aesthetics; it acts as the primary defense mechanism against environmental degradation.
Anodizing builds a controlled layer of aluminum oxide that is integral to the metal itself. Specifying the correct anodic film thickness is critical for the lifespan of outdoor architectural installations.
Powder coating introduces a different set of quality variables related to chemical adhesion. If the pre-treatment baths are contaminated, the powder layer will eventually blister and peel under ultraviolet exposure.
The financial fallout from a peeling architectural facade is devastating. Replacing installed vertical mullions on a commercial high-rise requires scaffolding, specialized labor, and profound disruption to the building occupants.
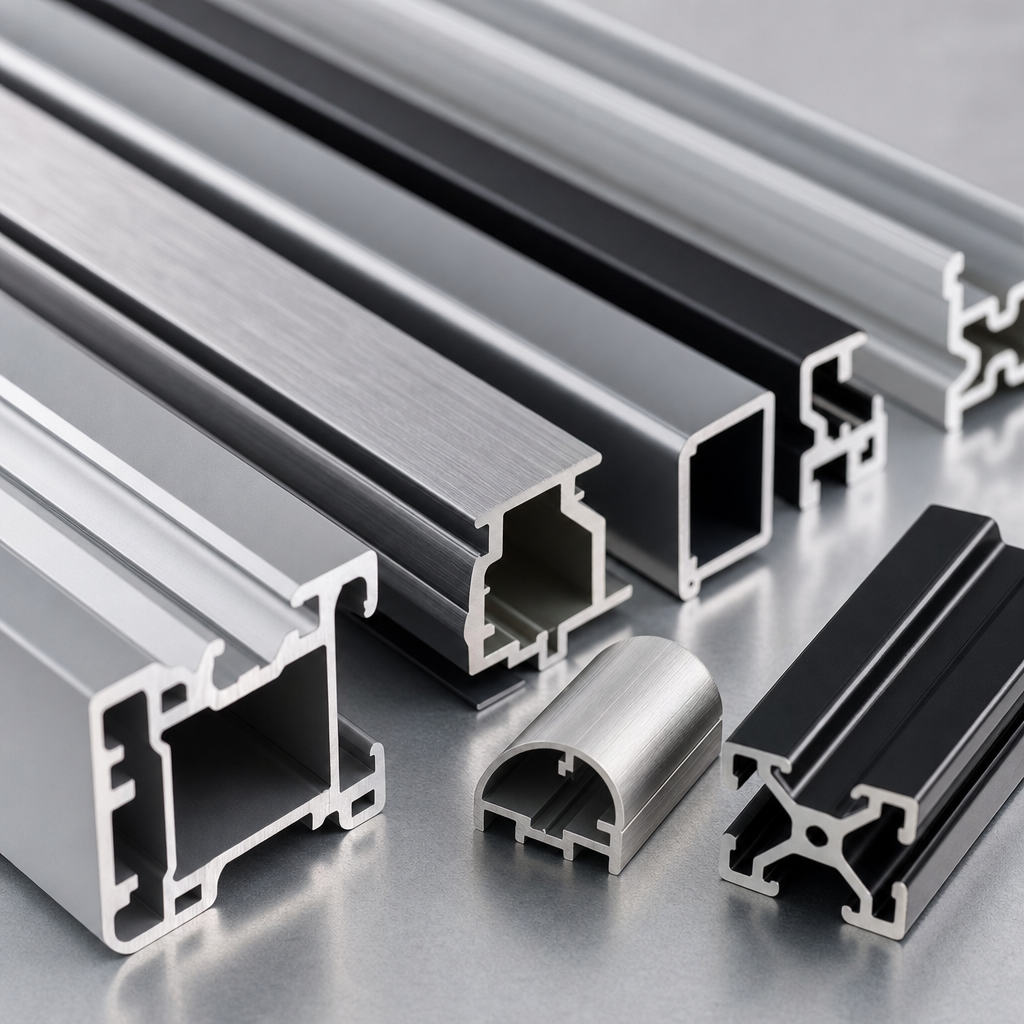
Standard geometric shapes are readily available, but they often force engineers into clumsy design compromises. Developing a custom die allows for the integration of screw bosses, snap-fits, and heat-sinking fins directly into a single profile.
This consolidation eliminates secondary brackets and fasteners, dramatically reducing your final assembly time. The initial investment in a custom steel die pays for itself rapidly through accelerated manufacturing throughput.
The risk lies in the iterative loop of die correction. Aluminum flows through different sections of a complex die at different speeds, which can cause the profile to twist as it exits the press.
Advanced thermal modeling software allows engineers to predict these flow imbalances before a single piece of steel is cut. Simulating the extrusion process minimizes the trial runs required to achieve the correct geometric profile.
When your custom aluminium profile supplier possesses in-house die manufacturing capabilities, the modification timeline shrinks from weeks to days. This agility allows your engineering team to iterate designs rapidly and respond to shifting market demands.
Understanding the landscape of suppliers helps in aligning your procurement strategy with your actual project requirements. Different tiers of manufacturers serve entirely different business models and risk profiles.
| Vendor Profile | Ideal Scenario | Hidden Risks | B2B ROI Impact |
|---|---|---|---|
| Mega-Conglomerates | Massive infrastructure projects requiring unlimited capacity. | Rigid minimum order quantities and slow response to design changes. | Low ROI for mid-sized custom batches due to administrative bloat. |
| Established Global Exporters | Projects demanding custom geometries, consistent volume, and export compliance. | Requires careful initial alignment on shipping logistics and packaging. | High ROI through reduced assembly friction and reliable defect-free yield. |
| Local Micro-Boutiques | Urgent prototyping or extremely low-volume domestic orders. | Inconsistent batch quality and lack of heavy press capabilities. | Negative ROI at scale due to high scrap rates and finishing bottlenecks. |
Relying on a mega-conglomerate guarantees raw capacity but strips away engineering support. You become a negligible account in their system, forced to adapt your designs to their rigid production schedules.
Conversely, depending on local micro-shops exposes your supply chain to sudden capacity constraints. When your product takes off, these small facilities lack the infrastructure to scale production up without sacrificing quality.
Partnering with an established exporter occupies the pragmatic middle ground. It provides the heavy industrial capacity necessary for scale, while retaining the engineering agility required to support complex product ecosystems.
The journey from the extrusion press to your loading dock is fraught with physical and environmental hazards. A perfectly extruded profile is worthless if it arrives scratched, bent, or chemically stained.
Aluminum is particularly vulnerable to water damage during oceanic transit. Condensation forming inside a shipping container can trigger a reaction known as water staining, leaving permanent white marks on the metal surface.
Preventing this requires a multi-layered approach to packaging and environmental control. Interleaving profiles with pH-neutral kraft paper prevents physical abrasion during transit vibrations.
Wrapping the bundles tightly in shrink film creates a localized barrier against moisture ingress. For highly sensitive architectural finishes, desiccant packs placed inside the container absorb the ambient humidity during the voyage.
Wooden crating provides the necessary structural rigidity to prevent the bundles from bending during crane loading operations. Refusing to cut corners on packaging is a defining characteristic of a mature export operation.
A thicker wall does not automatically equate to superior load-bearing capacity. The structural integrity of an extrusion is governed by its cross-sectional geometry and the calculated moment of inertia. Intelligent die design can hollow out non-critical areas, reducing weight and cost while maintaining structural rigidity.
Anodizing relies on electrochemical reactions that are highly sensitive to bath temperature, acid concentration, and electrical current density. Slight variations in these parameters alter the pore structure of the anodic film, changing how it refracts light. Strict automated controls over the chemical baths are required to maintain color consistency across months of production.
While advanced presses can achieve extremely tight dimensional accuracy, extrusion is fundamentally a high-heat deformation process. It cannot replicate the micron-level precision of a cold CNC milling machine. You must design your mating components to absorb the natural tolerance window of the extrusion standard.
The quality of recycled aluminum depends entirely on the sorting and remelting process. Properly processed secondary billets can match the mechanical properties of primary metal perfectly. The danger arises when suppliers mix unknown scrap without conducting rigorous spectrographic analysis of the molten pool.
Your supply chain strategy must evolve past the simple solicitation of blind quotes. Establishing a matrix of technical requirements ensures that you are comparing capable partners rather than gambling on the lowest bidder.
Demand transparency regarding their die correction processes and typical trial timelines. A competent facility will gladly share their engineering workflows and thermal modeling capabilities to prove their technical depth.
Assess their approach to surface finishing and environmental testing. Request salt spray test data for their powder coating lines and verify their adherence to international anodic film thickness standards.
Evaluate their capacity to handle your projected growth rather than just your current volume. A partner with a broad range of press tonnages can scale your components seamlessly as your market share expands.
By prioritizing reliable yield, engineering agility, and rigorous process control, you insulate your assembly lines from chaotic supply shocks. Aligning your procurement with a technically sophisticated aluminium profile manufacturer is the most direct path to stabilizing costs and accelerating your product velocity.
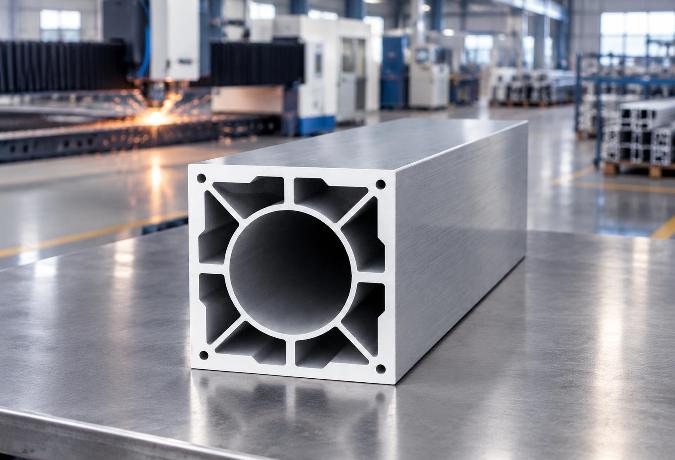
Choosing Industrial Aluminium Profiles for Laser Cutting Machines: A Technical Guide
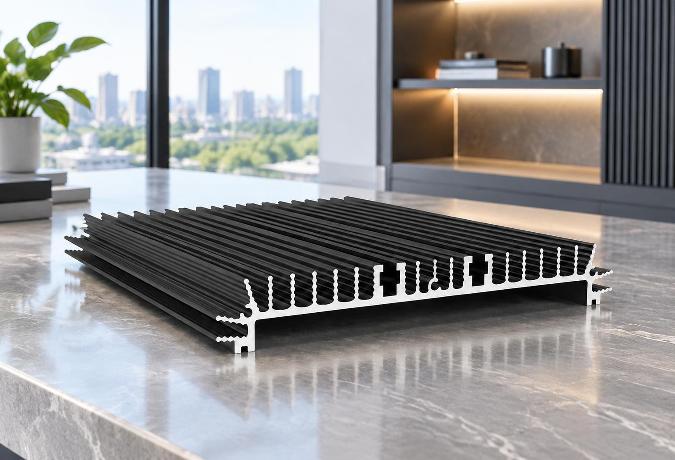
How LED Aluminium Profile Heatsinks Manage Thermal Challenges in High-Performance Lighting
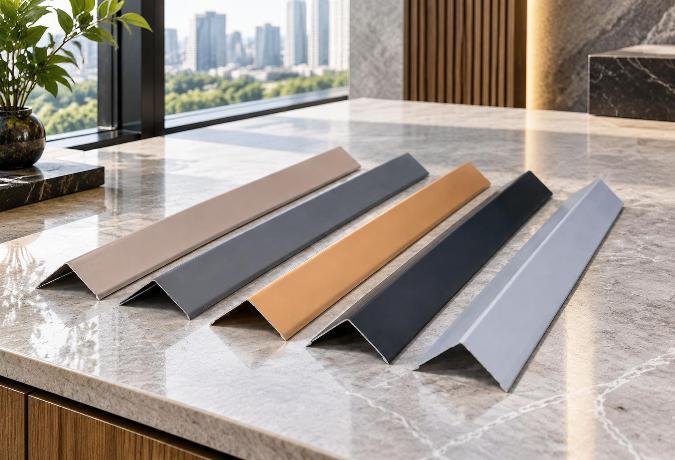
Architectural Aluminium Profiles: Choosing the Right Angle Design for Framing and Trim
Choosing the Right Aluminium Balustrade Profiles for Your Project
Choosing the Right Aluminium Door Profiles for Narrow-Frame Sliding Systems
Aluminium Window Profiles: Engineering Durable Facades for Modern Buildings
Aluminium Thermal Break Profiles: Design Principles and Practical Applications
Aluminium Extrusion for Furniture: Structural Logic Behind Lightweight Precision
Aluminium Wardrobe Profiles: A Practical Guide to Frames, Tracks, and Finishes
Choosing the Right Aluminium Linear Rail Profile for Motion Systems
Anodized Aluminium Profiles: Material Selection and Practical Applications in Modern Design
Anodized Aluminium Profiles: Material Selection and Practical Applications in Modern Design
Aluminium Decorative Profiles: Design, Installation, and Interior Applications
Aluminium Profiles for Automation: A Practical Guide to Modular Frame Design
Aluminium Extrusion for Furniture: Structural Logic Behind Lightweight Precision
Aluminium Thermal Break Profiles: Design Principles and Practical Applications
How do suppliers normally handle Sliding door installation problems overseas?
Choosing the Right Aluminium Balustrade Profiles for Your Project
Aluminium Louver Profiles: Light Control and Ventilation in Modern Architecture
Aluminium Curtain Wall Profiles: Structural Design and Performance in Modern Architecture
Aluminium Trim Profiles: Bridging Aesthetics and Performance in Modern Interior Design
How do I verify Casement window production capacity before signing a contract?
Powder Coated Aluminium Profiles: Durability and Design in Modern Applications
How Aluminium Heatsink Profiles Keep Electronics From Cooking Themselves
How do FOB and CIF change my risks when importing Sliding doors?
What support should I receive if Architecture profile dimensions are wrong?
Aluminium Profile Alloys 6063 T5 T6: Properties, Heat Treatment Differences, and Application Selecti
Inside an Aluminium Profile Factory: How Angle Profiles Are Made and Chosen
What is a realistic MOQ for a first Sliding window trial order?
Which factory records should I review before buying Industrial profile?
Aluminium Extrusion for Machinery: Choosing the Right Profile for Industrial Equipment
Aluminium Extrusion for LED Lighting: Choosing the Right Heatsink Profile
Can a Floding door supplier protect my private design from competitors?
Which Industrial profile tolerances affect assembly accuracy and finished quality?
Can trade credit insurance cover my Architecture profile purchase risk?
Custom Aluminium Extrusion Profiles: Engineering Precision into Industrial Motion Systems
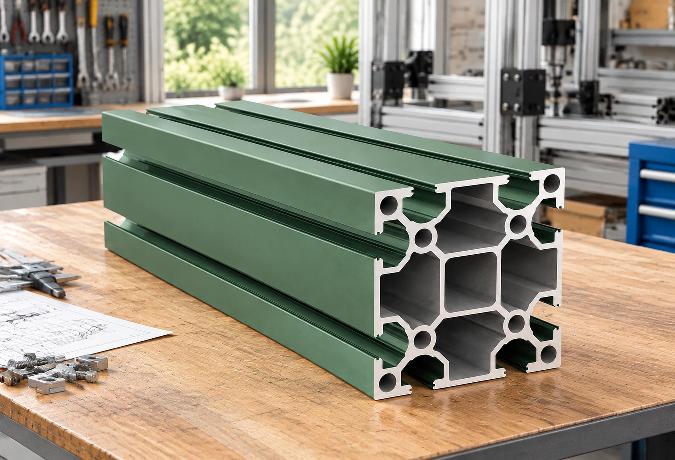
T-Slot Aluminium Extrusion: Structural Framework Design Without Welding
Which recycled-content records are credible for Sliding window procurement?
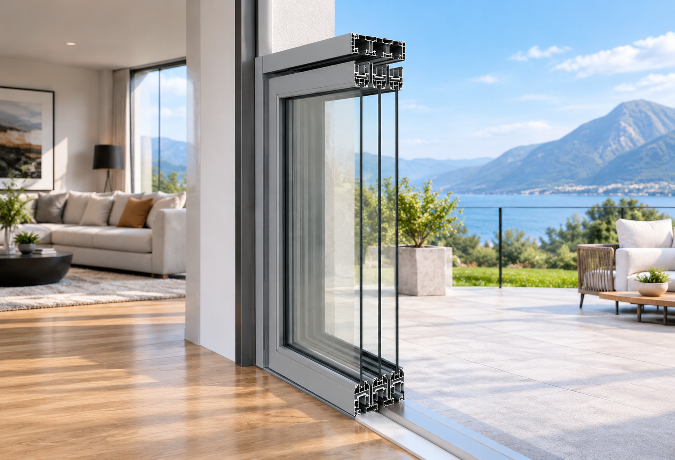
Aluminium Sliding Door Profiles: A Practical Guide to Frame Design and Performance
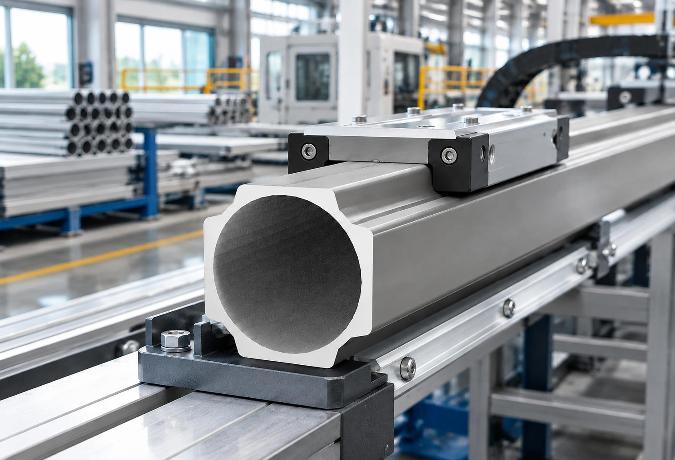
How Aluminium Extrusion Manufacturers in China Support Linear Motion Systems
What contract clauses protect my money if Casement door quality is unacceptable?
How do I confirm Sliding door testing equipment is calibrated and current?
Should I visit an Architecture profile plant before placing a large order?
Which compliance tests should a Floding door pass before international shipment?
How do I compare Decorative profile color samples under different lighting?
What payment and price terms make sense for a small Casement window order?
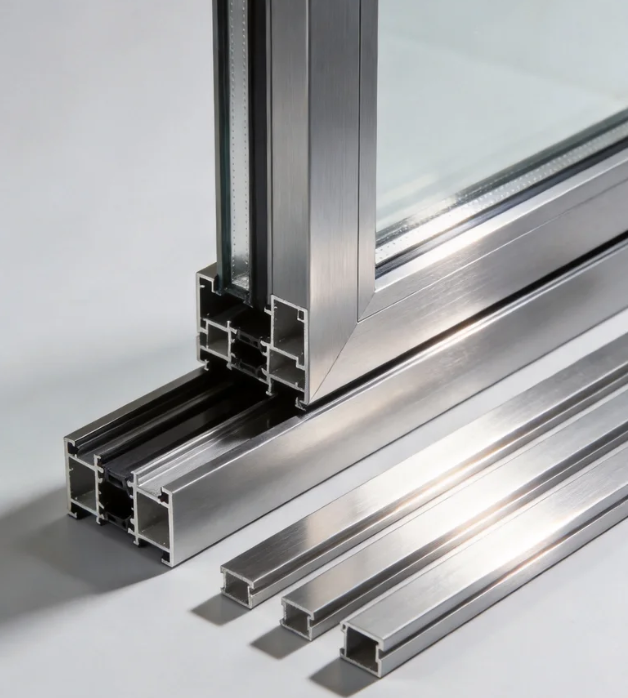
What lead time should I allow for a seasonal Floding door order?
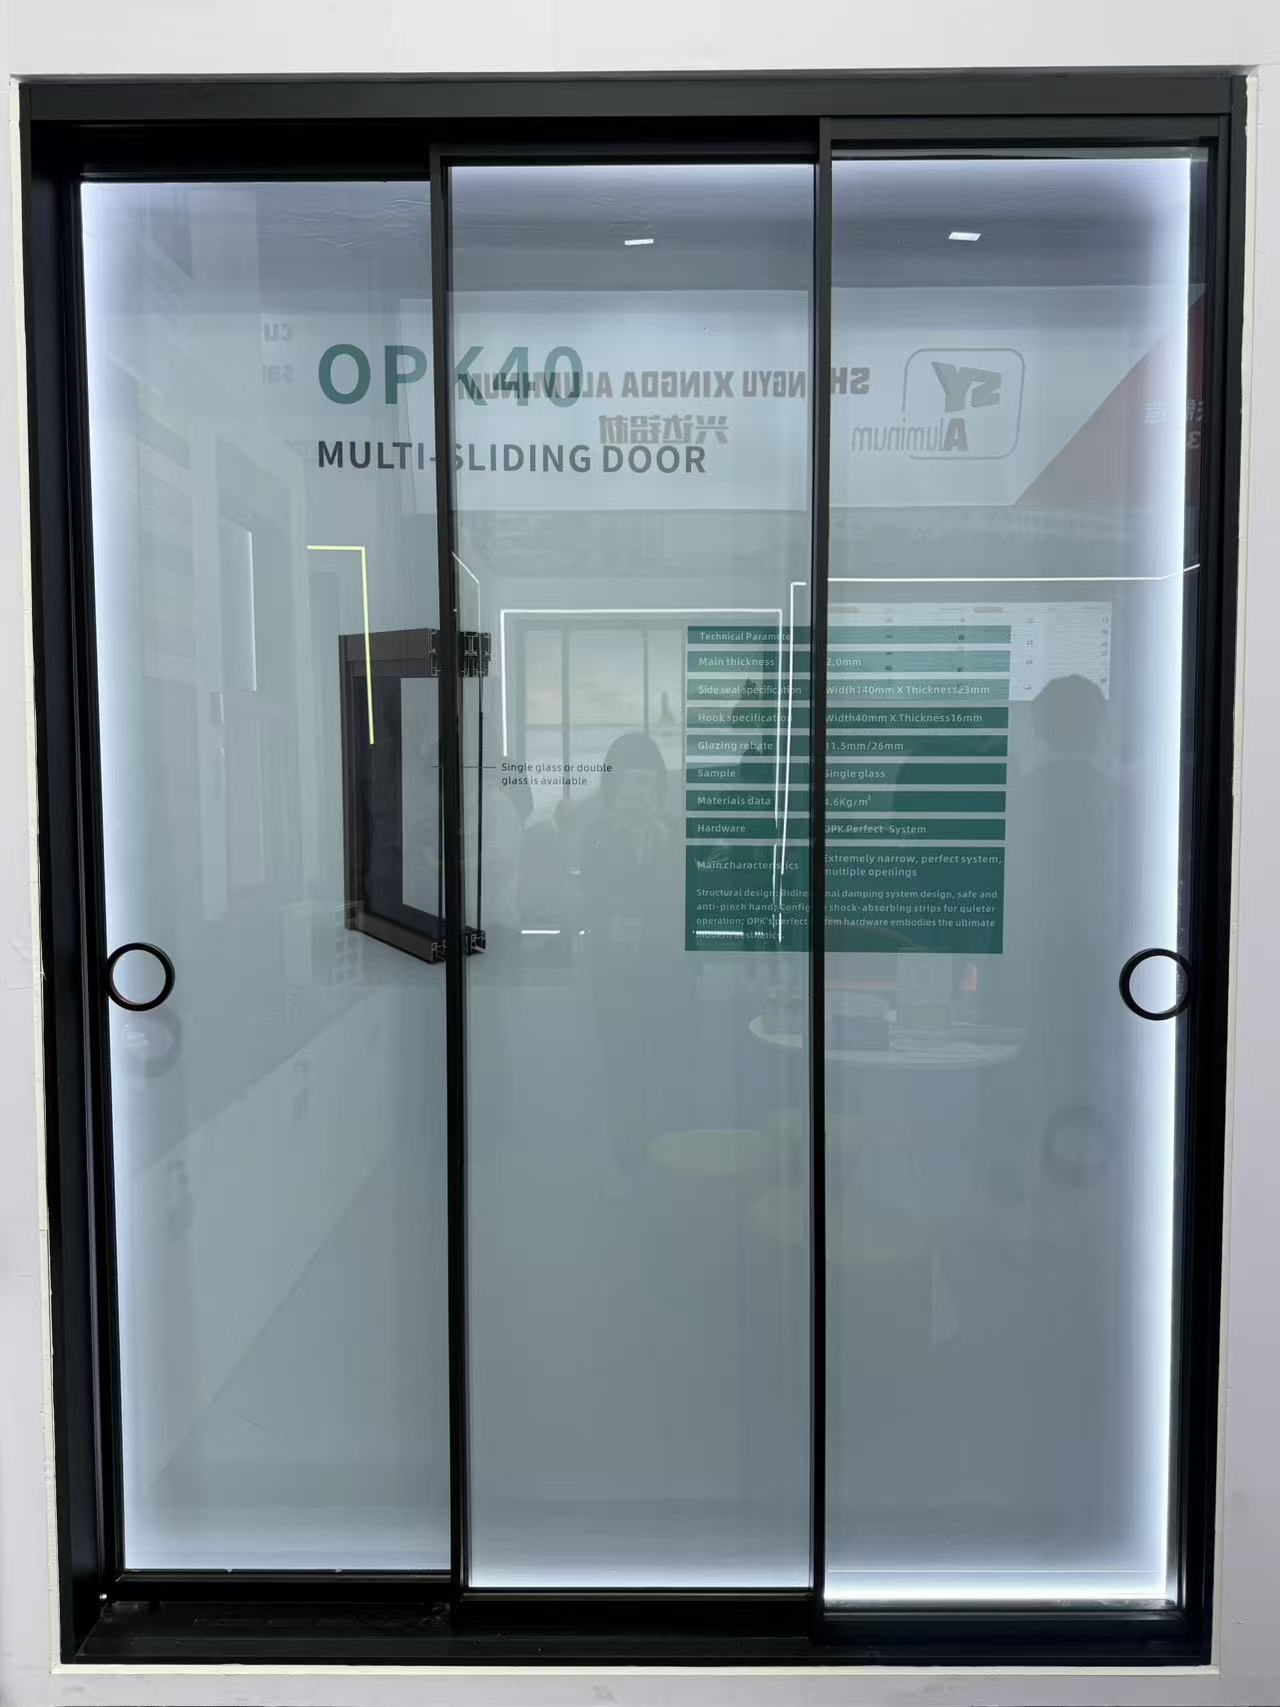
How can I compare Floding door alternatives when supply costs suddenly rise?
Which new Sliding door technologies can lower maintenance costs over time?
How are recycled materials changing the future cost of Floding doors?
How long should a custom Casement door sample normally take to prepare?
What gap between a Sliding window sample and bulk order is acceptable?
Which Decorative profile finishes are becoming more sustainable and cost-effective?
What logistics fees should be listed separately in a Sliding window quote?
How might volatile aluminum prices affect future Sliding window sourcing?
Which audit questions reveal labor risks at a Casement door factory?
Can Decorative profile suppliers provide fast remote guidance for finish defects?
What should a Shutter sample include so I can assess production quality?
Do Sliding door materials need traceability records for customs clearance?
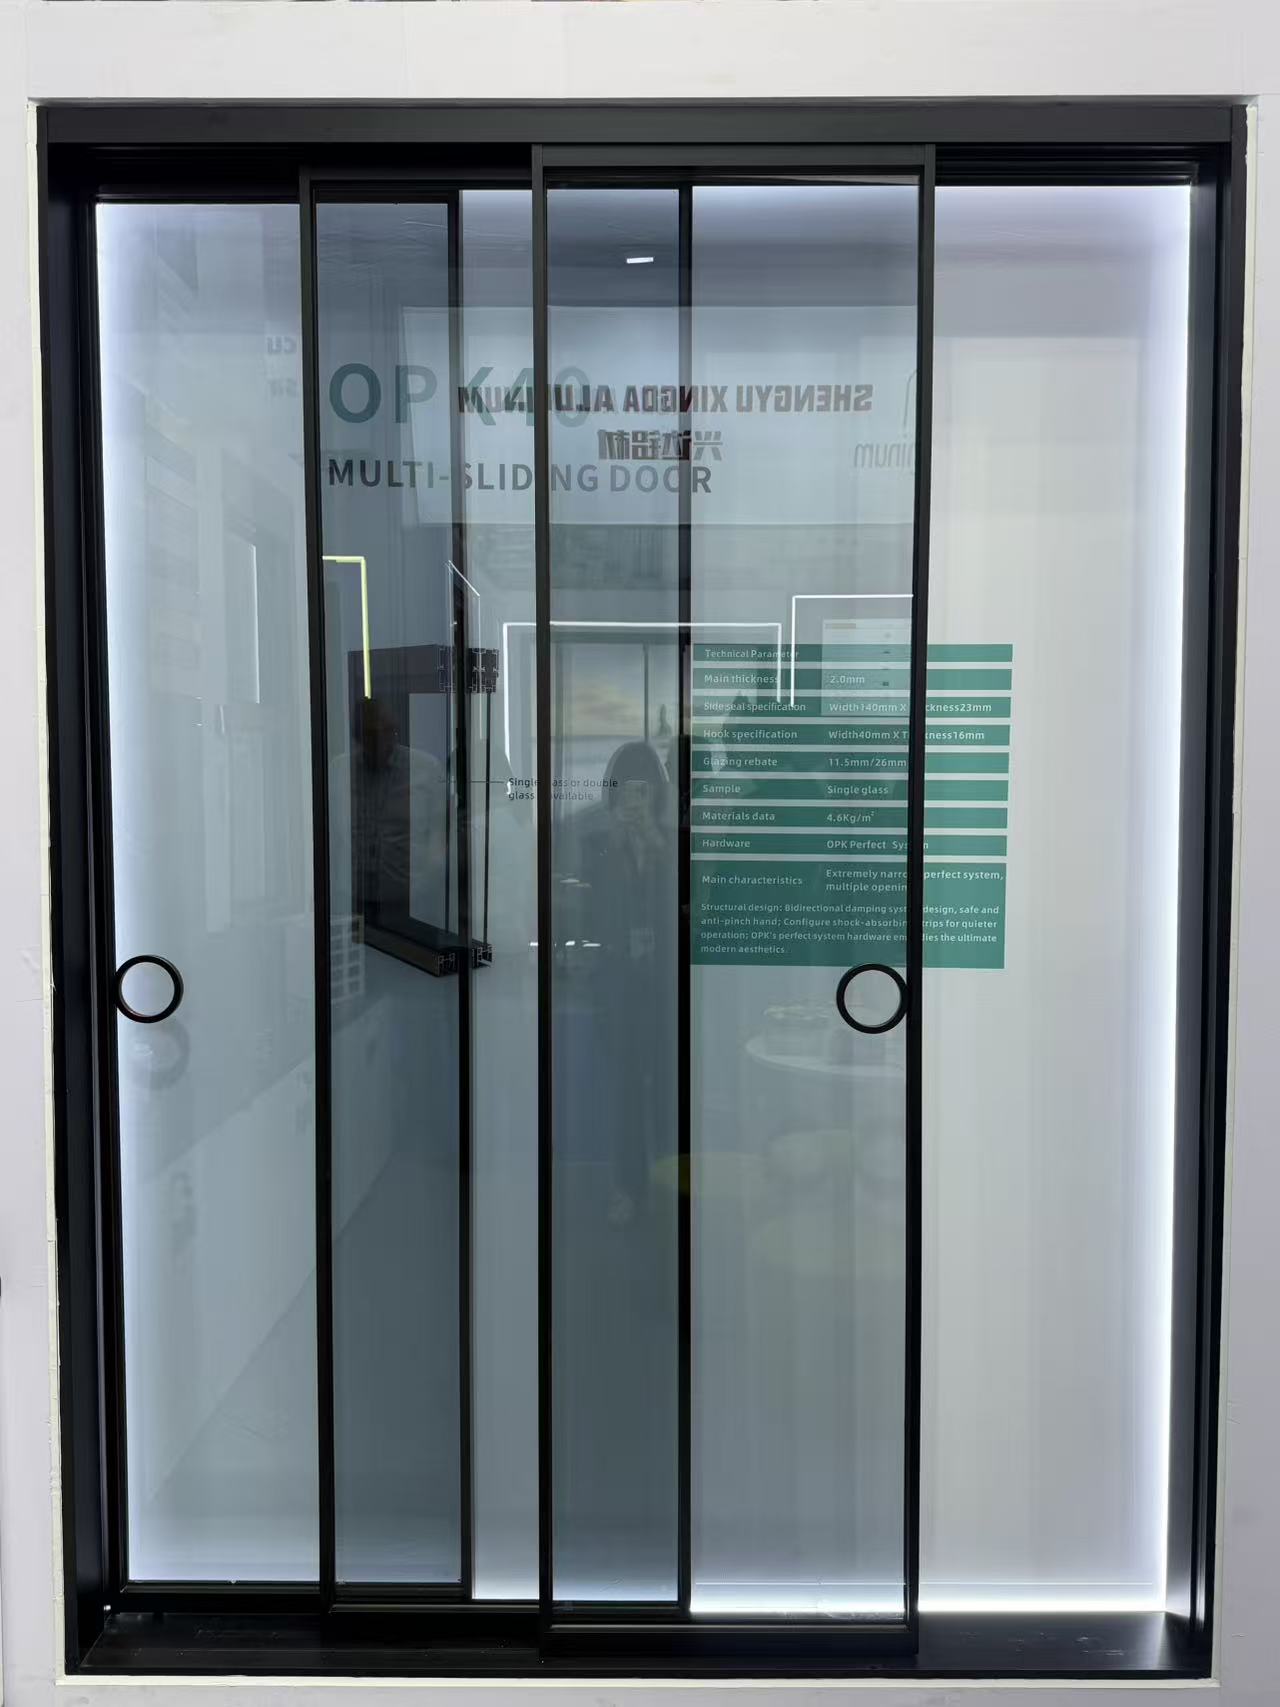
What environmental declarations are useful when importing Architecture profile?
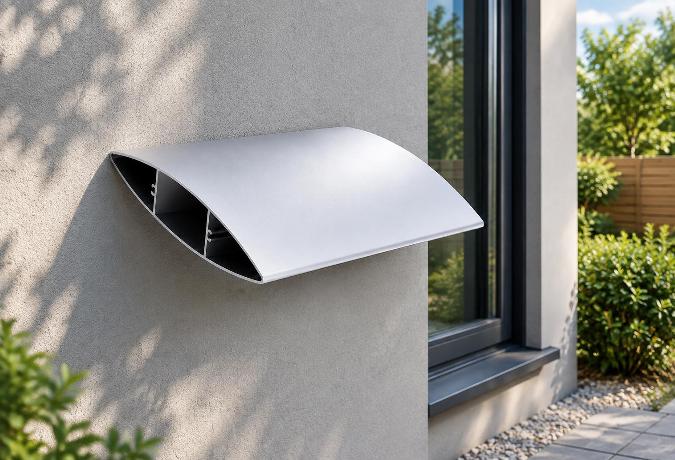
Why Blade Geometry Determines Whether Aluminium Louvers Actually Work
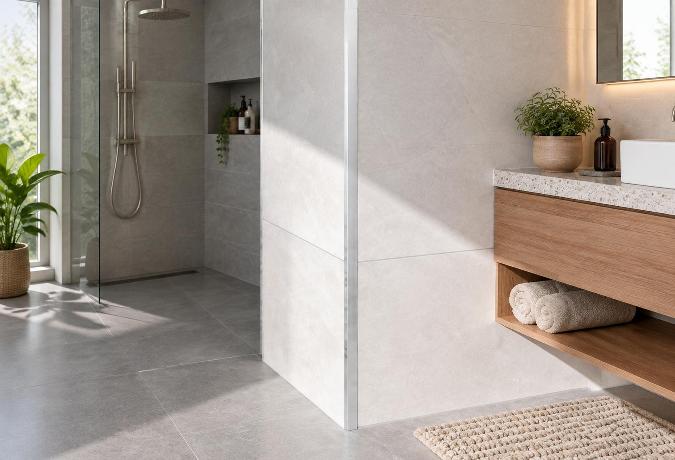
Engineering an Aluminium Angle Profile: Structural Mechanics and Application Realities
What usually drives Architecture profile costs more, alloy or surface treatment?
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
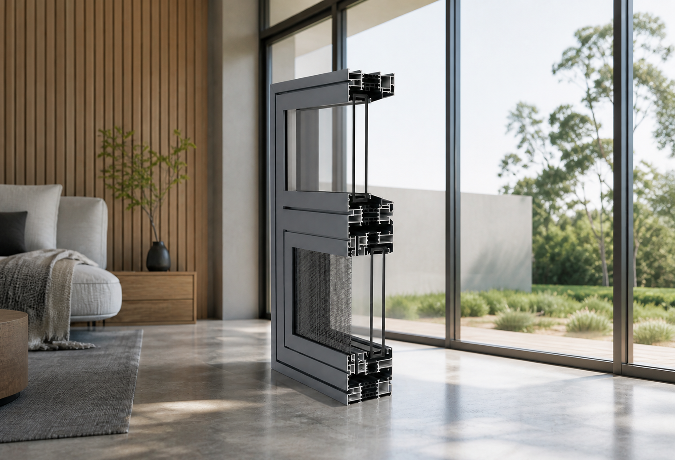
Why the Thermal Break Cavity Matters More Than Frame Thickness in Aluminium Framed Windows and Doors
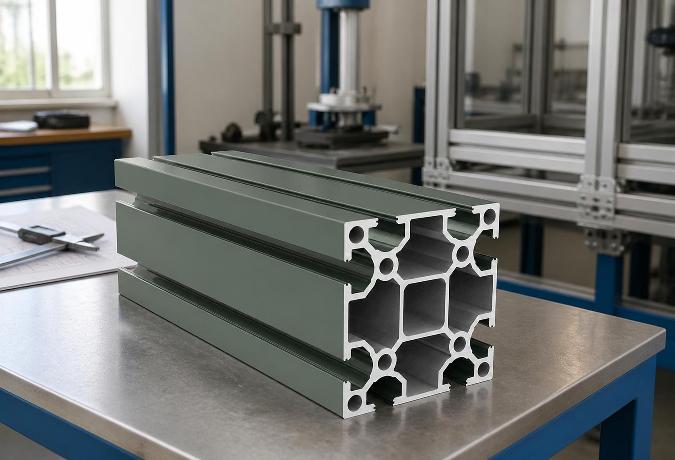
The T-Slot Groove Geometry That Makes Aluminium Framing Weld-Free
Why the One-Piece Molding on Aluminium Trim Profiles Matters More Than the Finish
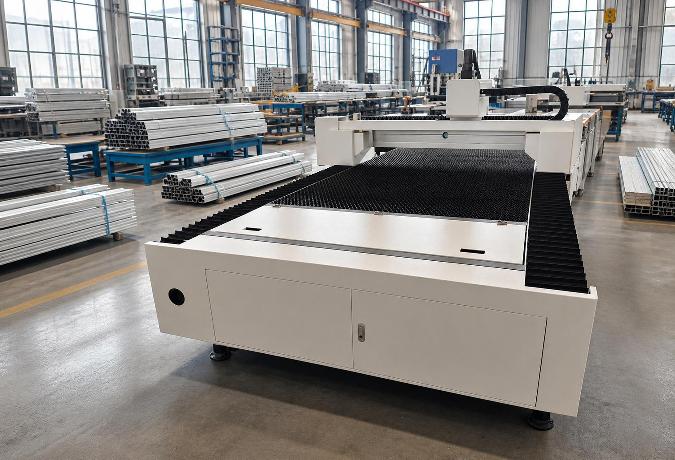
Structural Dynamics of Industrial Aluminium Profiles in Laser Cutting Gantries
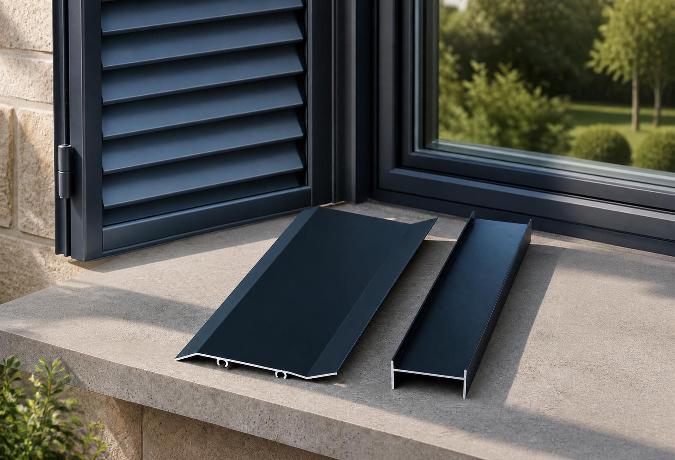
The Engineering Mechanics Behind High-Performance Aluminium Shutters
What factory documents should I request for a Floding door supplier review?
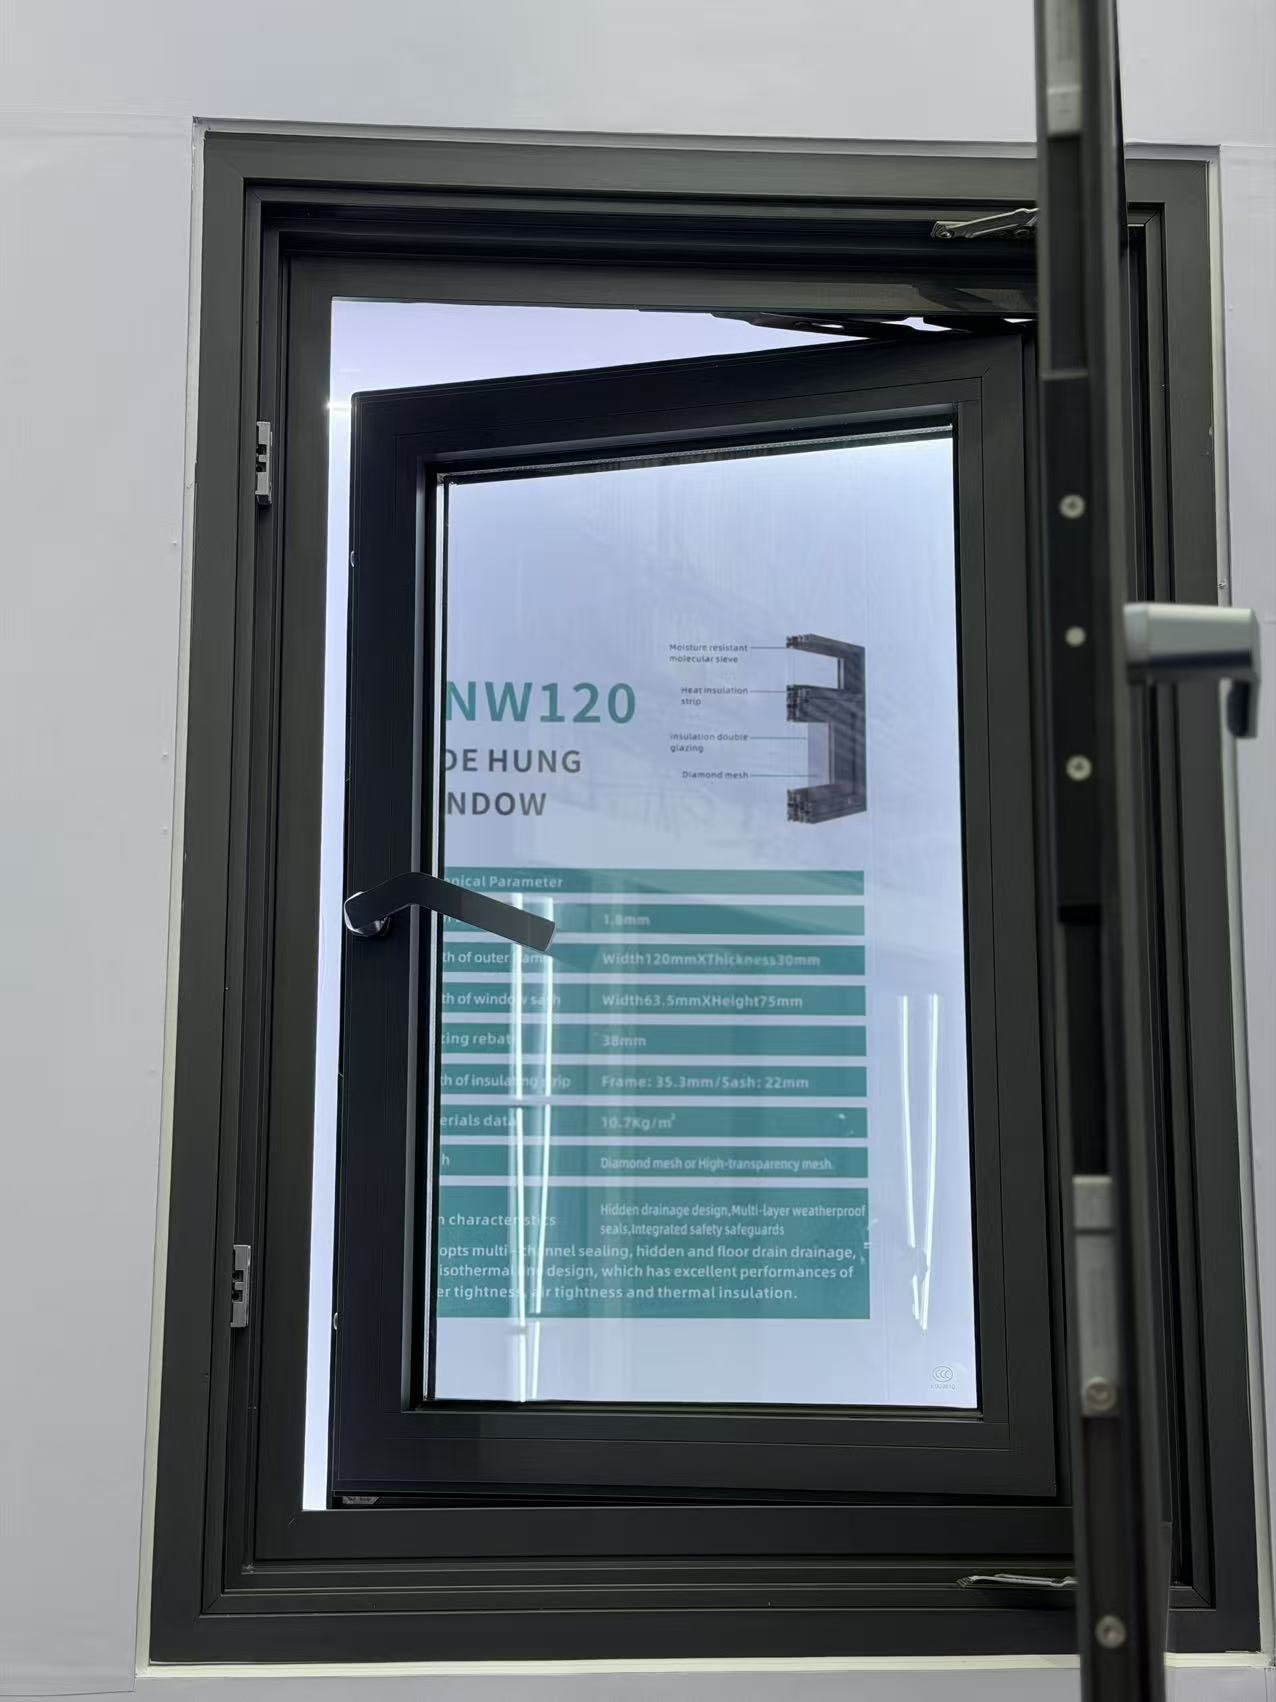
Which delivery term gives me better control over Decorative profile freight costs?
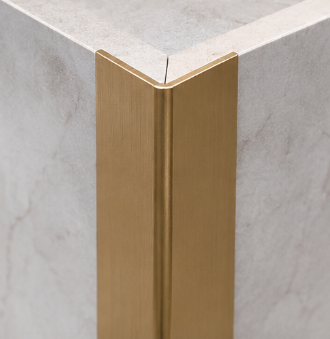
What low-carbon Awing window materials are gaining wider market acceptance?
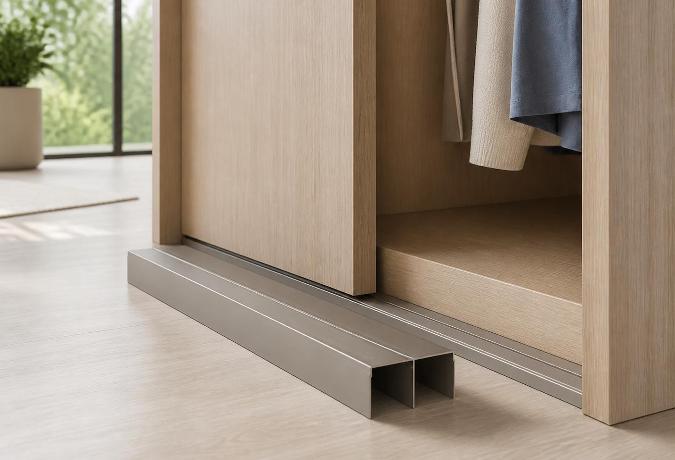
Why Sliding Door Track Geometry Determines Wardrobe Longevity
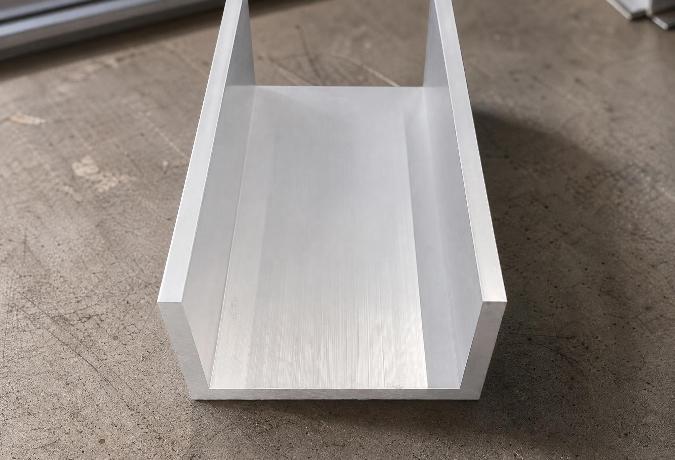
Engineering Mechanics and Surface Dynamics of Aluminium Channel Profiles
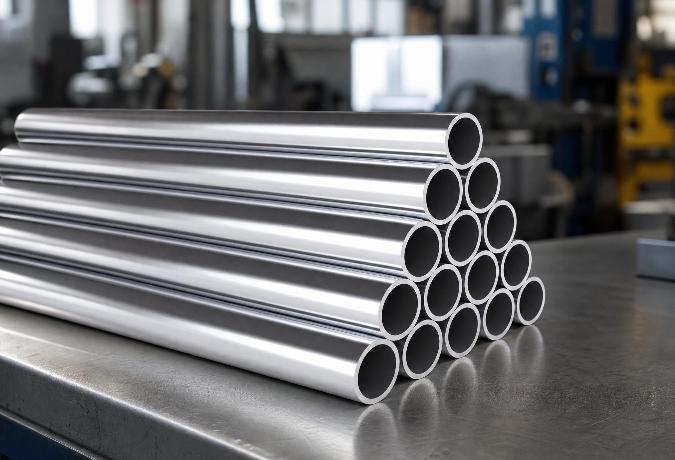
Understanding Aluminium Round Tube Specifications for Structural Engineering
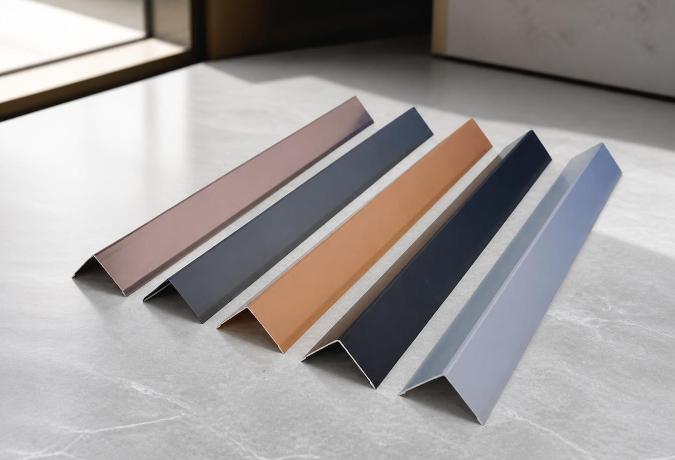
Why the 90-Degree Angle in Standard Aluminium Profiles Determines Structural Reliability
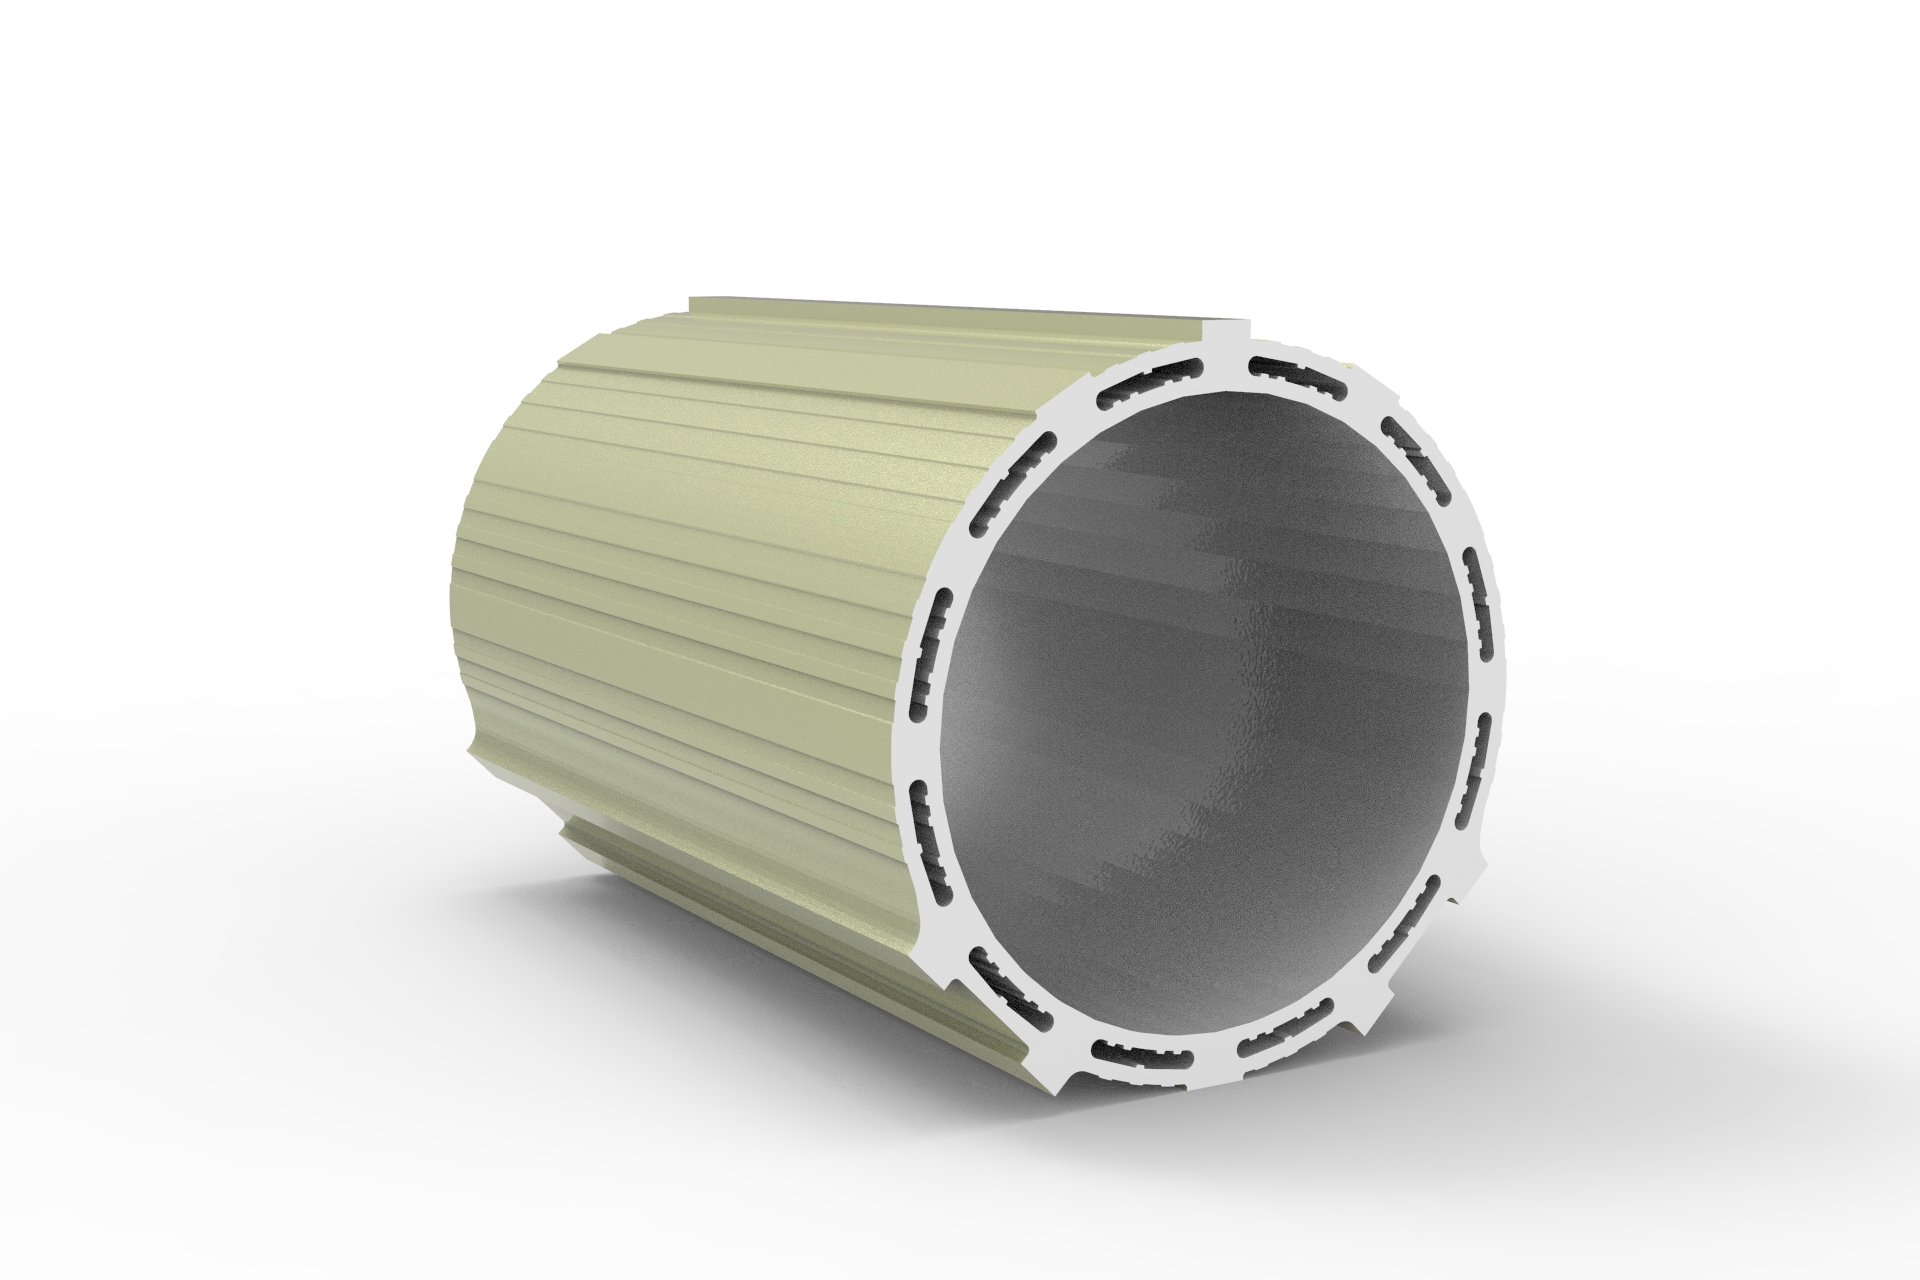
How can I ensure a Floding door sample matches the planned mass production?
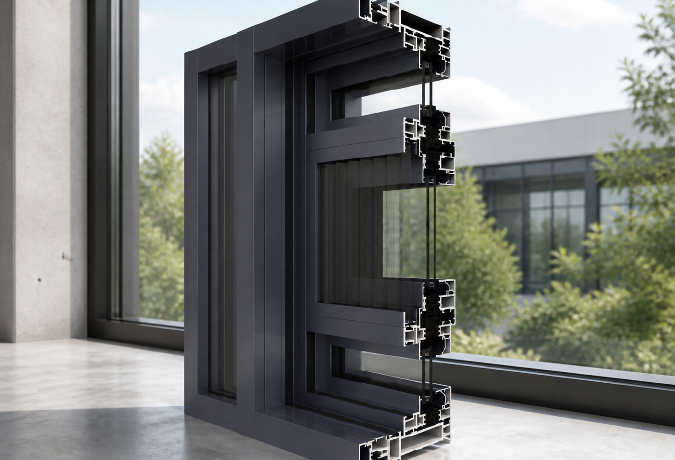
Why Mullion Thickness Determines How Much Glass an Aluminium Curtain Wall Can Actually Hold
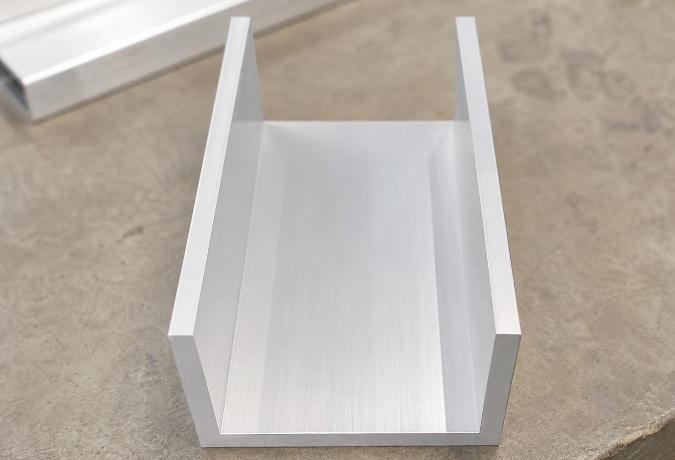
Engineering Dimensional Stability in Aluminium Extrusions for Channel Profiles
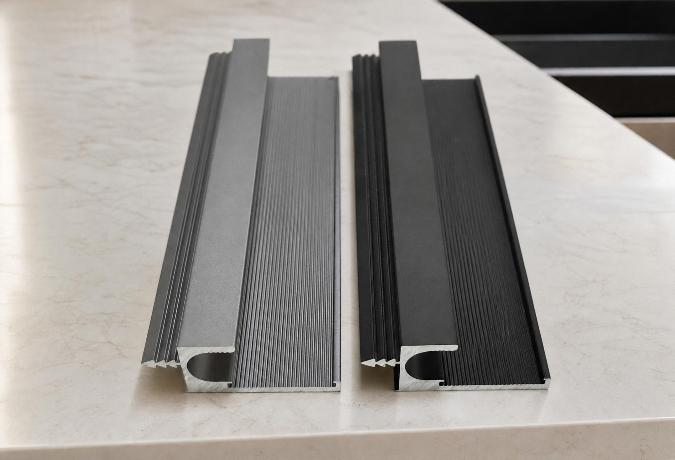
Engineering the Structural Framework: The Mechanics of Aluminium Profiles for Kitchen Cabinets
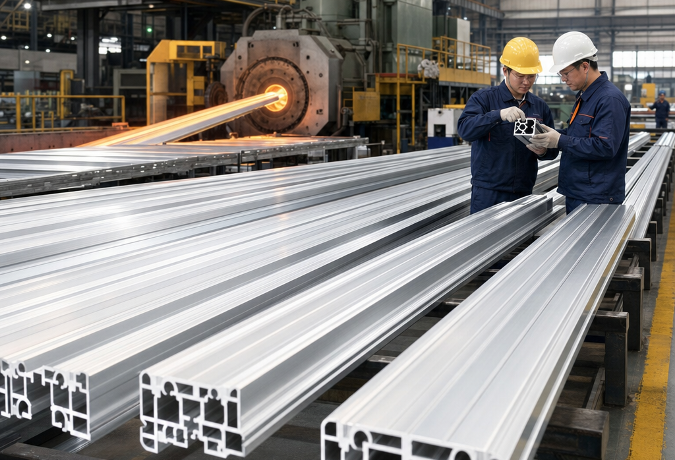
Choosing an Aluminium Profile Supplier: What Actually Separates the Reliable Ones from the Rest
Can Awing window orders ship in batches to avoid project delays?
What response time should I expect for Awing window warranty claims?
Engineering Structural Integrity Through Precision L-Shaped Aluminium Profiles
Thermal Dynamics in High-Power Electronics: Engineering Aluminium Heatsink Profiles
Why the T-Slot Design Determines the Real Strength of Structural Aluminium Extrusions
How long should replacement Sliding window parts remain available after purchase?
Should I expect volume discounts when reordering the same Sliding window model?
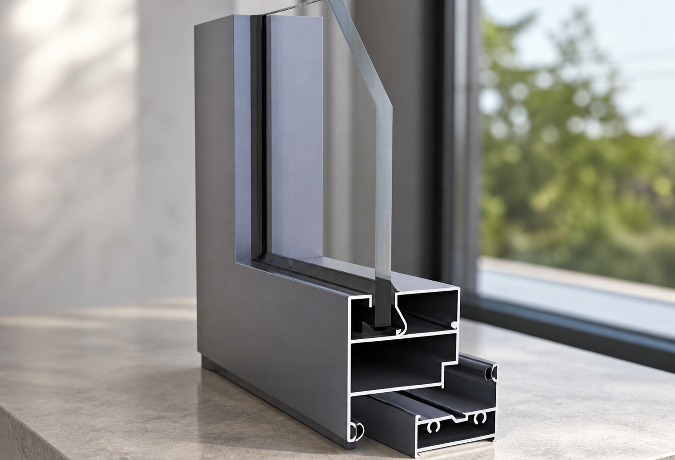
The Multi-Strip Sealing Structure Inside Aluminium Windows and Doors
Engineering Lightweight Rail Structures Through Extruded Aluminium Profiles
Why the Frame Width on an Aluminium Sliding Door Determines Your Room’s Light
The Engineering Behind Decorative Aluminium Profiles: Alloys, Surface Treatments, and Edge Protectio
What alternative materials could make Casement doors more resilient and recyclable?
How can I compare Awing window quotes without missing hidden packing costs?
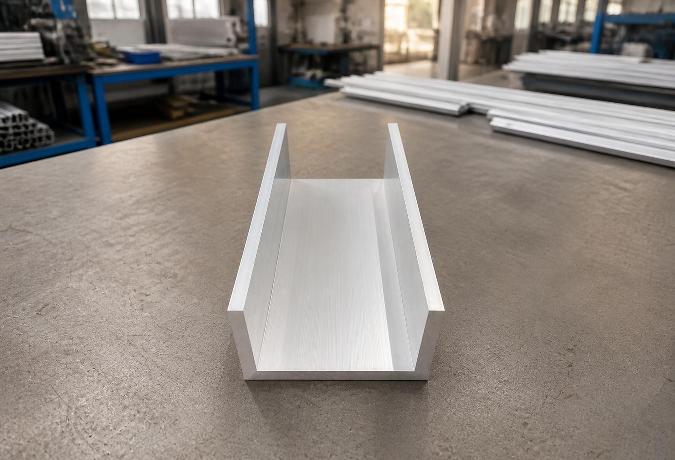
Decoding Structural Tolerances in Aluminium Extrusion Profiles for Channel Applications
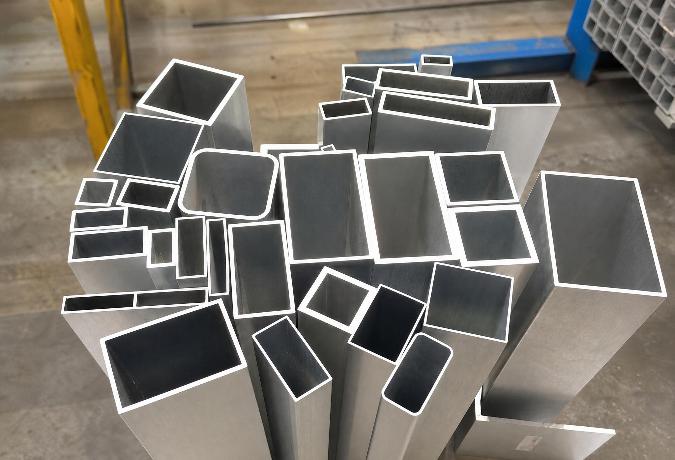
Engineering an Aluminium Square Tube for Modern Structural Integrity
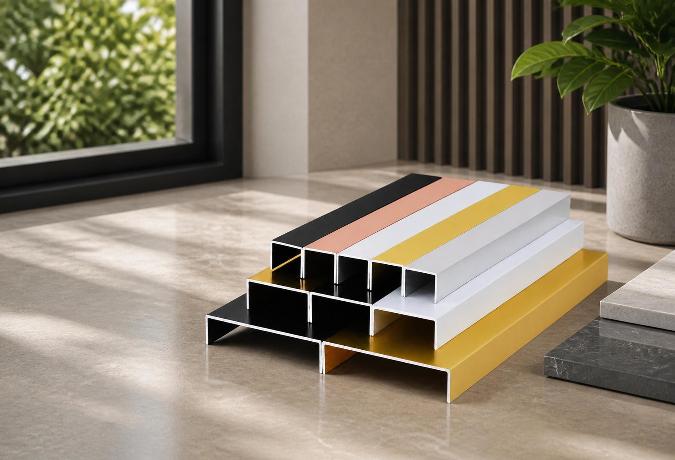
Engineering Tolerances and Alloy Mechanics in Extruded Aluminium Construction Profiles
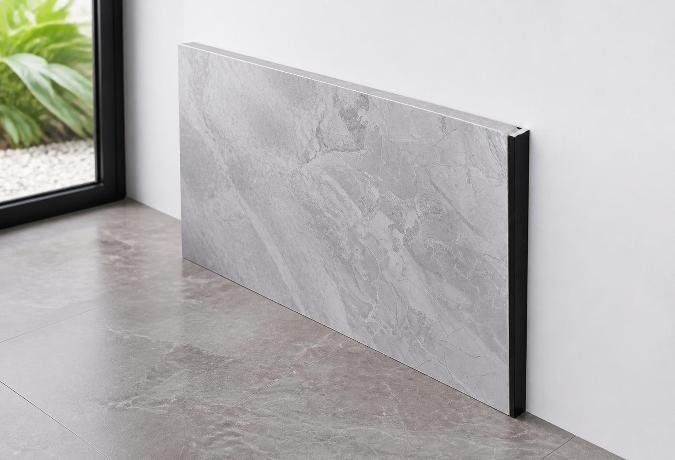
The Engineering Mechanics Behind Aluminium Angle Profiles in Modern Construction
Can an Industrial profile be modified for my assembly without weakening it?
What warning signs suggest a Sliding door seller may disappear after payment?
What energy-efficient alternatives to Casement doors are worth comparing now?
Can a Casement window handle temperature changes without seal failure?
Who pays for unloading and destination handling under Casement door CIF terms?
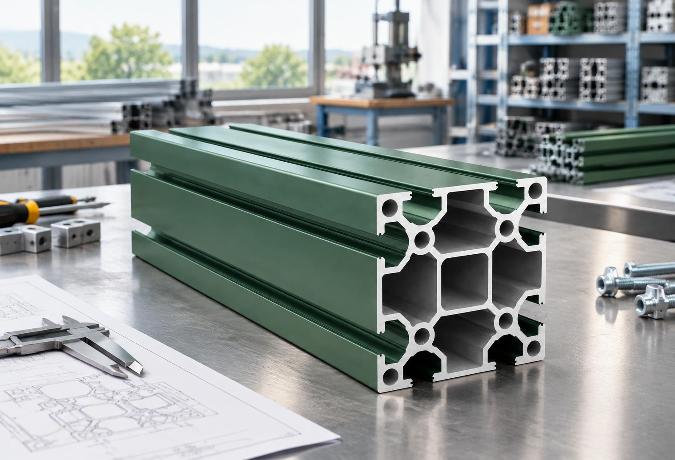
Custom Aluminium Extrusion Profiles: The Engineering Mechanics of T-Slot Frameworks
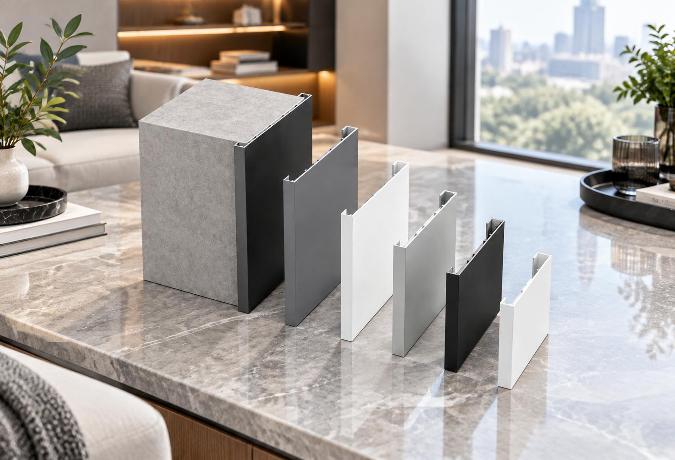
Material Transitions and Geometric Stability in Decorative Aluminium Profiles
Can I negotiate a lower Sliding door MOQ for a showroom launch?
Key Advantages of Using Structural Aluminium Extrusion Profiles in Construction
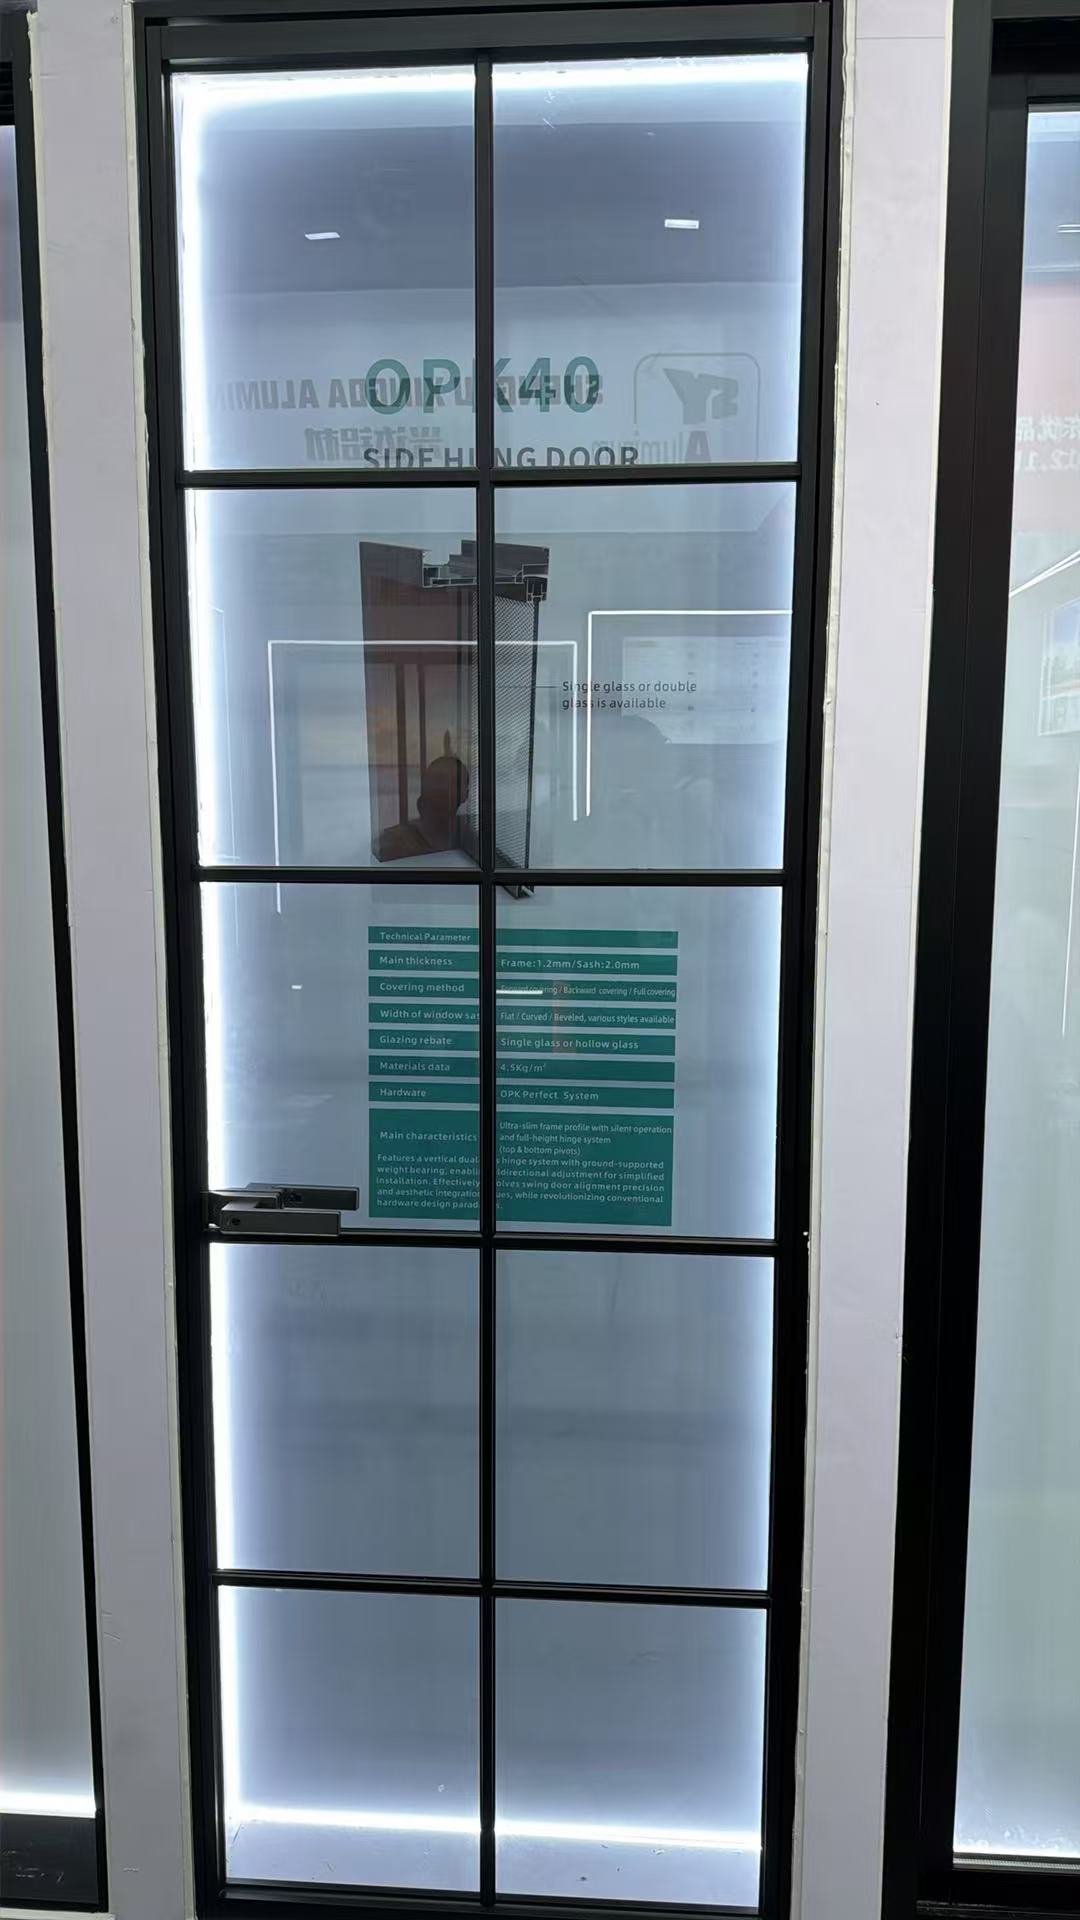
What evidence shows an Awing window factory manages coating waste properly?
How can I protect my deposit when ordering custom Decorative profile?
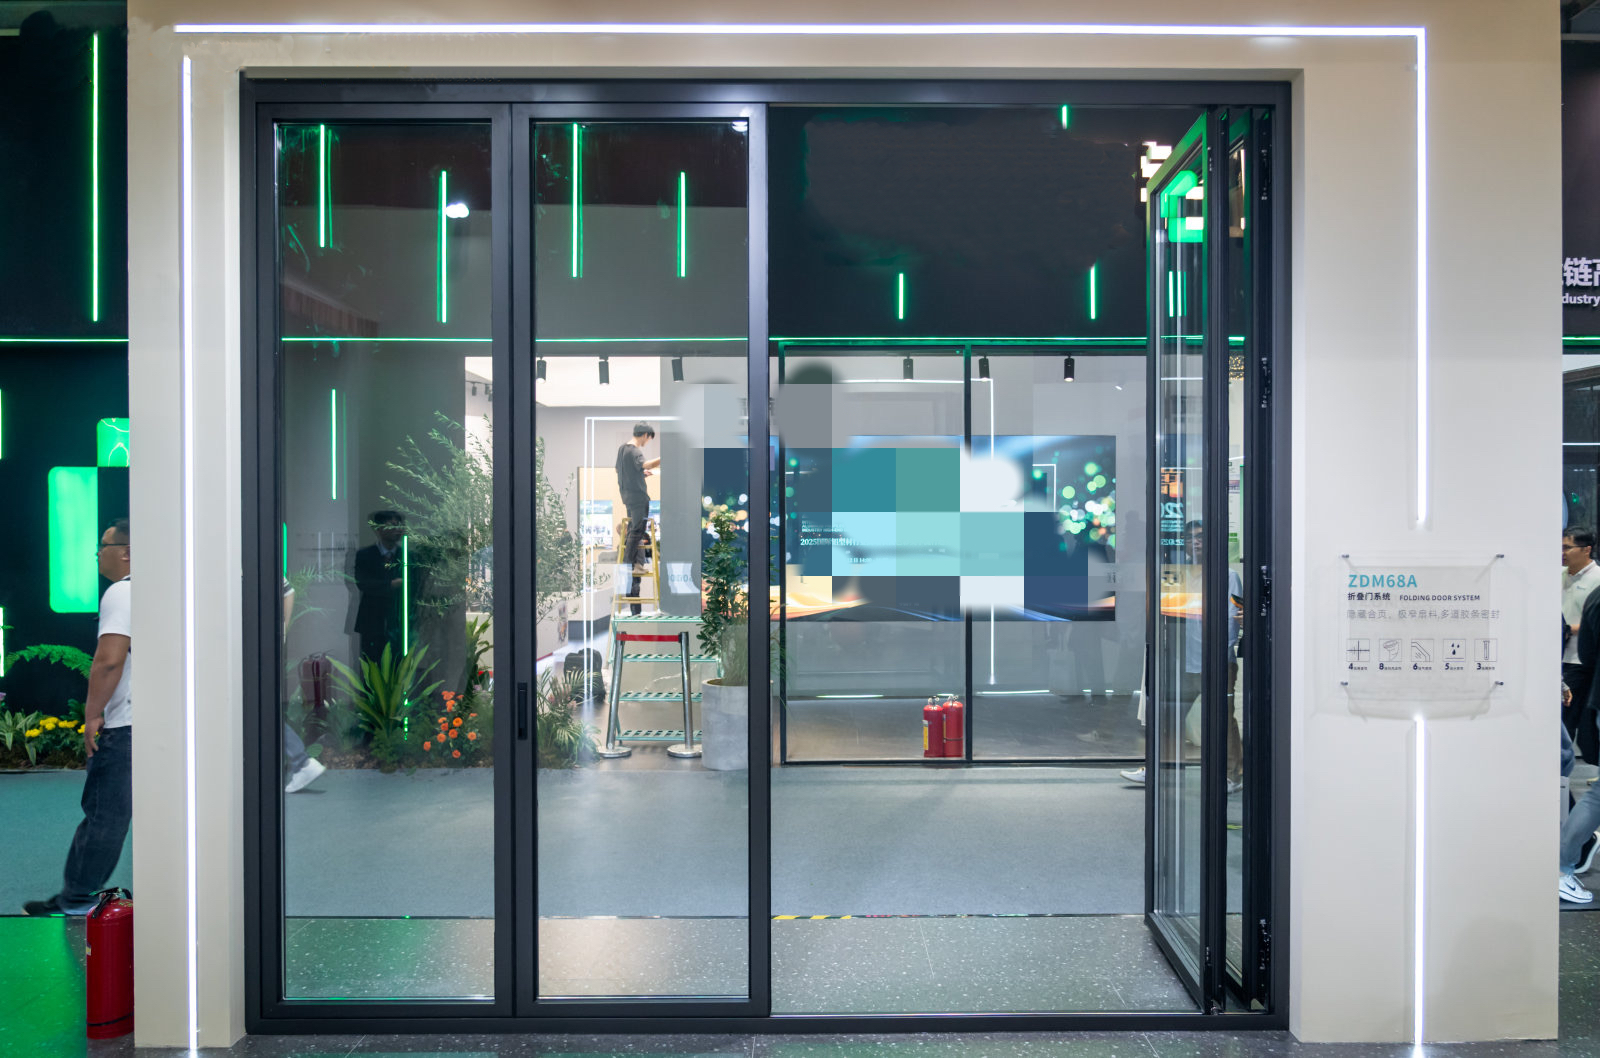
How do I spot unusually low Industrial profile prices before committing funds?
How can I check that a Shutter supplier is not using unapproved subcontractors?
What contract terms protect my Casement door drawings and branding?
How can I compare Casement door insulation ratings before placing an order?
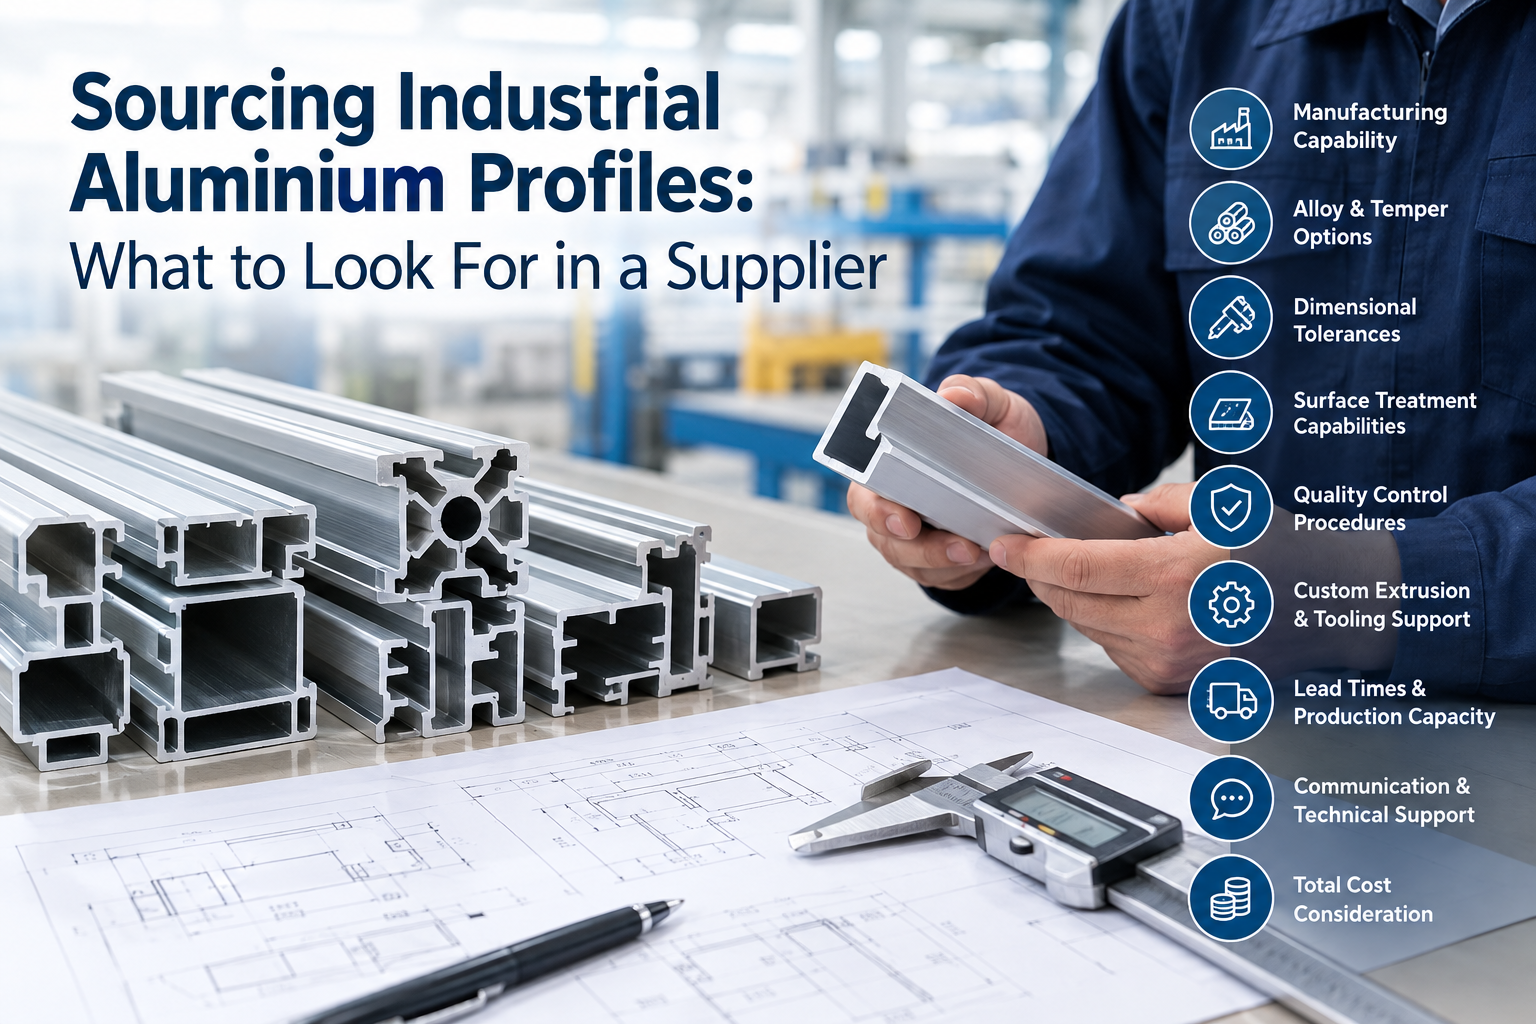
Sourcing Industrial Aluminium Profiles: What to Look For in a Supplier
How do I keep ownership of a custom Architecture profile extrusion die?
The Energy Efficiency Benefits of an Aluminium Frame Sliding Glass Window
How do I check Industrial profile alloy grades against the shipping documents?
What Casement window warranty period is reasonable for an overseas buyer?
How are defective Sliding window units usually replaced internationally?
How can I reduce breakage risks when shipping Casement windows overseas?
The Structural Mechanics Behind Decorative Aluminium Profiles
How Do Engineers Select Industrial Aluminium Profiles for High-Load Frameworks?
What payment structure reduces my risk on a first Industrial profile order?
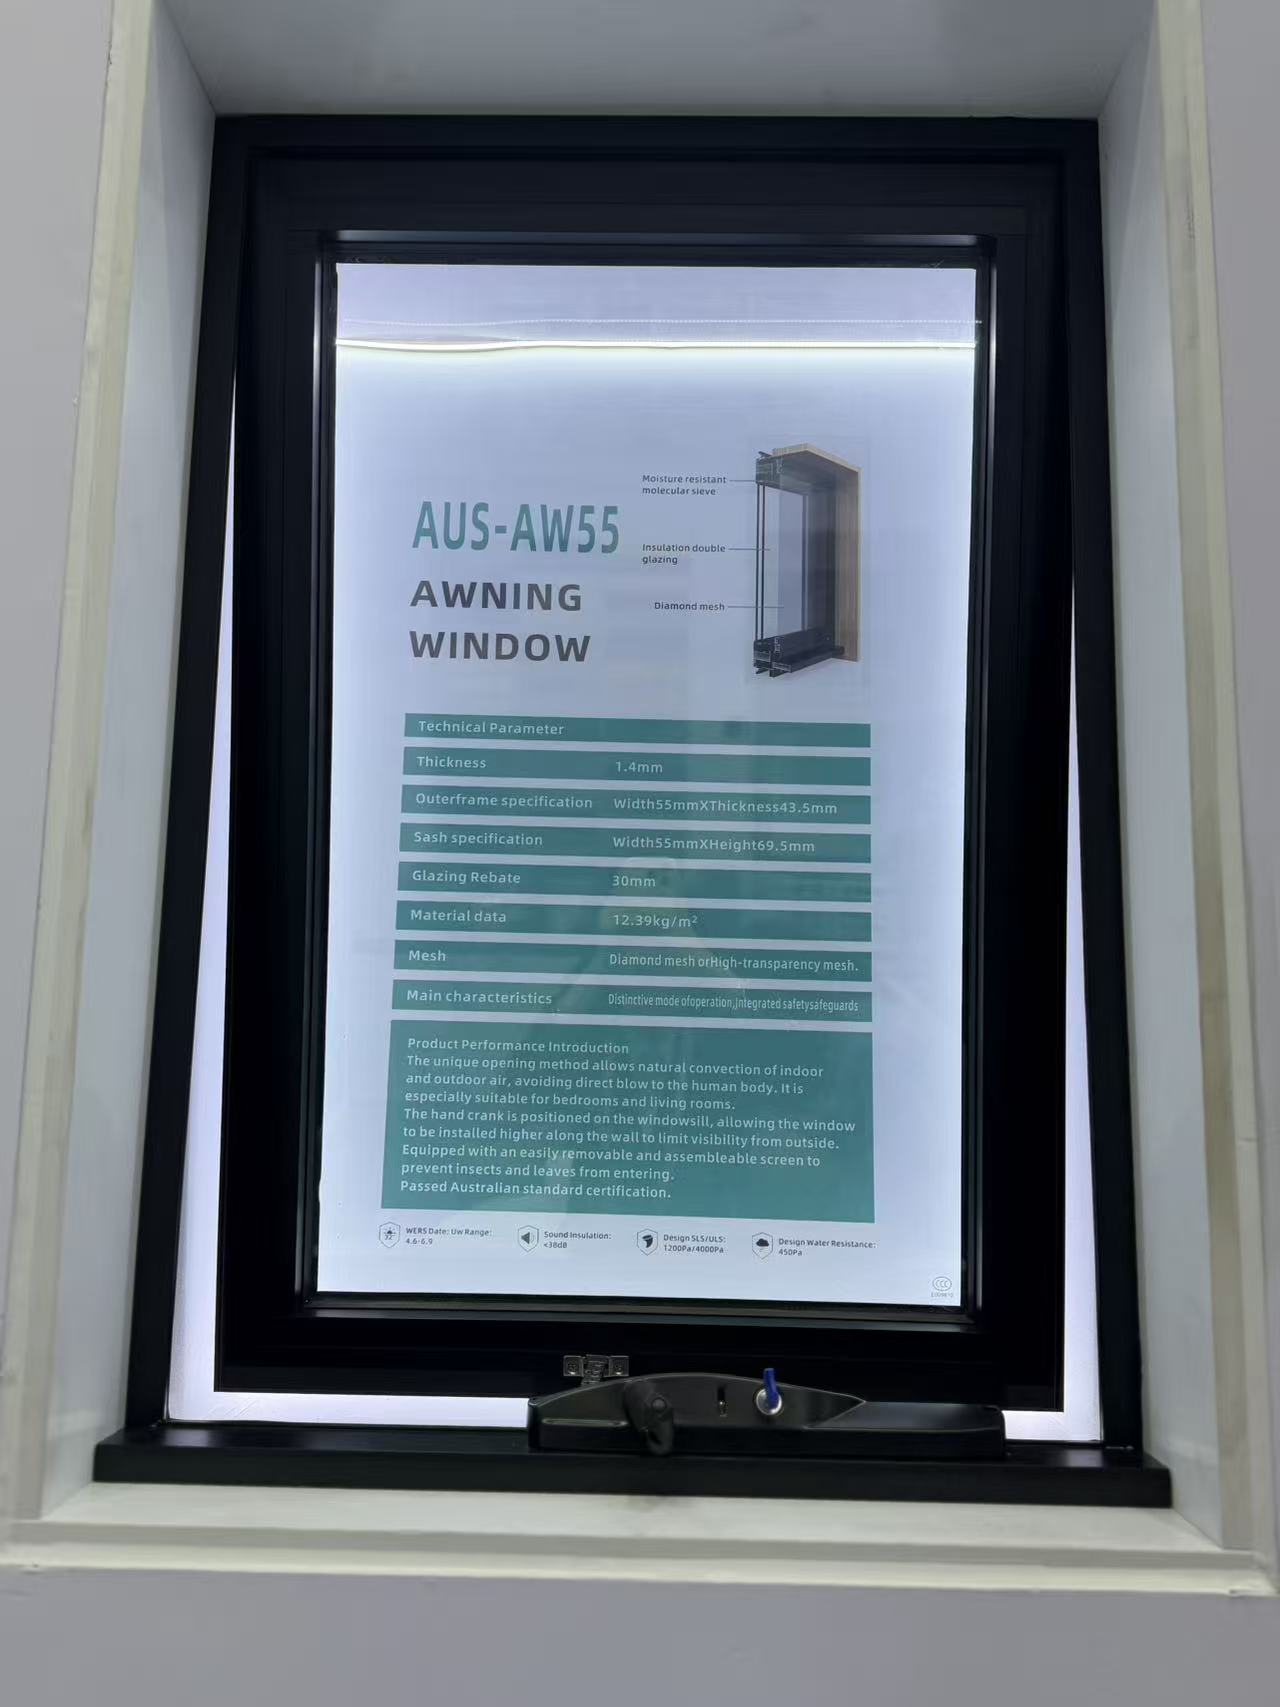
Should I approve a Casement window sample before checking its hardware strength?
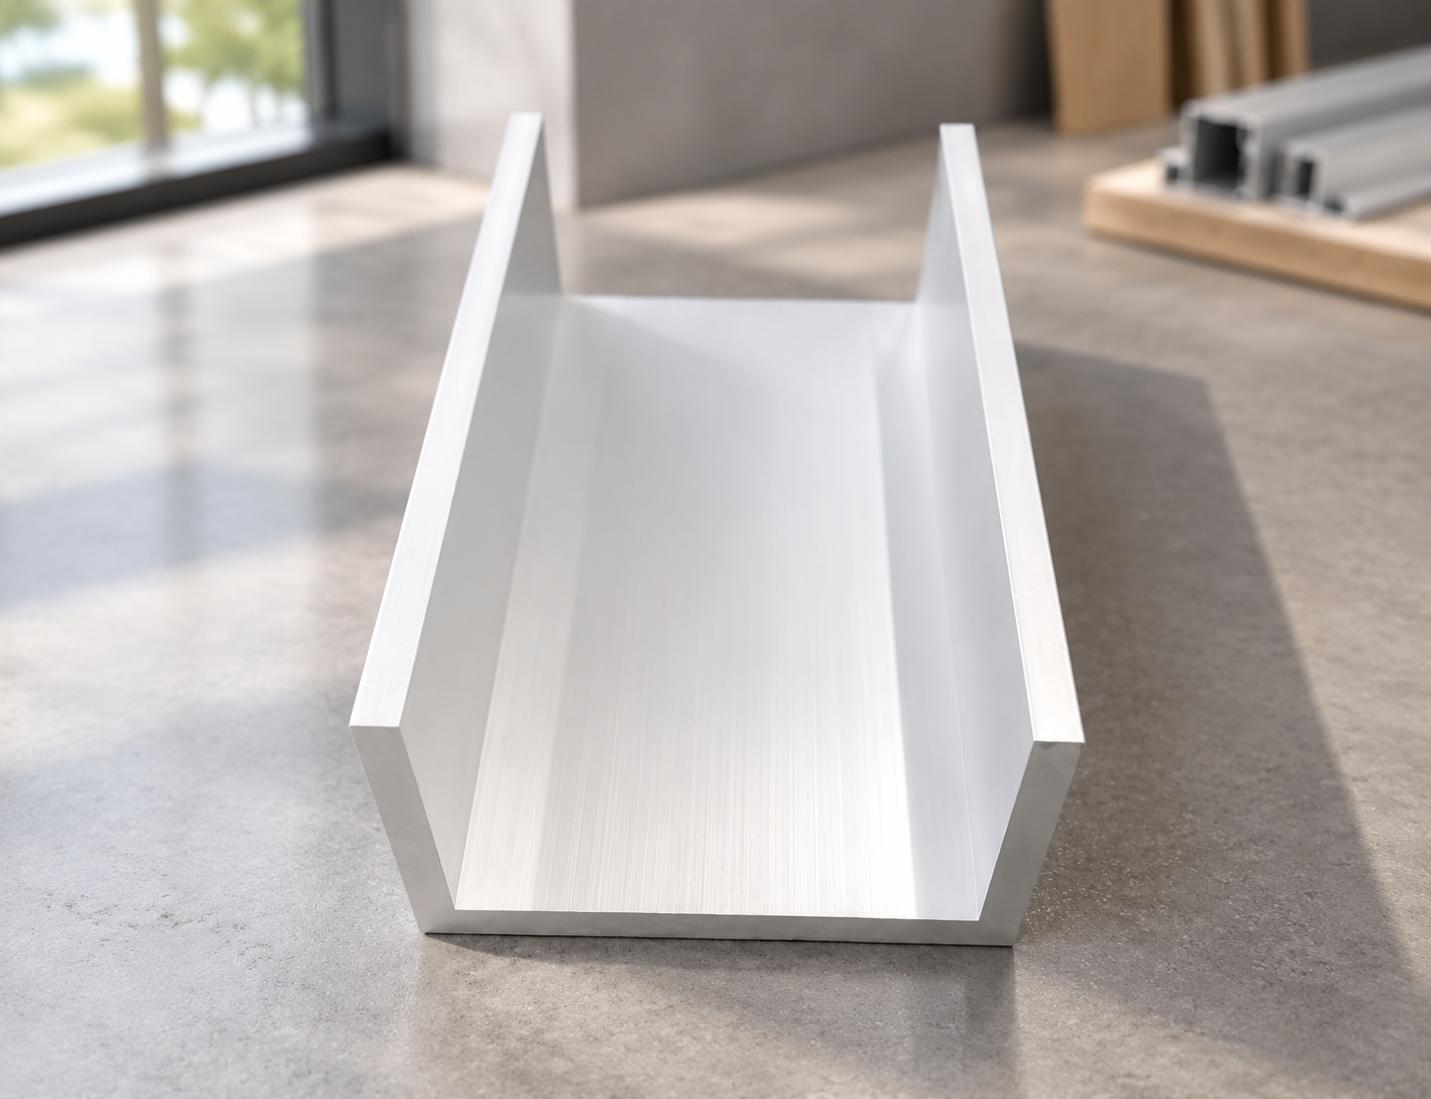
Structural Mechanics of Channel Extrusions in Architectural Aluminium Profiles
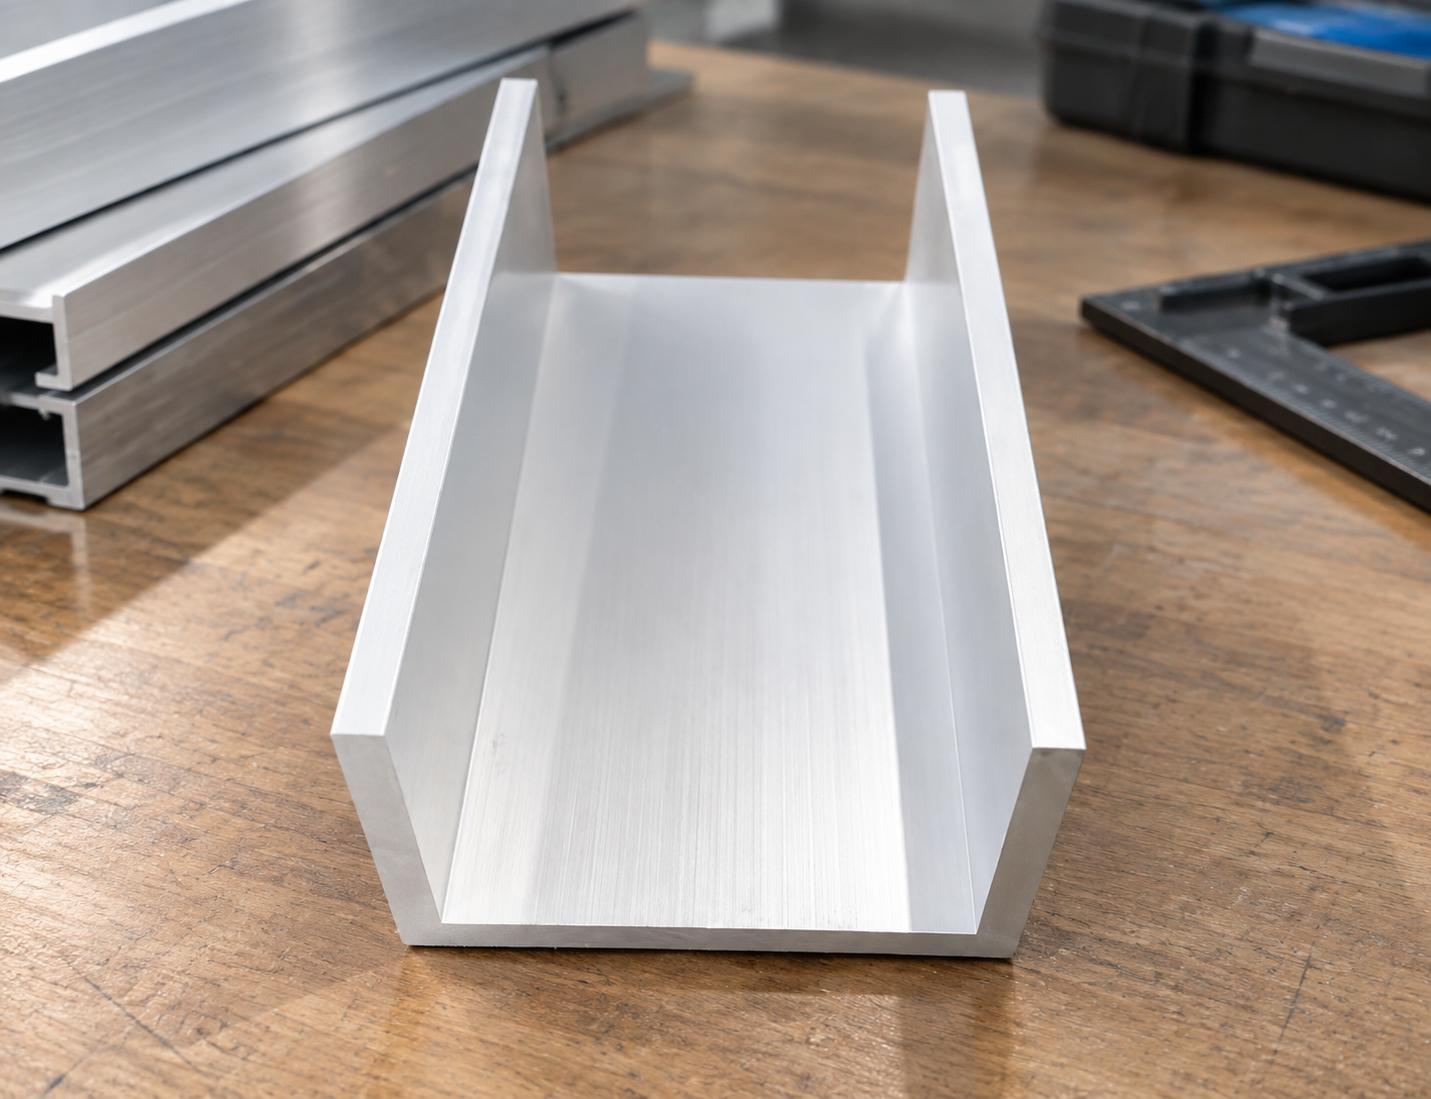
Engineering Mechanics of Aluminium Extrusion Profiles in Channel Systems
What functional tests should I perform on a Sliding door prototype?
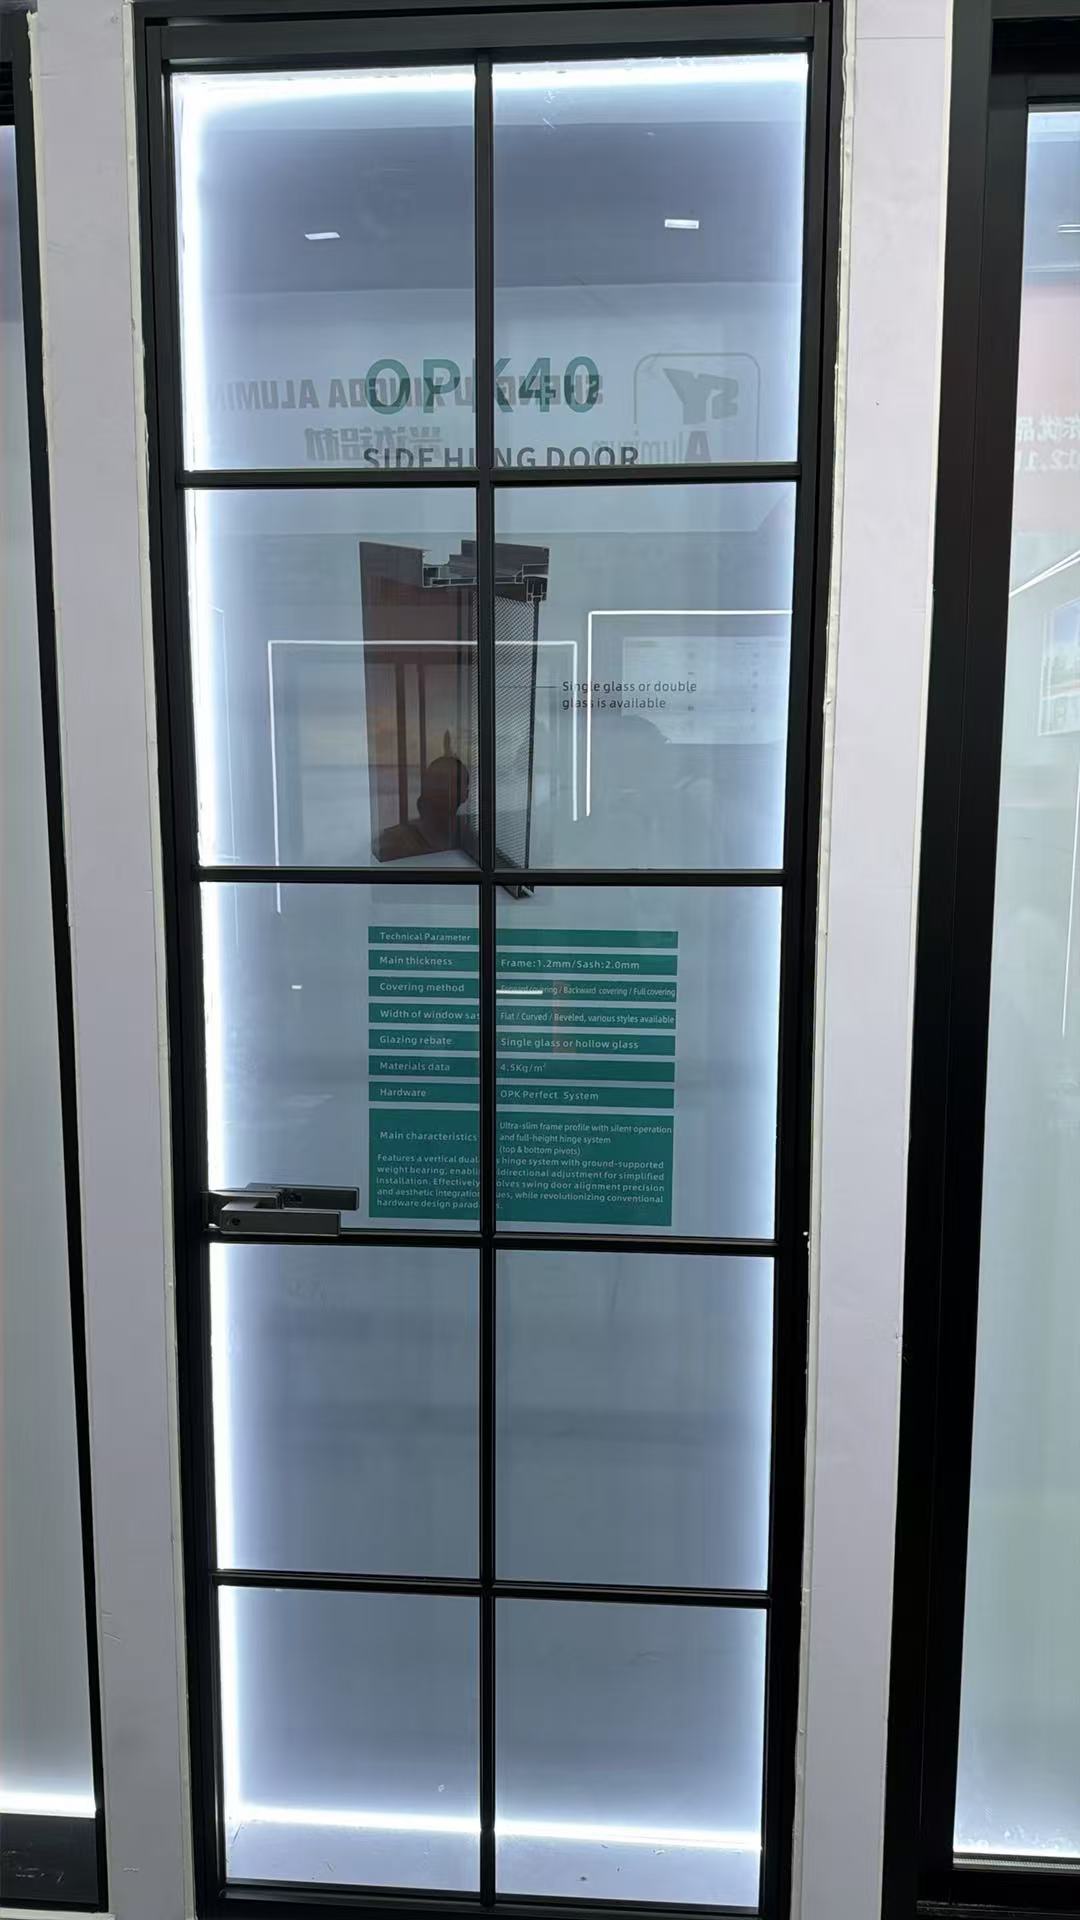
What payment terms are fair when Decorative profile colors remain unconfirmed?
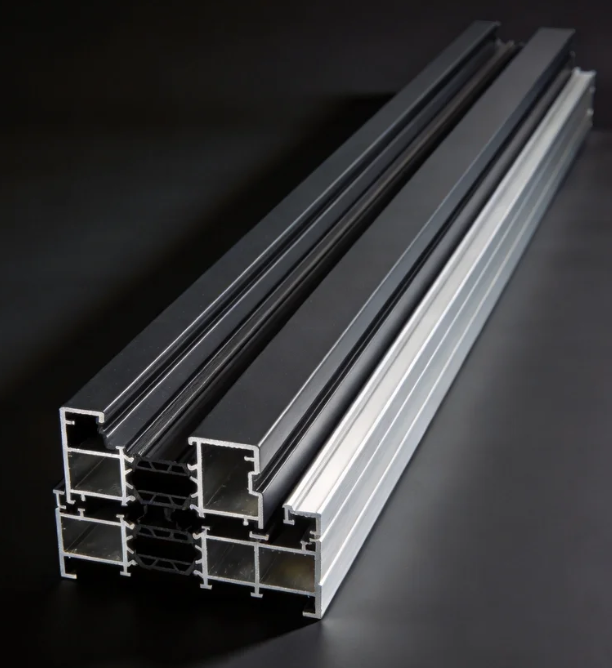
Is a letter of credit practical for a large Casement window shipment?
How should Industrial profile bundles be packed to prevent transit damage?
Which safety documents should I request for Awing window imports?
What shipping delays commonly affect Architecture profile orders during peak season?
How to Specify Extruded Aluminium Profiles: Costs, Alloys, and Tolerances
Is a Floding door suitable for a wide opening exposed to strong winds?
Structural Integrity in Modular Design: Engineering T-Slot Aluminium Extrusion Profiles
Resolving Corner Stress: The Engineering Mechanics Behind Aluminium Profiles in Architectural Framin
How do Floding door prices change with glass, hardware, and finish choices?
How can I prove Shutter defects remotely without returning every unit?
How can I shorten Awing window sampling without losing critical tests?
Does ordering mixed Shutter sizes usually change the unit price or MOQ?
How should Industrial profile warranty responsibility be shared after assembly?
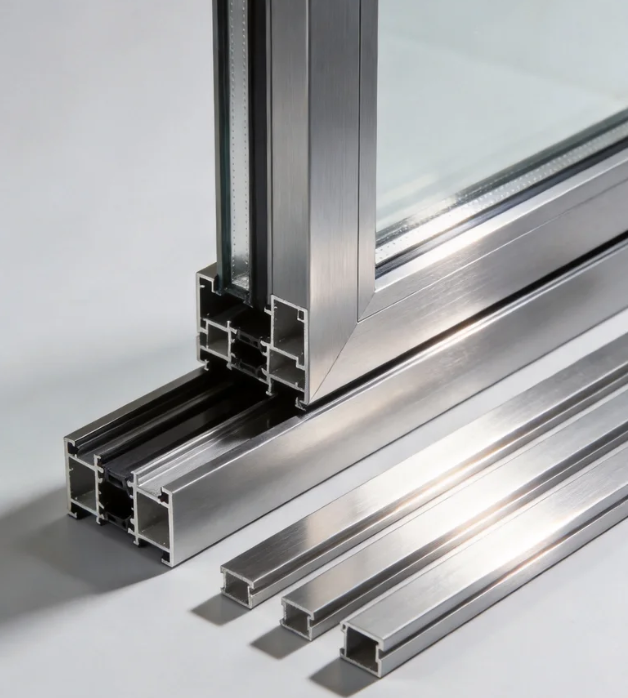
How should I plan Shutter inventory when ocean freight schedules change?
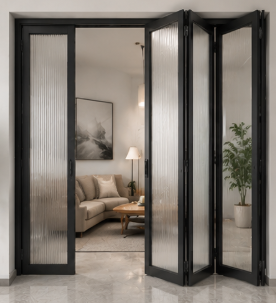
How do escrow arrangements reduce risk for a new Floding door supplier?
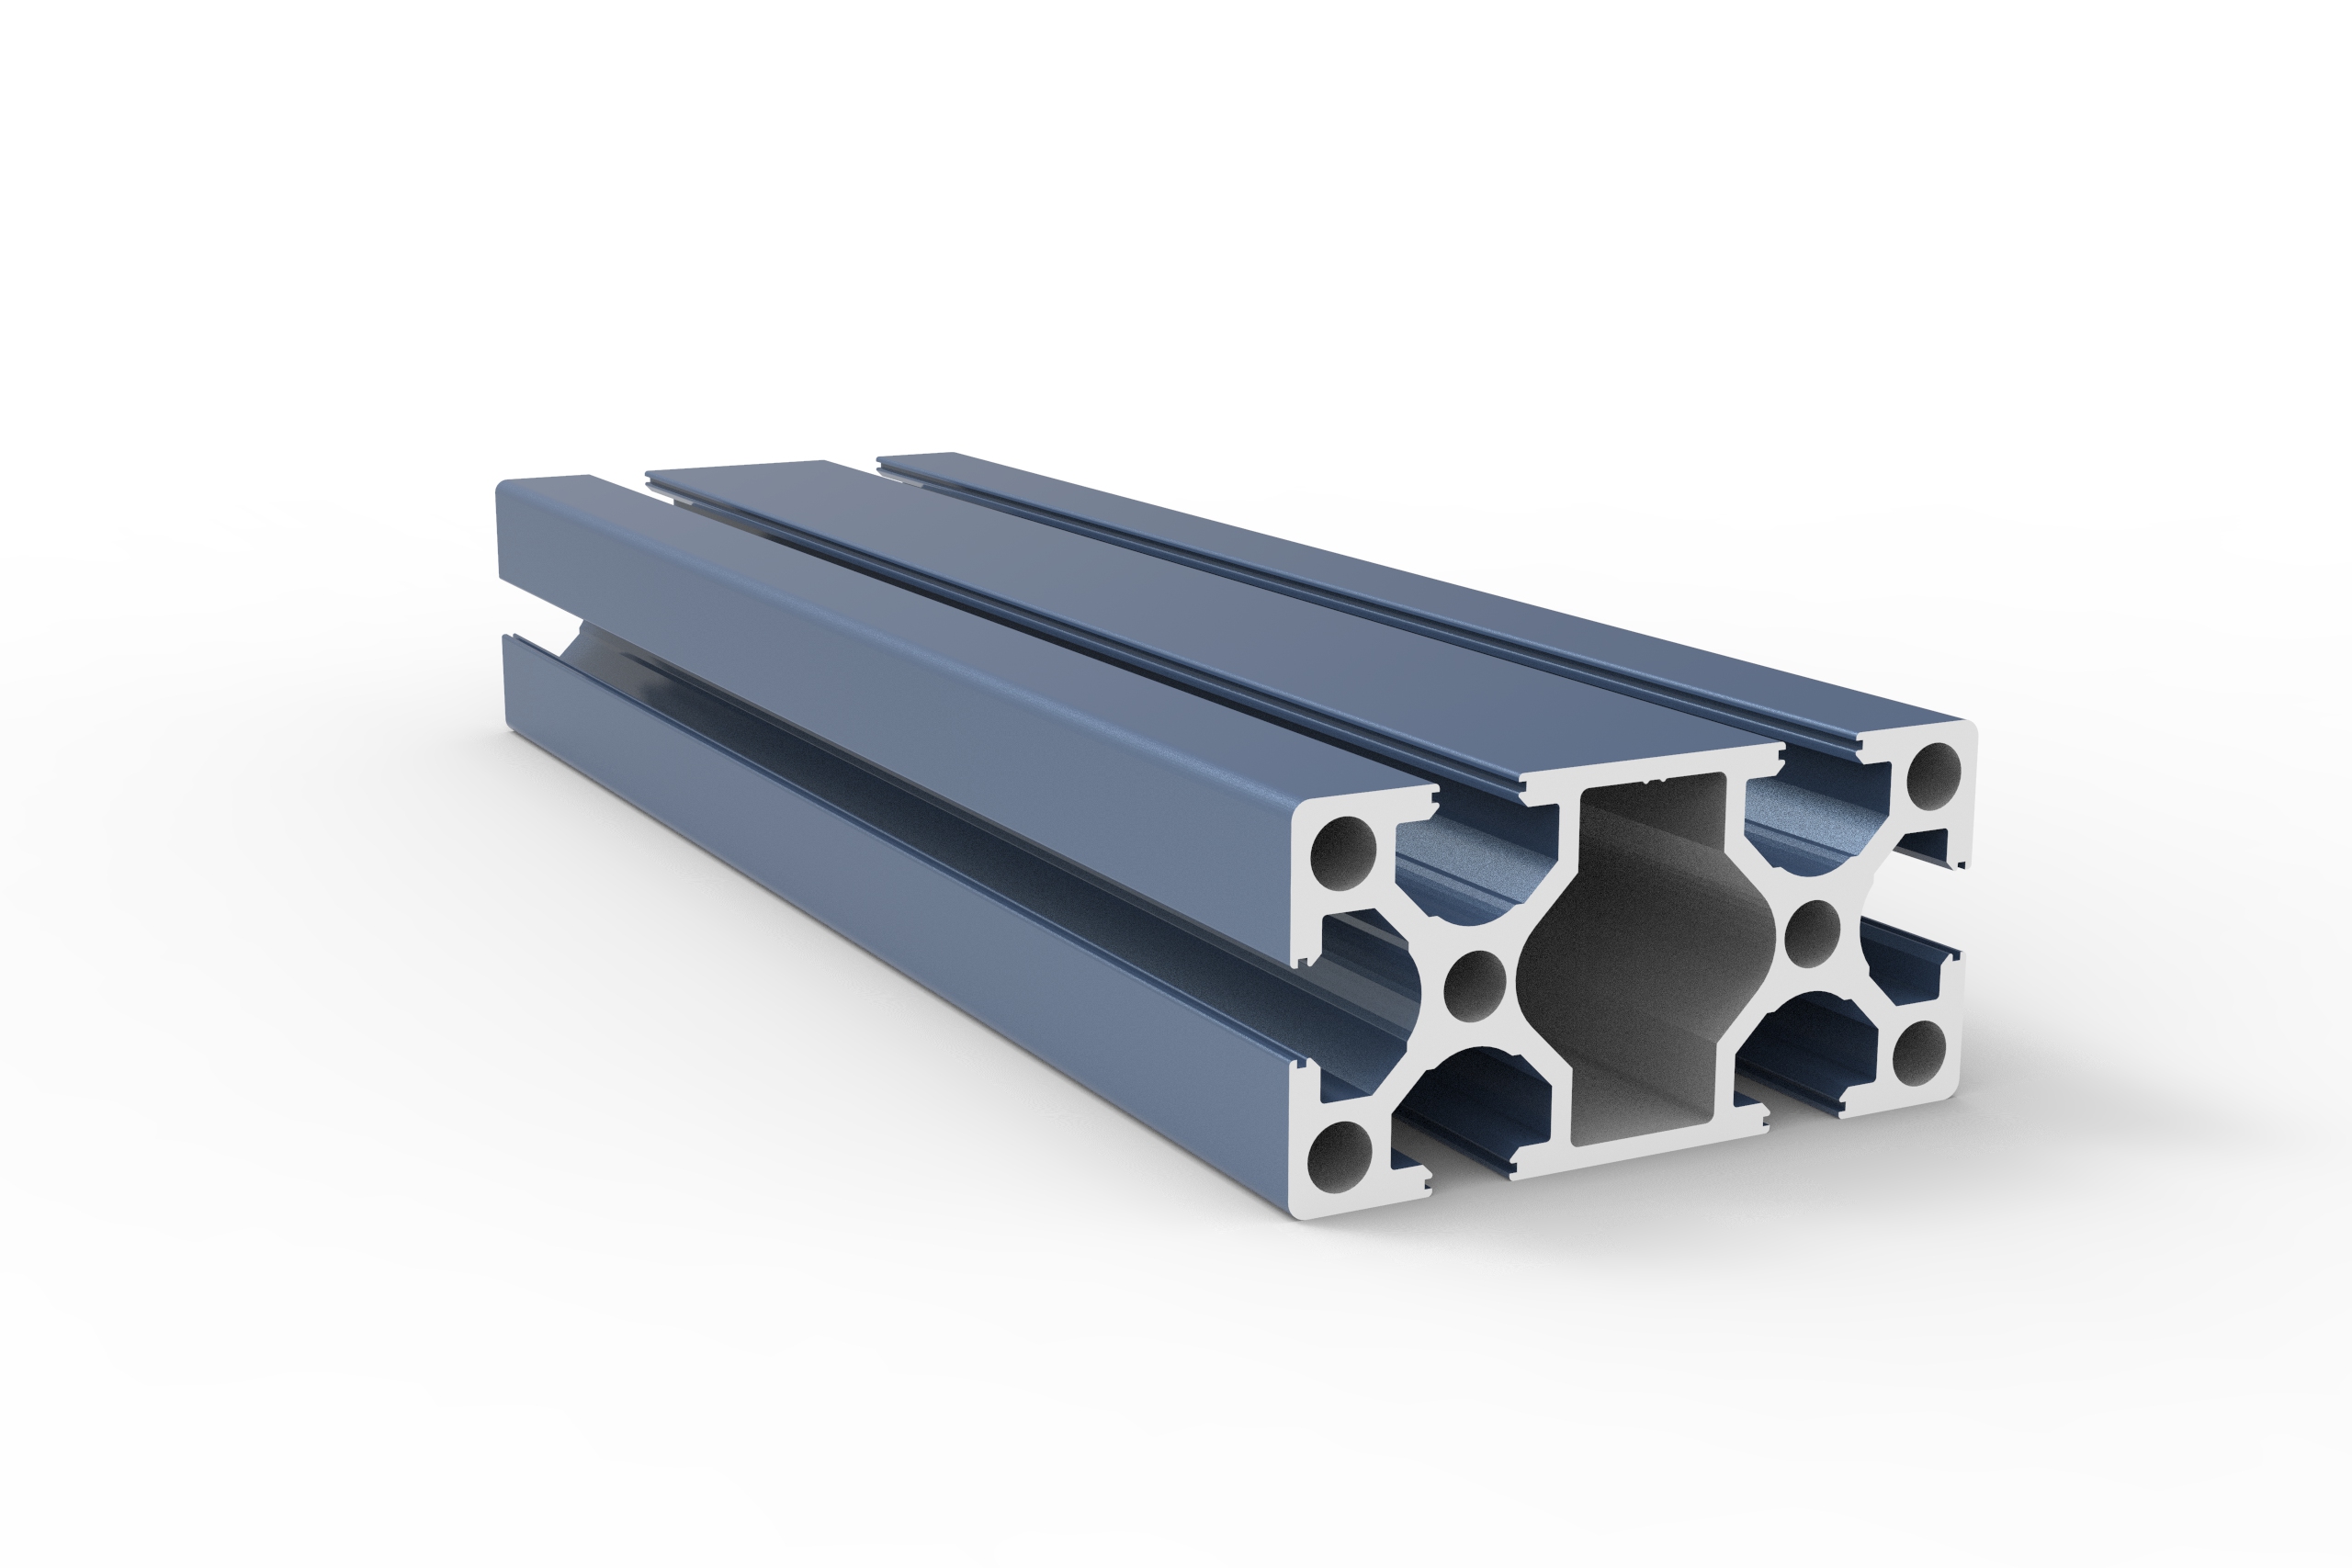
What frame materials make a Sliding window last in harsh coastal weather?
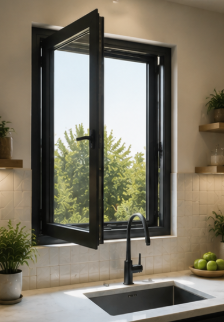
How can I verify that a Shutter certificate matches the actual product?
Can automated Shutters replace manual systems without raising lifecycle costs?
How do I choose the right Casement window size for a windy building?
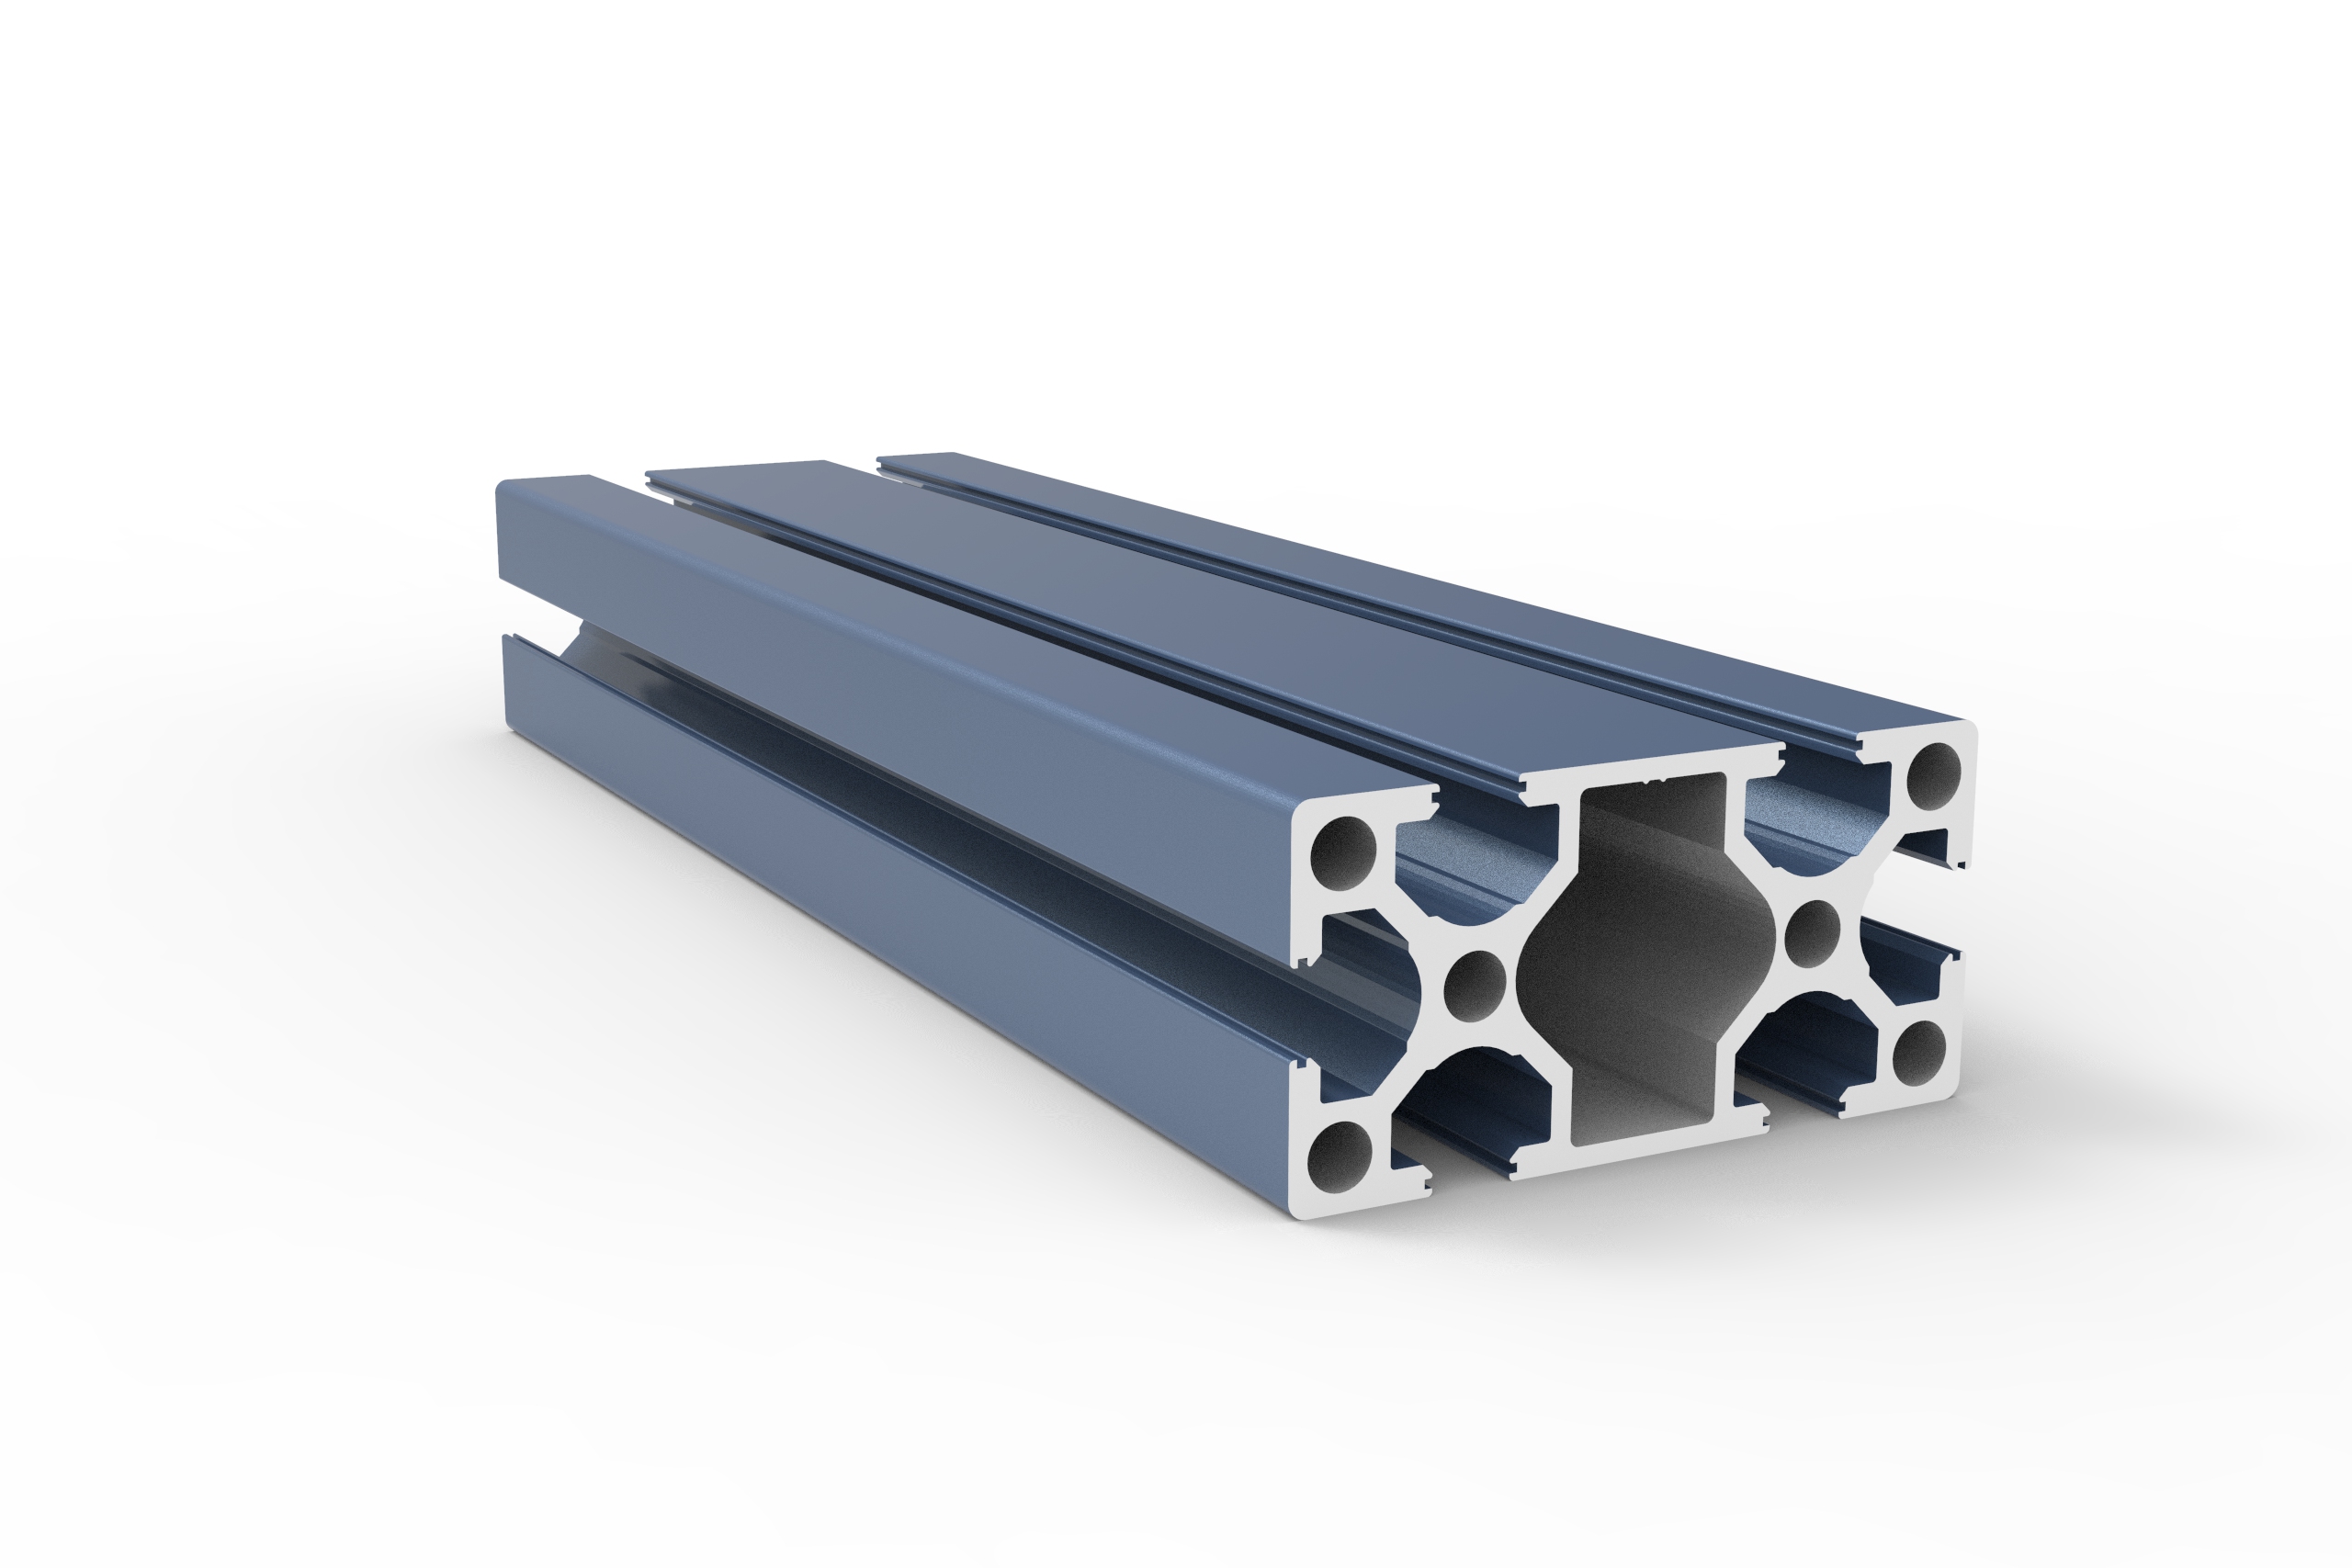
What should an ethical audit cover at a Decorative profile factory?
How should I document Industrial profile defects before disputing the final payment?
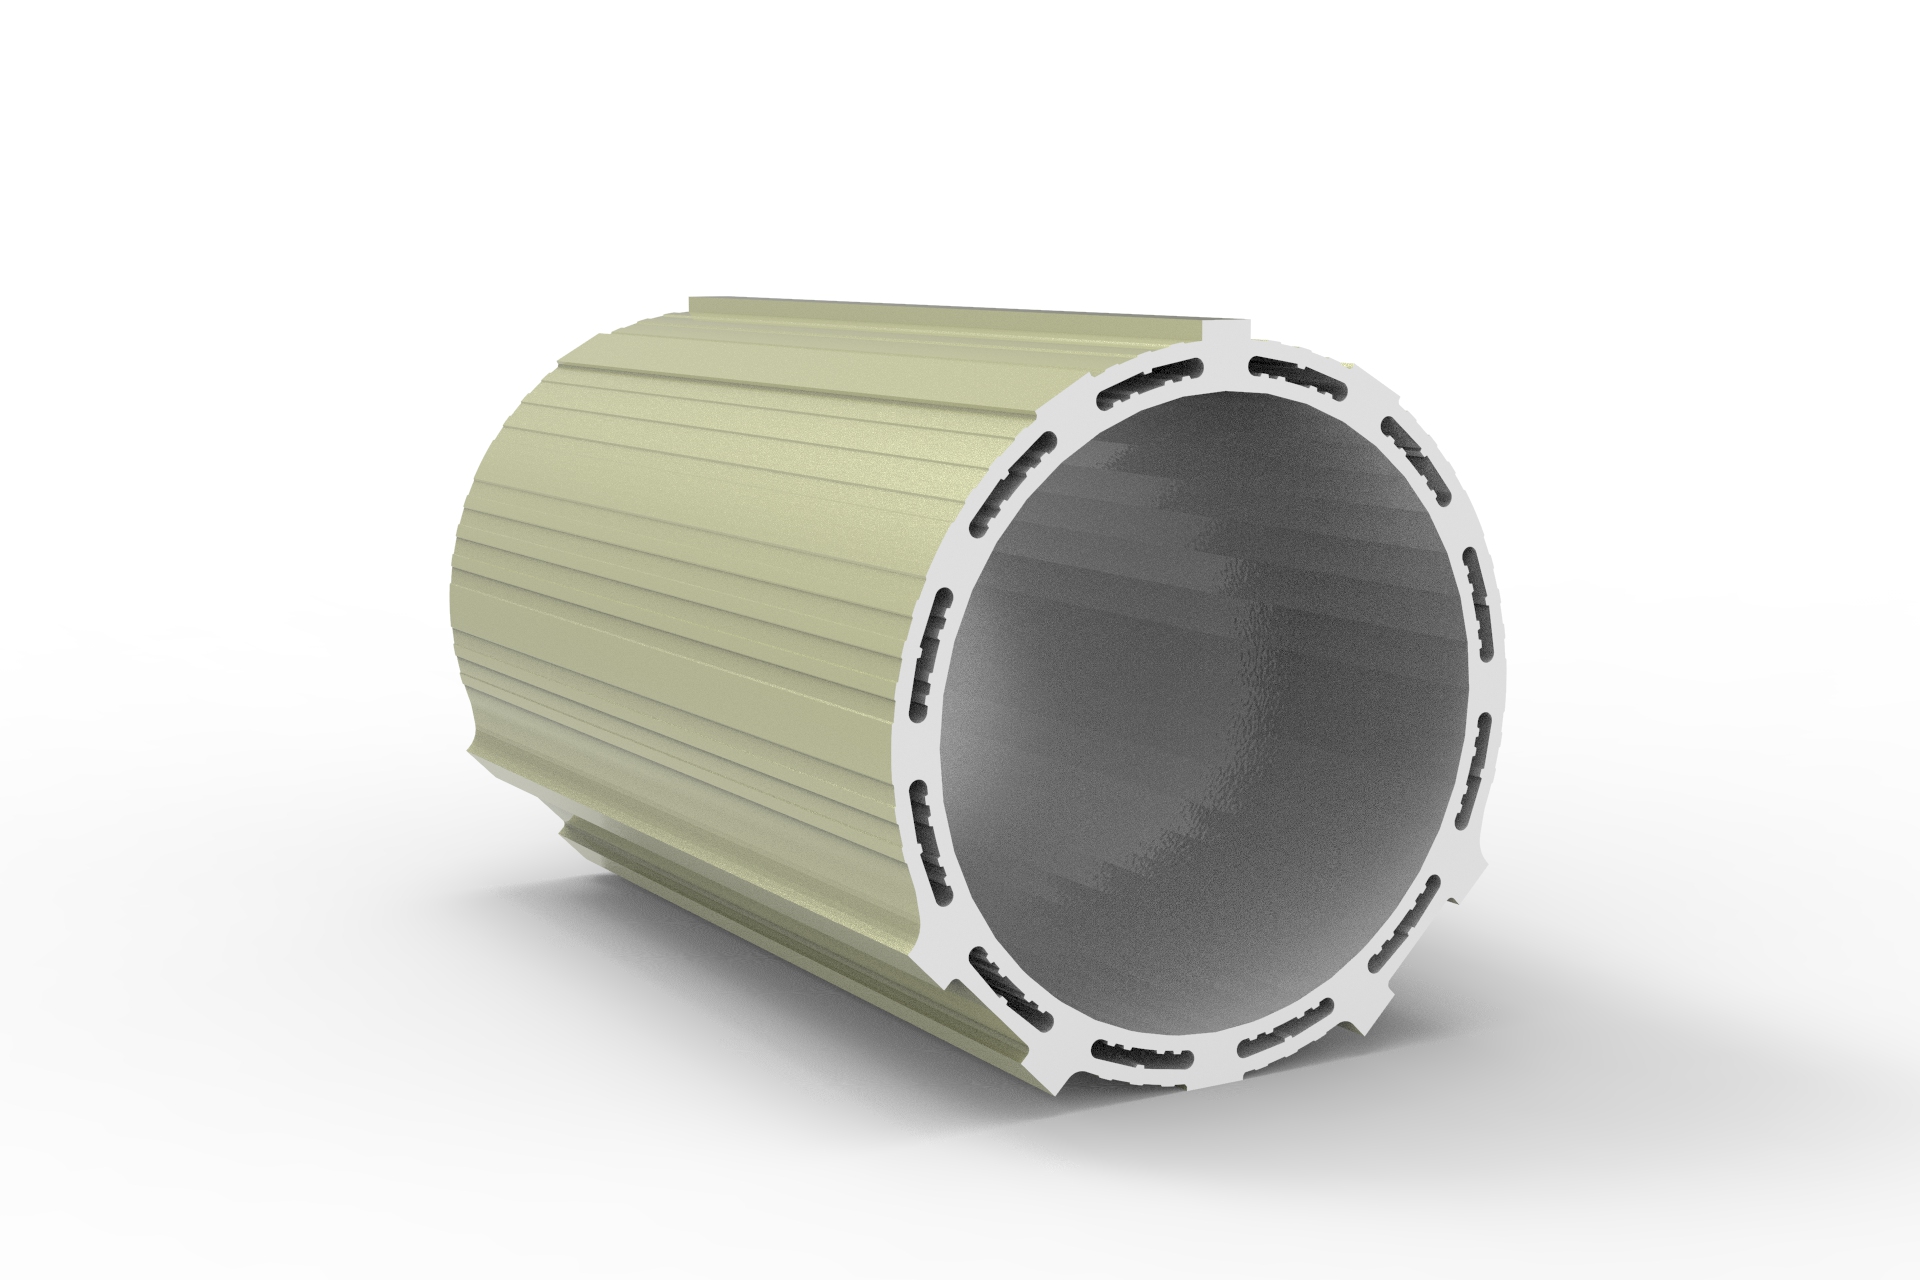
Are lightweight Industrial profile alloys reliable enough for demanding machinery?
Are thermal-break casement windows becoming a better long-term choice than standard frames?
What is a realistic MOQ for custom sliding windows without pushing up unit cost?
What casement window specs should I compare for windy and rainy project sites?
Are there better material options for sliding windows if aluminum prices rise?
How do I ensure aluminum casement windows can handle extreme coastal winds?
What is the typical minimum order quantity for commercial sliding windows?
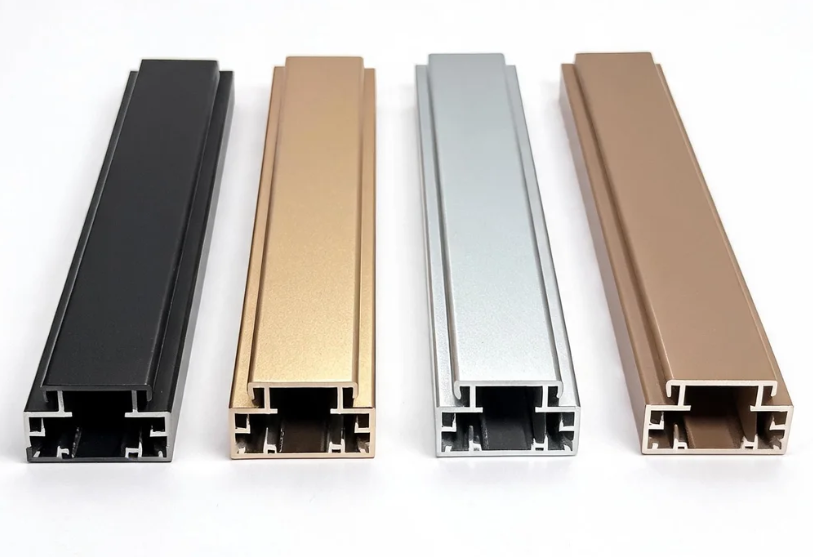
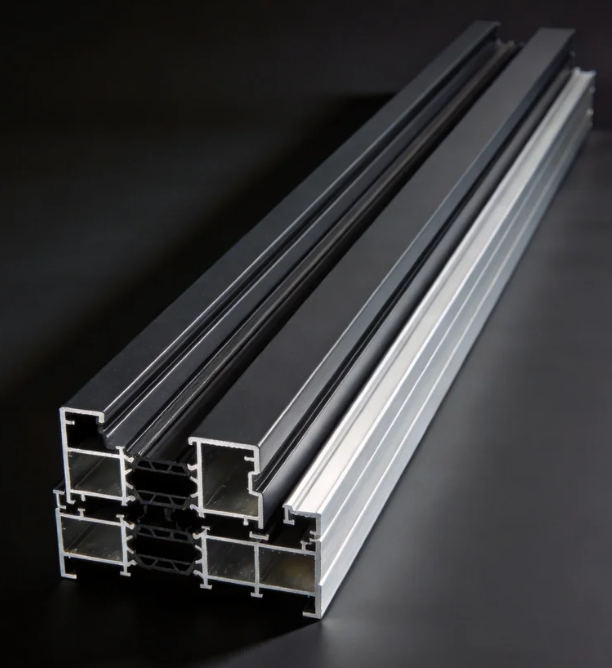
Are there energy-saving alternatives to sliding windows that reduce material and maintenance costs?
Are energy-efficient Awing windows a practical alternative for reducing long-term building costs?
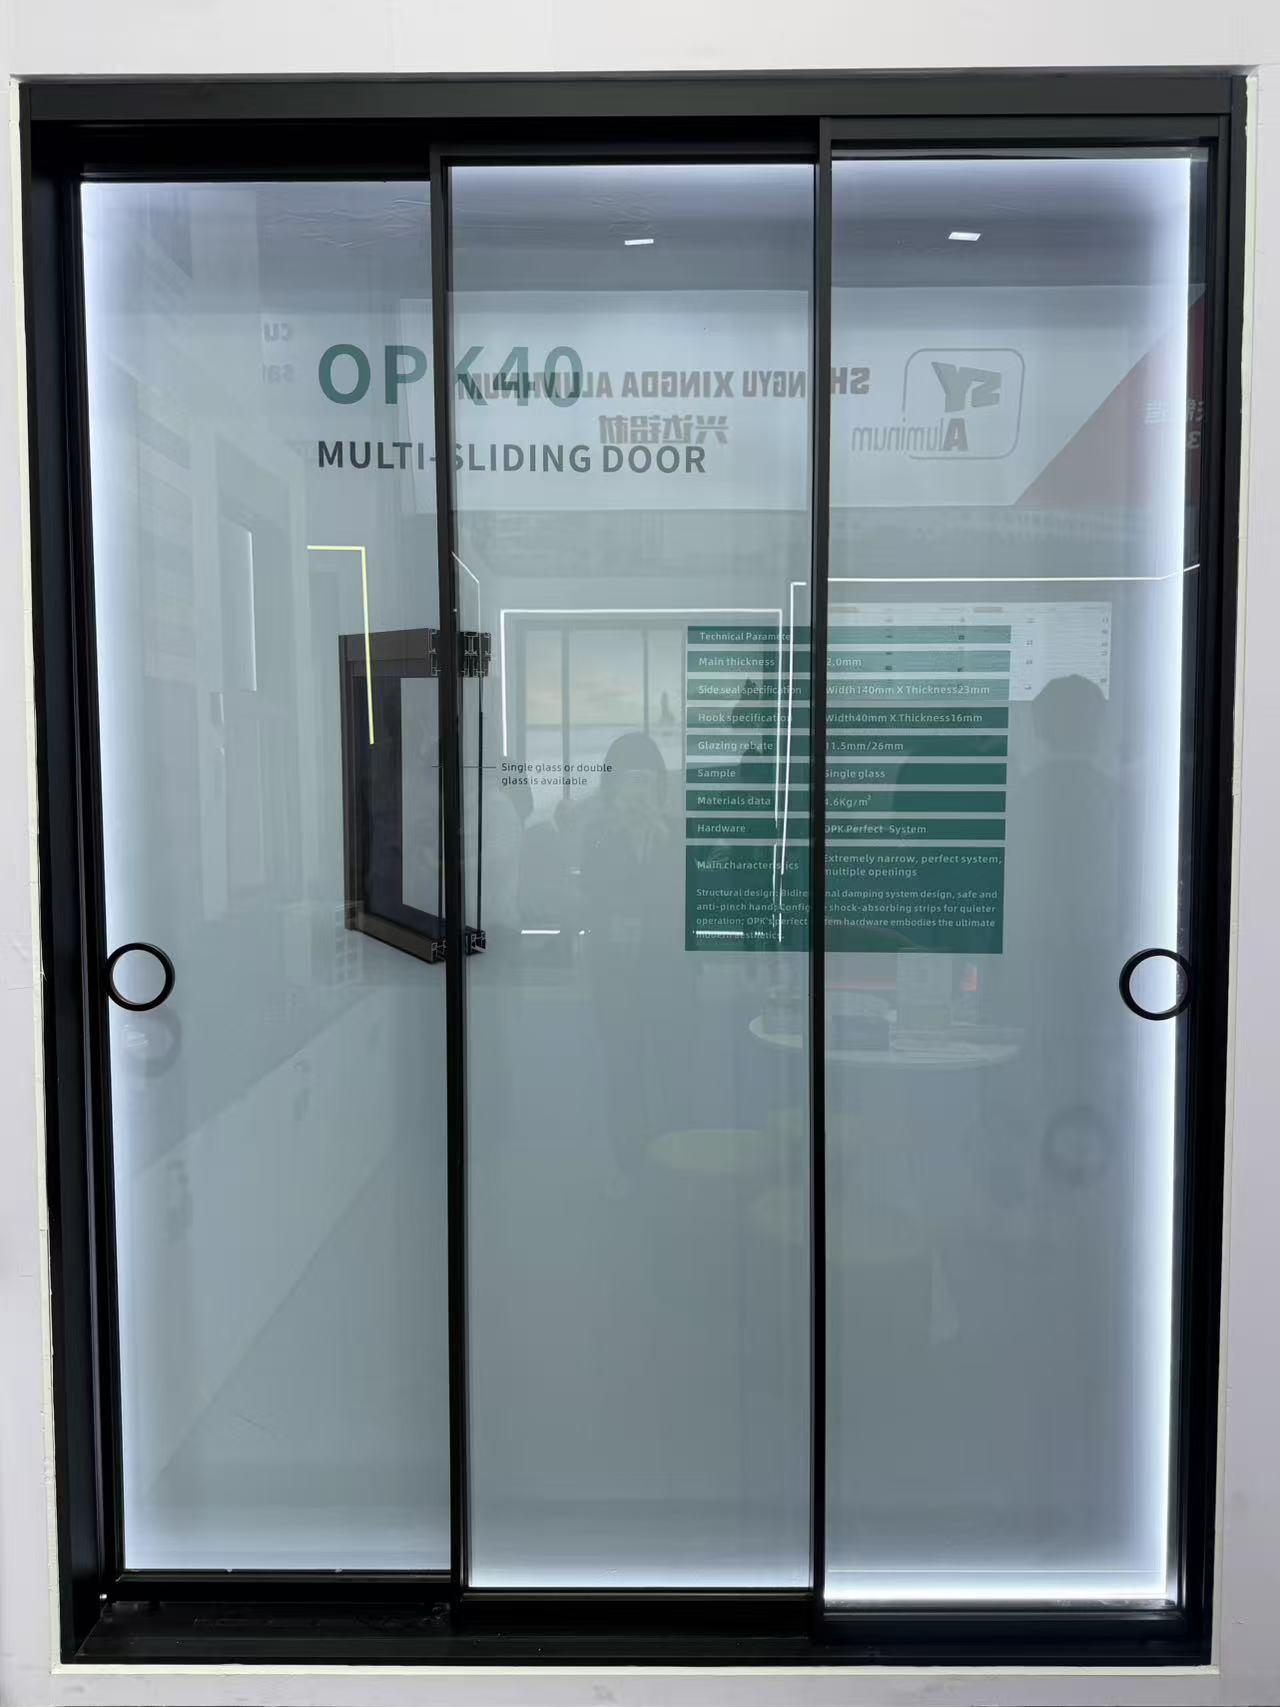
What alternatives to traditional sliding doors can lower costs without sacrificing durability?
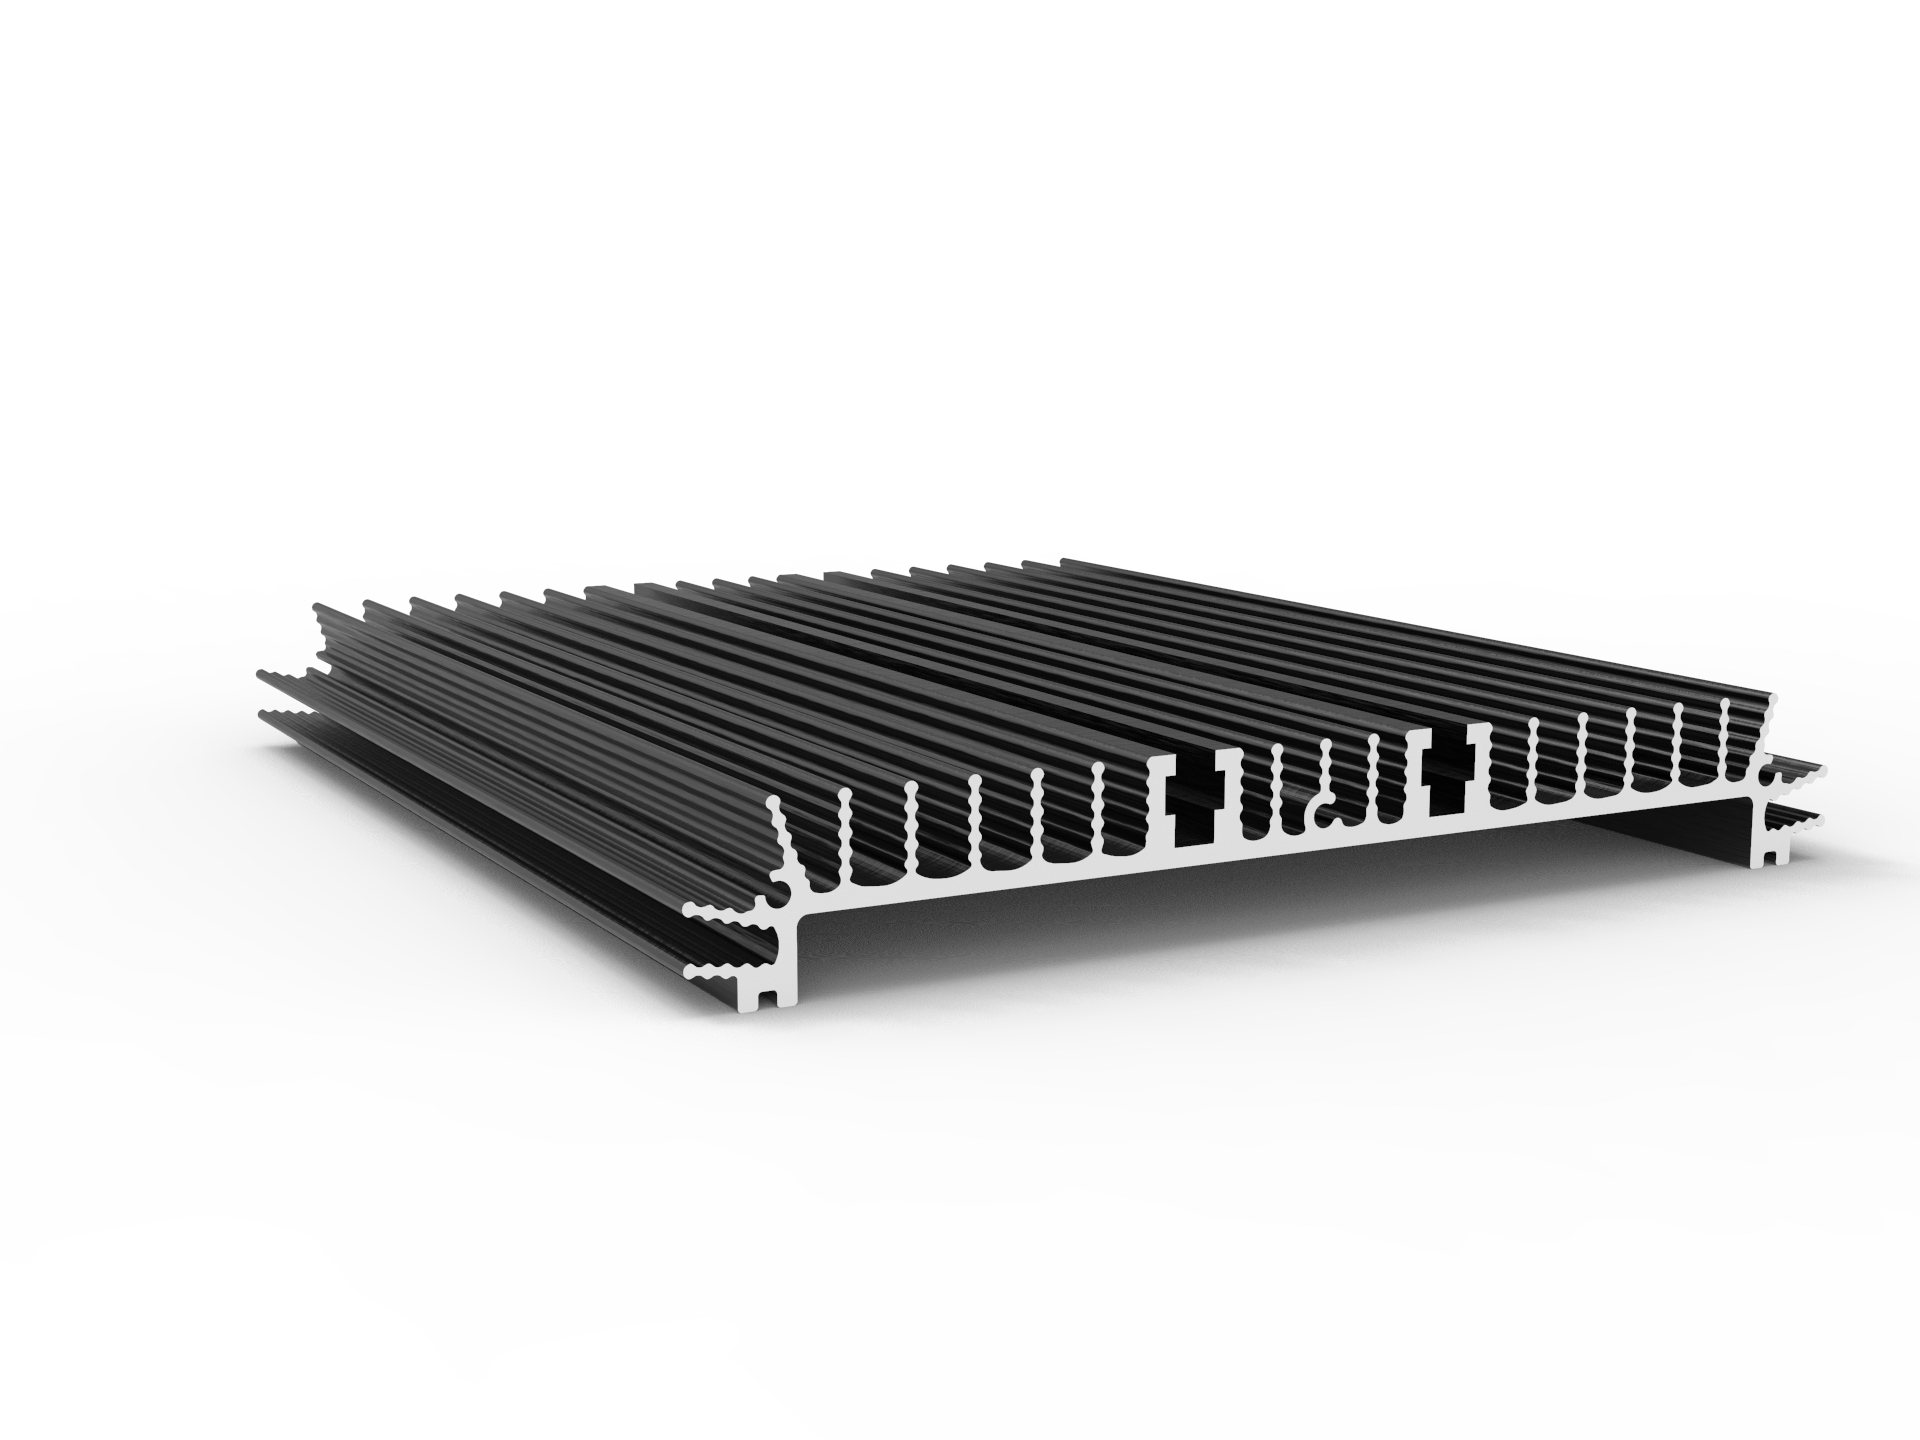
What alternatives to industrial profiles can reduce material costs without hurting strength?
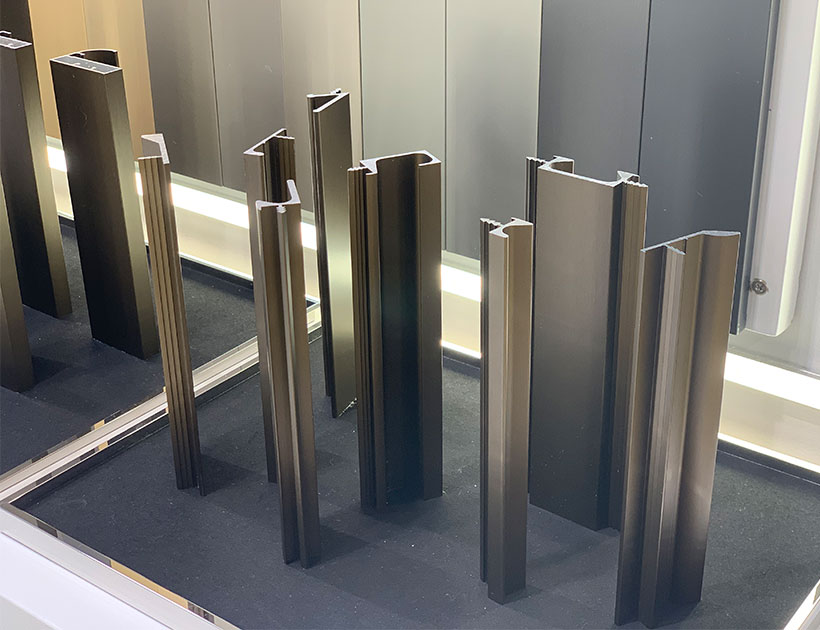
Extruded Aluminium Profiles: Flexible Manufacturing for Diverse Customer Needs
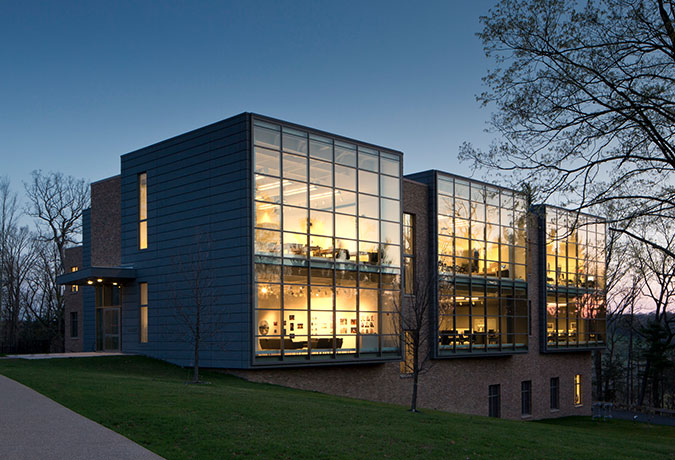
Why Aluminium Curtain Walls Are Popular in Modern Architecture
How do I choose a decorative profile that stays stable in humid or harsh environments?
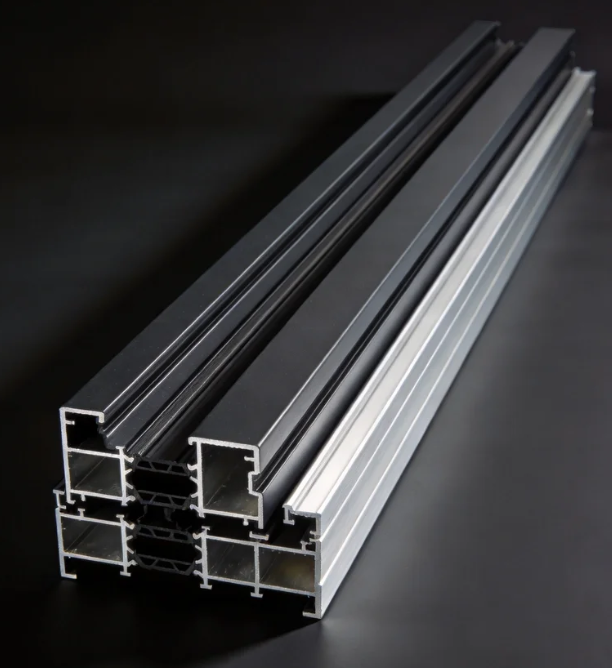
How do I choose an architecture profile that stays stable in harsh outdoor conditions?
How can I compare Awing window specs to avoid poor performance in harsh weather?
How can I compare Sliding door sizes and hardware ratings for harsh commercial environments?
How do I choose the right shutter specifications for harsh climates without overpaying?
What eco-friendly alternatives to folding doors can cut costs without hurting durability?
How do I choose the right shutter specifications for harsh weather without overpaying?
What eco-friendly casement door materials can lower costs without hurting durability?
What newer materials can replace industrial profiles without raising costs or supply risks?
How do I choose a decorative profile that stays stable in humid, high-traffic spaces?
What sustainable material alternatives can replace aluminum architecture profiles?
What should I check in Awing window specs to ensure reliable performance in harsh weather?
How can I compare Sliding door sizes and thermal ratings for harsh climates before buying?
What newer materials can replace aluminum in awning windows without raising our costs?
How do I choose the right Sliding door specs for smooth operation in harsh environments?
How do I choose a folding door that stays stable in harsh weather and heavy daily use?
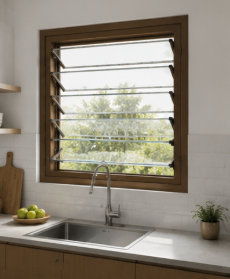
How can I choose the right shutter specifications for harsh weather and long-term use?
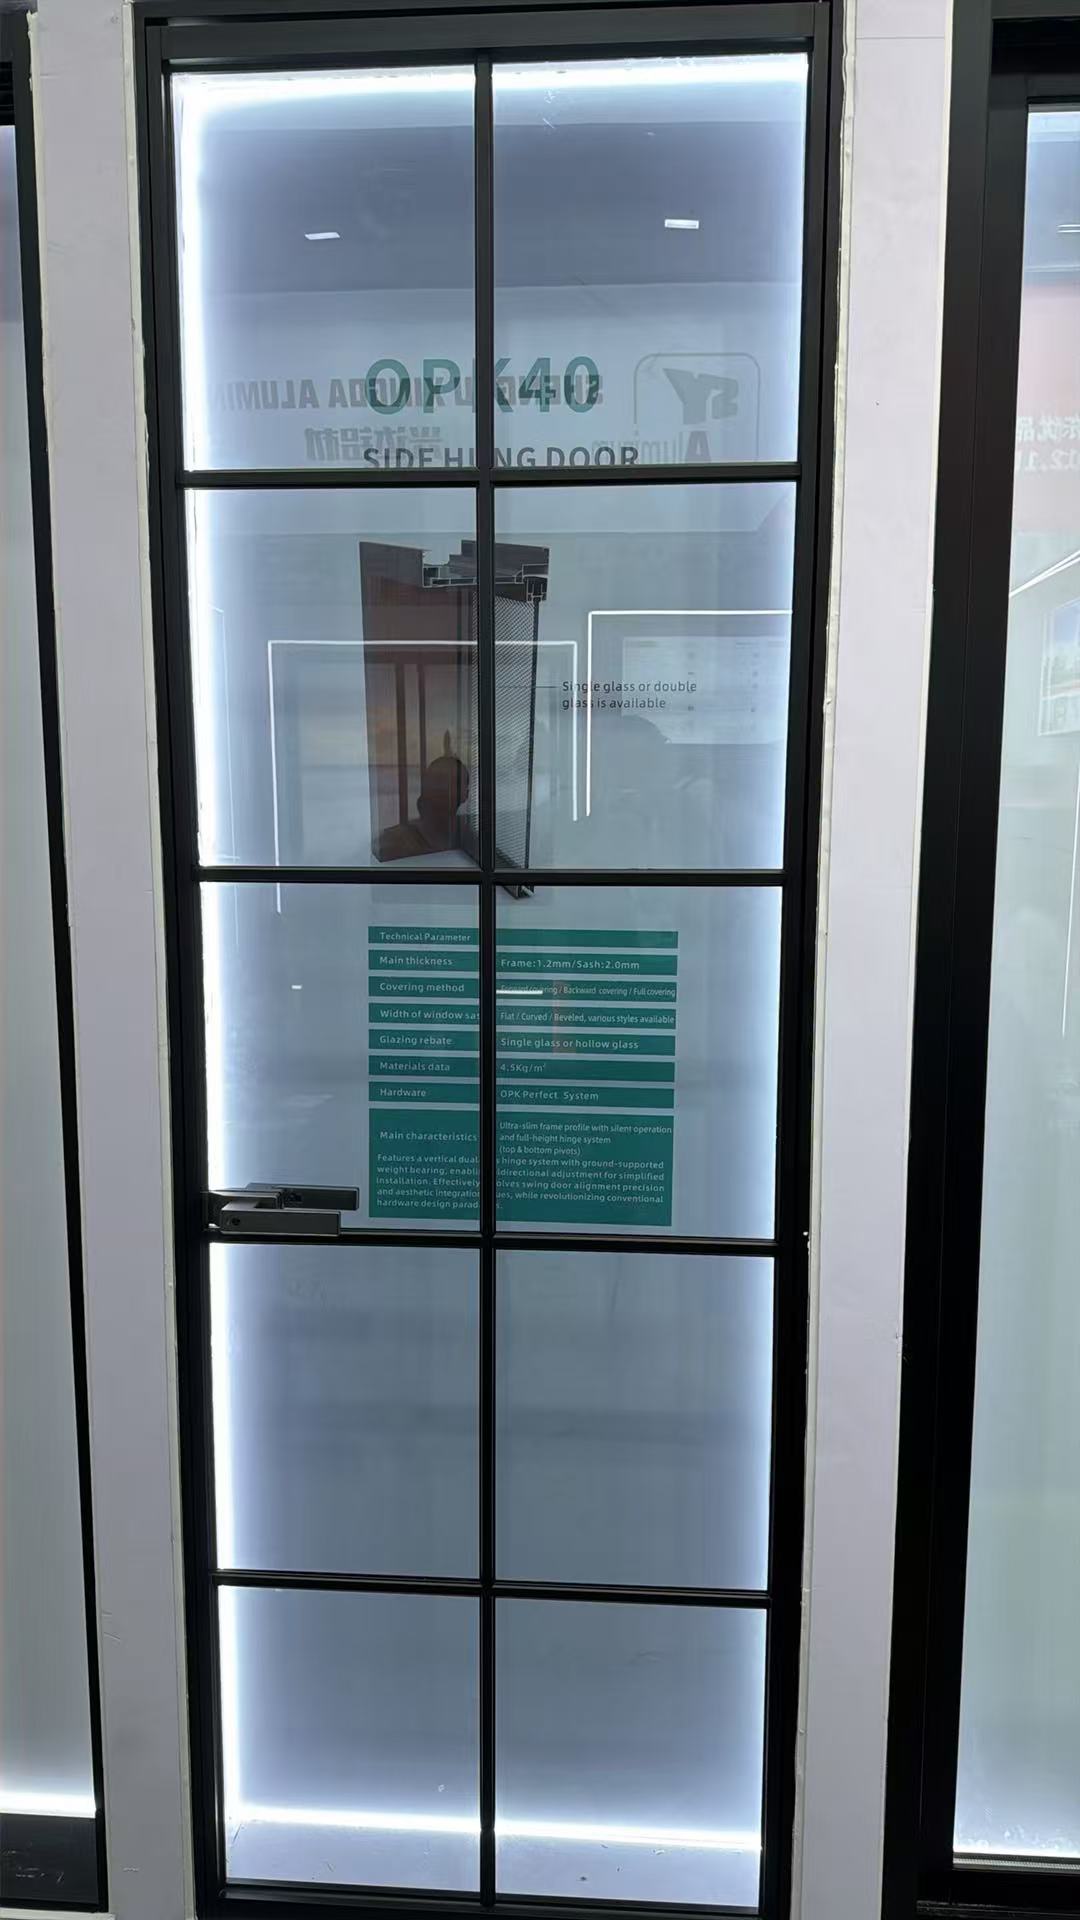
How do I compare casement door U-values, hardware, and weather sealing before buying?
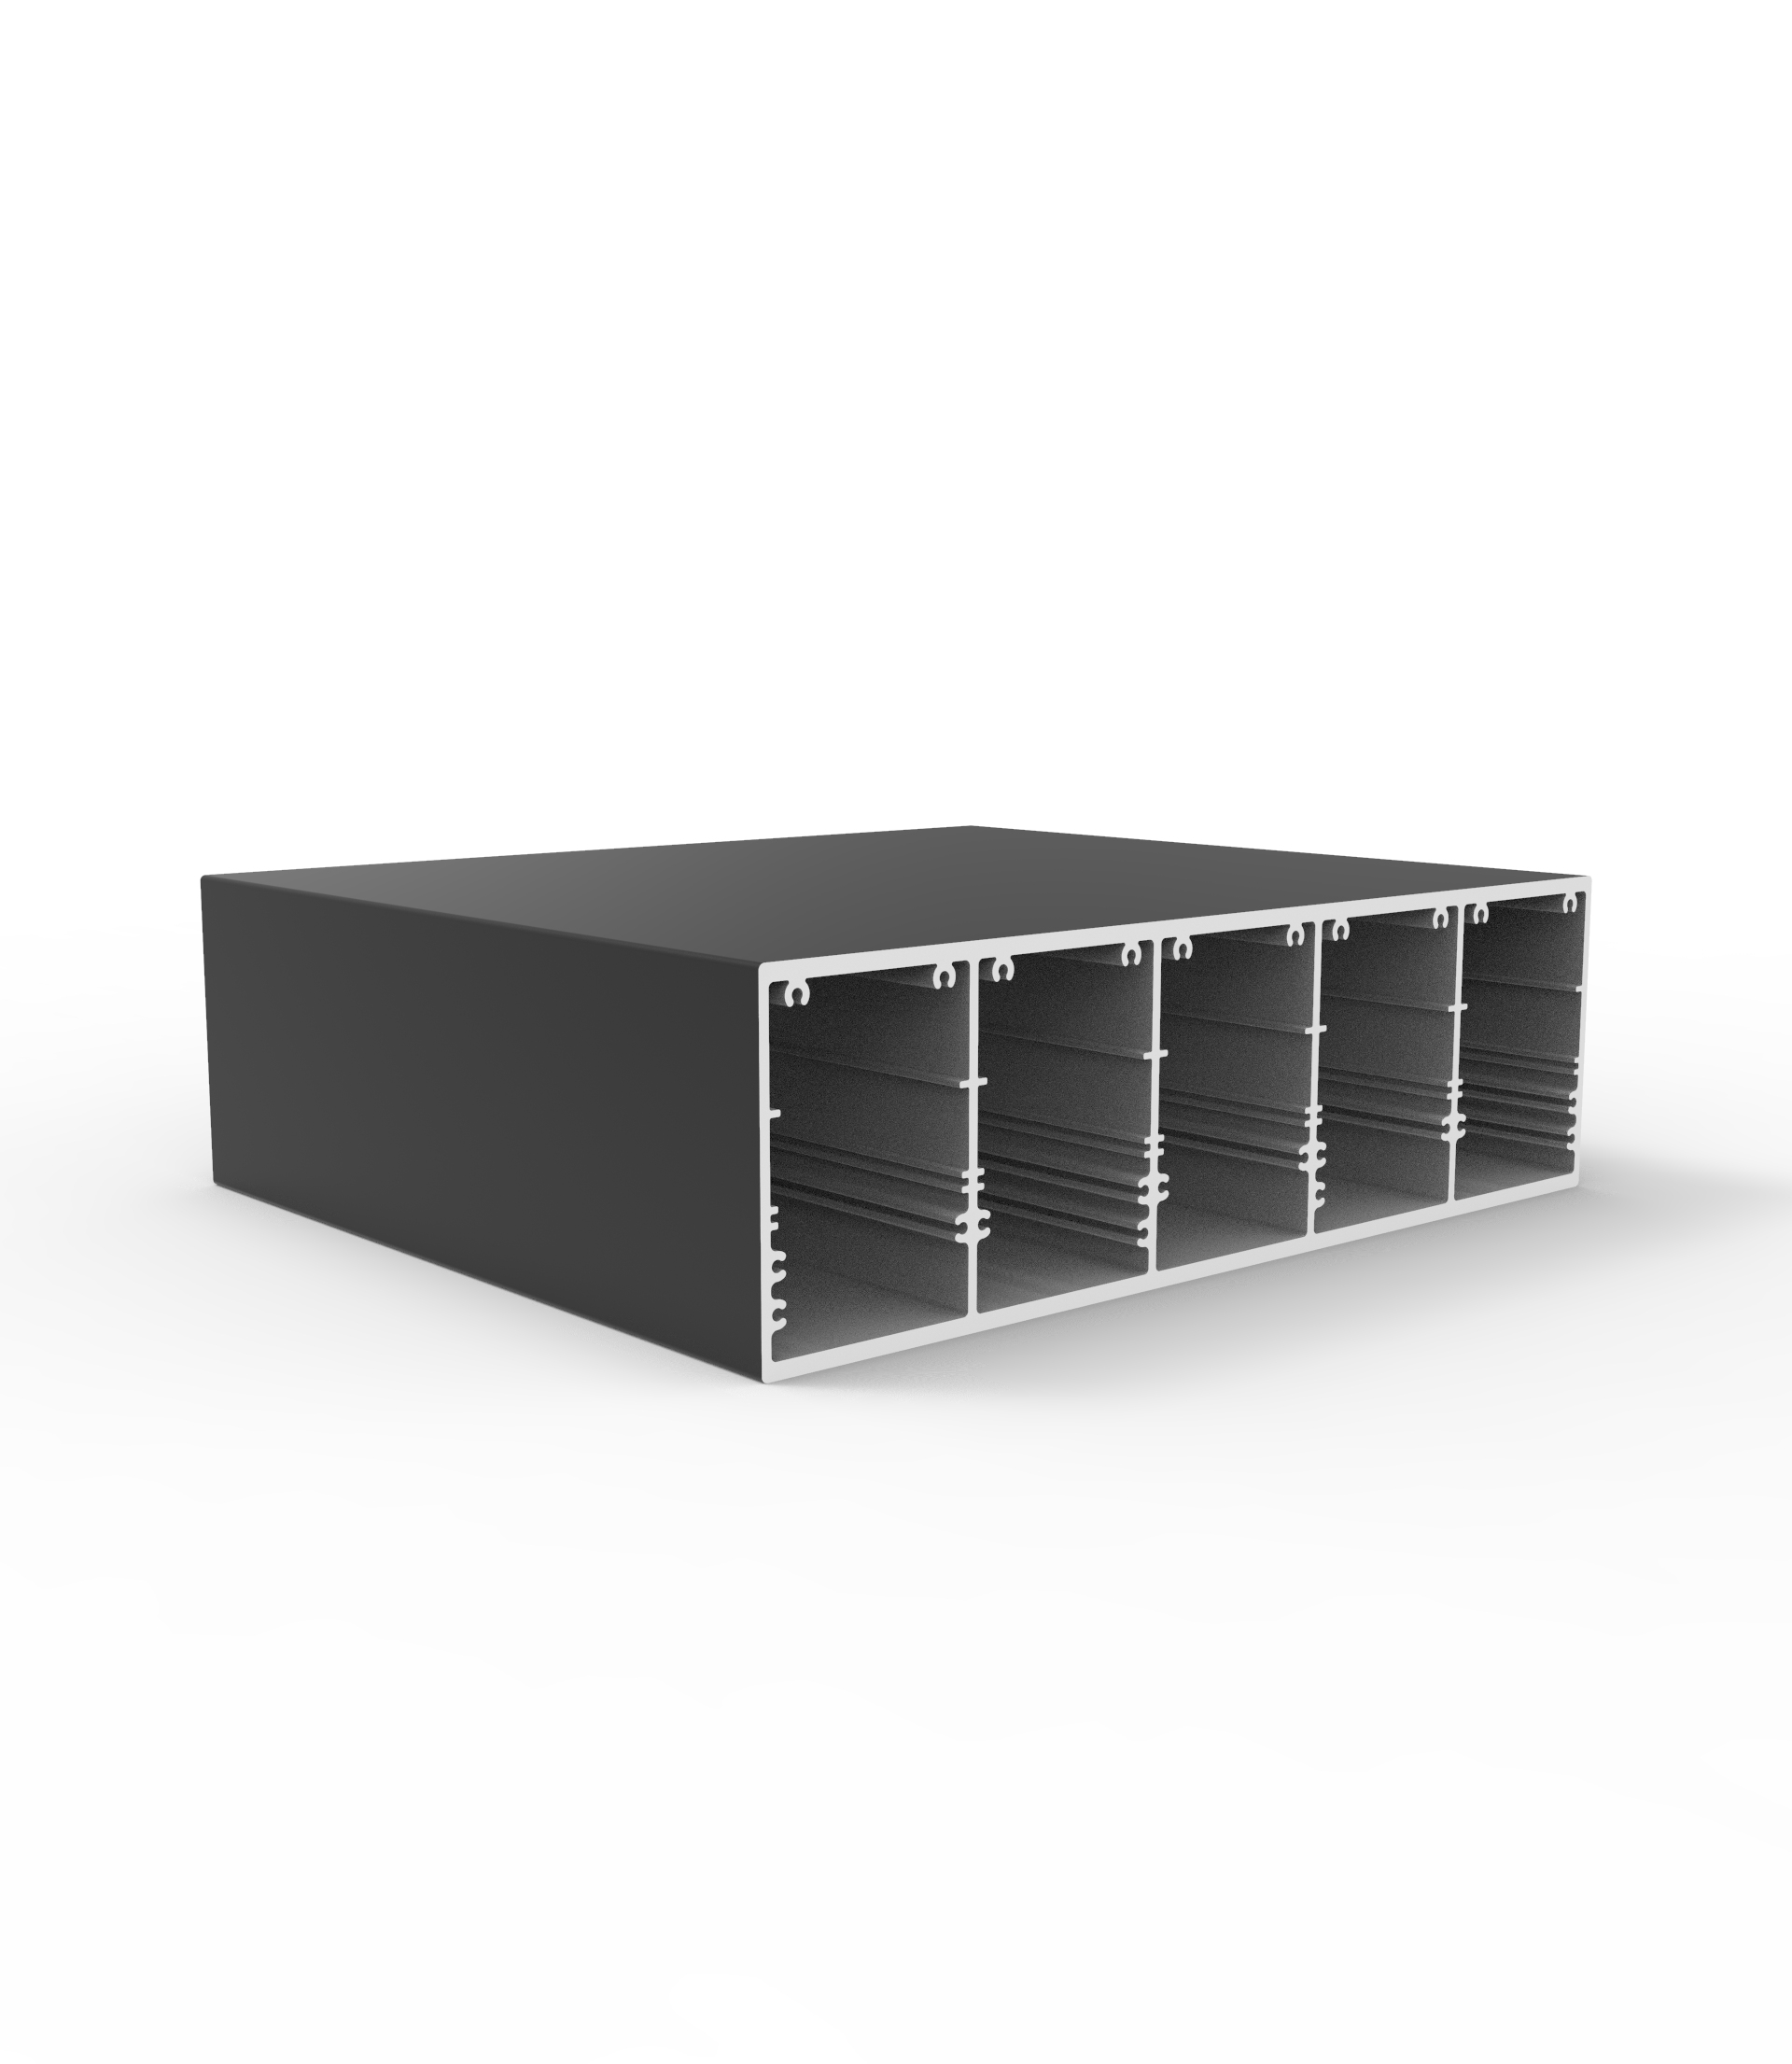
How do I choose the right industrial profile size for strength and load needs?
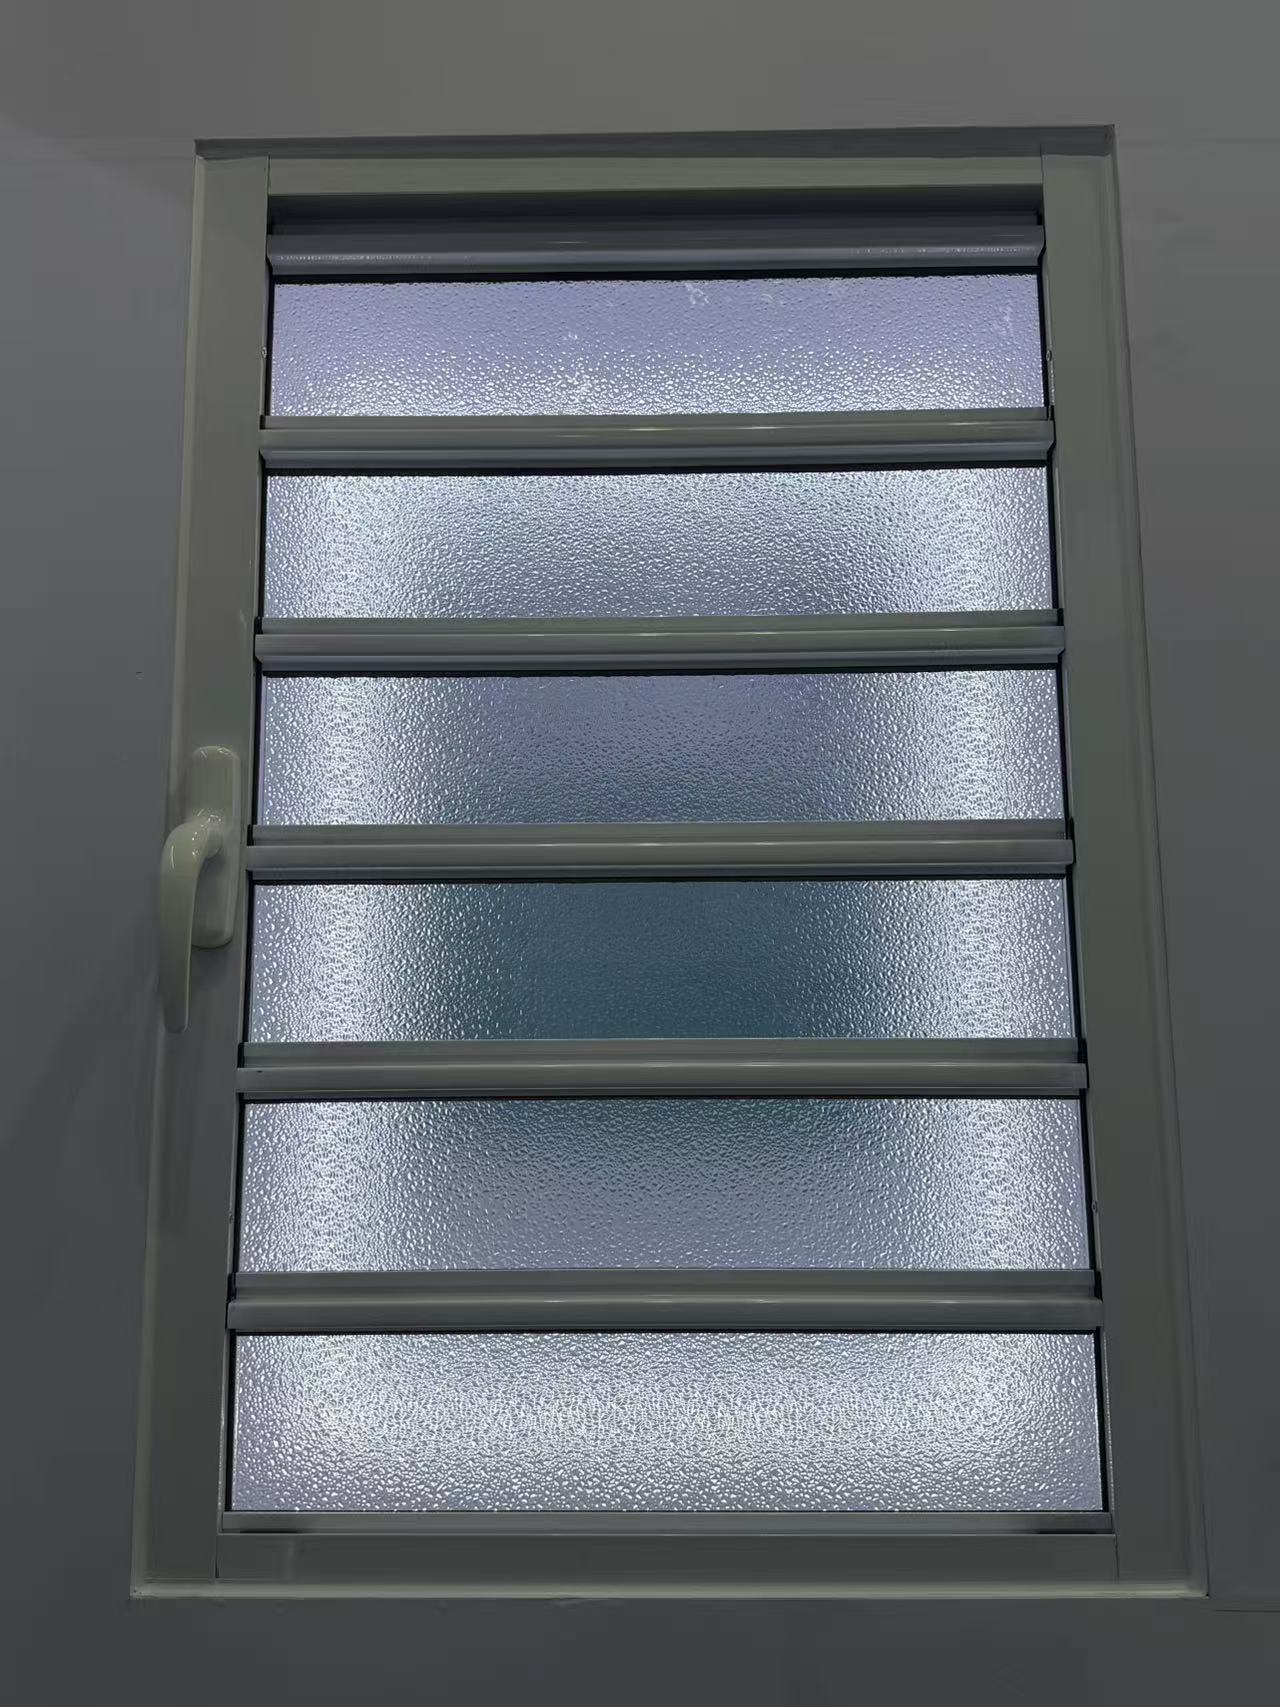
How do I choose the right shutter specifications for harsh weather and long-term commercial use?
How do I choose the right Casement door size and hardware for harsh weather?
What greener alternatives to decorative profile can cut costs without hurting durability?
What lower-cost, eco-friendly materials can replace decorative profiles?
What lower-carbon alternatives to aluminum architecture profiles are practical for our project?
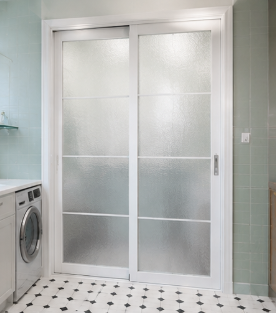
How can I compare sliding door systems for insulation, security, and long-term use?
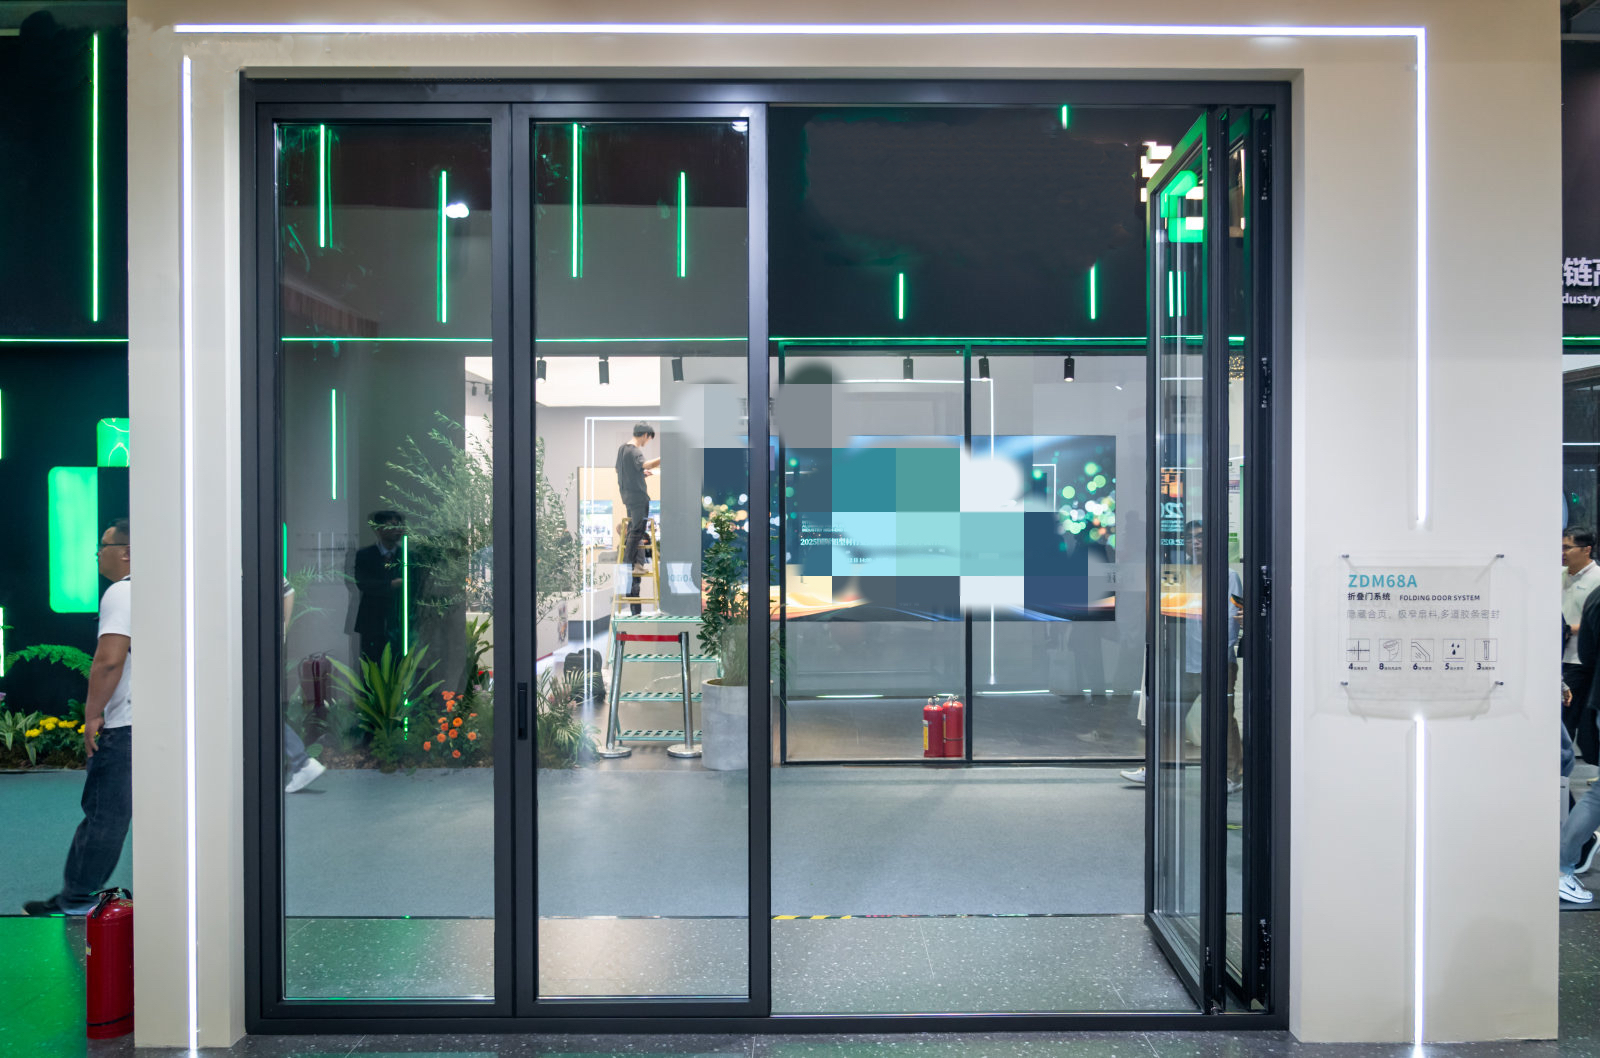
What is the standard production lead time for bulk orders of folding doors?
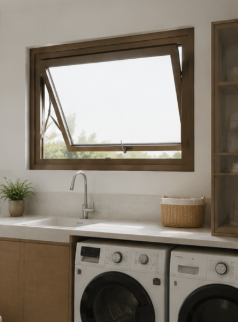
How do I choose the right Awing window size and glass specification for harsh weather?
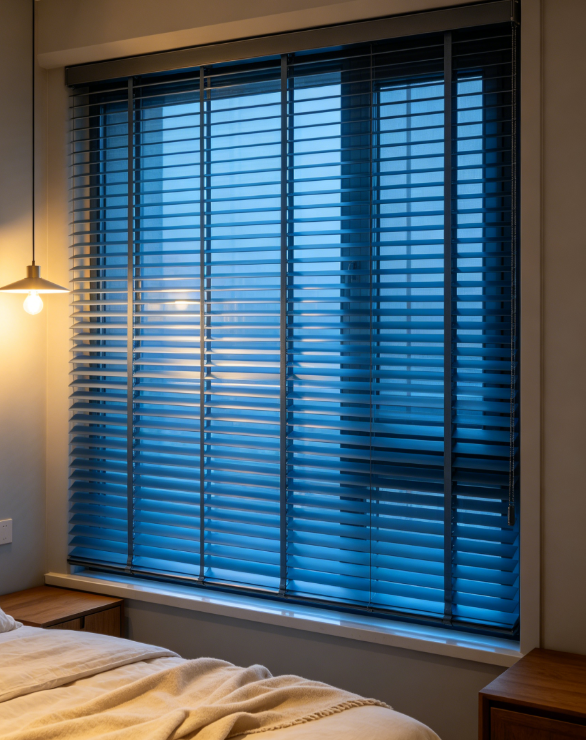
How can I test shutter samples so the final bulk order matches their quality and finish?
Can suppliers make custom double glass casement doors from my CAD drawings?
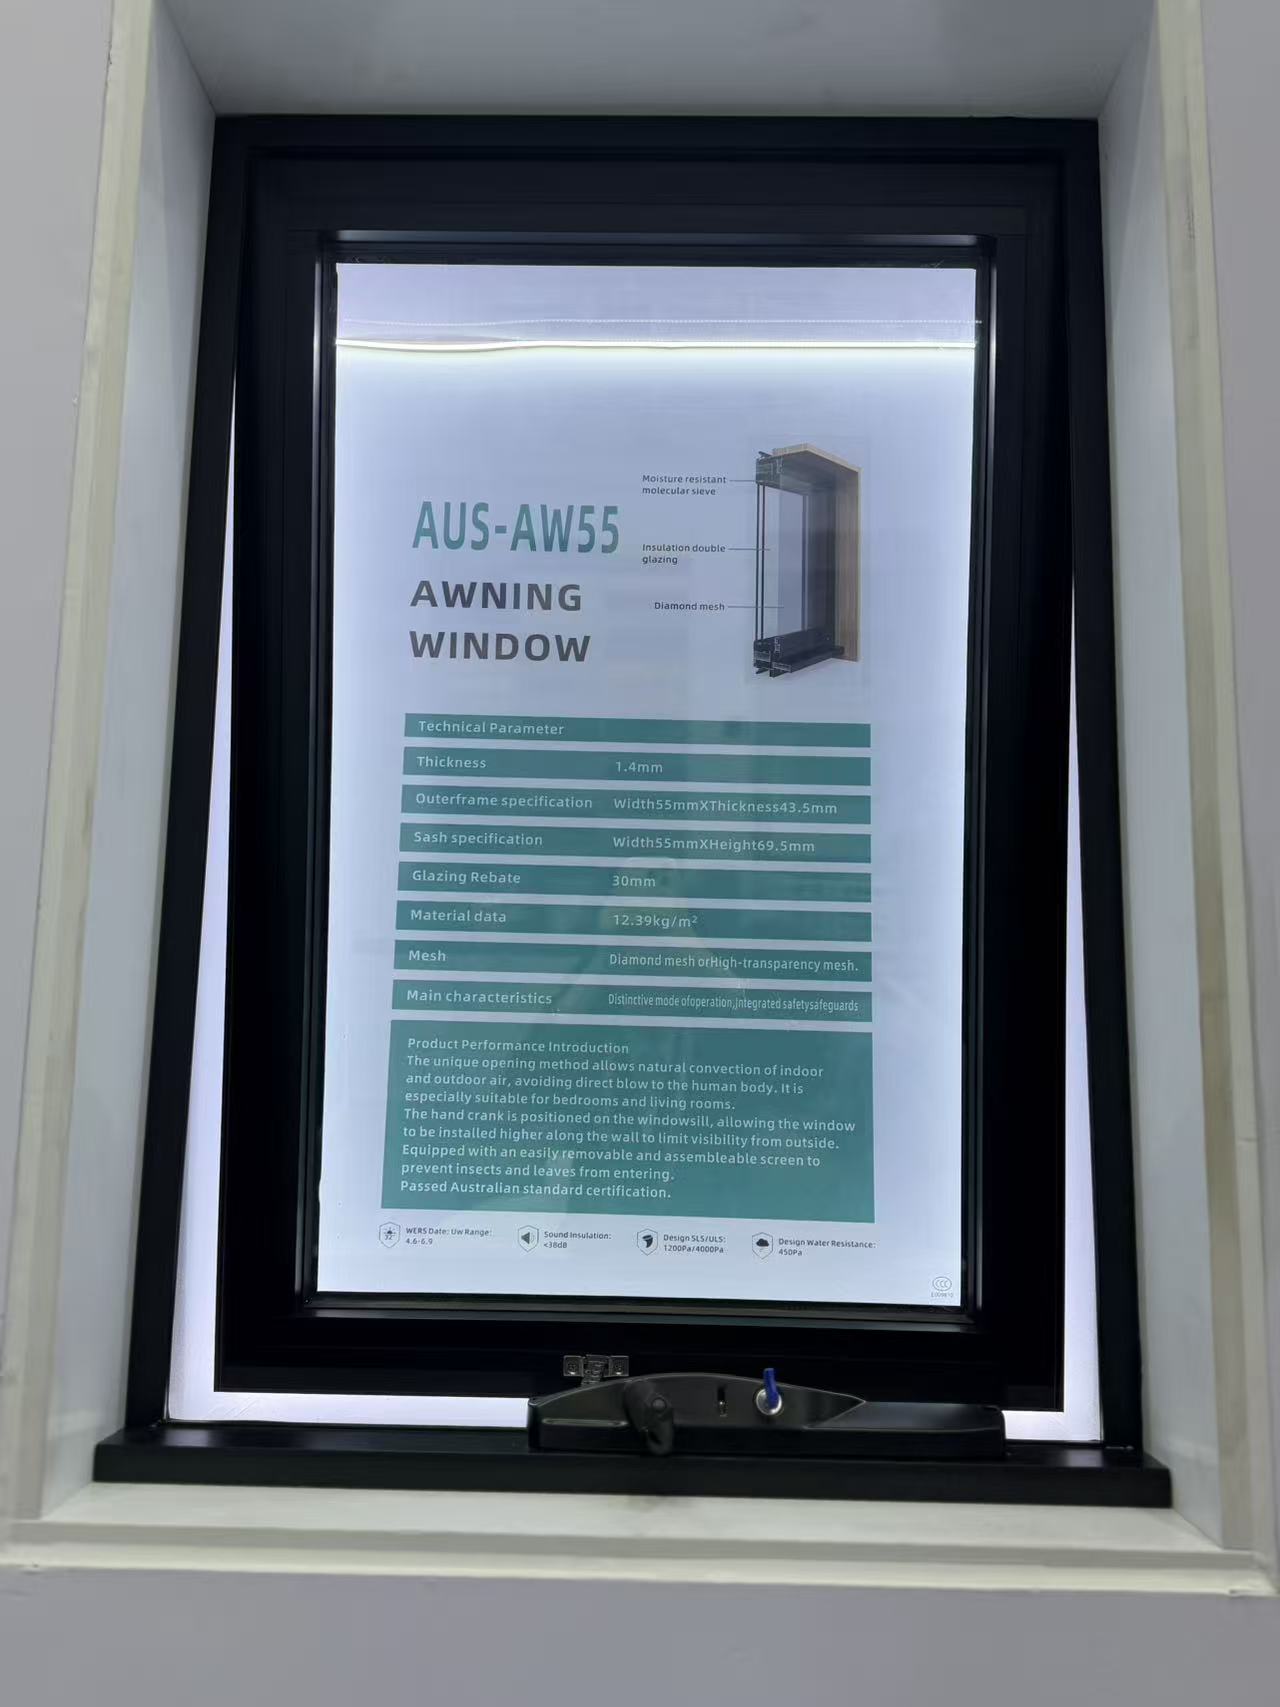
What safety certifications should I request when importing awning windows?
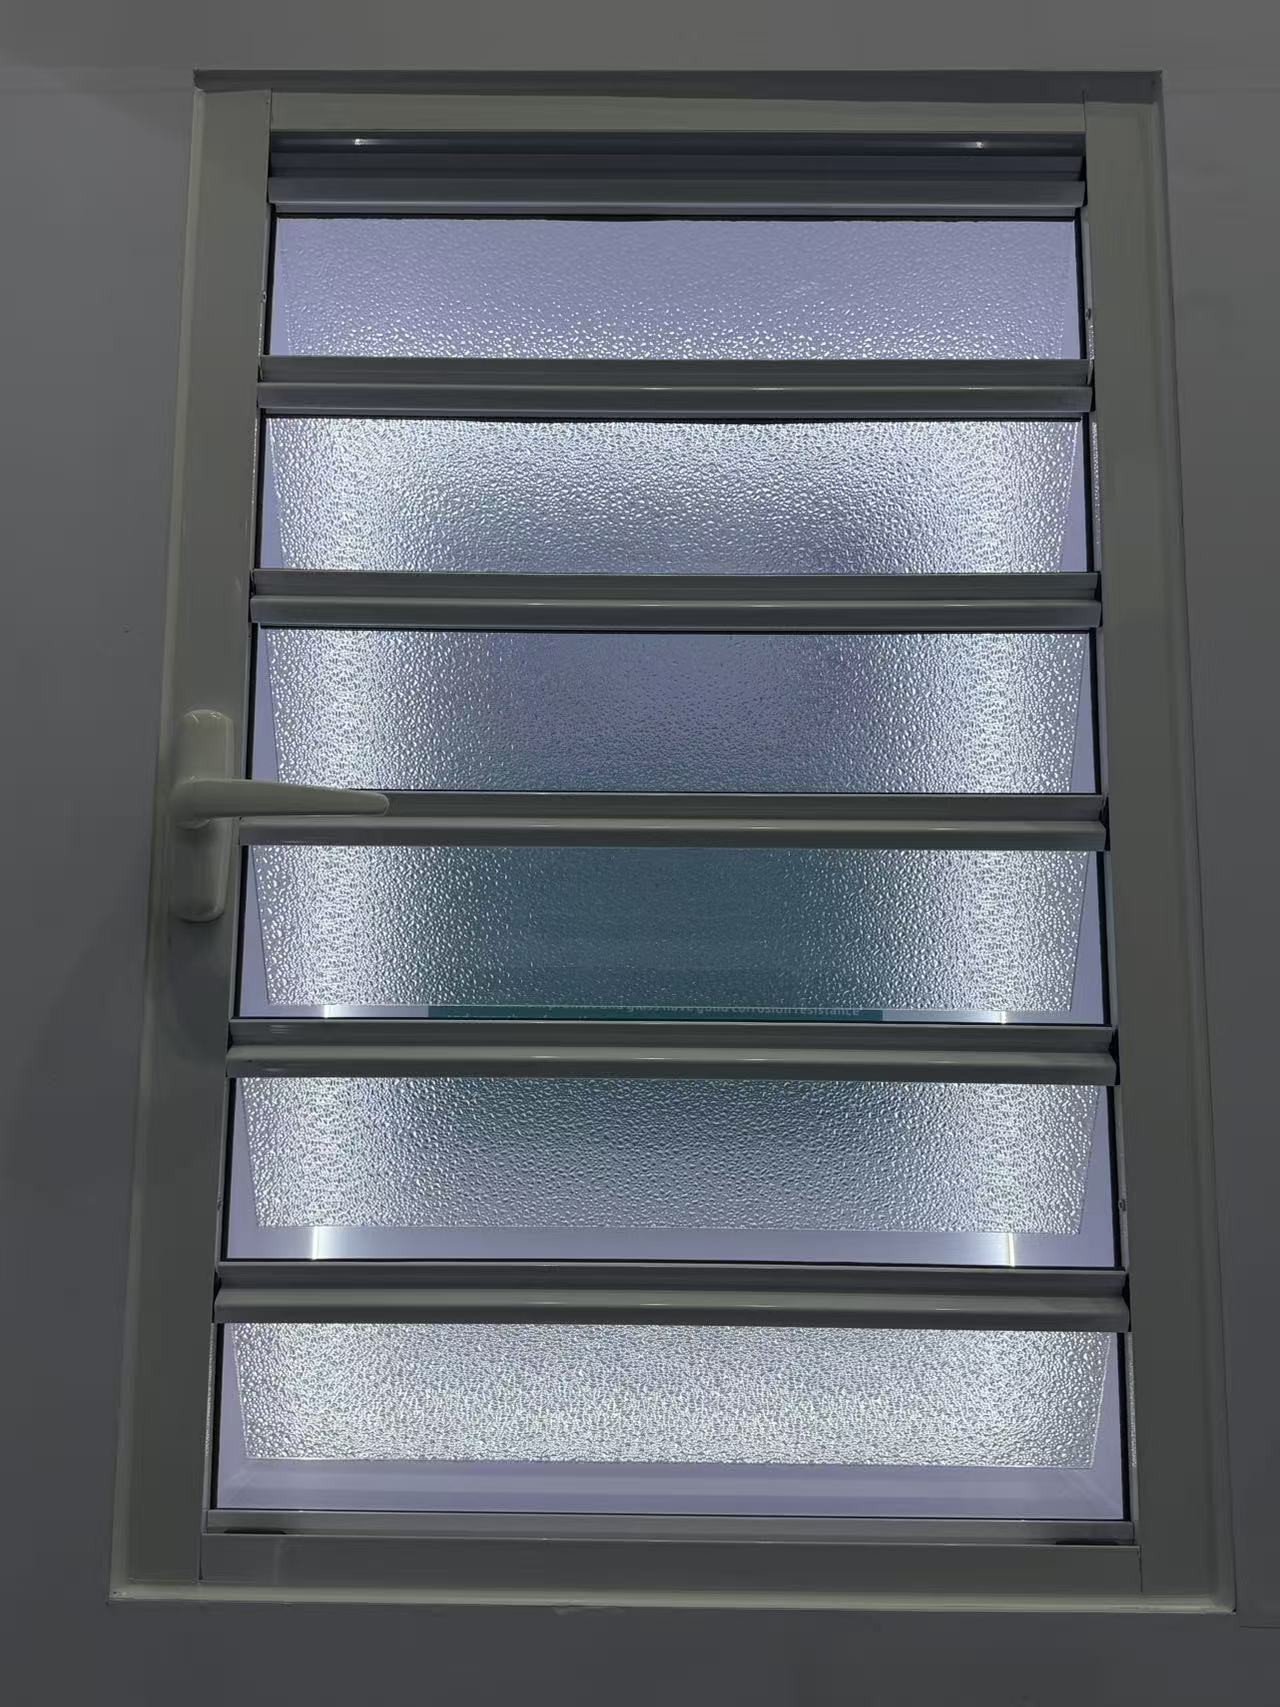
How long does it usually take a factory to make custom shutter samples?
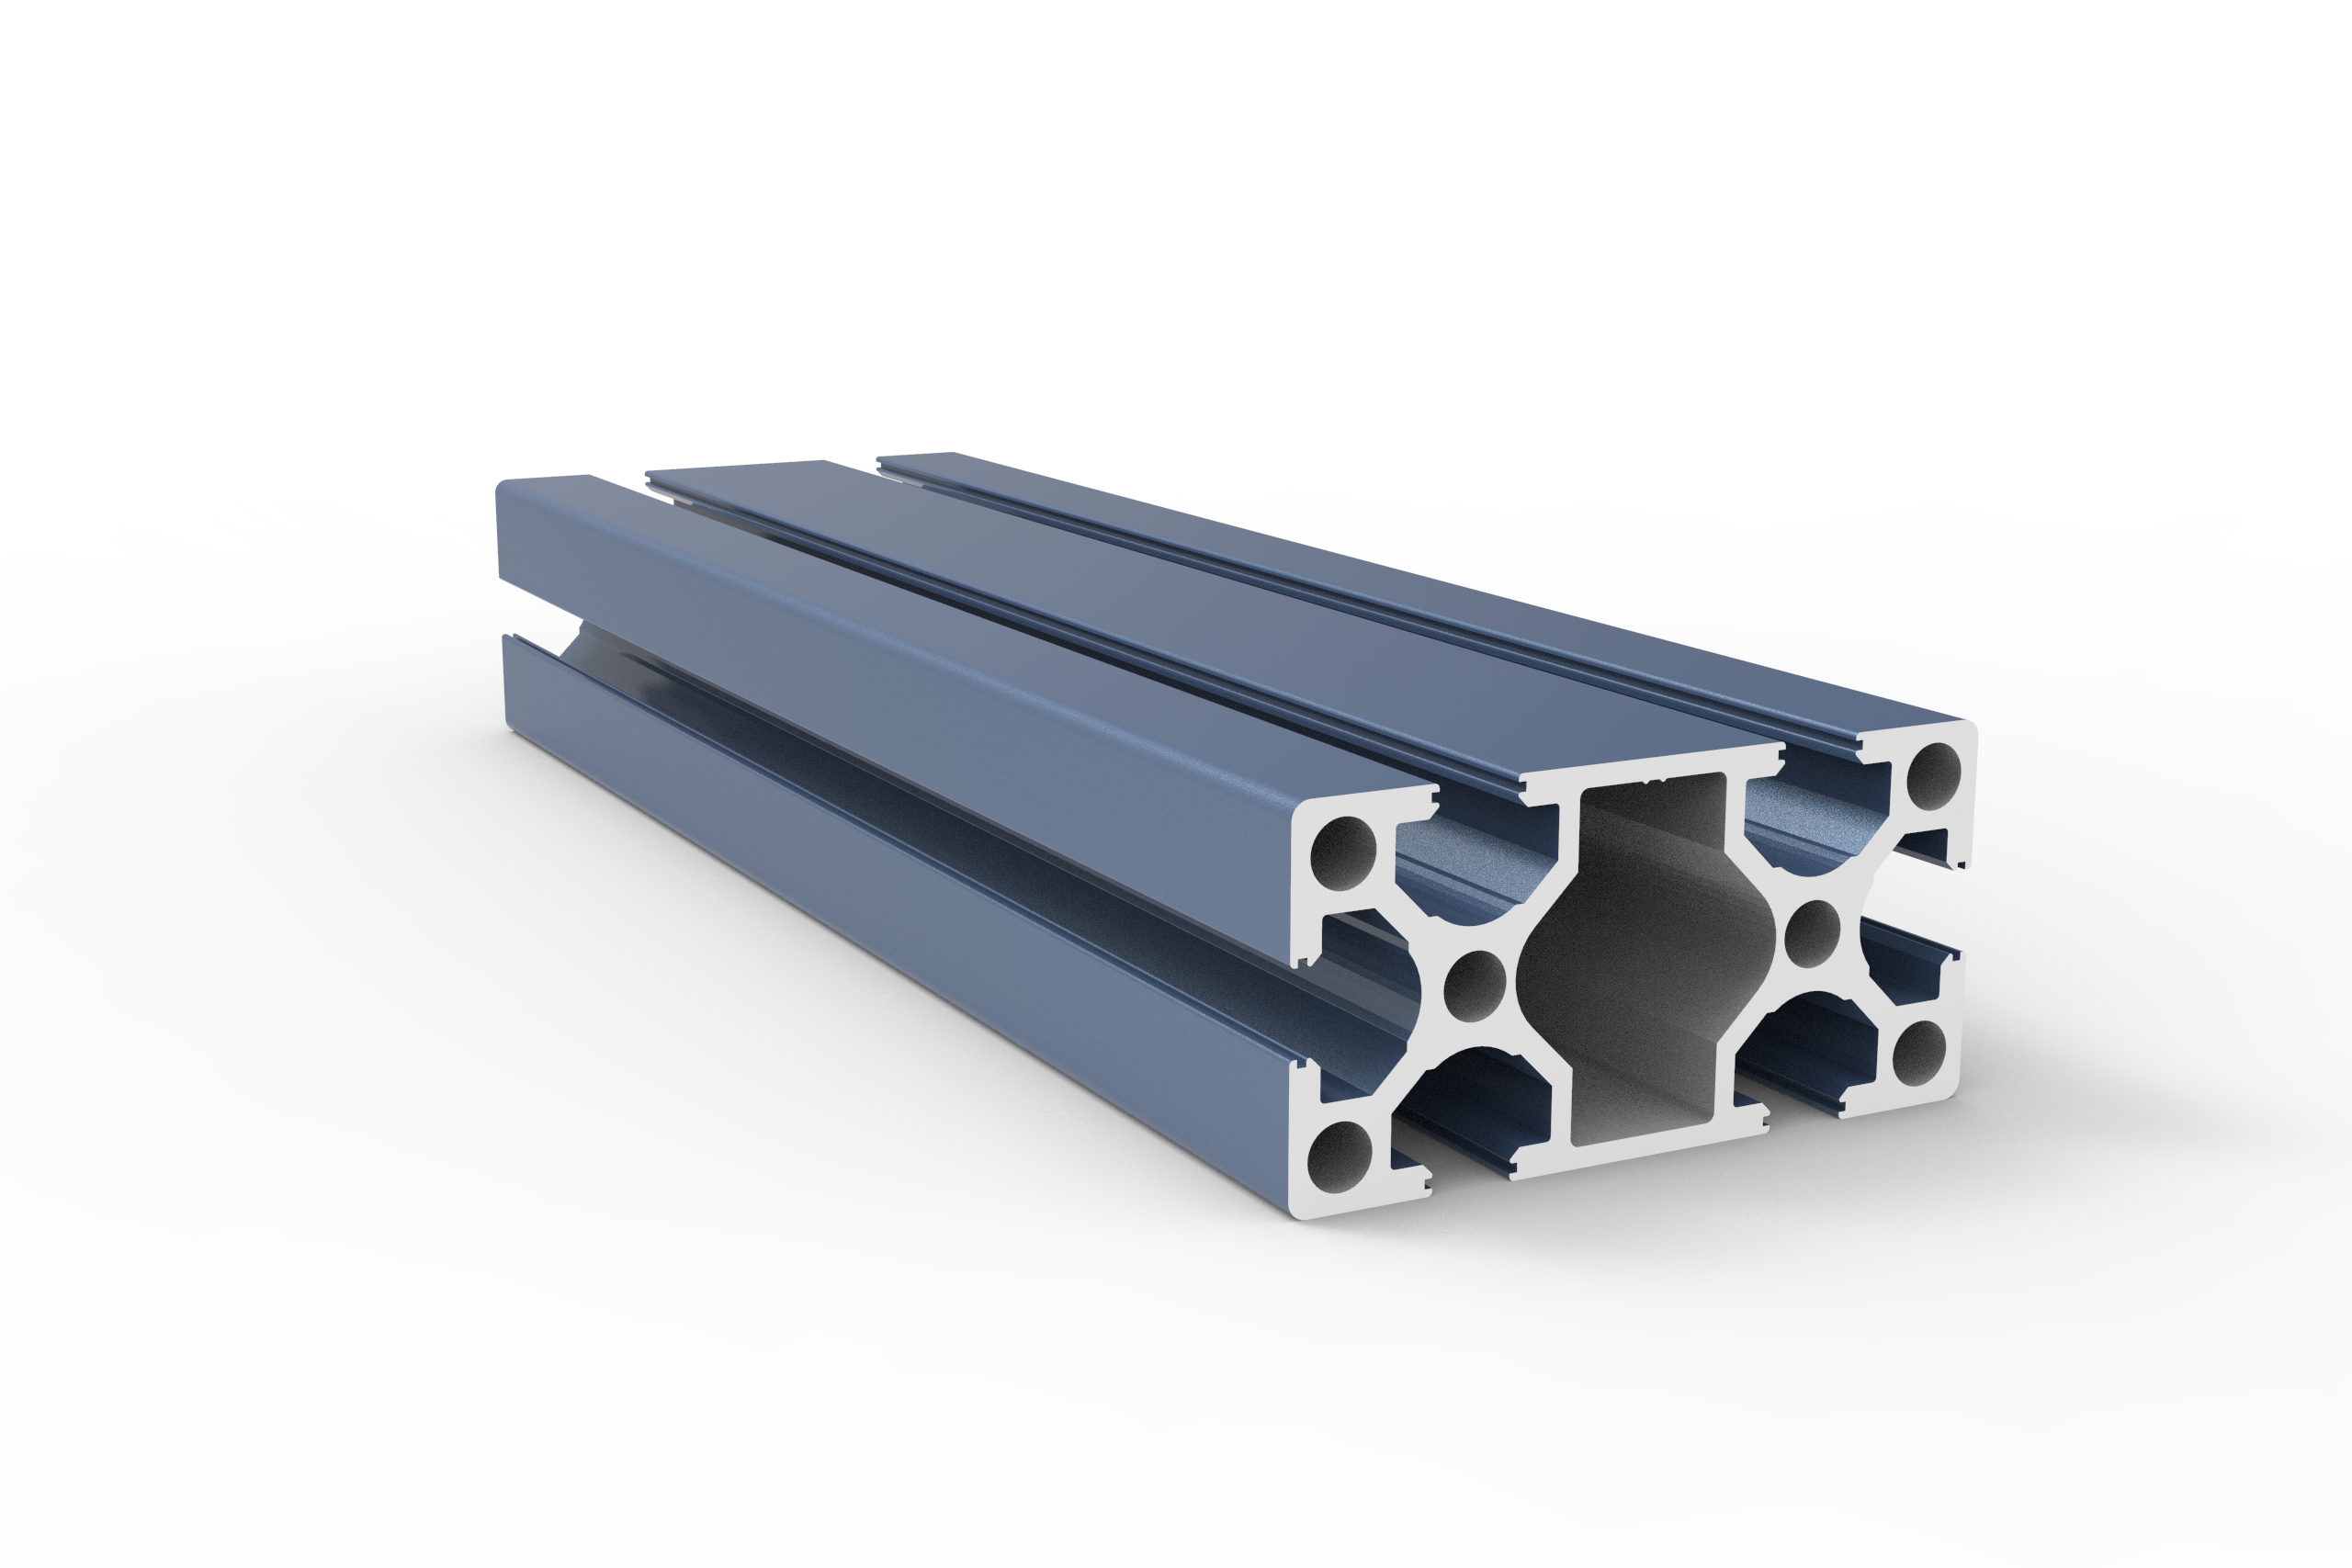
What T-slot industrial profile size is best for a heavy duty machine frame?
How do I choose the right stainless steel decorative profile for high humidity areas?
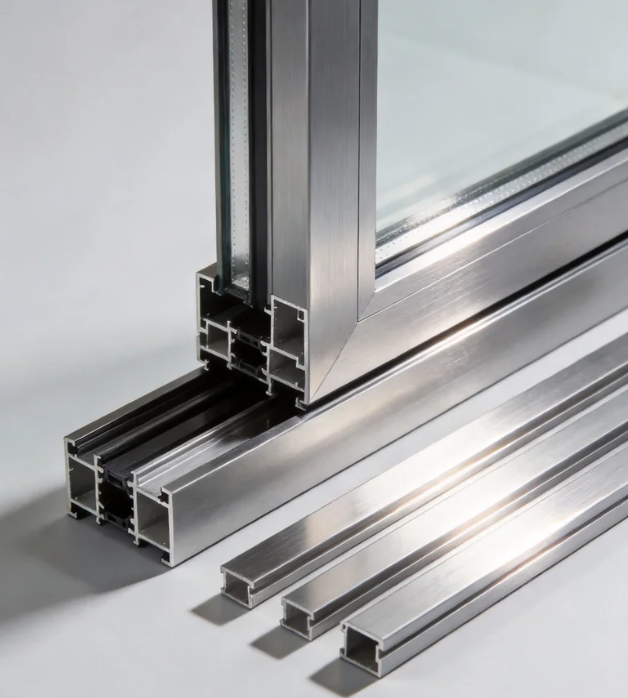
How do I choose the right aluminum architecture profile for coastal buildings?
How do I choose the right stainless steel decorative profile for high humidity areas?
What wind load specs should I check for aluminum casement windows in coastal high-rises?
How do I know which aluminum industrial profile alloy is best for heavy machinery frames?
How do I choose the right alloy grade for aluminum architecture profiles?
How do I select the right heavy-duty hardware for exterior commercial floding doors?
How do I select the right glass thickness for bulk awing window orders?
What frame thickness is recommended for commercial aluminum casement doors?
What frame thickness is best for high-rise commercial sliding windows?
How to choose weather resistant aluminum floding door specs for commercial use?
How do I choose the best water tightness rating for commercial awing windows?
How do I choose the right frame material for commercial casement doors?
How do I choose the right wind load rating for sliding windows in coastal areas?
What is the best material for outdoor decorative profiles to prevent rust and fading?
How do I choose the right track thickness for high-traffic commercial sliding doors?
How do I choose between PVC and basswood shutters for high-humidity areas?
How do I choose between double and triple glazing for casement windows in cold climates?
How do I choose the right industrial profile thickness for heavy-duty cnc machine frames?
How do I choose the right alloy for outdoor architecture profiles to prevent corrosion?
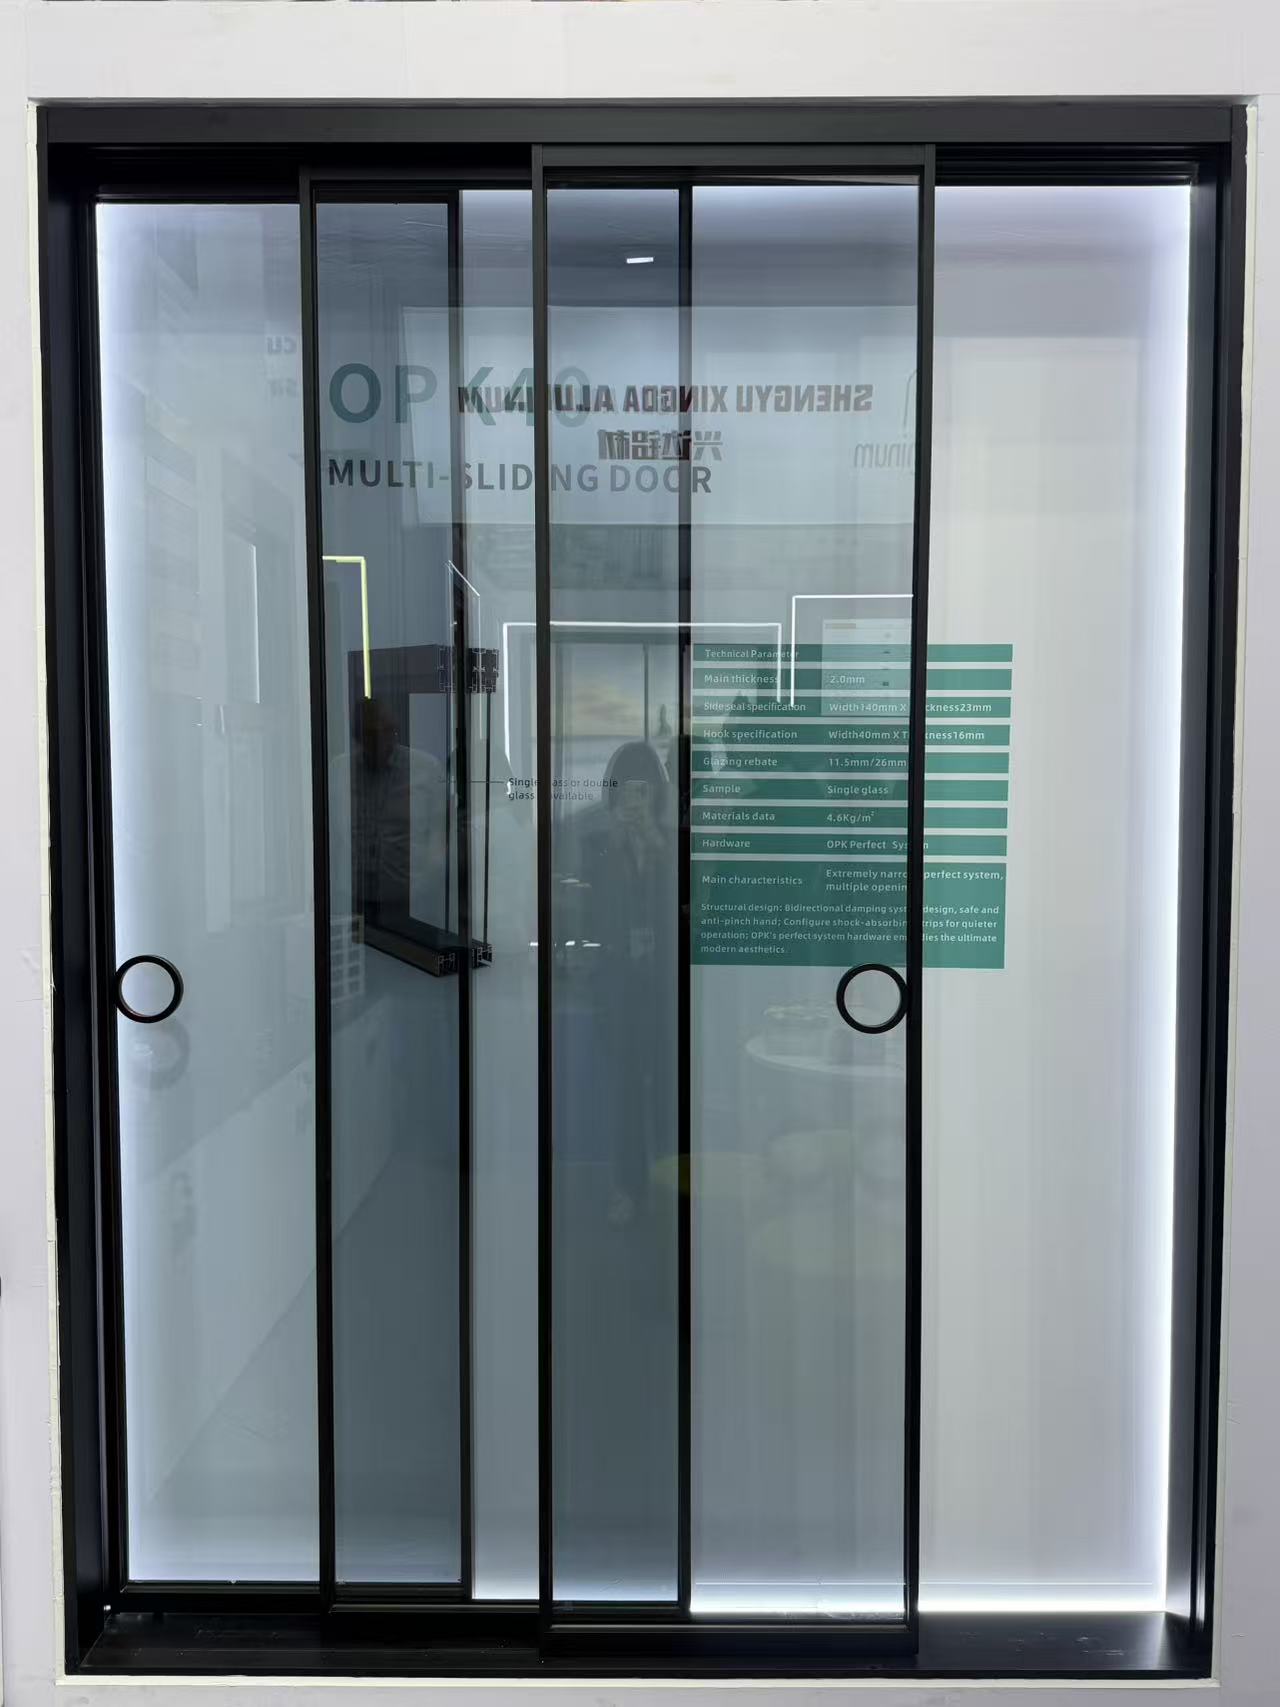
Can you design a slim frame profile for modern minimalist look?
How do I choose the right wind-resistant floding door for a coastal commercial building?
What key specs ensure a casement window can withstand heavy rain and high winds?
How do I choose the right aluminum alloy grade for heavy-duty industrial profiles?
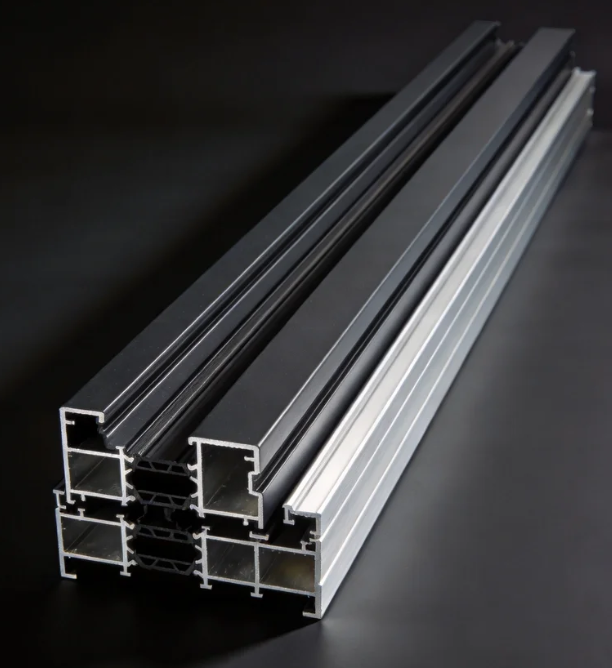
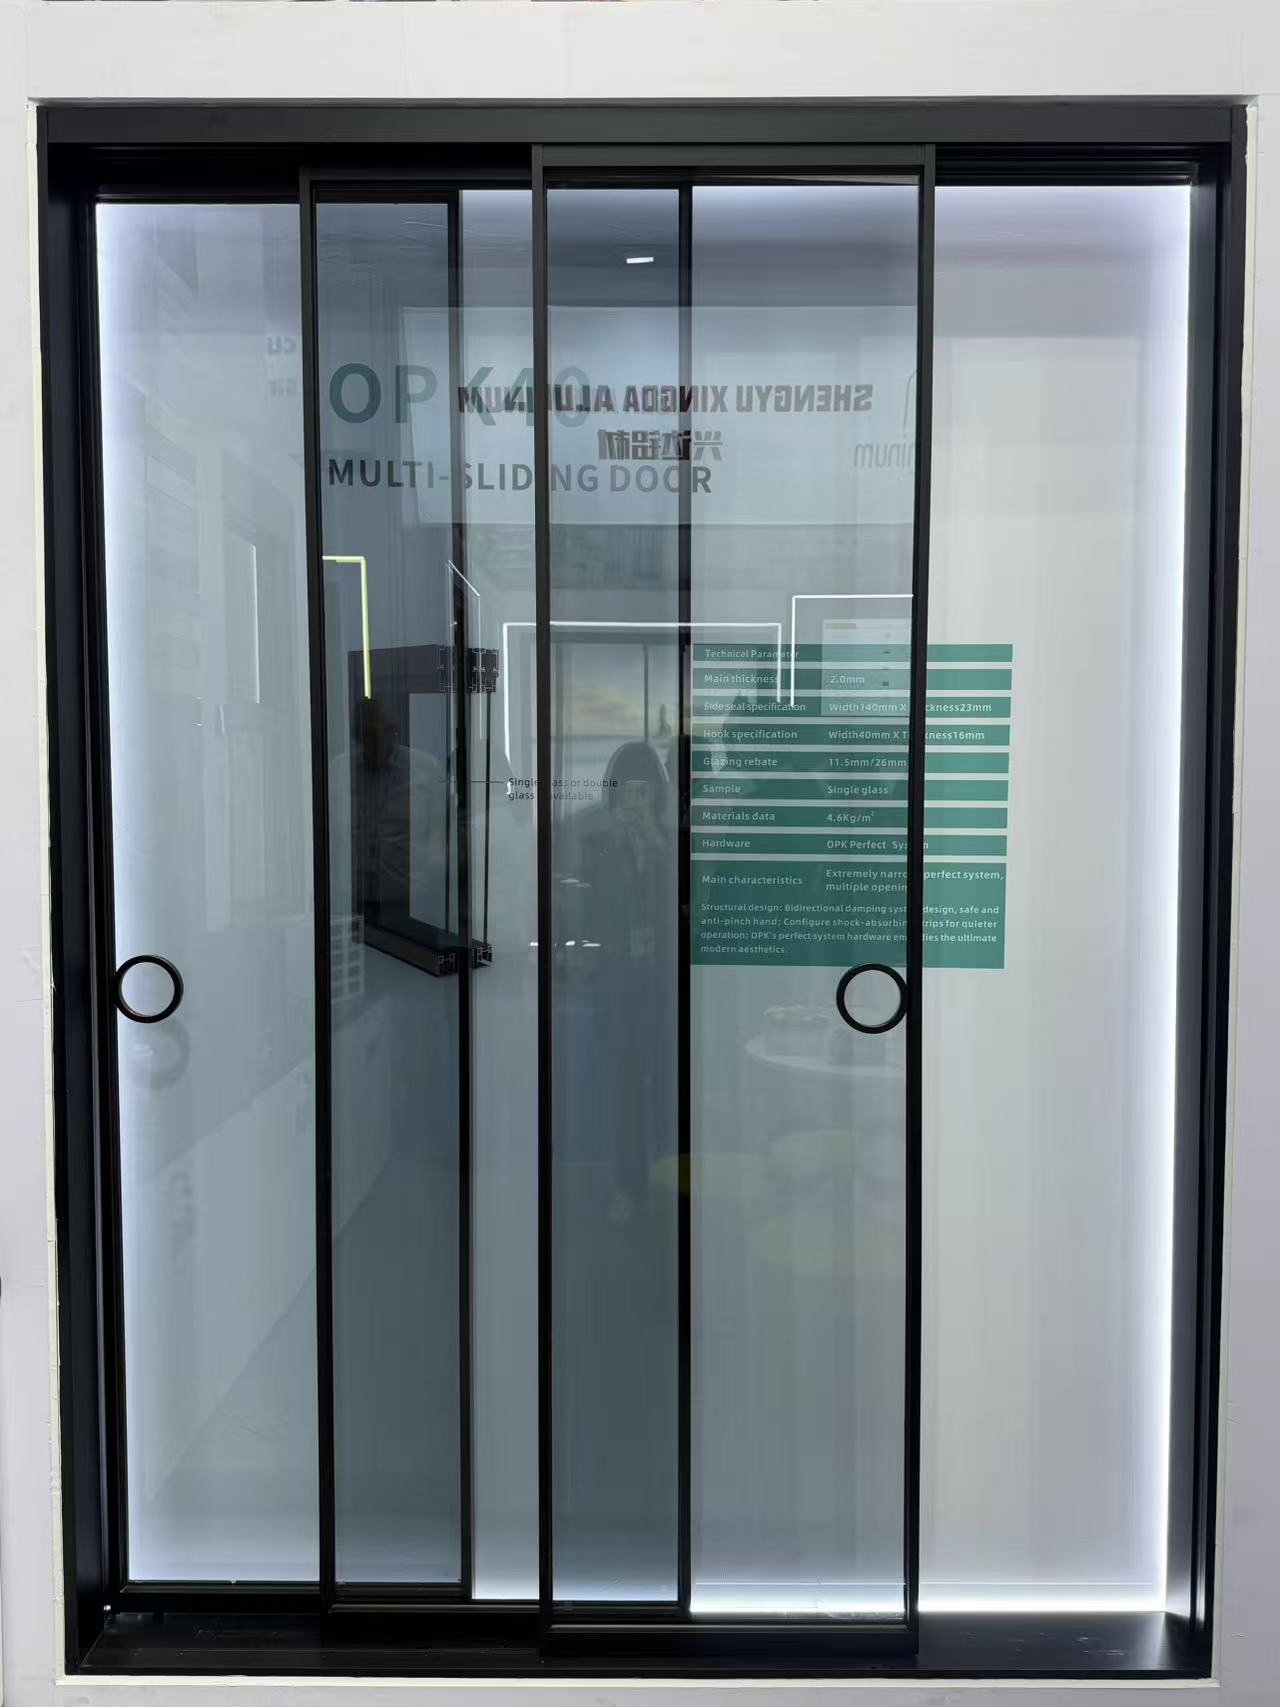
Which alloy grade of architecture profile is best for coastal areas to resist rust?
How do you pack windows to prevent glass breakage in transit?
Are slim-frame thermal break systems replacing traditional ones?
Does the price include the matching frame and installation kit?
How do you protect our proprietary design drawings from leaks?
How do I choose the right decorative profile for high-traffic hotel lobbies?
Is your factory the actual manufacturer or a trading partner?
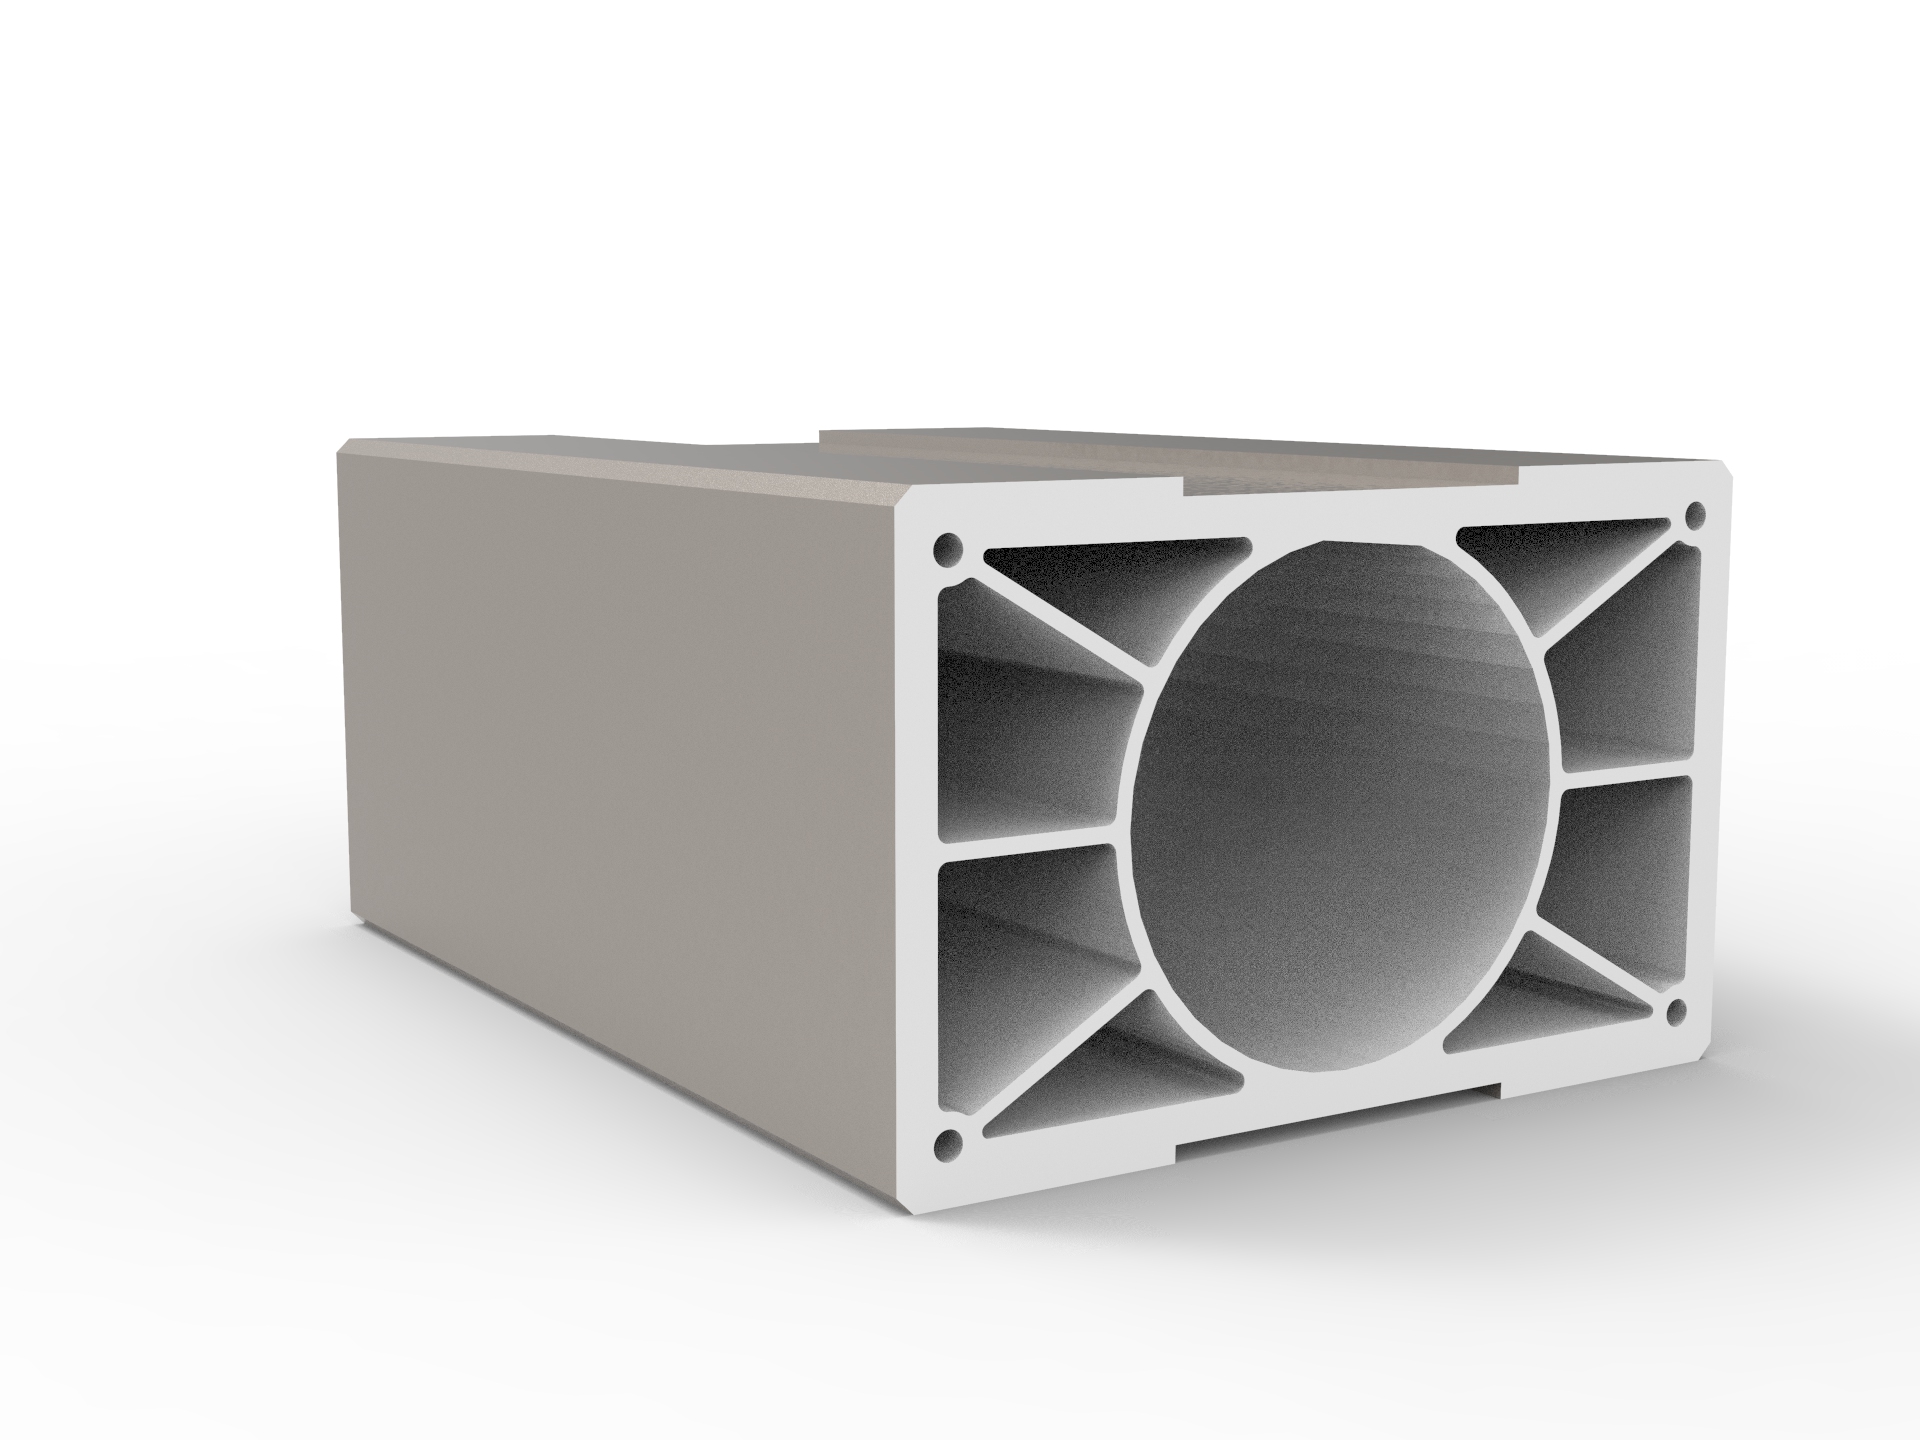
Is it possible to 3D print a prototype before cutting steel?
Do you outsource any part of the painting process to others?
How do you handle replacement parts for damaged track rollers?
Do you accept escrow payments through third-party platforms?
Do you have ISO 9001 certification for your production line?
Are there extra fees if we pay via bank telegraphic transfer?
What is the price difference between powder coat and anodized?
What is the warranty period for the lock and hinge hardware?
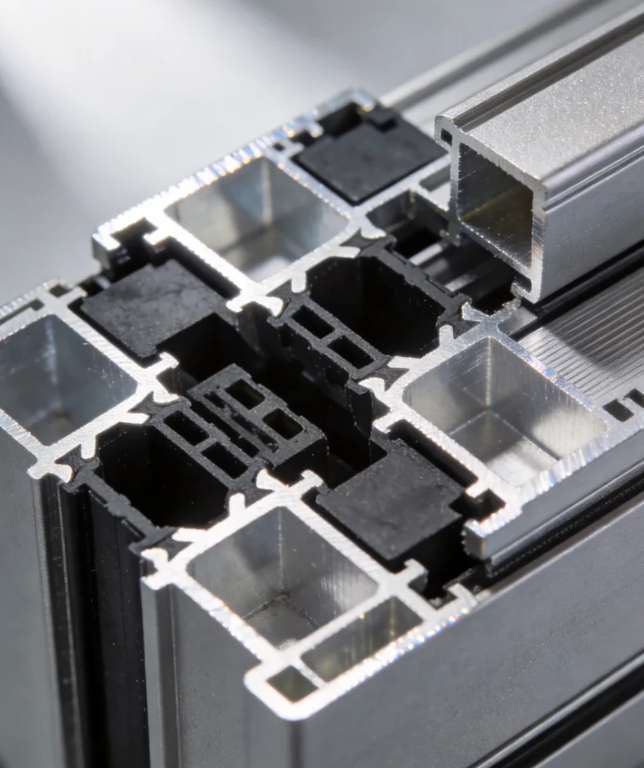
What is your policy for dimensional deviations in the batch?
What happens if the shipment is delayed due to factory error?
Do you offer online technical support if color fading occurs?
Is it possible to engrave our brand logo on the tension screw?
Do you offer credit terms for long-term purchasing partners?
Can you palletize the shipments for easy forklift unloading?
What are the latest eco-friendly finish trends for decorative profiles in modern interior design?
What are the tooling cost and design limitations for customizing heavy-duty industrial profiles?
Has your architecture profile manufacturing facility passed ISO 9001 certification?
Can we use Alibaba Trade Assurance for our initial sliding door order to mitigate risk?
Do you provide free corner samples of the casement window frame for color verification?
Is it possible to custom-match a specific RAL color for a decorative profile order?
Can I request a 3D-printed sample before ordering a custom industrial profile mold?
Can you extrude an architecture profile based on our proprietary CAD drawings?
What thermal performance certifications does a sliding door need for the UK market?
How are heavy floding door panels crated to ensure safe unloading at the job site?
Can we arrange our own freight forwarder to pick up the casement door shipment FOB?
What is the estimated ocean freight transit time for a shutter shipment from China to Europe?
How can we source replacement seals for your awing window models in the future?
How are sliding windows typically packaged to prevent glass breakage during ocean transit?
What is the average lead time for a 40ft container of standard aluminum casement windows?
Are there any extra tooling fees if my decorative profile order doesn’t meet the MOQ?
Can I get 3D printed prototypes of custom architecture profiles before committing to mold tooling?
How is smart glass technology being integrated into modern residential sliding door units?
What options do you have for customizing the threshold height of an aluminum floding door?
What thermal break technology should I look for in a heavy-duty aluminum casement door?
What quality control processes do you perform on shutter hardware before final assembly?
Do you offer DDP shipping terms for awing window orders delivered to our warehouse?
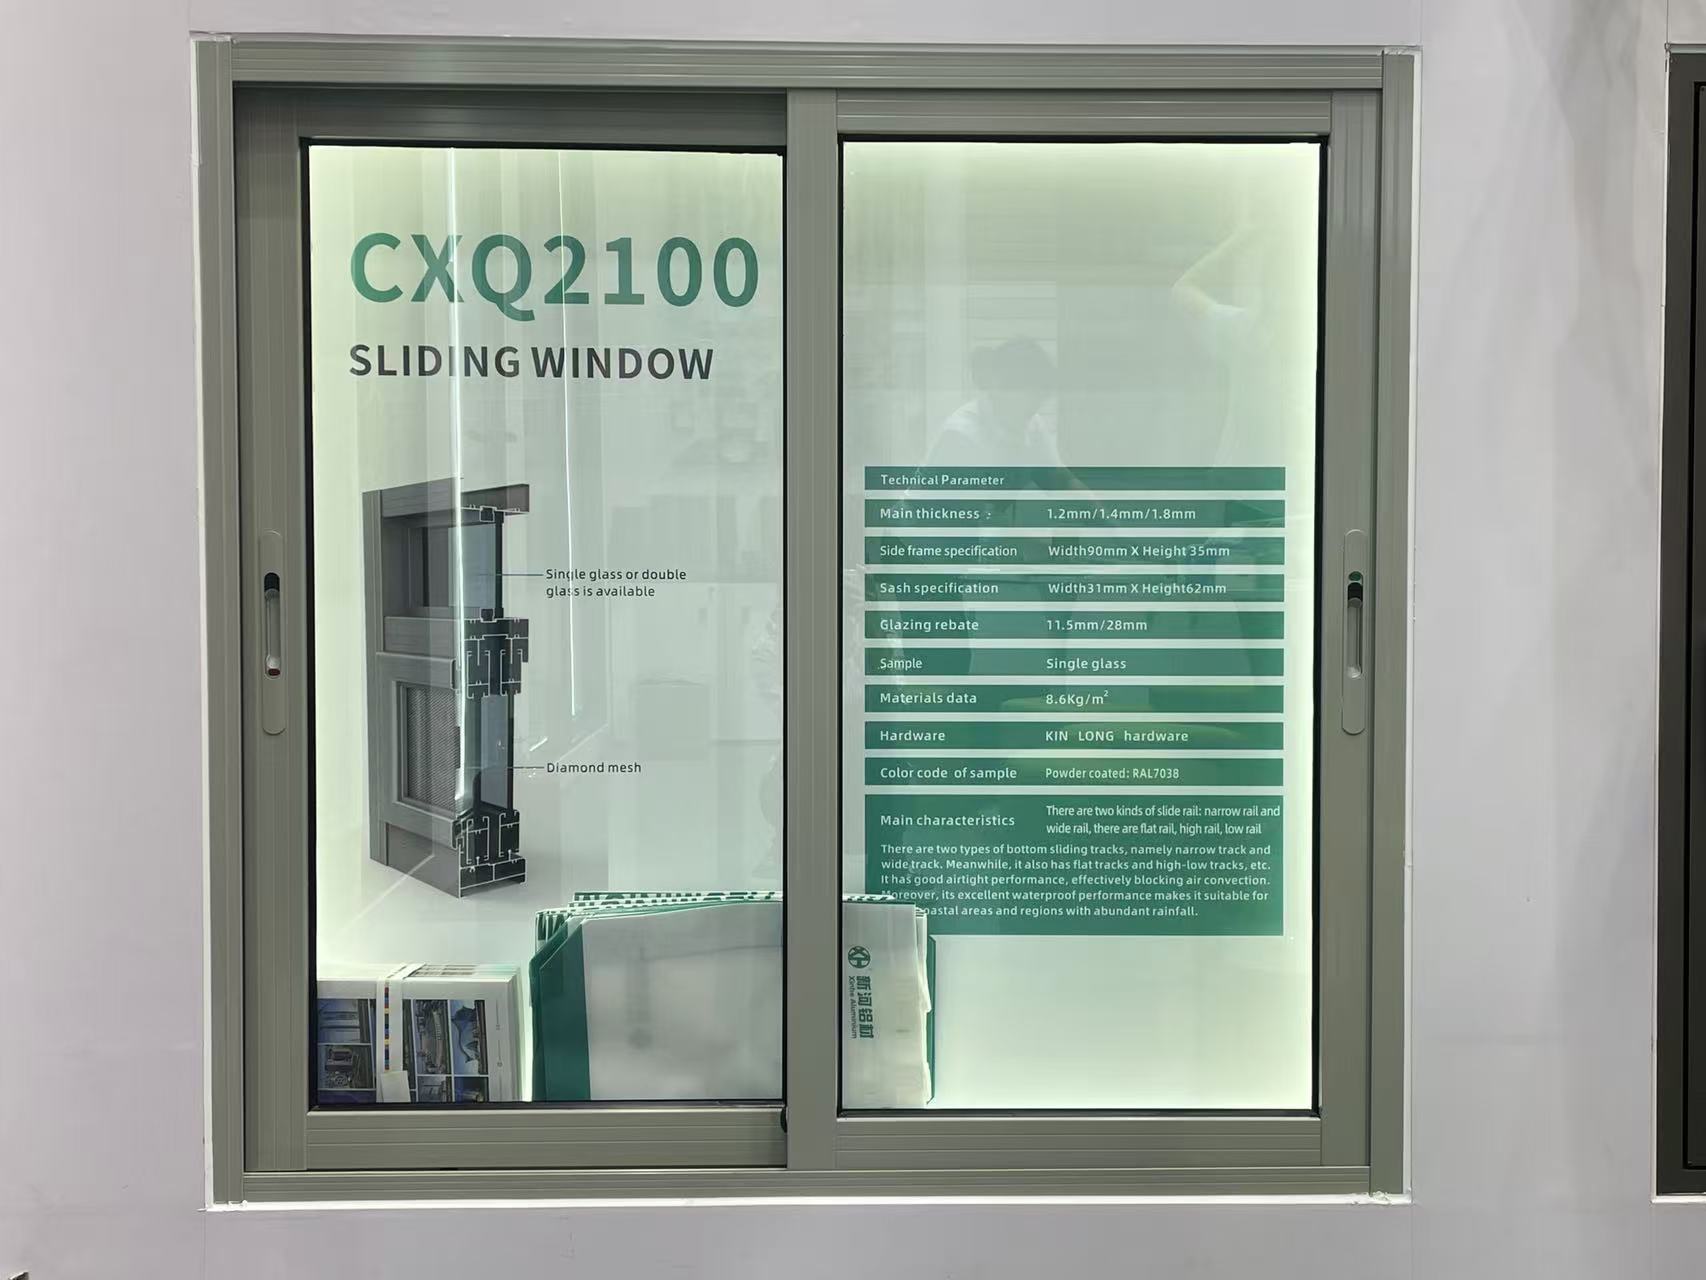
Is it possible to order a fully functional sliding window sample for mock-up testing?
Do you provide replacement hardware if the casement window hinges fail within 5 years?
How do you handle claims for decorative profile items damaged during transit?
What is the standard MOQ for custom-extruded aluminum industrial profile orders?
How does the order volume affect the per-ton price of custom architecture profile designs?
What is the warranty period for the rollers and tracks on your heavy-duty sliding doors?
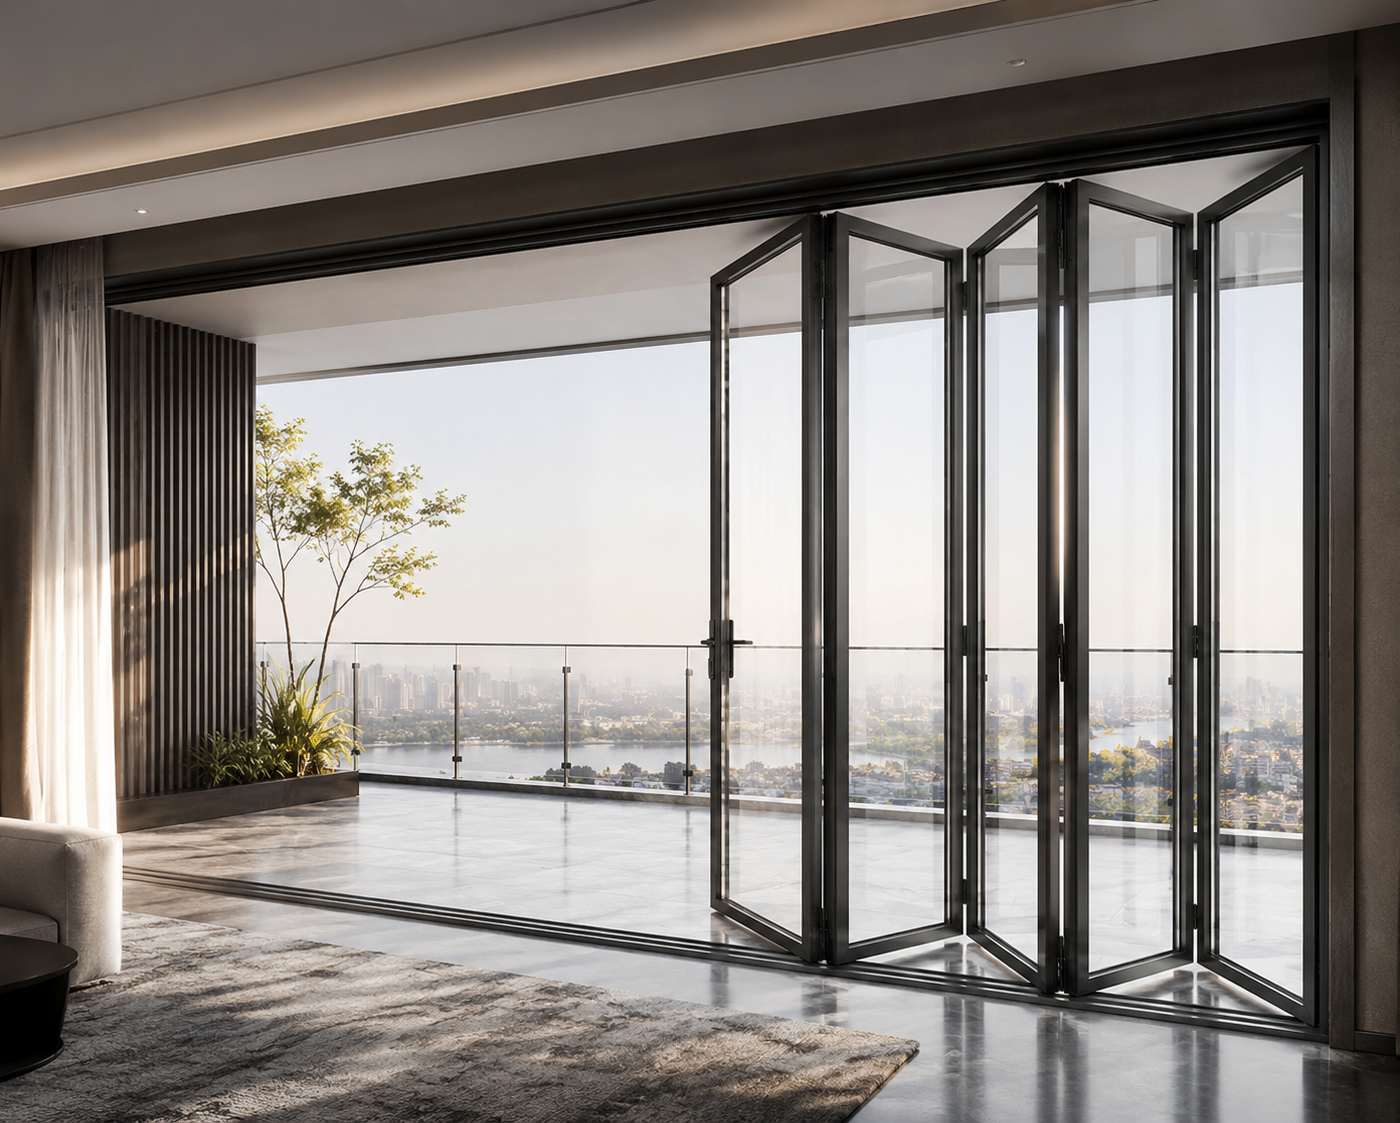
How can we secure our deposit when purchasing high-value custom floding doors from a new supplier?
Can your factory match custom anodized colors for decorative profiles based on physical samples?
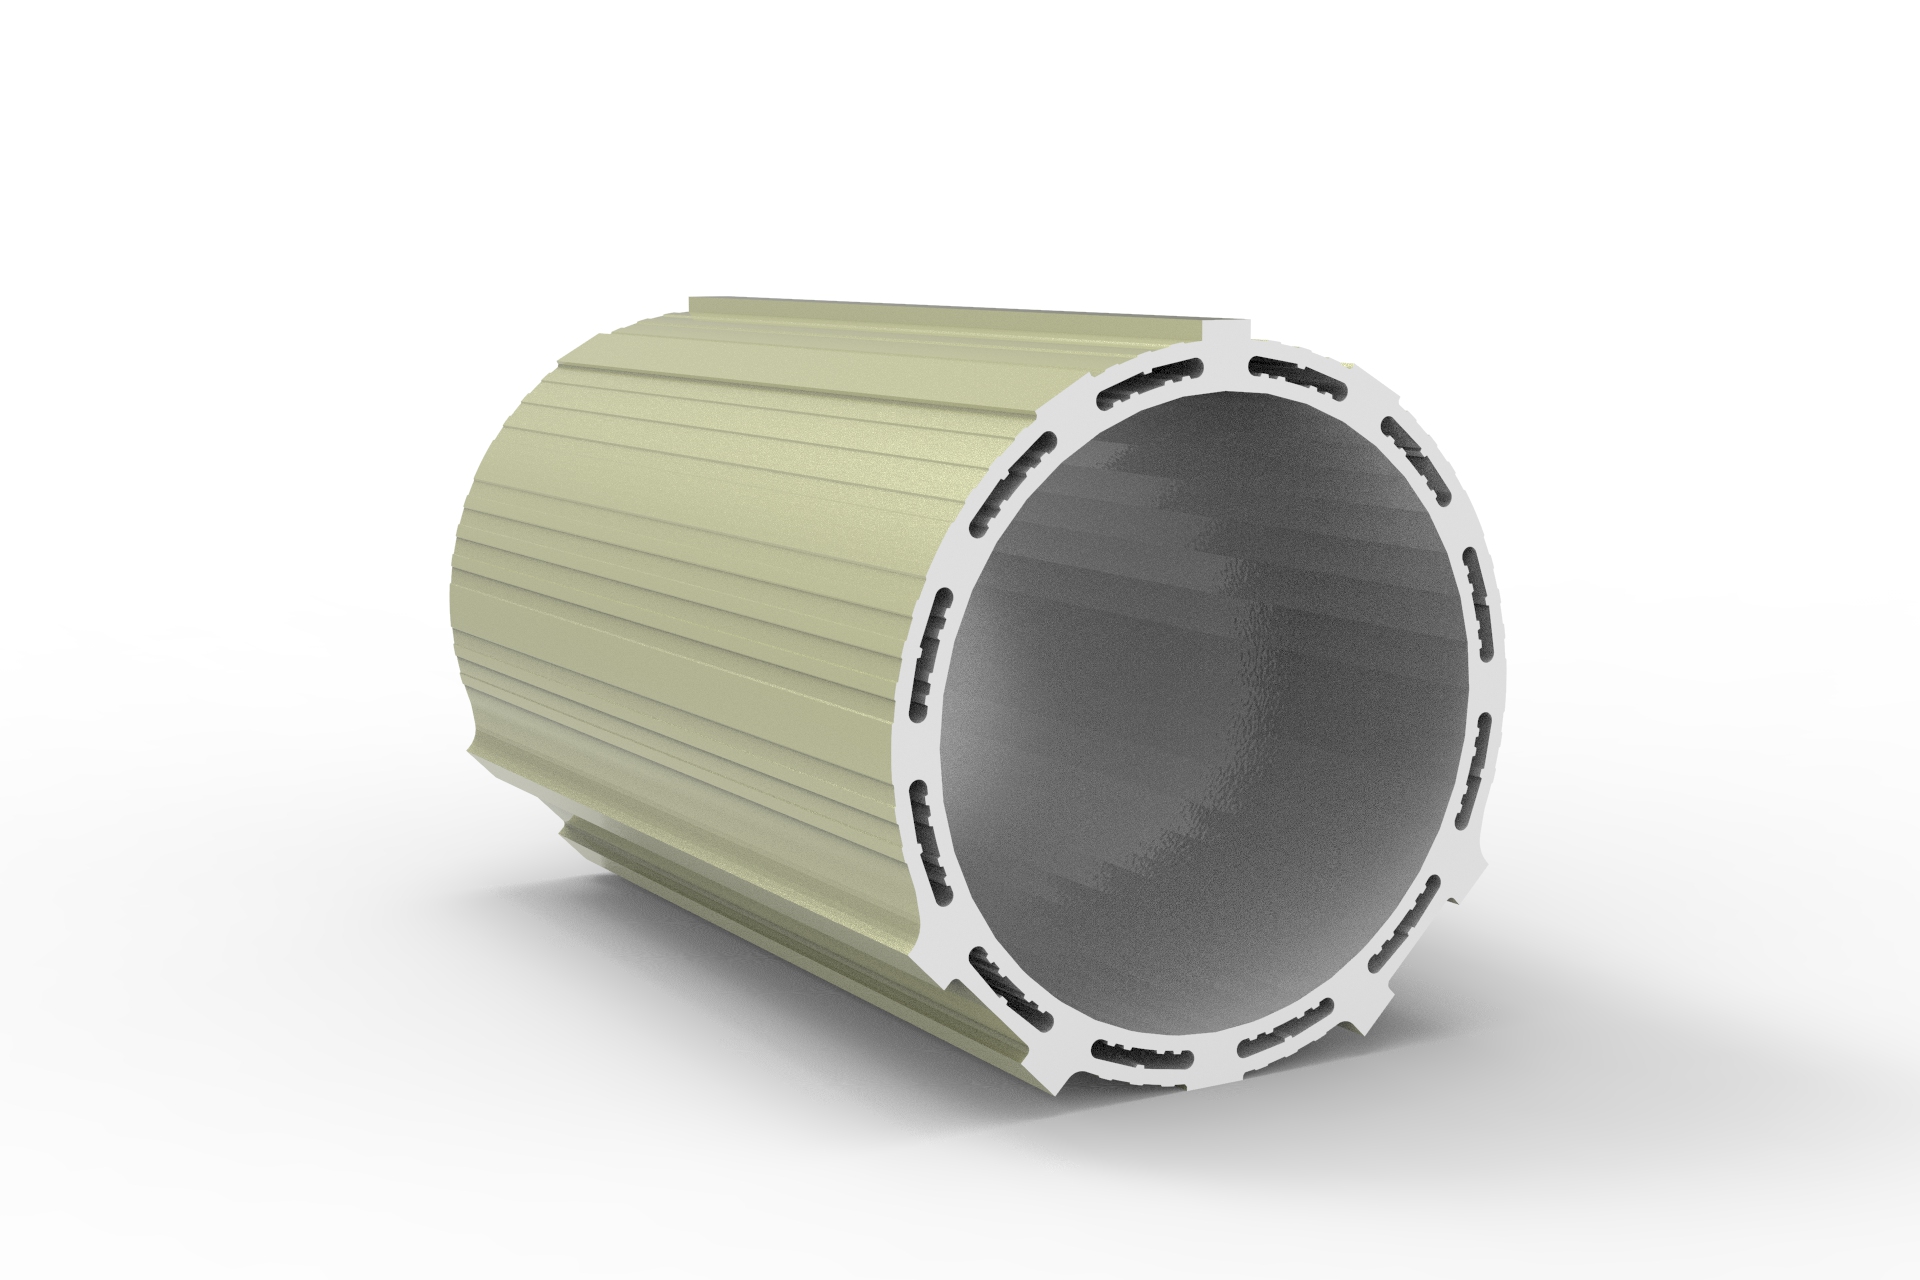
Is there a lighter alternative to aluminum industrial profile structures for robotics?
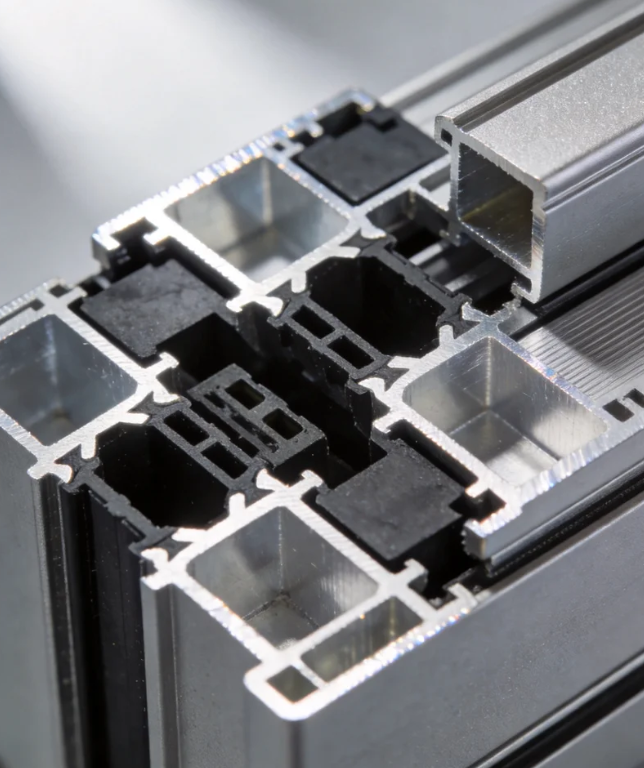
What payment security measures do you have for custom architecture profile tooling fees?
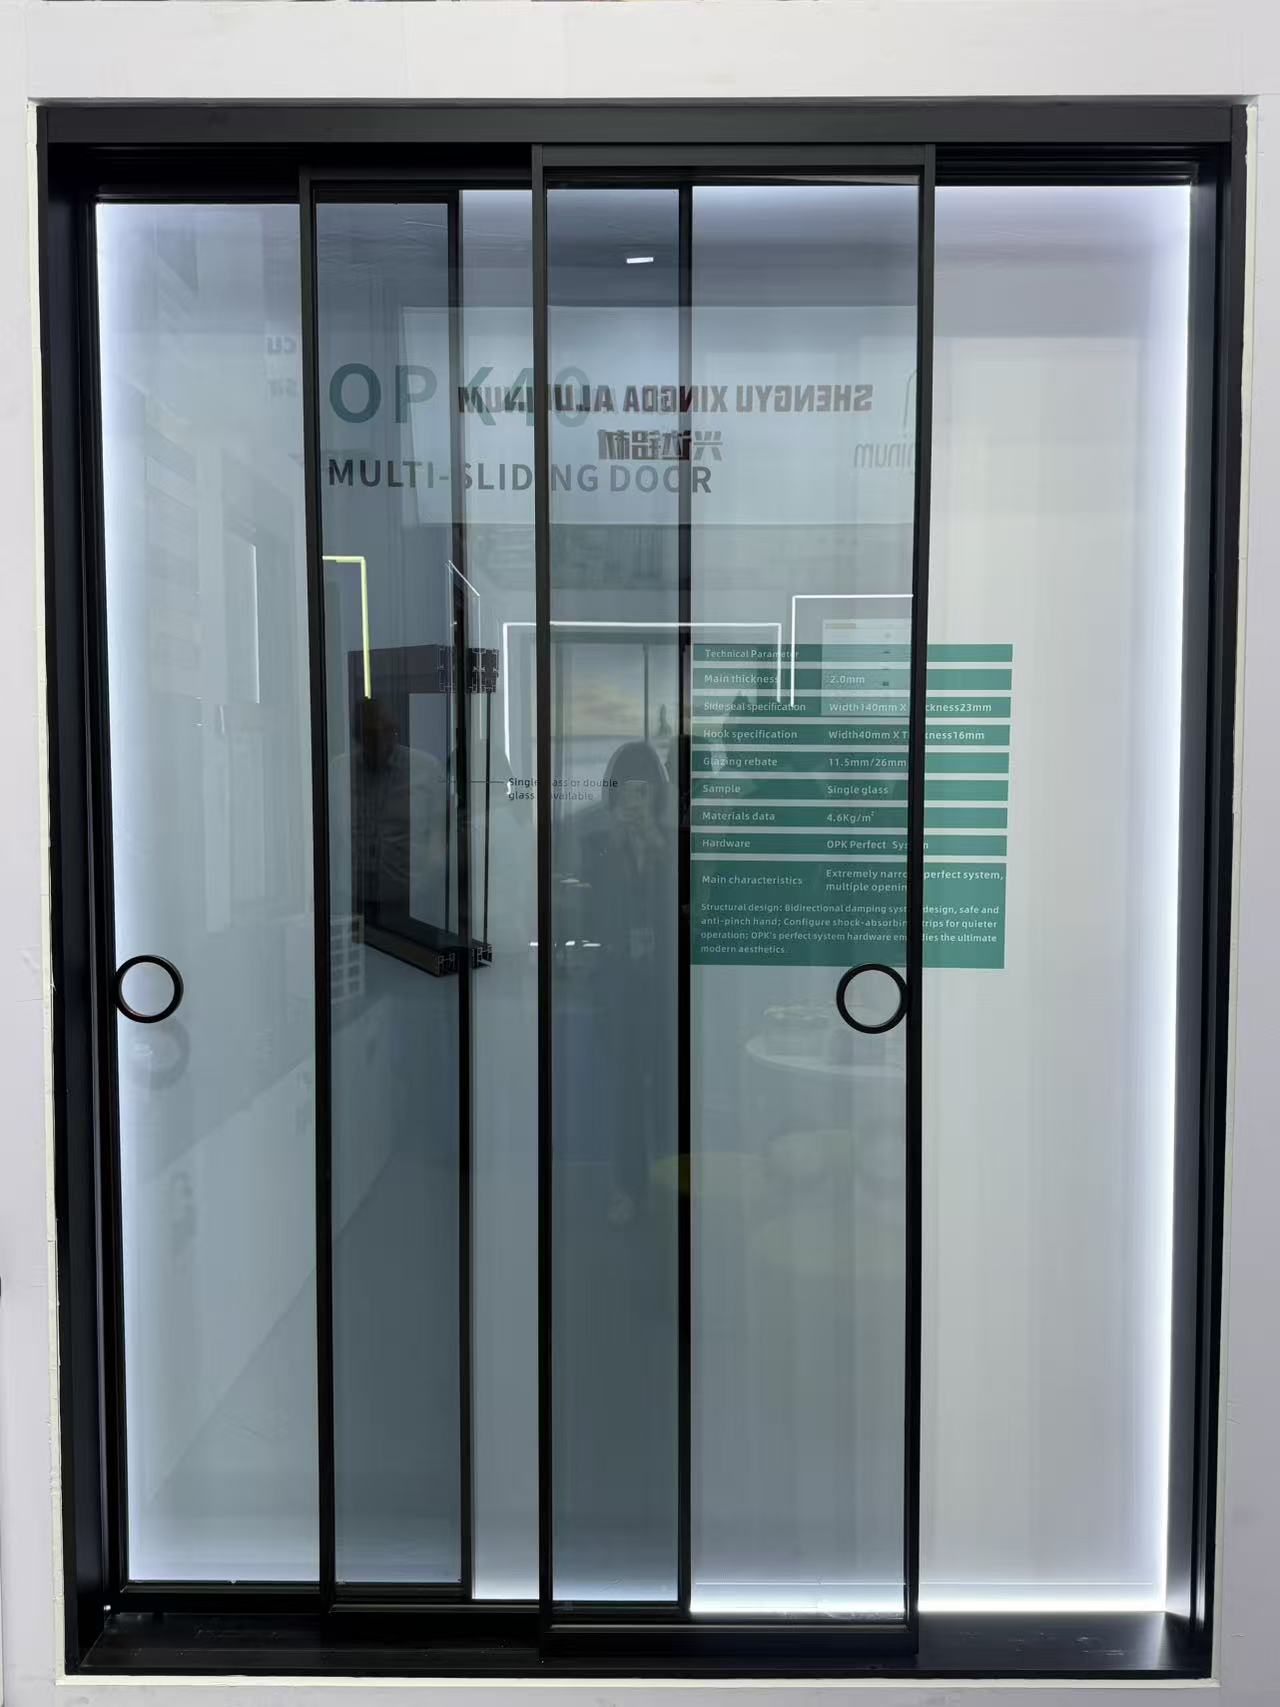
Can I order a sliding door with custom grid patterns between the glass panes?
How do you protect buyers against financial loss if the floding door shipment is delayed?
Are slim-frame aluminum casement door designs becoming more popular in modern offices?
What is your policy for replacing shutter components that arrive with color mismatch?
What kind of remote technical support do you offer for sliding window installation?
What is the maximum safe size for a top-hung awing window in commercial projects?
What environmental management standards does your decorative profile plant follow?
What is the standard lead time for producing a 40ft container of casement window orders?
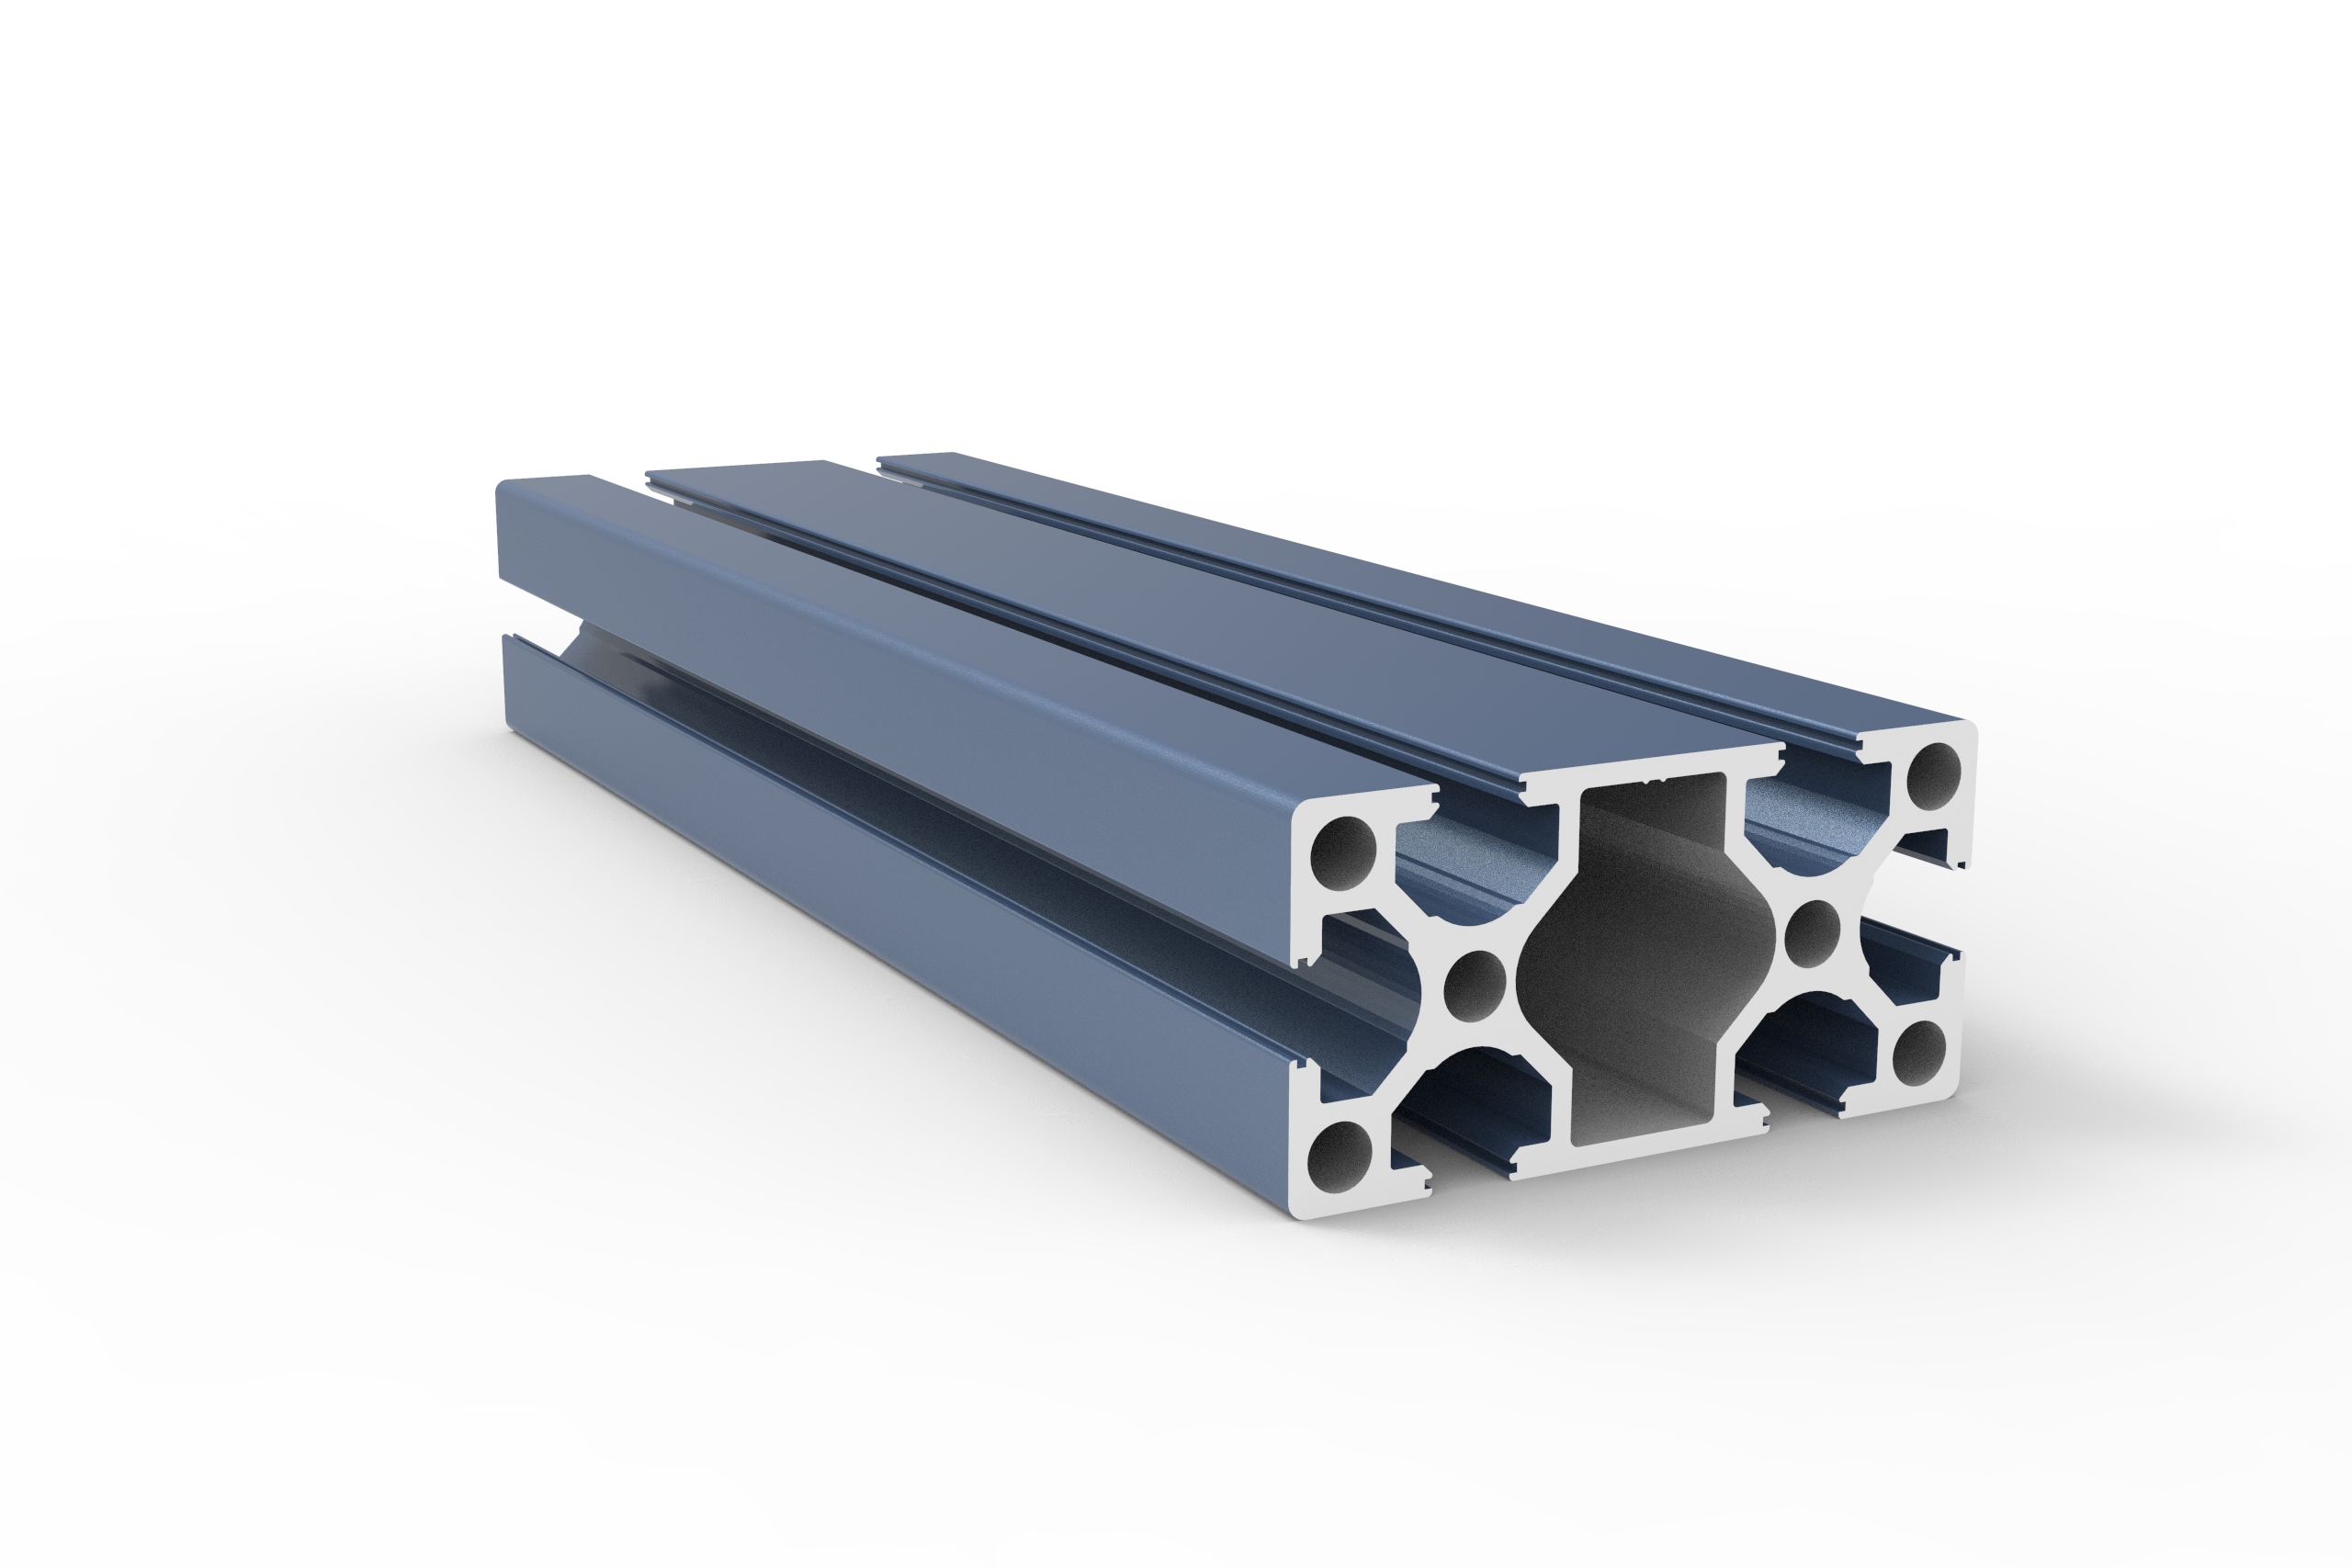
What is the warranty period for the anodized finish on your industrial profile?
What are the latest eco-friendly trends in architecture profile manufacturing?
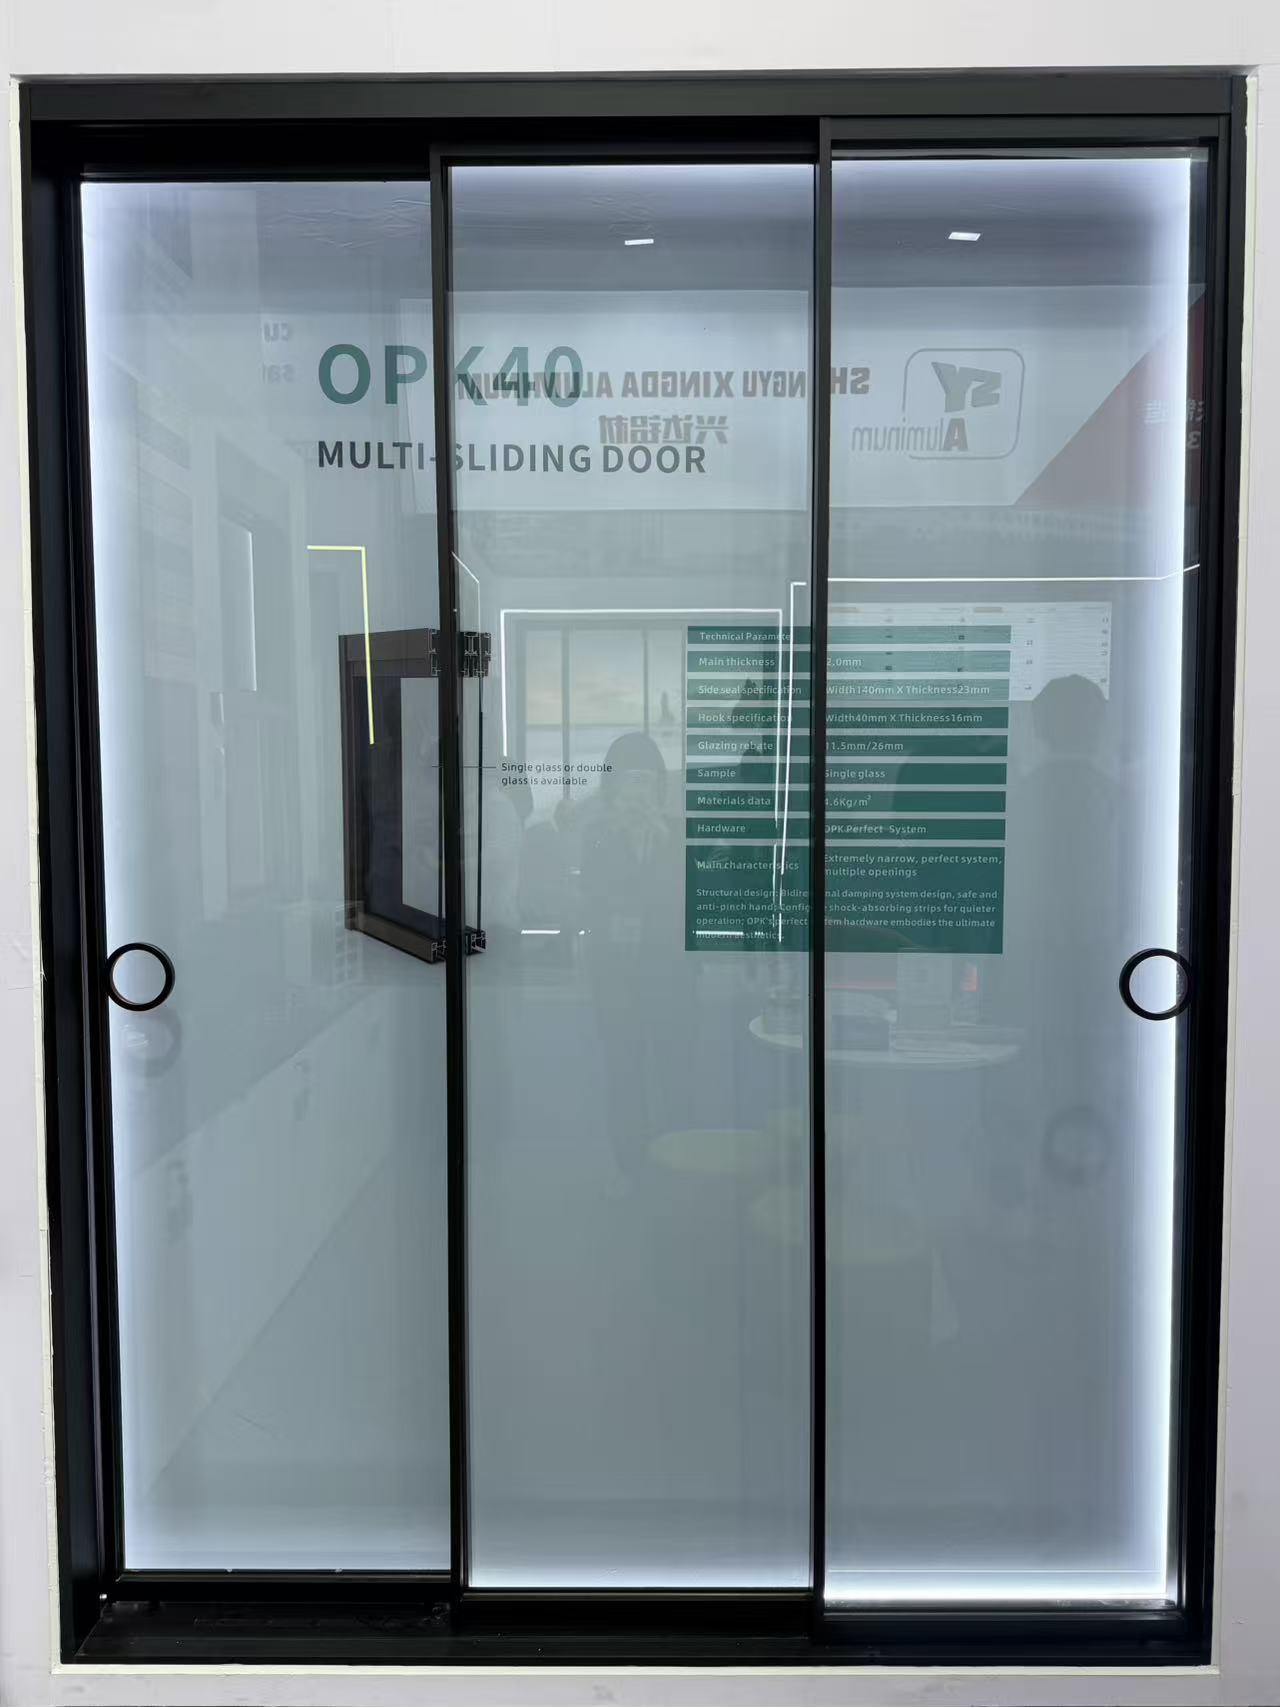
What is the average wholesale price per square meter for double-glazed sliding door systems?
How do I calculate the structural load requirement for a 5-panel exterior floding door?
Do your exterior shutter systems comply with Florida building codes for hurricane protection?
Do you offer Letter of Credit (L/C) payment options for casement door bulk orders?
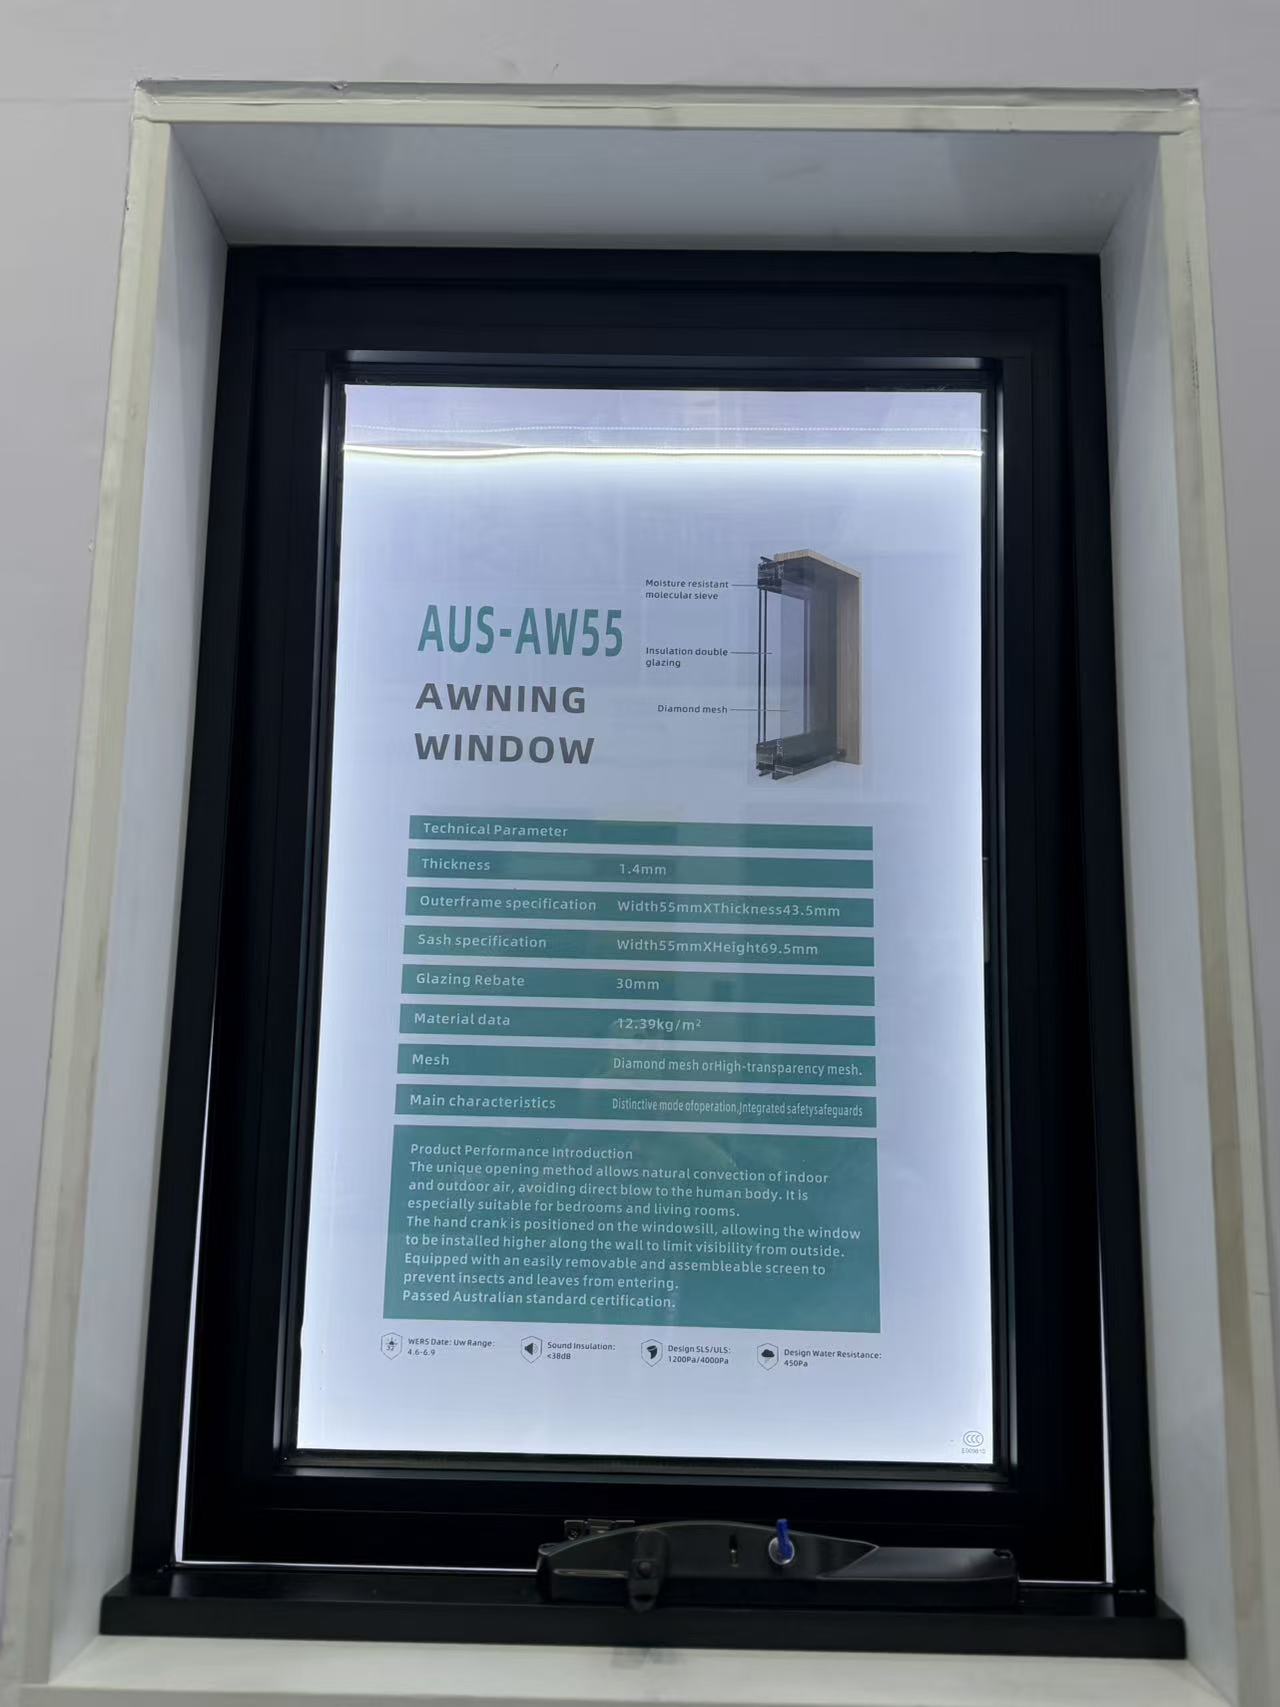
Which water tightness certifications are required for importing an awing window to Europe?
Do you allow virtual factory tours to inspect the sliding window assembly line?
What is the typical MOQ for ordering standard-sized aluminum casement window units?
How long does it take to receive a physical sample of a gold-anodized decorative profile?
How do I choose the right alloy grade for architecture profiles in high-rise coastal buildings?
How do I choose the right track and roller specs for heavy-duty commercial sliding doors?
The core advantages of using aluminium profiles for the canopy
International demand: Dual drive by new energy and infrastructure
The advantages of using aluminium profiles to manufacture robot arms
The advantages of using aluminum profiles for door and window frames
The impact of the conflict between the United States and Iran on the price of aluminum
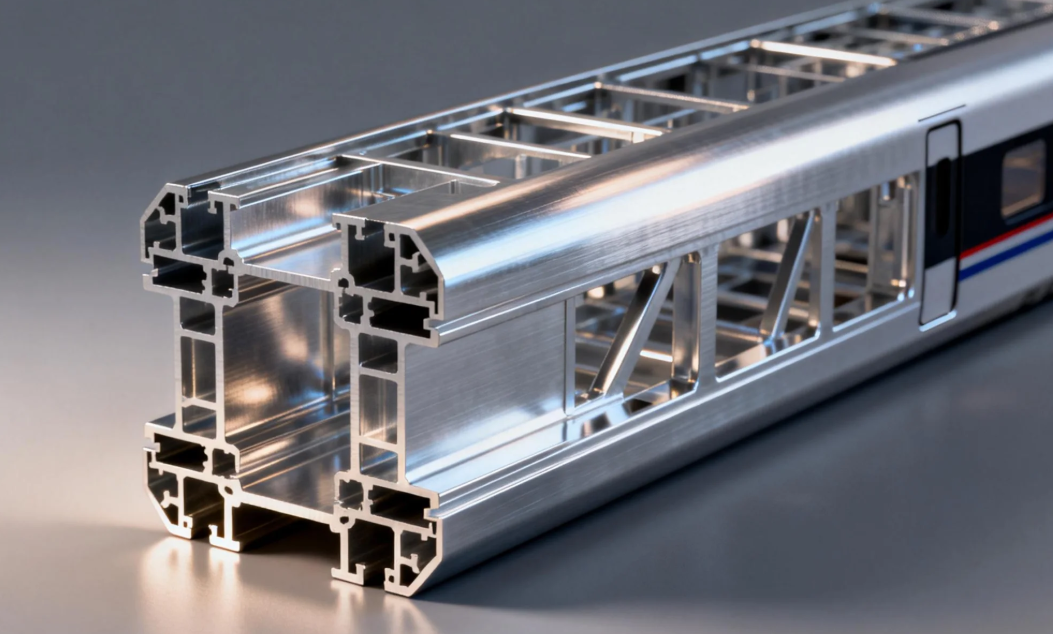
The advantages of using aluminium alloy for the main structure of high-speed train carriages
Methods for distinguishing Indoor and Outdoor Aluminium Doors
Maintenance methods and tips for aluminium doors and windows
Characteristic of outward-opening and hung aluminium windows
Xinhe Aluminium Research: 7.14-7.18 Analysis of Aluminium Prices
Seven Benefits Of Using Aluminium Profiles In Curtain Wall Systems
The Application of Aluminium Profiles in New Energy Vehicles
The Composition and Application of Series 6 Aluminium Alloys
Top 5 Benefits of Using LED Aluminium Profiles in Modern Lighting
A Complete Guide to Aluminium Frame Profiles for Modern Structures
Exploring the Strength and Versatility of Aluminium Extrusion Profiles
How to Choose the Right Aluminium Profile Supplier for Your Project
COMPANY